EP1135264B1 - Verfahren zum partiellen beschichten einer platte - Google Patents
Verfahren zum partiellen beschichten einer platte Download PDFInfo
- Publication number
- EP1135264B1 EP1135264B1 EP99958155A EP99958155A EP1135264B1 EP 1135264 B1 EP1135264 B1 EP 1135264B1 EP 99958155 A EP99958155 A EP 99958155A EP 99958155 A EP99958155 A EP 99958155A EP 1135264 B1 EP1135264 B1 EP 1135264B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- masking layer
- plate
- transfer foil
- layer
- applying
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 22
- 238000000576 coating method Methods 0.000 title claims abstract description 9
- 239000011248 coating agent Substances 0.000 title claims abstract description 8
- 230000000873 masking effect Effects 0.000 claims abstract description 66
- 239000011888 foil Substances 0.000 claims abstract description 22
- 239000012530 fluid Substances 0.000 claims abstract description 9
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 11
- 238000005520 cutting process Methods 0.000 claims description 6
- 239000002184 metal Substances 0.000 claims description 5
- 229910052751 metal Inorganic materials 0.000 claims description 5
- 239000000463 material Substances 0.000 claims description 3
- 229920003023 plastic Polymers 0.000 claims description 2
- 230000005855 radiation Effects 0.000 claims description 2
- 239000010410 layer Substances 0.000 description 63
- 239000010408 film Substances 0.000 description 48
- PCHJSUWPFVWCPO-UHFFFAOYSA-N gold Chemical compound [Au] PCHJSUWPFVWCPO-UHFFFAOYSA-N 0.000 description 11
- 239000012790 adhesive layer Substances 0.000 description 7
- 239000007788 liquid Substances 0.000 description 5
- 239000002245 particle Substances 0.000 description 3
- 230000035515 penetration Effects 0.000 description 3
- 238000003825 pressing Methods 0.000 description 3
- 238000007639 printing Methods 0.000 description 2
- 239000002904 solvent Substances 0.000 description 2
- BQCADISMDOOEFD-UHFFFAOYSA-N Silver Chemical compound [Ag] BQCADISMDOOEFD-UHFFFAOYSA-N 0.000 description 1
- 230000001427 coherent effect Effects 0.000 description 1
- 239000013039 cover film Substances 0.000 description 1
- 230000001066 destructive effect Effects 0.000 description 1
- 239000007888 film coating Substances 0.000 description 1
- 238000009501 film coating Methods 0.000 description 1
- 239000003292 glue Substances 0.000 description 1
- 229910052737 gold Inorganic materials 0.000 description 1
- 239000010931 gold Substances 0.000 description 1
- 230000001788 irregular Effects 0.000 description 1
- 238000003698 laser cutting Methods 0.000 description 1
- 239000011344 liquid material Substances 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 235000011837 pasties Nutrition 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 239000002985 plastic film Substances 0.000 description 1
- 229920006255 plastic film Polymers 0.000 description 1
- 229920003229 poly(methyl methacrylate) Polymers 0.000 description 1
- 239000004926 polymethyl methacrylate Substances 0.000 description 1
- 230000003405 preventing effect Effects 0.000 description 1
- 238000007650 screen-printing Methods 0.000 description 1
- 229910052709 silver Inorganic materials 0.000 description 1
- 239000004332 silver Substances 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 230000008961 swelling Effects 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C1/00—Processes, not specifically provided for elsewhere, for producing decorative surface effects
- B44C1/22—Removing surface-material, e.g. by engraving, by etching
- B44C1/227—Removing surface-material, e.g. by engraving, by etching by etching
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C1/00—Processes, not specifically provided for elsewhere, for producing decorative surface effects
- B44C1/16—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like
- B44C1/165—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like for decalcomanias; sheet material therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C1/00—Processes, not specifically provided for elsewhere, for producing decorative surface effects
- B44C1/16—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like
- B44C1/165—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like for decalcomanias; sheet material therefor
- B44C1/175—Transfer using solvent
Definitions
- the invention relates to the partial coating of a Plate with a transfer film.
- Transfer foils are usually metal foils, for example Gold or silver foils created by heat and pressure a carrier medium can be transferred.
- transfer films cannot, however, be discreet through a printing process Places of the carrier medium are applied, but must are initially transferred with their entire roll width. Only after the entire roll width of the transfer film has been applied in a second step, the transfer film in areas where they are not on the Plate should remain, removed again.
- a carrier plate in before applying the transfer film the areas where the transfer film is not on the Plate should remain, covered with a masking cover. Only then is the transfer film placed on the Plate surface applied, so both on the cover film masked as well as on the areas without cover foil the plate.
- the cover sheet is put together with the transfer film covering it from the plate again subtracted so that the result is only partially the transfer film remains in the desired areas on the plate.
- DE 44 40 762 a method is known in which for masking a non-stick layer on the plate is applied.
- the anti-stick layer prevents Adhesion of the transfer film to both the surface of the plate as well as on the anti-adhesion layer itself. When peeling off the masked areas of the transfer film remain Anti-adhesion layer on the plate.
- the anti-stick layer must therefore be transparent and is due to their adhesion preventing Properties are difficult to print.
- the object of the invention is the method for partial coating to simplify a plate with a transfer film.
- a amorphous or soluble masking layer on the plate surface for masking the plate areas not to be coated applied is not one-piece self-contained film, but one closed brittle layer built up of many particles, the can only be removed destroyed.
- the transfer sheet After applying the entire layer surface is covered with the masking layer coated the transfer sheet, the transfer sheet for example by applying pressure and / or heat is connected to the plate surface or to the masking layer.
- the masking layer is included the transfer film covering it by application removed from a fluid. The masking layer first broken into small pieces or through the fluid dissolves and detaches, and simultaneously or subsequently ablated by the fluid.
- An amorphous masking layer is one made, for example, of many coherent particles built up top layer, the has no regular or smooth shape, that is to say shapeless or crumbly. Due to its amorphous structure, the Masking layer points of attack for a fluid flow, so that the masking layer - if necessary also without prior detachment by means of a liquid - only by applying the Fluid flow broken up and thereby detached from the plate can be. So under an amorphous masking layer to understand a layer of irregular structure.
- a soluble masking layer Under a soluble masking layer is one Understand material layer that deals with a suitable Liquid as quickly as possible to a pasty or liquid Material film can be released, the no adhering and none cohesive properties more. Possibly can the masking layer at the same time swell and thereby the transfer film above set out.
- Under a transfer film is a film-like Understood layer of material, which is typically a thin, is not holding metal foil together.
- the transfer film with the help of a carrier film transfer the plate, the carrier film a cohesive film, typically a plastic film.
- the transfer film is on the plate with the carrier film applied and the backing film then removed again, so that the transfer film remains alone on the plate.
- the transfer film is thin, so that even without further preparatory work, e.g. Perforate or Contour cutting, a sharply contoured detachment of the Transfer film is possible.
- a perforation or The transfer film is only contoured when it is used thicker transfer films required.
- the basic idea of the invention is the removal of the masking layer by applying mechanical destructive power on the masking layer or by dissolving the masking layer.
- the masking layer therefore does not remain on the Plate, but is fragmented, including it covering transfer film, completely removed from the plate or solved by it.
- Removing the masking layer by applying a fluid is easy to implement and thus an inexpensive process, with a high Quality of the edge areas of the transfer film areas remaining on the plate is feasible.
- a water-soluble is preferably used as the masking layer Layer applied, while removing the masking layer the plate surface or the transfer film of a treatment is subjected to water so that the water-soluble masking layer is solved.
- the masking layer swells through the penetrating water and can then easily be rinsed off.
- the masking layer can be included the transfer film covering it by applying pressure jets be removed.
- the pressure jet can be in Form of a water jet or a compressed air jet his.
- the strength of the pressure jet can be dosed so that that the masking layer with that covering it Transfer film is reliably removed from the plate
- the pressure jet is not so strong that transfer foil, that adheres directly to the plate and remains there is also undesirably removed.
- the transfer film is preferably removed before the Masking layer perforated in the masked areas. Thereby becomes a liquid to dissolve the soluble Masking layer facilitates penetration of the transfer film and thus the penetration of the liquid to the masking layer improved and accelerated.
- perforating also increases the mechanical strength of the transfer film in the masked areas and possibly also the Strength of the masking layer deteriorated, so that Removal of the masking layer, including that covering it Transfer film is facilitated and accelerated.
- the transfer film also in the area of the contours of the underlying masking layer cut, i.e. the contours are pre-cut. This causes tearing when the masking layer is removed the transfer film reliably prevented in the edge areas, creating a clean edge on the remaining on the plate Transfer film is generated.
- Cutting, perforating and / or scoring is preferred the transfer film made contactless by means of laser radiation. This allows very precise cuts with a realize defined penetration depth.
- the cutting, perforating and scratches in the transfer sheet can also be caused by a knife or similar be made.
- the transfer film is preferably a metal film which with the help of heat and pressure in the transfer process to the Plate surface is applied.
- the plate can be transparent Be plastic plate.
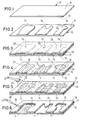
- Figs. 1 to 6 is a transparent acrylic glass carrier plate 10 shown, the printed and coated becomes and in illuminated banners, displays and the like to information and advertising purposes.
- the inside Surface 11 is the inside to be printed on a display box while the opposite surface 12 is the visible outside of a display box.
- the Carrier plate 10 is printed only on the inside 11 and coated so that the pressure applied there and the coatings applied there in a display later visible through the transparent plate 10 and protected from the weather are.
- the carrier plate 10 is shown, which on the inside Surface 11 in screen printing with a gelatin-like one Masking layer 14 was printed.
- the masking layer 14 is amorphous, i.e. it is not formed in one piece, but consists of many particles juxtaposed and are layered on top of each other and a brittle covering Form a layer on the plate surface 11.
- the masking layer 14 is water soluble, i.e. she takes water on, swelling at the same time and their sticking and holding together Properties loses.
- the masking layer 14 is printed only in the areas of the plate surface 11, in which a permanent coating with a transfer film is not desired.
- the masking layer 14 is So a negative template of the desired transfer film coating.
- a commercially available transfer gold foil 16 as a transfer foil by applying pressure and heat of approx. 120 ° C applied to the plate 10.
- the gold foil 16 is with transfer their entire roll width to the carrier plate 10.
- the gold foil 16 sticks to it Adhesive layer 17 in the areas 15 free of masking layers directly on the carrier plate surface 11 on and in the masked areas on the masking layer 14.
- the gold foil 16 is cut in with a cutting plotter the masked areas 15 perforated by auxiliary cuts 19 or incised and in the area of contours 20 with contour cuts 21 provided, as shown in Fig. 4.
- the auxiliary cuts 19 and the contour cuts 21 are made by laser cutting generated, the cutting laser adjusted in this way is that the auxiliary cuts 19 and the contour cuts 21 the Completely penetrate the gold foil 16 and the adhesive layer 17.
- the surface of the metal foil 16 with water 22 from a spray head 23 wetted The water penetrates through the contour cuts 21 and the auxiliary cuts 19 through the gold foil 16 and the adhesive layer 17 into the water-soluble masking layer 14 a.
- the water 22 swells the masking layer 14 slowly to a gelatin-like Layer, whereby it simultaneously expands and the one above it Adhesive layer 17 and the gold foil 16 upwards and pushes apart.
- the already solved is then Masking layer 14 together with the one above it Gold foil 16 and its adhesive layer 17 by applying a Compressed air jet 25 by means of a compressed air nozzle 26 as Peeling nozzle detached from the carrier plate 10 without residue and blown away.
- a water jet can also be used for detachment the masking layer 14, the gold foil 16 and the adhesive layer 17 can be used.
- the plate 10 After the carrier plate 10 has dried, the plate 10 can be printed and then, for example, by deep drawing be changed in shape.
- the carrier plate 10 can, however can also be printed before the gold foil is applied.
- masking layers that are solvent soluble are also used are, at the same time that in the adhesive layer 17th used glue insensitive to the solvent in question have to be.
- auxiliary cuts 19 and contour cuts 21 can also with be cut with a knife.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Decoration By Transfer Pictures (AREA)
- Laminated Bodies (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
- Laser Beam Processing (AREA)
Description
- Fig. 1
- die mit einer Übertragungsfolie zu beschichtende Platte,
- Fig. 2
- die Platte der Fig. 1 mit einer auf die Plattenoberfläche aufgedruckten Maskierungsschicht,
- Fig. 3
- die Platte der Fig. 1 mit aufgedruckter Maskierungsschicht und Übertragungsfolie,
- Fig. 4
- die Platte der Fig. 3 mit Einritzungen in der Übertragungsfolie im Bereich der Maskierungsschicht und Schnitten im Bereich der Konturen der Maskierungsschicht,
- Fig. 5
- Aufbringen einer Flüssigkeit auf die Platte, und
- Fig. 6
- Abtragen der Maskierungsschicht durch einen Druckluftstrahl.
Claims (10)
- Verfahren zum partiellen Beschichten einer Platte (10) mit einer Übertragungsfolie (16), mit den Schritten:Aufbringen einer amorphen oder löslichen Maskierungsschicht (14) auf die Plattenoberfläche (11) zur Maskierung der nicht zu beschichtenden Plattenbereiche (15),Beschichten der gesamten Plattenoberfläche (11) einschließlich der maskierten Bereiche mit der Übertragungsfolie,Abtragen der Maskierungsschicht (14) einschließlich der sie bedeckenden Übertragungsfolie (16) durch Aufbringen eines Fluides (22,25).
- Verfahren nach Anspruch 1, dadurch gekennzeichnet, daß als Maskierungsschicht (14) eine wasserlösliche Schicht aufgebracht wird, und daß beim Abtragen der Maskierungsschicht (14) die Übertragungsfolie einer Behandlung mit Wasser (22) ausgesetzt wird, wobei die wasserlösliche Maskierungsschicht (14) aufgelöst wird.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß die Maskierungsschicht (14) einschließlich der sie bedeckenden Übertragungsfolie (16) durch Druckstrahlbeaufschlagung abgetragen wird.
- Verfahren nach Anspruch 3, dadurch gekennzeichnet, daß die Maskierungsschicht (14) einschließlich der sie bedeckenden Übertragungsfolie (16) durch Aufbringen eines Wasserstrahles abgetragen wird.
- Verfahren nach Anspruch 4, dadurch gekennzeichnet, daß die Maskierungsschicht (14) einschließlich der sie bedeckenden Übertragungsfolie (16) durch Aufbringen eines Druckluft-Strahles (25) abgetragen wird.
- Verfahren nach einem der Ansprüche 1-5, dadurch gekennzeichnet, daß vor dem Abtragen der Maskierungsschicht (14) die Übertragungsfolie (16) in den maskierten Bereichen (15) perforiert wird.
- Verfahren nach einem der Ansprüche 1-6, dadurch gekennzeichnet, daß die Übertragungsfolie (16) im Bereich der Konturen (20) der darunterliegenden Maskierungsschicht (14) eingeschnitten wird.
- Verfahren nach Anspruch 6 oder 7, dadurch gekennzeichnet, daß das Schneiden und/oder Ritzen berührungslos mittels Laserstrahlung vorgenommen wird.
- Verfahren nach einem der Ansprüche 1-8, dadurch gekennzeichnet, daß die Übertragungsfolie (16) eine Metallfolie ist, die mit Hilfe von Hitze und Druck im Transferverfahren auf die Plattenoberfläche (11) aufgebracht wird.
- Verfahren nach einem der Ansprüche 1-9, dadurch gekennzeichnet, daß die Platte (10) eine transparente Kunststoffplatte (10) ist.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19856030 | 1998-12-04 | ||
| DE19856030A DE19856030C2 (de) | 1998-12-04 | 1998-12-04 | Verfahren zum partiellen Beschichten einer Platte |
| PCT/EP1999/009427 WO2000034053A1 (de) | 1998-12-04 | 1999-12-02 | Verfahren zum partiellen beschichten einer platte |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1135264A1 EP1135264A1 (de) | 2001-09-26 |
| EP1135264B1 true EP1135264B1 (de) | 2003-04-09 |
Family
ID=7890006
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99958155A Expired - Lifetime EP1135264B1 (de) | 1998-12-04 | 1999-12-02 | Verfahren zum partiellen beschichten einer platte |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1135264B1 (de) |
| AT (1) | ATE236795T1 (de) |
| AU (1) | AU1558600A (de) |
| DE (2) | DE19856030C2 (de) |
| WO (1) | WO2000034053A1 (de) |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1547547A (fr) * | 1967-08-30 | 1968-11-29 | Procédé pour confectionner des objets décoratifs artistiques et produits obtenus | |
| DE3337128A1 (de) * | 1983-10-12 | 1985-04-25 | Fritz Borsi KG, 7601 Schutterwald | Verfahren zum beschichten einer transparenten traegerplatte mit einer metallischen praegeschicht sowie einer danach beschichteten traegerplatte |
| DE3430111C1 (de) * | 1984-08-16 | 1985-10-24 | Leonhard Kurz GmbH & Co, 8510 Fürth | Folie,insbesondere Heisspraegefolie,mit einer dekorativen Metallschicht und Verfahren zu deren Herstellung |
| DE4438536A1 (de) * | 1994-10-28 | 1996-05-02 | Borsi Kg F | Verfahren zum selektiven, bereichsweise Beschichten einer transparenten Trägerplatte mit einer Wirkschicht unter Verwendung eines Ätzverfahrens |
| DE4440762C1 (de) * | 1994-11-15 | 1996-04-04 | Borsi Kg F | Verfahren zum selektiven, bereichsweisen Beschichten einer transparenten Trägerlatte |
| ES2137609T3 (es) * | 1996-01-24 | 1999-12-16 | Borsi Kg F | Procedimiento para el recubrimiento de una placa soporte transparente y la placa soporte transparente recubierta segun el mismo, especialmente para una caja de visualizacion. |
-
1998
- 1998-12-04 DE DE19856030A patent/DE19856030C2/de not_active Expired - Fee Related
-
1999
- 1999-12-02 DE DE59904999T patent/DE59904999D1/de not_active Expired - Lifetime
- 1999-12-02 EP EP99958155A patent/EP1135264B1/de not_active Expired - Lifetime
- 1999-12-02 AT AT99958155T patent/ATE236795T1/de not_active IP Right Cessation
- 1999-12-02 AU AU15586/00A patent/AU1558600A/en not_active Abandoned
- 1999-12-02 WO PCT/EP1999/009427 patent/WO2000034053A1/de not_active Ceased
Also Published As
| Publication number | Publication date |
|---|---|
| EP1135264A1 (de) | 2001-09-26 |
| DE19856030A1 (de) | 2000-06-08 |
| DE59904999D1 (de) | 2003-05-15 |
| ATE236795T1 (de) | 2003-04-15 |
| DE19856030C2 (de) | 2002-05-02 |
| WO2000034053A1 (de) | 2000-06-15 |
| AU1558600A (en) | 2000-06-26 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0690794B1 (de) | Formular mit heraustrennbarer karte und herstellungs- verfahren dafür | |
| DE69218332T2 (de) | Verfahren zur Herstellung von Zeichen, das eine durch Waschen entfernbare Antiklebschicht verwendet und Vorrichtung hierfür | |
| DE69610897T2 (de) | Perforierte, klebende Anordnung | |
| EP0866750A1 (de) | Mit einem laserstrahl beschriftbare folie | |
| DE3818283C2 (de) | ||
| DE2459598A1 (de) | Schablone | |
| EP2017809A2 (de) | Sicherheitsklebeband und Verfahren zu dessen Herstellung | |
| DE2613131A1 (de) | Kennzeichen in form einer plakette oder dergleichen und verfahren zu seiner herstellung | |
| EP1224650A1 (de) | Mit einem laserstrahl beschriftetes etikett, sowie verfahren und vorrichtung zu seiner herstellung | |
| DE4112517A1 (de) | Vorrichtung zur diebstahlssicherung von kraftfahrzeugen durch einen in am fahrzeug vorhandene glasflaechen eingeaetzten buchstaben- und/oder zahlen-kenncode unter verwendung einer aetzpaste | |
| DE10346683C5 (de) | Manipulationsgeschützter Folienaufbau für Etiketten und Verfahren zu dessen Herstellung | |
| DE19856030C2 (de) | Verfahren zum partiellen Beschichten einer Platte | |
| DE3823379A1 (de) | Selbstklebendes etikett | |
| EP1234863B1 (de) | Verfahren zur Herstellung eines Abdeckmaterials mit Stanzformteilen | |
| DE1669234C3 (de) | Verfahren zur Herstellung von aufeinanderfolgenden Zeichenausschnitten aufweisenden Schablonen und/oder von aufeinanderfolgenden, schablonenartig ausgeschnittenen Zeichen | |
| DE19918473A1 (de) | Verfahren und Vorrichtung zum Beschriften eines flächigen klebenden Systems aus einem Polymer, insbesondere eines transdermalen therapeutischen Systems | |
| DE4438536A1 (de) | Verfahren zum selektiven, bereichsweise Beschichten einer transparenten Trägerplatte mit einer Wirkschicht unter Verwendung eines Ätzverfahrens | |
| EP1053096B1 (de) | Verfahren und vorrichtung zum herstellen von laminatetiketten | |
| DE4105949A1 (de) | Recyclingfaehiges verbundmaterial | |
| DE650662C (de) | Verfahren zur Herstellung von bedruckten bzw. erhaben gepraegten aufklebbaren Etiketten o. dgl., die mit Dauerklebstoff versehen sind | |
| DE19927175A1 (de) | Verwendung einer Prägefolie als Dekorationsmaterial | |
| EP4059617B1 (de) | Lackierverfahren mit gedruckter maske sowie druckvorrichtung | |
| WO1992018354A1 (de) | Vorrichtung zur diebstahlssicherung von kraftfahrzeugen durch einen in am fahrzeug vorhandene glasflächen eingeätzten buchstaben- und/oder zahlen-kenncode unter verwendung einer ätzpaste | |
| WO1998013210A1 (de) | Formular mit integrierter karte sowie träger- und mehrschichtmaterial zur herstellung eines solchen formulars | |
| EP1213697B1 (de) | Verfahren und Vorrichtung zur Herstellung von Klebeetiketten oder Klebetapeten |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20010508 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 20020305 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20030409 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030409 Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030409 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030409 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: TROESCH SCHEIDEGGER WERNER AG Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030709 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030709 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030709 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030709 |
|
| ET | Fr: translation filed | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20030409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031030 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D Ref document number: 1135264E Country of ref document: IE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20031202 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031202 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20031231 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040112 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20081219 Year of fee payment: 10 Ref country code: CH Payment date: 20081222 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20081218 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20081216 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20090107 Year of fee payment: 10 |
|
| BERE | Be: lapsed |
Owner name: *WTS WERBETECHNIK G.M.B.H. Effective date: 20091231 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20100701 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091202 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20100831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100701 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091231 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091231 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091231 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20091231 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20141222 Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59904999 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160701 |