EP1207109B1 - Verfahren und Vorrichtung zum Anbringen und Heisssiegeln einer heissschrumpfbaren Haube zum Erzeugen einer wasserdichten palletisierten Verpackung - Google Patents
Verfahren und Vorrichtung zum Anbringen und Heisssiegeln einer heissschrumpfbaren Haube zum Erzeugen einer wasserdichten palletisierten Verpackung Download PDFInfo
- Publication number
- EP1207109B1 EP1207109B1 EP01410152A EP01410152A EP1207109B1 EP 1207109 B1 EP1207109 B1 EP 1207109B1 EP 01410152 A EP01410152 A EP 01410152A EP 01410152 A EP01410152 A EP 01410152A EP 1207109 B1 EP1207109 B1 EP 1207109B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- heat
- cover
- sealing
- pallet
- cladding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B53/00—Shrinking wrappers, containers, or container covers during or after packaging
- B65B53/02—Shrinking wrappers, containers, or container covers during or after packaging by heat
- B65B53/06—Shrinking wrappers, containers, or container covers during or after packaging by heat supplied by gases, e.g. hot-air jets
- B65B53/066—Mobile frames, hoods, posts or the like
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
- B65B9/10—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs
- B65B9/13—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs the preformed tubular webs being supplied in a flattened state
- B65B9/135—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs the preformed tubular webs being supplied in a flattened state for palletised loads
Definitions
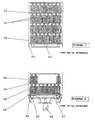
- glass containers 10 are arranged in layers on shelves. dividers 12 made of cardboard or plastic to form a stack of bottles supported on a pallet 14.
- a floor mat 16 is placed on the pallet 14 and under the first layer of containers 10, and a film sheath 18 shrink plastic, for example polyethylene, is attached from above the stacking is then joined by heat sealing to the floor mat 16 for constitute a tight packaging free of folds.
- Hooding and shrinking machines have already been proposed to make a sealed packaging intended to withstand external storage conditions by all weather and with large temperature variations.
- the covering of the sheath 18 is carried out on a first station of work after transfer of the load, and a holding device 20 ensures the leaky nipping of the lower end of the sheath 18 against the studs 22 of the pallet 14 to prevent the vertical shrinkage of the film before the phase of heat-sealed with the floor mat 16.
- a reversible 24 suction fan and blower is placed under the pallet 14 to remove the folds of the sheath 18.
- the fan 24 is in blowing mode, the duct 18 inflates further at the air inlet between the floor mat 16 and the lower end of the sheath 18.
- the fan 24 is switched to mode suction to completely absorb the inflation so as to guarantee good load stability.
- FIG. 3 corresponds to document EP 0376028, which on the one hand uses grippers that grip the bottom edge of the cover to pull it down around the load during the hooding phase, and on the other hand the levers pressing cooperating by pivoting with stops which are spaced apart with respect to the pallet, and arranged at the level of the load laying plane, or below.
- the pressing levers are mounted on the handling table by fixed joints, and are not movable vertically. They only serve absolutely not for the cover. The cover is stretched around the load using grippers until its open bottom edge covers the stops fixed on the table. The pressing levers then take over, pressing the edge against the stops, so that the grippers can be released. The film is no longer stretched after removing the grippers.
- the lever race of pressing is limited by the stops, which are projecting from the edge of the floor mat.
- the retraction of the cover by the retraction frame is not achievable in the presence of grippers, which are integral with the frame of hood, since the retraction frame would abut against the frame hooding. This results in a risk of wrinkling during heat sealing, causing a leak and a poor mechanical strength at the area to be connected.
- the object of the invention is to provide a packaging method and device waterproof under retractable sheath of a stack of glass containers, allowing obtain regular heat sealing and reinforcement of the sheath in the area for attachment to the support pallet.
- the method according to the invention is characterized in that the film of the cover is stretched on the four sides by said gripping means during the stroke of the frame shrinkage and during heat sealing of the end of the sheath to the floor mat.
- the excess perimeter at the end of the sheath is transferred locally in its all against the four corners of the pallet before heat sealing. Air is drawn in so as to evacuate the trapped air and to fold up the area to be connected under the upper pallet floor. This process ensures the shrinkage of the film on the same position reserved for the cover, to keep the cover in engagement with the clamps having carried the hooding of the palletized load, and to avoid the folds along the sheath, and creating a guy line after heat sealing, so that reinforce the mechanical resistance at the base of the waterproof cover.
- the method of covering and heat sealing according to the invention is also applicable without inflation of the sheath during retraction (claim 13).
- the means for holding the end of the sheath during heat sealing are said movable gripping means for guarantee the heat sealing the area to be connected while keeping the film stretched over the four faces.
- a pleating mechanism having a pair of control levers arranged on each side of each clamp allows in addition to carry the excess perimeter at the end of the sheath against the four corners of the pallet before the heat sealing.
- each pair of control levers is pivotally mounted between an inactive position tilted at the rear of the clamp and away from the house film, and an active position requesting the end of the sheath against the floor mat on all four sides of the pallet while now a transverse tension on the film.
- a reversible fan is arranged under the pallet, and is switchable either in blowing mode during heating of the sheath during the downward movement of the retraction frame, either in suction to evacuate the air trapped in the cover before heat sealing. All the fingers, pliers and levers of the pleating mechanism are released of the cover film to optimize heat sealing and final shrinkage in four lower corners so as to create a guy line in each corner.
- the sheath of the cover is shaped on a motorized accumulator roller mounted on a movable transfer arm of a gripping robot.
- the retraction frame is movable between a raised position and a lowered position on a second post of the retraction device, which is mounted in opposition to the hood.
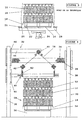
- the packaging machine designated by the general reference 30 uses the basic structure of the device described in the patent application French FR-A-2794720 of 10/6/1999 published on 15/12/2000, to which was adapted according to the invention a mechanism specific to the glass packaging process, with a particular cycle.
- the packaging machine 30 is composed of a covering device 32 and a retraction device 34 for ensuring the retraction phase on the post of cover.
- the two devices 32, 34 are mounted in opposition on two fixed uprights 36, 38 arranged on either side of the palletized CH load of containers 10.
- the retraction device 34 is provided with a retraction frame 39 for distribution hot air intended to heat the polyethylene film of the sheath 18.
- the frame of retraction 39 is mounted mobile on the upright 38 between a raised position (case of Figure 4) and a lowered position.
- the hood 32 comprises a motorized accumulator roller 40 on which is wound part of the sheath 18 constituting the cover for the load CH, and opening arms provided with retaining rollers 42.
- the roller accumulator 40 is secured to a transfer arm 44 mounted on a first slide 46 of the upright 36, and forming part of a gripping robot to be moved between a first position for winding and cutting the sheath 18, and a second position for depositing the cover on the palletized CH load. This device ensures the transfer and the opening of the sheath 18 adapted to the load CH in hooding lessons.
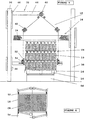
- a gripping assembly 48 is movably mounted on a second slide 50 upright 36, and has four fingers 52 and grippers 54 for gripping the cover open above the load CH placed on the conveyor 56.
- the loading of the cover on the fingers 52 is carried out after its transfer to the rollers 42 inside the retraction frame 39 being in the raised position.
- the four fingers 52 and grippers 54 of the gripping assembly 48 are arranged at the four corners of the sheath 18.
- the cover 18 is fully threaded on the load CH, and held in this position by the four fingers 52 and clamps 54 of the assembly of grip 48 which is at the bottom end of travel.
- the retraction frame 39 is turns on from top to bottom, and fan 24 is activated in mode blowing for the inflation of the cover 18 causing the removal of folds during the entire stroke of the frame 39.
- the air intake in the sheath of the cover 18 takes place through the orifice 58 formed between the open lower end of the sheath 18 and the floor mat 16.
- a pleating mechanism 60 comprises two control levers 62 arranged on either side of each clamp 54, and pivotally mounted between a inactive position ( Figures 7, 8 and 11) and an active position ( Figure 9). In the inactive position, the control levers 62 are tilted at the rear of the clamp 54 and the associated finger 52, being separated from the film of the cover 18.
- the fingers 52 are brought closer to the pallet 14, with simultaneously the passage of the four pairs of control levers 62 towards the active position on either side of the fingers 52.
- the cover 18 is urged against the floor mat 16 on all four sides of the pallet 14, while maintaining tension transverse on the film. This stage of the process occurs at the instant preceding the emission of hot air at the level of the floor mat 16.
- the excess perimeter of the film relative to the dimension of the pallet 14 at the level of the pads 22, is carried over in its entirety against the four corners of the pallet 14.
- the film of the cover 18 is stretched on all four sides to guarantee perfect heat sealing of the area to connected.
- the fan 24 is actuated simultaneously in suction mode to take the relay of mechanical action of fingers 52, pliers 54 and levers 62 of pleating, in order to avoid the vertical shrinkage of the film under the effect of its vertical shrinkage.
- the area to be connected between the lower end of the cover 18 and the floor mat 16, is positioned, for example by folding, under the upper floor of the pallet 14 under the combined effect of the suction of the fan 24, of the transverse withdrawal from of the retraction, and of the initial stress of the pleating levers 62.
- the aspiration is maintained as long as possible before the evacuation of the palletized load downstream of the packaging line. The risk of tearing the area to be connected is thus limited under the effect of the cold shrinkage of the film.
- the assembly of fingers 52, pliers 54, and levers 62 pleating is released from the cover 18, so as to optimize the heat sealing and the final retraction of the cover 18 in the four lower corners.
- the surplus of film transferred locally in the four angles created after heat sealing, a guy 63 which strengthens the mechanical resistance of the cover 18 at the level of the base, which is very stressed during subsequent handling of transport, loading, and storage of the palletized CH load.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Basic Packing Technique (AREA)
- Closing Of Containers (AREA)
- Packages (AREA)
- Packaging Of Machine Parts And Wound Products (AREA)
- Vacuum Packaging (AREA)
- Lining Or Joining Of Plastics Or The Like (AREA)
Claims (13)
- Verfahren zum Überziehen und zur Thermoversiegelung einer Hülle (18) oder eines elastischen Schlauchs aus über einer Palette aufschrumpfbarem Kunststoff, um über einer Last (CH) eine dichte Verpackung zu bilden, wobei die folgenden Schritte durchzuführen sind:dadurch gekennzeichnet, dass die Folie der Hülle (18) während der Bewegung des Retraktionsrahmens (39) und während der Thermoversiegelung des Schlauchendes mit der Bodenmatte durch die besagten Greifmittel (48) über die vier Seiten gespannt wird.Überziehen der Hülle (18) über die Last (CH), indem sie nach unten gezogen und an den vier Ecken des viereckigen Endes durch Greifmittel (48) offen gehalten wird,Erhitzen der Hülle (18) mit Warmluft, die aus einem Retraktionsrahmen (39) strömt, der entlang der Seitenfläche der Hülle (18) verschiebbar ist,Aufblasen der Hülle (18) mit Gebläseluft, um Faltenbildung während der Abwärtsbewegung des Retraktionsrahmens (39) zu vermeiden,und Thermoversiegelung des Schlauchendes mit einer Bodenmatte (16) am Ende der Bewegung des Retraktionsrahmens (39), nachdem die in der Hülle (18) eingeschlossene Luft abgesaugt wurde,
- Verfahren zum Überziehen und zur Thermoversiegelung nach Anspruch 1, dadurch gekennzeichnet, dass der Umfangsüberschuss am Ende der Hülle (18) vor der Thermoversiegelung lokal gegen die vier Ecken der Palette (14) verschoben wird.
- Verfahren zum Überziehen und zur Thermoversiegelung nach Anspruch 1 oder 2, dadurch gekennzeichnet, dass die Luft so angesaugt wird, dass die eingeschlossene Luft abgesaugt und der Verbindungsbereich unter den oberen Boden der Palette (14) positioniert wird.
- Verfahren zum Überziehen und zur Thermoversiegelung nach Anspruch 3, dadurch gekennzeichnet, dass die Positionierung des Verbindungsbereichs durch Falten erfolgt.
- Verfahren zum Überziehen und zur Thermoversiegelung nach einem der Ansprüche 1 bis 4, dadurch gekennzeichnet, dass die überschüssige Folie, die lokal in die vier unteren Ecken verschoben wird, nach der Thermoversiegelung eine Verspannung bildet, die die mechanische Festigkeit an der Basis der dichten Hülle verstärkt.
- Vorrichtung zum Überziehen und zur Thermoversiegelung einer Hülle aus aufschrumpfbarem Kunststoff über einer palettierten Last (CH), die vor allem Behälter (10) aus Glas einschließt, und aufweist:dadurch gekennzeichnet, dass die Haltemittel die besagten beweglichen Greifmittel (48) sind, um die Thermoversiegelung des Verbindungsbereichs bei Aufrechterhaltung der Spannung der Folie an den vier Seiten zu gewährleisten.Mittel zum Überziehen der Hülle (18) über die Last (CH) durch Zug nach unten und indem sie an den vier Ecken des viereckigen Endes durch Greifmittel (48) offen gehalten wird,Mittel zum Erhitzen der Hülle (18) mit Warmluft, die aus einem Retraktionsrahmen (39) entlang der Außenfläche der Hülle (18) strömt,Mittel zum Aufblasen der Hülle (18) mit Gebläseluft, um Faltenbildung während der Abwärtsbewegung des Retraktionsrahmens (39) zu vermeiden,Mittel zur Thermoversiegelung des Schlauchendes mit einer Bodenmatte (16) am Ende der Bewegung des Retraktionsrahmens (39), nachdem die in der Hülle (18) eingeschlossene Luft abgesaugt wurde, wobei die Greifmittel (48) auf einem ersten Ständer (36) der Überzugvorrichtung (32) beweglich montiert sind und eine Vielzahl von Fingern (52) und Klemmen (54) aufweisen, um die Erfassung an den vier Ecken der während der Bewegung des Retraktionsrahmens (39) offenen Hülle zu gewährleisten,und Mittel zum Halten des Schlauchendes während der Thermoversiegelung,
- Vorrichtung zum Überziehen und zur Thermoversiegelung nach Anspruch 6, dadurch gekennzeichnet, dass die Greifmittel (48) einen Faltmechanismus (60) mit paarigen Steuerhebeln (62) aufweisen, die beiderseits jeder Klemme (54) angeordnet sind, um den überschüssigen Umfang am Ende der Hülle (18) vor der Thermoversiegelung gegen die vier Ecken der Palette (14) zu verschieben.
- Vorrichtung zum Überziehen und zur Thermoversiegelung nach Anspruch 7, dadurch gekennzeichnet, dass jedes Steuerhebelpaar (62) schwenkbar montiert ist zwischen einer inaktiven, hinter die Klemme (54) und den entsprechenden Finger (52) geneigten Position, wobei es von der Folie der Hülle (18) abgewandt ist, und einer aktiven Position, bei der das Schlauchende gegen die Bodenmatte (16) auf die vier Seiten der Palette (14) bei Aufrechterhaltung einer Querspannung auf die Folie gedrückt wird.
- Vorrichtung zum Überziehen und zur Thermoversiegelung nach einem der Ansprüche 6 bis 8, dadurch gekennzeichnet, dass unter der Palette (14) ein Wendeventilator (24) angeordnet ist, der entweder im Blasmodus während der Erwärmung des Schlauchs (18) bei der Abwärtsbewegung des Rektraktionsrahmens (39) schaltbar ist oder im Ansaugmodus, um vor der Thermoversiegelung die in der Hülle eingeschlossene Luft abzusaugen.
- Vorrichtung zum Überziehen und zur Thermoversiegelung nach einem der Ansprüche 8 oder 9, dadurch gekennzeichnet, dass alle Finger (52), Klemmen (54) und Hebel (62) des Faltmechanismus (60) von der Folie der Hülle (18) gelöst werden, um die Thermoversiegelung und das letztendliche Zusammenziehen in die vier unteren Ecken zu optimieren, so dass in jeder Ecke eine Verspannung (63) entsteht.
- Vorrichtung zum Überziehen und zur Thermoversiegelung nach Anspruch 6, dadurch gekennzeichnet, dass der Schlauch der Hülle (18) über einer motorisierten Speicherwalze (40), die auf einem mobilen Transferarm (44) eines Greifroboters montiert ist, in Form gebracht wird.
- Vorrichtung zum Überziehen und zur Thermoversiegelung nach Anspruch 11, dadurch gekennzeichnet, dass der Retraktionsrahmen (39) zwischen einer angehobenen und einer abgesenkten Position auf einem zweiten Ständer (38) der Retraktionsvorrichtung (34) beweglich ist, die gegenüber der Überzugvorrichtung (32) montiert ist.
- Verfahren zum Überziehen und zur Thermoversiegelung einer Hülle (18) oder eines elastischen Schlauchs aus über einer Palette aufschrumpfbarem Kunststoff, um über einer Last (CH) eine dichte Verpackung zu bilden, wobei die folgenden Schritte durchzuführen sind:dadurch gekennzeichnet, dass die Folie der Hülle (18) während der Bewegung des Retraktionsrahmens (39) und während der Thermoversiegelung des Schlauchendes mit der Bodenmatte durch die besagten Greifmittel an den vier Seiten gespannt wird, wobei der überschüssige Umfang am Ende des Schlauchs (18) vor der Thermoversiegelung lokal gegen die vier Ecken der Palette (14) verschoben wird.Überziehen der Hülle (18) über die Last (CH), indem sie nach unten gezogen und an den vier Ecken des viereckigen Endes durch Greifmittel offen gehalten wird,Erhitzen der Hülle (18) mit Warmluft, die aus einem Retraktionsrahmen (39) strömt, der entlang der Seitenfläche der Hülle (18) verschiebbar ist,und Thermoversiegelung des Schlauchendes mit einer Bodenmatte (16) am Ende der Bewegung des Retraktionsrahmens (39),
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR0014806A FR2816587B1 (fr) | 2000-11-16 | 2000-11-16 | Procede et dispositif de houssage et de thermoscellage d'une housse en matiere plastique thermoretractable pour constituer un emballage etanche sur une charge palettisee |
| FR0014806 | 2000-11-16 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1207109A1 EP1207109A1 (de) | 2002-05-22 |
| EP1207109B1 true EP1207109B1 (de) | 2004-11-03 |
Family
ID=8856553
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01410152A Expired - Lifetime EP1207109B1 (de) | 2000-11-16 | 2001-11-15 | Verfahren und Vorrichtung zum Anbringen und Heisssiegeln einer heissschrumpfbaren Haube zum Erzeugen einer wasserdichten palletisierten Verpackung |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1207109B1 (de) |
| AT (1) | ATE281358T1 (de) |
| DE (1) | DE60106845T2 (de) |
| ES (1) | ES2232579T3 (de) |
| FR (1) | FR2816587B1 (de) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2850949B1 (fr) | 2003-02-10 | 2005-10-21 | Thimon | Dispositif et procede d'emballage d'une charge palettisee au moyen d'une housse a film en matiere plastique thermoretractable |
| ITBO20040174A1 (it) * | 2004-03-26 | 2004-06-26 | Aetna Group Spa | Apparecchiatura per la copertura di gruppi di prodotti con film tubolare estensibile |
| FR2869876B1 (fr) * | 2004-05-07 | 2006-07-21 | Thimon Sa | Dispositif et procede d'ouverture d'une gaine plastique a soufflets pour la mise en forme d'une housse souple d'emballage d'une charge |
| FR3069232B1 (fr) * | 2017-07-24 | 2021-10-29 | Thimon | Procede de houssage et thermoscellage et dispositif de houssage et thermoscellage |
| KR102140430B1 (ko) * | 2018-08-08 | 2020-08-03 | (주)범영인터팩 | 스트레치 후드 필름 포장장치 |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2417434A1 (fr) * | 1978-02-18 | 1979-09-14 | Moellers Maschf | Dispositif pour l'introduction de parties d'une feuille contractable d'emballage dans des zones en retrait prevues sur les cotes d'une pile d'objets |
| DE8816085U1 (de) | 1988-12-24 | 1989-03-09 | MSK-Verpackungs-Systeme GmbH, 4190 Kleve | Vorrichtung zum Verpacken eines auf einer Palette angeordneten Gutstapels |
| IT1229317B (it) * | 1989-05-02 | 1991-08-08 | Sestese Off Mec | Macchina incappucciatrice automatica per l'imballaggio di prodotti, in particolare di unita' pallettizzate, con pellicola tubolare termoretraibile. |
| ATE153940T1 (de) * | 1992-07-24 | 1997-06-15 | Erapa Ceka Maschbau | Verfahren und vorrichtung zur verpackung von gestapelten gütern |
| DE4342490C2 (de) * | 1993-12-13 | 1996-09-26 | Lachenmeier Kurt Aps | Verfahren und Vorrichtung zum Schrumpfen einer aus heißschrumpffähigem Material bestehenden Folienhaube, die über eine auf einer Palette befindliche Ladung gezogen ist |
-
2000
- 2000-11-16 FR FR0014806A patent/FR2816587B1/fr not_active Expired - Fee Related
-
2001
- 2001-11-15 ES ES01410152T patent/ES2232579T3/es not_active Expired - Lifetime
- 2001-11-15 AT AT01410152T patent/ATE281358T1/de not_active IP Right Cessation
- 2001-11-15 EP EP01410152A patent/EP1207109B1/de not_active Expired - Lifetime
- 2001-11-15 DE DE60106845T patent/DE60106845T2/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DE60106845T2 (de) | 2005-11-10 |
| ATE281358T1 (de) | 2004-11-15 |
| ES2232579T3 (es) | 2005-06-01 |
| FR2816587B1 (fr) | 2003-03-07 |
| FR2816587A1 (fr) | 2002-05-17 |
| DE60106845D1 (de) | 2004-12-09 |
| EP1207109A1 (de) | 2002-05-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1188676B1 (de) | Satz von Zuschnitten, Verfahren und Vorrichtung zum Verpacken eines Produktes oder einer Menge Artikeln nichtspezifischer Form | |
| JPH0212161Y2 (de) | ||
| JP2670980B2 (ja) | フィルム包装体の開梱装置 | |
| JP2561178B2 (ja) | ストレッチ包装体の開梱装置 | |
| US5042235A (en) | System for shrink-wrapping palletized goods | |
| FR2473985A1 (fr) | Machine d'emballage d'une charge dans un troncon de gaine en un materiau souple | |
| FR2628391A1 (fr) | Appareils de regroupement d'articles et procedes de regroupement, d'empilage, d'emballage et de stabilisation d'articles | |
| FR2501628A1 (fr) | Procede et dispositif pour ouvrir et charger des recipients flexibles | |
| EP1060988B1 (de) | Verfahren und Vorrichtung zum Herstellen und Anbringen einer flexiblen heissschrumpfbaren Haube auf einer palletizierten Ladung | |
| WO2007054647A1 (fr) | Procede et machine de preparation et de depose d'un manchon d'emballage a film etirable sur une charge palettisee | |
| FR2458466A1 (fr) | Procede et installation de remplissage et de fermeture de sachets | |
| EP1207109A1 (de) | Verfahren und Vorrichtung zum Anbringen und Heisssiegeln einer heissschrumpfbaren Haube zum Erzeugen einer wasserdichten palletisierten Verpackung | |
| US5247783A (en) | System for wrapping palletized goods | |
| FR2768403A1 (fr) | Procede de conditionnement de gants | |
| EP0354083B1 (de) | Verfahren und Anlage zum Behandeln und Verpacken von Gegenständen, wie leeren Behältern und auf diese Art palettisierte Ladung | |
| JP2757141B2 (ja) | フィルム包装体の開梱装置 | |
| EP1445197B1 (de) | Vorrichtung und Verfahren zum Umhüllen einer palettisierten Ladung mit einer Heissschrumpffolienhaube | |
| EP0249534B2 (de) | Verfahren und Vorrichtung zum Verpacken einer Palettenladung in eine Hülle aus wärmeschrumpffähiger Kunststoffolie | |
| FR2628390A1 (fr) | Appareil et procede de regroupement d'articles par enveloppement | |
| FR2639611A1 (fr) | Dispositif de pose de coiffe sur une charge emballee par banderolage | |
| FR2664234A1 (fr) | Procede de suremballage d'une charge palettisee au moyen d'une housse en film plastique etirable. | |
| JPH08175510A (ja) | フィルム包装体の開梱装置 | |
| EP0151364A2 (de) | Verpackungsstrasse für Produkte mit einem Film in einem aus einem flachen vorgeschnittenen Zuschnitt hergestellten Behälter | |
| EP1486420B1 (de) | Verfahren und Vorrichtung zum Umhüllen einer Ladung mittels einer flexiblen heissschrumpfbaren Folie | |
| EP1048571A1 (de) | Vorrichtung zum umhüllen einer palettisierten Ladung mittels eines Heissschrumpfschlauches |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20021118 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: THIMON |
|
| 17Q | First examination report despatched |
Effective date: 20031112 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041103 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041103 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041103 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041103 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041103 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041103 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20041103 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041130 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041130 |
|
| REF | Corresponds to: |
Ref document number: 60106845 Country of ref document: DE Date of ref document: 20041209 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: FRENCH |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050203 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20050203 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20050222 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| BERE | Be: lapsed |
Owner name: THIMON Effective date: 20041130 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2232579 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: MSK-VERPACKUNGS-SYSTEME GMBH Effective date: 20050803 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20051130 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20051130 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PLAY | Examination report in opposition despatched + time limit |
Free format text: ORIGINAL CODE: EPIDOSNORE2 |
|
| PLAH | Information related to despatch of examination report in opposition + time limit modified |
Free format text: ORIGINAL CODE: EPIDOSCORE2 |
|
| PLBC | Reply to examination report in opposition received |
Free format text: ORIGINAL CODE: EPIDOSNORE3 |
|
| BERE | Be: lapsed |
Owner name: *THIMON Effective date: 20041130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050403 |
|
| PLCK | Communication despatched that opposition was rejected |
Free format text: ORIGINAL CODE: EPIDOSNREJ1 |
|
| APBM | Appeal reference recorded |
Free format text: ORIGINAL CODE: EPIDOSNREFNO |
|
| APBP | Date of receipt of notice of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA2O |
|
| APAH | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNO |
|
| APBQ | Date of receipt of statement of grounds of appeal recorded |
Free format text: ORIGINAL CODE: EPIDOSNNOA3O |
|
| APBU | Appeal procedure closed |
Free format text: ORIGINAL CODE: EPIDOSNNOA9O |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 20130507 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R100 Ref document number: 60106845 Country of ref document: DE Effective date: 20130507 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 16 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20201110 Year of fee payment: 20 Ref country code: DE Payment date: 20201201 Year of fee payment: 20 Ref country code: ES Payment date: 20201209 Year of fee payment: 20 Ref country code: GB Payment date: 20201130 Year of fee payment: 20 Ref country code: FR Payment date: 20201130 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 60106845 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20211114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20211114 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20220225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20211116 |