EP1223247A1 - Verfahren und Einrichtung zur Schienenvorspannung durch elektrische Erwärmung und Verfahren zum Einlegen von Schienen - Google Patents
Verfahren und Einrichtung zur Schienenvorspannung durch elektrische Erwärmung und Verfahren zum Einlegen von Schienen Download PDFInfo
- Publication number
- EP1223247A1 EP1223247A1 EP01200076A EP01200076A EP1223247A1 EP 1223247 A1 EP1223247 A1 EP 1223247A1 EP 01200076 A EP01200076 A EP 01200076A EP 01200076 A EP01200076 A EP 01200076A EP 1223247 A1 EP1223247 A1 EP 1223247A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- rails
- temperature
- heating
- current source
- current
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000010438 heat treatment Methods 0.000 title claims abstract description 30
- 238000000034 method Methods 0.000 title claims abstract description 23
- 230000007935 neutral effect Effects 0.000 claims abstract description 15
- 239000004020 conductor Substances 0.000 claims abstract description 13
- 230000006835 compression Effects 0.000 description 2
- 238000007906 compression Methods 0.000 description 2
- 238000005259 measurement Methods 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 238000003466 welding Methods 0.000 description 2
- 241000532348 Gallirallus modestus Species 0.000 description 1
- 238000010924 continuous production Methods 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000005485 electric heating Methods 0.000 description 1
- 230000001105 regulatory effect Effects 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 1
Images
Classifications
-
- E—FIXED CONSTRUCTIONS
- E01—CONSTRUCTION OF ROADS, RAILWAYS, OR BRIDGES
- E01B—PERMANENT WAY; PERMANENT-WAY TOOLS; MACHINES FOR MAKING RAILWAYS OF ALL KINDS
- E01B31/00—Working rails, sleepers, baseplates, or the like, in or on the line; Machines, tools, or auxiliary devices specially designed therefor
- E01B31/02—Working rail or other metal track components on the spot
- E01B31/18—Reconditioning or repairing worn or damaged parts on the spot, e.g. applying inlays, building-up rails by welding; Heating or cooling of parts on the spot, e.g. for reducing joint gaps, for hardening rails
-
- E—FIXED CONSTRUCTIONS
- E01—CONSTRUCTION OF ROADS, RAILWAYS, OR BRIDGES
- E01B—PERMANENT WAY; PERMANENT-WAY TOOLS; MACHINES FOR MAKING RAILWAYS OF ALL KINDS
- E01B29/00—Laying, rebuilding, or taking-up tracks; Tools or machines therefor
- E01B29/16—Transporting, laying, removing, or replacing rails; Moving rails placed on sleepers in the track
-
- E—FIXED CONSTRUCTIONS
- E01—CONSTRUCTION OF ROADS, RAILWAYS, OR BRIDGES
- E01B—PERMANENT WAY; PERMANENT-WAY TOOLS; MACHINES FOR MAKING RAILWAYS OF ALL KINDS
- E01B29/00—Laying, rebuilding, or taking-up tracks; Tools or machines therefor
- E01B29/42—Undetachably joining or fastening track components in or on the track, e.g. by welding, by gluing; Pre-assembling track components by gluing; Sealing joints with filling components
- E01B29/44—Methods for effecting joining of rails in the track, e.g. taking account of ambient temperature
Definitions
- the present invention relates to a method and apparatus for heating rails by means of electric current.
- a prestressing force in longitudinal direction is set up in the rails, which force is so large that the rails are stressless at a specific temperature.
- This temperature is the so-called neutral temperature, i.e. the temperature of the rail at which no longitudinal forces are present in the rail.
- this neutral temperature is 25 °C.
- the prestressing force that is to be created in order to make the rail stressless at the neutral temperature depends on the ambient temperature that prevails when the rails are being laid. The smaller the difference between the temperature during laying and the neutral temperature, the lower the prestressing force that needs to be created. Rails may not be laid at temperatures above the neutral temperature.
- Methods for setting up a prestressing force in rails when laying said rails comprise the prestressing of the rails by means of hydraulic equipment (a continuous process, which cannot be used in arches), and the heating of the rails by means of gas burners (a discontinuous process).
- the two methods are used after the rails have been placed in their end position in the track and before they are definitively fixed in position.
- said prestressing is an operation which conventionally can only take place next to the placing of the rails.
- a major advantage of heating the rails by means of electric current, in order to heat the rails to the neutral temperature and thus make it possible to lay the rails in stressless condition, is that said heating can take place before the rail in question is fitted, simultaneously with other operations. Further advantages are the continuity of the process, the even distribution of the prestressing force over the rails and the applicability of the method in arches.
- a current source is connected to two rails, in such a manner that the rails are connected in series. Following that, current is led through the rails and, as a result of their resistance, the rails are heated to a desired temperature or a slightly higher temperature.
- the object of the present invention is to provide a method for heating rails wherein the above drawback is eliminated in an efficient manner.
- the method according to the invention is characterized in that the heating of the rails by means of a series connection is followed by heating of the rails by means of a parallel connection thereof.
- the current is controlled in dependence on the temperature, for example by varying the voltage of the current source.
- the measuring of the temperature takes place by measuring the resistance in the circuit.
- the invention furthermore relates to a method for prestressing rails when laying rails in a track, in such a manner that the rails will be at least substantially stressless at a neutral temperature, wherein the rails are heated to said neutral temperature and maintained at said temperature by using the above-described method.
- the invention furthermore relates to an apparatus for heating rails by means of electric current, which apparatus includes a current source, conductors as well as connecting elements for connecting said conductors to the rails, wherein according to the invention said conductors and said connecting elements are arranged for successively connecting the current source in series and in parallel to the rails.
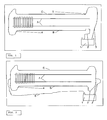
- Fig. 1 is a schematic top plan view of a railway track with rails to be fitted, which rails are electrically heated in a series connection for the purpose of increasing their temperature.
- Fig. 2 is a view corresponding to Fig. 1, wherein the rails are connected in parallel, however, for the purpose of maintaining the obtained temperature.
- the invention relates to the heating of rails for the purpose of laying said rails in a railway track.
- the invention is used in replacing the rails of an existing track. It should be understood, however, that the invention can be used with any form of fixing rails to a support.
- Rails B, C may have a length of for example a few hundred metres, for example about 500 metres. In that case they consist of a number of lengths of rails of for example 180 metres, which have been connected by welding, which lengths are in turn comprised of for example five rails of 36 metres each, which have been connected by welding by a supplier.
- the rails to be replaced are cut loose from track A and detached from the sleepers. Subsequently the rails of the existing track A are put aside by means of a special machine, and the new rails B, C are placed on the sleepers. The machine thereby rides on the rails to be replaced with its front side and on the newly laid rails B and C with its rear side.
- the new rails B, C must be built into the existing track in such a manner that the tensile stress in the rails will be zero at the neutral temperature.
- rails B and C are heated to said temperature, and during a first stage of the heating process, heating to this temperature takes place in the manner that is shown in Fig. 1.
- Said heating of the rails B and C involves the use of a current source or prestressing unit 1.
- Said current source 1 preferably consists of a direct current source with an operating voltage of for example 48 Volt.
- the power of current source 1 can be regulated by varying the voltage while the electric current remains constant.
- Said current may be as high as thousands of Amp.
- Current source 1 includes a transformer, which provides the transformation and regulation of the power.
- the apparatus comprises conductors, in this embodiment in the form of connecting cables 2 and 3 and an interconnecting cable 4, for connecting current source 1 to rails B and C.
- Said cables 2 - 4 must conduct a strong current, and to that end they have a diameter of for example 700 mm 2 .
- the ends of cables 2, 3 and 4 are provided with cable lugs 5, by means of which a sparkless connection can be made between power cables 2 - 4 and rails B and C.
- rails B and C are connected in series in the electric circuit with respect to the current source 1. Said electric circuit ensures that the supplied power from the current source is taken up by the two rails B, C. Rails B and C thus obtain a higher temperature as a result of resistance heating. The heating of the rails B and C can take place either quickly or slowly. There is a relationship between the speed at which said heating takes place and the supplied power. Quick heating requires relatively much power, whilst slow heating requires comparatively little power. Since the rails can be preheated whilst other operations are being carried out, it is possible to heat the rails only slowly.
- the temperature of said rails must have been raised to at least substantially the desired value.
- Said temperature may be equal to the neutral value, but it is also possible that a slightly higher temperature is selected, so that some cooling of rails B and C is allowed.
- the circuit current will be distributed evenly over the two rails B and C, and there will be hardly any difference in voltage, if at all, between the two rails, as a result of which the temperature in the two rails can be maintained at an identical value and a short-circuit can be created between rails B and C without any damage being caused to the equipment that creates the short circuit.
- this parallel circuit will be maintained until the fitting of the two rails has been completed.
- the temperature is maintained at the correct value by direct or indirect measurement of the temperature and control of the power in dependence thereon.
- the indirect measurement of the temperature can for example take place by measuring (the difference in) the resistance, which is dependent on the temperature in the rails.
- the additional parallel cable 6 must have a great length, for example in the order of the length of the rails B, C that are to be fitted. It is noted that current can also be supplied in a different manner than by means of a connecting cable, for example via an adjacent additional rail or via a hose containing acidified water functioning as a conductor.
- the invention provides a method and apparatus for heating rails and fitting rails which make it possible to work in an efficient and safe manner.
Landscapes
- Engineering & Computer Science (AREA)
- Architecture (AREA)
- Civil Engineering (AREA)
- Structural Engineering (AREA)
- Mechanical Engineering (AREA)
- Control Of Resistance Heating (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP01200076A EP1223247A1 (de) | 2001-01-11 | 2001-01-11 | Verfahren und Einrichtung zur Schienenvorspannung durch elektrische Erwärmung und Verfahren zum Einlegen von Schienen |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP01200076A EP1223247A1 (de) | 2001-01-11 | 2001-01-11 | Verfahren und Einrichtung zur Schienenvorspannung durch elektrische Erwärmung und Verfahren zum Einlegen von Schienen |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1223247A1 true EP1223247A1 (de) | 2002-07-17 |
Family
ID=8179739
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01200076A Withdrawn EP1223247A1 (de) | 2001-01-11 | 2001-01-11 | Verfahren und Einrichtung zur Schienenvorspannung durch elektrische Erwärmung und Verfahren zum Einlegen von Schienen |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP1223247A1 (de) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1920867A3 (de) * | 2006-11-07 | 2008-12-10 | VolkerRail Nederland BV | Verfahren und Vorrichtung zum Schweißen von Schienen |
| NL2008641C2 (nl) * | 2012-04-16 | 2013-10-17 | Brouwers Holding B V | Werkwijze voor het verwarmen van een spoorstaafsamenstel. |
| CN114606815A (zh) * | 2022-04-24 | 2022-06-10 | 沈阳铁路信号有限责任公司 | 一种钢轨加热方法及系统 |
| IT202100028691A1 (it) * | 2021-11-11 | 2023-05-11 | Srt Soc A Responsabilita Limitata Con Socio Unico | Terminale e relativa apparecchiatura per il riscaldamento di rotaie |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2246253A (en) * | 1990-06-23 | 1992-01-22 | Ceramaspeed Ltd | Heating level selecting switch arrangement |
| US5804793A (en) * | 1994-08-26 | 1998-09-08 | Faroldi; Bruno | Apparatus for heating rails during the laying down thereof |
-
2001
- 2001-01-11 EP EP01200076A patent/EP1223247A1/de not_active Withdrawn
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2246253A (en) * | 1990-06-23 | 1992-01-22 | Ceramaspeed Ltd | Heating level selecting switch arrangement |
| US5804793A (en) * | 1994-08-26 | 1998-09-08 | Faroldi; Bruno | Apparatus for heating rails during the laying down thereof |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1920867A3 (de) * | 2006-11-07 | 2008-12-10 | VolkerRail Nederland BV | Verfahren und Vorrichtung zum Schweißen von Schienen |
| NL2008641C2 (nl) * | 2012-04-16 | 2013-10-17 | Brouwers Holding B V | Werkwijze voor het verwarmen van een spoorstaafsamenstel. |
| IT202100028691A1 (it) * | 2021-11-11 | 2023-05-11 | Srt Soc A Responsabilita Limitata Con Socio Unico | Terminale e relativa apparecchiatura per il riscaldamento di rotaie |
| EP4180577A1 (de) * | 2021-11-11 | 2023-05-17 | Srt Societa' A Responsabilita' Limitata Con Socio Unico | Endgerät und zugehörige vorrichtung zum erwärmen von schienen |
| CN114606815A (zh) * | 2022-04-24 | 2022-06-10 | 沈阳铁路信号有限责任公司 | 一种钢轨加热方法及系统 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DK2866320T3 (en) | Apparatus and method for working on wiring | |
| DE10337937A1 (de) | Verfahren und Anordnung zum Verhindern oder Beseitigen einer Vereisung am Fahrdraht einer Eisenbahnstrecke | |
| EP1808049A1 (de) | Steuervorrichtung für wechselstrom-reduktionsöfen | |
| DE69514639T2 (de) | Vorrichtung zum erwärmen von schienen während des verlegens | |
| US20170241082A1 (en) | Method, apparatus and vehicle for welding rails | |
| DE4415727C2 (de) | Verfahren zur Regelung des Schmelzprozesses in einem Drehstrom-Lichtbogenofen | |
| KR20180032079A (ko) | 용접 및 예열 병행작업이 가능한 용접장치 | |
| CH300162A (de) | Vorrichtung zum Abisolieren elektrischer Leiter. | |
| CN207559435U (zh) | 一种10kV导线张力加强器 | |
| US444855A (en) | Portable electric welding apparatus | |
| RU239805U1 (ru) | Установка для индукционного нагрева рельсовых плетей | |
| US5019687A (en) | Welding system and apparatus | |
| US1778973A (en) | Arc welding system | |
| RU216175U1 (ru) | Установка для индукционного нагрева рельсовых плетей | |
| GB2557972A (en) | Electrical design for a Hall-Héroult electrolysis plant comprising a plurality of electrolytic cells connected in series, and method to start-up said plant | |
| ATE20630T1 (de) | Verfahren zum verlegen von elektrischen hochspannungsfreileitungen und vorrichtung zur durchfuehrung des verfahrens. | |
| CN112531564A (zh) | 一种旁路作业结合绝缘短杆桥接法检修方法 | |
| CN113504431B (zh) | 一种运行变电站消弧线圈配置和运行合理性的判断系统 | |
| DE202004018204U1 (de) | Mobile Widerstandsschweissmaschine | |
| EP3492851A1 (de) | Überwachungsverfahren und überwachungsvorrichtung für elektrische isolierungen eines industriellen elektroofens, sowie industrieller elektroofen | |
| CN220902131U (zh) | 一种整流桥焊接治具 | |
| DE661692C (de) | Anordnung und Verfahren zum Schutz von elektrischen Starkstromkabeln | |
| ITTO960230A1 (it) | Apparecchiatura e procedimento per la correzione della regolazione termica di rotaie posate. | |
| CN116338332A (zh) | 一种10kV系统错位核相的方法 | |
| US475232A (en) | And arthur ii |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid | ||
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20030118 |