EP1233081A1 - Procédé et dispositif pour le revêtement par plasma d'une aube de turbine - Google Patents
Procédé et dispositif pour le revêtement par plasma d'une aube de turbine Download PDFInfo
- Publication number
- EP1233081A1 EP1233081A1 EP01103457A EP01103457A EP1233081A1 EP 1233081 A1 EP1233081 A1 EP 1233081A1 EP 01103457 A EP01103457 A EP 01103457A EP 01103457 A EP01103457 A EP 01103457A EP 1233081 A1 EP1233081 A1 EP 1233081A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- axis
- blade
- turbine blade
- coating
- plasma
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000000576 coating method Methods 0.000 title claims abstract description 67
- 239000011248 coating agent Substances 0.000 title claims abstract description 58
- 238000000034 method Methods 0.000 title claims abstract description 34
- 230000008569 process Effects 0.000 title description 7
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims abstract description 12
- 238000007750 plasma spraying Methods 0.000 claims abstract description 10
- 238000005260 corrosion Methods 0.000 claims abstract description 5
- 230000007797 corrosion Effects 0.000 claims abstract description 4
- 230000003647 oxidation Effects 0.000 claims abstract description 3
- 238000007254 oxidation reaction Methods 0.000 claims abstract description 3
- 229910000531 Co alloy Inorganic materials 0.000 claims abstract 2
- 229910000990 Ni alloy Inorganic materials 0.000 claims abstract 2
- 239000007921 spray Substances 0.000 claims description 32
- 238000005507 spraying Methods 0.000 claims description 10
- 241001156002 Anthonomus pomorum Species 0.000 description 19
- 239000010410 layer Substances 0.000 description 12
- 238000010290 vacuum plasma spraying Methods 0.000 description 7
- 239000000463 material Substances 0.000 description 5
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 4
- 229910017052 cobalt Inorganic materials 0.000 description 4
- 239000010941 cobalt Substances 0.000 description 4
- GUTLYIVDDKVIGB-UHFFFAOYSA-N cobalt atom Chemical compound [Co] GUTLYIVDDKVIGB-UHFFFAOYSA-N 0.000 description 4
- 238000010438 heat treatment Methods 0.000 description 4
- 229910052759 nickel Inorganic materials 0.000 description 4
- 230000004048 modification Effects 0.000 description 3
- 238000012986 modification Methods 0.000 description 3
- 210000002023 somite Anatomy 0.000 description 3
- 229910000601 superalloy Inorganic materials 0.000 description 3
- 229910045601 alloy Inorganic materials 0.000 description 2
- 239000000956 alloy Substances 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 2
- 229910052742 iron Inorganic materials 0.000 description 2
- 239000011148 porous material Substances 0.000 description 2
- 239000000243 solution Substances 0.000 description 2
- 241001136792 Alle Species 0.000 description 1
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 description 1
- 239000002318 adhesion promoter Substances 0.000 description 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 1
- 229910052782 aluminium Inorganic materials 0.000 description 1
- 230000008901 benefit Effects 0.000 description 1
- 239000000919 ceramic Substances 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 239000011651 chromium Substances 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000009413 insulation Methods 0.000 description 1
- 238000005457 optimization Methods 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 230000002265 prevention Effects 0.000 description 1
- 230000001681 protective effect Effects 0.000 description 1
- 239000011241 protective layer Substances 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 229910052702 rhenium Inorganic materials 0.000 description 1
- WUAPFZMCVAUBPE-UHFFFAOYSA-N rhenium atom Chemical compound [Re] WUAPFZMCVAUBPE-UHFFFAOYSA-N 0.000 description 1
- 238000007751 thermal spraying Methods 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
- 229910052727 yttrium Inorganic materials 0.000 description 1
- VWQVUPCCIRVNHF-UHFFFAOYSA-N yttrium atom Chemical compound [Y] VWQVUPCCIRVNHF-UHFFFAOYSA-N 0.000 description 1
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
- C23C4/134—Plasma spraying
Definitions
- the invention relates to a method for plasma coating a turbine blade directed along a blade axis by means of thermal plasma spraying.
- the invention relates also a coating device for implementation of the procedure.
- a coating process for plasma coating a turbine blade emerges from EP 1 033 417 A1.
- One of the possible coatings to be applied to the turbine blade consists of an MCrAlX alloy, M for one or more elements comprising iron, cobalt or nickel, Cr for chrome, Al for aluminum and X for one or more elements the group comprising yttrium, rhenium and the elements of rare earths.
- This metallic layer is achieved by thermal spraying using the VPS (Vacuum Plasma Spraying) or LPPS (Low Pressure Plasma Spraying) applied the turbine blade.
- the gas turbine blade exists in particular from a nickel or iron or cobalt-based superalloy.
- the MCrAlX alloy serves in particular a corrosion and oxidation prevention.
- the application One layer usually includes heat treatment on.
- a process time of about 30 minutes during the post heat treatment the gas turbine blade has a process time of about Has 120 minutes.
- the plasma coating is done with a plasma gun or a plasma torch. Such a Plasma torch is also often used before the coating process used to heat the component to be coated.
- the Turbine blade to be coated is usually on one Turntable arranged while the plasma torch is on a multi-axis robot is arranged. During the coating the turbine blade is at a coating temperature kept from about 1100 ° K to 1200 ° K.
- the object of the invention is to provide a method for Plasma coating of a turbine blade, in particular an improved quality of by thermal plasma spraying applied coating results.
- Another task the invention is the specification of a coating device to carry out this procedure.
- the object is directed to a method solved by specifying a process for plasma coating a turbine blade directed along a blade axis, with the at least three plasma torches for thermal Plasma spraying can be used simultaneously.
- the invention is based on the knowledge that in the conventional Certain use of a single plasma torch Loss of quality for the coating of the turbine blade consequences.
- it occurs on certain critical areas like the transition area between the airfoil and adjacent blade platforms to an undesirably high Layer thickness because the coating of the platform on the one hand and the leaf on the other hand in the border area to one after conventional coating method inevitable overlap and thus lead to an increased layer thickness.
- Such pore formation leads to one increased corrosion of the coating actually protective base material.
- the invention in a coating with only one Burner an unfavorable temperature control for the to be coated Component, since with only one burner only one insufficiently uniform heating of the component is possible.
- the task directed at a coating device becomes solved according to the invention by specifying a coating device for coating a turbine blade by means of a Method according to one of the possibilities described above.
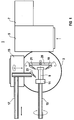
- Figure 1 shows a coating device 1.
- the coating device 1 has a coating chamber 3. With the pre-chamber 5 of the coating chamber 3 is vacuum-tight connected. In the coating chamber 3 is one along Blade axis 9 arranged turbine blade 11 arranged. The turbine blade 11 is on one in the coating chamber 3 arranged blade manipulator 13 arranged. Via an expansion chamber connected to the coating chamber 3 15 also carries a burner manipulator 17 into the coating chamber 3. A first plasma torch 19 and a second plasma torch 21 are on a torch carrier 25 arranged. A third plasma torch 23 is on the torch manipulator 17 arranged. The three plasma torches 19, 21, 23 are decoupled from each other and thus controllable independently of each other and agile.
- Farther can be one of the particularly large turbine blades Plasma torch 19, 21, 23 for heating the turbine blade 11 are used, which means a targeted heat input exactly is achieved where it is needed, which in turn changes results in a qualitative improvement for the layer.
- particularly large turbine blades for example on the order of a length of 1 m, a coating possible with sufficiently high quality the use of at least three plasma torches 19, 21, 23.
- the use of the three plasma torches 19, 21, 23 also to an overall more constant layer thickness distribution on the turbine blade 11.
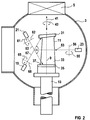
- FIG. 2 shows a particularly simple construction type of installation of the three plasma torches 19, 21, 23.
- the turbine blade 11 is therefore a gas turbine blade made of a nickel or cobalt base superalloy base 30. It has an airfoil 33 to which it is attached Blade tip a tip platform 31 and blade foot side a foot platform 35 borders. Between platforms 31, 35, The airfoil 33 has rounded regions 37, in which it especially to the overspray when using only one Plasma torches can come as described above.
- the turbine blade 11 is attached to the blade manipulator 13 in such a way that they are in a direction of rotation by means of the blade manipulator 13 43 is rotatable about the blade axis 9.
- a first plasma torch 19 sprays along a first spray direction 67 onto the turbine blade 11.
- the first plasma torch 19 is about a first axis of rotation 66 rotatable in the direction of rotation 65.
- a second Plasma torch 21 sprays along a second spray direction 63 on the turbine blade 11.
- the second plasma torch 21 is along a second axis of rotation 62 in a direction of rotation 61 rotatable.
- the first plasma torch 19 is along a direction parallel to the blade axis 9 in the foot area the turbine blade 11 arranged while the second Plasma torch 21 along this direction at the height of the Blade tip of the turbine blade 11 is arranged.
- the first spray direction 67 forms with the second spray direction 63 an angle ⁇ that is greater than 90 °. In this configuration the first plasma torch 19 is used for a coating the tip platform 31, while the second plasma torch 21 serves to coat the foot platform 35.
- a third is arranged on the side of the turbine blade 11 Plasma torch 23.
- This third plasma torch 23 injects along a third spray direction 53 onto the turbine blade 11.
- the third plasma torch 23 is along one Rotation axis 56 rotatable about the direction of rotation 55.
- the turbine blade 11 Before coating the turbine blade 11 with a a coating material 81, preferably a MCrAlX oxidation-corrosion protection layer, the turbine blade 11 is heated. This happens in particularly evenly by all three plasma torches 19, 21, 23 at the same time. After reaching the desired temperature the coating material is applied, as described, the first plasma torch 19 and the second Plasma torches 21 serve to coat the platforms 31, 35, while a coating over the third plasma torch 23 of the airfoil 33 is made.
- a coating material 81 preferably a MCrAlX oxidation-corrosion protection layer
- FIG. 3 shows a modification of the coating device 1 from Figure 2, this modification the third plasma torch 23 concerns. This is now also in one direction 51 movable perpendicular to the plane E through the blade axis 9 and the third spray direction 53 is fixed. Furthermore, the third plasma torch 23 is also at a distance to the turbine blade 11 along a mobility the third spray direction 53 movably arranged. While the axis of rotation 56 of the third plasma torch 23 according to FIG Arrangement in Figure 2 aligned parallel to the blade axis 9 was, it is now along the spray direction 53 and thus directed perpendicular to the blade axis 9. The axis of rotation 56 lies in level E. As already in FIG.
- FIG. 4 shows a common mobility of the first plasma torch 19 and the second plasma torch 21 by means of a drive unit 71, the one Carrier 72 for the first and second plasma torches 19, 21 in parallel moved to the blade axis 9.
- a chain 73 moved parallel to the blade axis 9.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Coating By Spraying Or Casting (AREA)
- Turbine Rotor Nozzle Sealing (AREA)
Priority Applications (9)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP01103457A EP1233081A1 (fr) | 2001-02-14 | 2001-02-14 | Procédé et dispositif pour le revêtement par plasma d'une aube de turbine |
| US10/467,939 US20040146657A1 (en) | 2001-02-14 | 2002-02-13 | Method for plasma coating a turbine blade and coating device |
| DE50204081T DE50204081D1 (de) | 2001-02-14 | 2002-02-13 | Verfahren zur plasmabeschichtung einer turbinenschaufel und beschichtungsvorrichtung |
| JP2002570793A JP2004526056A (ja) | 2001-02-14 | 2002-02-13 | タービン翼のプラズマ被覆法 |
| EP02722074A EP1360342B1 (fr) | 2001-02-14 | 2002-02-13 | Procede et dispositif pour revetir de plasma une aube de turbine |
| CA002438156A CA2438156A1 (fr) | 2001-02-14 | 2002-02-13 | Procede et dispositif pour revetir de plasma une aube de turbine |
| PCT/EP2002/001515 WO2002070772A1 (fr) | 2001-02-14 | 2002-02-13 | Procede et dispositif pour revetir de plasma une aube de turbine |
| CNA2005100729046A CN1699615A (zh) | 2001-02-14 | 2002-02-13 | 用于对透平叶片进行等离子喷镀的方法和喷镀装置 |
| CNB028049861A CN1237197C (zh) | 2001-02-14 | 2002-02-13 | 用于对透平叶片进行等离子喷镀的方法和喷镀装置 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP01103457A EP1233081A1 (fr) | 2001-02-14 | 2001-02-14 | Procédé et dispositif pour le revêtement par plasma d'une aube de turbine |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1233081A1 true EP1233081A1 (fr) | 2002-08-21 |
Family
ID=8176493
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01103457A Withdrawn EP1233081A1 (fr) | 2001-02-14 | 2001-02-14 | Procédé et dispositif pour le revêtement par plasma d'une aube de turbine |
| EP02722074A Expired - Lifetime EP1360342B1 (fr) | 2001-02-14 | 2002-02-13 | Procede et dispositif pour revetir de plasma une aube de turbine |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02722074A Expired - Lifetime EP1360342B1 (fr) | 2001-02-14 | 2002-02-13 | Procede et dispositif pour revetir de plasma une aube de turbine |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20040146657A1 (fr) |
| EP (2) | EP1233081A1 (fr) |
| JP (1) | JP2004526056A (fr) |
| CN (2) | CN1237197C (fr) |
| CA (1) | CA2438156A1 (fr) |
| DE (1) | DE50204081D1 (fr) |
| WO (1) | WO2002070772A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2009144109A1 (fr) * | 2008-05-29 | 2009-12-03 | Siemens Aktiengesellschaft | Procédé de projection à la flamme supersonique |
| EP2145974A1 (fr) * | 2008-07-16 | 2010-01-20 | Siemens Aktiengesellschaft | Procédé destiné à l'injection de flammes à vitesse élevée |
| EP2444590A1 (fr) * | 2010-10-19 | 2012-04-25 | Siemens Aktiengesellschaft | Procédé de revêtement de trous de refroidissement |
Families Citing this family (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA2520705C (fr) * | 2004-11-02 | 2012-12-18 | Sulzer Metco Ag | Appareil de projection a chaud et egalement processus de projection a chaud |
| EP1816229B1 (fr) * | 2006-01-31 | 2010-03-24 | Siemens Aktiengesellschaft | Dispositif et procédé de pulvériation thermique |
| US8191504B2 (en) * | 2006-11-27 | 2012-06-05 | United Technologies Corporation | Coating apparatus and methods |
| JP5710159B2 (ja) * | 2010-06-29 | 2015-04-30 | 株式会社東芝 | 溶射システムおよび溶射方法 |
| CN102500531A (zh) * | 2011-09-30 | 2012-06-20 | 库博汽车标准配件(昆山)有限公司 | 离子焰喷射装置 |
| FR2991614B1 (fr) * | 2012-06-06 | 2014-07-18 | Snecma | Procede de rechargement global de piece metallique pour turboreacteurs d'aeronefs, et outillage de protection globale pour la mise en œuvre du procede |
| US9126232B2 (en) * | 2013-02-21 | 2015-09-08 | Pratt & Whitney Canada Corp. | Method of protecting a surface |
| US10294806B2 (en) | 2013-03-15 | 2019-05-21 | United Technologies Corporation | Multiple coating configuration |
| KR101615911B1 (ko) | 2014-05-30 | 2016-05-12 | 주식회사 아이스기술 | 회전체가 구비된 진공로를 이용하여 모재를 브레이징 코팅하는 방법 |
| FR3092779B1 (fr) * | 2019-02-19 | 2021-02-26 | Safran Aircraft Engines | Outillage amélioré pour le revêtement de léchettes |
| DE102020209085A1 (de) * | 2020-07-21 | 2022-01-27 | MTU Aero Engines AG | Leitschaufelanordnung für eine strömungsmaschine |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3461268A (en) * | 1967-01-24 | 1969-08-12 | Inoue K | Kinetic deposition of particulate materials |
| US4683148A (en) * | 1986-05-05 | 1987-07-28 | General Electric Company | Method of producing high quality plasma spray deposits of complex geometry |
| DE4040893A1 (de) * | 1989-12-26 | 1991-06-27 | Gen Electric | Verstaerkte mikrolaminierte metall-matrix-verbundstruktur |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4334495A (en) * | 1978-07-11 | 1982-06-15 | Trw Inc. | Method and apparatus for use in making an object |
| US6120854A (en) * | 1999-02-19 | 2000-09-19 | Northrop Grumman | Liquid crystal polymer coating process |
-
2001
- 2001-02-14 EP EP01103457A patent/EP1233081A1/fr not_active Withdrawn
-
2002
- 2002-02-13 CN CNB028049861A patent/CN1237197C/zh not_active Expired - Fee Related
- 2002-02-13 EP EP02722074A patent/EP1360342B1/fr not_active Expired - Lifetime
- 2002-02-13 CN CNA2005100729046A patent/CN1699615A/zh active Pending
- 2002-02-13 CA CA002438156A patent/CA2438156A1/fr not_active Abandoned
- 2002-02-13 JP JP2002570793A patent/JP2004526056A/ja active Pending
- 2002-02-13 WO PCT/EP2002/001515 patent/WO2002070772A1/fr not_active Ceased
- 2002-02-13 DE DE50204081T patent/DE50204081D1/de not_active Expired - Lifetime
- 2002-02-13 US US10/467,939 patent/US20040146657A1/en not_active Abandoned
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3461268A (en) * | 1967-01-24 | 1969-08-12 | Inoue K | Kinetic deposition of particulate materials |
| US4683148A (en) * | 1986-05-05 | 1987-07-28 | General Electric Company | Method of producing high quality plasma spray deposits of complex geometry |
| DE4040893A1 (de) * | 1989-12-26 | 1991-06-27 | Gen Electric | Verstaerkte mikrolaminierte metall-matrix-verbundstruktur |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2009144109A1 (fr) * | 2008-05-29 | 2009-12-03 | Siemens Aktiengesellschaft | Procédé de projection à la flamme supersonique |
| EP2145974A1 (fr) * | 2008-07-16 | 2010-01-20 | Siemens Aktiengesellschaft | Procédé destiné à l'injection de flammes à vitesse élevée |
| EP2444590A1 (fr) * | 2010-10-19 | 2012-04-25 | Siemens Aktiengesellschaft | Procédé de revêtement de trous de refroidissement |
| US8920882B2 (en) | 2010-10-19 | 2014-12-30 | Siemens Aktiengesellschaft | Setting the quantity of cooling air for a turbine blade or vane by controlled overspray |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2002070772A1 (fr) | 2002-09-12 |
| US20040146657A1 (en) | 2004-07-29 |
| EP1360342B1 (fr) | 2005-08-31 |
| CN1237197C (zh) | 2006-01-18 |
| EP1360342A1 (fr) | 2003-11-12 |
| CN1699615A (zh) | 2005-11-23 |
| CA2438156A1 (fr) | 2002-09-12 |
| JP2004526056A (ja) | 2004-08-26 |
| DE50204081D1 (de) | 2005-10-06 |
| CN1491292A (zh) | 2004-04-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1360342B1 (fr) | Procede et dispositif pour revetir de plasma une aube de turbine | |
| EP1029103B1 (fr) | Procede d'application de revetement et dispositif | |
| DE2355532C2 (de) | Verfahren zum Pulver-Auftragschweißen von Metallen und Legierungen | |
| EP2038083B1 (fr) | Procédé de réparation et/ou de remplacement d'éléments individuels d'une pièce d'une turbine à gaz | |
| DE102012007114B3 (de) | Verfahren zur Ausbildung einer Beschichtung oder dreidimensionaler Strukturelemente auf Substratoberflächen, die mit TiAl gebildet ist/sind, durch Laserauftragsschweißen | |
| DE3815006A1 (de) | Vorrichtung zum herstellen von beschichtungen mit abgestufter zusammensetzung | |
| EP2824216A1 (fr) | Procédé de fabrication d'un produit en acier plat pourvu, par revêtement par galvanisation à chaud, d'une couche de protection métallique et four à passage continu pour une installation de revêtement par galvanisation à chaud | |
| DE3784548T2 (de) | Verfahren zum Aufbringen von Überzügen hoher Qualität und komplexer Geometrie durch Plasmaspritzen. | |
| DE102010024083A1 (de) | Verfahren zur Reparatur von Rotorschaufeln | |
| CH691761A5 (de) | Ueberwachung und Regelung von thermischen Spritzverfahren. | |
| EP1165854B1 (fr) | Procede et dispositif pour appliquer un revetement sur un produit | |
| DE2812311A1 (de) | Verfahren und vorrichtung zum vakuumaufdampfen duenner schichten mittels elektronenstrahlen, insbesondere zur herstellung von turbinenschaufeln | |
| EP0142083A2 (fr) | Procédé et dispositif pour l'obtention de revêtements métalliques | |
| DE4135326C1 (en) | Coating components by thermal spraying - using preheating kiln to heat workpiece before plasma spraying in vacuum chamber | |
| EP0263469B1 (fr) | Procédé pour l'enduction thermique de surfaces | |
| CH674650A5 (en) | Heat-treating coated surfaces - with high energy beam and pre- or post-heat treatment using induction heating devices to prevent cracking in high hardness alloys | |
| EP2859979A1 (fr) | Réparation de surfaces au moyen d'un mélange brasage/matériau de base et composant | |
| DE3147755C2 (de) | Verfahren zum Beschichten eines Metalls mit einem davon verschiedenen Metall | |
| EP1387896B1 (fr) | Ustensile de cuisine a revetement par projection thermique et procede de production de ce revetement | |
| EP0389959B1 (fr) | Procédé de réalisation de revêtements protecteurs contre la corrosion et l'usure | |
| EP0571796B1 (fr) | Couche de protection superficielle et procédé pour sa préparation | |
| DE10328596A1 (de) | Verfahren und Vorrichtung zum Laserschweißen von Bauteilen | |
| EP2145974A1 (fr) | Procédé destiné à l'injection de flammes à vitesse élevée | |
| DE19513919C2 (de) | Verfahren zur Hochgeschwindigkeitsbeschichtung von Bauteilen und Werkstücken sowie mögliche Vorrichtung zur Hochgeschwindigkeitsbeschichtung von Bauteilen und Werkstücken | |
| WO2010088879A1 (fr) | Procédé de fabrication d'un revêtement résistant à l'usure sur un élément de construction |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid | ||
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20030222 |