EP1252946A2 - Verfahren zum Herstellen von rotationssymmetrischen Bauteilen - Google Patents
Verfahren zum Herstellen von rotationssymmetrischen Bauteilen Download PDFInfo
- Publication number
- EP1252946A2 EP1252946A2 EP02002515A EP02002515A EP1252946A2 EP 1252946 A2 EP1252946 A2 EP 1252946A2 EP 02002515 A EP02002515 A EP 02002515A EP 02002515 A EP02002515 A EP 02002515A EP 1252946 A2 EP1252946 A2 EP 1252946A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- tube
- wall thickness
- component
- outer diameter
- rotationally symmetrical
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21K—MAKING FORGED OR PRESSED METAL PRODUCTS, e.g. HORSE-SHOES, RIVETS, BOLTS OR WHEELS
- B21K21/00—Making hollow articles not covered by a single preceding sub-group
- B21K21/12—Shaping end portions of hollow articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C37/00—Manufacture of metal sheets, rods, wire, tubes, profiles or like semi-manufactured products, not otherwise provided for; Manufacture of tubes of special shape
- B21C37/06—Manufacture of metal sheets, rods, wire, tubes, profiles or like semi-manufactured products, not otherwise provided for; Manufacture of tubes of special shape of tubes or metal hoses; Combined procedures for making tubes, e.g. for making multi-wall tubes
- B21C37/15—Making tubes of special shape; Making tube fittings
- B21C37/16—Making tubes with varying diameter in longitudinal direction
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21K—MAKING FORGED OR PRESSED METAL PRODUCTS, e.g. HORSE-SHOES, RIVETS, BOLTS OR WHEELS
- B21K1/00—Making machine elements
- B21K1/06—Making machine elements axles or shafts
- B21K1/12—Making machine elements axles or shafts of specially-shaped cross-section
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49826—Assembling or joining
- Y10T29/49945—Assembling or joining by driven force fit
Definitions
- the invention relates to a method for producing rotationally symmetrical Components from a tube, in particular hollow monoblock shafts, the tube initially having a constant outside diameter and a constant Has wall thickness and the rotationally symmetrical component at least over a range of its total length a different one, in particular smaller outer diameter and / or a different one, in particular has greater wall thickness.
- the invention also relates to a rotationally symmetrical component, in particular a hollow monoblock shaft, with an outside diameter that varies over the entire length of the component and / or a varying wall thickness.
- Rotationally symmetrical components that differ over their entire length Have outside diameter and different wall thicknesses, in particular in motor vehicles as drive shafts, camshafts, intermediate shafts or gear shafts used. Under the generally stronger Attentive point of view of "weight loss" have been some time ago, instead of shafts made from solid rods, made from pipes Waves, so-called hollow shafts are used.
- Pipes especially steel pipes, are manufactured either seamless, d. H. from the full material without Longitudinal seam, or in a welded version, d. H. made of bent sheet metal or Strip steel with longitudinal seam. Welded parts are usually used for rotating components Pipes used, since seamless tubes have the required concentricity cannot always be guaranteed with sufficient certainty. Beyond that the production of seamless tubes is generally more expensive than the production of welded ones Tube.
- Wall thickness cannot be increased arbitrarily, but depends on the one hand Outside diameter and wall thickness of the original pipe to other on the outside diameter of the end portion of the shaft (material conservation or constant volume). Should the end area be a particularly large one Have wall thickness, it is necessary that the starting material, i.e. the original pipe, a sufficiently large wall thickness or one has a correspondingly large outer diameter. This can then do so cause the wall thickness and / or the outer diameter of the original Pipe must be larger than the desired wall thickness or the outer diameter of the finished shaft in the middle. With the pipe not only do the end areas have to be kneaded, but also the middle area must also be stretched both reduced in its outer diameter and in its wall thickness become.
- the invention is therefore based on the object of a method for producing of a rotationally symmetrical component described at the outset from a Specify pipe, which is carried out as simply and therefore inexpensively can be.
- the method according to the invention is therefore simpler and therefore less expensive carry out that as a starting material a tube with a wall thickness, which corresponds to the smallest wall thickness of the finished component becomes.
- only the wall thickness is used considered a region of the component with a certain length. has For example, the edge of the component has a short approach, which is a very has a small wall thickness, this is not the smallest wall thickness of the component to understand.
- the component will have its smallest wall thickness in have approximately in the middle area, the area of the smallest wall thickness but does not have to be exactly in the middle of the component.
- the process that is usually necessary in the prior art is eliminated Stretching an area, in particular the central area of the Tube.
- the pipe is a welded one that has not been retightened Tube is used. This can - as explained above - the manufacturing cost of the raw material i.e. the pipe significantly reduced become.
- the method according to the invention can thereby be advantageously further develop that axial upsetting and radial forging the heated area of the tube in one setting, preferably in one step. Must the tube in the individual processing steps not being switched from one machine to another, this results in shorter manufacturing times for the rotationally symmetrical Component, which also has a favorable effect on the manufacturing costs.
- the method according to the second teaching of the invention is reduced the manufacturing costs in that a tube as a starting material is used, which is only welded, but not tightened is. That for achieving an edge area of the tube with a relatively large Wall thickness required material volume is used in this process provided that the tube from a sheet or a Steel strip with a large thickness is bent.
- the wall thickness of the pipe with the smallest wall thickness of the finished component is reduced.
- 1a shows a simply welded tube 2 with an outer diameter D 1 and a wall thickness d 1 .
- the wall thickness d 1 corresponds to the thickness of the sheet or strip steel from which the tube 2 has been bent.
- 1b shows the tube 2 'after it has been drawn through a drawing nozzle or a drawing ring. By pulling the tube 2, it has an outer diameter D 2 ⁇ D 1 and a wall thickness d 2 > d 1 .
- This tube 2 ' is dimensioned such that a shaft 1 with an end region 3 with the desired outer diameter D E and the desired wall thickness d E can be produced by kneading.
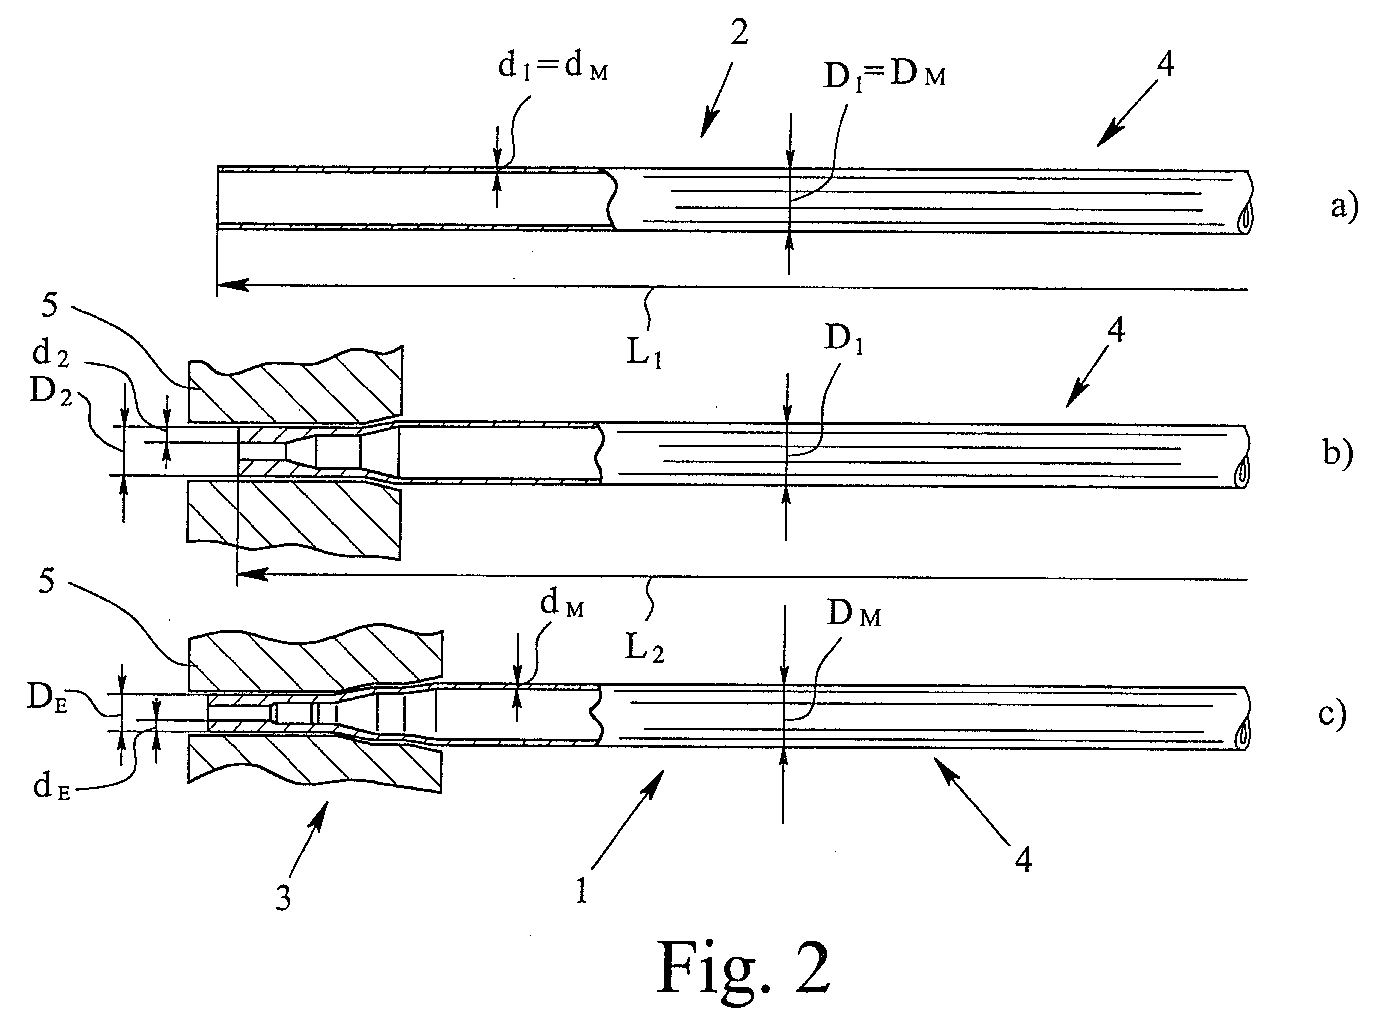
- FIG. 2 shows an embodiment of the method according to the invention for producing a shaft 1 using three manufacturing steps.
- the first manufacturing step (FIG. 2a) corresponds to the first manufacturing step (FIG. 1a) in the method known from the prior art, namely it shows a simply welded tube 2 with an outside diameter D 1 and a wall thickness d 1 .
- the wall thickness d 1 of the tube 2 corresponds to the wall thickness d M of the central region 4 of the finished shaft 1.
- the outer diameter D 1 of the tube 2 also corresponds to the outer diameter D M of the central region 4 of the shaft 1, so that the central region 4 of the tube 2 or the shaft 1 does not have to be machined.
- tube 2 is a simply welded tube 2 that is not tightened can be used. This allows in the inventive method a processing step in the manufacture of the tube 2, namely the drawing of the tube 2 can be saved.
- the pipe 2b shows that the pipe 2, which is partially heated in the end region 3, is compressed axially, so that the pipe 2 has an overall length L 2 ⁇ L 1 .
- the axial upsetting of the tube 2 leads to a thickening of the wall thickness in the end region 3.
- the heated region of the tube 2, ie the end region 3 is machined by radial forging with a forging tool 5, as a result of which the desired outer diameter D E is achieved.
- a multi-stage change in the outside diameter and wall thickness in the end region 3 is achieved by several radial forging processes.
- the end region 3 has an outer diameter D 2 ⁇ D 1 .
- a mandrel is inserted into the tube 2 during the axial upsetting and the radial forging of the heated area.
- the desired wall thickness d E of the shaft 1 is then also determined by the choice of the outside diameter of the mandrel. Because the tube 2 is partially heated, no or significantly reduced work hardening processes occur, which makes a greater degree of deformation possible.
- the tube 2 shown in FIG. 2 or the shaft 1 shown has, for example, the following outer diameters D and wall thicknesses d in the individual production steps:
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Forging (AREA)
- Compositions Of Oxide Ceramics (AREA)
- Ceramic Products (AREA)
- Shafts, Cranks, Connecting Bars, And Related Bearings (AREA)
Abstract
Description
- Fig. 1
- eine Welle, dargestellt in verschiedenen Fertigungsstufen bei einem aus dem Stand der Technik bekannten Verfahren, und
- Fig. 2
- eine Welle, dargestellt in verschiedenen Fertigungsstufen bei einer bevorzugten Ausführung des erfindungsgemäßen Verfahrens.
Claims (11)
- Verfahren zum Herstellen von rotationssymmetrischen Bauteilen aus einem Rohr, insbesondere von hohlen Monoblockwellen, wobei das Rohr anfangs einen konstanten Außendurchmesser und eine konstante Wandstärke aufweist und das rotationssymmetrische Bauteil zumindest über einen Bereich seiner Gesamtlänge einen davon abweichenden, insbesondere kleineren Außendurchmesser und/oder eine davon abweichende, insbesondere größere Wandstärke aufweist, gekennzeichnet durch folgende Verfahrensschritte:Verwendung eines Rohres mit einer Wandstärke, die der kleinsten
Wandstärke des fertigen Bauteils entspricht,partielle Erwärmung mindestens eines Bereichs des Rohres,axiales Stauchen des erwärmten Bereichs des Rohres undradiales Schmieden des erwärmten Bereichs des Rohres. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, daß als Rohr ein geschweißtes, nicht nachgezogenes Rohr verwendet wird.
- Verfahren nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß das axiales Stauchen und das radiale Schmieden des erwärmten Bereichs des Rohres in einer Aufspannung erfolgen.
- Verfahren nach Anspruch 3, dadurch gekennzeichnet, daß das axiales Stauchen und das radiale Schmieden des erwärmten Bereichs des Rohres in einem Arbeitsschritt erfolgen.
- Verfahren nach einem der Ansprüche 1 bis 4, dadurch gekennzeichnet, daß während des axialen Stauchens und/oder während des radialen Schmiedens des erwärmten Bereichs des Rohres ein Dorn zumindest in einem Teil des erwärmten Bereichs eingeführt ist.
- Verfahren nach einem der Ansprüche 1 bis 5, dadurch gekennzeichnet, daß das Rohr einen Außendurchmesser aufweist, der dem größten Außendurchmesser des fertigen Bauteils entspricht.
- Verfahren zum Herstellen von rotationssymmetrischen Bauteilen aus einem Rohr, insbesondere von hohlen Monoblockwellen, wobei das Rohr anfangs einen konstanten Außendurchmesser und eine konstante Wandstärke aufweist und das rotationssymmetrische Bauteil zumindest über einen Bereich seiner Gesamtlänge einen davon abweichenden, insbesondere kleineren Außendurchmesser und/oder eine davon abweichende, insbesondere größere Wandstärke aufweist, gekennzeichnet durch folgende Verfahrensschritte:Verwendung eines geschweißten, nicht nachgezogenen Rohres mit einer
relativ großen Wandstärke undBearbeiten mindestens eines Bereichs des Rohres mittels Rundkneten bei
Raumtemperatur. - Verfahren nach Anspruch 7, dadurch gekennzeichnet, daß die Wandstärke des Rohres der kleinsten Wandstärke des fertigen Bauteils entspricht.
- Rotationssymmetrisches Bauteil, insbesondere hohle Monoblockwelle, mit einem über die Gesamtlänge des Bauteils variierendem Außendurchmesser und/oder einer variierender Wandstärke, dadurch gekennzeichnet, daß das Bauteil aus einem Rohr (2) mit einem konstanten Außendurchmesser (D1) und einer konstanten Wandstärke (d1) gemäß dem Verfahren nach einem der Ansprüche 1 bis 8 hergestellt worden ist.
- Rotationssymmetrisches Bauteil nach Anspruch 9, dadurch gekennzeichnet, daß ein Endbereich (3) oder beide Endbereiche des Bauteils einen geringeren Außendurchmesser (DE) und/oder eine größere Wandstärke (dE) als der Mittenbereich (4) des Bauteils aufweist bzw. aufweisen.
- Rotationssymmetrisches Bauteil nach Anspruch 9 oder 10, dadurch gekennzeichnet, daß der Mittenbereich (4) des Bauteils denselben Außendurchmesser (DM) und dieselbe Wandstärke (dM)wie das ursprüngliche Rohr (2) aufweist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10120392 | 2001-04-25 | ||
| DE10120392A DE10120392B4 (de) | 2001-04-25 | 2001-04-25 | Verfahren zum Herstellen von rotationssymmetrischen Bauteilen |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1252946A2 true EP1252946A2 (de) | 2002-10-30 |
| EP1252946A3 EP1252946A3 (de) | 2003-10-08 |
| EP1252946B1 EP1252946B1 (de) | 2006-04-12 |
Family
ID=7682753
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02002515A Expired - Lifetime EP1252946B1 (de) | 2001-04-25 | 2002-02-02 | Verfahren zum Herstellen von rotationssymmetrischen Bauteilen |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US7275407B2 (de) |
| EP (1) | EP1252946B1 (de) |
| JP (1) | JP2002321035A (de) |
| AT (1) | ATE322949T1 (de) |
| DE (2) | DE10120392B4 (de) |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1997569A1 (de) * | 2007-05-22 | 2008-12-03 | Benteler Automobiltechnik GmbH | Verfahren zur Bearbeitung der Enden von Rohren |
| CN100460138C (zh) * | 2004-08-19 | 2009-02-11 | 中国北车集团大同电力机车有限责任公司 | 法兰式台阶薄壁长套类锻件的整体随形锻造方法 |
| DE102007053551A1 (de) * | 2007-11-07 | 2009-05-28 | Rauschnabel, Eberhard, Dr.-Ing. | Verfahren zu Querschnittsveränderungen an Hohlteilen |
| DE102010015835A1 (de) | 2010-04-20 | 2011-10-20 | IFUTEC Ingenieurbüro für Umformtechnik GmbH | Verfahren zum maschinellen Herstellen von zylinderförmigen Werkstücken |
| CN102581153A (zh) * | 2012-01-06 | 2012-07-18 | 昌河飞机工业(集团)有限责任公司 | 一种收口拉杆加工方法 |
| CN101987343B (zh) * | 2009-08-07 | 2012-12-05 | 上海重型机器厂有限公司 | 核电设备锥形筒体的锻造方法 |
| DE102011086125B4 (de) * | 2010-12-07 | 2015-07-02 | Nsk Deutschland Gmbh | Rohrverdickungsverfahren, derart gefertigtes Lenkrohr und Fahrzeug mit derartigem Lenkrohr |
Families Citing this family (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20080061555A1 (en) * | 2005-02-16 | 2008-03-13 | Colin Knight | Flared cone fitting |
| US7776166B2 (en) * | 2006-12-05 | 2010-08-17 | Praxair Technology, Inc. | Texture and grain size controlled hollow cathode magnetron targets and method of manufacture |
| US20100068428A1 (en) * | 2007-05-26 | 2010-03-18 | Neumayer Tekfor Holding Gmbh | Method for Producing Hollow Shaft Base Bodies and Hollow Shaft Base Body Produced Thereby |
| US7922593B2 (en) * | 2008-10-23 | 2011-04-12 | American Axle & Manufacturing, Inc. | Driveshaft assembly |
| DE102012106423A1 (de) * | 2012-07-17 | 2014-01-23 | Benteler Automobiltechnik Gmbh | Verfahren zur Herstellung eines Rohrstabilisators für ein Kraftfahrzeug |
| KR101389193B1 (ko) | 2012-09-11 | 2014-04-24 | 현대위아 주식회사 | 등속조인트용 샤프트의 제조방법 |
| CN104668892B (zh) * | 2013-12-02 | 2018-01-16 | 江西昌河航空工业有限公司 | 直升机收口拉杆加工工艺方法 |
| DE102014014818B4 (de) * | 2014-04-06 | 2024-08-22 | IFUTEC Ingenieurbüro für Umformtechnik GmbH | Verfahrenskombination Warm-Kalt-Umformung von Hohlkörpern |
| EP3282025B1 (de) * | 2015-04-10 | 2026-07-22 | Tecniforja Forjagem e Estampagem de Peças Técnicas Lda. | Stahlwarmschmieden in einer horizontalen presse |
| JP6521914B2 (ja) * | 2016-07-26 | 2019-05-29 | トヨタ自動車株式会社 | 製造方法、スタビライザの製造方法およびスタビライザ製造用金型 |
| US11122741B2 (en) * | 2018-01-30 | 2021-09-21 | Cnh Industrial America Llc | Stalk roller assembly for an agricultural system |
| DE102018005356B4 (de) * | 2018-07-05 | 2026-03-19 | Neumayer Tekfor Engineering Gmbh | Verfahren und Herstellungsvorrichtung zur Herstellung eines Rohrs |
| KR102174259B1 (ko) * | 2018-09-28 | 2020-11-04 | 일진제강(주) | 업세팅 공법을 이용한 중공 드라이브 샤프트 및 이의 제조 방법 |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2054244A (en) * | 1936-07-10 | 1936-09-15 | William W Criley | Method of extruding socket forgings |
| US2133091A (en) * | 1936-10-07 | 1938-10-11 | Clark Equipment Co | Axle and method of forming same |
| US2256065A (en) * | 1939-10-21 | 1941-09-16 | Pittsburgh Steel Co | Tubular car axle and method for making it |
| US3564896A (en) * | 1965-09-03 | 1971-02-23 | North American Rockwell | Method of making axle beam |
| US3585832A (en) * | 1968-06-14 | 1971-06-22 | Battelle Development Corp | Metal working |
| DE1804673C3 (de) * | 1968-10-23 | 1985-02-07 | Benteler-Werke Ag, 4794 Schloss Neuhaus | Verfahren zur Herstellung einer Kraftfahrzeug-Hohlachse |
| DE2812803C2 (de) * | 1978-03-23 | 1982-11-18 | Laeis-Werke Ag, 5500 Trier | Vorrichtung zum Anstauchen von Rohrenden, insbesondere für Bohrgestängerohre mit Vorschweißverbindern |
| AT366938B (de) * | 1980-12-22 | 1982-05-25 | Gfm Fertigungstechnik | Verfahren zum herstellen oertlicher mantelverst[rkungen an hohlkoerpern |
| FR2498095A1 (fr) * | 1981-01-20 | 1982-07-23 | Vallourec | Procede de fabrication d'ebauches d'essieux creux en une seule piece et ebauches d'essieux obtenues |
| JPS63149038A (ja) * | 1986-12-15 | 1988-06-21 | Nippon Steel Corp | 外アツプセツト・プレスによる鋼管端部の加工方法 |
| DE19818653A1 (de) * | 1998-04-25 | 1999-10-28 | Bpw Bergische Achsen Kg | Verfahren zur Herstellung eines einteiligen Achskörpers sowie nach dem Verfahren hergestellter Achskörper |
-
2001
- 2001-04-25 DE DE10120392A patent/DE10120392B4/de not_active Withdrawn - After Issue
-
2002
- 2002-02-02 AT AT02002515T patent/ATE322949T1/de not_active IP Right Cessation
- 2002-02-02 DE DE50206354T patent/DE50206354D1/de not_active Expired - Fee Related
- 2002-02-02 EP EP02002515A patent/EP1252946B1/de not_active Expired - Lifetime
- 2002-02-26 JP JP2002050004A patent/JP2002321035A/ja active Pending
- 2002-04-25 US US10/131,138 patent/US7275407B2/en not_active Expired - Fee Related
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN100460138C (zh) * | 2004-08-19 | 2009-02-11 | 中国北车集团大同电力机车有限责任公司 | 法兰式台阶薄壁长套类锻件的整体随形锻造方法 |
| EP1997569A1 (de) * | 2007-05-22 | 2008-12-03 | Benteler Automobiltechnik GmbH | Verfahren zur Bearbeitung der Enden von Rohren |
| DE102007053551A1 (de) * | 2007-11-07 | 2009-05-28 | Rauschnabel, Eberhard, Dr.-Ing. | Verfahren zu Querschnittsveränderungen an Hohlteilen |
| CN101987343B (zh) * | 2009-08-07 | 2012-12-05 | 上海重型机器厂有限公司 | 核电设备锥形筒体的锻造方法 |
| DE102010015835A1 (de) | 2010-04-20 | 2011-10-20 | IFUTEC Ingenieurbüro für Umformtechnik GmbH | Verfahren zum maschinellen Herstellen von zylinderförmigen Werkstücken |
| DE102011086125B4 (de) * | 2010-12-07 | 2015-07-02 | Nsk Deutschland Gmbh | Rohrverdickungsverfahren, derart gefertigtes Lenkrohr und Fahrzeug mit derartigem Lenkrohr |
| CN102581153A (zh) * | 2012-01-06 | 2012-07-18 | 昌河飞机工业(集团)有限责任公司 | 一种收口拉杆加工方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| DE50206354D1 (de) | 2006-05-24 |
| US7275407B2 (en) | 2007-10-02 |
| US20020160844A1 (en) | 2002-10-31 |
| JP2002321035A (ja) | 2002-11-05 |
| ATE322949T1 (de) | 2006-04-15 |
| DE10120392A1 (de) | 2002-10-31 |
| EP1252946B1 (de) | 2006-04-12 |
| DE10120392B4 (de) | 2004-09-23 |
| EP1252946A3 (de) | 2003-10-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE10120392B4 (de) | Verfahren zum Herstellen von rotationssymmetrischen Bauteilen | |
| DE1804673C3 (de) | Verfahren zur Herstellung einer Kraftfahrzeug-Hohlachse | |
| EP1989011B1 (de) | Verfahren zur herstellung eines lenkspindelteils und lenkspindel mit einem solchen lenkspindelteil | |
| EP3924114B1 (de) | Verfahren und vorrichtung zum axialen umformen eines rohres | |
| DE102013226929A1 (de) | Verfahren und Vorrichtung zur Herstellung einer Hohlwelle durch Radialumformen sowie hiermit hergestellte Hohlwelle | |
| EP1702695B1 (de) | Verfahren zur Herstellung eines Übergangs an einem Hohlformteil | |
| DE69710640T2 (de) | Verfahren zur Erhöhung der Wanddicke von Metallrohren | |
| EP2992978A1 (de) | Matrizenmodulsatz für presswerkzeuge zum herstellen von schrauben | |
| WO2000068583A1 (de) | Blindniet für bauteile unterschiedlicher wandstärke und verfahren zum herstellen eines solchen blindniets | |
| DE102004001141B4 (de) | Verfahren zur Herstellung von Wellenzapfen und zur Herstellung einer gebauten Welle | |
| DE3019592C2 (de) | Vorrichtung zum Bearbeiten von Stahlrohren | |
| EP0014474B1 (de) | Verfahren zur Herstellung eines Rohres | |
| EP1464566B1 (de) | Verfahren zur Herstellung eines Hohlformteils mit geschlossenem Querschnitt und einer Verstärkung | |
| DE102007045855A1 (de) | Verfahren zur Herstellung von Rohr-in-Rohr-Systemen | |
| EP3737514B1 (de) | Verfahren und vorrichtung zum herstellen von hohlen, innengekühlten ventilen | |
| DE3506220A1 (de) | Verfahren zum herstellen von rohren mit dickwandigen enden durch kaltumformen eines rohrfoermigen rohlings | |
| EP2446980A2 (de) | Rohr und Verfahren zur Bearbeitung von Rohrenden | |
| DE10215415A1 (de) | Verfahren zum Herstellen von rotationssymmetrischen Bauteilen | |
| EP2706276A1 (de) | Innenwandig verstärktes Rohr und Verfahren zu dessen Herstellung | |
| DE102011107450A1 (de) | Vorrichtung und Verfahren zum Umformen eines Rohrs | |
| DE102020130222A1 (de) | Verfahren und Vorrichtung zur Herstellung von zumindest abschnittsweise profilierten rohrförmigen Bauteilen | |
| EP4046725A1 (de) | Verfahren zum herstellen einer stufenförmigen querschnittsverjüngung an einem einteiligen, rohrförmigen werkstück aus metall, damit hergestelltes einteiliges, rohrförmiges werkstück und vorrichtung zur durchführung des verfahrens | |
| DE102010008164A1 (de) | Verfahren zur Anbindung einer Rohrstabilisatorhälfte und Rohrstabilisator | |
| DE102016107240A1 (de) | Verfahren zur Herstellung einer Schiebemuffe für eine Schaltgetriebe-Synchronbaugruppe sowie mittels des Verfahrens hergestellte Schiebemuffe | |
| DE102012110792B4 (de) | Umformverfahren zur Herstellung einer stufenförmigen Querschnittsverjüngung an einem rohrförmigen Werkstück aus Metall |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: 7B 21K 21/12 B Ipc: 7B 21K 1/12 A Ipc: 7B 21K 1/06 B Ipc: 7B 21K 1/10 B |
|
| AKX | Designation fees paid | ||
| 17P | Request for examination filed |
Effective date: 20040604 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |
|
| 17Q | First examination report despatched |
Effective date: 20040714 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20060412 Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060412 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060412 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060412 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060412 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 50206354 Country of ref document: DE Date of ref document: 20060524 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060712 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060712 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060723 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060912 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| ET | Fr: translation filed | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20060412 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20070116 Year of fee payment: 6 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20070206 Year of fee payment: 6 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 |
|
| 26 | Opposition filed |
Opponent name: DAIMLERCHRYSLER AG Effective date: 20070112 |
|
| PLAF | Information modified related to communication of a notice of opposition and request to file observations + time limit |
Free format text: ORIGINAL CODE: EPIDOSCOBS2 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| BERE | Be: lapsed |
Owner name: MUHR UND BENDER K.G. Effective date: 20070228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20070509 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060713 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20070109 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080202 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20081031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080902 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080229 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060412 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070202 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080202 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060412 |
|
| PLBP | Opposition withdrawn |
Free format text: ORIGINAL CODE: 0009264 |
|
| PLBD | Termination of opposition procedure: decision despatched |
Free format text: ORIGINAL CODE: EPIDOSNOPC1 |
|
| PLAM | Termination of opposition procedure: information related to despatch of decision modified |
Free format text: ORIGINAL CODE: EPIDOSCOPC1 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| R26 | Opposition filed (corrected) |
Opponent name: DAIMLERCHRYSLER AG Effective date: 20070112 |
|
| PLBM | Termination of opposition procedure: date of legal effect published |
Free format text: ORIGINAL CODE: 0009276 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION PROCEDURE CLOSED |
|
| 27C | Opposition proceedings terminated |
Effective date: 20100115 |