EP1264550A2 - Méthode et installation pour la manipulation d'un materiau d'enrobage d'un produit de l'industrie du tabac et méthode et installation pour ensurer l'authenticité de produits de l'industrie du tabac - Google Patents
Méthode et installation pour la manipulation d'un materiau d'enrobage d'un produit de l'industrie du tabac et méthode et installation pour ensurer l'authenticité de produits de l'industrie du tabac Download PDFInfo
- Publication number
- EP1264550A2 EP1264550A2 EP02011138A EP02011138A EP1264550A2 EP 1264550 A2 EP1264550 A2 EP 1264550A2 EP 02011138 A EP02011138 A EP 02011138A EP 02011138 A EP02011138 A EP 02011138A EP 1264550 A2 EP1264550 A2 EP 1264550A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- marking
- wrapping material
- radiation
- products
- image
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/26—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for marking or coding completed packages
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24C—MACHINES FOR MAKING CIGARS OR CIGARETTES
- A24C5/00—Making cigarettes; Making tipping materials for, or attaching filters or mouthpieces to, cigars or cigarettes
- A24C5/38—Machines combined with printing devices
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24C—MACHINES FOR MAKING CIGARS OR CIGARETTES
- A24C5/00—Making cigarettes; Making tipping materials for, or attaching filters or mouthpieces to, cigars or cigarettes
- A24C5/60—Final treatment of cigarettes, e.g. marking, printing, branding, decorating
- A24C5/601—Marking, printing or decorating cigarettes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B19/00—Packaging rod-shaped or tubular articles susceptible to damage by abrasion or pressure, e.g. cigarettes, cigars, macaroni, spaghetti, drinking straws or welding electrodes
- B65B19/02—Packaging cigarettes
- B65B19/22—Wrapping the cigarettes; Packaging the cigarettes in containers formed by folding wrapping material around formers
Definitions
- the invention relates to a method and a device for processing a wrapping material of a product the tobacco processing industry as well as a process and a system for checking the authenticity of products from the tobacco processing industry.
- counterfeit products which in the following also include piracy products are sometimes called easy to recognize and partly not even recognizable by experts.
- the invention is based on the object to specify a method and a device by means of which is possible quickly and easily and reliable way of packaging or tobacco products like adding elements to cigarettes with which it is possible to ascertain with certainty whether it is this is an original product or a counterfeit is.
- the appropriate to be attached or existing Elements to determine the authenticity of each Products are said to be very difficult themselves or can only be faked with great effort. After all, fakes of this are supposed to be relatively easy be recognizable.
- a corresponding method and a appropriate system to ensure authenticity of tobacco processing products, with which a corresponding review or assurance the authenticity of the products in a simple way and possible and relatively quickly and inexpensively is another object of the present Invention.
- the method according to the invention makes it possible to to generate appropriate markings by means of which the authenticity of the tobacco processing products Industry can be checked in a simple manner can.
- Under wrapping material in the context of this invention in particular topping paper, cigarette paper, box blanks, Wrapping film and packaging material in the general viewed.
- the geometric shape of the marking is preferably definable or predefinable. This can have a relatively simple shape, such as for example a cross like a Swiss flag; the However, marking can also be a very complex form exhibit.
- the shape comprises alternately acute and obtuse angles.
- the marker preferably has predeterminable characteristic features.
- the step of changing the area by area Wrapping material includes removing material is one Imitation of a corresponding marking is difficult to do to reach. If preferably a perforation in the The markings can also be generated as the otherwise usual perforation in, for example, cigarette paper Find use. Then it is not necessary or only partially necessary, further perforations, like this otherwise in the manufacture of It is common to provide cigarettes.
- the marking can be made more easily visible or is one automatic detection of the marking simplified.
- chemical change is especially a coloring, another, for example crystalline or amorphous structure as the starting material, the creation of new ones chemical compounds or, for example, an oxidation understood, whereby in particular, for example, the reflection coefficient of the wrapping material changes. If at melting of the envelope material in some areas happens, this can be done in a simple manner to be changed.
- lines of weakness Apply lines of weakness.
- the radiation is preferably focused in particular on the enveloping material or in a focus in the vicinity of the enveloping material. If the marking has an extent of up to 50 ⁇ m, it is difficult to produce it mechanically, for example by punching it out, so that copying of a corresponding marking by a counterfeiter is made more difficult. Such an expansion is usually generated with a CO 2 laser. When using a YAG laser, markings with an extension of 10 ⁇ m are also possible. Basically, the resolution, ie the sharpness of the edges of the marking, depends on the wavelength of the light used and the quality of the focusing optics used. The maximum possible resolution is approximately half the wavelength of the light used. It is therefore preferred to use a laser that emits short-wave radiation.
- the task is also carried out by a facility for Processing wrapping material of the tobacco processing industry Industry, comprising at least one radiation device, can be directed onto the enveloping material by means of the radiation is solved, at least by means of the radiation an area of the wrapping material can be processed, wherein a marker can also be generated, which is a geometric one Has shape, the outline of which partially discontinuous slope and / or convex and concave areas.
- the geometric shape is preferably definable or specifiable.
- the mark is in particular an area in the wrapping material in which the casing material has been changed mechanically, physically or chemically. For this purpose, for example, material ablated.
- the removal can be carried out as far as that a perforation is created or previously interrupted be so that material in the area of the marking remains.
- the marking can also be colored or comprise melting the wrapping material.
- a transport device for transporting the Envelope material If a transport device for transporting the Envelope material is provided, a number of Markings at different points on the wrapping material be attached. This set of markings, which can then be attached, can also be installed in a Type coding should be provided. This will be different Markings in a certain marking area applied or generated, which then for the corresponding products should be characteristic.
- the radiation device preferably comprises a laser, in particular a CO 2 laser, a YAG laser or an excimer laser. If the intensity and / or power density and / or energy density of the radiation can be controlled and / or selected, markings of a desired quality can be generated.
- the radiation device comprises an element specifying the shape of the marking.
- This embodiment of the invention is a given particularly easy to implement.
- the element preferably comprises an aperture and / or a Focusing.
- the element is a diffractive optical element.
- a diffractive optical element is disclosed, for example, in DE 195 11 393 A1. It deals is basically an optical element that creates a focus by diffraction. With an appropriate diffractive optical element, which in hereinafter also referred to as DOE, the various geometric shapes as markings be generated.
- DOE diffractive optical element
- the Figures 3 and 5 of DE 195 11 393 A1 referenced various focal spots in the form of a peripheral perforation represent.
- a cigarette rod machine is preferably one Filter attachment machine, a cigarette packaging machine and / or a film wrapping machine with an inventive Furnish.
- the task is also highlighted on a Wrapping material of the tobacco processing industry, comprehensive a geometric shape, the outline of which is partly a discontinuous slope and / or concave and includes convex areas.
- the Slope is discontinuous.
- a preferred one Embodiment alternate corners with pointed Angles and corners with obtuse angles.
- the embodiment is the largest diameter Marking in the range of less than or equal to 50 ⁇ m. This marking can also be reduced, so that, for example, the largest diameter in the range of approximately Is 10 ⁇ m. If the edges of the marking have a structure or have sharpness in the range from 150 to 350 nm, it is very difficult and expensive for counterfeiters, produce appropriate markings. Under structure or sharpness is particularly the degree of discontinuity on the edge, where physically one approximate discontinuity of the edge in the range of 150 nm to 350 nm is preferably achievable.
- the edge area or the inaccuracy of the edge extends over a path of 150 nm to 350 nm. Is preferred the mark a material weakening. If the mark is a perforation of the wrapping material, it is possible, for example only a few in the case of cigarette paper to provide additional perforations or even to provide no further perforations, so that putting the mark in place of the usual Perforations can be used, which means no more time to generate the mark or the perforation in the manufacture of cigarettes is necessary.
- the marking is particularly easy to recognize given if it has a color other than the wrapping material outside the mark.
- Preferably comprises a line of weakness of a wrapping material the tobacco processing industry several of the vorgen. Markings according to the invention. Regarding the Conceptual content of a line of weakness is applied to the Application 100 41 020.0 referenced to the applicant full reference is made. Preferably there is the line of weakness exclusively from the invention Marks.
- a rod-shaped product is preferably the tobacco processing product Industry, especially using a cigarette provided at least one marking according to the invention.
- a packaging of products is preferably the tobacco processing industry with at least one provided marking according to the invention.
- the marking according to the invention is preferably used for Authenticity testing of tobacco processing products Industry used.
- the task is further accomplished through a safeguard procedure the authenticity of tobacco processing products Industry, comprising the procedural steps of Sighting on a wrapping material of the products Marking and comparing the mark solved with the mark given for these products. For example, with a correspondingly large marking by the end user through simple viewing be determined whether there is a corresponding Marking of a sufficient quality is available to determine whether it is the one to be considered Cigarette or packaging to be considered a real one Product and not a counterfeit. Under Sifting is particularly within the scope of this invention Recording, rearing and photography, in particular by means of a digital camera.
- Sifting is preferably carried out by means of an enlarging device such as a reading magnifier or a microscope or a magnifying lens.
- the viewed image is saved, is an automation of the method according to the invention easily possible. If in a subsequent Image processing the marker saved as an image is standardized to a standard size, is a comparison with predefined markings easily possible. If preferred comparing by comparing the sighted marking of the stored image and / or standardized image with a specifiable, in particular stored further image happens is a very given a safe way to determine whether the Products are real or fake. If the further picture on a computer system remote from the sighting site is stored, for example, on a computer system of the manufacturer, is a very safe process to ensure or ascertain the authenticity of Products of the tobacco processing industry possible.
- the further picture is selected, the possibility of counterfeiting further restricted as the counterfeiters are typically don't know what other data related to of the respective marking are relevant.
- the others Data can be, for example, the brand name or a package stamp be entered into a computer system can be sent to a computer system can be selected by selecting the further image.
- a signal is preferably used as the result of the method for a real product or for a fake product output.
- the task is carried out by a system Ensuring the authenticity of tobacco processing products Industry with an image acquisition device and a storage device on which predefinable images are storable in memory, solved, one Data connection between the image recording device of the Storage device is provided and wherein a Comparison device is provided by means of a image recorded by the image recording device comparable to a memory content of the memory device and wherein an output device for output of comparison data is provided.
- comparison data in particular understood a signal that indicates whether it is a fake or an original or a real product.
- Comparative data can also Differential values such as squares of errors or superimposed images as added images or Difference images, by means of which a person such as a Customs officers or wholesalers can instantly tell if it is is a fake or a real product is.
- the image recording device preferably comprises a magnifying element. This is, for example, a microscope or a magnifying lens. If an image processing device is provided by means of the particular captured images can be digitized is one Automation of checking the authenticity of products the tobacco processing industry without further ado possible.
- the storage device comprises a database.
- the comparison device is in one Embodiment of the invention a computer.
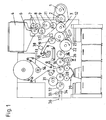
- Fig. 1 The machine shown in Fig. 1 is around a Hauni MAX filter attachment machine Maschinenbau AG, with one working with a laser Separation arrangement and a laser perforation arrangement.
- a Hauni MAX filter attachment machine Maschinenbau AG With one working with a laser Separation arrangement and a laser perforation arrangement.
- Such a machine is known, for example, from US Pat. No. 4,281,670 and DE 198 24 849 A1 known. She points out the following Details on.
- An infeed drum 1 transfers them to a cigarette manufacturing machine produced cigarettes in two Relay drums 2, which feed the staggered Unstack cigarettes and in rows of two with a space between the cigarettes to one Deliver assembly drum 3.
- the filter rods arrive from a magazine 4 onto a cutting drum 6 from two circular knives 7 to filter plugs double Cut to length of use, on a relay drum 8 staggered, from a sliding drum 9 to a row aligned plug aligned and from an accelerator drum 11 in the spaces between the Rows of cigarettes placed on the assembly drum 3.
- the cigarette filter cigarette groups are pushed together so that they lie axially close together. Then they are transferred from a transfer drum 12 accepted.
- a covering paper strip 13 is one Bobine 14 is drawn off by means of take-off rollers 16.
- the stripe 13 is around a sharp edge Prebreaker 17 steered around by a gluing device 18 glued and cut on a cutting drum 19.
- the separated covering sheets (connecting sheets) are attached to the cigarette filter groups on the transfer drum 12 attached and on a roller drum 22 by means of a rolling hand 23 around the cigarette filter groups rolled around.
- the finished groups of double filter cigarettes are a drying drum 24 one Cutting drum 26 fed and on this by center Cut through the filter plug Single filter cigarettes assembled, at the same time defective filter cigarettes are ejected.
- One with a transfer drum 27 and a collecting drum 28 cooperating turning device 29 turns one Row of filter cigarettes and simultaneously transfers them into via the transfer drum 27 and the collecting drum 28 continuous unturned filter cigarette row.
- a test drum 31 an ejection drum 32 on which before the ejection process in addition, the head scan of the filter cigarettes takes place.
- a depositing drum cooperating with a brake drum 33 34 places the filter cigarettes on a deposit belt 36th
- the device according to the invention is with the reference number 38 provided.
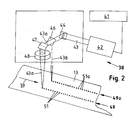
- the as an embodiment of the invention Perforating device 38 from FIG. 1 in a schematic represents perspective view.
- the perforating arrangement 38 has one of a control arrangement 41 controlled laser 42, which emits a pulsed laser beam 43.
- the Laser beam 43 is deflected by a deflecting mirror 44 and from a translucent mirror 46 into two of the same Partial beams 43a) and 43b) split.
- the partial beam 43b) is made by the partially transparent mirror 46 at the same time deflected towards the topping paper strip 13.
- On another mirror 47 directs the partially transparent Partial beam 43a) passing mirror 46 also for Covering paper strips 13 around.
- the partial beams 43a) and 43b) are separated by optics 48, only one of which is shown in FIG two traces of perforation 49 and 49a) on the covering paper strip 13 focused, where they perforations 51 or 51a) generate.
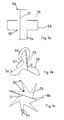
- the perforations 51 and 51a) are in Fig. 2 shown as circles or holes. As part of the Invention will be equivalent to the circles instead Perforations or markings made, for example. how the geometric shapes look, which are shown in fig. 3a) to 3c) are shown.
- Diffractive lenses are provided as optics 48 have a correspondingly predeterminable intensity profile.
- the intensity profile is such that an im substantially uniform intensity in the area of mark to be made exists, whereas outside this marking if possible no intensity at all should be present.
- Diffractive optical elements are basically in DE 198 24 849 A1 and DE 195 11 393 A1 discloses, it being possible without problems is to design these diffractive optics in this way or to calculate and produce that the desired Shape of the focal spots of the laser radiation on the envelope material is set. The revelation of these two Registrations should be fully in this registration be included.
- 3a) to 3c) are corresponding according to the invention Markings shown, as shown in Fig. 2, in rows 49 and 49a) for example on a covering paper strip 13 can be produced. These marks can but also on cigarette packs or wrapping material of cigarette packs or on cigarette paper.
- the corresponding invention Markers have different shapes on. In the case of FIG. 3a), the marking represents one Kind of cross, like this one in the Swiss flag can be seen.
- the area within the outline 58 is designed differently than the area outside the Outline 58. For example, some material can be inside the area 58 be removed, so that a Thinning of the wrapping material in the marking 55 given is.
- the 3a has several Areas of discontinuous slope 59 on as well relatively sharp edges 54.
- the one in the marking 55 The largest diameter D shown is, for example, in one Range between 10 ⁇ m and 50 ⁇ m depending on the used Laser. It should be assumed that such a sharp-edged marking not mechanically like is made possible, for example, by punching out.
- the mark can also be such that in the area of the outline 58 no wrapping material is left, so that there is a kind of perforation.
- FIG. 3b shows a different geometric shape Mark 55.
- convex areas 56 and concave areas 57 simultaneously in one marking intended.
- Fig. 3c) there is a marking accordingly represented in the form of a star shape, which due to the relatively fine structures even more difficult to copy is.
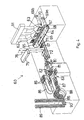
- FIG. 4 is three-dimensional in a very schematic form a cigarette packaging machine shown in the a device according to the invention is provided. It are cigarettes in a mass flow feed 61 Cigarette packing machine fed. These cigarettes fall through the feed chute 62 into block formation chutes 63. Of the block formation shafts 63 corresponding cigarettes in a known manner Bags 65 of a bag conveyor 64 transferred. To Transfer of cigarettes 66 from the block formation shaft in the respective pockets 65 is a drive element 69b) provided that an insertion plunger 70 emotional.
- the pocket conveyor 64 is by means of a Drive roller 68, which has a drive element 69a) is driven, cyclically, for example, in steps twice Division moves.
- a finished cigarette block 67 is then by means of a Block slide 71 in the effective area of an inner wrapping material strip 76 brought.
- the inside wrap strip 76 is in advance above the Engagement area with the cigarette blocks 67 by means of the removal device 75, which, for example, also a laser and appropriate optics includes, accordingly with the markings according to the invention have been provided.
- the removal device 75 which, for example, also a laser and appropriate optics includes, accordingly with the markings according to the invention have been provided.
- the removal device 75 which, for example, also a laser and appropriate optics includes, accordingly with the markings according to the invention have been provided.
- the removal device 75 which, for example, also a laser and appropriate optics includes, accordingly with the markings according to the invention have been provided.
- the block conveyor 72 further folding steps are taken.
- the corresponding folding organs and also other organs a corresponding cigarette packaging machine for the sake of simplicity and clarity 4 has been omitted.
- Cigarette blocks then come into the effective range of one first folding plate, in which this with a collar 80 in Be connected.
- a package consisting of one arrives Collar 80, which is on an inside wrap material provided cigarette block is arranged in a Transfer station 82, at which blankets 85 in Be connected with the package just mentioned, whereby when transferring from the 1st folding plate to the 2nd Folding plate already the first folding steps on the respective Blankets 85 are made.
- the blankets 85 are via a blanket conveyor 86 to the transfer station 82 fed.
- a corresponding Packaging machine is, for example, from DE 199 47 Applicant's 709.4, the United States patent application 09 / 678.671 corresponds, known.
- the corresponding almost completely folded blank sheets 85 provided Blocks of cigarettes via a pack conveyor 87 to one Drying drum 88 transferred.
- the still open side tabs provided with glue and folded onto the inside flaps.
- the glue is dried in the drying drum 88.
- the finished Cigarette packs 115 via a delivery conveyor 90 in Delivery chutes 89 transferred.
- the marking or the markings are applied to an inside wrap Service.
- these can also be in the area of the blank conveyor onto the blank be or at a later date on e.g. another wrapping material into which the finished Cigarette packs 115 can still be wrapped.
- FIG. 5 is a schematic representation of a Foil feed device with an inventive Device for generating corresponding markings shown.
- a strip of wrapping material a film strip 122 is on a bobbin 120 rolled up and is in the conveying direction 121 via a Deflection roller 123 finally in the engagement area of Brought cigarette packs with the foil too are enveloping.
- the film comes into the effective range of a laser beam 126 emitted by a laser 124 and is bundled via an optic 125, the optic 125
- the optic 125 For example, can be provided with an aperture, the corresponding a desired mark is formed.
- the laser preferably operated in a pulsed manner becomes.
- the film comes into the Area of a film cross cutter 127, which can be specified Place a cross section of the film so that appropriate film sections are generated.
- Foil sections are cigarette packs 115, which in the conveying direction 128 of the cigarette pack 115 is conveyed are initially introduced in the form of a U. Then the partially wrapped cigarette packets 115 transferred into folding pockets of folding turret 129, in which then the further required folding operations be carried out.
- Devices of the type designation IMPACT 3000 from Lumonics GmbH, Junkerstrasse 5, D-82178 Puchheim, DE, can be used. These are C02 lasers, which is a pulsed laser radiation with a very short Send out the beam duration and very high energy content can. Diffractive lenses are, for example, from Coherent, Inc., 2301 Lindberghstreet, Auburn, CA 95602, USA or Laser Components, Werner-von-Siemens-Strasse 15, D-82140 Olching.
- the control of the marking can also be different Way. For example. can with or without inexpensive tools such as a reading magnifier the end user himself determines whether there is any the corresponding marking is present.
- Fig. 6 schematically an inventive system for securing the authenticity of tobacco processing products Industry represents very sure to determine whether a counterfeit product is present or not.
- the image processing system comprises a test chamber 100, to which a microscope 101 is connected.
- a test chamber 100 can, for example, packs of cigarettes 115 be introduced.
- the ones on the cigarette packs 115 Markings applied can be viewed using microscope 101 taken enlarged by means of a digital camera 102 become.
- the digital image taken with the digital camera was recorded is connected via a connecting cable 103 fed to a computer 105.
- Via a monitor 106 the recorded image can then be displayed.
- a Keyboard 107 such as the brand name of the cigarettes or a possibly applied embossing, which, for example, can be a sequence of digits, can now, for example. marks present in the computer 105 that this Additional information should correspond with the recorded Image to be compared.
- the captured image or sample is digitized accordingly and if necessary with the additional information to a host computer 108, which also is a computer, via a data line or a Data cable 104 is transmitted.
- the computer 108 the for example at the manufacturer of the corresponding cigarettes can be set up, includes a hard disk 109 on the one for certain batches of cigarette packs Additional information such as the sequence of digits on the each pack can be shaped, stored. It can also be used for the respective brand name valid markings or combinations of different Markings using the data on the hard disk be assigned.
- the host computer can then do this be programmed so that by means of a correlation comparison, i.e.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Wrapping Of Specific Fragile Articles (AREA)
- Image Analysis (AREA)
- Manufacturing Of Cigar And Cigarette Tobacco (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10128043A DE10128043A1 (de) | 2001-06-08 | 2001-06-08 | Verfahren und Einrichtung zum Bearbeiten eines Füllmaterials eines Produkts der tabakverarbeitenden Industrie und Verfahren und System zur Sicherstellung der Echtheit von Produkten der tabakverarbeitenden Industrie |
| DE10128043 | 2001-06-08 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1264550A2 true EP1264550A2 (fr) | 2002-12-11 |
| EP1264550A3 EP1264550A3 (fr) | 2003-02-05 |
Family
ID=7687758
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02011138A Withdrawn EP1264550A3 (fr) | 2001-06-08 | 2002-05-21 | Méthode et installation pour la manipulation d'un materiau d'enrobage d'un produit de l'industrie du tabac et méthode et installation pour ensurer l'authenticité de produits de l'industrie du tabac |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20020185141A1 (fr) |
| EP (1) | EP1264550A3 (fr) |
| JP (1) | JP2003024034A (fr) |
| CN (1) | CN1396095A (fr) |
| DE (1) | DE10128043A1 (fr) |
| PL (1) | PL354306A1 (fr) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2006002719A1 (fr) * | 2004-06-29 | 2006-01-12 | Hauni Maschinenbau Ag | Procede et dispositif pour appliquer de la colle |
| RU2365316C2 (ru) * | 2004-04-07 | 2009-08-27 | Бритиш Америкэн Тобэкко (Джемени) Гмбх | Способ и устройство для маркировки одного или нескольких курительных изделий и упаковка для курительных изделий, содержащая одно или несколько маркированных курительных изделий |
| EP2359703A3 (fr) * | 2010-02-15 | 2014-12-17 | Hauni Maschinenbau AG | Machine à plusieurs tronçons pour la fabrication de produits de l'industrie de traitement de tabac et procédé de commande d'une machine à plusieurs tronçons |
| WO2017013635A1 (fr) * | 2015-07-23 | 2017-01-26 | Boegli-Gravures Sa | Procédé et dispositif d'application de caractéristiques d'identification à un ruban d'emballage afin d'authentifier l'emballage traité, emballage traité et emballage |
Families Citing this family (19)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20080022098A1 (en) * | 2005-09-30 | 2008-01-24 | Muscat Robert G | Authentication process |
| US20070075125A1 (en) * | 2005-09-30 | 2007-04-05 | Muscat Robert G | Packaging and process of authenticating packaging |
| ITBO20050595A1 (it) * | 2005-10-06 | 2006-01-05 | Gd Spa | Metodo e macchina per l'incarto di un prodotto in almeno un foglio di incarto |
| US20080154425A1 (en) * | 2006-04-27 | 2008-06-26 | Velociti Alliance North America, Inc. | Systems and methods for stamping packaged goods in the nature of cigarettes |
| US7933674B2 (en) * | 2006-04-27 | 2011-04-26 | Velociti Alliance North America, Inc. | Tobacco product stamping machine interface |
| US8760508B2 (en) | 2010-01-13 | 2014-06-24 | R.J. Reynolds Tobacco Company | Filtered smoking article inspection system, and associated method |
| US20120120229A1 (en) * | 2010-11-16 | 2012-05-17 | Rj Reynolds Tobacco Company | Cigarette package inspection system, and associated method |
| DE102010063523A1 (de) * | 2010-12-20 | 2012-06-21 | Hauni Maschinenbau Ag | Perforation von Zigaretten |
| US20130085052A1 (en) | 2011-09-29 | 2013-04-04 | R. J. Reynolds Tobacco Company | Apparatus for Inserting Microcapsule Objects into a Filter Element of a Smoking Article, and Associated Method |
| US8831764B2 (en) | 2011-10-17 | 2014-09-09 | R. J. Reynolds Tobacco Company | Cigarette package coding system and associated method |
| US9664570B2 (en) | 2012-11-13 | 2017-05-30 | R.J. Reynolds Tobacco Company | System for analyzing a smoking article filter associated with a smoking article, and associated method |
| US9844232B2 (en) | 2014-03-11 | 2017-12-19 | R.J. Reynolds Tobacco Company | Smoking article inspection system and associated method |
| US10063814B2 (en) | 2014-03-12 | 2018-08-28 | R.J. Reynolds Tobacco Company | Smoking article package inspection system and associated method |
| CH708200A8 (de) * | 2014-09-12 | 2015-03-13 | Boegli Gravures Sa | Verfahren und Vorrichtung zur Authentifizierung von Identifikations-Merkmalen auf einer Verpackungsfolie. |
| JP6662910B2 (ja) * | 2015-02-10 | 2020-03-11 | ジェイティー インターナショナル エス.エイ. | 物品のパッケージにマーキングするための方法および装置 |
| US10078029B2 (en) | 2015-08-14 | 2018-09-18 | R.J. Reynolds Tobacco Company | System for testing an article wrapped with an overwrap and associated method |
| DE102017119819A1 (de) * | 2017-08-29 | 2019-02-28 | Delfortgroup Ag | Verfahren zum Aufbringen von Registermarken auf Umhüllungspapier für Rauchartikel |
| CN108158037B (zh) * | 2017-12-25 | 2020-11-17 | 湖北金叶玉阳化纤有限公司 | 彩色聚乳酸纤维及制备烟用过滤嘴棒时彩色聚乳酸纤维的调节装置 |
| DE102024128975A1 (de) * | 2024-10-08 | 2026-04-09 | Körber Technologies Gmbh | Vorrichtung und ein Verfahren zum Bereitstellen einer Materialbahn |
Family Cites Families (21)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4281670A (en) * | 1977-06-13 | 1981-08-04 | Hauni-Werke Korber & Co. Kg | Apparatus for increasing the permeability of wrapping material for rod-shaped smokers products |
| DE2754104C2 (de) * | 1977-12-05 | 1987-01-15 | Hauni-Werke Körber & Co KG, 2050 Hamburg | Vorrichtung zum Herstellen einer Zone gewünschter Luftdurchlässigkeit in einem Hüllmaterialstreifen für stabförmige Artikel der tabakverarbeitenden Industrie |
| US4816824A (en) * | 1980-06-23 | 1989-03-28 | Light Signatures, Inc. | Merchandise verification and information system |
| US4463250A (en) * | 1981-07-11 | 1984-07-31 | Mcneight David L | Method and apparatus for use against counterfeiting |
| US4766911A (en) * | 1986-06-23 | 1988-08-30 | R. J. Reynolds Tobacco Company | Method for tracing smoking articles |
| GB8700765D0 (en) * | 1987-01-14 | 1987-02-18 | Wiggins Teape Group Ltd | Laser apparatus |
| DE4033300C2 (de) * | 1990-10-19 | 1994-06-23 | Gao Ges Automation Org | Mehrschichtiger, kartenförmiger Datenträger und Verfahren zur Herstellung desselben |
| DE4218266A1 (de) * | 1992-06-03 | 1993-12-09 | Hauni Werke Koerber & Co Kg | Vorrichtung zum Drehen von auf einem umlaufenden Förderer geförderten Zigaretten |
| DE19511393B4 (de) * | 1995-03-28 | 2005-08-25 | Carl Baasel Lasertechnik Gmbh | Gerät zur Substratbehandlung, insbesondere zum Perforieren von Papier |
| JPH11509781A (ja) * | 1996-04-26 | 1999-08-31 | セルビシオ インダストリアル ド マルカジェ イコディフィカシオン,エス.エイ. | マーキングまたはパーフォレーションのための装置と方法 |
| DE19722799A1 (de) * | 1997-05-30 | 1998-12-03 | Hauni Maschinenbau Ag | Verfahren zum Bearbeiten eines Streifens und Anordnung in einer Filteransetzmaschine |
| FR2765014B1 (fr) * | 1997-06-24 | 2000-02-11 | Rene Boulnois | Procede d'authentification d'un document en papier, document de securite en papier, et dispositif de controle de l'authenticite de documents en papier |
| US6442276B1 (en) * | 1997-07-21 | 2002-08-27 | Assure Systems, Inc. | Verification of authenticity of goods by use of random numbers |
| DE19736730A1 (de) * | 1997-08-22 | 1999-02-25 | Focke & Co | Gebindepackung für Zigaretten sowie Verfahren und Vorrichtung zum Herstellen derselben |
| US6172328B1 (en) * | 1998-02-17 | 2001-01-09 | Advanced Foliar Technologies, Inc. | Laser marking of plant material |
| DE19824849A1 (de) * | 1998-06-04 | 1999-12-09 | Hauni Maschinenbau Ag | Verfahren und Vorrichtung zum Bearbeiten eines Belagpapierstreifens |
| DE19939206A1 (de) * | 1999-08-18 | 2001-02-22 | Hauni Maschinenbau Ag | Verfahren und Vorrichtung zum Bearbeiten eines Hüllmaterials von Zigaretten |
| AUPQ273799A0 (en) * | 1999-09-08 | 1999-09-30 | Accudent Pty Ltd | Document authentication method and apparatus |
| DE10057623A1 (de) * | 1999-12-15 | 2001-06-21 | Topack Verpacktech Gmbh | Verfahren und Vorrichtung zum Ausbilden und Überführen von Blöcken von Zigaretten an eine mehrbahnige Packmaschine |
| DE10003674A1 (de) * | 2000-01-28 | 2001-08-02 | Hauni Maschinenbau Ag | Verfahren und Anordnung zum Herstellen eines aus mehreren Verpackungskomponenten gebildeten Verpackungsbehälters |
| US6333486B1 (en) * | 2000-04-25 | 2001-12-25 | Igor Troitski | Method and laser system for creation of laser-induced damages to produce high quality images |
-
2001
- 2001-06-08 DE DE10128043A patent/DE10128043A1/de not_active Withdrawn
-
2002
- 2002-05-21 EP EP02011138A patent/EP1264550A3/fr not_active Withdrawn
- 2002-06-06 PL PL02354306A patent/PL354306A1/xx unknown
- 2002-06-07 JP JP2002166974A patent/JP2003024034A/ja not_active Withdrawn
- 2002-06-08 CN CN02141908.6A patent/CN1396095A/zh active Pending
- 2002-06-10 US US10/164,704 patent/US20020185141A1/en not_active Abandoned
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| RU2365316C2 (ru) * | 2004-04-07 | 2009-08-27 | Бритиш Америкэн Тобэкко (Джемени) Гмбх | Способ и устройство для маркировки одного или нескольких курительных изделий и упаковка для курительных изделий, содержащая одно или несколько маркированных курительных изделий |
| WO2006002719A1 (fr) * | 2004-06-29 | 2006-01-12 | Hauni Maschinenbau Ag | Procede et dispositif pour appliquer de la colle |
| EP2359703A3 (fr) * | 2010-02-15 | 2014-12-17 | Hauni Maschinenbau AG | Machine à plusieurs tronçons pour la fabrication de produits de l'industrie de traitement de tabac et procédé de commande d'une machine à plusieurs tronçons |
| WO2017013635A1 (fr) * | 2015-07-23 | 2017-01-26 | Boegli-Gravures Sa | Procédé et dispositif d'application de caractéristiques d'identification à un ruban d'emballage afin d'authentifier l'emballage traité, emballage traité et emballage |
| EP3127435A1 (fr) * | 2015-07-23 | 2017-02-08 | Boegli-Gravures S.A. | Procédé et dispositif permettant d'appliquer des caractéristiques d'identification à un feuillard d'emballage afin d'authentifier le garnissage traité |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2003024034A (ja) | 2003-01-28 |
| EP1264550A3 (fr) | 2003-02-05 |
| US20020185141A1 (en) | 2002-12-12 |
| PL354306A1 (en) | 2002-12-16 |
| CN1396095A (zh) | 2003-02-12 |
| DE10128043A1 (de) | 2002-12-12 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE10128043A1 (de) | Verfahren und Einrichtung zum Bearbeiten eines Füllmaterials eines Produkts der tabakverarbeitenden Industrie und Verfahren und System zur Sicherstellung der Echtheit von Produkten der tabakverarbeitenden Industrie | |
| EP1463421B1 (fr) | Dispositif et systeme pour mesurer des proprietes de filtres a segments multiples et procede correspondant | |
| EP1561197B8 (fr) | Procede et dispositif pour caracteriser et verifier l'authenticite de produits | |
| DE2754104C2 (de) | Vorrichtung zum Herstellen einer Zone gewünschter Luftdurchlässigkeit in einem Hüllmaterialstreifen für stabförmige Artikel der tabakverarbeitenden Industrie | |
| DE102014004135A1 (de) | Vorrichtung zur Herstellung und/oder Verpackung von Produkten der Tabakindustrie | |
| EP0881026A2 (fr) | Procédé pour l'usinage de bande et dispositif d'une assembleuse cigarettes-filtres | |
| EP3239696A1 (fr) | Procédé de contrôle de cigarettes ou d'emballages de cigarettes | |
| EP2769632B1 (fr) | Procédé de mesure et dispositif de mesure pour l'enregistrement de la position d'un objet dans une tige de filtre transportée en direction axiale longitudinale et machine de l'industrie de traitement du tabac | |
| WO2003074361A1 (fr) | Installation de fabrication et d'emballage (de cigarettes), procede et dispositif de commande de ladite installation | |
| DE102010063523A1 (de) | Perforation von Zigaretten | |
| DE19753333A1 (de) | Verfahren zur Kontrolle der Vollzähligkeit von Zigarettengruppen und der Befüllung der Zigaretten | |
| DE10003674A1 (de) | Verfahren und Anordnung zum Herstellen eines aus mehreren Verpackungskomponenten gebildeten Verpackungsbehälters | |
| EP1836909B1 (fr) | Dispositif de perforation de l'industrie du traitement du tabac destiné à perforer une enveloppe d'un article en forme de tige | |
| DE60004486T2 (de) | Verpacken von rauchwaren | |
| EP2022347A1 (fr) | Contrôle optique de produits de l'industrie du traitement du tabac | |
| EP0962154A2 (fr) | Méthode et appareil pour traiter une de papier de recouvrement | |
| EP2996870A2 (fr) | Procédé et dispositif de fabrication d'emballages pour des produits à base de tabac | |
| DE10161424A1 (de) | Verfahren und Vorrichtung zum Erkennen von Produktfehlern bei der Herstellung von Briefhüllen, Versandtaschen und dergleichen | |
| DE102004040912A1 (de) | Optische Kontrolle von Produkten der Tabakverarbeitenden Industrie | |
| EP4106557B1 (fr) | Procédé et dispositif d'examen de produits en forme de tige de l'industrie des cigarettes | |
| DE102022124016A1 (de) | Verfahren und Vorrichtung zum Überprüfen einer Schnittfläche eines stabförmigen Heat-not-Burn-Produkts der Tabak verarbeitenden Industrie, Maschine der Tabak verarbeitenden Industrie und Verwendung | |
| DE4108166A1 (de) | Verfahren und vorrichtung zum perforieren von zigaretten | |
| DE10257143B4 (de) | Schnittkontrolle für eine Innenumhüllung für eine Zigarettengruppe | |
| WO2010072318A1 (fr) | Procédé et dispositif pour fabriquer des documents de sécurité | |
| DE102017007239A1 (de) | Verfahren und Vorrichtung zur Herstellung einstückiger, flächiger Zuschnittte aus einem faltbaren Material, insbesondere aus Geschenkpapier |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: 7G 07D 7/00 B Ipc: 7A 24C 5/60 B Ipc: 7A 24C 5/38 A |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO SI |
|
| 17P | Request for examination filed |
Effective date: 20030704 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| 17Q | First examination report despatched |
Effective date: 20040513 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20040924 |