EP1282557B1 - Procede et dispositif pour remplir un tube - Google Patents
Procede et dispositif pour remplir un tube Download PDFInfo
- Publication number
- EP1282557B1 EP1282557B1 EP01943332A EP01943332A EP1282557B1 EP 1282557 B1 EP1282557 B1 EP 1282557B1 EP 01943332 A EP01943332 A EP 01943332A EP 01943332 A EP01943332 A EP 01943332A EP 1282557 B1 EP1282557 B1 EP 1282557B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- tube
- filling
- die
- counterpart
- filling orifice
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 26
- 239000006071 cream Substances 0.000 claims abstract description 25
- 239000002674 ointment Substances 0.000 claims abstract description 5
- 239000006072 paste Substances 0.000 claims abstract description 5
- 239000000499 gel Substances 0.000 claims abstract description 3
- 239000004816 latex Substances 0.000 claims description 10
- 229920000126 latex Polymers 0.000 claims description 10
- 229910052782 aluminium Inorganic materials 0.000 claims description 6
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 6
- 239000000463 material Substances 0.000 claims description 3
- 229910052751 metal Inorganic materials 0.000 claims description 2
- 239000002184 metal Substances 0.000 claims description 2
- 239000007789 gas Substances 0.000 description 12
- 239000000945 filler Substances 0.000 description 10
- 230000008569 process Effects 0.000 description 8
- 238000003466 welding Methods 0.000 description 8
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 description 7
- 230000003647 oxidation Effects 0.000 description 7
- 238000007254 oxidation reaction Methods 0.000 description 7
- QVGXLLKOCUKJST-UHFFFAOYSA-N atomic oxygen Chemical compound [O] QVGXLLKOCUKJST-UHFFFAOYSA-N 0.000 description 4
- 230000008901 benefit Effects 0.000 description 4
- 230000008859 change Effects 0.000 description 4
- 230000001590 oxidative effect Effects 0.000 description 4
- 239000001301 oxygen Substances 0.000 description 4
- 229910052760 oxygen Inorganic materials 0.000 description 4
- 229910052757 nitrogen Inorganic materials 0.000 description 3
- 230000005489 elastic deformation Effects 0.000 description 2
- 239000003676 hair preparation Substances 0.000 description 2
- 239000003978 infusion fluid Substances 0.000 description 2
- 239000004922 lacquer Substances 0.000 description 2
- 239000012528 membrane Substances 0.000 description 2
- 239000004033 plastic Substances 0.000 description 2
- 230000001154 acute effect Effects 0.000 description 1
- 239000002519 antifouling agent Substances 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 238000004040 coloring Methods 0.000 description 1
- 238000011109 contamination Methods 0.000 description 1
- 230000006866 deterioration Effects 0.000 description 1
- 229910001873 dinitrogen Inorganic materials 0.000 description 1
- 238000002845 discoloration Methods 0.000 description 1
- 238000011038 discontinuous diafiltration by volume reduction Methods 0.000 description 1
- 230000007717 exclusion Effects 0.000 description 1
- 238000005429 filling process Methods 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 239000004920 heat-sealing lacquer Substances 0.000 description 1
- 230000001771 impaired effect Effects 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 230000003287 optical effect Effects 0.000 description 1
- 239000003973 paint Substances 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B7/00—Closing containers or receptacles after filling
- B65B7/14—Closing collapsible or resilient tubes, e.g. for tooth paste, for lighter fuel
Definitions
- the invention relates to a method for filling a tube with paste, ointment, Gel or cream, the tube being made of a tube or cone Sheath made of a flexible material, with a closable end Has filler opening and at the end opposite the filler opening is closed, whereby after filling the paste, ointment, cream or of the gel flattens the filling opening at least in its edge area, that Internal volume of the tube by means of a stamp deforming the jacket reduced and closes the filler opening.
- the invention relates in particular to the filling of aluminum or Laminate tubes with products that can be oxidized in the air, e.g. B. oxidative Color creams for coloring hair in hair cosmetics.
- B. oxidative Color creams for coloring hair in hair cosmetics It is known to be a to fill such a color cream tube in several steps. First, the empty tube gassed with nitrogen. Then the color cream from the bottom up, that is, starting with the still closed tube end. To a further gassing with nitrogen, the fill opening is flattened and folded by closing two jaws. The folding process takes place in in a manner known per se. To prevent air from entering later prevent an annular latex coating on the inside of the tube applied or a heat seal lacquer applied on the inside.
- the procedure of the type mentioned is from the German utility model DE 87 08 939 U1 known.
- a bag for a medical Infusion liquid after closing the container in it remaining air volume can be significantly reduced.
- the plastic container is done here in a first Welding process reduced the size of the filler opening.
- the Filling level due to an elastic deformation of the container in the filler neck raised in. It presses in the blow mold for the plastic bottle integrated stamp against the main part of the container shell, which clearly away from the filling opening and below the liquid level Infusion liquid is arranged.
- a second welding process the mouth opening remaining after the first welding process of the filler neck welded.
- a disadvantage of this known method is the effort required which is expressed on the one hand in the number of process steps.
- the necessary change in the filling device is also complex.
- a separate stamp with a Actuator and a corresponding drive can be attached.
- a control for driving the stamp must be installed which are necessary for maintaining a predetermined deformation of the Container provides. If the container is deformed too much, it will The contents of the container are pushed out of the filling opening so that a corresponding pollution of the tube filling system and a difficulty when welding the inside to the product Filler neck is the result.
- the invention is therefore based on the object of the method at the outset continue to develop in such a way that the volume of the remaining Gas space in the sealed tube on inexpensive, simple and problem-free manner is significantly reduced, with only minor modifications the bottling plant and no change in the filling process as well no change of the tube should be necessary.
- the tube has a triangular area adjacent to the filling opening
- the jacket presses against the opposite side of the jacket, the Point the triangle to the closed end of the tube.
- the deformation of the container is mainly in the area above the product, in the area of the gas fraction.
- the provided according to the invention Deformation can remain after the tube is finally closed because they are just the transition from the cylindrical part of the filled tube corresponds to the flat area and therefore not the aesthetic appearance impaired or relatively unremarkable.
- tubes on the inside the filling opening are coated in a ring with latex or the like. Such tubes are particularly airtight after folding and welding Area of the fold.
- the invention also relates to a device for performing the invention Procedure, with two opposite, towards and from each other away movable clinching jaws are provided. These clinching jaws are used for flattening and folding the filling opening of the tube.
- the above-mentioned object according to the invention is achieved here by that a stamp on one clinch jaw and a stamp on the other clinch jaw plate-shaped counterpart is attached.
- the clinching jaws move when closing the tube towards each other, the Covering the gas space of the tube to a predetermined extent compressed, the remaining gas content is significantly reduced.
- the container is not required.
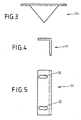
- the stamp be triangular in shape Has plate, the tip of the triangle pointing away from one clinching jaw.
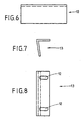
- the pressure surface of the stamp essentially parallel to the longitudinal axis of the device and the pressure surface of the Counterpart are arranged obliquely outwards with respect to this longitudinal axis.
- the longitudinal axis of the device is predetermined by the longitudinal axis of the tube.
- the counterpart prevents damage to the attached to the front of the tube, which is generally labeled wearing.
- the legs of the counterpart or Stamp are arranged at right angles to each other. But the legs can to each other at an acute angle of up to 45 °.
- the angles for the counterpart and the stamp are not identical in the Tegel, but the stamp has a right angle and the counterpart has a smaller one Angle on.
- the invention is particularly well suited for filling tubes with oxidative color creams used in hair cosmetics. Since there are often many here different color series and many different shades per color series are and different color series also different cream bases and correspondingly mean different volumes, this leads usefully to one used uniform tube size for all color series and Nuances to different filling levels of the tubes. Therefore, in one Case filled such a large volume in the tube, so that Product just not in the fold with the filling opening closed can reach. At the other extreme, however, the fill level is so low that a comparatively large gas space remains above the product. There a complete exclusion of atmospheric oxygen is technically not possible, it can to oxidation at the boundary layer in these oxidative color creams come. The result is a significant deterioration in the quality of the product, and the color-changed layer can be pressed out of the Tube lead to optical complaints by the customer.
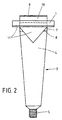
- Figure 1 shows a clamped between 2 clinching jaws (folding jaws) 1, 2 Tube 3 in a side view.
- the terms "front” and “Side view” refer to the finished, at its rear end flattened tube, the front of the tube being the main one Lettering bears.
- oxidative color cream 4 filled into the aluminum tube 3, which is completely closed in its lower area.
- the opening 6 of the Outlet port 5 is also in the usual way with an aluminum membrane tightly and gas-tightly closed. The membrane is opened the first time puncture the tube by the user.
- the gas space 7 above the color cream 4 was gassed with nitrogen, has an oxidation layer 8 on the due to residual oxygen Interface between the color cream 4 and the gas space 7 is formed.
- the latex layer 10 which is known per se, can also be seen on the inside the tube 3, which is almost immediately adjacent to the filling opening 9.
- the shape, size and curvature of the Stamp 11 and the counterpart 13 varied and optimized as required become.
- the advantages of the invention are in particular the reduction the color-changed oxidation layer. Because the color cream through the stamp 11 in the top corners of the tube 3, namely in the area of Folded, is pressed, the rejected oxidation layer can no longer the tube.
- the shape of the stamp 11 is chosen such that between the color cream 4 and the fold the necessary spare space is available, but is sufficiently small. Due to the geometric design of the stamp 11, it is largely exclude that the product undesirably with the latex layer 10 of the tube 3 comes into contact. This is achieved in that the Color cream 4 in the tube through the stamp 11 only in the two outermost Corners. This will result in a significantly lower product volume into the latex layer 10 at the end of the tube than at a maximum filling Tube without applying the invention. In addition, by attacking the Clinching jaws 1, 2 about 5 to 10 below the latex layer 10 and still once about 2 mm lower arrangement of the stamp 11 for this small Product quantity a sufficiently large reserve space available. In extreme Fluctuations in the filling levels, for example due to gas inclusions of the color cream itself, it is also possible to attach the stamp 11 to the clinching jaw 1 in such a way that it more or presses less on the tube coat.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Tubes (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Basic Packing Technique (AREA)
- Closing Of Containers (AREA)
Claims (9)
- Procédé pour remplir un tube (3) de pâte, de pommade, de gel ou de crème (4), le tube (3) étant constitué d'une enveloppe en manchon ou en cône réalisée en un matériau flexible, présentant à une extrémité une ouverture de remplissage (9) apte à être fermée et étant fermé à l'extrémité opposée à celle de l'ouverture de remplissage (9), dans lequel, après avoir rempli le tube de pâte, de pommade, de crème (4) ou de gel, on comprime à plat au moins la bordure de l'ouverture de remplissage (9), on réduit le volume intérieur du tube (3) au moyen d'un tampon (11) qui déforme l'enveloppe et on ferme l'ouverture de remplissage (9),
caractérisé en ce que l'on réduit le volume intérieur du tube (3) en même temps que l'on comprime à plat et que l'on ferme l'ouverture de remplissage (9). - Procédé selon la revendication 1, caractérisé en ce que pour réduire le volume intérieur du tube (3), on comprime contre le côté opposé de l'enveloppe une région triangulaire de l'enveloppe qui est adjacente à l'ouverture de remplissage (9), la pointe du triangle étant tournée vers l'extrémité fermée du tube (3).
- Procédé selon la revendication 1 ou 2, caractérisé en ce que le tube (3) est réalisé en métal et en particulier en aluminium.
- Procédé selon l'une des revendications précédentes, caractérisé en ce que l'on utilise des tubes (3) qui sont revêtus de latex (10) ou similaires en forme d'anneau sur le côté intérieur de l'ouverture de remplissage (9).
- Dispositif en vue de la mise en oeuvre du procédé selon l'une des revendications 1 à 4, avec deux mâchoires de pinçage (1, 2) qui peuvent être déplacées l'une par rapport à l'autre dans le sens d'un rapprochement ou d'un éloignement mutuels pour comprimer à plat et fermer l'ouverture de remplissage (9),
caractérisé en ce qu'un tampon (11) est installé sur l'une des mâchoires de pinçage(1), une pièce complémentaire (13) en forme de plaque étant installée sur l'autre des mâchoires de pinçage (2) pour réduire le volume intérieur du tube (3). - Dispositif selon la revendication 5, caractérisé en ce que le tampon (11) présente la forme d'une plaque triangulaire dont la pointe du triangle est tournée dans le sens opposé à la mâchoire de pinçage (1).
- Dispositif selon la revendication 5 ou 6, caractérisé en ce que le tampon (11) et la pièce complémentaire (13) sont reliées directement et rigidement à la mâchoire de pinçage (1, 2) respective.
- Dispositif selon l'une des revendications 5 à 7, caractérisé en ce que la surface de poussée du tampon (11) est disposée essentiellement parallèlement à l'axe longitudinal du dispositif et en ce que la surface de poussée de la pièce complémentaire (13) est disposée obliquement vers l'extérieur par rapport à cet axe longitudinal.
- Dispositif selon la revendication précédente, caractérisé en ce que la pièce complémentaire (13) respectivement le tampon (11) présentent des ailes qui forment un angle de 45° à 90°.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| SI200130074T SI1282557T1 (en) | 2000-05-17 | 2001-05-08 | Method for filling a tube and corresponding device |
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10024262A DE10024262C2 (de) | 2000-05-17 | 2000-05-17 | Verfahren zum Befüllen einer Tube und dazu geeignete Vorrichtung |
| DE10024262 | 2000-05-17 | ||
| PCT/EP2001/005192 WO2001087711A1 (fr) | 2000-05-17 | 2001-05-08 | Procede et dispositif pour remplir un tube |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1282557A1 EP1282557A1 (fr) | 2003-02-12 |
| EP1282557B1 true EP1282557B1 (fr) | 2003-12-10 |
Family
ID=7642446
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP01943332A Expired - Lifetime EP1282557B1 (fr) | 2000-05-17 | 2001-05-08 | Procede et dispositif pour remplir un tube |
Country Status (9)
| Country | Link |
|---|---|
| US (1) | US6772576B2 (fr) |
| EP (1) | EP1282557B1 (fr) |
| JP (1) | JP2003533409A (fr) |
| AT (1) | ATE256030T1 (fr) |
| DE (2) | DE10024262C2 (fr) |
| ES (1) | ES2215136T3 (fr) |
| PT (1) | PT1282557E (fr) |
| TR (1) | TR200400419T4 (fr) |
| WO (1) | WO2001087711A1 (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB201405591D0 (en) * | 2014-03-28 | 2014-05-14 | Ge Healthcare Ltd | Heatseal |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1975996A (en) * | 1932-08-04 | 1934-10-09 | Stokes Machine Co | Tube closing machine |
| US2300567A (en) * | 1939-01-16 | 1942-11-03 | Karl Kiefer Machine Company | Tube wall juxtaposing mechanism |
| US2503171A (en) * | 1944-11-13 | 1950-04-04 | Power John Kennedy | Method and apparatus for manufacturing containers |
| US2691474A (en) * | 1953-06-15 | 1954-10-12 | Edward A Olson | Method of and apparatus for forming a fluid-tight seal in thermoplastic material |
| US3037869A (en) * | 1958-12-31 | 1962-06-05 | American Can Co | Process for packing comestibles in a thin walled metal tube |
| US4351692A (en) * | 1981-01-07 | 1982-09-28 | Ouellette Machinery Systems | Apparatus and method for automatically filling and heat weld sealing lengths of plastic tubing |
| DE8708939U1 (de) * | 1987-06-27 | 1987-11-26 | Hansen, Gerhard, 74429 Sulzbach-Laufen | Vorrichtung zum Befüllen und anschließenden Verschweißen eines Behälters |
| FR2633249B1 (fr) * | 1988-06-28 | 1990-11-02 | Valois Sa | Procede de conditionnement sous vide de liquides et de pates en tube souple avec valve ou pompe de distribution et dispositif pour sa mise en oeuvre |
| FR2639903B1 (fr) * | 1988-12-05 | 1991-05-10 | Cebal | Procede et dispositif de fermeture d'un tube souple apres remplissage |
| US5714023A (en) * | 1996-02-23 | 1998-02-03 | Wheaton Holdings, Inc. | Method for sealing two compartment containers |
-
2000
- 2000-05-17 DE DE10024262A patent/DE10024262C2/de not_active Expired - Fee Related
-
2001
- 2001-05-08 AT AT01943332T patent/ATE256030T1/de not_active IP Right Cessation
- 2001-05-08 EP EP01943332A patent/EP1282557B1/fr not_active Expired - Lifetime
- 2001-05-08 ES ES01943332T patent/ES2215136T3/es not_active Expired - Lifetime
- 2001-05-08 WO PCT/EP2001/005192 patent/WO2001087711A1/fr not_active Ceased
- 2001-05-08 TR TR2004/00419T patent/TR200400419T4/xx unknown
- 2001-05-08 DE DE50101145T patent/DE50101145D1/de not_active Expired - Fee Related
- 2001-05-08 JP JP2001584123A patent/JP2003533409A/ja active Pending
- 2001-05-08 PT PT01943332T patent/PT1282557E/pt unknown
-
2002
- 2002-10-31 US US10/284,925 patent/US6772576B2/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| EP1282557A1 (fr) | 2003-02-12 |
| WO2001087711A1 (fr) | 2001-11-22 |
| PT1282557E (pt) | 2004-04-30 |
| US20030061789A1 (en) | 2003-04-03 |
| US6772576B2 (en) | 2004-08-10 |
| ATE256030T1 (de) | 2003-12-15 |
| DE10024262A1 (de) | 2001-12-20 |
| ES2215136T3 (es) | 2004-10-01 |
| TR200400419T4 (tr) | 2004-03-22 |
| DE50101145D1 (de) | 2004-01-22 |
| DE10024262C2 (de) | 2002-06-13 |
| JP2003533409A (ja) | 2003-11-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3802314C1 (fr) | ||
| DE69311019T2 (de) | Austragsvorrichtung für Medien und deren Herstellungsverfahren | |
| DE68902962T2 (de) | Verfahren zum vakuumverpacken von fluessigkeiten und pasten in weichen, mit abgabeventil oder -pumpe versehenen tuben und vorrichtung zur durchfuehrung dieses verfahrens. | |
| DE3202275A1 (de) | Einhandbetaetigter behaelter zur abgabe gleicher oder verschiedener volumenmengen viskoser fuellgueter sowie seine befuellung | |
| EP1027268B1 (fr) | Procede de production d'une bombe a aerosol presentant deux chambres, et dispositif pour mettre en oeuvre ledit procede | |
| DE2810899A1 (de) | Verfahren zur herstellung und fuellung eines behaelters, wie becher oder flasche, aus kunststoff | |
| DE102010038031B4 (de) | Verfahren zur Herstellung einer Bördelkappe, Bördelkappe und Behältnis | |
| EP0017147A1 (fr) | Récipient sous pression à deux compartiments pour distribuer un produit | |
| EP0011822A1 (fr) | Dispositif de fermeture à charnière pour récipient compressible | |
| DE10024262C2 (de) | Verfahren zum Befüllen einer Tube und dazu geeignete Vorrichtung | |
| DE1761083C3 (de) | Verpackung für flüssige, unter Druck stehende Füllgüter | |
| DE19809255B4 (de) | Kartusche zur Aufnahme einer viskosen oder pastösen Masse | |
| EP3829992B1 (fr) | Emballage de tube | |
| WO2004058597A1 (fr) | Bombe aerosol partiellement ovale | |
| DE2918429C2 (de) | Vorrichtung zum Verschließen eines Behälters | |
| DE2211652C3 (de) | Presse zum hydrostatischen Strangpressen von Rohren | |
| DE2264120A1 (de) | Rohrfoermiger behaelter, z.b. zahnpastatube, sowie verfahren und vorrichtung zu seiner herstellung | |
| DE2454832A1 (de) | Einrichtung zum befestigen eines mundstuecks an einem behaelter | |
| EP2114784A1 (fr) | Fermeture de tube | |
| DE4418394C2 (de) | Kartusche | |
| DE2063402C3 (de) | Verfahren, Vorrichtung und Folie zum Herstellen von einseitig offenen Behältern aus thermoplastischer Kunststorfolie | |
| DE2133117C3 (de) | Vorrichtung zum Füllen eines Behälters mit Gas | |
| DE10223842A1 (de) | Matrjoschka-Tube | |
| DE19940614C2 (de) | Verfahren und Vorrichtung zum Füllen von Behältnissen für fließfähige Medien | |
| EP0708033A1 (fr) | Récipient d'emballage composé d'un film tubulaire obturé à ses deux extrémités |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20021108 |
|
| AK | Designated contracting states |
Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: SI |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE TR |
|
| AX | Request for extension of the european patent |
Extension state: SI |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50101145 Country of ref document: DE Date of ref document: 20040122 Kind code of ref document: P |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20040302 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040310 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20040400922 Country of ref document: GR |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: HANS SCHWARZKOPF & HENKEL GMBH & CO. KG |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20040309 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040508 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20031210 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040531 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20040507 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: PD4A Free format text: HANS SCHWARZKOPF & HENKEL GMBH & CO. KG DE Effective date: 20040507 |
|
| NLT2 | Nl: modifications (of names), taken from the european patent patent bulletin |
Owner name: HANS SCHWARZKOPF & HENKEL GMBH & CO. KG |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2215136 Country of ref document: ES Kind code of ref document: T3 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040913 |
|
| REG | Reference to a national code |
Ref country code: SI Ref legal event code: IF |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GR Payment date: 20050413 Year of fee payment: 5 |
|
| NLT1 | Nl: modifications of names registered in virtue of documents presented to the patent office pursuant to art. 16 a, paragraph 1 |
Owner name: HANS SCHWARZKOPF & HENKEL GMBH & CO. KG |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20050502 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20050503 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20050504 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20050506 Year of fee payment: 5 Ref country code: DE Payment date: 20050506 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20050511 Year of fee payment: 5 Ref country code: AT Payment date: 20050511 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050531 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050531 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20050624 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20050714 Year of fee payment: 5 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060508 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060508 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060509 Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060509 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060531 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20060531 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061108 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061201 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061201 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MM4A Free format text: LAPSE DUE TO NON-PAYMENT OF FEES Effective date: 20061108 |
|
| EUG | Se: european patent has lapsed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20060508 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20061201 |
|
| REG | Reference to a national code |
Ref country code: SI Ref legal event code: KO00 Effective date: 20070122 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20070131 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20060509 |
|
| BERE | Be: lapsed |
Owner name: HANS *SCHWARZKOPF & HENKEL G.M.B.H. & CO. K.G. Effective date: 20060531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061205 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070508 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 |