EP1428654A1 - Verfahren zur Herstellung von mehrlagigen Tissuepapieren und mehrlagige Tissuepapiere - Google Patents
Verfahren zur Herstellung von mehrlagigen Tissuepapieren und mehrlagige Tissuepapiere Download PDFInfo
- Publication number
- EP1428654A1 EP1428654A1 EP02027415A EP02027415A EP1428654A1 EP 1428654 A1 EP1428654 A1 EP 1428654A1 EP 02027415 A EP02027415 A EP 02027415A EP 02027415 A EP02027415 A EP 02027415A EP 1428654 A1 EP1428654 A1 EP 1428654A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- plies
- embossing
- ply
- tissue paper
- protrusions
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000000034 method Methods 0.000 title claims abstract description 39
- 238000010030 laminating Methods 0.000 title claims abstract description 6
- 238000004049 embossing Methods 0.000 claims abstract description 102
- 238000006073 displacement reaction Methods 0.000 claims abstract description 23
- 239000003292 glue Substances 0.000 claims description 13
- 239000000853 adhesive Substances 0.000 claims description 9
- 230000001070 adhesive effect Effects 0.000 claims description 9
- 238000003466 welding Methods 0.000 claims description 3
- 239000000123 paper Substances 0.000 description 44
- 229910000831 Steel Inorganic materials 0.000 description 6
- 239000010959 steel Substances 0.000 description 6
- 238000012986 modification Methods 0.000 description 4
- 230000004048 modification Effects 0.000 description 4
- 230000006870 function Effects 0.000 description 3
- 238000004519 manufacturing process Methods 0.000 description 2
- 230000035807 sensation Effects 0.000 description 2
- 238000004804 winding Methods 0.000 description 2
- 230000000052 comparative effect Effects 0.000 description 1
- 238000007796 conventional method Methods 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 210000003746 feather Anatomy 0.000 description 1
- 239000002657 fibrous material Substances 0.000 description 1
- 230000005484 gravity Effects 0.000 description 1
- 238000007373 indentation Methods 0.000 description 1
- 239000002655 kraft paper Substances 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 238000004806 packaging method and process Methods 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- 235000012773 waffles Nutrition 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F—MECHANICAL WORKING OR DEFORMATION OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31F1/00—Mechanical deformation without removing material, e.g. in combination with laminating
- B31F1/07—Embossing, i.e. producing impressions formed by locally deep-drawing, e.g. using rolls provided with complementary profiles
Definitions
- the present invention relates to a process for laminating plies of tissue paper according to the preamble of claim 1, and to a laminated tissue paper according to the preamble of claim 10.
- Embossment patterns are produced by feeding tissue plies through at least one embossing unit. Subsequently; the tissue plies are generally ply bonded to produce, for example, a 2-ply or a 4-ply tissue paper.
- the creation of bulk by embossing is limited by various factors.
- the depth of the pattern, the hardness of the backing roll in an embossing unit for steel/rubber embossing, the type of embossing pattern, if union embossing is used and, last but not least, the tissue paper itself are all factors which can limit the bulk that is achievable in a hygiene paper product.
- EP-A-0,344,056 describes a process and apparatus for producing a multi-ply embossed fibrous sheet. Separate non-woven fibrous webs are combined into a multi-ply sheet before embossment, embossed as a multi-ply sheet, the embossed webs separated from one another and longitudinally displaced relative to one another, and then recombined into an embossed multi-ply sheet with the embossments out of register with one another.
- the disclosed process results in a multi-ply sheet with a thickness essentially the same as that embossed with the same pattern and not separated and recombined in a displaced manner after embossing.
- US 3,668,055 discloses superimposed embossed packaging sheets. A series of sheets of relatively heavy paper or similar matted fibrous materials are embossed and then passed through shorter or longer paths of travel before again being assembled so that their matching mounds and recesses are offset in such a manner that they no longer match.
- the disclosed method is, however, designed for kraft paper and is not suitable for tissue paper.
- the object underlying the present invention is to provide a process for laminating plies of tissue paper, as well as a laminated tissue paper, of the above mentioned kind, wherein bulk is increased in an easy manner.
- At least two plies of tissue as it is used for manufacturing hygiene paper products, for example toilet paper, household towels, or the like, are embossed with one and the same embossing nip. Both plies are provided with substantially the same embossing pattern consisting of embossing protrusions.
- the protrusions of the ply which is nearest to the embossing roll stack backwards into the indentations (protrusions) of the second ply.
- the generated bulk of the paper depends on the height of the protrusions, i.e. the embossing depth.
- the maximum distance D in the displacement direction between an embossing protrusion of a first ply and an embossing protrusion of a second ply, which has been displaced relatively to said first ply is set as a function of the height H of the embossing protrusions and the length L of the embossing protrusions in the displacement direction of the two plies, so that D is equal to the smaller one of the values of 12H and 14L.
- the embossing displacement can be subsequently fixed by any conventional, well-known ply bonding technique.
- the resulting laminated tissue paper has an increased thickness, which creates more volume in the product.
- the embossing protrusions of the respective tissue plies are reliably prevented from nesting, and the recombined tissue paper has an increased volume as compared to the two plies the protrusions of which are in register, before having displaced the plies.
- the defined distance D in the displacement direction between an embossing protrusion of a first ply and an embossing protrusion of a second ply prevents the unembossed areas on one ply from being pressed down under the effect of gravity by the embossing protrusions of the other ply.
- the higher bulk gives an improved sensation of bulk softness, a critical feature for the feeling of softness.
- the increase in thickness moreover creates a textile-like appearance which is a very desirable feature of high quality tissue paper products.
- the embossing protrusions will extend outwards. This might slightly impair the aesthetic appearance and the haptics of the product. To avoid this, another ply, either unembossed or embossed, can be joined to the laminate. In case an embossed ply is used, the embossing protrusions thereof ought to be directed inwards.
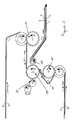
- Fig. 1 shows a first embodiment of an apparatus for carrying out the process according to the invention.
- the apparatus serves for embossing and combining four plies 1, 2, 3, 4 of tissue in the form of a fibrous web, and operates as follows.
- Two plies 1, 2 are combined and fed to a bottom embossing roll 10 by means of which they are embossed in combination.
- the two plies 1, 2 are embossed with one and the same nip and, therefore, provided with the same embossing pattern consisting of embossing protrusions.
- the protrusions of the ply 2 which is nearer to the embossing roll 10 stack into the protrusions of the other ply 1.
- embossed tissue plies 1, 2 are then separated and displaced relatively to one another so that the embossing protrusions are not in register with each other.
- this displacement or phase difference between plies 1 and 2 is effected by passing ply 1 over a deviating roll 15 so that it travels along a longer path than ply 2.
- plies 1, 2 are recombined at a merging roll which, in this case, is a design roll 20.
- a merging roll which, in this case, is a design roll 20.
- two further plies 3, 4 are fed to a top embossing roll 11 and are also embossed in combination. Afterwards, they are also fed to the design roll 20.
- a glue application roll 30 is provided for applying glue to the upper one of the plies 3, 4.
- design roll 20 can also correspond to a further embossing roll to apply a further embossing pattern to all the plies 1 to 4.
- the plies 3, 4 are fixed to the previously mentioned plies 1, 2 at a marrying roll 40.
- the resultant 4-ply sheet, comprising the two embossed, relatively displaced plies 1, 2 and the two further plies 3, 4 which are also embossed, is then discharged from the apparatus.
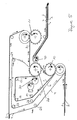
- FIG. 2 is a modification of the process of Fig. 1.
- the further plies 3, 4 are also separated and displaced relatively to each other, in a similar manner as in the case of ply 1.
- the bulk of the plies 3, 4 is increased so that the overall bulk of the resultant 4-ply tissue is even greater than that produced in the apparatus of Figure 1.
- one of the first plies 1, 2 can also be directed to the glue application roll 30 by means of further deviating rolls 17, 18 and 19. Glue is then applied to ply 1 before ply 1 is recombined with ply 2, to ply bond plies 1 and 2.
- Figure 4 shows a fourth inventive embodiment in an arrangement wherein plies 1, 2 and 4 are simultaneously fed to the bottom embossing roll 10, while only ply 3 is fed to the top embossing roll 11.
- the same embossing pattern is applied to plies 1, 2 and 4, while a different pattern may be applied to ply 3.
- plies 1, 2 and 4 are separated by means of deviating rolls 15 and 17, 18, 19 and 21, respectively, and glue is applied to ply 4 by means of the glue application roll 30.
- the four plies 1, 2, 3, 4 are then recombined at the design roll 20 and marrying roll 40.
- Figure 5 shows, as a fifth embodiment, a similar arrangement to that of Fig. 4 wherein, however, ply 1 is directed to the glue application roll 30 by means of deviating rolls 17, 18 and 19, whereas ply 4, after having been embossed together with plies 1 and 2, is fed directly to the design roll 20 by means of deviating rolls 22, 23 and 24.
- the embossed tissue paper has a base plane, i.e. the plane of the unembossed parts of the paper, and embossing protrusions protruding there from.
- the height H of the embossing protrusions from the base plane to the top of the protrusion may be measured by means of a so-called UBM measuring method such as disclosed in WO-A-00/63489, which is incorporated herein by reference. According to such a method, a cross section of the paper is measured. The length L of the protrusions is measured in the base plane.
- base tissue The abbreviations in the column “base tissue” have the following meaning, the base tissues being manufactured by SCA Hygiene Products GmbH, Mannheim, Germany:
- embossing combination shows which embossing and design rolls were used, the embossing designs being those used by SCA Hygiene Products GmbH, Mannheim, Germany:
- the embossing patterns falling within the scope of the present invention can be of any conventional design.
- the embossing protrusions have dimensions ususally up to about 5 mm in the machine and cross machine directions. However, certain embossing patterns can also have dimensions up to about 20 mm in length in the machine direction and about 2 mm in the cross machine direction. Additionally, the embossing protrusions can extend at an angle to the machine direction. The height of the embossing protrusions can be about 1 mm to 2 mm. Naturally, however, the dimensions and shapes of the embossing protrusions are not limited to the examples given and are well known in the art.
- the plies of the laminated tissue paper and the laminated tissue paper product may be plybonded with mechanical or adhesive plybonding as known in the art.
- Mechanical plybonding as known in the art can be achieved by application of a high pressure, e.g. in an additional embossing nip.
- ultrasonic welding for plybonding a method that is explained in the US pending provisional patent application No. 60/341803.
- the glue can, for example, be added to all the protrusions of one ply or with a structured glue application roller to just some of the protrusions.
- the paper can also be further embossed in a further embossing nip, for example by giving the paper an embossed spot pattern.
- a further embossing nip for example by giving the paper an embossed spot pattern.
- spot protrusions will be covered with glue and will be the part that bonds to the other plies.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Machines For Manufacturing Corrugated Board In Mechanical Paper-Making Processes (AREA)
- Paper (AREA)
- Sanitary Thin Papers (AREA)
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP02027415A EP1428654A1 (de) | 2002-12-09 | 2002-12-09 | Verfahren zur Herstellung von mehrlagigen Tissuepapieren und mehrlagige Tissuepapiere |
| EP03772330A EP1572443A1 (de) | 2002-12-09 | 2003-11-12 | Verfahren zur herstellung von mehrlagigen tissuepapieren und mehrlagige tissuepapiere |
| PL03375730A PL375730A1 (en) | 2002-12-09 | 2003-11-12 | Process for laminating plies of tissue paper and laminated tissue paper |
| PCT/EP2003/012650 WO2004052635A1 (en) | 2002-12-09 | 2003-11-12 | Process for laminating plies of tissue paper and laminated tissue paper |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP02027415A EP1428654A1 (de) | 2002-12-09 | 2002-12-09 | Verfahren zur Herstellung von mehrlagigen Tissuepapieren und mehrlagige Tissuepapiere |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1428654A1 true EP1428654A1 (de) | 2004-06-16 |
Family
ID=32319554
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP02027415A Withdrawn EP1428654A1 (de) | 2002-12-09 | 2002-12-09 | Verfahren zur Herstellung von mehrlagigen Tissuepapieren und mehrlagige Tissuepapiere |
| EP03772330A Ceased EP1572443A1 (de) | 2002-12-09 | 2003-11-12 | Verfahren zur herstellung von mehrlagigen tissuepapieren und mehrlagige tissuepapiere |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP03772330A Ceased EP1572443A1 (de) | 2002-12-09 | 2003-11-12 | Verfahren zur herstellung von mehrlagigen tissuepapieren und mehrlagige tissuepapiere |
Country Status (3)
| Country | Link |
|---|---|
| EP (2) | EP1428654A1 (de) |
| PL (1) | PL375730A1 (de) |
| WO (1) | WO2004052635A1 (de) |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1845193A1 (de) * | 2006-04-14 | 2007-10-17 | Georgia-Pacific France | Mehrlagiger saugfähiger Papierbogen, Rolle und Verfahren zu seiner Herstellung |
| US8309194B2 (en) | 2007-04-13 | 2012-11-13 | Georgia-Pacific France | Roll of sheets of absorbent product of the bathroom tissue type |
| US8383223B2 (en) | 2007-03-28 | 2013-02-26 | Georgia-Pacific France | Roll of fibrous cellulose-based product |
| US11363917B2 (en) * | 2017-06-30 | 2022-06-21 | Daio Paper Corporation | Toilet paper |
| EP4114240A4 (de) * | 2020-03-05 | 2023-11-29 | Kimberly-Clark Worldwide, Inc. | Geprägte mehrlagige tissueprodukte |
| EP4269690A3 (de) * | 2018-09-28 | 2024-01-03 | Kimberly-Clark Worldwide, Inc. | Geprägtes mehrlagiges tissueprodukt |
| US11987934B2 (en) | 2019-03-06 | 2024-05-21 | Kimberly-Clark Worldwide, Inc. | Embossed multi-ply tissue product |
| US12134863B2 (en) | 2019-03-06 | 2024-11-05 | Kimberly-Clark Worldwide, Inc. | Embossed multi-ply tissue product |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2014186043A1 (en) | 2013-03-15 | 2014-11-20 | Corrugated Synergies International, Llc | Establishing a registered score, slit or slot in corrugated board, and articles produced therefrom |
| US11420417B2 (en) | 2013-03-15 | 2022-08-23 | Scorrboard Llc | Methods and apparatus for producing scored mediums, and articles and compositions resulting therefrom |
| US10800133B2 (en) | 2016-04-20 | 2020-10-13 | Scorrboard, Llc | System and method for producing a facing for a board product with strategically placed scores |
| US10328654B2 (en) | 2016-04-20 | 2019-06-25 | Scorrboard, Llc | System and method for producing a multi-layered board having a medium with improved structure |
| US11027513B2 (en) | 2016-04-20 | 2021-06-08 | Scorrboard Llc | System and method for producing an articulating board product having a facing with score lines in register to fluting |
| US11027515B2 (en) | 2016-04-20 | 2021-06-08 | Scorrboard Llc | System and method for producing multi-layered board having at least three mediums with at least two mediums being different |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0344056A2 (de) * | 1988-05-24 | 1989-11-29 | James River Corporation Of Virginia | Verfahren und Gerät zum Herstellen eines mehrlagigen, geprägten Blattes aus faserigem Material |
| EP0905318A2 (de) * | 1997-09-26 | 1999-03-31 | Fort James Corporation | Weiches, saugfähiges, chemi-mechanisch geprägtes Papierprodukt, und Verfahren zu seiner Herstellung |
| US6245414B1 (en) * | 1995-12-05 | 2001-06-12 | Fabio Perini, S.P.A. | Embossing and laminating machine for gluing embossed layers |
-
2002
- 2002-12-09 EP EP02027415A patent/EP1428654A1/de not_active Withdrawn
-
2003
- 2003-11-12 EP EP03772330A patent/EP1572443A1/de not_active Ceased
- 2003-11-12 PL PL03375730A patent/PL375730A1/xx not_active Application Discontinuation
- 2003-11-12 WO PCT/EP2003/012650 patent/WO2004052635A1/en not_active Ceased
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0344056A2 (de) * | 1988-05-24 | 1989-11-29 | James River Corporation Of Virginia | Verfahren und Gerät zum Herstellen eines mehrlagigen, geprägten Blattes aus faserigem Material |
| US6245414B1 (en) * | 1995-12-05 | 2001-06-12 | Fabio Perini, S.P.A. | Embossing and laminating machine for gluing embossed layers |
| EP0905318A2 (de) * | 1997-09-26 | 1999-03-31 | Fort James Corporation | Weiches, saugfähiges, chemi-mechanisch geprägtes Papierprodukt, und Verfahren zu seiner Herstellung |
Cited By (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1845193A1 (de) * | 2006-04-14 | 2007-10-17 | Georgia-Pacific France | Mehrlagiger saugfähiger Papierbogen, Rolle und Verfahren zu seiner Herstellung |
| WO2007119003A1 (fr) * | 2006-04-14 | 2007-10-25 | Georgia-Pacific France | Feuille absorbante delitable multiplis, rouleau et procede de fabrication associes |
| US8182907B2 (en) | 2006-04-14 | 2012-05-22 | Georgia-Pacific France | Multi-ply disintegratable absorbent sheet, associated roll and associated manufacturing process |
| EA017694B1 (ru) * | 2006-04-14 | 2013-02-28 | Джорджия - Пасифик Франс | Расслаивающийся многослойный впитывающий лист, соответствующие рулон и способ производства |
| US9352527B2 (en) | 2006-04-14 | 2016-05-31 | Sca Tissue France | Multi-ply disintegratable absorbent sheet, associated roll and associated manufacturing process |
| US9643376B2 (en) | 2006-04-14 | 2017-05-09 | Sca Tissue France | Multi-ply disintegratable absorbent sheet, associated roll and associated manufacturing process |
| US8383223B2 (en) | 2007-03-28 | 2013-02-26 | Georgia-Pacific France | Roll of fibrous cellulose-based product |
| US8309194B2 (en) | 2007-04-13 | 2012-11-13 | Georgia-Pacific France | Roll of sheets of absorbent product of the bathroom tissue type |
| US11363917B2 (en) * | 2017-06-30 | 2022-06-21 | Daio Paper Corporation | Toilet paper |
| EP4269690A3 (de) * | 2018-09-28 | 2024-01-03 | Kimberly-Clark Worldwide, Inc. | Geprägtes mehrlagiges tissueprodukt |
| US12018439B2 (en) | 2018-09-28 | 2024-06-25 | Kimberly-Clark Worldwide, Inc. | Embossed multi-ply tissue product |
| AU2019350714B2 (en) * | 2018-09-28 | 2025-02-27 | Kimberly-Clark Worldwide, Inc. | Embossed multi-ply tissue product |
| US11987934B2 (en) | 2019-03-06 | 2024-05-21 | Kimberly-Clark Worldwide, Inc. | Embossed multi-ply tissue product |
| US12134863B2 (en) | 2019-03-06 | 2024-11-05 | Kimberly-Clark Worldwide, Inc. | Embossed multi-ply tissue product |
| US12281446B2 (en) | 2019-03-06 | 2025-04-22 | Kimberly-Clark Worldwide, Inc. | Embossed multi-ply tissue product |
| EP4114240A4 (de) * | 2020-03-05 | 2023-11-29 | Kimberly-Clark Worldwide, Inc. | Geprägte mehrlagige tissueprodukte |
Also Published As
| Publication number | Publication date |
|---|---|
| PL375730A1 (en) | 2005-12-12 |
| WO2004052635A1 (en) | 2004-06-24 |
| EP1572443A1 (de) | 2005-09-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5840404A (en) | Absorbent multilayer sheet and method for making same | |
| AU2012394470B2 (en) | Method for embossing a multi-ply paper product and an embossed multi-ply paper product | |
| US5727458A (en) | Method and apparatus for contour multi-level embossing with perforation bonding in selected spaced locations | |
| US7871692B2 (en) | Multi-ply tissue paper, paper converting device and method for producing a multi-ply tissue paper | |
| US4927588A (en) | Method multi-ply embossed fibrous sheet | |
| EP1911574B1 (de) | Papiermaterial mit verbessertem Prägemuster und Herstellungsverfahren dafür | |
| US8936845B2 (en) | Multiply thin paper sheet having press-to-bond structure | |
| US20040166290A1 (en) | Process for laminating plies of tissue paper and laminated tissue paper | |
| WO2004052635A1 (en) | Process for laminating plies of tissue paper and laminated tissue paper | |
| US20240229362A1 (en) | Tissue product and method and apparatus for producing same | |
| US20040163783A1 (en) | Method and device for producing a multi-ply web of flexible material, such as paper and nonwoven, and multi-ply material produced by the method | |
| EP2018959A2 (de) | Geprägtes Papiermaterial sowie Verfahren und Vorrichtung zu dessen Herstellung | |
| US20030026953A1 (en) | Multi-ply tissue paper product and method for producing same | |
| GB2376436A (en) | Multi-ply tissue paper and method for producing same. | |
| EP4166314A2 (de) | Verfahren zur herstellung eines tissueprodukts | |
| US20050147797A1 (en) | Device and method for joining layers for forming sheet products and resulting products | |
| JP7345443B2 (ja) | 家庭用薄葉紙及び家庭用薄葉紙の製造方法 | |
| EP0684132B2 (de) | Verfahren zur Herstellung eines mehrschichtigen Tissuepapierproduktes | |
| AU2005335397B2 (en) | Multi-ply tissue paper product and method for producing same | |
| US20070042209A1 (en) | Multi-ply planar absorbent product and process for manufacturing such a product | |
| WO2004028706A1 (en) | Method for producing a multi-ply web of flexible material, such as paper and nonwoven, and multi-ply material produced by the method | |
| HK40049586B (en) | Tissue product and method and apparatus for producing same | |
| HK40049021B (en) | Tissue product and method and apparatus for producing same |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR IE IT LI LU MC NL PT SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK RO |
|
| AKX | Designation fees paid | ||
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20041217 |