EP1493468B1 - Planche de sport de glisse comprenant un noyau en bambou - Google Patents
Planche de sport de glisse comprenant un noyau en bambou Download PDFInfo
- Publication number
- EP1493468B1 EP1493468B1 EP03028220A EP03028220A EP1493468B1 EP 1493468 B1 EP1493468 B1 EP 1493468B1 EP 03028220 A EP03028220 A EP 03028220A EP 03028220 A EP03028220 A EP 03028220A EP 1493468 B1 EP1493468 B1 EP 1493468B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- bamboo
- core
- board
- gliding sports
- sports according
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 235000017166 Bambusa arundinacea Nutrition 0.000 title claims abstract description 113
- 235000017491 Bambusa tulda Nutrition 0.000 title claims abstract description 113
- 241001330002 Bambuseae Species 0.000 title claims abstract description 113
- 235000015334 Phyllostachys viridis Nutrition 0.000 title claims abstract description 113
- 239000011425 bamboo Substances 0.000 title claims abstract description 113
- 239000000463 material Substances 0.000 claims abstract description 15
- 239000002023 wood Substances 0.000 claims abstract description 9
- 239000010410 layer Substances 0.000 claims description 59
- 238000010276 construction Methods 0.000 claims description 23
- 238000004519 manufacturing process Methods 0.000 claims description 23
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 16
- 230000004888 barrier function Effects 0.000 claims description 8
- 239000011241 protective layer Substances 0.000 claims description 6
- 241001645254 Guadua angustifolia Species 0.000 claims description 5
- 239000000835 fiber Substances 0.000 claims description 5
- 244000302661 Phyllostachys pubescens Species 0.000 claims description 2
- 235000003570 Phyllostachys pubescens Nutrition 0.000 claims description 2
- 239000000945 filler Substances 0.000 claims description 2
- 238000003825 pressing Methods 0.000 claims description 2
- 238000004026 adhesive bonding Methods 0.000 claims 3
- 238000005452 bending Methods 0.000 abstract description 3
- 239000002184 metal Substances 0.000 abstract 1
- 230000008901 benefit Effects 0.000 description 11
- 239000002994 raw material Substances 0.000 description 8
- 240000003096 Chimonobambusa quadrangularis Species 0.000 description 7
- 229910000831 Steel Inorganic materials 0.000 description 6
- ISWSIDIOOBJBQZ-UHFFFAOYSA-N phenol group Chemical group C1(=CC=CC=C1)O ISWSIDIOOBJBQZ-UHFFFAOYSA-N 0.000 description 6
- 239000010959 steel Substances 0.000 description 6
- 238000003801 milling Methods 0.000 description 4
- 239000004033 plastic Substances 0.000 description 4
- 229920003023 plastic Polymers 0.000 description 4
- 238000012546 transfer Methods 0.000 description 4
- 239000000853 adhesive Substances 0.000 description 3
- 230000001070 adhesive effect Effects 0.000 description 3
- 238000013461 design Methods 0.000 description 3
- 239000003921 oil Substances 0.000 description 3
- 235000019198 oils Nutrition 0.000 description 3
- 238000012545 processing Methods 0.000 description 3
- 230000001681 protective effect Effects 0.000 description 3
- 230000006378 damage Effects 0.000 description 2
- 238000013016 damping Methods 0.000 description 2
- 235000021388 linseed oil Nutrition 0.000 description 2
- 239000000944 linseed oil Substances 0.000 description 2
- 239000002966 varnish Substances 0.000 description 2
- 239000013585 weight reducing agent Substances 0.000 description 2
- 229920000049 Carbon (fiber) Polymers 0.000 description 1
- 240000008120 Dendrocalamus strictus Species 0.000 description 1
- 235000016936 Dendrocalamus strictus Nutrition 0.000 description 1
- 240000000731 Fagus sylvatica Species 0.000 description 1
- 235000010099 Fagus sylvatica Nutrition 0.000 description 1
- 208000027418 Wounds and injury Diseases 0.000 description 1
- 238000005299 abrasion Methods 0.000 description 1
- 230000009471 action Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000005540 biological transmission Effects 0.000 description 1
- 239000004917 carbon fiber Substances 0.000 description 1
- 150000001875 compounds Chemical class 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000006263 elastomeric foam Substances 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 239000011152 fibreglass Substances 0.000 description 1
- 238000000227 grinding Methods 0.000 description 1
- 239000011121 hardwood Substances 0.000 description 1
- -1 however Substances 0.000 description 1
- 208000014674 injury Diseases 0.000 description 1
- 239000004922 lacquer Substances 0.000 description 1
- 230000002045 lasting effect Effects 0.000 description 1
- VNWKTOKETHGBQD-UHFFFAOYSA-N methane Chemical compound C VNWKTOKETHGBQD-UHFFFAOYSA-N 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 229930014626 natural product Natural products 0.000 description 1
- 238000012856 packing Methods 0.000 description 1
- 230000035515 penetration Effects 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 239000011253 protective coating Substances 0.000 description 1
- 230000005855 radiation Effects 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000007789 sealing Methods 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 230000000007 visual effect Effects 0.000 description 1
- 238000004018 waxing Methods 0.000 description 1
Images
Classifications
-
- A—HUMAN NECESSITIES
- A63—SPORTS; GAMES; AMUSEMENTS
- A63C—SKATES; SKIS; ROLLER SKATES; DESIGN OR LAYOUT OF COURTS, RINKS OR THE LIKE
- A63C5/00—Skis or snowboards
- A63C5/12—Making thereof; Selection of particular materials
- A63C5/126—Structure of the core
-
- A—HUMAN NECESSITIES
- A63—SPORTS; GAMES; AMUSEMENTS
- A63C—SKATES; SKIS; ROLLER SKATES; DESIGN OR LAYOUT OF COURTS, RINKS OR THE LIKE
- A63C5/00—Skis or snowboards
- A63C5/12—Making thereof; Selection of particular materials
Definitions
- the invention relates to a sliding board sports equipment according to the preamble of claim 1 and a manufacturing method for a Gleitbrettsport réelle according to the preamble of claim 18th
- Skis and snowboards generally consist of a top chord and a bottom chord, between which a core is arranged.
- the core, the top and bottom chords are made of wood, or the top and bottom chords are made of laminates, such as fiberglass or carbon fiber constructions, in which case the core can also be made of an elastomeric foam.
- the constructions consisting of foamed, non-load-bearing cores in connection with external high-strength laminates have replaced the conventional wooden constructions in recent decades.
- a ski is described, which consists of a foamed plastic core with an enveloping, supporting structure.
- the laminated structures generally do not have good damping properties, which can lead to unpleasant vibrations during driving.
- the materials used are poor or not recyclable, so these skis and snowboards have a poor life cycle assessment.
- Another disadvantage is that the core has a pure filling function, ie the weight of the core increases that Total weight without the core contributing to the stability of the construction.
- FR-A-2 429 377 discloses board sports equipment partly made of bamboo.
- the invention is based on the object to develop an improved Gleitbrettsport réelle, in particular a ski, a snowboard, a water ski, a wakeboard or kiteboard, with which the disadvantages of conventional Gleitbrettsportieri be avoided and the simplest possible production and high rigidity improved Life Cycle Assessment and improved driving characteristics.
- the object is achieved with a Gleitbrettsporthold according to claim 1 and a manufacturing method for such Gleitbrettsportperformance according to claim 17.
- the invention is based on the physical knowledge that the choice of a suitable material for the core of Gleitbrettsportuzes, such as a ski, snowboards, water skis, wakeboards or kite boards damping properties, driving characteristics and life cycle assessment can be improved.
- the core of the Gleitbrettsportuzes invention consists at least partially of bamboo.
- bamboo is a fast-growing, recyclable raw material that can absorb high tensile, compressive and torsional loads.
- bamboo is a low-cost material that is easy to work with. This advantageously results in an inexpensive production.
- the laminates can either be dispensed with completely, or they can be made in a smaller thickness, which further improves the LCA. By reducing or eliminating the laminate layers In addition, the total weight can be reduced.
- the weight reduction made possible by the bamboo structure is of particular advantage, since the ski, unlike the snowboard, is connected to one leg only fixed in one place. Even a slight reduction in weight is particularly noticeable in a ski, since the mass moment of inertia of the ski around the axis of the leg which is decisive for torsional loads on the leg is disproportionately reduced.
- the core consists partly or wholly of bamboo slats.
- the bamboo slats may have a rectangular cross-section or even another cross-section, for example with six or a different number of corners.
- the bamboo slats can be square bamboo sticks, which are installed side by side in the core and glued together. This construction has the advantage of being very easy to manufacture.
- the use of solid square bamboo slats achieves maximum rigidity of the core.
- the core may also or exclusively comprise angle-milled bamboo tubes.
- Angled milled bamboo can be made, for example, from bamboo cane with the help of a square milling machine. This results in a square bamboo rod having a cavity inside, wherein the size of the cavity is dependent on the size of the cavity of the bamboo tube used for the production.
- the angle-milled bamboo tubes can be arranged in the core side by side or side by side and one above the other so that a specific core cross-section is formed.
- the advantage here is the weight reduction due to the cavities of the angle-milled bamboo tubes.
- Angularly milled bamboo tubes are used with a thickness that corresponds to the thickness of the core.
- a filler of lesser density than bamboo can be arranged in the core.
- This has the advantage that the weight of the core can be reduced.
- a filling material known foamed plastics or natural products can be used.
- the Gleitbrettsport réelle has a layer structure in which above and below the core, an at least partially made of bamboo inner veneer layer is arranged.
- This veneer layer can consist entirely or partially of square bamboo sticks, which have been glued together, for example.
- the veneer layers, in combination with the core, give the snowboard, the ski, the water ski, the wakeboard or the kiteboard a very high degree of rigidity, since a torsionally rigid box is created in a non-positive connection with the core.
- the veneer layers are fixed directly to the core without laminates, without a laminate layer being arranged. This has the advantage that can be dispensed with in this area on laminate layers that would deteriorate the environmental balance. If an increased rigidity of the construction is desired, but can Laminate around the core or the inner veneer layers are arranged.
- an upper and a lower chord are arranged according to the invention, which consist at least partially of bamboo.
- the upper and lower chords increase the rigidity of the construction, whereby, if required, several upper and lower chords can be arranged.
- the upper and lower chords can also be made of a material combination of bamboo with, for example, a laminate, and a combination with other natural materials such as wood is also possible in order to increase the strength at certain points.
- the upper and lower chords are each mounted directly on the inner veneer layer. If the inner veneer layers are mounted directly on the core, this results in a stack or sandwich construction which is free of laminates and yet highly stable.
- the bamboo of the core, the lower chord, the upper chord or the inner veneer layers is unthreaded in the longitudinal direction.
- the longitudinal direction refers to a direction of travel of the ski, the snowboard, the water ski, the wakeboard or the kite board. Since impact is generally difficult to transfer and thrust transfer, a bum-free construction offers the advantage of consistently high strength. However, if impacts due to structural details are necessary, they are arranged as possible staggered to ensure a continuous power transmission in the components in the longitudinal direction.
- square bamboo rods or angularly milled bamboo tubes are used made of bamboo tubes whose length is greater than the length of the Gleitbrettsportuzes to be produced.
- side cheeks are arranged laterally of the core, which laterally cover the core or the inner veneer layers.
- the top flange and the bottom flange are wider than the core with the inner veneer layers and are also non-positively connected to the side cheeks, for example glued. This creates a torsion box, which increases the rigidity of the construction.
- Sideways means in the longitudinal direction of Gleitbrettsportêts next to the core.
- vapor barriers are arranged on the core side of the side cheeks.
- the vapor barriers lie between the core and the sidewalls and prevent the entry of water into the core.
- inner veneer layers are arranged above and below the core, the vapor barriers also advantageously cover these veneer layers in order to reliably protect the core and the veneer layers against lateral water ingress.
- the vapor barriers may also be bamboo, which may be specially treated to resist water. If the bamboo vapor barrier connected non-positively with the inner veneer, so advantageously creates a box that increases the torsional stiffness of the snowboard, the ski, the water ski, the wakeboard or the kite board.
- the core advantageously has special features in order to absorb the high forces that are exerted on the binding on the sliding board sports device.
- the core may have wood in the load transfer area, in particular, higher-strength wood types are beneficial. For example, a massive location can Beech wood to be glued.
- the inner veneer layers, the upper or the lower flange wood may also have a force introduction.
- the load introduction area may, for example, each attachment device have a size of about 5 x 5 cm, but it may also be much larger, for example. Have a length of 60 cm. If the core is made of square-edged bamboo tubes, replacement of square-edged bamboo tubes with solid bamboo slats in the load-transfer area can also be advantageous, as it increases the strength in this area.
- the upper belt can be at least partially enclosed with a metallic cover.
- the metallic cover can run in the region of the upper edge and, for example, consist of Titanal. Titanal has the advantage that it has a high resistance to mechanical attacks at low density.
- adjacent bamboo parts are provided in the core with alternately opposite growth directions with respect to the longitudinal direction of the sports equipment, there may be advantages for increased stability of the core structure.
- the bamboo used for these components preferably has a tensile strength of at least 20 kN / cm 2 , 30 kN / cm 2 or 40 kN / cm 2 , a tensile elastic modulus of at least 2.0 MN / cm 2 , 2.5 MN / cm 2 or 3.2 MN / cm 2 or a fiber length of at least 1 cm.
- a high modulus of elasticity has the advantage that the Gleitbrettsport réelle a high rigidity is awarded.
- a high tensile strength in turn has the advantage that the Gleitbrettsport réelle has a high strength. The higher the strength, the higher the sliding board sports equipment can be loaded. Long fibers increase the resistance and strength of the bamboo.
- the Gleitbrettsport réelle has a cover layer which is disposed above the upper flange.
- This cover layer protects the underlying layers against mechanical influences, such as, for example, knocks.
- the cover layer is preferably made at least in part from bamboo of the genus "Phyllopstachys pubescens" or a similar genus. By using bamboo in combination with a transparent protective layer, an attractive graphic design of the snowboard can be achieved.
- the bamboo used for the top layer should have a Brinell hardness of at least 32 HB.
- the bulk density of the bamboo used is preferably at least 0.79 g / cm 3 .
- the abrasion resistance of the cover layer is higher than 3.7. This achieves a high resistance to mechanical grinding loads.
- a protective layer is advantageously applied, for example, to the cover layer.
- This protective layer may, for example, consist of a two-component lacquer or a plastic sealing system and protects the surface against moisture, mechanical effects and UV radiation.
- Particular advantages for the protection and the visual appearance of the surface may result if the protective layer is formed from a protective oil, in particular linseed oil. The oil-protective layer can penetrate into the material below the surface, so there is less chance of injury of deeper layers and superficial scratches can be easily corrected.
- a manufacturing method for producing a Gleitbrettsportmixs invention is an independent subject of the invention.
- the bamboo used to manufacture a sliding board sports equipment according to the invention should generally have a fiber length of at least 1 cm, at a height of no more than 2000 m above sea level, have a maximum residual moisture of 10%, are stored vertically after being whipped and air-dried over a period of 4 to 6 weeks, beaten for a cool and dry season, and heavily silicified nodiums Have diaphragms.
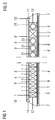
- Fig. 1 the left side of a ski is shown in sectional view.
- the section runs perpendicular to the longitudinal axis (longitudinal direction) of the ski.
- the core of the ski shown in Figure 1 consists of bamboo slats 1 having a width of 0.5 cm, a height of 1.5 cm and a length corresponding to the length of the ski.
- the bamboo slats 1 are made of bamboo of the genus "Guadua angustifolia”.
- the bamboo used to make the bamboo battens of the core should, in addition to the above features, also have at least one of the following characteristics: a tenacity of at least 40,000 m, a tensile strength of at least 40 kN / cm 2 , a compressive strength of at least 93 kN / cm 2, a modulus of elasticity under tensile load of at least 32 MN / cm 2, a modulus of elasticity at compression stress of at least 16.5 MN / cm 2, a modulus in flexure of at least 32.5 MN / cm 2, a bending strength of at least 27 , 6 kN / cm 2 or a shear strength of at least 2.2 kN / cm 2 .
- the bamboo slats of the core dried bamboo which has a raw material length of at least 200 cm
- a circular saw which has a double saw blade sawed in the direction of the longitudinal axis in five to eight uniform circular sections, which are then planed four-sided for further processing
- the sections of the circle are planed into rectangular slats measuring about 7 cm x 3 cm x the length of the raw material.
- the slats are divided horizontally so that they have a thickness of 1.5 cm.
- the slats along the longitudinal axis in 0.5 cm wide and 1.5 cm high strips sawed.
- the product of this step already corresponds to the bamboo slats 1 of the core.
- every other one of the bamboo slats 1 is rotated so that every other slat comes to lie in a reverse growth direction with respect to the longitudinal direction of the ski.
- 30 of the adjacent bamboo slats are pressed together with a two-component adhesive under pressure to the actual approx. 15 cm x 1.5 cm x the length of the raw material long raw core.
- This raw core is suitable for further processing as a skier.
- two of these cores are glued together again under pressure.
- the resulting raw core is milled with the aid of a milling cutter so that it receives the necessary dimensions for the snowboard to be produced.
- bamboo slats 1 inner veneer layers 2, 3 are arranged.
- bamboo is used, to which the same requirements are made as to the bamboo of the core.
- bamboo is processed into slats of 7.5 cm ⁇ 1.5 cm ⁇ the length of the raw material.
- the slats are sawed along the longitudinal axis in 2.5 cm wide strips. Each second of the sawed slats is in turn rotated to compensate for material non-uniformities and then crimped to a 15 cm x 1.5 cm x the length of the raw material measuring raw slab.
- a snowboard To produce a snowboard, two of the green sheets are glued together again under pressure. From the resulting raw slabs are using a veneer saw cut veneer with a thickness of about 0.6 to 1 mm. Analogously, a top flange 4 and a bottom flange 5 are produced.
- a running surface 6 milled onto the contour of the snowboard is pressed together with contoured steel edges 7 into a shape corresponding to the outer contour of the ski.
- the steel edges 7 and the tread 6 are generally known in the art.
- an approximately 0.2 mm thick rubber layer 8 is glued, with the compound, in particular between the steel edges and the tread can be improved.
- the further layered structure of the ski consists of the lower flange 5, the inner veneer layer 2, the bamboo slats 1 of the core, the second inner veneer layer 3, the top flange 4 and a veneer top layer 9.
- the veneer top layer is produced in an analogous process as the internal veneer layers, however, bamboo of the genus "Phyllostachys pubescens" is used.
- the bamboo of the upper veneer layer 9 should have a Brinell hardness of at least 32 HB, a bulk density of at least 0.79 g / cm 2 and be provided after processing with a protective coating.
- Each side of the core a phenolic sidewall 10 is arranged.
- Above the phenol side cheek a finishing edge 11 is arranged, which is adapted to the contour of the ski and consists of Titanal.
- a vertical bamboo strip is installed between the core and the phenol side cheek .
- this bamboo strip is made of bamboo veneer and serves as a vapor barrier 12. For this purpose, it is pretreated with a protective varnish.
- the ski design which is completely inserted in the contour shape, is inserted into a heatable vacuum autoclave press and there pressed with a pressure of about 5 to 10 kN / m 2 .
- the press is heated for about one minute to a temperature of 150 ° C. At this temperature, a lasting plastic deformation is imposed on the bamboo, giving the ski its final shape.
- the press is cooled to room temperature over a period of 4 to 6 hours.
- sanding and milling removes any adhesive residue, sanding and waxing the tread, and treating the bamboo surface with a varnish or oil.
- a protective oil a linseed oil with the highest possible penetration capacity is used, as it is known from boat building.
- FIG. 2 shows a sectional view of a perpendicular to the longitudinal cut ski.
- the components provided with the primed reference numerals correspond to those shown in Figure 1 and provided with uncoated reference numerals components, which is why this will not be discussed again here.
- the difference of the ski shown in Fig. 2 compared to Fig. 1 relates to the construction of the core.
- the core consists of angularly milled bamboo tubes 21 and bamboo slats 1 '.
- the angularly milled bamboo tubes 21 are manufactured by making dried bamboo tubes of the genus "Guadua angustifolia" with a diameter of about 1.2 cm and a wall thickness of about 0.3 cm by means of a square milling machine to angularly milled bamboo tubes 21 of about 0.85 cm x 0 , 85 cm x the length of the raw material are milled.
- the resulting angularly milled bamboo tubes 21 then become together with the bamboo slats 1 'with a permanently elastic two-component adhesive under pressure to a raw core with the dimensions 15 cm x 1.5 cm x the length of the raw material pressed.
- a snowboard core two of the resulting cores are again glued together under pressure to produce a double raw core of width 30 cm.
- bamboo slats 1 ' was installed to about 60 cm in length.
- the further manufacturing process corresponds to the manufacturing process described above in connection with FIG.
- the result of the manufacturing process may be a bamboo construction for a snowboard and a ski of all kinds, consisting of an internal, independent of laminates, in bending and torsion resistant bamboo torsion box.
- the inner torsion box consists of longitudinally unpunched bamboo veneers 2, 3 and core elements 1, 1 ', 21 which are perpendicular to the inner torsion box and ideally consist of bamboo veneers 1, 1', which are unscathed in the longitudinal direction, or angularly milled bamboo tubes 21.
- the construction may be considered to have an outer torsion box embedded in the inner torsion box and consisting of a top flange 4, a bottom flange 5 and the side cheeks 10.
- the top flange 3, the bottom flange 2 of the inner torsion box are ideally made of highly tensile, compressive, and torsion-loadable materials such as.
- the side cheeks 10 are made of impact resistant, but flexible materials such as phenol, ABS or hardwood.
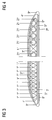
- FIG. 3 shows a further embodiment of the invention.
- FIG. 3 shows a sectional view of a wakeboard, the section being perpendicular to the longitudinal direction.
- the wakeboard shown in FIG. 3 also has a core of bamboo slats 1 ", inner veneer layers 2", 3 ", a top flange 4", a bottom flange 5 ", a running surface 6" and a cover layer 9 " ,
- the tread 6 " is adapted to the requirements of water sports, in which case it is possible to use materials which are known per se from the prior art.
- the illustrated wakeboard has no upper end edge, no phenolic sidewall and no steel edge, the cover layer 9" is round the edge running around so that it abuts directly on the running surface 6 "Further, the upper flange 4" is formed so that it reaches down to the lower inner veneer layer 5 ", with which it is glued Skis shown and described in FIG.
- FIG. 4 shows a cross section through another embodiment of a wakeboard according to the invention.
- the components provided with the reference numerals correspond to those shown in Figure 3 and are provided with double-painted reference numerals.
- the difference of the wakeboard shown in Figure 4 compared to that shown in Figure 3 relates to the construction of the core.
- the core consists of angularly milled bamboo tubes 21 'and bamboo slats 1' '.
- the angularly milled bamboo tubes 21' are manufactured as described above in connection with FIG.
- snowboards can be produced in the same way as skis.
- the main difference consists in the larger width of the snowboards.
- kiteboard also water ski or wakeboards can be constructed.
Landscapes
- Laminated Bodies (AREA)
- Road Paving Structures (AREA)
- Chemical And Physical Treatments For Wood And The Like (AREA)
- Machines For Manufacturing Corrugated Board In Mechanical Paper-Making Processes (AREA)
- Dry Formation Of Fiberboard And The Like (AREA)
Claims (21)
- Planche de sport de glisse, en particulier de ski, snowboard, ski nautique, wakeboard ou kiteboard, avec un noyau (1, 1', 1'', 1''', 21, 21') au moins partiellement en bambou, et une semelle supérieure (4, 4', 4'', 4''') disposée au-dessus du noyau (1, 1', 1'', 1''', 21, 21'), caractérisée par une semelle inférieure (5, 5', 5'', 5''') disposée au-dessous du noyau (1, 1', 1'', 1''', 21, 21'), la semelle supérieure (4, 4', 4'', 4''') et la semelle inférieure (5, 5', 5'', 5''') étant au moins partiellement en bambou.
- Planche de sport de glisse selon la revendication 1, caractérisée en ce que le noyau (1, 1', 1'', 1''', 21, 21') comprend des lattes de bambou (1, 1', 1'', 1''').
- Planche de sport de glisse selon la revendication 1 ou 2, caractérisée en ce que le noyau (1, 1', 1'', 1''', 21, 21') comprend des cannes de bambou fraisées par fraise conique (21, 21').
- Planche de sport de glisse selon la revendication 1 ou 2, caractérisée en ce que le noyau (1, 1', 1'', 1''', 21, 21') comprend un matériau de remplissage de densité inférieure à celle du bambou.
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée par une structure stratifiée, où une couche de placage intérieure (2, 2', 2'', 2''', 3, 3', 3'', 3''') au moins partiellement en bambou est disposée directement au-dessus et en-dessous du noyau (1, 1', 1'', 1''', 21, 21').
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée en ce que la semelle supérieure (4, 4', 4'', 4''') et la semelle inférieure (5, 5', 5'', 5''') sont appliquées chacune directement sur la couche de placage intérieure (2, 2', 2'', 2''', 3, 3', 3'', 3''').
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée en ce que le bambou du noyau (1, 1', 1'', 1''', 21, 21'), de la semelle inférieure (5, 5', 5'', 5'''), de la semelle supérieure (4, 4', 4'', 4''') et/ou des couches de placage intérieures (2, 2', 2'', 2''', 3, 3', 3'', 3''') est sans joints dans le sens longitudinal de la planche de sport de glisse.
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée par des joues latérales (10, 10') recouvrant latéralement le noyau (1, 1', 1'', 1''', 21, 21') et/ou les couches de placage intérieures (2, 2', 2", 2''', 3, 3', 3'', 3''').
- Planche de sport de glisse selon la revendication 8, caractérisée en ce que les joues latérales (10, 10') présentent des barrières contre la vapeur (12, 12') au niveau du noyau.
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée en ce qu'un dispositif de fixation est prévu pour une attache, le noyau (1, 1', 1'', 1''', 21, 21') et/ou les couches de placage intérieures (2, 2', 2'', 2''', 3, 3', 3'', 3''') comportant du bois dans la zone d'application de contrainte du dispositif de fixation.
- Planche de sport de glisse selon l'une des revendications 3 à 9, caractérisée en ce qu'un dispositif de fixation est prévu pour une attache, le noyau (1, 1', 1'', 1''', 21, 21') étant en lattes de bambou (1, 1', 1'', 1''') dans la zone d'application de contrainte du dispositif de fixation, et en bambou fraisé par fraise conique (21, 21') dans les autres zones.
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée en ce que la semelle supérieure (4, 4', 4'', 4''') est au moins partiellement bordée par une couverture métallique (11, 11').
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée en ce que le bambou du noyau (1, 1', 1'', 1''', 21, 21'), des couches de placage intérieures (2, 2', 2'', 2''', 3, 3', 3'', 3'''), de la semelle supérieure (4, 4', 4'', 4''') et/ou de la semelle inférieure (5, 5', 5'', 5''') comporte un bambou de l'espèce « Guadua angustifolia ».
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée en ce que le bambou du noyau (1, 1', 1'', 1''', 21, 21'), des couches de placage intérieures (2, 2', 2'', 2''', 3, 3', 3'', 3'''), de la semelle supérieure (4, 4', 4'', 4''') et/ou de la semelle inférieure (5, 5', 5'', 5''') présente une résistance à la traction d'au moins 30 kN/cm2, un module d'élasticité en cas de contrainte de traction d'au moins 2,5 MN/cm2, et/ou une longueur de fibre d'au moins 1 cm.
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée par une couche de couverture (9, 9', 9'', 9''') comprenant un bambou de l'espèce « Phyllostachys pubescens » et/ou un bambou avec une dureté Brinell d'au moins 32 HB et/ou une densité apparente d'au moins 0,79 g/cm3.
- Planche de sport de glisse selon l'une des revendications précédentes, caractérisée par une couche de protection appliquée au moins sur des parties de la surface de la couche de couverture (9, 9', 9'', 9''').
- Procédé de fabrication d'une planche de sport de glisse selon l'une des revendications 1 à 16, où une semelle inférieure (5, 5', 5'', 5'''), un noyau (1, 1', 1'', 1''', 21, 21') et une semelle supérieure (4, 4', 4'', 4''') sont superposés dans une forme de contour, comprenant les étapes suivantes :- fabrication du noyau (1, 1', 1'', 1''', 21, 21') au moins partiellement en bambou,- fabrication de la semelle inférieure (5, 5', 5'', 5''') et/ou de la semelle supérieure (4, 4', 4'', 4''') au moins partiellement en bambou,- collage par superposition directe de la semelle inférieure (5, 5', 5'', 5'''), du noyau (1, 1', 1'', 1''', 21, 21') et de la semelle supérieure (4, 4', 4'', 4'''), et- compression à 150° C de la semelle inférieure (5, 5', 5'', 5'''), du noyau (1, 1', 1'', 1''', 21, 21') et de la semelle supérieure (4, 4', 4'', 4''').
- Procédé de fabrication selon la revendication 17, caractérisé par la mise en place et le collage d'une couche de placage intérieures (2, 2', 2'', 2''', 3, 3', 3'', 3''') entre le noyau (1, 1', 1'', 1''', 21, 21') et la semelle supérieure (4, 4', 4'', 4'''), et/ou entre le noyau (1, 1', 1'' , 1''', 21, 21') et la semelle inférieure (5, 5', 5'', 5''').
- Procédé de fabrication selon la revendication 17 ou 18, caractérisé par l'utilisation de plaques brutes ayant une épaisseur comprise entre 0,5 cm et 3cm pour le noyau (1, 1', 1'', 1''', 21, 21'), les couches de placage intérieures (2, 2', 2'', 2''', 3, 3', 3'', 3'''), la semelle supérieure (4, 4', 4'', 4''') et/ou la semelle inférieure (5, 5', 5'', 5'''), les plaques brutes étant fabriquées par collage de bambous fraisés par fraise conique (21, 21') et/ou de lattes de bambou (1, 1' , 1'', 1''').
- Procédé de fabrication selon l'une des revendications 17 à 19, caractérisé en ce que le noyau en bambou est fabriqué avec des sens alternés par rapport au sens longitudinal du noyau (1, 1', 1'', 1''', 21, 21').
- Procédé de fabrication selon l'une des revendications 17 à 20, caractérisé en ce qu'un bambou de l'espèce « Guadua angustifolia » est utilisé.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE20310246U | 2003-07-03 | ||
| DE20310246U DE20310246U1 (de) | 2003-07-03 | 2003-07-03 | Bambuskernkonstruktion, für Snowboard und Ski aller Art, bestehend aus einem innenliegenden, von Laminaten unabhängigen, in sich biege- und verwindungssteifen Torsionskasten aus Bambus |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1493468A2 EP1493468A2 (fr) | 2005-01-05 |
| EP1493468A3 EP1493468A3 (fr) | 2005-02-02 |
| EP1493468B1 true EP1493468B1 (fr) | 2006-12-06 |
Family
ID=33426902
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP03028220A Expired - Lifetime EP1493468B1 (fr) | 2003-07-03 | 2003-12-09 | Planche de sport de glisse comprenant un noyau en bambou |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP1493468B1 (fr) |
| AT (1) | ATE347414T1 (fr) |
| DE (3) | DE20310246U1 (fr) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2005056132A1 (fr) * | 2003-12-05 | 2005-06-23 | K-2 Corporation | Ame de ski |
| FR2909893B1 (fr) * | 2006-12-14 | 2010-01-15 | Alain Zanco | Mecanisation optimisee pour une planche de glisse sur neige. |
| AT504841B1 (de) | 2007-02-09 | 2009-03-15 | Theurl Leimholzbau Gmbh | Gleitbrettkern für schi oder snowboards |
| FR2916983B1 (fr) * | 2007-06-06 | 2010-08-13 | Salomon Sa | Planche de glisse ou de roulage |
| DE202009001846U1 (de) | 2009-02-13 | 2009-05-20 | Theurl Leimholzbau Gmbh | Leichtbaukörper aus einem Faserverbundwerkstoff auf Basis von Holzfasermatten, insbesondere für Rotorblätter in Windkraftanlagen |
| WO2012117581A1 (fr) * | 2011-02-28 | 2012-09-07 | 光洋産業株式会社 | Planche en bambou et planche composite et leur procédé de fabrication |
| FR2999944B1 (fr) * | 2012-12-20 | 2015-02-13 | Salomon Sas | Chant lateral pour planche de glisse |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2429377A1 (fr) * | 1978-06-20 | 1980-01-18 | Saget Michel | Perfectionnements apportes aux planches de sport |
| US6648363B2 (en) * | 2001-12-05 | 2003-11-18 | Shale Gordon | Composite sports board such as a skateboard deck |
-
2003
- 2003-07-03 DE DE20310246U patent/DE20310246U1/de not_active Expired - Lifetime
- 2003-12-09 EP EP03028220A patent/EP1493468B1/fr not_active Expired - Lifetime
- 2003-12-09 AT AT03028220T patent/ATE347414T1/de active
- 2003-12-09 DE DE50305904T patent/DE50305904D1/de not_active Expired - Lifetime
-
2004
- 2004-01-26 DE DE102004003855A patent/DE102004003855A1/de not_active Withdrawn
Also Published As
| Publication number | Publication date |
|---|---|
| DE102004003855A1 (de) | 2005-01-27 |
| DE20310246U1 (de) | 2004-11-04 |
| ATE347414T1 (de) | 2006-12-15 |
| EP1493468A3 (fr) | 2005-02-02 |
| EP1493468A2 (fr) | 2005-01-05 |
| DE50305904D1 (de) | 2007-01-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| AT504841B1 (de) | Gleitbrettkern für schi oder snowboards | |
| DE60009857T2 (de) | Kern für gleitbrett | |
| AT410518B (de) | Kern für ein gleitbrett | |
| CH669331A5 (fr) | ||
| DE10224721B4 (de) | Formteil aus Holz und Verfahren zu seiner Herstellung | |
| DE102008034749B3 (de) | Holzwerkstoffplatte | |
| EP2247222B1 (fr) | Structure porteuse, procédé de fabrication et utilisation d une telle structure porteuse | |
| AT398380B (de) | Ski, insbesondere alpinski, und verfahren zu seiner herstellung | |
| DE102004003855A1 (de) | Gleitbrettsportgerät mit einem Bambuskern | |
| EP0426015B1 (fr) | Produits lamellés en bois tels que poutres, planches et panneaux multiples collés et procédé pour leur fabrication | |
| AT406825B (de) | Hockeyschläger | |
| DE10304029A1 (de) | Tischtennisschläger mit einem Schlagblatt, welches einen mit einer Mittelschicht versehenen mehrlagigen Grundkörper umfaßt sowie Verfahren zur Herstellung der Mittelschicht | |
| DE3011528A1 (de) | Geruesttafel aus mehreren werkstofflagen | |
| AT504001B1 (de) | Gleitbrett oder rollbrett mit verbundstruktur | |
| DE2135278A1 (de) | Leichtski | |
| EP1404420B1 (fr) | Noyau leger et son procede de production | |
| DE3913969A1 (de) | Ski und verfahren zu seiner herstellung | |
| WO2021239769A1 (fr) | Panneau fonctionnel asymétrique | |
| EP2157271B1 (fr) | Ebauche de porte et procédé de fabrication d'une ébauche de porte | |
| DE102018126956A1 (de) | Bambuseinheit | |
| DE4232444C2 (de) | Ski, insbesondere Alpinski | |
| AT276177B (de) | Ski | |
| DE102007048562A1 (de) | Wassersportgerät, insbesondere Wasserski oder Surfbrett | |
| DE69917320T2 (de) | Tragende struktur | |
| EP3838354A1 (fr) | Planche de glisse, en particulier ski |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK |
|
| 17P | Request for examination filed |
Effective date: 20050401 |
|
| 17Q | First examination report despatched |
Effective date: 20050705 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20061206 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061231 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061231 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 50305904 Country of ref document: DE Date of ref document: 20070118 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070306 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070306 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070317 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: RITSCHER & PARTNER AG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070507 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20061206 |
|
| EN | Fr: translation not filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20070907 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 |
|
| BERE | Be: lapsed |
Owner name: SCHWABE & BAER ENTWICKLUNGS G.M.B.H. Effective date: 20061231 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PCAR Free format text: RITSCHER & PARTNER AG;RESIRAIN 1;8125 ZOLLIKERBERG (CH) |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070727 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070307 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070607 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061206 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PFA Owner name: SCHWABE AND BAER ENTWICKLUNGS GMBH, DE Free format text: FORMER OWNER: SCHWABE AND BAER ENTWICKLUNGS GMBH, DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PCOW Free format text: NEW ADDRESS: KAPUZINERPLATZ 5, 80337 MUENCHEN (DE) |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 347414 Country of ref document: AT Kind code of ref document: T Effective date: 20131209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131209 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: NFJG Ref document number: 347414 Country of ref document: AT Kind code of ref document: T Effective date: 20150618 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20191231 Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20191219 Year of fee payment: 17 Ref country code: CH Payment date: 20191227 Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 50305904 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 347414 Country of ref document: AT Kind code of ref document: T Effective date: 20201209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201209 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201231 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210701 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20201231 |