EP1527858A2 - Stanzstation mit einer Kontrolleinrichtung für Verpackungen - Google Patents
Stanzstation mit einer Kontrolleinrichtung für Verpackungen Download PDFInfo
- Publication number
- EP1527858A2 EP1527858A2 EP04015081A EP04015081A EP1527858A2 EP 1527858 A2 EP1527858 A2 EP 1527858A2 EP 04015081 A EP04015081 A EP 04015081A EP 04015081 A EP04015081 A EP 04015081A EP 1527858 A2 EP1527858 A2 EP 1527858A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- punching
- packaging
- station according
- control device
- punching station
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B57/00—Automatic control, checking, warning, or safety devices
- B65B57/02—Automatic control, checking, warning, or safety devices responsive to absence, presence, abnormal feed, or misplacement of binding or wrapping material, containers, or packages
- B65B57/04—Automatic control, checking, warning, or safety devices responsive to absence, presence, abnormal feed, or misplacement of binding or wrapping material, containers, or packages and operating to control, or to stop, the feed of such material, containers, or packages
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D5/00—Arrangements for operating and controlling machines or devices for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D5/20—Arrangements for operating and controlling machines or devices for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting with interrelated action between the cutting member and work feed
- B26D5/26—Arrangements for operating and controlling machines or devices for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting with interrelated action between the cutting member and work feed wherein control means on the work feed means renders the cutting member operative
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/04—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for severing webs, or for separating joined packages
- B65B61/06—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for severing webs, or for separating joined packages by cutting
- B65B61/065—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for severing webs, or for separating joined packages by cutting by punching out
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/18—Means for removing cut-out material or waste
- B26D7/1845—Means for removing cut-out material or waste by non mechanical means
- B26D7/1863—Means for removing cut-out material or waste by non mechanical means by suction
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/38—Cutting-out; Stamping-out
- B26F1/40—Cutting-out; Stamping-out using a press, e.g. of the ram type
Definitions
- the invention relates to a stamping station for a product in packaging packaging machine, in particular a thermoforming machine, for punching out packaging from a foil strip, with a by means of a drive in a punching position adjustable punching tool and with a transport device for the removal of the punched out packaging.
- Packaging machines are usually called Blister packs produced by which products such as Tablets, capsules, dragees or the like in deep-drawn cups of a mold film filled specifically and then by means of a cover sheet in a film strip to be sealed. It is a mandatory requirement that under no circumstances defective packaging in the continue packaging process, so packaging which either the products are faulty or in the Wells are missing, or the packaging is not correct is sealed because, for example, a sealed seam a Faulty or the foil tape is damaged. at such defective packaging is the durability of Packaged products are not guaranteed and it is not ensured that several in one outer package summarized individual packaging on the Repackaging specified number of products included.
- the invention is therefore based on the object, a Stamping station of the type mentioned above in such a way that a secure separation of defective packaging from error-free packaging in a simple way is ensured.
- downstream of the punch a arranged a cutting knife having trimmer is to get the opportunity the foil tape including the defective packaging too shred and properly disposed of or to feed a waste cycle.
- a particularly preferred embodiment of the invention is characterized in that the control device to distinguish between filled and partially filled and empty Packaging is provided, and that the Control device with a switch for separating the Packaging is connected depending on the signal.
- the control device to distinguish between filled and partially filled and empty Packaging is provided, and that the Control device with a switch for separating the Packaging is connected depending on the signal.
- the Products are arranged in the form of a matrix, as shown in the rule in blister packs is the case, there is the Possibility of individual rows or columns from the Separate foil tape, and so small, easy to handle To create units. It is also important that through this Design ensures that the products themselves not be damaged and therefore not Pharmaceuticals, some high in very low doses are effective, released.
- control device has a Camera for optical pattern recognition, since on this Paths in a simple way the desired distinction defective packaging is possible. comparable Benefits also arise when the recording of the Hofkanten sensor provided a light barrier to Has control.
- a Suction gripper is provided for handover as error-free recognized packaging to the transport device, since so easily clean packaging of the Foil tape net can be removed.
- the transport device a revolving conveyor belt with which the packaging hanging transportable. This also allows that related to the conveying direction of the film strip the Punching tool a control device for differentiation faultless packaging of faulty packaging upstream, and that the control facility is equipped with the Drive communicates for the purpose of preventing the Adjustment of the punching tool in the punching position at Detection of faulty packaging by the Control device.
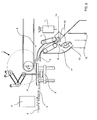
- Packaging machine is a punching station 1 in FIG shown with the products containing packaging 2, 3 can be punched out of a foil strip 4.
- a control device 7 Relative to the conveying direction of the film strip 4 is before the Punching tool 5 a control device 7 is arranged, the includes a camera for optical pattern recognition and the Distinguishing error-free packaging 2 from defective packaging 3 is used.
- Control device 7 error-free packaging 2, ie Packaging 2 in which the deep-drawn cups 8 in a mold film correctly filled with products and means a cover sheet are properly sealed, it will Punching tool 5 adjusted in the punching position and the error-free packaging 2 by means of a suction pad 9 at the transport device 6 pass through a revolving conveyor belt is realized, with which the Packaging 2 are transported hanging, with the Contour of punched packaging 2 by means of a optical detection system 10 is again checked.
- the control device 7 is faulty Packaging 3 firm, so a packaging in which a Cup 8 is not filled in the foil strip 4 or the Sealing seam between cover foil and foil is not correct is formed or another error is present, so acts the control device 7 on the drive of Punching tool 5 a to the punching of the package. 3 to suppress, so that with the film strip 4 on is transported.
- the foil strip 4 is a downstream the punching tool 5 arranged waste cutter 11th fed to a cutting blade 12 for crushing the Foil tape 4 has.
- the cutting blade 12 is made a rotating drivable cutting blade 13 and a stationary arranged in the trash cutter 11 Counter blade 14 formed, wherein the axis of rotation of the Cutting blade 13 transverse to the feed direction of the Foil tape 4 is oriented.
- the rotation is through a sensor 15 regulated to a line by line separation To ensure the cups 8 of the foil strip 4.
- Dependence of the signals of the control device is continue to set a switch 16, the separation of the Packaging 3 due to lack or presence of products in serves the cups.
- the sensor 15 detects by means of a Photocell the edges of the edges in the packaging 3 trained cups 8 and can be so clearly between Divide areas of the film strip 4, in which the Cut the cutting blade 12 without risk to the products can.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Life Sciences & Earth Sciences (AREA)
- Forests & Forestry (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Gasket Seals (AREA)
- Diaphragms For Electromechanical Transducers (AREA)
Abstract
Description
- Fig. 1
- eine schematische Darstellung einer Stanzstation einer Thermoformmaschine in einer Seitenansicht mit Positionierung der Weiche in einer ersten Stellung,
- Fig. 2
- eine der Fig. 1 entsprechende Darstellung mit Positionierung der Weiche in einer zweiten Stellung,
- Fig. 3
- eine perspektivische Darstellung der Stanzstation aus Fig. 1, und
- Fig. 4
- eine isolierte Darstellung eines Folienbandes mit einer ausgestanzten fehlerfreien Verpackung sowie einer durch die Kontrolleinrichtung als fehlerhaft erkannten Verpackung.
Claims (11)
- Stanzstation für eine Produkte in Folien verpackende Verpackungsmaschine, insbesondere einer Thermoformmaschine, zum Ausstanzen von
Verpackungen (2) aus einem Folienband (4), mit einem mittels eines Antriebes in eine Stanzposition verstellbaren Stanzwerkzeug (5) und mit einer Transporteinrichtung (6) für den Abtransport der ausgestanzten Verpackungen (2), dadurch gekennzeichnet, daß bezogen auf die Förderrichtung des Folienbandes (4) dem Stanzwerkzeug (5) eine Kontrolleinrichtung (7) zur Unterscheidung fehlerfreier Verpackungen (2) von fehlerhaften Verpackungen (3) vorgelagert ist, und daß die Kontrolleinrichtung (7) mit dem Antrieb in Verbindung steht zum Zwecke des Verhinderns der Verstellung des Stanzwerkzeugs (5) in die Stanzposition bei Detektion einer fehlerhaften Verpackung (3) durch die Kontrolleinrichtung (7). - Stanzstation nach Anspruch 1, dadurch gekennzeichnet, daß stromab des Stanzwerkzeugs (5) ein ein Schneidmesser (12) aufweisender Abfallschneider (11) angeordnet ist.
- Stanzstation nach Anspruch 2, dadurch gekennzeichnet, daß die Kontrolleinrichtung (7) zur Unterscheidung gefüllter und teilgefüllter und leerer
Verpackungen (3) vorgesehen ist, und daß die Kontrolleinrichtung (7) mit einer Weiche (16) zur Separierung der Verpackungen (3) in Abhängigkeit des Signals verbunden ist. - Stanzstation nach Anspruch 3, dadurch gekennzeichnet, daß ein Sensor (15) zur Erfassung der Hofkanten der in der Verpackung (3) ausgebildeten Näpfe (8) zur Aufnahme der Produkte und/oder der Produktgrenzen vorgesehen ist zum Zwecke des Durchtrennens des Folienbandes (4) zwischen den Produkten.
- Stanzstation nach Anspruch 4, dadurch gekennzeichnet, daß das Schneidmesser (12) aus einer rotierend antreibbaren Schneidklinge (13) und einer stationär im Abfallschneider (11) angeordneten Gegenklinge (14) gebildet ist.
- Stanzstation nach Anspruch 4 oder 5, dadurch gekennzeichnet, daß die Rotationsachse der Schneidklinge (13) quer zur Vorschubrichtung des Folienbandes (4) orientiert und die Rotation durch den Sensor (15) regelbar ist.
- Stanzstation nach einem der Ansprüche 1 bis 6, dadurch gekennzeichnet, daß die Kontrolleinrichtung (7) eine Kamera zur optischen Mustererkennung aufweist.
- Stanzstation nach einem der Ansprüche 4 bis 7, dadurch gekennzeichnet, daß der Sensor (15) eine Lichtschranke zur Kontrolle aufweist.
- Stanzstation nach einem der Ansprüche 1 bis 8, dadurch gekennzeichnet, daß ein Sauggreifer (9) vorgesehen ist zur Übergabe als fehlerfrei erkannter Verpackungen (2) an die Transporteinrichtung (6).
- Stanzstation nach einem der Ansprüche 1 bis 9, dadurch gekennzeichnet, daß die Transporteinrichtung (6) ein umlaufendes Förderband aufweist, mit dem die Verpackungen (2) hängend transportierbar sind.
- Stanzstation nach einem der Ansprüche 1 bis 10, dadurch gekennzeichnet, daß der
Transporteinrichtung (6) ein optisches Detektionssystem zur Kontrolle der Kontur der ausgestanzten Verpackungen (2) zugeordnet ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE10350423A DE10350423A1 (de) | 2003-10-29 | 2003-10-29 | Stanzstation |
| DE10350423 | 2003-10-29 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1527858A2 true EP1527858A2 (de) | 2005-05-04 |
| EP1527858A3 EP1527858A3 (de) | 2005-07-27 |
| EP1527858B1 EP1527858B1 (de) | 2006-05-17 |
Family
ID=34399586
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP04015081A Expired - Lifetime EP1527858B1 (de) | 2003-10-29 | 2004-06-26 | Stanzstation mit einer Kontrolleinrichtung für Verpackungen |
Country Status (7)
| Country | Link |
|---|---|
| US (2) | US20050095099A1 (de) |
| EP (1) | EP1527858B1 (de) |
| JP (1) | JP3983756B2 (de) |
| AT (1) | ATE326318T1 (de) |
| DE (2) | DE10350423A1 (de) |
| DK (1) | DK1527858T3 (de) |
| ES (1) | ES2260716T3 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2025601A3 (de) * | 2007-08-07 | 2009-03-18 | Grifols, S.A. | Maschine zur Handhabung von Blisterpackungen |
Families Citing this family (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ITBO20040269A1 (it) * | 2004-04-29 | 2004-07-29 | Ima Spa | Metodo e unita' per la realizzazione di confezioni blister mediante recisione di un nastro alveolato |
| DE102005009279A1 (de) * | 2005-02-25 | 2006-09-07 | Cfs Germany Gmbh | Verpackungsmaschine mit einer verschieblich angeordneten Lochstanze |
| EP1800645A1 (de) * | 2005-12-21 | 2007-06-27 | Körber AG | Verpackung für medizinische Produkte und dergleichen |
| US7818950B1 (en) | 2007-05-30 | 2010-10-26 | Walgreen Co. | Method of loading a multi-dose blister card using a transfer fixture |
| DE102008039841A1 (de) * | 2008-08-27 | 2010-03-04 | Ulma Packaging Technological Center, S. Coop | Verpackungsmaschine mit Abfallschneider |
| US7992364B2 (en) | 2009-03-25 | 2011-08-09 | Rennco Llc | Vertical bagging machine |
| ITBO20120594A1 (it) * | 2012-10-31 | 2014-05-01 | Ima Ind Srl | Apparato e metodo per alimentare capsule vuote ad una macchina confezionatrice |
| CN109436798B (zh) * | 2018-12-31 | 2023-08-22 | 浙江希望机械有限公司 | 单板独立剔除旋转机械手 |
| CN110774116B (zh) * | 2019-11-04 | 2021-07-23 | 深圳市普林司顿模具塑胶有限公司 | 一种模具镜面加工工艺及其加工设备 |
| CN113955228B (zh) * | 2021-11-25 | 2022-12-09 | 山东华致林医药科技有限公司 | 一种具备空盒剔除功能的药品热封包装生产线用送料设备 |
Family Cites Families (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2950469C2 (de) * | 1979-12-14 | 1983-12-01 | I.M.A. Industria Macchine Automatiche S.p.A., Ozzano Emilia, Bologna | Vorrichtung zum automatischen Schneiden von rechteckigen Platten mit abgerundeten Ecken |
| IT1145011B (it) * | 1981-01-23 | 1986-11-05 | Ima Spa | Apparecchiatura per il controllo delle operazioni lungo la linea operativa di macchine confezionatrici, particolarmente di confezioni-"blisters" e simili |
| FR2499508B1 (fr) * | 1981-02-07 | 1986-11-14 | Illig Maschinenbau Adolf | Dispositif de coupe pour machine d'emballage |
| IT1242534B (it) * | 1990-06-07 | 1994-05-16 | Ima Spa | Apparecchiatura per il ricevimento di blister da una linea di blister per il confezionamento di articoli vari in singoli blister, e per l'alimentazione, con pile di tali blister di relativi contenitori situati in una linea di allestimento contenitori. |
| US5040353A (en) * | 1990-07-26 | 1991-08-20 | Glaxo Inc. | System for inspecting and recycling goods from defective packages on a blister packaging machine |
| US5363968A (en) * | 1991-08-23 | 1994-11-15 | Pfizer Inc. | Automatic blister inspection system |
| DE4243206A1 (de) * | 1992-12-19 | 1994-06-23 | Hoefliger & Oehlmann Ges Zum B | Verfahren und Vorrichtung zum Überprüfen einer automatischen Abfüllanlage auf korrektes Befüllen |
| US5555707A (en) * | 1994-02-18 | 1996-09-17 | Schwenger; Hans O. | Blister pack scanner device |
| US5568715A (en) * | 1994-05-31 | 1996-10-29 | Johnson & Johnson Vision Products, Inc. | Automated inspection system with transport and ejector conveyor |
| DE19505256A1 (de) * | 1995-02-16 | 1996-08-22 | Rose Verpackungsmasch | Vorrichtung zum Vorschub einer Einwickelmaterialbahn und zum Abtrennen einzelner Einwickelmaterialabschnitte für eine Verpackungsmaschine sowie Verfahren zum Steuern derselben |
| DE19617014C2 (de) * | 1996-04-27 | 1998-04-09 | Uhlmann Pac Systeme Gmbh & Co | Verfahren und Vorrichtung zum Nachfüllen von Füllgut in Näpfe einer Folienbahn |
| JP2994638B1 (ja) * | 1999-01-07 | 1999-12-27 | 旭マシナリー株式会社 | 平盤打抜き装置 |
| DE19917436C2 (de) * | 1999-04-17 | 2003-11-13 | Uhlmann Pac Systeme Gmbh & Co | Vorrichtung zum Übergeben einer Blisterpackung |
| IT1321251B1 (it) * | 2000-05-10 | 2004-01-08 | Ima Spa | Dispositivo di tranciatura di confezioni blister in una macchinablisteratrice. |
-
2003
- 2003-10-29 DE DE10350423A patent/DE10350423A1/de not_active Ceased
-
2004
- 2004-06-26 EP EP04015081A patent/EP1527858B1/de not_active Expired - Lifetime
- 2004-06-26 DK DK04015081T patent/DK1527858T3/da active
- 2004-06-26 AT AT04015081T patent/ATE326318T1/de not_active IP Right Cessation
- 2004-06-26 ES ES04015081T patent/ES2260716T3/es not_active Expired - Lifetime
- 2004-06-26 DE DE502004000577T patent/DE502004000577D1/de not_active Expired - Lifetime
- 2004-10-28 US US10/975,924 patent/US20050095099A1/en not_active Abandoned
- 2004-10-29 JP JP2004316404A patent/JP3983756B2/ja not_active Expired - Lifetime
-
2008
- 2008-02-25 US US12/072,233 patent/US20080202070A1/en not_active Abandoned
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2025601A3 (de) * | 2007-08-07 | 2009-03-18 | Grifols, S.A. | Maschine zur Handhabung von Blisterpackungen |
Also Published As
| Publication number | Publication date |
|---|---|
| ATE326318T1 (de) | 2006-06-15 |
| DE502004000577D1 (de) | 2006-06-22 |
| JP2005132494A (ja) | 2005-05-26 |
| DE10350423A1 (de) | 2005-06-16 |
| EP1527858B1 (de) | 2006-05-17 |
| ES2260716T3 (es) | 2006-11-01 |
| DK1527858T3 (da) | 2006-06-12 |
| US20050095099A1 (en) | 2005-05-05 |
| US20080202070A1 (en) | 2008-08-28 |
| EP1527858A3 (de) | 2005-07-27 |
| JP3983756B2 (ja) | 2007-09-26 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69904354T2 (de) | Vorrichtung zum befüllen eines blisterbandes mit gegenständen | |
| EP2807004B2 (de) | Aufschneiden in die packung | |
| US4270910A (en) | Apparatus for separating portions of flat material cut-out from a web or sheet | |
| EP2551203B1 (de) | Verfahren zum Schneiden von Packungen | |
| EP1527858B1 (de) | Stanzstation mit einer Kontrolleinrichtung für Verpackungen | |
| DE102011010601B4 (de) | Verpackungsmaschine zum Herstellen einer Mehrlagenpackung | |
| EP1598276B1 (de) | Verpackungsmaschine und Verfahren zum Schneiden von Packungen | |
| DE60120539T2 (de) | Maschine zum herstellen von Zigarettenpackungen sowie das Verfahren zur Steuerung der Maschine | |
| DE102011115142B4 (de) | Verfahren zum Vereinzeln von Verpackungen | |
| EP2463204A2 (de) | Verpackungsanlage mit Sortierstation | |
| DE102008019028A1 (de) | Verfahren und Vorrichtung zum Stapeln verpackter Lebensmittelscheiben | |
| DE102010034675A1 (de) | Portionsbildung beim mehrspurigen Aufschneiden | |
| EP0613819B1 (de) | Verfahren und Vorrichtung zum Herstellen einer Blister-Karton-Packung | |
| DE2556044C3 (de) | Vorrichtung zum Öffnen und Entleeren von Zigarettenpackungen | |
| EP4490044B1 (de) | Vorrichtung und verfahren zum handhaben von zuschnitten für eine umhüllung von packungen für produkte der zigarettenindustrie | |
| EP1238921B1 (de) | Trinkhalmanbringvorrichtung und -verfahren | |
| EP4000824B1 (de) | Vorrichtung zum zuschneiden von lebensmittelverpackungen entlang einer längsrichtung und verfahren zum betreiben einer solchen vorrichtung | |
| WO2014040952A1 (de) | Verfahren zur korrektur von portionen in verpackungsmulden | |
| WO2023147998A1 (de) | Anlage und verfahren zum verpacken von lebensmittelprodukten | |
| WO2012076152A1 (de) | Verpackungsmachine mit einer randstreifenausbringung | |
| DE60305499T2 (de) | Verfahren zur entfernung einer packungsfolie von palettengebinden | |
| DE2639216C2 (de) | Verfahren und Vorrichtung zum Abtrennen von Zuschnitten für Zigarettenpackungen oder dgl. vom vorderen Ende einer fortlaufenden Materialbahn | |
| DE19706561C2 (de) | Verfahren zum Entfernen von pharmazeutischen und anderen Produkten aus kindergesicherten oder feuchtigkeitsgeschützten, nichtdurchdrückbaren Blisterverpackungen und Blisterentleerungsmaschine | |
| DE10314807A1 (de) | Verfahren zur getrennten Aussonderung von fehlerhaften Gegenständen, insbesondere von Streifenpackungen, beim Überführen von einer Verpackungslinie zu einer Transportlinie | |
| EP3116793B1 (de) | Vorrichtung zum trennen von zu behältergruppen verbundenen behältern und entsprechendes verfahren |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL HR LT LV MK |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL HR LT LV MK |
|
| 17P | Request for examination filed |
Effective date: 20050625 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: CH Ref legal event code: NV Representative=s name: ISLER & PEDRAZZINI AG |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 502004000577 Country of ref document: DE Date of ref document: 20060622 Kind code of ref document: P |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20060607 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060630 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060630 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061017 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2260716 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20070220 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20070517 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DK Payment date: 20070604 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20070629 Year of fee payment: 4 Ref country code: IE Payment date: 20070629 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PCAR Free format text: ISLER & PEDRAZZINI AG;POSTFACH 1772;8027 ZUERICH (CH) |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20070412 Year of fee payment: 4 |
|
| BERE | Be: lapsed |
Owner name: UHLMANN PAC-SYSTEME G.M.B.H. & CO. KG Effective date: 20060630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060818 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20060626 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061118 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20080624 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20060517 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20080423 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20080502 Year of fee payment: 5 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20090101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080626 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080630 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080630 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20080627 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080627 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090106 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20090626 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20100226 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090626 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090627 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100917 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080626 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20140630 Year of fee payment: 11 Ref country code: IT Payment date: 20140617 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502004000577 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160101 |