EP1612329A1 - Revêtement de rouleau en matière composite renforcée de fibres - Google Patents
Revêtement de rouleau en matière composite renforcée de fibres Download PDFInfo
- Publication number
- EP1612329A1 EP1612329A1 EP05103508A EP05103508A EP1612329A1 EP 1612329 A1 EP1612329 A1 EP 1612329A1 EP 05103508 A EP05103508 A EP 05103508A EP 05103508 A EP05103508 A EP 05103508A EP 1612329 A1 EP1612329 A1 EP 1612329A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- fiber
- component
- roll cover
- roll
- fiber composite
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000000835 fiber Substances 0.000 title claims abstract description 173
- 239000011208 reinforced composite material Substances 0.000 title 1
- 239000000945 filler Substances 0.000 claims abstract description 73
- 239000011159 matrix material Substances 0.000 claims abstract description 66
- 239000000203 mixture Substances 0.000 claims abstract description 51
- 238000000034 method Methods 0.000 claims abstract description 42
- 239000000463 material Substances 0.000 claims abstract description 30
- 229920005989 resin Polymers 0.000 claims abstract description 27
- 239000011347 resin Substances 0.000 claims abstract description 27
- 238000009826 distribution Methods 0.000 claims abstract description 19
- 239000002131 composite material Substances 0.000 claims description 34
- 229920000647 polyepoxide Polymers 0.000 claims description 8
- -1 for example Substances 0.000 claims description 7
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims description 6
- 239000004760 aramid Substances 0.000 claims description 6
- 229920003235 aromatic polyamide Polymers 0.000 claims description 6
- 229910052799 carbon Inorganic materials 0.000 claims description 6
- 239000003822 epoxy resin Substances 0.000 claims description 6
- 239000011521 glass Substances 0.000 claims description 6
- 239000004696 Poly ether ether ketone Substances 0.000 claims description 5
- 239000004734 Polyphenylene sulfide Substances 0.000 claims description 5
- 239000004743 Polypropylene Substances 0.000 claims description 5
- JUPQTSLXMOCDHR-UHFFFAOYSA-N benzene-1,4-diol;bis(4-fluorophenyl)methanone Chemical compound OC1=CC=C(O)C=C1.C1=CC(F)=CC=C1C(=O)C1=CC=C(F)C=C1 JUPQTSLXMOCDHR-UHFFFAOYSA-N 0.000 claims description 5
- 239000003795 chemical substances by application Substances 0.000 claims description 5
- 230000001419 dependent effect Effects 0.000 claims description 5
- 229910052751 metal Inorganic materials 0.000 claims description 5
- 239000002184 metal Substances 0.000 claims description 5
- 229920002530 polyetherether ketone Polymers 0.000 claims description 5
- 229920000069 polyphenylene sulfide Polymers 0.000 claims description 5
- 229920005749 polyurethane resin Polymers 0.000 claims description 5
- 229920001169 thermoplastic Polymers 0.000 claims description 5
- 239000004416 thermosoftening plastic Substances 0.000 claims description 5
- ZOXJGFHDIHLPTG-UHFFFAOYSA-N Boron Chemical compound [B] ZOXJGFHDIHLPTG-UHFFFAOYSA-N 0.000 claims description 3
- 229910052796 boron Inorganic materials 0.000 claims description 3
- 239000004643 cyanate ester Substances 0.000 claims description 3
- 238000002347 injection Methods 0.000 claims description 3
- 239000007924 injection Substances 0.000 claims description 3
- 150000002739 metals Chemical class 0.000 claims description 3
- 229920001568 phenolic resin Polymers 0.000 claims description 3
- 239000005011 phenolic resin Substances 0.000 claims description 3
- 229920000728 polyester Polymers 0.000 claims description 3
- 229920001155 polypropylene Polymers 0.000 claims description 3
- 239000004698 Polyethylene Substances 0.000 claims description 2
- 239000000919 ceramic Substances 0.000 claims description 2
- 150000001913 cyanates Chemical class 0.000 claims description 2
- 229920006258 high performance thermoplastic Polymers 0.000 claims description 2
- 239000012784 inorganic fiber Substances 0.000 claims description 2
- 150000001247 metal acetylides Chemical class 0.000 claims description 2
- 239000004810 polytetrafluoroethylene Substances 0.000 claims description 2
- 229920001343 polytetrafluoroethylene Polymers 0.000 claims description 2
- 229920003225 polyurethane elastomer Polymers 0.000 claims description 2
- 239000012815 thermoplastic material Substances 0.000 claims description 2
- 150000002118 epoxides Chemical class 0.000 claims 1
- 239000004634 thermosetting polymer Substances 0.000 claims 1
- 238000004519 manufacturing process Methods 0.000 abstract description 8
- 239000004848 polyfunctional curative Substances 0.000 abstract description 8
- 238000002156 mixing Methods 0.000 abstract description 6
- 239000002245 particle Substances 0.000 abstract description 3
- 150000001875 compounds Chemical class 0.000 abstract 4
- 230000007423 decrease Effects 0.000 description 4
- 229920001187 thermosetting polymer Polymers 0.000 description 4
- 229920000049 Carbon (fiber) Polymers 0.000 description 3
- 239000004917 carbon fiber Substances 0.000 description 3
- 238000009730 filament winding Methods 0.000 description 3
- 238000003475 lamination Methods 0.000 description 3
- 238000005299 abrasion Methods 0.000 description 2
- 239000004841 bisphenol A epoxy resin Substances 0.000 description 2
- 238000011161 development Methods 0.000 description 2
- 230000018109 developmental process Effects 0.000 description 2
- 229920001971 elastomer Polymers 0.000 description 2
- 238000009499 grossing Methods 0.000 description 2
- 239000002105 nanoparticle Substances 0.000 description 2
- 239000004593 Epoxy Substances 0.000 description 1
- 239000002318 adhesion promoter Substances 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 229910052782 aluminium Inorganic materials 0.000 description 1
- 150000001412 amines Chemical class 0.000 description 1
- 150000004982 aromatic amines Chemical class 0.000 description 1
- 239000004842 bisphenol F epoxy resin Substances 0.000 description 1
- 239000003054 catalyst Substances 0.000 description 1
- 238000004132 cross linking Methods 0.000 description 1
- ZBCBWPMODOFKDW-UHFFFAOYSA-N diethanolamine Chemical compound OCCNCCO ZBCBWPMODOFKDW-UHFFFAOYSA-N 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000000806 elastomer Substances 0.000 description 1
- 230000005670 electromagnetic radiation Effects 0.000 description 1
- 125000003700 epoxy group Chemical group 0.000 description 1
- 239000004744 fabric Substances 0.000 description 1
- 239000007789 gas Substances 0.000 description 1
- 239000003365 glass fiber Substances 0.000 description 1
- 230000002401 inhibitory effect Effects 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 229910044991 metal oxide Inorganic materials 0.000 description 1
- 150000004706 metal oxides Chemical class 0.000 description 1
- TWNQGVIAIRXVLR-UHFFFAOYSA-N oxo(oxoalumanyloxy)alumane Chemical compound O=[Al]O[Al]=O TWNQGVIAIRXVLR-UHFFFAOYSA-N 0.000 description 1
- 230000002093 peripheral effect Effects 0.000 description 1
- 230000002787 reinforcement Effects 0.000 description 1
- 238000004073 vulcanization Methods 0.000 description 1
Images

Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F3/00—Press section of machines for making continuous webs of paper
- D21F3/02—Wet presses
- D21F3/08—Pressure rolls
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21G—CALENDERS; ACCESSORIES FOR PAPER-MAKING MACHINES
- D21G1/00—Calenders; Smoothing apparatus
- D21G1/02—Rolls; Their bearings
- D21G1/0233—Soft rolls
Definitions
- the invention relates to a roll cover made of a fiber composite material and a method for its production.
- Roll coverings made of fiber composite materials are used in web-processing machines in a variety of ways. The most demanding requirements are placed on elastic calendar covers with regard to compressive stress and dynamic stress on paper machines. These covers are usually constructed of fiber composite material.
- the so-called filament winding method in which fiber bundles are wound onto a roll body and then joined together by means of resins to form a fiber composite material.
- the disadvantage is that the finished roll cover is made up of different layers.
- the interface between different layers is often here, due to the sudden change in material properties, the starting point for Delaminationserscheinonne in roll cover.
- the second application method is not suitable, for example, for the production of wear layers to be brought into contact with the paper web in straighteners, since such roll shells lead to an uneven smoothing of the paper web, since the wound fibers are substantially rectified.
- roller covers produced by the filament winding method are additionally provided with one or more laminated layers, which takes over the function of the wear layer.
- roller covers are created here, which are composed of several different layers.
- roller covers known from the prior art it is the object of the present invention to propose a roller cover and a method for its production, in which the o. Disadvantages are prevented.
- the present invention is based on the idea that the load capacity of roll coverings can be increased by inhibiting a step-by-step change in the material properties as a result of the lamination process. Accordingly, the present invention provides a fiber composite roll cover made of a material with a fiber component and with a matrix component in which the material composition of fiber component and matrix component changes quantitatively and qualitatively at least in sections continuously.
- a matrix component is to be understood as meaning the material or the material composition in which other dissolved or undissolved materials are embedded.
- the fiber component is embedded in the matrix component.
- the invention thus provides, at least in sections, a roll cover without boundary layers, since the material composition of the roll cover changes continuously in sections.
- a roll cover which has a continuous course of characteristic properties such as, for example, Young's modulus, fracture toughness, abrasion resistance or hardness.
- the material of the roll cover has a filler component, wherein the material composition of fiber component and / or matrix component and / or filler component changes continuously at least in sections.
- a roll cover At a roll cover a variety of requirements are made. So it is e.g. often necessary that a roll cover is dimensionally stable and at the same time has a high wear resistance.
- the dimensional stability is realized here by the radially inward areas.
- the wear resistance is realized by the radially outward areas.
- a preferred embodiment of the invention therefore provides that the material composition in the axial direction and / or in the radial direction of the roll cover changes continuously at least in sections.
- the material composition of the roll cover material can change continuously.
- the proportion of the material composition of at least one of the components namely the fiber component and / or the matrix component and / or the filler component, to change.
- the proportion of the fiber component in the radial direction it is possible for the proportion of the fiber component in the radial direction to be reduced from 30% to 5% to the outside, whereas the proportion of the matrix component increases correspondingly while the proportion of the filler component remains the same.
- composition of one or more of the components changes.
- the fiber component is preferably formed by one or more fiber types.
- a change in the composition of the fiber component should be understood to mean that the proportion and / or the diameter and / or the length distribution and / or the orientation of the fibers of at least one fiber type change.
- a desired property profile of the roll cover can be adjusted depending on the location.
- the stability can be influenced location-dependent.
- the tensile strength is heavily dependent on the orientation of the fibers.
- the matrix component preferably comprises one or more resin types and one or more types of curing agents.
- a change in the composition of the matrix component should be understood to mean that the mixing ratio of at least one type of resin and / or at least one hardener component in the matrix component changes.
- the mixing ratio of at least one type of resin changes while maintaining the hardness in the radial direction of the roll cover, in which the proportion of epoxy resin from the interior of the roll cover towards the outside (paper side) of the roll cover from 100% to 0% continuously decreases whereas the proportion of polyurethane resin inversely increases from 0% to 100% in the direction of the outside of the roll cover from the inside of the roll cover.
- a roll cover is produced, which has a paper-side wear layer of polyurethane resin and a base layer of epoxy resin, wherein the two layers merge continuously in the radial direction.
- the filler component is preferably formed by one or more types of fillers.
- a change in the composition of the filler component should be understood to mean that the proportion and / or the grain size of at least one filler type changes.
- Preferred fiber types include inorganic fibers of glass, metal, ceramic fibers, boron or organic fibers, for example carbon and / or aramid and / or polypropylene or polyester or high-performance thermoplastics such as, for example, PPS or PEEK or PTFE fibers.
- the fiber component consists of only one type of fiber
- the proportion of one fiber type for example glass fibers
- the proportion of the fiber component in the material composition can be changed continuously in the radial direction.
- a preferred embodiment of the invention provides that at least one fiber type is formed by fiber pieces with a defined length distribution, which are not connected to one another before being embedded in the matrix component.
- Fiber pieces should be understood in this context that the fibers are not formed as fiber bundles (in contrast to filament winding process) or as fiber mats (in contrast to the lamination process). Rather, pieces of fiber having a defined length distribution prior to embedding in the matrix component are discrete, i.e., loose. unconnected fiber pieces.
- a preferred embodiment of the invention provides that at least one type of fiber comprises a portion of fiber pieces embedded in an undirected orientation in the matrix component.
- a preferred embodiment of the invention provides that at least one fiber type from the range of inorganic and / or organic fibers (elastomer, thermoplastics or thermosets) fiber pieces with a length distribution of 0.1 to 100 mm, preferably from 1 to 30mm, more preferably from 1 up to 3 mm and / or from 3 to 10 mm, preferably fibers of aramid and / or glass and / or carbon.
- fibers from the range of inorganic and / or organic fibers (elastomer, thermoplastics or thermosets) fiber pieces with a length distribution of 0.1 to 100 mm, preferably from 1 to 30mm, more preferably from 1 up to 3 mm and / or from 3 to 10 mm, preferably fibers of aramid and / or glass and / or carbon.
- the types of resins used are preferably elastomeric or thermosetting resins. Accordingly, one embodiment of the invention provides that at least one type of resin is an elastomeric or thermosetting resin (epoxies, cyanate esters, phenolic resins), but also thermoplastic materials (PE, PP, PPS, PEEK, ...) and / or mixtures thereof.
- elastomeric or thermosetting resin epoxies, cyanate esters, phenolic resins
- thermoplastic materials PE, PP, PPS, PEEK, ...) and / or mixtures thereof.
- a duroplastic resin for example, epoxy resin or cyanate ester resins also phenolic resins may be mentioned.
- bisphenol A epoxy resins with amine hardener wherein the proportions hardener per 100 parts of resin in the range 0 to 300 parts (eg Ancamine 2390 [Air Products] 107 parts), but especially 5 to 40 parts, particularly preferably 5 to 25 parts.
- the crosslinking can also be prepared by catalysts that crosslink the epoxy resin three-dimensionally without curing agents.
- the elastomeric resins polyurethane resin or rubber is used as the elastomeric resins.
- preferred embodiments of the invention provide for use as fillers wear-reducing fillers and / or fillers influencing the viscosity and / or fillers influencing the surface tension and / or fillers influencing the conductivity.
- Carbide or metals or oxides such as, for example, Cr, Fe, Al or their oxides are preferably used as wear-reducing filler types, in a range from 0 to 100% by weight, in particular in a range from 10 to 60% by weight. %, more preferably in a range of 20 to 50 wt.%.
- Thermoplastics or ionic fillers are preferably used as fillers influencing the surface tension, in a range from 0 to 60% by weight, in particular 5 to 20% by weight, to achieve a surface tension of 20 to 70mN / m, preferably 25 to 56mN / m. more preferably from 25 to 48mN / m.
- the filler types may have a grain size in the nanometer and / or micrometer and / or millimeter range, i. Filler types are conceivable which only have particle sizes in the nanometer range as well as filler types which have a particle size distribution from the nanometer range to the millimeter range.
- An embodiment of the method according to the invention provides that a filler component is likewise applied with the fiber component and the matrix component.
- a continuous change of the fiber component can be adjusted if the fiber component is formed by one or more fiber types, wherein prior to application of the fiber component at least one fiber type loose fiber pieces are produced with a defined length distribution. Furthermore, it is particularly easy to distribute the loose fiber pieces with a defined length distribution undirected, whereby the roll cover on the one hand has a lower tendency to mark and on the other hand in all directions of the layer in which the loose fibers are arranged has an equal stability.
- the process according to the invention is particularly simple and cost-effective if the fiber component and / or the matrix component and / or the filler component are applied by an injection process; An application by combining syringes and sprinkling of the fillers is also possible.
- the composition and / or the proportion of the applied fiber component and / or the applied matrix component and / or the applied filler component is dependent on the axial and / or radial position of the application location on the roll body.
- a concrete embodiment of the method provides that the material of the roll cover is applied to the roll body with an applicator, wherein the applicator can move in the axial and / or in the radial direction of the roll body.
- the material composition can be adjusted in the axial direction. This can be constant both in the axial direction as well as varüeren.
- the feed rate of the application device in the axial direction is included in the application quantity of the application device.
- the distance to the roller body can be adjusted and thus specifically the mixing and the impact density, for example, the fiber component, the matrix component or the filler component can be controlled.
- a preferred embodiment of the invention provides that the roller body rotates during application about its axial axis, whereby a uniform thickness in the circumferential direction of the roll cover can be produced.
- the peripheral speed of the roller body is an important factor for the order quantity.
- a plurality of application devices are provided, which are arranged, for example, in the circumferential direction at different positions. With this configuration, it is possible to further improve the continuous blending of fiber component, matrix component and filler component.
- the roll cover is applied in one layer or in several layers.
- a particularly preferred development of the method according to the invention provides that the roll cover is cured in a pressurized or overpressure atmosphere.
- the air released from the fiber composite material can be sucked through the negative pressure, whereby a bubble-free and pore-free roll cover can be produced.
- curing by means of electromagnetic radiation such as UV light or microwaves is possible.
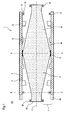
- FIG. 1 shows a roll 1 with a roll cover 8 according to the invention in side view.
- the roll cover according to the invention was applied to a roll body 4 by the method according to the invention.
- the roll cover 8 has a roll side 2 and a paper or wear side 3.
- the roll cover 8 is applied to the roll side 2 on the lateral surface 14 of the roller body 4 and connected thereto.
- the roll cover 8 has a fiber component 5, a matrix component 6 and a filler component 9, wherein the fiber component 5 and the filler component 9 are embedded in the matrix component 6.
- the material composition of the roll cover 8, consisting of fiber component 5, matrix component 6 and filler component 9, changes continuously in the radial direction 7 of the roll 1.
- the fiber component 5 is formed by a single type of fiber, for example in the form of carbon fibers 5.
- the composition of the fiber component changes continuously in the radial direction 7 of the roll cover 8, in which the proportion of carbon fibers 5 in the material composition of fiber component 5, matrix component 6 and filler component 9 in the radial direction 7 of Roll cover 8 from the roll side 2 to the paper or wear side 3 decreases continuously and by the length distribution of the carbon fibers 5 in the radial direction 7 of the roll cover 8 from the roll side 2 to the paper or wear side 3 decreases continuously.
- the matrix component 6 is formed by a first matrix type 10 (shown as a white area) and a second matrix type 11 (shown as a black round dots).
- the first matrix type 10 comprises in the present exemplary embodiment an epoxy resin fraction.
- the second matrix type 11 comprises in the present embodiment, a polyurethane resin portion.
- a roll cover 8 is provided which is dimensionally stable and has an abrasion-resistant paper or wear side 3.
- the filler component 9 (shown as black squares) is formed in the present embodiment by a wear-reducing filler, for example, in the form of nanoparticles 9 made of aluminum oxide or the like.
- the proportion of nanoparticles 9 in the radial direction 7 increases continuously from the roll side 2 towards the paper or wear side 3.
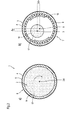
- FIG. 2 shows an arrangement 12 for carrying out the method according to the invention.
- the arrangement is essentially formed by the roll body 4 to be coated with a roll jacket 8 and by an applicator device 18, which is spaced apart from it in the radial direction of the roll body 4.
- roller body 4 of the present embodiment is made of a metallic material. It would also be conceivable that the roller body 8 is at least partially made of a composite material.
- the roller body 4 rotates in the rotational direction 15 about its axial axis of rotation 29 while the applicator 18 moves parallel to the axis of rotation 29 along the direction of movement 16 and optionally additionally can move perpendicular to the axis of rotation 29 along the direction of movement 17.
- the application device 18 has an ejection opening 25 for the exit of loose fiber pieces 26 of the fiber component 5 and an outlet opening 28 for the exit of a mixture 27 of the matrix component 6, the filler component 9 and other components such as. A color component and the like.
- the ejection opening 25 and the outlet opening 28 are set in such a way that the mixture 27 and the loose fiber pieces 26 impinge substantially on the same point of the lateral surface 14 of the roller body 4 and thereby form a fiber composite material.
- the mixture 27 and the loose fiber pieces 26 are thus applied in an injection process in which the loose fiber pieces 26 are embedded in the mixture 27 of matrix component 6, filler component 9 and color component.
- An application of individual components by scattering (not shown) is also possible according to the invention.
- the application device 18 has a feed device 23 for feeding in the fiber component 5.
- the feed device is designed as a feed opening 23 into which the fiber component 5 is introduced.
- the supplied fiber component 5 is in the form of long fiber strands.
- a crushing device 29 is provided between the feed opening 23 and the discharge opening 25, a crushing device 29 is provided.
- the introduced fiber component 5 is comminuted into loose fiber pieces 26 having a defined length distribution.
- the applicator 18 has feed openings 19, 20, 21 and 22 for feeding the matrix component 6, the filler component 9 (also pre-bleached with another component, for example, resin) and the color component.
- the matrix component 6 typically comprises one or more resin types and one or more types of curing agents.
- the resin type (s) of the application device 18 are supplied via the feed opening 19.
- the hardener type or types are supplied to the application device 18 via the feed opening 20.
- the filler component 9 and the color component are supplied to the application device 18 via the feed openings 21 and 22, respectively.
- the supplied matrix component 6, the filler component 9 and the color component are mixed to form the mixture 27, which is injected via the outlet opening 28 onto the roll body 4 to produce a roll cover 8 according to the invention.
- the loose fiber pieces 26 of the fiber component 5 and the mixture 27 of matrix component 6 and filler component 9 by rotating the roller body 4 and by moving the applicator 18 along the direction of movement 16 at different locations applied to the roll body 4, wherein the composition of loose fiber pieces 26 and mixture 27 and the composition of the loose Fasem 26 and / or the mixture 27 itself is set depending on the axial and / or radial position of the location on the roll body 4 to achieve that the material composition of fiber component 5, matrix component 6 and filler component 9 according to the invention, according to the respective requirements of the roll cover 8, at least in sections continuously changes.
- the fiber component 5 is formed by one or more types of fibers, such as glass or carbon or aramid or boron or polypropylene or polyester or PPS or PEEK fibers and / or that the composition the fiber component 5 changes, in which the proportion and / or the diameter and / or the length distribution and / or the orientation of the fiber pieces of at least one fiber type changes.
- the loose fiber pieces have a length distribution of 1 to 10 mm, preferably from 1 to 3 mm and / or from 3 to 10 mm, wherein the length distribution according to the invention depending on the axial and radial position of the location on which these are applied to the roll body 4 may vary or varies.
- the matrix component 6 is formed by one or more resin types and by one or more types of hardeners.
- resin types for example, elastomeric and / or thermoplastic and / or thermosetting resins are conceivable.
- the composition of the matrix component 6 changes, for example, in that the mixing ratio and the components of at least one type of resin and / or at least one hardener component changes, for example the change from a bisphenol A epoxy resin type to a bisphenol F epoxy resin type and / or a variation of aromatic and / or aliphatic amine hardeners.
- the filler component is formed by one or more types of filler, wherein as fillers, for example, wear-reducing fillers and / or viscosity-influencing fillers and / or surface tension influencing fillers and / or conductivity-influencing fillers can be used.
- wear-reducing filler types are carbides or metals or oxides such as metal oxides such as Cr oxide, Fe oxide or Al oxide or fiber pulp of carbon and / or aramid and / or glass in the size range of 1 to 1000 .mu.m, preferably 5 to 100 .mu.m conceivable , Thermoplastics or ionic fillers are conceivable as fillers influencing the surface tension.
- the composition of the filler component changes, for example, in which the proportion and / or the grain size of at least one filler type changes.
- at least one type of filler may have a grain size in the nanometer and / or micrometer and / or millimeter range.
- a typical rubber cover can be applied to the fiber composite roll cover 8 according to the invention, which is crosslinked by vulcanization.
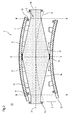
- FIG. 3 shows a further arrangement 30 for carrying out the method according to the invention.
- a plurality of application devices 31, 32 and 33 are provided, which are arranged one behind the other in the circumferential direction of the roll body 4 to be coated with a roll cover 8.
Landscapes
- Rolls And Other Rotary Bodies (AREA)
- Yarns And Mechanical Finishing Of Yarns Or Ropes (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102004025116A DE102004025116A1 (de) | 2004-05-21 | 2004-05-21 | Faserverbund Walzenbezug |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1612329A1 true EP1612329A1 (fr) | 2006-01-04 |
| EP1612329B1 EP1612329B1 (fr) | 2009-06-24 |
| EP1612329B2 EP1612329B2 (fr) | 2013-01-09 |
Family
ID=35124569
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05103508A Expired - Lifetime EP1612329B2 (fr) | 2004-05-21 | 2005-04-28 | Revêtement de rouleau en matière composite renforcée de fibres |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP1612329B2 (fr) |
| AT (1) | ATE434683T1 (fr) |
| DE (2) | DE102004025116A1 (fr) |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2010079261A1 (fr) | 2009-01-07 | 2010-07-15 | Metso Paper, Inc. | Rouleau de machine à voile de fibre et calandre à voile de fibre |
| WO2011035969A1 (fr) * | 2009-09-23 | 2011-03-31 | Voith Patent Gmbh | Revêtement de rouleau |
| CN101454505B (zh) * | 2006-06-30 | 2011-11-09 | 美卓造纸机械公司 | 弹性辊覆层、带覆层的辊和制造带覆层辊的方法 |
| WO2013160117A1 (fr) * | 2012-04-27 | 2013-10-31 | Voith Patent Gmbh | Rouleau et son procédé de fabrication |
| CN104204347A (zh) * | 2012-03-30 | 2014-12-10 | 福伊特专利公司 | 辊包覆物 |
| CN104220670A (zh) * | 2012-03-30 | 2014-12-17 | 福伊特专利公司 | 制造辊包覆物的方法以及辊包覆物 |
| CN113167027A (zh) * | 2018-12-04 | 2021-07-23 | 安德里茨库斯特斯有限责任公司 | 辊子及辊子的制造方法 |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102006021035B4 (de) * | 2006-04-27 | 2014-03-06 | Paul Sauer Gmbh & Co. Walzenfabrik Kg | Walze mit elastomerer Beschichtung |
| DE102009000738A1 (de) * | 2009-02-10 | 2010-08-12 | Voith Patent Gmbh | Biegeeinstellwalze |
| DE102009028210A1 (de) * | 2009-08-04 | 2011-02-17 | Voith Patent Gmbh | Selbstkonditionierende Walzenbeschabung |
| DE102012205221A1 (de) | 2012-03-30 | 2013-10-02 | Voith Patent Gmbh | Walzenbezug |
| DE102015213512A1 (de) * | 2015-07-17 | 2017-01-19 | Voith Patent Gmbh | Verfahren zur Herstellung eines Walzenbezugs |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0487477A1 (fr) * | 1990-11-19 | 1992-05-27 | Valmet Paper Machinery Inc. | Methode pour revêtir un rouleau et revêtement de rouleau |
| EP0487447A1 (fr) | 1990-11-17 | 1992-05-27 | HILTI Aktiengesellschaft | Outils de coupe, de forage et de burinage equipés de metal dur ou de matériau dur |
| WO1994009208A1 (fr) | 1992-10-16 | 1994-04-28 | Beloit Technologies, Inc. | Procede de fabrication d'une enveloppe pour un rouleau exprimeur |
| EP0924337A2 (fr) * | 1997-12-17 | 1999-06-23 | Voith Sulzer Papiertechnik Patent GmbH | Rouleau de presse |
| DE19925421A1 (de) | 1999-06-02 | 2000-12-07 | Voith Sulzer Papiertech Patent | Elastische Walze und Verfahren zum Herstellen einer solchen |
| US6319185B1 (en) | 1999-03-31 | 2001-11-20 | Voith Sulzer Papiertechnik Patent Gmbh | Resilient roll and process for producing such a roll |
| US20020045523A1 (en) | 2000-09-18 | 2002-04-18 | Voith Paper Patent Gmbh | Elastic roll |
-
2004
- 2004-05-21 DE DE102004025116A patent/DE102004025116A1/de not_active Withdrawn
-
2005
- 2005-04-28 EP EP05103508A patent/EP1612329B2/fr not_active Expired - Lifetime
- 2005-04-28 DE DE502005007553T patent/DE502005007553D1/de not_active Expired - Lifetime
- 2005-04-28 AT AT05103508T patent/ATE434683T1/de active
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0487447A1 (fr) | 1990-11-17 | 1992-05-27 | HILTI Aktiengesellschaft | Outils de coupe, de forage et de burinage equipés de metal dur ou de matériau dur |
| EP0487477A1 (fr) * | 1990-11-19 | 1992-05-27 | Valmet Paper Machinery Inc. | Methode pour revêtir un rouleau et revêtement de rouleau |
| WO1994009208A1 (fr) | 1992-10-16 | 1994-04-28 | Beloit Technologies, Inc. | Procede de fabrication d'une enveloppe pour un rouleau exprimeur |
| EP0924337A2 (fr) * | 1997-12-17 | 1999-06-23 | Voith Sulzer Papiertechnik Patent GmbH | Rouleau de presse |
| US6319185B1 (en) | 1999-03-31 | 2001-11-20 | Voith Sulzer Papiertechnik Patent Gmbh | Resilient roll and process for producing such a roll |
| DE19925421A1 (de) | 1999-06-02 | 2000-12-07 | Voith Sulzer Papiertech Patent | Elastische Walze und Verfahren zum Herstellen einer solchen |
| US20020045523A1 (en) | 2000-09-18 | 2002-04-18 | Voith Paper Patent Gmbh | Elastic roll |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101454505B (zh) * | 2006-06-30 | 2011-11-09 | 美卓造纸机械公司 | 弹性辊覆层、带覆层的辊和制造带覆层辊的方法 |
| WO2010079261A1 (fr) | 2009-01-07 | 2010-07-15 | Metso Paper, Inc. | Rouleau de machine à voile de fibre et calandre à voile de fibre |
| WO2011035969A1 (fr) * | 2009-09-23 | 2011-03-31 | Voith Patent Gmbh | Revêtement de rouleau |
| CN104204347A (zh) * | 2012-03-30 | 2014-12-10 | 福伊特专利公司 | 辊包覆物 |
| CN104220670A (zh) * | 2012-03-30 | 2014-12-17 | 福伊特专利公司 | 制造辊包覆物的方法以及辊包覆物 |
| WO2013160117A1 (fr) * | 2012-04-27 | 2013-10-31 | Voith Patent Gmbh | Rouleau et son procédé de fabrication |
| CN104254646A (zh) * | 2012-04-27 | 2014-12-31 | 福伊特专利公司 | 辊以及制造辊的方法 |
| CN113167027A (zh) * | 2018-12-04 | 2021-07-23 | 安德里茨库斯特斯有限责任公司 | 辊子及辊子的制造方法 |
| CN113167027B (zh) * | 2018-12-04 | 2023-08-29 | 安德里茨库斯特斯有限责任公司 | 辊子及辊子的制造方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP1612329B1 (fr) | 2009-06-24 |
| DE502005007553D1 (de) | 2009-08-06 |
| DE102004025116A1 (de) | 2005-12-08 |
| ATE434683T1 (de) | 2009-07-15 |
| EP1612329B2 (fr) | 2013-01-09 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69634136T2 (de) | Beschichtete rolle und verfahren zu ihrer herstellung | |
| EP1310316B1 (fr) | Scie à fil | |
| EP1612329B2 (fr) | Revêtement de rouleau en matière composite renforcée de fibres | |
| DE4226789A1 (de) | Faserverstärkte Kunststoffwalze mit äußerer, verschleißfester, füllerhaltiger Kunststoffschicht | |
| EP0655561A1 (fr) | Rouleau en matière plastique renforcée de fibres à surface rainurée en losanges | |
| EP0229983A2 (fr) | Meule anti-bruit | |
| EP1943369B1 (fr) | Procede de revetement d'un composant | |
| EP1976697B1 (fr) | Procédé de production d'un élément de revêtement | |
| EP2841648A1 (fr) | Rouleau et son procédé de fabrication | |
| DE102014213294A1 (de) | Verfahren zur Herstellung von Prothesen-Formteilen aus faserverstärktem Kunststoff | |
| EP3651936B1 (fr) | Meule en éventail pour meuleuse d'angle | |
| DE2639845C3 (de) | Verfahren zum Ausbilden einer verschleißbeständigen Beschichtung auf der Innenoberfläche eines Rohres | |
| EP3490782B1 (fr) | Procédé pour la fabrication d'une pièce composite à fibres multicouche, tridimensionnelle | |
| AT502579A1 (de) | Faserverbund walzenbezug | |
| EP2105211B1 (fr) | Procédé de revêtement d'une lame | |
| EP1116892B1 (fr) | Rouleau élastique et procédé de fabrication d' un tel rouleau | |
| DE102011075179B4 (de) | Zur Herstellung der Konstruktion einer Faserbahnmaschinen-Walze bestimmtes Verfahren, Mantelkonstruktion einer Faserbahnmaschinen-Walze und Walze einer Faserbahnmaschine | |
| EP1470868A2 (fr) | Procédé pour revêtir un corps cylindrique | |
| EP2274156B1 (fr) | Procédé de fabrication d'un rouleau pour l'usinage d'un matériau en forme de bande et rouleau fabriqué conformément à ce procédé | |
| EP1586703A1 (fr) | Surface pour un dispositif de traitement et procédé de fabrication d'un tel dispositif de traitement | |
| DE9318285U1 (de) | Mit Fasern verstärkte Kunststoffwalze mit Rautierung | |
| EP1082206A1 (fr) | Bras de chargement | |
| DE1729771A1 (de) | Verfahren zur Herstellung eines Verstaerkungselementes fuer Gegenstaende aus Gummi | |
| DE4235226C1 (de) | Bahnleitwalze | |
| WO2004092599A1 (fr) | Procede de revetement de rouleaux et rouleau muni d'un revetement |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR LV MK YU |
|
| 17P | Request for examination filed |
Effective date: 20060704 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: VOITH PATENT GMBH |
|
| 17Q | First examination report despatched |
Effective date: 20070228 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REF | Corresponds to: |
Ref document number: 502005007553 Country of ref document: DE Date of ref document: 20090806 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090924 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091005 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091024 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090924 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091024 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: METSO PAPER, INC. Effective date: 20100324 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090925 |
|
| BERE | Be: lapsed |
Owner name: VOITH PATENT G.M.B.H. Effective date: 20100430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20100428 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20101230 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100428 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091225 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100428 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| PUAH | Patent maintained in amended form |
Free format text: ORIGINAL CODE: 0009272 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT MAINTAINED AS AMENDED |
|
| 27A | Patent maintained in amended form |
Effective date: 20130109 |
|
| AK | Designated contracting states |
Kind code of ref document: B2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R102 Ref document number: 502005007553 Country of ref document: DE Effective date: 20130109 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090624 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20150413 Year of fee payment: 11 Ref country code: DE Payment date: 20150421 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20150421 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502005007553 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 434683 Country of ref document: AT Kind code of ref document: T Effective date: 20160428 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161101 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160428 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160428 |