EP1634664A1 - Dispositif de fabrication des muselets semi-finis, à partir d'un fil en métal, pour des bouteilles - Google Patents
Dispositif de fabrication des muselets semi-finis, à partir d'un fil en métal, pour des bouteilles Download PDFInfo
- Publication number
- EP1634664A1 EP1634664A1 EP04425670A EP04425670A EP1634664A1 EP 1634664 A1 EP1634664 A1 EP 1634664A1 EP 04425670 A EP04425670 A EP 04425670A EP 04425670 A EP04425670 A EP 04425670A EP 1634664 A1 EP1634664 A1 EP 1634664A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- actuating
- jaws
- metal wire
- axes
- pair
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21F—WORKING OR PROCESSING OF METAL WIRE
- B21F45/00—Wire-working in the manufacture of other particular articles
- B21F45/04—Wire-working in the manufacture of other particular articles of elements, e.g. levers or links, for bottle stoppers
Definitions
- the present invention relates to a device for semi-finished products made of metal wire, in particular for the manufacture of retention cages for bottles containing sparkling drinks.
- retention cages comprise a reticular body positioned on a cap of the bottle and a circumferential retention ring connected to the reticular body to secure the reticular body to the bottle.
- the cages are obtained by plastic deformation of a metal wire thanks to automated machines which comprise a first station for forming the reticular body and a second station for mounting the retention ring on the reticular body.
- Machines commonly used to obtain the reticular bodies comprise in a same plane four pincers actuated by a first cam and slidable along a first pair of perpendicular axes and four linear actuators actuated by a second cam and slidable along a second pair of perpendicular axes having the same origin as the first pair of axes and angularly offset in phase by 45 degrees.
- the metal wire is automatically sheared and positioned at the pincers which close gripping it or retaining in an initial circular position so that respective ends are superposed and maintained tight by a single pincer.
- the linear actuators and the pincers move towards the origin of the axes in co-ordinated way, obtaining a cross-shaped body that constitutes the starting semi-finished product for the manufacture of the reticular body.
- the object of the present invention is to provide a device for the manufacture of semi-finished products made of metal wire that is free of the drawbacks described above.
- a further object of the present invention is further to increase the production rate.
- a device for the manufacture of semi-finished products made of metal wire, as defined in claim 1.
- the reference number 1 globally designates a device for the manufacture of semi-finished products made of metal wire, particularly for the manufacture of a reticular body 2 of a cage 3 further comprising a retention ring 4 connected to the reticular body 2 to close a cap of a body containing sparkling drinks.
- the reticular body 2 ( Figure 2) is obtained from a single segment of metal wire and comprises four equidistant uprights 5 obtained by twisting the metal wire and connected to each other by respective curvilinear segments 6 globally delimiting a circular profile 7 closed substantially perpendicular to the uprights 5.
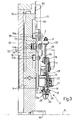
- the reticular body 2 is obtained by means of the device 1, comprising a fixed support 8, four pincer assemblies 9 movable on the fixed support 8 along respective orthogonal axes A having an origin 10 and four tappet linear actuators 11 movable on the fixed support 8 along respective axes B positioned coplanar to and along the bisectors of the axes A.
- Each pincer assembly 9 comprises a gearwheel element 12 rigidly connected to the fixed support 8, a slide 13 movable on the fixed support 8 along the axis A, a mandrel 14 supported rotatably around the axis A by the slide 13 and a pair of jaws of the type 15, 15a depending on whether the pincer assembly 9 respectively grips a single portion of metal wire or two ends of the segment. Both types of jaws 15, 15a are hinged on the mandrel 14 towards the origin 10 and maintained in an open position by an annular spring 16.
- the gearwheel element 12 supports, freely rotatable around the axis A, a shaft 17 comprising at opposite ends a bevel pinion 18 and grooved portion 19 engaging in a corresponding coaxial grooved slot 20 borne by the mandrel 14 and open at the opposite part with respect to the jaws 15, 15a.
- Each pinion 18 is connected to the two pinions 18 of the adjacent pincer assemblies 9 thanks to respective transmission shafts 21 comprising a pair of end bevel gears 22 meshing with the related pinions 18 and globally forming a closed gear transmission 23 driven by an intermittent motor unit 24 connected to one of the transmission shafts 21 to command the simultaneous rotary motion of the jaws 15, 15a.
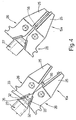
- the jaws 15, 15a are positioned symmetrically to the respective axes A and comprise respective grip portions 25 oriented towards the origin 10 and actuating portions 26 positioned at the opposite part of the grip portions 25 relative to the hinge and superficially co-operating with an end shaped portion 27 connected in detachable way to a respective actuating tappet rod 28 movable along the axis A and slidable in guide holes 29 having the axis A and borne respectively by the mandrel 14 and by the shaft 17.
- Each actuating rod 28 is connected in freely rotatable way around the axis A on a slide support 30 comprising a spring assembly 31 to dampen the impacts in a direction parallel to the axis A.
- each actuating portion 26 has an end projection 32 maintained in contact with the shaped portion 27 of the actuating rod 28 by the action of the annular spring 16 and a pair of planar surfaces 33 which convert towards the origin 10 starting from the end projection 32 and are made of wear-resistant material.
- the shaped portion 27 ( Figure 5) has a pair of planar guide surfaces 34 defining a respective angle ⁇ relative to the axis A to impose the law for opening and closing the jaws 15.
- the shaped portion 27 of the pincer assembly 9 comprising the jaws 15a, i.e. the one which grips the ends of the segment of metal wire, has, at the guide surfaces, 34 a shaped profile 35 ( Figure 6) having starting from an opposite end to the actuating rod 28, a first and a second rectilinear segment 36 inclined by the angle ⁇ relative to the axis A, a concave segment 37 intermediate between the rectilinear segments 36 and a last lateral segment 38 parallel to the axis A and defining a lateral flank of the guide surface 34.
- a desmodromic cam device comprising a disk 50 ( Figure 7) connected to the fixed support 8 slidably around an axis C passing through the origin 10 perpendicularly to the axes A and B and having guide walls 51, 52 respectively for the linear actuators 11 and the slides 13.
- the guide walls 51, 52 are closed and continuous, having respective pairs of rolling surfaces 60, 61 having generatrices parallel to the axis C and co-operate with respective multiplicities of pairs of rollers 53, 54a each borne by the respective linear actuators 11 and by the respective slides 13.
- both the roller 53 and the rollers 54a are positioned at opposite parts of the respective guide walls 51, 52 co-operating with the respective rolling surfaces 60, 61 borne at radially opposite parts of the respective walls 51, 52.
- the disk 50 has a guide groove 55 circumferentially obtained in the guide wall 52 and having a pair of rolling surfaces 62 facing each other and co-operating with four pairs of pulleys 14b having respective axes, parallel to each other and integral with the respective slide supports 30.
- the guide walls 51, 52 and the guide grooves 55 are axially symmetrically having identical sectors every 90° and the slides 13 of the pincer assemblies 9 and the linear actuators 11 are positioned equidistant with respect to the axis C.
- the rolling surfaces 61, 62 have profiles comprising a succession of ascending, descending and circumference arc segments following the teaching, for example, of the patent IT 1264109.
- the rolling surface 60 is obtained similarly in relation to the surface 61 considering that, in the instants in which the linear actuators 11 move simultaneously with the slides 13, the segments of the rolling surfaces 60 must be offset in phase by 45° from the corresponding segments of the rolling surfaces 61.
- the operation of the device 1 is as follows.
- the disk 50 is driven by a motor member not shown herein, rotating at constant speed around the axis C and the guide walls and grooves 51, 52, 55 actuate in simultaneous and mutually identical way respectively the linear actuators 11 and the four slides 13 of the pincer assemblies 9 since they are axially symmetrical and have four identical angular sectors and the actuators 11 and the pincer assemblies 9 are angularly equidistant.
- the cross-shaped body of the reticular body 2 is obtained starting from a step in which the rollers 53, 54a, 54b are in a radially extreme end stop position and the segment of metal wire is positioned in known way between the grip portions 25 according to a circular trace.
- the metal wire is bent forming the cross-shaped body in a plane that is perpendicular to the axis C after defining in continuous way a succession of closed intermediate geometric figures having rectilinear sides and rounded bending vertices both at respective junction portions between arched segments 6 and uprights 5 and at respective bending projections 56 exiting perpendicularly to the respective axis A from the grip portions 25 of the respective jaws 15, 15a.
- the vertices rounded at the jaws 15, 15a are defined by portions of metal wire bend around the bending projections 56 and the perimeter of the intermediate geometric figures can be calculated instant by instant based on the positions of the pincer assemblies 9 and of the linear actuators 11.
- the profiles of the rolling surfaces 60, 61, 62 are radially and circumferentially dimensioned so the percent change in length of the perimeter of the two intermediate geometric figures remains unaltered or may vary within a margin that is smaller than the percentage of yielding or ultimate elongation of any metal wire suitable for working processes by plastic deformation.
- damping heads 59 supported by the respective linear actuators 11 abut against a pivot 60 of axis C and the transmission 23 simultaneously actuates the four mandrels 14 which, rotating around the respective axes A, twist the wire obtaining the uprights 5.
- rollers 54b impose point by point to the respective actuating rods 28 the identical displacements defined by identical radial dimensions every 90 degrees on the rolling surfaces 62 actuating the jaws 15 together with the respective guide surfaces 34.
- the jaws 15a instead, co-operate with the shaped profile 35 integral with the respective actuating rod 28 and being positioned in the opening step along the concave segment 37, follow the entire concave segment 37 and then the rectilinear segment 36 until closing when they reach the rectilinear segment 38. Subsequently, the shaped portion 27 further advances until the rectilinear segments 36 impact with the planar surfaces 33 achieving the locking of the jaws 15a and actuating the spring assembly 31.
- the concave segment 37 locally a slope relative to the upper axis A with respect to the angle ⁇ , allowing a shorter closing time of the jaws 15a which close pressing on the end portions of the metal wire before the jaws 15.
- the jaws 15 are actuated similarly to the manner described above, but following the guide surface 34 and during the closing phase the projection 56 is coupled with a conjugated seat borne by a grip portion 25 opposite to the grip portion 25 having the projection 56 radially locking the segment in the radial direction.
- the jaws 15 close pressing on the metal wire after the jaws 15a, but radially retain the wire already when they are closing, whilst the jaws 15a retain the end portions of the wire only when the respective shaped portion 27 abuts against the actuating portions 26.
- the guide surface 34 and the shaped profile 35 are therefore studied to convert the long and relatively slow travel of the actuating rods 28 actuating by the cam 50 into rapid and shorter displacements of the jaws 15, 15a.
- the jaws 15a can be actuated independently from the jaws 15 to lock more rapidly the two ends which in case of excessively slow closure could escape, requiring the idling of the machine for maintenance purposes.
- the early closure of the jaws 15a stably secures the wire segment and makes more reliable the subsequent grip by the jaws 15, enhancing the precision of the subsequent work processes.
- both the guide surfaces 34 and the shaped profile 35 are dimensioned to obtain a rapid closure reducing the slopes of the rolling surfaces 61, 62 and thus minimising wear.
- the shaped portions 27 can be worked more easily and are less costly than the disk 50 and are easily replaceable enabling to correct any geometric inaccuracies of the guide walls 52 by acting on the geometry of the profile, which can differ from the one described to obtain other laws of motion.
- the choice of appropriate geometry of the rolling surfaces 60, 61, 62 respectively of the guide walls and grooves 51, 52, 55 allows reliably to reach particularly low elongation values, enabling to use various types of metal wires suitable for plastic deformation work processes without breaks.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Wire Processing (AREA)
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP04425670A EP1634664B1 (fr) | 2004-09-08 | 2004-09-08 | Dispositif de fabrication des muselets semi-finis, à partir d'un fil en métal, pour des bouteilles |
| AT04425670T ATE350179T1 (de) | 2004-09-08 | 2004-09-08 | Vorrichtung zur herstellung von halbfertigen sicherheitsdrahtstücken für flaschen aus metalldraht |
| DE602004004126T DE602004004126T2 (de) | 2004-09-08 | 2004-09-08 | Vorrichtung zur Herstellung von halbfertigen Sicherheitsdrahtstücken für Flaschen aus Metalldraht |
| ES04425670T ES2279334T3 (es) | 2004-09-08 | 2004-09-08 | Dispositivo de fabricacion de productos semi-acabados, hechos de alambre metalico para botellas. |
| AU2005209611A AU2005209611B2 (en) | 2004-09-08 | 2005-09-08 | Device for manufacturing semi-finished products made of metal wire |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP04425670A EP1634664B1 (fr) | 2004-09-08 | 2004-09-08 | Dispositif de fabrication des muselets semi-finis, à partir d'un fil en métal, pour des bouteilles |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1634664A1 true EP1634664A1 (fr) | 2006-03-15 |
| EP1634664B1 EP1634664B1 (fr) | 2007-01-03 |
Family
ID=34932749
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP04425670A Expired - Lifetime EP1634664B1 (fr) | 2004-09-08 | 2004-09-08 | Dispositif de fabrication des muselets semi-finis, à partir d'un fil en métal, pour des bouteilles |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP1634664B1 (fr) |
| AT (1) | ATE350179T1 (fr) |
| AU (1) | AU2005209611B2 (fr) |
| DE (1) | DE602004004126T2 (fr) |
| ES (1) | ES2279334T3 (fr) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2025428A1 (fr) * | 2007-07-24 | 2009-02-18 | ME COM S.r.l. | Unité pour la production de cages de sécurité pour les bouchons de bouteilles de boissons effervescentes |
| ITMO20080312A1 (it) * | 2008-12-02 | 2010-06-03 | Paolo Panizza | Stazione per la realizzazione della stella nella produzione di gabbiette fermatappi in filo metallico. |
| ITRM20090301A1 (it) * | 2009-06-12 | 2010-12-13 | Meccaniche Turchi Giova Nni Costruzioni | Macchina per la realizzazione dell'elemento a stella nella produzione delle gabbiette di sicurezza per tappo per vini spumanti |
| WO2016083953A1 (fr) * | 2014-11-25 | 2016-06-02 | Mec Project Di Brossa Roberto | Ensemble de torsion pour un fil pour la fabrication de muselets pour des bouteilles de vin mousseux et machine de fabrication de celui-ci |
| WO2016181295A1 (fr) * | 2015-05-12 | 2016-11-17 | Mec Project Di Brossa Roberto | Ensemble permettant de fabriquer au moins un œillet sur une étoile pour la production d'une cage destinée à des bouchons de vin mousseux |
| CN112309700A (zh) * | 2020-10-26 | 2021-02-02 | 马鞍山豪远电子有限公司 | 一种用于变压器的线头折弯设备 |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| PT3205598T (pt) | 2016-02-09 | 2018-11-08 | Lligats Metala·Lics S L | Conjunto de tampa e gaiola para retenção de rolhas de garrafa |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2416672A (en) * | 1945-05-15 | 1947-03-04 | Accessories Inc | Wire hood forming machine |
| IT1072710B (it) * | 1977-03-23 | 1985-04-10 | Icas S A S Di Giovanni Poma & | Dispositivo per la produzione di gabbiette di sicurezza per tappi di bottiglie di vini spumanti o simili |
| DE4412203A1 (de) * | 1993-04-08 | 1994-10-13 | Gefin Srl | Verfahren und Vorrichtung zur Herstellung von Halbfertigteilen aus Draht |
-
2004
- 2004-09-08 ES ES04425670T patent/ES2279334T3/es not_active Expired - Lifetime
- 2004-09-08 DE DE602004004126T patent/DE602004004126T2/de not_active Expired - Lifetime
- 2004-09-08 EP EP04425670A patent/EP1634664B1/fr not_active Expired - Lifetime
- 2004-09-08 AT AT04425670T patent/ATE350179T1/de active
-
2005
- 2005-09-08 AU AU2005209611A patent/AU2005209611B2/en not_active Expired
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2416672A (en) * | 1945-05-15 | 1947-03-04 | Accessories Inc | Wire hood forming machine |
| IT1072710B (it) * | 1977-03-23 | 1985-04-10 | Icas S A S Di Giovanni Poma & | Dispositivo per la produzione di gabbiette di sicurezza per tappi di bottiglie di vini spumanti o simili |
| DE4412203A1 (de) * | 1993-04-08 | 1994-10-13 | Gefin Srl | Verfahren und Vorrichtung zur Herstellung von Halbfertigteilen aus Draht |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2025428A1 (fr) * | 2007-07-24 | 2009-02-18 | ME COM S.r.l. | Unité pour la production de cages de sécurité pour les bouchons de bouteilles de boissons effervescentes |
| ITMO20080312A1 (it) * | 2008-12-02 | 2010-06-03 | Paolo Panizza | Stazione per la realizzazione della stella nella produzione di gabbiette fermatappi in filo metallico. |
| ITRM20090301A1 (it) * | 2009-06-12 | 2010-12-13 | Meccaniche Turchi Giova Nni Costruzioni | Macchina per la realizzazione dell'elemento a stella nella produzione delle gabbiette di sicurezza per tappo per vini spumanti |
| WO2010143220A1 (fr) * | 2009-06-12 | 2010-12-16 | Costruzioni Meccaniche Turchi Giovanni | Machine pour la fabrication de la partie en forme d'étoile des muselets en fil métallique pour la fixation du bouchon en liège dans des bouteilles de champagne ou d'autre vin mousseux |
| WO2016083953A1 (fr) * | 2014-11-25 | 2016-06-02 | Mec Project Di Brossa Roberto | Ensemble de torsion pour un fil pour la fabrication de muselets pour des bouteilles de vin mousseux et machine de fabrication de celui-ci |
| EA032241B1 (ru) * | 2014-11-25 | 2019-04-30 | Мек Проект Ди Бросса Роберто | Скручивающее устройство для проволоки для изготовления мюзле, предназначенных для бутылок для игристых вин, и станок для изготовления мюзле |
| WO2016181295A1 (fr) * | 2015-05-12 | 2016-11-17 | Mec Project Di Brossa Roberto | Ensemble permettant de fabriquer au moins un œillet sur une étoile pour la production d'une cage destinée à des bouchons de vin mousseux |
| CN112309700A (zh) * | 2020-10-26 | 2021-02-02 | 马鞍山豪远电子有限公司 | 一种用于变压器的线头折弯设备 |
| CN112309700B (zh) * | 2020-10-26 | 2022-03-22 | 马鞍山豪远电子有限公司 | 一种用于变压器的线头折弯设备 |
Also Published As
| Publication number | Publication date |
|---|---|
| AU2005209611B2 (en) | 2011-03-03 |
| AU2005209611A1 (en) | 2006-03-23 |
| DE602004004126T2 (de) | 2007-11-15 |
| ATE350179T1 (de) | 2007-01-15 |
| ES2279334T3 (es) | 2007-08-16 |
| EP1634664B1 (fr) | 2007-01-03 |
| DE602004004126D1 (de) | 2007-02-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2123372B1 (fr) | Procédé pour plier des tuyaux, tiges, sections profilées et éléments similaires et dispositif correspondant | |
| JP6414957B2 (ja) | 缶の製造方法、ボトムリフォーム機構及びこれに用いるトップ支持部材 | |
| EP0475047B1 (fr) | Appareil et procédé pour transformer le bout chauffé d'un tube en verre et application dudit appareil dans une machine pour fabriquer des petites bouteilles | |
| EP1634664B1 (fr) | Dispositif de fabrication des muselets semi-finis, à partir d'un fil en métal, pour des bouteilles | |
| US5471858A (en) | Apparatus and process for the production of a hollow workpiece being profiled in a straight or helical manner relative to the workpiece axis | |
| JPS6316214B2 (fr) | ||
| US8245555B2 (en) | Headrest frame and method | |
| KR100291682B1 (ko) | 강판제 치차의 냉간성형방법 및 강판제 냉간성형치차 | |
| TWI568519B (zh) | 用於製造金屬罐的設備 | |
| CA2615220A1 (fr) | Procede pour realiser des dentures interieures et exterieures sur des pieces creuses cylindriques a paroi mince | |
| CN106424523B (zh) | 具有轴向侧凹的齿轮 | |
| EP2025428B1 (fr) | Unité pour la production de cages de sécurité pour les bouchons de bouteilles de boissons effervescentes | |
| US20220203422A1 (en) | Multi-axis roll-forming of stepped-diameter cylinder | |
| US20160089708A1 (en) | Method and device for producing rotationally symmetrical metal components | |
| US8539806B2 (en) | Roll forming method for producing longitudinally toothed profiled bodies in pot-shaped cylindrical workpieces | |
| EP2736660A2 (fr) | Cartouche porte-rouleau pour laminoir | |
| US9573180B2 (en) | Method and apparatus for fabricating a metal pipe having at least one smooth portion and at least one grooved portion | |
| US5946959A (en) | Process for producing annular workpieces from metal with a profiled cross section and a rolling facility for carrying out the method | |
| US11905065B2 (en) | Method and apparatus for producing a rolled curl on an open end of metal container | |
| US4331416A (en) | Article transfer device | |
| ITBO930135A1 (it) | Metodo e dispositivo per la realizzazione di semilavorati in filo metallico. | |
| RU2429931C1 (ru) | Полуавтомат для гибки проволочных изделий | |
| EP2239068B1 (fr) | Unité de formage du croisillon dans la fabrication de muselets de fil métallique pour bouchons de bouteilles | |
| JPH0318970B2 (fr) | ||
| SU997905A1 (ru) | Станок дл изготовлени змеевиков |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20050316 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL HR LT LV MK |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PL PT RO SE SI SK TR |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 Ref country code: LI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 Ref country code: CH Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 602004004126 Country of ref document: DE Date of ref document: 20070215 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602004004126 Country of ref document: DE Effective date: 20070215 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070403 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070403 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070604 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2279334 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 |
|
| 26N | No opposition filed |
Effective date: 20071005 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602004004126 Country of ref document: DE Effective date: 20071005 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070930 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070404 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070910 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20080908 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070908 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070704 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20070103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080908 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 15 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230517 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 602004004126 Country of ref document: DE Representative=s name: MUELLER-BORE & PARTNER PATENTANWAELTE PARTG MB, DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20230904 Year of fee payment: 20 Ref country code: AT Payment date: 20230919 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20230926 Year of fee payment: 20 Ref country code: DE Payment date: 20230928 Year of fee payment: 20 Ref country code: BE Payment date: 20230926 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20231017 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 602004004126 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20240927 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 350179 Country of ref document: AT Kind code of ref document: T Effective date: 20240908 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20240909 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20240909 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MK Effective date: 20240908 |