EP1634972A2 - Alliage réfractaire pour moulage par injection - Google Patents
Alliage réfractaire pour moulage par injection Download PDFInfo
- Publication number
- EP1634972A2 EP1634972A2 EP05012365A EP05012365A EP1634972A2 EP 1634972 A2 EP1634972 A2 EP 1634972A2 EP 05012365 A EP05012365 A EP 05012365A EP 05012365 A EP05012365 A EP 05012365A EP 1634972 A2 EP1634972 A2 EP 1634972A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- alloy
- concentration
- atomized
- refractory alloy
- refractory
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C19/00—Alloys based on nickel or cobalt
- C22C19/03—Alloys based on nickel or cobalt based on nickel
- C22C19/05—Alloys based on nickel or cobalt based on nickel with chromium
- C22C19/051—Alloys based on nickel or cobalt based on nickel with chromium and Mo or W
- C22C19/056—Alloys based on nickel or cobalt based on nickel with chromium and Mo or W with the maximum Cr content being at least 10% but less than 20%
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C19/00—Alloys based on nickel or cobalt
- C22C19/03—Alloys based on nickel or cobalt based on nickel
- C22C19/05—Alloys based on nickel or cobalt based on nickel with chromium
- C22C19/051—Alloys based on nickel or cobalt based on nickel with chromium and Mo or W
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2998/00—Supplementary information concerning processes or compositions relating to powder metallurgy
- B22F2998/10—Processes characterised by the sequence of their steps
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2999/00—Aspects linked to processes or compositions used in powder metallurgy
Definitions
- the present invention relates to a refractory alloy for metal injection molding, especially, to a refractory alloy for metal injection molding having similar composition to Inconel® 713C.
- refractory parts are manufactured by casting or forging, and metal injection molding (hereinafter, referred to as MIM) spreads in recent days for manufacturing the same.
- MIM metal injection molding
- the MIM is a method in which a mixture of a metal impalpable powder and a resin binder is injected into a mold to be molded.
- the metal impalpable powder causes high filling factor and the surface of the product to be smooth, and permits manufacturing a three-dimensional complex shape in a near net shape. Then such as a vane of a turbo charger is manufactured by MIM.
- the metal impalpable powder is generally manufactured by an atomization method, especially, by a water atomization method using water as a fluid.
- molten alloy streams from the outlet or teeming nozzle at the bottom of a tundish in a narrow stream, the stream of the molten alloy goes through an annular nozzle, the fluid is jetted from outlets in the circumference of the annular nozzle to the stream of the molten alloy, and energy of a jet of the fluid allows the molten alloy to be atomized and coagulated.
- the refractory alloys for MIM today such as SUS series (310, etc.), Hastelloy® series and Nimonic® series are all insufficient in strength.
- Inconel® 713C may be used as an atomized refractory alloy for MIM because it has higher strength than Nimonic® 90 as a material for casting.
- Inconel® 713C has the composition of 0.08-0.20 wt % C, 0.25 max wt % Mn, 0.015 max wt % S, 0.50 max wt % Si, 12.0-14.0 wt % Cr, 3.80-5.20 wt % Mo, 0.50-1.00 wt % Ti, 5.50-6.50 wt % Al, 2.5 max wt % Fe, 1.80-2.80 wt % Nb, 0.05-0.15 wt % Zr, 0.005-0.015 wt % B, 1.00 max wt % Co and the balance Ni.
- Inconel® 713C makes the nozzle blocked up in the atomizing step of the atomization method. That is, the outlet at the bottom of the tundish becomes blocked and the stream of molten alloy is stopped. This prevents from manufacturing impalpable powders for MIM.
- the concentration of Ti in more than 0.1 wt % and not more than 1 wt % causes the block of the molten alloy stream.
- the content of Ti is set to be other than the above-described range and the concentration of Nb is regulated such that the total of Ti atoms and Nb atoms be approximately equal to that in Inconel® 713C. Nb atoms are added for the purpose of development of solidifying.
- the object indicated above may be achieved according to a first aspect of the invention, which provides refractory alloy for metal injection molding characterized by comprising: 0.08-0.20 wt % C, 0-0.25 wt % Mn, 0-0.015 wt % S, 0.2-1.0 wt % Si, 12.0-14.0 wt % Cr, 3.80-5.20 wt % Mo, 0-0.1 wt % Ti, 5.50-6.50 wt % Al, 2.58-4.74 wt % Nb, 0-2.5 wt % Fe, 0-0.015 wt % B, 0-1.00 wt % Co and the balance being Ni and unavoidable impurities.
- the object indicated above may be achieved according to a second aspect of the invention, which provides refractory alloy for metal injection molding characterized by comprising: 0.08-0.20 wt % C, 0-0.25 wt % Mn, 0-0.015 wt % S, 0.2-1.0 wt % Si, 12.0-14.0 wt % Cr, 3.80-5.20 wt % Mo, 1.00-2.44 wt % Ti, 5.50-6.50 wt % Al, 0-2.5 wt % Fe, 0-0.015 wt % B, 0-1.00 wt % Co, (from ⁇ 1 to ⁇ 2 ) wt % Nb, and the balance being Ni and unavoidable impurities; where ⁇ 1 represents (1.43- ⁇ ) x 92.91/47.88, ⁇ 2 represents (2.44- ⁇ ) x 92.91/47.88 and ⁇ represents the concentration of Ti.
- the object indicated above may be achieved according to a third aspect of the invention, which provides the refractory alloy according to the first or second aspect of the invention, which is atomized by a water atomization method that allows molten metal atomized by jetting high pressure water.
- a fourth aspect of the invention provides a method of manufacturing a part made of refractory alloy comprising: (a) a mixing step of mixing an atomized material of the refractory alloy according to any one of the first to third aspects of the invention and a resin binder, (b) an injection molding step of filling a molding cavity of a predetermined mold with a mixture of the atomized material and the resin binder by injecting the mixture into the molding cavity, and molding a product which has a shape substantially corresponding to a shape of the molding cavity, (c) a binder removing step of removing the resin binder in the product by heat treatment, (d) a sintering step of sintering the product at a predetermined temperature.
- the object indicated above may be achieved according to a fifth aspect of the invention, which provides the method according to the fourth aspect of the invention, wherein the product is sintered at 1,250-1,280 °C to be a part made of refractory alloy having a density of not less than 7.8 g/cm 3 in the sintering step.
- the object indicated above may be achieved according to a sixth aspect of the invention, which provides the method according to the fourth or fifth aspect of the invention, wherein the part made of refractory alloy is a part that is to be exposed to exhaust fumes generated by an engine.
- a seventh aspect of the invention which provides the method according to the sixth aspect of the invention, wherein the part is a vane of a turbine of a turbo charger
- the concentration of 0-0.1 wt % Ti permits manufacturing impalpable powder for MIM by the atomization method without blocking the stream of molten alloy.
- the concentration of more than 1.00 wt % Ti permits manufacturing impalpable powder for MIM by the atomization method without blocking the stream of molten alloy.
- the molded product of the refractory alloy prior to sintering has an advantage in strength due to its irregular shape of the atomized alloy by the water atomization method in which molten alloy jetted with high pressure water becomes the impalpable powder.
- the method of manufacturing a part made of refractory alloy comprising: (a) a mixing step of mixing an atomized material of the refractory alloy according to any one of the first to third aspects of the invention and a resin binder, (b) an injection molding step of filling a molding cavity of a predetermined mold with a mixture of the atomized material and the resin binder by injecting the mixture into the molding cavity, and molding a product which has a shape substantially corresponding to a shape of the molding cavity, (c) a binder removing step of removing the resin binder in the product by heat treatment, (d) a sintering step of sintering the product at a predetermined temperature. Therefore, the refractory alloy part having the similar performance of refractoriness or heat resistance and in strength to Inconel® 713C is obtained.
- the molded product is sintered at 1,250-1,280 °C to be a part made of refractory alloy having a density of not less than 7.8 g/cm 3 in the sintering step according to the fourth aspect of the invention, the refractory alloy part having the high density and high strength is obtained.
- the refractory alloy part provided in the fourth or fifth aspect of the invention is a part that is to be exposed to exhaust fumes generated by such as an engine, the refractory alloy part having high heat resistance and high durability is obtained.
- the refractory alloy part provided in the sixth aspect of the invention is a vane of a turbine of a turbo charger, the turbo charger having high heat resistance and high durability is obtained.
- composition of the alloy of the present invention is based on Inconel® 713C and the rates of Si, Ti, Nb, B and Zr differ from those of Inconel® 713C as follows.
- Si is added for preventing oxidation of the molten alloy. Less than 0.2 wt % Si causes insufficient anti-oxidation effect and the previously-described block of the molten alloy stream. Excessive addition of Si causes cracks due to increase in hardness. Less than 0.1 wt % Si is preferable for preventing the lowering of heat-resistant temperature due to the lowering of the melting point.
- B (boron) is added in Inconel® 713C so that crystal grains may not grow larger in the casting step. And B (boron) may not necessarily be added in MIM because the alloy is in a form of an impalpable powder. However, the same content of B (boron) as that in Inconel® 713C may be added for the purpose of reinforcement of the grain boundary. Therefore, the concentration of B (boron) ranging from 0-0.015 wt % is preferable in this invention.
- Zr is not added in this invention because the nozzle is likely to be clogged with the zirconium oxide generated by cooling in the atomization method.
- the concentration of Nb is determined by the addition of Ti then. Since the concentration of Ti should be in the range of 1.43-2.44 wt % if the added Nb atoms are all replaced by Ti atoms, Nb atoms corresponding to from (1.43- ⁇ ) to (2.44- ⁇ ) wt % Ti, where ⁇ represents the concentration of Ti, should be added.
- the upper limit of the concentration of Ti is 2.44 wt % as described above if the concentration of Ti is not less than 1.0 wt %. It is the case that Nb atoms are all replaced by Ti atoms.
- the range of the concentration ofNb is given by the above Expressions 3 and 4 if the concentration of Ti is not less than 1.0 wt %. Then ⁇ is not less than one (1) and the concentration of Nb should be regarded as zero (0) if ⁇ is not less than 1.43 and then Expression 3 gives the value less than zero.
- the atomized material or the powder of the refractory alloy for metal injection molding according to the first or second aspect of the invention is used as an atomized metal.
- atomized metal such as polypropylen resin, polyethylene resin, acrylic resin, polystylene resin, kinds of waxes or the mixture of a plurality of these materials is used as a resin binder.
- the mixture may consist of each of the predetermined rate of the material.
- the rate of the atomized metal and the resin binder is appropriately determined considering the kinds of the atomized metal and the resin binder such that the mixture has proper flowability for molding upon heating and the binder removed product keeps its shape without being broken.
- the mixture of the atomized metal and the resin binder is heated at a predetermined temperature to have high flowability, is injected into the molding cavity or molding space in the mold, and is refrigerated in the mold to be solidified.
- the resin binder in the molded product is removed by heating below the sintering temperature and over the evaporation, decomposition or burn-off temperature of the resin binder in the vacuum, the predetermined depressurized atmosphere or the atmosphere.
- the heating temperature and the heating speed in the binder removing step are appropriately determined considering kinds of the atomized metal and the resin binder so as to prevent reaction of the resin binder component and the atomized metal or so as to prevent the damage of the molded product due to sudden evaporation or decomposition of the resin binder.
- the sintering temperature and sintering duration in the sintering step are appropriately determined so as to obtain the refractory alloy part of the sintered metal product having the desired density without perfect melting of the atomized refractory alloy for MIM according to the first or second aspect of the invention and with sufficient or appropriate shrinking of the molded product in the vacuum or the predetermined depressurized atmosphere.
- the refractory alloy part sintered at 1,250-1,280 °C obtained the density of not less than 7.8 g/cm 3 in the sintering step.
- the refractory alloy part as the sintered product in the sintering step is preferably used as a part that is exposed to the exhaust fumes in the internal combustion engine such as the gasoline engine and the diesel engine, the external combustion engine, the combustion device such as the burner.
- the refractory alloy part is preferably used as a part that requires the property of heat resistance such as the turbine vane of the turbo charger and the refractory nozzle.
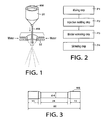
- Fig. 1 illustrates a main of a device used for the water atomization method to produce the atomized alloy.
- Fig. 2 illustrates steps for producing the refractory alloy part using the atomized alloy produced in an embodiment of the present invention.
- Fig. 3 illustrates a shape of a test piece for the tensile test.
- Fig. 1 illustrates a main of an atomization device.
- the molten alloy MM in a tundish 20 streams through a teeming nozzle or outlet at the bottom of the tundish 20 in a narrow stream.
- the diameter of the teeming nozzle is conditioned as below.
- An annular nozzle 22 is provided through which the narrow stream of the molten alloy M M passes. From outlets in the circumference of the annular nozzle 22 the pressurized water is jetted to the stream of the molten alloy MM.
- the pressure and the quantity of water is determined as below.
- the energy of the jetted water makes the molten alloy MM atomized and solidified.
- the Ti concentration is slightly higher than zero (0) and the Nb concentration is the minimum value given by Expression 3 with the above Ti concentration substituted. It was possible to produce the atomized alloy by the atomization method using the alloy having this composition.
- the Ti concentration is substantially the same as that in Embodiment 1 and the Nb concentration is the maximum value given by Expression 4 with this Ti concentration substituted. It was also possible to produce the atomized alloy by the atomization method using the alloy having this composition.
- the Nb concentration is an intermediate value between those in Embodiment 1 and Embodiment 2 and the balance is substantially the same as that in Embodiment 1 or Embodiment 2.
- Comparative Example 2 the Ti concentration is a little higher than that in Embodiment 1 and the Nb concentration is the minimum value given by Expression 3 with the above Ti concentration substituted as in Embodiment 1. Since this resulted in the block of the molten alloy stream at the teeming nozzle, it was not possible to produce the atomized alloy by the atomization method using the alloy having this composition in Comparative Example 2. In Comparative Example 3, the Ti concentration is a little higher than that in Embodiment 2 and the Nb concentration is the maximum value given by Expression 4 with the above Ti concentration substituted as in Embodiment 2.
- the Ti concentration is an intermediate value between the upper limit of the first aspect of the invention and the lower limit of the second aspect of the invention. Since this resulted in the block of the molten alloy stream at the teeming nozzle, it was not possible to produce the atomized alloy by the atomization method using the alloy having this composition.
- the Ti concentration is a little higher than one (1) and the Nb concentration is the minimum value given by Expression 3 with the above Ti concentration substituted. It was possible to produce the atomized alloy by the atomization method using the alloy having this composition. In Embodiment 4, the Ti concentration is substantially the same as that in Embodiment 3 and the Nb concentration is the maximum value given by Expression 4 with this Ti concentration substituted. It was also possible to produce the atomized alloy by the atomization method using the alloy having this composition. These show that it is possible to produce the atomized alloy by the atomization method using the alloy having all the range of the Nb concentration determined according to Expression 3 and 4 when the Ti concentration is higher than 1 wt %.
- Comparative Examples 5 and 6 have substantially the same composition as Embodiment 3 and 4, respectively, other than slightly different Ti concentration and the following slightly different Nb concentration. That is, in Comparative Example 5, the Ti concentration is a little lower than one (1) and the Nb concentration is the minimum value given by Expression 3 with the above Ti concentration substituted as in Embodiment 3. In Comparative Example 6, the Ti concentration is substantially the same as that in Comparative Example 5 and the Nb concentration is the maximum value given by Expression 4 with the above Ti concentration substituted as in Embodiment 4. Since these resulted in the block of the molten alloy stream at the teeming nozzle, it was not possible to produce the atomized alloy by the atomization method using the alloy having the composition in Comparative Examples 5 and 6.
- the composition of Comparative Example 1 is substantially the same as that in Embodiment 1 other than the addition of Si. Since this resulted in the block of the molten alloy stream at the teeming nozzle, it was not possible to produce the atomized alloy by the atomization method using the alloy having this composition.
- Embodiment 9 has the slight Ti concentration as Embodiment 1 and has the lower Si concentration than Embodiment 1. It was possible to produce the atomized alloy by the atomization method using the alloy having this composition in Embodiment 9. These show that the concentration of at least 0.2 wt % Si is required for the atomization method.
- the Ti and Nb concentrations are substantially the same as those in Embodiment 3, respectively, and the addition of Si is lower than 0.2 wt %. Since this resulted in the block of the molten alloy stream at the teeming nozzle, it was not possible to produce the atomized alloy by the atomization method using the alloy having this composition.
- the Ti concentration is substantially the same as that in Embodiment 3 or Comparative Example 7 and the addition of Si is between those in Embodiment 3 and Comparative Example 7. It was possible to produce the atomized alloy by the atomization method using the alloy having this composition in Embodiment 10. These show that the concentration of not lower than 0.2 wt % Si is required for the atomization method even when the Ti concentration is higher than 1.0 wt %.
- the B (boron) concentration is approximately equal to the upper limit defined in Inconel® 713C.
- the B (boron) concentration is approximately equal to the upper limit defined in Inconel® 713C. Since it was possible to produce the atomized alloy by the atomization method using the alloy having the composition in Embodiments 5, 6 and 7, these show that the B (boron) concentration within the range defined in Inconel® 713C exercises no influence to the block of the molten alloy stream at the teeming nozzle in the whole range of Ti and Nb concentration defined in the present invention.
- Table 2 lists the measured results of the properties of the sintered product manufactured by MIM using the atomized alloy prepared in the above Enbodiments with the properties of the sintered product of Nimonic® 90 (Comparative Example 8) that is known as a material for a high strength sintered product by MIM.
- the main of the manufacturing method of the sintered product is shown in the following explanation of Fig. 2.
- the part that is exposed to the exhaust fumes in the internal combustion engine such as the gasoline engine and the diesel engine, the external combustion engine, the combustion device such as the burner, especially, the turbine vane of the turbo charger and the refractory nozzle are manufactured using the atomized alloy prepared in the above Embodiments in a set of these steps in Fig. 2.
- the mixture for injection molding is prepared in the mixing step P1.
- the resin binder of 60 vol % including 55 wt % polypropylen, 30 wt % paraffin wax, 13.5 wt % carnauba wax and 1.5 wt % dioctyl phthalate and the atomized alloy prepared in the above Embodiments are mixed at 160 °C for 30 minutes in the mixing step P1.
- the injection molding step P2 the mixture of the atomized material and the resin binder that is heated at a predetermined temperature is injected into the molding cavity or molding space in the mold for molding using such as a 50-ton injection molding machine. Then the mixture is refrigerated in the mold to be solidified and then to be a molded product.
- the shape of the molded product substantially corresponds to the shape of the molding cavity.
- the molded product is drawn from the mold.
- the binder removing step P3 the resin binder in the molded product is removed by a solvent removal of removing the binder using a solvent in a hexane flow at 67 °C for 24 hours and then by a heat removal of removing the binder with heating in Ar (argon) flow under the atmospheric pressure at 440 °C for an hour.
- Ar argon
- the binder removed product is sintering at a predetermined temperature so that the sintering density is substantially constant such as 1,250-1,280 °C in the Ar atmosphere.
- a round bar of the sintered product was manufactured in the present test following these steps. The diameter of the round bar is 13 mm in diameter and 60 mm in length.
- a test piece of 13 mm in diameter and 10 mm in length was prepared from the above round bar, the test piece was disposed in an alumina crucible lidded, heat treatment was carried out in an atmospheric furnace at the temperature and duration shown in Table 2 and the increase in weight between the values before and after the heat treatment. The surface area of the test piece is calculated based upon the diameter and the height of the test piece.
- Table 2 shows that the sintered products in Embodiments 1-8 have similar or superior properties to that in Comparative Example 8, especially, in oxidation resistance and tensile strength at high temperature.
- the alloy having the composition based upon Inconel® 713C other than the Ti concentration of 0-0.1 wt % or 1.00-2.44 wt % and the regulated addition ofNb to be substantially the same total of Ti atoms and Nb atoms as Inconel® 713C is capable of being utilized for manufacturing the atomized alloy in the atomization method.
- the sintered product manufactured in M I M using the atomized alloy has similar or superior properties to that manufactured in MIM using conventional Nimonic® 90.
- Refractory alloy for metal injection molding including 0.08-0.20 wt % C, 0-0.25 wt % Mn, 0-0.015 wt % S, 0.2-1.0 wt % Si, 12.0-14.0 wt % Cr, 3.80-5.20 wt % Mo, 0-0.1 wt % Ti, 5.50-6.50 wt % Al, 2.58-4.74 wt % Nb, 0-2.5 wt % Fe, 0-0.015 wt % B, 0-1.00 wt % Co and the balance being Ni and unavoidable impurities.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Powder Metallurgy (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2004171078A JP2005350710A (ja) | 2004-06-09 | 2004-06-09 | 金属粉末射出成形用耐熱合金 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1634972A2 true EP1634972A2 (fr) | 2006-03-15 |
Family
ID=35520747
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05012365A Withdrawn EP1634972A2 (fr) | 2004-06-09 | 2005-06-08 | Alliage réfractaire pour moulage par injection |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP1634972A2 (fr) |
| JP (1) | JP2005350710A (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN107709586A (zh) * | 2015-08-12 | 2018-02-16 | 山阳特殊制钢株式会社 | 层叠造型用Ni基超合金粉末 |
| CN110512119A (zh) * | 2019-09-29 | 2019-11-29 | 湖南英捷高科技有限责任公司 | 一种注射成形镍基合金粉、注射成形方法及镍基合金制品 |
| US11511339B2 (en) | 2016-04-05 | 2022-11-29 | Mitsubishi Heavy Industries Aero Engines, Ltd. | Sintered body, method of manufacturing sintered body, combustor panel, and method of manufacturing combustor panel |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| RU2321652C1 (ru) * | 2006-05-31 | 2008-04-10 | Юлия Алексеевна Щепочкина | Сплав на основе никеля |
| CN106011541B (zh) * | 2016-07-26 | 2018-03-13 | 四川六合锻造股份有限公司 | 一种Ni‑Cr‑Mo系高温合金材料及其制备方法 |
| JP6774369B2 (ja) | 2017-04-25 | 2020-10-21 | 三菱重工航空エンジン株式会社 | 金属部材及びその製造方法 |
| JP2021021140A (ja) * | 2020-09-07 | 2021-02-18 | 三菱重工航空エンジン株式会社 | ニッケル基合金の射出成型品及びニッケル基合金の射出成型品の製造方法 |
-
2004
- 2004-06-09 JP JP2004171078A patent/JP2005350710A/ja active Pending
-
2005
- 2005-06-08 EP EP05012365A patent/EP1634972A2/fr not_active Withdrawn
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN107709586A (zh) * | 2015-08-12 | 2018-02-16 | 山阳特殊制钢株式会社 | 层叠造型用Ni基超合金粉末 |
| EP3336210A4 (fr) * | 2015-08-12 | 2019-03-13 | Sanyo Special Steel Co., Ltd. | Poudre de superalliage à base de ni destinée au moulage de pièces en stratifié |
| US11511339B2 (en) | 2016-04-05 | 2022-11-29 | Mitsubishi Heavy Industries Aero Engines, Ltd. | Sintered body, method of manufacturing sintered body, combustor panel, and method of manufacturing combustor panel |
| US11666967B2 (en) | 2016-04-05 | 2023-06-06 | Mitsubishi Heavy Industries Aero Engines, Ltd. | Sintered body, method of manufacturing sintered body, combustor panel, and method of manufacturing combustor panel |
| CN110512119A (zh) * | 2019-09-29 | 2019-11-29 | 湖南英捷高科技有限责任公司 | 一种注射成形镍基合金粉、注射成形方法及镍基合金制品 |
| CN110512119B (zh) * | 2019-09-29 | 2021-06-01 | 湖南英捷高科技有限责任公司 | 一种注射成形镍基合金粉、注射成形方法及镍基合金制品 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2005350710A (ja) | 2005-12-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1925682B1 (fr) | Procédé de production de pièces de soupape creuses pour moteurs à combustion ou turbines et pièce ainsi produite | |
| EP2450557B1 (fr) | Buse d'injection de carburant pour moteur à combustion interne, ébauche de buse et son procédé de fabrication | |
| US10632535B2 (en) | Cobalt based alloy additive manufactured article, cobalt based alloy product, and method for manufacturing same | |
| CA2738936C (fr) | Formulation chimique metallique en vrac de poudre d'alliage d'aluminium | |
| US20120073303A1 (en) | Metal injection molding process and components formed therewith | |
| EP0378702B1 (fr) | Alliage d'acier fritte presentant une excellente resistance a la corrosion et procede de production | |
| KR20090053934A (ko) | 금속 분말 | |
| JP2010144251A (ja) | ディーゼルエンジンの燃料バルブのためのノズルを製造する方法、及び、ノズル | |
| US20060018780A1 (en) | Method and composition for making a wire | |
| JP2009542905A (ja) | 金属射出成形による合金部品の製造方法及びその合金部品 | |
| CN114535602A (zh) | 一种基于激光近净成形技术的镍基高温合金/不锈钢梯度复合材料及其制备方法 | |
| US20070051199A1 (en) | Superalloy powder | |
| CN101516549A (zh) | 铁基粉末 | |
| JP3355190B2 (ja) | 燃料弁のノズルの製造方法及びノズル | |
| KR20250053101A (ko) | 적층 제조를 위한 금속 분말 | |
| DE10120172C1 (de) | Herstellung von Bauteilen durch Metallformspritzen (MIM) | |
| JP4779997B2 (ja) | 焼結体の製造方法 | |
| EP0354666B1 (fr) | Poudres d'alliages d'acier pour moulage par injection, leurs composés, et procédé de fabrication des pièces frittées | |
| CN110512119B (zh) | 一种注射成形镍基合金粉、注射成形方法及镍基合金制品 | |
| JP2005350710A (ja) | 金属粉末射出成形用耐熱合金 | |
| JP5470955B2 (ja) | 金属粉末および焼結体 | |
| US20250376743A1 (en) | Ni-base superalloy | |
| JP2002047502A (ja) | Cr含有Fe系合金粉末及びそれを用いたCr含有Fe系合金焼結体 | |
| US20250162029A1 (en) | Alloy powder, method for manufacturing a part based on this alloy, and part thus obtained | |
| JPS6312133B2 (fr) |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR LV MK YU |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20080103 |