EP1679169A1 - Methode pour produire articles decoratifs - Google Patents
Methode pour produire articles decoratifs Download PDFInfo
- Publication number
- EP1679169A1 EP1679169A1 EP05000130A EP05000130A EP1679169A1 EP 1679169 A1 EP1679169 A1 EP 1679169A1 EP 05000130 A EP05000130 A EP 05000130A EP 05000130 A EP05000130 A EP 05000130A EP 1679169 A1 EP1679169 A1 EP 1679169A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- molding material
- recesses
- pattern
- base
- decorating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 13
- 238000000034 method Methods 0.000 title claims abstract description 13
- 239000012778 molding material Substances 0.000 claims abstract description 29
- 229920001296 polysiloxane Polymers 0.000 claims abstract description 17
- 239000002184 metal Substances 0.000 claims abstract description 13
- 229910052751 metal Inorganic materials 0.000 claims abstract description 13
- 229920002379 silicone rubber Polymers 0.000 claims abstract description 4
- 239000004945 silicone rubber Substances 0.000 claims abstract description 4
- 239000000203 mixture Substances 0.000 claims description 10
- 239000003822 epoxy resin Substances 0.000 claims description 6
- LNEPOXFFQSENCJ-UHFFFAOYSA-N haloperidol Chemical compound C1CC(O)(C=2C=CC(Cl)=CC=2)CCN1CCCC(=O)C1=CC=C(F)C=C1 LNEPOXFFQSENCJ-UHFFFAOYSA-N 0.000 claims description 6
- 239000000049 pigment Substances 0.000 claims description 6
- 229920000647 polyepoxide Polymers 0.000 claims description 6
- 229920005749 polyurethane resin Polymers 0.000 claims description 6
- 239000000843 powder Substances 0.000 claims description 4
- 239000000654 additive Substances 0.000 claims description 2
- 230000000996 additive effect Effects 0.000 claims description 2
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 5
- 229910052802 copper Inorganic materials 0.000 description 5
- 239000010949 copper Substances 0.000 description 5
- 239000000463 material Substances 0.000 description 4
- 238000000465 moulding Methods 0.000 description 4
- 239000004033 plastic Substances 0.000 description 3
- 229920003023 plastic Polymers 0.000 description 3
- 230000002411 adverse Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C5/00—Processes for producing special ornamental bodies
- B44C5/04—Ornamental plaques, e.g. decorative panels, decorative veneers
- B44C5/0453—Ornamental plaques, e.g. decorative panels, decorative veneers produced by processes involving moulding
Definitions
- This invention relates to a method for manufacturing decorative articles, more particularly to a method for manufacturing decorative articles by using a silicone mold.
- decorative articles are essentially made from plastic materials that are harmful to the environment and that are not recyclable.
- Manufacture of the conventional decorative articles begins with preparing a plurality of copper molds, each of which def ines a desired pattern, and a molding mixture including the aforesaid plastic materials and a pigment powder or paste.
- the molding mixture is subsequently fed into each copper mold in small amounts.
- the copper molds are heated to cure the molding mixture therein, so as to form the decorative articles.
- the mass-production of the conventional decorative articles involves use of many copper molds, the production cost is relatively high.
- the molding mixture used for preparing the conventional decorative articles includes the aforesaid plastic materials, the decorative articles thus made tend to have an adverse impact upon the environment.
- the object of the present invention is to provide a method for manufacturing a decorative article that is clear of the aforesaid drawbacks of the prior art.
- a method for manufacturing a decorative article includes (a) preparing a metal mold defining a cavity and a pattern of separated recesses disposed within the cavity, (b) filling the cavity and the recesses in the metal mold with a silicone rubber so as to form a silicone mold that defines a pattern of protrusions corresponding respectively to the recesses, and a pattern of grooves among the protrusions, (c) filling the silicone mold with a first molding material selected from the group consisting of polyurethane resins, epoxy resins and mixtures thereof, and curing the first molding material so as to form a base that defines a pattern of decorating recesses which correspond respectively to the protrusions of the silicone mold, and (d) filling the decorating recesses in the base with a second molding material selected from the group consisting of polyurethane resins, epoxy resins and mixtures thereof, and curing the second molding material so as to form a pattern of decorative elements in the decorating recesses in the base.
- the preferred embodiment of a method for manufacturing a decorative article according to this invention involves preparation of a metal mold 6.
- the metal mold 6 defines a cavity and a pattern of separated recesses disposed within the cavity.
- the metal mold 6 is a copper mold.
- the cavity and the recesses of the metal mold 6 are filled with a silicone rubber so as to form a silicone mold 7.
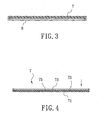
- the silicone mold 7 has a bottom plate 71, and defines a pattern of protrusions 73 that protrude from the bottom plate 71 and that correspond respectively to the recesses in the metal mold 6, and a pattern of grooves 75 among the protrusions 73 of the silicone mold 7.
- the silicone mold 7 is filled with a first molding material that is subsequently cured so as to form a base 8 that defines a pattern of decorating recesses 81 which correspond respectively to the protrusions 73 of the silicone mold 7.
- the first molding material is selected from the group consisting of polyurethane resins, epoxy resins and mixtures thereof.
- the curing operation of the first molding material is preferably conducted at a temperature ranging from 110 °C to 130°C for 10 minutes to 20 minutes.
- the decorating recesses 81 in the base 8 removed from the silicone mold 7 are subsequently filled with a second molding material.
- the second molding material is selected from the group consisting of polyurethane resins, epoxy resins and mixtures thereof.
- the second molding material in the decorating recesses 81 in the base 8 is cured so as to form a pattern of decorative elements 92 in the decorating recesses 81 in the base 8.
- the decorative elements 92 and the base 8 are bonded together to form a decorative article 9.
- the curing operation of the second molding material is preferably conducted at a temperature ranging from 90°C to 110°C for 25 minutes to 35 minutes.
- each of the first and second molding materials further includes an additive selected from the group consisting of a pigment powder and a pigment paste in such a manner that the first molding material has a color different from that of the second molding material.
- the decorative recesses 81 in the base 8 can be filled with a plurality of second molding materials including different pigment powders or pastes so as to form a color pattern of decorative elements 92.
- the base 8' is shown to have a configuration different from that of the base 8 of Fig. 6.
- the decorative article 9' that is prepared using the base 8' and that includes decorative elements 92' , is shown in Fig. 8.
- the decorative articles 9, 9' can be mass-produced by forming a plurality of the silicone molds 7 from a single metal mold 6 so that the production cost can be reduced.
- the first and second molding materials of this invention are recyclable and pollution-free materials, environmental concerns can be avoided.
Landscapes
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP05000130A EP1679169A1 (fr) | 2005-01-05 | 2005-01-05 | Methode pour produire articles decoratifs |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP05000130A EP1679169A1 (fr) | 2005-01-05 | 2005-01-05 | Methode pour produire articles decoratifs |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1679169A1 true EP1679169A1 (fr) | 2006-07-12 |
Family
ID=34933207
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05000130A Withdrawn EP1679169A1 (fr) | 2005-01-05 | 2005-01-05 | Methode pour produire articles decoratifs |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP1679169A1 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2010046698A1 (fr) * | 2008-10-20 | 2010-04-29 | Acell Group Limited | Produit composite à motifs |
| WO2019110970A1 (fr) * | 2017-12-05 | 2019-06-13 | Bentley Motors Limited | Éléments de véhicules automobiles comprenant de nouvelles incrustations en céramique et procédés de formation de ceux-ci |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2301356A1 (fr) * | 1975-02-18 | 1976-09-17 | Andrea Felix | Procede pour la fabrication de moules destines a la m |
| JPS59133011A (ja) * | 1983-01-20 | 1984-07-31 | Dainippon Printing Co Ltd | ポリエステル化粧板成型用エンボスシ−トの製造法 |
| EP0606570A1 (fr) * | 1992-12-12 | 1994-07-20 | Gorden Klüh | Procédé pour la fabrication d'imitations de pierres naturelles, notamment imitations de blocs de rochers de grand volume |
| EP0629480A2 (fr) * | 1993-06-17 | 1994-12-21 | Volkhard Kähler | Procédé et dispositif pour la fabrication de moules |
| EP0985507A1 (fr) * | 1998-09-04 | 2000-03-15 | Bruce E. Harrington | Procédé et disposatif pour la fabrication d'articles ayant un aspect naturel |
| US20040183225A1 (en) * | 2003-03-17 | 2004-09-23 | Paul Chang | Method of fabricating a pvc ornamental article having effects of imitated materials |
-
2005
- 2005-01-05 EP EP05000130A patent/EP1679169A1/fr not_active Withdrawn
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2301356A1 (fr) * | 1975-02-18 | 1976-09-17 | Andrea Felix | Procede pour la fabrication de moules destines a la m |
| JPS59133011A (ja) * | 1983-01-20 | 1984-07-31 | Dainippon Printing Co Ltd | ポリエステル化粧板成型用エンボスシ−トの製造法 |
| EP0606570A1 (fr) * | 1992-12-12 | 1994-07-20 | Gorden Klüh | Procédé pour la fabrication d'imitations de pierres naturelles, notamment imitations de blocs de rochers de grand volume |
| EP0629480A2 (fr) * | 1993-06-17 | 1994-12-21 | Volkhard Kähler | Procédé et dispositif pour la fabrication de moules |
| EP0985507A1 (fr) * | 1998-09-04 | 2000-03-15 | Bruce E. Harrington | Procédé et disposatif pour la fabrication d'articles ayant un aspect naturel |
| US20040183225A1 (en) * | 2003-03-17 | 2004-09-23 | Paul Chang | Method of fabricating a pvc ornamental article having effects of imitated materials |
Non-Patent Citations (1)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 008, no. 262 (M - 341) 30 November 1984 (1984-11-30) * |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2010046698A1 (fr) * | 2008-10-20 | 2010-04-29 | Acell Group Limited | Produit composite à motifs |
| US10479054B2 (en) | 2008-10-20 | 2019-11-19 | Acell Industries Limited | Patterned composite product |
| US11590715B2 (en) | 2008-10-20 | 2023-02-28 | Acell Industries Limited | Patterned composite product |
| WO2019110970A1 (fr) * | 2017-12-05 | 2019-06-13 | Bentley Motors Limited | Éléments de véhicules automobiles comprenant de nouvelles incrustations en céramique et procédés de formation de ceux-ci |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US8337654B2 (en) | Configurable tooling and molding method using the same | |
| US4528227A (en) | Mosaic style artwork | |
| US20060138695A1 (en) | Method for manufacturing decorative articles | |
| US20160236268A1 (en) | Green sand mold and its production method, and production method of iron-based casting | |
| CN101715278B (zh) | 壳体及其制造方法 | |
| KR101928490B1 (ko) | 3d 프린터용 세라믹 소재의 제조방법 및 이의 제조방법에 의해 제조된 3d 프린터용 세라믹 소재 | |
| JP4456130B2 (ja) | 加飾樹脂成形品の製造方法 | |
| CN104325264A (zh) | 一种模具直接成型的工艺方法 | |
| US20100229682A1 (en) | Cold cast mass element | |
| JP2003183705A5 (fr) | ||
| JP2006142710A (ja) | メラミン樹脂製食器及びその圧縮成形方法 | |
| CN212352719U (zh) | 一种包袱式复合产品及其多射注塑模具 | |
| KR102076303B1 (ko) | 조형석 블록 제조 방법 | |
| CN1135637C (zh) | 不定形发光二极管的制造方法及其成形模具 | |
| JP5290555B2 (ja) | 成形用金型の製法 | |
| KR20020088794A (ko) | 화강석 무늬를 갖는 강화 플라스틱 및 그 제조방법 | |
| KR102107647B1 (ko) | 리얼카본 제품 및 이의 제조방법 | |
| JP3622177B2 (ja) | 原型の原料およびその製造方法 | |
| KR101304269B1 (ko) | 에폭시수지 컬러판재의 제조방법 및 그에 의해 제조된 에폭시수지 컬러판재 | |
| CN215281575U (zh) | 一种砂轮毛坯制造模具 | |
| CN105003064B (zh) | 一种表面晶莹剔透的人造石装饰花纹线条的制造方法 | |
| CN203220751U (zh) | 新型娱乐麻将牌 | |
| EP0341479A3 (fr) | Procédé et dispositif de moulage pour la fabrication de pièces moulées à partir d'un mélange réactif liquide | |
| US6787087B1 (en) | Method of fabricating a PVC ornamental article having effects of imitated materials | |
| KR100758801B1 (ko) | 줄눈이 일체화된 인조석 및 이의 제조방법 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR LV MK YU |
|
| AKX | Designation fees paid | ||
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20070113 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |