EP1838472B1 - Verfahren zur formung des offenen endes eines rohrförmigen körpers - Google Patents
Verfahren zur formung des offenen endes eines rohrförmigen körpers Download PDFInfo
- Publication number
- EP1838472B1 EP1838472B1 EP06700148A EP06700148A EP1838472B1 EP 1838472 B1 EP1838472 B1 EP 1838472B1 EP 06700148 A EP06700148 A EP 06700148A EP 06700148 A EP06700148 A EP 06700148A EP 1838472 B1 EP1838472 B1 EP 1838472B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- diameter
- tubular body
- open end
- tube
- mouth
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D41/00—Application of procedures in order to alter the diameter of tube ends
- B21D41/02—Enlarging
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D51/00—Making hollow objects
- B21D51/16—Making hollow objects characterised by the use of the objects
- B21D51/26—Making hollow objects characterised by the use of the objects cans or tins; Closing same in a permanent manner
Definitions
- the present invention relates to a method of shaping metal tubular closures or can bodies such that the open end of the tube is formed into a flared shape.
- it relates to the shaping of a metal closure or can body in which the side wall height is greater than the diameter of the open end(s) and/or end wall.
- metal closures or can bodies from such easily worked materials as aluminium. These are typically formed from a flat sheet of relatively thin metal which may be shaped by means of one. Or a series of, die or spin-flanging tools such that the finished product is tubular with one axial end closed integrally and with the other end open.
- the finished product is then typically rolled onto a bottle neck so that threads are formed in the sides of the closure corresponding to the threads on the bottle neck.
- the tubular nature of these products is such that the diameter of the end of the tube is substantially the same as the closed end.
- a flange is formed at the axially distal open end of the can body by means of die or spin flanging tools.
- the flange acts as a feature for connecting the lid to the body for sealing proposes and is therefore typically oriented perpendicularly to the axial length of the can body.
- the flange is created by stretching and bending part of the can wall.
- a prior art closure having a flared sidewall is disclosed in DE-A-28 29 755 .
- the invention provides a method of shaping on open end of a metal tubular body into a flared shape so that the diameter of the tubular body increases gradually from a point axially spaced from the mouth at the open end of the tubular body towards the said mouth itself, the method being characterised by comprising the steps of:
- An advantage of this method is that splitting of the metal is avoided by the expansion of the overall desired axial length taking place in stages. Further, by increasing the open end to the desired diameter in one step, rather than in more than one step, there is less change of work-hardening of the metal which may cause splitting.
- the flare may be formed either straight or curved, which has advantages in matching the profiles of containers, in the case of closures. Further embodiments are disclosed in the dependent claims attached hereto.
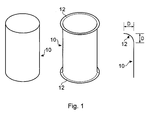
- a tube of metal 10 is shown in perspective on the left with substantially cylindrical sidewalls. This could be a food or drink can body.
- the middle drawing also in perspective, shows this came can body with flanges 12 formed at both ends.
- the drawing on the right is an enlarged view of one of flanges 12 seen in cross-section.
- the flange 12 is formed such that the distance of the end of the flange from the wall of the tube 'D' is substantially equal to the axial length of can wall which has been stretched. Further, this flange lies substantially perpendicular to the longitudinal axis of the can body 10.
- the greatest value for 'D', at which no splitting of the metal occurs, is known to be approximately 3mm with typical food or drink cons in which the call wall is comparatively thin (less than 1 mm).
- the can body could be formed from one sheet of metal so that the can body has on integral closed end and an open opposite end.
- Figure 2 shows a cross section of a typical metal closure 20.
- the closure has a closed end 22 and has a milling 24 formed at one end to increase grip.
- the walls 26 of the closure extend axially away from the closed end 22 and terminate at a mouth 25 at an open end. In some instances part of the walls 26 of the closure 20 have already been shaped such as bulge 28.
- the mouth 25 at the open end of the closure 20 is expanded outwards so as to form flange 30.
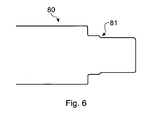
- the tool 80 is inserted inside the body of the closure 20 until the axial end of the walls 26 butt up against the curved stop 81 of the tool. Further respective movement of the tool 80 and closure 20 forces the open end of the tube outwards so that it conforms to the shape of the tool.
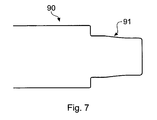
- the next step of the method is to use a subsequent forming tool, for instance the one shown in Figure 7 .
- This tool 90 is inserted into the closure body.
- the portion of the wall which is immediately adjacent but axially "behind" this flange 30, that is the portion between the mouth 25 and a point 27 spaced axially from the open end or mouth 25, is forced outwards such that the diameter of this wall is increased.
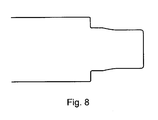
- This figure shows a portion of wall 26. Only one side of the cross-sectional view of the tube is shown as it is symmetrical about the longitudinal axis shown as "X". The wall thickness is exaggerated so that it is indicated by two parallel lines to improve understanding.
- the original shape of the wall is straight without any curve at the right hand end as indicated by reference 45.
- the portion indicated 50 extending between the mouth 25 at the open end and the axially spaced point 27 shows how the mouth 25 at the open end of the tube has been expanded by the first step, as described above, such that a flange has been formed.
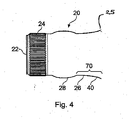
- the flange 30 which is initially distinct from the rest of the tubular sidewalls ( Figure 2 ), and become less distinct and in fact may become indistinguishable from the overall flare ( Figure 4 ).
- the flange 30 may merge and become one with the expanded wall portion 70, such that the diameter of the tube increases gradually from a point 27 spaced from the end of the tube towards the mouth 25 at the open end of the tube.
- the resultant flare shape of the closure or can body would typically be formed with the open end lying at an angle which is less than 45 degrees from the longitudinal axis.
- a tube with any wall thickness could be shaped by this method, is advantageously possible to shape tubes with walls of thickness less than 1 mm. This is due to careful design of the flanging and forming tools, the pressure of contact between the tube and the tools, and the sequence of tool shapes utilised. Accordingly, typically relatively thin walled metal tubes, such as found in metal closures or food or drink can bodies, may indeed be shaped this way.
- tubular walls of less than 1 mm thickness has been quoted, it has been found that the method will also perform well with walls with thickness of less than 0.50mm, and even less than 0.25mm.
- the diameter of the tube measured at the distal end, may be increase in a range from 1 to 20% of the original diameter, with the diameter of the portion of the tube immediately behind this distal end also being increased such that the overall diameter of the tube increases gradually from a point axially before the distal end of the tube to a point located at the distal end of the tube.
- This gradual increase in diameter may be formed over an axial length, measured back from the open end, which is grater than the increase in diameter of the tube. Indeed, the increase in diameter could be achieved over an axial length which is almost equal to the entire length of the tube.
- a tube could be shaped such that a series of flared profiles are formed axially along the length of the tube. Each profile could have a progressively smaller diameter than the preceding profile so that a set of tubes shaped in this way would be nestable.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
- Rigid Containers With Two Or More Constituent Elements (AREA)
- Containers Having Bodies Formed In One Piece (AREA)
- Resistance Heating (AREA)
- Processing Of Meat And Fish (AREA)
Claims (7)
- Verfahren zum Formen eines offenen Endes eines rohrförmigen Metallkörpers in eine aufgeweitete Form, sodass sich der Durchmesser des rohrförmigen Körpers allmählich von einem Punkt aus vergrößert, der sich axial von der Mündung am offenen Ende des rohrförmigen Körpers in Richtung der besagten Mündung selbst befindet,
dadurch gekennzeichnet, dass
das Verfahren aus folgenden Verfahrensschritten besteht:(a) aus dem Formen eines Flansches (12; 30; 60) mit einem Flanschwerkzeug (80), wodurch der Durchmesser der besagten Mündung am offenen Ende des rohrförmigen Körpers (10; 20; 26) auf einen gewünschten Durchmesser vergrößert wird; und(b) nach dem Formen des Flansches (12; 30; 60) aus der Vergrößerung des rohrförmigen Körpers im Bereich (50; 60; 70) zwischen dem besagten Punkt und der besagten Mündung mit einem oder mehreren Flanschwerkzeugen (90), sodass der Durchmesser der besagten Mündung des rohrförmigen Körpers (10; 20; 26) von dem in Schritt (a) des Verfahrens geformten Durchmessers unverändert bleibt. - Verfahren gemäß Anspruch 1,
dadurch gekennzeichnet,
dass ein axiales Ende des rohrförmigen Körpers geschlossen und das andere Ende offen ist. - Verfahren gemäß Anspruch 1 oder 2,
dadurch gekennzeichnet,
dass die besagte aufgeweitete Form gebogen ist. - Verfahren gemäß Anspruch 1,
dadurch gekennzeichnet,
dass die besagte aufgeweitete Form gerade ist. - Verfahren gemäß einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass der Durchmesser des rohrförmigen Körpers (10; 20; 26) um einen Bereich von 1 bis 20 % des ursprünglichen Durchmessers erweitert wird. - Verfahren gemäß einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass der Durchmesser des rohrförmigen Körpers (10; 20; 26) um eine axiale Länge (50; 60; 70) vergrößert wird, was größer ist als die Vergrößerung des Durchmessers des rohrförmigen Körpers (10, 20, 26) zwischen dem besagten Punkt und der Mündung am offenen Ende des besagten rohrförmigen Körpers (10, 20, 26). - Verfahren gemäß einem der vorhergehenden Ansprüche,
dadurch gekennzeichnet,
dass die aufgeweitete Form des rohrförmigen Körpers einen Winkel darstellt, der um weniger als 45 Grad von seiner Längsachse abweicht.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP06700148A EP1838472B1 (de) | 2005-01-17 | 2006-01-04 | Verfahren zur formung des offenen endes eines rohrförmigen körpers |
| PL06700148T PL1838472T3 (pl) | 2005-01-17 | 2006-01-04 | Sposób kształtowania otwartego końca metalowego korpusu rurowego |
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP05100255A EP1681110A1 (de) | 2005-01-17 | 2005-01-17 | Verfahren zum Formen von metallischen Verschlüssen oder Dosenkörpern |
| PCT/GB2006/000012 WO2006075132A1 (en) | 2005-01-17 | 2006-01-04 | Method of shaping metal closures or can bodies |
| EP06700148A EP1838472B1 (de) | 2005-01-17 | 2006-01-04 | Verfahren zur formung des offenen endes eines rohrförmigen körpers |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1838472A1 EP1838472A1 (de) | 2007-10-03 |
| EP1838472B1 true EP1838472B1 (de) | 2009-05-13 |
Family
ID=34938523
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05100255A Withdrawn EP1681110A1 (de) | 2005-01-17 | 2005-01-17 | Verfahren zum Formen von metallischen Verschlüssen oder Dosenkörpern |
| EP06700148A Expired - Lifetime EP1838472B1 (de) | 2005-01-17 | 2006-01-04 | Verfahren zur formung des offenen endes eines rohrförmigen körpers |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05100255A Withdrawn EP1681110A1 (de) | 2005-01-17 | 2005-01-17 | Verfahren zum Formen von metallischen Verschlüssen oder Dosenkörpern |
Country Status (8)
| Country | Link |
|---|---|
| EP (2) | EP1681110A1 (de) |
| AT (1) | ATE431205T1 (de) |
| DE (1) | DE602006006793D1 (de) |
| ES (1) | ES2327060T3 (de) |
| MY (1) | MY140608A (de) |
| PL (1) | PL1838472T3 (de) |
| TW (1) | TWI290863B (de) |
| WO (1) | WO2006075132A1 (de) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB0817942D0 (en) * | 2008-10-01 | 2008-11-05 | Obrist Closures Switzerland | A method of shaping metal closures |
| GB2547016B (en) | 2016-02-04 | 2019-04-24 | Crown Packaging Technology Inc | Metal containers and methods of manufacture |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS59120329A (ja) * | 1982-12-27 | 1984-07-11 | Mitsuboshi Seisakusho:Kk | 段付きパイプの成形法 |
| GB9726606D0 (en) * | 1997-12-18 | 1998-02-18 | Metal Box Plc | Can shaping |
| CN1313222C (zh) * | 2001-07-05 | 2007-05-02 | 马格纳构造系统公司 | 用于膨胀管坯的方法 |
-
2005
- 2005-01-17 EP EP05100255A patent/EP1681110A1/de not_active Withdrawn
-
2006
- 2006-01-04 PL PL06700148T patent/PL1838472T3/pl unknown
- 2006-01-04 DE DE602006006793T patent/DE602006006793D1/de not_active Expired - Lifetime
- 2006-01-04 ES ES06700148T patent/ES2327060T3/es not_active Expired - Lifetime
- 2006-01-04 WO PCT/GB2006/000012 patent/WO2006075132A1/en not_active Ceased
- 2006-01-04 AT AT06700148T patent/ATE431205T1/de not_active IP Right Cessation
- 2006-01-04 EP EP06700148A patent/EP1838472B1/de not_active Expired - Lifetime
- 2006-01-09 MY MYPI20060086A patent/MY140608A/en unknown
- 2006-01-10 TW TW095100910A patent/TWI290863B/zh not_active IP Right Cessation
Also Published As
| Publication number | Publication date |
|---|---|
| WO2006075132A1 (en) | 2006-07-20 |
| TWI290863B (en) | 2007-12-11 |
| HK1113103A1 (en) | 2008-09-26 |
| MY140608A (en) | 2009-12-31 |
| EP1681110A1 (de) | 2006-07-19 |
| ATE431205T1 (de) | 2009-05-15 |
| DE602006006793D1 (de) | 2009-06-25 |
| PL1838472T3 (pl) | 2009-10-30 |
| TW200631690A (en) | 2006-09-16 |
| ES2327060T3 (es) | 2009-10-23 |
| EP1838472A1 (de) | 2007-10-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5355710A (en) | Method and apparatus for necking a metal container and resultant container | |
| KR101689244B1 (ko) | 금속 용기의 직경을 확장하는 방법 | |
| EP0195157B1 (de) | Verfahren zur Formung von Rahmenteilen mit Kastenquerschnitt | |
| AU2007265132B2 (en) | Method of manufacturing containers | |
| CN102076575B (zh) | 双壁容器及制造方法 | |
| JP4713471B2 (ja) | 縦方向にスロットを有し、そして、異なる断面を有するいくつかの縦方向セグメントを備えている中空形材を、金属シートから製造する方法 | |
| JP2701878B2 (ja) | 多辺形状の断面を有し部分的に補強されたフレーム部材の製造方法 | |
| US20100107718A1 (en) | Necking die with redraw surface and method of die necking | |
| WO2012170618A1 (en) | Method of forming a metal container | |
| JP2021167024A (ja) | 缶体の製造方法 | |
| US20040048013A1 (en) | Method for shaping an initial profile or a similar workpiece using an internal high pressure and profile therefor | |
| JP7261228B2 (ja) | ロール縁部を形成する方法 | |
| EP1681110A1 (de) | Verfahren zum Formen von metallischen Verschlüssen oder Dosenkörpern | |
| US6112567A (en) | Method and apparatus for manufacturing a hollow body from a tubular blank by internal high-pressure shaping | |
| HK1113103B (en) | Method of shaping an open end of a metal tubular body | |
| EP3344406B1 (de) | Verfahren und vorrichtung für dosenexpansion | |
| JP2005334941A (ja) | パイプ状製品の成形方法およびパイプ状製品 | |
| US20050097935A1 (en) | Method for shaping a bent single- or multiple-chamber hollow profile internal high pressure | |
| KR101502825B1 (ko) | 머플러 제조용 금형장치 | |
| US20170333970A1 (en) | Method and apparatus for producing a rolled curl on an open end of metal container | |
| EP1308402B1 (de) | Dom für eine Aerosoldose und Aerosoldose mit einem solchen Dom | |
| NL1012557C2 (nl) | Werkwijze voor het vervaardigen van een n-hoekige conservenbus. | |
| EP2342030B1 (de) | Verbesserungen eines verfahrens zur herstellung von metallartikeln oder dieses betreffend | |
| KR101502971B1 (ko) | 머플러 제조방법 | |
| WO2000064609A1 (en) | Method of forming a can body |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20070531 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20080229 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| REG | Reference to a national code |
Ref country code: HK Ref legal event code: DE Ref document number: 1113103 Country of ref document: HK |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RTI1 | Title (correction) |
Free format text: METHOD OF SHAPING AN OPEN END OF A METAL TUBULAR BODY |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 602006006793 Country of ref document: DE Date of ref document: 20090625 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: HK Ref legal event code: GR Ref document number: 1113103 Country of ref document: HK |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2327060 Country of ref document: ES Kind code of ref document: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090913 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090813 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090913 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090813 |
|
| 26N | No opposition filed |
Effective date: 20100216 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100131 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100131 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090814 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100131 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100104 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20110801 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20110629 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20091114 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100104 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20120928 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090513 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120801 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602006006793 Country of ref document: DE Effective date: 20120801 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120131 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20200227 AND 20200304 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A Owner name: UNITED CLOSURES AND PLASTICS LIMITED Effective date: 20200326 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A Owner name: GCL INTERNATIONAL S.A.R.L. Effective date: 20200408 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: RO Payment date: 20201228 Year of fee payment: 16 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220104 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230711 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20240425 AND 20240501 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A Owner name: GUALA CLOSURES S.P.A. Effective date: 20241010 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20250225 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20250127 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250122 Year of fee payment: 20 Ref country code: GB Payment date: 20250128 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20260126 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20260103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20260105 |