EP1930141B1 - Dispositif d'acheminement pour un ou plusieurs composants d'un matériau de chargement pouvant s'écouler vers une machine de traitement - Google Patents
Dispositif d'acheminement pour un ou plusieurs composants d'un matériau de chargement pouvant s'écouler vers une machine de traitement Download PDFInfo
- Publication number
- EP1930141B1 EP1930141B1 EP07117413.0A EP07117413A EP1930141B1 EP 1930141 B1 EP1930141 B1 EP 1930141B1 EP 07117413 A EP07117413 A EP 07117413A EP 1930141 B1 EP1930141 B1 EP 1930141B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- components
- feeder device
- feeder
- component
- thermoplastic
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 239000000463 material Substances 0.000 claims description 15
- 244000025254 Cannabis sativa Species 0.000 claims description 13
- 235000012766 Cannabis sativa ssp. sativa var. sativa Nutrition 0.000 claims description 13
- 235000012765 Cannabis sativa ssp. sativa var. spontanea Nutrition 0.000 claims description 13
- 235000009120 camo Nutrition 0.000 claims description 13
- 235000005607 chanvre indien Nutrition 0.000 claims description 13
- 239000011487 hemp Substances 0.000 claims description 13
- 238000002156 mixing Methods 0.000 claims description 10
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 9
- 238000000034 method Methods 0.000 claims description 7
- 229920001169 thermoplastic Polymers 0.000 claims description 7
- 239000004416 thermosoftening plastic Substances 0.000 claims description 6
- 239000007788 liquid Substances 0.000 claims description 5
- 235000013311 vegetables Nutrition 0.000 claims description 4
- 229920000426 Microplastic Polymers 0.000 claims description 3
- 239000000835 fiber Substances 0.000 claims description 3
- 239000008187 granular material Substances 0.000 claims description 3
- 238000001746 injection moulding Methods 0.000 claims description 3
- 239000000203 mixture Substances 0.000 claims description 3
- 239000012815 thermoplastic material Substances 0.000 claims description 3
- 239000002245 particle Substances 0.000 claims description 2
- 239000004033 plastic Substances 0.000 claims description 2
- 229920003023 plastic Polymers 0.000 claims description 2
- 238000003860 storage Methods 0.000 claims description 2
- 235000013312 flour Nutrition 0.000 description 10
- 239000002657 fibrous material Substances 0.000 description 4
- 239000000126 substance Substances 0.000 description 4
- 241000196324 Embryophyta Species 0.000 description 3
- HEMHJVSKTPXQMS-UHFFFAOYSA-M Sodium hydroxide Chemical compound [OH-].[Na+] HEMHJVSKTPXQMS-UHFFFAOYSA-M 0.000 description 3
- 239000011230 binding agent Substances 0.000 description 3
- 238000011049 filling Methods 0.000 description 3
- 238000004519 manufacturing process Methods 0.000 description 3
- MHAJPDPJQMAIIY-UHFFFAOYSA-N Hydrogen peroxide Chemical compound OO MHAJPDPJQMAIIY-UHFFFAOYSA-N 0.000 description 2
- 229920002472 Starch Polymers 0.000 description 2
- 238000010276 construction Methods 0.000 description 2
- 238000009413 insulation Methods 0.000 description 2
- 235000019698 starch Nutrition 0.000 description 2
- 239000008107 starch Substances 0.000 description 2
- 238000003756 stirring Methods 0.000 description 2
- 229920001187 thermosetting polymer Polymers 0.000 description 2
- 241001474791 Proboscis Species 0.000 description 1
- 244000061456 Solanum tuberosum Species 0.000 description 1
- 235000002595 Solanum tuberosum Nutrition 0.000 description 1
- 239000000654 additive Substances 0.000 description 1
- 230000000996 additive effect Effects 0.000 description 1
- 229920001222 biopolymer Polymers 0.000 description 1
- 239000011093 chipboard Substances 0.000 description 1
- 239000004035 construction material Substances 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000000605 extraction Methods 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 238000000227 grinding Methods 0.000 description 1
- 239000012774 insulation material Substances 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
- 238000004886 process control Methods 0.000 description 1
- 238000007873 sieving Methods 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000000758 substrate Substances 0.000 description 1
- 239000005418 vegetable material Substances 0.000 description 1
- 238000005303 weighing Methods 0.000 description 1
- 239000002023 wood Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N1/00—Pretreatment of moulding material
- B27N1/02—Mixing the material with binding agent
Definitions
- the invention relates to a supply device for one or more components of a free-flowing and a difficult pourable feed material to a processing machine with different components.
- the invention is therefore based on the object to avoid the disadvantages mentioned and to provide a supply device for one or more components of a free-flowing feed, in which a high degree of homogeneity in terms of the substances to be processed is ensured.
- the essential advantage of the invention lies in the fact that the component, which consists of vegetable fiber materials, comes into contact with liquid in a mixing device, that is, the liquid is metered in and at the same time mixed with the material.
- the liquid is finely atomized and exposed to both components, i. both the vegetable fiber material component and the further component, detected and supplied gravimetrically.
- the second component consists of hemp in ground form.
- Hemp flour is ideal as an additive to products to reduce weight and use as sound insulation.
- Hemp flour is ground press cake, which is obtained during the extraction of oil from hemp seed.
- the first component is a plastic granules, in particular a thermoplastic plastic granules. Especially in combination with hemp flour a good mixing before processing is necessary.
- the first component is removed via a suction conveyor from a reservoir and passed through an intermediate container to a gravimetric device.
- the material to be processed has a water content of 0.3 to 8.0 percent by weight, depending on the recipe.
- the invention also relates to a process for producing a thermoplastic molded body, wherein particles of a vegetable material with at least one thermoplastic material are mixed.
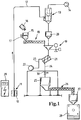
- the supply device has a reservoir 10 in which thermoplastic granules are located. At this reservoir, a removal device 11 is arranged. This removal device 11 is connected to a delivery line 12, the delivery line leads to a conveyor 13. The conveyor 13 is equipped with a suction pump 14.
- a further reservoir 15 is provided.
- the reservoir 15 is equipped with a mixer 17.
- a metering screw 18 is arranged below the reservoir.
- the hemp flour is fed to a hopper balance 19.
- Above the hopper scale is an intermediate container 20, which is connected between the conveyor 13 and the filling opening of the hopper scale 19.
- a mixing device 21 is provided below the hopper scale. This mixing device is connected to a water connection 22. The water is finely atomized fed to the mixing device 21 via line 23.
- the mixed material passes via the line 24 to a reservoir 25 and from there via a screw conveyor 26th to a machine hopper 27, which is arranged on a plastic injection molding machine or Kunststoffxtrudiermaschine 28.
- the entire device is operated via a control device 29 and defines the process.
- the process control is continuous or discontinuous.
- the removed from the reservoir 10 plastic granules is usually fed discontinuously to the conveyor 13, passes from there via the intermediate container to the hopper scale 19, which detects a certain amount, which is to be mixed with the hemp flour.
- the weighed material passes into the mixing device 21 and is mixed there by circulating agitators, at the same time finely atomized water is supplied until the appropriate moisture content is set.
- the thus prepared material passes through a discharge valve 30 to the reservoir 25th
- thermoplastic molded body formed by the injection molding machine may be used as a member having excellent acoustic properties, i. find application with a high insulating effect in a vehicle.
- the component can also be used as a technical element for the production of profiles for the construction industry.
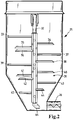
- FIG. 2 shows the in FIG. 1 described reservoir 25, which is provided with a stirrer construction 31.
- This improves the transportability of the supplied mixture and consists of a drive shaft 32 which is driven by a motor, not shown here.
- On the drive shaft 32 individual stirring rods 33, 34, 35, 36, 37, 38, 39, 40, 41, 42, 43, 44 and 45 are arranged in a different configuration.
- These stirrers can be attached to other positions as required and can thus be optimally adjusted to the consistency of the mixture supplied.
- a paddle 64 At the lower end of the drive shaft 32 is a paddle 64, which ensures good transport of the container contents in this area of the reservoir.
- FIG. 3 shows a variant for filling the reservoir 15 in FIG. 1 , It is a suction container 46, which is equipped with a suction nozzle 47.
- the proboscis is plugged into a side wall of the suction container 46 and operates with negative pressure, ie the material contained in the suction container 46 - in this case hemp flour - is fed to the storage container 15 with negative pressure via the suction grommet 47.
- a loosening device 48 consisting of a shaft 49 and bars 50, 51, 52, 53, 54, 55, 56 arranged thereon.
- the shaft is driven by an electric motor 57.
- the rods loosen the hemp flour in the container and ensure that no bridges or cavities form in the lower region, ie in the region of the suction pipe 47.
- the trunk is arranged laterally offset to the loosening device 48. At the same time inclined at an angle of about 10 ° to 20 ° so that the suction point 58 is close to the last stirring rod 56.
- the suction nozzle 47 is equipped with a tube 59 which is led to the reservoir.
- the lid 60 is removed. Equipped with rollers 61, 62 and a transport handle 63, the suction container is displaceable and can thus be adapted to different local conditions.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Wood Science & Technology (AREA)
- Forests & Forestry (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
- Filling Or Emptying Of Bunkers, Hoppers, And Tanks (AREA)
- Compositions Of Macromolecular Compounds (AREA)
Claims (8)
- Dispositif d'amenée, à une machine de traitement (28), pour un ou plusieurs composants d'un matériau de chargement apte à s'écouler,
dans lequel les composants suivants sont compris: un dispositif de transport (12) pour un premier composant du matériau de chargement, un dispositif de dosage (18) pour un deuxième composant en matières fibreuses végétales, un dispositif gravimétrique (19) destiné à déterminer la quantité amenée des premier et deuxième composants, un dispositif de mélange (21) pour les deux composants,
dans lequel du liquide, en particulier de l'eau, est ajouté(e) de manière dosée audit dispositif de mélange (21), et
dans lequel un récipient de transport (25) monté en aval qui est destiné à délivrer les composants mélangés à la machine de traitement est prévu. - Dispositif d'amenée selon la revendication 1, dans lequel le liquide est amené de manière finement pulvérisée aux deux composants.
- Dispositif d'amenée selon la revendication 1 ou 2, dans lequel le deuxième composant se compose de matière biodégradable, par exemple de chanvre, sous forme broyée.
- Dispositif d'amenée selon l'une quelconque des revendications précédentes, dans lequel le premier composant est un granulé de matière plastique, en particulier un granulé de matière plastique thermoplastique.
- Dispositif d'amenée selon l'une quelconque des revendications précédentes, dans lequel le premier composant est sorti d'un réservoir de stockage (10) par un refoulement par aspiration (13) et est amené via un récipient intermédiaire (20) au dispositif gravimétrique (19).
- Dispositif d'amenée selon l'une quelconque des revendications précédentes, dans lequel le mélange des composants présente une teneur en eau comprise entre 0,3 et 8,0 % en poids.
- Dispositif d'amenée selon l'une quelconque des revendications précédentes, dans lequel ladite machine de traitement (28) est une machine de moulage par injection ou une extrudeuse pour des matières plastiques thermoplastiques, et un formage thermoplastique se fait à la température usuelle pour les matières plastiques.
- Procédé de fabrication d'un corps moulé thermoplastique, dans lequel des particules d'une matière végétale sont mélangées à au moins une matière plastique thermoplastique en utilisant un dispositif d'amenée selon l'une quelconque des revendications précédentes.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE200610048134 DE102006048134A1 (de) | 2006-10-10 | 2006-10-10 | Zufuhrvorrichtung für eine oder mehrere Komponenten eines rieselfähigen Aufgabegutes zu einer Verarbeitungsmaschine |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1930141A2 EP1930141A2 (fr) | 2008-06-11 |
| EP1930141A3 EP1930141A3 (fr) | 2010-12-22 |
| EP1930141B1 true EP1930141B1 (fr) | 2017-02-22 |
Family
ID=38658435
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP07117413.0A Not-in-force EP1930141B1 (fr) | 2006-10-10 | 2007-09-27 | Dispositif d'acheminement pour un ou plusieurs composants d'un matériau de chargement pouvant s'écouler vers une machine de traitement |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP1930141B1 (fr) |
| DE (1) | DE102006048134A1 (fr) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2463188B (en) * | 2007-05-10 | 2011-11-16 | Bong Tech L L C | Electronic fluid dispensing apparatus and related method |
| CN102285093B (zh) * | 2011-06-03 | 2015-07-08 | 王根乐 | 匀料装置在自动控制挤出机均匀出料的装置上的新应用 |
| CN104057595A (zh) * | 2014-06-04 | 2014-09-24 | 浙江太湖远大新材料有限公司 | 双阶挤出机混合装置 |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3117682C2 (de) * | 1981-05-05 | 1987-04-09 | Triangel Spanplatten KG, 3177 Sassenburg | Verfahren und Vorrichtung zum kontinuierlichen Beleimen von Holzspänen und anderen lignozellulosehaltigen Partikeln |
| DE19603491C2 (de) * | 1996-01-31 | 1999-04-08 | Abu Shaar Isam | Verfahren zur Herstellung eines fasrigen Zellulosestoffes und dessen Verwendung |
| DE19746383A1 (de) * | 1997-10-21 | 1999-04-22 | Hofa Homann Gmbh & Co Kg | Verfahren und Vorrichtung zur Herstellung von Faserplatten sowie nach dem Verfahren hergestellte Faserplatten |
| DE29815667U1 (de) * | 1998-09-01 | 1999-10-28 | Anton Heggenstaller AG, 86556 Kühbach | Strangpresse zur Verarbeitung von mit Bindemitteln vermengten pflanzlichen Kleinteilen |
| DE19857287A1 (de) * | 1998-12-13 | 2000-06-15 | Dieffenbacher Gmbh Maschf | Verfahren und Anlage zur Herstellung von faserverstärkten Kunststoffmassen |
| DE10032804A1 (de) * | 1999-06-29 | 2001-02-15 | Hanf Faser Fabrik Uckermark Gm | Verfahren zur Herstellung von Pellets oder Granulaten aus Naturfasern sowie Verfahren zur Einmischung von Naturfasern in eine Kunststoffmatrix und daraus hergestellte faserverstärkte Kunststoffe |
| DE19949975B4 (de) * | 1999-10-08 | 2005-04-28 | Univ Dresden Tech | Verfahren zur Herstellung von biologisch abbaubaren, plattenförmigen Werkstoffen und Formteilen |
| AT410943B (de) * | 2001-10-23 | 2003-08-25 | Markus Dipl Ing Rettenbacher | Formkörper aus naturfasern und kunststoff, seine herstellung in gegenwart von feuchtigkeit und dessen verwendung |
| DE10301817B4 (de) * | 2003-01-20 | 2007-08-16 | MöllerTech GmbH | Verfahren zur Herstellung geschäumter Bauteile |
| DE10330756B4 (de) * | 2003-07-07 | 2005-11-17 | Jupiter Gmbh | Verfahren zur Herstellung eines Faserstoffes |
| DE102005014930A1 (de) * | 2005-04-01 | 2006-10-05 | Azo Holding Gmbh | Anlage zum gravimetrischen Zusammenführen von Schüttgut-Komponenten |
-
2006
- 2006-10-10 DE DE200610048134 patent/DE102006048134A1/de not_active Withdrawn
-
2007
- 2007-09-27 EP EP07117413.0A patent/EP1930141B1/fr not_active Not-in-force
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| DE102006048134A1 (de) | 2008-04-17 |
| EP1930141A3 (fr) | 2010-12-22 |
| EP1930141A2 (fr) | 2008-06-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| AT393272B (de) | Verfahren zur herstellung von extrudierten, direkt expandierten biopolymerprodukten und holzfaserplatten, verpackungs- und isoliermaterialien | |
| EP2236261B1 (fr) | Procédé et installation de fabrication cadencée et de préparation continue d'un mélange de matériau de remplissage en résine lors de la production de pièces de formage en matière synthétique | |
| EP2101983B1 (fr) | Mélange de matière plastique avec des particules de bois | |
| AT503371B1 (de) | Vorrichtung und verfahren zur verarbeitung von material durch mischung und bzw. oder plastifizierung oder agglomerierung | |
| DE102008061270B4 (de) | Vorrichtung und Verfahren zur Herstellung von Formteilen aus plastifizierbarem Material und aus faserförmigen Einlagen | |
| EP3730275B1 (fr) | Procédé de compoundage direct des compositions renforcées par des fibres pour la fabrication de pièces moulées en matière plastique et dispositif de compoundage direct | |
| WO2000040384A1 (fr) | Procede et dispositif pour produire en continu des corps moules | |
| EP1263562B1 (fr) | Procede de moulage par transfert de melanges de matieres plastiques | |
| EP2476526B1 (fr) | Méthode et appareil pour la fabrication d'un aggloméré de fibres ou de copeaux | |
| DE10121034B4 (de) | Vorrichtung zum kontinuierlichen Dosieren von Schnipsel und Fasermaterial | |
| EP1930141A2 (fr) | Dispositif d'acheminement pour un ou plusieurs composants d'un matériau de chargement pouvant s'écouler vers une machine de traitement | |
| EP1434674B1 (fr) | Dispositif et procede d'impregnation sous vide | |
| EP1541239A1 (fr) | Dispositif pour déchirer de matière solide, ajouter du fluide et transporter de la suspension à une installation | |
| WO2014198503A1 (fr) | Dispositif et procédé pour l'alimentation d'unités d'injection de thermodurcissable, ou d'unités d'extrusion de thermodurcissable | |
| EP2205422B1 (fr) | Dispositif d'amenée de fibres courtes | |
| DE2165148A1 (de) | Verfahren und Vorrichtung zum Mischen trockener und flüssiger Materialien und zur Herstellung verstärkter Kunststoffgegenstände | |
| WO2009135239A1 (fr) | Matériau à base de cuir | |
| DE2837135C2 (de) | Vorrichtung zum Beschicken eines Extruders mit Folienschnitzeln aus thermoplastischen Kunststoffen | |
| DE69909368T2 (de) | Anlage zur Herstellung von Materialien für Spritzguss- und Formpressverfahren | |
| WO2011029904A1 (fr) | Système pour amener des fibres de bois dans un état permettant le traitement par des dispositifs de dosage, matière à base de fibres de bois préparée et produit extrudé produit à partir de cette matière | |
| DE202007008256U1 (de) | Mischgranulator | |
| DE3714624A1 (de) | Schneckenpresse sowie verfahren zur herstellung von handhabbaren presslingen aus abfallpapier | |
| EP0289015A1 (fr) | Presse à vis et un procédé pour transformer les vieux papiers en blocs maniables | |
| EP3924157B1 (fr) | Procédé pour l'encollage de copeaux de bois | |
| DE10316232B4 (de) | Verfahren und Vorrichtung zum Beschicken eines Extruders |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20080331 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK RS |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK RS |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: PROTEC POLYMER PROCESSING GMBH |
|
| 17Q | First examination report despatched |
Effective date: 20130327 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20160531 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 868907 Country of ref document: AT Kind code of ref document: T Effective date: 20170315 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502007015453 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20170222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170523 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170522 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170622 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502007015453 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20171123 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20170930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170930 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170930 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170930 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 12 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20181231 Year of fee payment: 8 Ref country code: FR Payment date: 20180925 Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 868907 Country of ref document: AT Kind code of ref document: T Effective date: 20170927 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20180919 Year of fee payment: 12 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20070927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190927 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20200221 Year of fee payment: 13 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170622 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20190927 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190927 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190930 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502007015453 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210401 |