EP1992424A1 - Verfahren und Vorrichtung zur Reinigung der umlaufenden Außenfläche geschweißter Metallrohre - Google Patents
Verfahren und Vorrichtung zur Reinigung der umlaufenden Außenfläche geschweißter Metallrohre Download PDFInfo
- Publication number
- EP1992424A1 EP1992424A1 EP08008241A EP08008241A EP1992424A1 EP 1992424 A1 EP1992424 A1 EP 1992424A1 EP 08008241 A EP08008241 A EP 08008241A EP 08008241 A EP08008241 A EP 08008241A EP 1992424 A1 EP1992424 A1 EP 1992424A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- pipe
- cleaning
- laser beam
- welding bead
- sublimating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B08—CLEANING
- B08B—CLEANING IN GENERAL; PREVENTION OF FOULING IN GENERAL
- B08B9/00—Cleaning hollow articles by methods or apparatus specially adapted thereto
- B08B9/02—Cleaning pipes or tubes or systems of pipes or tubes
- B08B9/023—Cleaning the external surfaces
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B08—CLEANING
- B08B—CLEANING IN GENERAL; PREVENTION OF FOULING IN GENERAL
- B08B7/00—Cleaning by methods not provided for in a single other subclass or a single group in this subclass
- B08B7/0035—Cleaning by methods not provided for in a single other subclass or a single group in this subclass by radiant energy, e.g. UV, laser, light beam or the like
- B08B7/0042—Cleaning by methods not provided for in a single other subclass or a single group in this subclass by radiant energy, e.g. UV, laser, light beam or the like by laser
Definitions
- the present invention relates to a method for cleaning the outer surface of welded metal pipes, thereby allowing the position of the welding bead of said tubes to be optically detected.
- the invention further relates to a device for carrying out this method.
- a detection of the position of the welding bead on the outer surfaces of welded metal pipes would improve any pipe making methods, since said position detection would allow the welding bead of a welded pipe to be properly processed, thereby enhancing the aesthetic and functional properties of said welded pipe.
- a further practical example is a welding of folding workpieces, since in such an application the welding bead negatively affect a proper operation and strength of the bent workpiece.
- Prior detection methods automatically detect the position of a welding bead on the outer surface of a welded pipe by optical detecting systems including an optical sensor which detects said welding bead position from brightness variations on the pipe surface, which generate contrast regions including a light band, corresponding to the welding bead, on a dark pipe, or vice versa.
- a prior optical system would either detect a low signal/noise ratio contrast or several signal brightness peaks, which cannot be so distinguished from one another as to allow to precisely detect the position of said welding bead.
- the aim of the present invention is to provide a method for cleaning pipes, in particular the outer surface of a metal tube, for removing therefrom elements hindering an optical read-out of the position of a welding bead.
- a further object of the present invention is to provide a device for carrying out the above cleaning method.
- a method for cleaning the circumferential outer surface of a welded metal pipe said method being characterized in that said surface is cleaned by melting, evaporating and/or sublimating extraneous materials or flaws on said surface.
- the device for carrying out the above method said device being characterized in that it comprises a laser beam source.
- the outer surface of a welded tube is so processed and cleaned to provide a clear optical contrast between the material of the pipe and its welding bead, thereby allowing a position detecting system to precisely detect and locate the position of the pipe welding bead, to in turn allow an operator to accurately set a proper position for performing further processing operations on said welding bead.
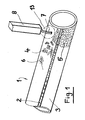
- the reference number 1 generally shows a pipe to be cleaned by a cleaning method according to the invention.
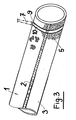
- Said pipe is a metal pipe, and has been welded at a welding bead 2 on the pipe surface 3 which welding bead 2 is partially smeared or covered by oil, fat or rust stains 4, paint layers 5, scratches or notches 6.
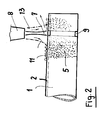
- the method according to the invention provides to cause a laser beam to impinge on said surface 3, said laser beam 7 being properly focalized on the surface 3 level.
- the laser beam 7 emitting head 8 is so arranged to cause said impinging laser beam to be only absorbed by the surface layers of said pipe 1, thereby allowing the laser impinging portion 9 of the surface 3 of the pipe 1 to be properly cleaned by melting, evaporating and/or sublimating the dirt, fat, oil and paint stains 4, 5, and scratches 6, the cleaning being achieved by melting, evaporating and/or sublimating the first surface layer 10 of said pipe 1 ( figure 3 ).
- an aiding gas jet 13 ( figure 2 ) is further caused to impinge on said portion 9, thereby forming on the surface 3 of the pipe 1 and easily detectable and identifiable optical contrast between said surface material and said welding bead 2 of said pipe 1.
- the laser beam 7 emitting head 8 used in the inventive method and device may comprise, for example, a laser beam emitting system of a commercially available type, such as of a type made by the same Applicant.
Landscapes
- Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Cleaning In General (AREA)
- Laser Beam Processing (AREA)
- Coating By Spraying Or Casting (AREA)
- Coating With Molten Metal (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT000985A ITMI20070985A1 (it) | 2007-05-16 | 2007-05-16 | Procedimento e dispositivo per la pulizia della superficie circonferenziale esterna di tubi metallici saldati |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP1992424A1 true EP1992424A1 (de) | 2008-11-19 |
Family
ID=39730578
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08008241A Withdrawn EP1992424A1 (de) | 2007-05-16 | 2008-04-30 | Verfahren und Vorrichtung zur Reinigung der umlaufenden Außenfläche geschweißter Metallrohre |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1992424A1 (de) |
| JP (1) | JP2008284548A (de) |
| BR (1) | BRPI0801317A2 (de) |
| IT (1) | ITMI20070985A1 (de) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2015192220A1 (en) * | 2014-06-19 | 2015-12-23 | Magna International Inc. | Method and apparatus for laser assisted power washing |
| CN110695008A (zh) * | 2019-10-28 | 2020-01-17 | 苏州艾思兰光电有限公司 | 一种移动式激光清洗及除锈设备 |
| CN110919192A (zh) * | 2019-12-26 | 2020-03-27 | 苏州吉格斯机械科技有限公司 | 刹车管双头激光去皮设备 |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111843217A (zh) * | 2020-09-11 | 2020-10-30 | 沈阳工业大学 | 可自适应加工表面的激光清洗与焊接装置及使用方法 |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4867796A (en) * | 1982-04-05 | 1989-09-19 | Maxwell Laboratories, Inc. | Photodecontamination of surfaces |
| EP0475806A2 (de) * | 1990-09-12 | 1992-03-18 | Framatome | Laser-Arbeitsgerät, insbesondere für die Reinigung einer Leitung eines Nuclearreaktors |
| FR2689423A1 (fr) * | 1992-04-01 | 1993-10-08 | Valinox | Dispositif et procédé permettant le nettoyage par faisceau laser de la paroi intérieure de tubes. |
| JPH1177308A (ja) * | 1997-09-12 | 1999-03-23 | Hitachi Ltd | 溶接線検出方法およびその装置並びに溶接装置 |
| JPH11216647A (ja) * | 1998-02-03 | 1999-08-10 | Mitsubishi Heavy Ind Ltd | 研削装置 |
| US6028316A (en) * | 1996-08-28 | 2000-02-22 | New Star Lasers, Inc. | Method and apparatus for removal of material utilizing near-blackbody radiator means |
| JP2000246332A (ja) * | 1999-02-24 | 2000-09-12 | Nisshin Steel Co Ltd | 拡管用溶接鋼管及びその製造方法 |
| US20050150522A1 (en) * | 2004-01-14 | 2005-07-14 | Usui Kokusai Sangyo Kaisha Limited | Method for removing resin layer from resin-coated metal tube |
-
2007
- 2007-05-16 IT IT000985A patent/ITMI20070985A1/it unknown
-
2008
- 2008-04-30 EP EP08008241A patent/EP1992424A1/de not_active Withdrawn
- 2008-05-12 JP JP2008124663A patent/JP2008284548A/ja not_active Withdrawn
- 2008-05-14 BR BRPI0801317-9A patent/BRPI0801317A2/pt not_active IP Right Cessation
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4867796A (en) * | 1982-04-05 | 1989-09-19 | Maxwell Laboratories, Inc. | Photodecontamination of surfaces |
| EP0475806A2 (de) * | 1990-09-12 | 1992-03-18 | Framatome | Laser-Arbeitsgerät, insbesondere für die Reinigung einer Leitung eines Nuclearreaktors |
| FR2689423A1 (fr) * | 1992-04-01 | 1993-10-08 | Valinox | Dispositif et procédé permettant le nettoyage par faisceau laser de la paroi intérieure de tubes. |
| US6028316A (en) * | 1996-08-28 | 2000-02-22 | New Star Lasers, Inc. | Method and apparatus for removal of material utilizing near-blackbody radiator means |
| JPH1177308A (ja) * | 1997-09-12 | 1999-03-23 | Hitachi Ltd | 溶接線検出方法およびその装置並びに溶接装置 |
| JPH11216647A (ja) * | 1998-02-03 | 1999-08-10 | Mitsubishi Heavy Ind Ltd | 研削装置 |
| JP2000246332A (ja) * | 1999-02-24 | 2000-09-12 | Nisshin Steel Co Ltd | 拡管用溶接鋼管及びその製造方法 |
| US20050150522A1 (en) * | 2004-01-14 | 2005-07-14 | Usui Kokusai Sangyo Kaisha Limited | Method for removing resin layer from resin-coated metal tube |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2015192220A1 (en) * | 2014-06-19 | 2015-12-23 | Magna International Inc. | Method and apparatus for laser assisted power washing |
| CN106413925A (zh) * | 2014-06-19 | 2017-02-15 | 麦格纳国际公司 | 用于激光辅助动力清洗的方法和设备 |
| US20170361403A1 (en) * | 2014-06-19 | 2017-12-21 | Magna International Inc. | Method and Apparatus for Laser Assisted Power Washing |
| US10906130B2 (en) * | 2014-06-19 | 2021-02-02 | Magna International Inc. | Method and apparatus for laser assisted power washing |
| CN110695008A (zh) * | 2019-10-28 | 2020-01-17 | 苏州艾思兰光电有限公司 | 一种移动式激光清洗及除锈设备 |
| CN110695008B (zh) * | 2019-10-28 | 2021-12-24 | 苏州艾思兰光电有限公司 | 一种移动式激光清洗及除锈设备 |
| CN110919192A (zh) * | 2019-12-26 | 2020-03-27 | 苏州吉格斯机械科技有限公司 | 刹车管双头激光去皮设备 |
Also Published As
| Publication number | Publication date |
|---|---|
| BRPI0801317A2 (pt) | 2009-04-28 |
| JP2008284548A (ja) | 2008-11-27 |
| ITMI20070985A1 (it) | 2008-11-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US20090272722A1 (en) | Method and device for cleaning the circumferential outer surface of welded metal pipes | |
| KR101361013B1 (ko) | 재료 이음부의 자동 검사 방법 | |
| EP0214046B1 (de) | Verfahren und System zum Lokalisieren und Prüfen einer Laschennat in einem längsgeschweissten Metallrohr | |
| Miyamoto et al. | Development of in-process monitoring system for laser welding | |
| WO2015037457A1 (ja) | レーザ溶接良否判定装置及びレーザ溶接良否判定方法 | |
| ATE368209T1 (de) | Vorrichtung zum erfassen, bestimmen und dokumentieren von schäden, insbesondere durch plötzliche ereignisse verursachte deformationen an lackierten oberflächen | |
| JP2008215879A (ja) | 清浄度判定装置および方法 | |
| JP2008284548A (ja) | 溶接金属管外周面のクリーニング方法とクリーニング装置 | |
| KR101984647B1 (ko) | 작업 품질 검사 기능을 구비한 레이저 클리닝 장치 및 그 방법 | |
| Yusof et al. | Detection of defects on weld bead through the wavelet analysis of the acquired arc sound signal | |
| JP7703673B2 (ja) | マシニングプロセス中の欠陥を識別する方法及びマシニング装置 | |
| KR20190011893A (ko) | 작업 품질 검사 기능을 구비한 레이저 클리닝 장치 및 그 방법 | |
| ATE294371T1 (de) | Verfahren und vorrichtung zum erfassen eines biegewinkels an einem werkstück | |
| JP4780334B2 (ja) | 溶接割れ検出方法 | |
| WO2008037580A3 (de) | Verfahren und vorrichtung zur echtzeitkontrolle von fügeverbindungen mit röntgenstrahlung und grauwertauswertung | |
| JP2008196866A (ja) | 溶接割れ検出方法および装置 | |
| JP4624089B2 (ja) | レーザ溶接部の品質判定装置および方法、並びに、レーザ溶接部の品質判定プログラムを記録した媒体 | |
| JP6142858B2 (ja) | 鍛接鋼管の形状計測方法および装置 | |
| JP2955618B2 (ja) | Uo鋼管の溶接部表面疵検査方法 | |
| JP2008191017A (ja) | 板状体の欠陥検出方法 | |
| JPH09122962A (ja) | レーザ加工ヘッド | |
| JP2003071939A (ja) | 樹脂部材の溶着方法およびその方法を用いて製造された溶着樹脂部材 | |
| JPH10132509A (ja) | 電縫鋼管のシーム部検出方法 | |
| Auger et al. | On-line monitoring of CO2 laser welding using neural networks | |
| Fréchette et al. | Application of process monitoring and quality control of laser-welded blanks using an integrated multiple-sensors approach |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA MK RS |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN WITHDRAWN |
|
| 18W | Application withdrawn |
Effective date: 20090323 |