EP2147131B1 - Procédé de passivation thermochimique d'acier inoxydable - Google Patents
Procédé de passivation thermochimique d'acier inoxydable Download PDFInfo
- Publication number
- EP2147131B1 EP2147131B1 EP08715970A EP08715970A EP2147131B1 EP 2147131 B1 EP2147131 B1 EP 2147131B1 EP 08715970 A EP08715970 A EP 08715970A EP 08715970 A EP08715970 A EP 08715970A EP 2147131 B1 EP2147131 B1 EP 2147131B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- stainless steel
- process according
- heat treatment
- weight
- salts
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C22/00—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C22/73—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals characterised by the process
- C23C22/74—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals characterised by the process for obtaining burned-in conversion coatings
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C22/00—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C22/05—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals using aqueous solutions
- C23C22/06—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals using aqueous solutions using aqueous acidic solutions with pH less than 6
- C23C22/48—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals using aqueous solutions using aqueous acidic solutions with pH less than 6 not containing phosphates, hexavalent chromium compounds, fluorides or complex fluorides, molybdates, tungstates, vanadates or oxalates
- C23C22/50—Treatment of iron or alloys based thereon
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C22/00—Chemical surface treatment of metallic material by reaction of the surface with a reactive liquid, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C22/82—After-treatment
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C8/00—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C8/02—Pretreatment of the material to be coated
Definitions
- the present invention relates to a novel method of passivating stainless steel surfaces which provides improved corrosion resistance of the treated surfaces as well as increasing the resistance of these surfaces to thermal discoloration.
- the process consists of a chemical treatment with an aqueous solution comprising complexing agents, a rinsing and a subsequent thermal treatment in a gaseous, oxygen-containing atmosphere.
- Stainless steel which is often referred to as stainless steel, is an iron alloy which, in addition to iron, may contain a number of other elements such as chromium, nickel, molybdenum, copper and others.
- the chromium present in the alloy reacts with oxygen from the environment at the surface and forms an oxide layer on the surface of the material.
- the resulting chromium oxide can reliably form a dense layer on the surface and thus protects the workpiece from corrosion.
- This protective layer is also called a passive layer.
- Such a passive layer is usually about 10 molecule layers thick and contains in addition to the chromium oxide especially iron oxide in a concentration of 10-55 wt .-%.
- the corrosion resistance of the workpiece depends on the content of chromium and other alloying elements such as nickel and molybdenum. These additional alloying elements are added to the stainless steel alloy to form the Corrosion resistance to further improve, if the addition of chromium alone is not able to give the workpiece the desired degree of corrosion resistance or other characteristics.
- these other corrosion resistance improving elements are expensive and thus increase the cost of producing the stainless steel to a considerable extent.
- Another known measure to increase corrosion resistance is to increase the ratio of chromium to iron in the passive layer.
- treatment of the surface with substances that have a high affinity for iron ions and thus are able to selectively dissolve out and bind iron ions from the passive layer is suitable for this purpose.
- aqueous solutions of complexing agents and / or chelating agents such as citric acid are frequently used, for example, the chromium / iron ratio on bright-rolled or ground stainless steel surfaces of a value of 0.8 to 1.2 before the treatment to a value of 3.0 can increase to 5.0 after treatment.
- This increased content of chromium oxide causes a correspondingly improved corrosion resistance of the workpiece.
- thermally grown oxide layers significantly reduce the corrosion resistance of the stainless steel by either preventing the formation of true passive layers or displacing existing passive layers at higher temperatures.
- thermally generated oxide layers such as the tarnish or scale described above
- thermally generated oxide layers such as the tarnish or scale described above
- no method is known in the prior art, which improves the resistance of stainless steel surfaces against thermal discoloration, ie against the formation of such thermally generated oxide layers.
- the aim of the present invention is a method for passivation of stainless steel surfaces, which in comparison to known passivation method according to the prior art, a significant increase in the corrosion potential, measured as pitting potential according to DIN 50900 causes.
- the increase in corrosion potential that can be achieved with the methods described herein ranges from +500 mV to +850 mV from the initial state. This makes it possible in many cases, instead of expensive molybdenum or copper-containing materials cheaper To use stainless steel grades that have the required corrosion resistance due to their passivation according to a method of the present invention.
- the corrosion resistance of the stainless steel surface can be markedly improved both for workpieces made of stainless steel with ferritic and austenitic structures by targeted heat treatment of the surfaces in an oxygen-containing atmosphere.
- This heat treatment in an oxygen-containing atmosphere is often referred to below as heat treatment or thermal treatment.
- the stainless steel workpiece is heated to a temperature of at least 80 ° C for a certain period of time.
- the upper limit of the temperature to be used is given by the temperature at which a thermally induced discoloration of the stainless steel surface begins and varies depending on the quality of stainless steel used.
- the present invention thus relates to a method for passivating stainless steel, wherein the stainless steel is first subjected to a chemical treatment with an aqueous solution, then rinsed with water and subsequently a heat treatment is carried out.
- the aqueous solution used in the chemical treatment comprises at least one complexing agent combination and an oxidizing agent.
- the complexing agent combination consists of those compounds known to complex iron ions in aqueous solution.
- the invention is based in particular on the observation that only with a combination of the complexing agents a passivation effect is achieved, which satisfies the objectives of the invention.
- complexing agents are used in particular hydroxcarboxylic acids, phosphonic acids and organic nitrosulfonic acids.
- the complexing agents used are multidentate complexing agents. These multidentate complexing agents form chelate complexes with the iron ions and therefore contribute to further increasing the ratio of chromium oxide to iron oxide in the passive layer.
- suitable complexing agents include, for example, hydroxycarboxylic acids which have 2 or 3 hydroxyl groups and 2 or 3 carboxyl groups or salts thereof.
- a particularly suitable example of such a hydroxycarboxylic acid is citric acid.
- Another suitable complexing agent is a diphosphonic acid of the general structure R "[- PO (OH) 2 ] 2 , where R" is a divalent alkyl, hydroxyalkyl or aminoalkyl radical.
- R is a divalent alkyl, hydroxyalkyl or aminoalkyl radical.
- R is a divalent alkyl, hydroxyalkyl or aminoalkyl radical.
- a particularly preferred example of such an acid is 1-hydroxyethane-1,1-diphosphonic acid (HEDP) or its salts.
- HEDP 1-hydroxyethane-1,1-diphosphonic acid
- nitrosulphonic acids ie the nitroalkylsulphonic acids, nitroarylsulphonic acids or their salts.
- a particularly preferred nitroarylsulfonic acid is meta- nitrobenzenesulfonic acid.
- the acid or the salt has sufficient solubility in the aqueous solution.
- the carbon chains whether linear, branched, cyclic or aromatic, comprise not more than about 12 carbon atoms, more preferably not more than 10 carbon atoms, and most preferably not more than 6 carbon atoms.
- oxidizing agent Another essential ingredient of the aqueous solution in the chemical treatment is an oxidizing agent.
- This oxidizing agent must be sufficient to ensure a normal potential of at least +300 mV in the solution.
- Suitable oxidizing agents include, for example, nitrates, peroxo compounds, iodates and cerium (IV) compounds in the form of the respective acids or the corresponding water-soluble salts.
- peroxo compounds are peroxides, persulfates, perborates or else percarboxylates, such as peracetate. These oxidizing agents can be used alone or in the form of mixtures.
- the term "stainless steel” refers to iron alloys containing at least 13 weight percent chromium. Other corrosion resistance improving elements may be included in the alloy.
- the chemical treatment according to the invention is not to be confused with a conventional pickling process, in which targeted metal from the surface of a metallic Workpiece is removed (see. DE 92 14 890 U1 EP 0596 273 A , and WO 88/00252 A1 ).
- the inventors of the present application suspect that the special effect of the method according to the invention is attributable to the fact that a passive layer is not first produced, but an already existing passive layer is changed in its composition and structure by the sequence of the method steps according to the invention. But this is rather a theoretical idea that can not be understood in the sense of a limitation of the present method.
- the aqueous solutions may also comprise one or more wetting agents which reduce the surface tension of the aqueous solution.
- suitable wetting agents are, for example, the nitroalkyl or nitroaryl sulfonic acids already described in the case of the complexing agents, or also alkyl glycols of the general structure H- (O-CHR-CH 2 ) n -OH, where R is hydrogen or an alkyl radical having 1, 2 or 3 Is carbon atoms, and n is preferably an integer between 1 and 5, for example 2 or 3; or other wetting agents.
- the at least one hydroxycarboxylic acid comprises citric acid, and / or the at least one diphosphonic acid HEDP, and / or the at least one nitroaryl or nitroalkyl sulfonic acid m- nitrobenzenesulfonic acid, and / or the at least one alkyl glycol, ethylene glycol and / or butyl glycol, and Oxidizing agent nitrate, peroxide, persulfate and / or cerium (IV) ions, in each case in the weight ratios indicated above.
- compositions may be added to the above compositions in a concentration between 0.02 and 2.0% by weight, preferably between 0.05 and 1.0% by weight.
- thickening agents may optionally be added to these compositions. These thickening agents, for example diatomaceous earth, can serve to increase the viscosity of the solution.
- the chemical treatment in aqueous solution is preferably carried out in a dip bath, so that such thickeners can be dispensed with.
- the aqueous solution preferably has a pH which is less than 7, preferably less than 4. This can be achieved by the aqueous solution containing at least one acid.
- a preferred method is that at least one of the complexing agents and / or at least one of the oxidizing agents is at least partially added in the form of an acid to the solution.
- the first step of the treatment according to the present invention in a preferred embodiment, is in an aqueous solution having a temperature of at most about 70 ° C. It is further preferred that the treatment takes place in aqueous solution at a temperature between room temperature and 60 ° C.
- the chemical treatment in aqueous solution is preferably carried out over a period of at least 60 minutes, for example, the chemical treatment can be carried out with an aqueous solution over a period of 1-4 hours.
- the workpiece is rinsed with water, preferably deionized water, to remove the passivating solution, and optionally dried, before the workpiece enters the passivation solution
- Water preferably deionized water
- Temperature treatment is subjected. This rinsing can be done by spraying or by (possibly repeated) immersion in a dipping bath or by combinations of these rinsing methods.
- the step of heat treatment is carried out at a temperature of at least 80 ° C in an oxygen-containing atmosphere.
- the heat treatment is preferably carried out at a temperature in the range between 80 ° C and 280 ° C, in particular at a temperature above 100 ° C and at most 260 ° C.
- the oxygen-containing atmosphere of the thermal treatment may be air in a preferred embodiment.
- the oxygen-containing atmosphere is primarily water vapor or a mixture of water vapor and air.
- Such a steam-containing atmosphere is preferably used at a temperature of at least 100 ° C.
- the optimum temperature range for the heat treatment depends essentially on the type of stainless steel to be treated. However, this optimum range can easily be determined by a person of ordinary skill in trial experiments.
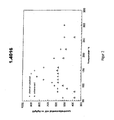
- a suitable temperature in a range between 100 ° C and 270 ° C, preferably between 150 ° C and 260 ° C, in particular between 220 ° C and 260 ° C, when the stainless steel is an austenitic steel having a content of about 16-20 wt .-% chromium and about 7-10 wt .-% nickel, such as stainless steel grade 1.4301 (see. FIG. 1 ).
- the term "essentially none" means that the elements in question, if present at all, are present in a concentration of less than 1% by weight, generally between 0 and 0.1% by weight, in the alloy.
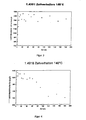
- This heat treatment should take place over a period of at least 2 minutes (cf. FIG. 3 for quality 1.4301 stainless steel). Preferably, the heat treatment takes place over a period of 15-45 minutes, for example for about 30 minutes. Depending on the quality of the stainless steel, too long a thermal treatment, for example over several hours, can lead to a fall in the corrosion resistance of the treated workpiece.
- a stainless steel of quality 1.4016 when heated to 140 ° C, ie at a temperature which is in the optimum range for the heat treatment first shows a rapid increase in the pitting potential to values around +1000 mV (cf. FIG. 4 ). However, if such a workpiece is exposed to this temperature for longer periods, the pitting potential drops again to values of about +700 mV. It is therefore important for some types of stainless steel that the heat treatment is carried out no longer than about 90 minutes, preferably not longer than about 60 minutes.
- Another important advantage of the method described here is that it is not only suitable for significantly increasing the corrosion resistance, measured as the pitting potential according to DIN 50900, compared with the starting state, but that the method is also suitable for the resistance of stainless steel workpieces to increase thermal discoloration.
- Such an increase in the resistance of stainless steel workpieces or their surfaces against thermal discoloration in their use by a passivation process has not been described and represents a further significant advantage of the invention described herein.
- the prior art discloses, inter alia, also a method for cleaning and passivating a stainless steel surface, in which a hydroxyacetic acid or citric acid is applied to the surface in an aqueous solution (cf. EP 0 776 256 B1 ).
- a hydroxyacetic acid or citric acid is applied to the surface in an aqueous solution
- the content of hydroxycarboxylic acid in this process is well below 3.0 wt .-%.
- the complexes used easily precipitate and are incorporated into the oxide film over the workpiece (see. Paragraph [0032] of the aforementioned EP 0 776 256 B1 ).
- Example 1 Stainless steel of quality 1.4301
- the chemical treatment was carried out at 40 ° C for 180 min. Subsequently, the sheet was rinsed with deionized water and dried in air.
- the pitting potential of plate B was measured at +750 mV, an increase of +200 mV compared to the initial state.
- sheet D was treated in a passivation solution whose composition is described in Example 1. The treatment takes place at room temperature (+ 22 ° C) for a duration of 2.5 h. Subsequently, the plate was rinsed clean with deionized water, dried in air and the pitting potential measured at +520 mV, an increase from the initial state by +150 mV.
- this example shows that when exceeding the optimal temperature range for a certain quality stainless steel corrosion resistance decreases again, but still higher than before the passivation treatment.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Chemical Treatment Of Metals (AREA)
- Crystals, And After-Treatments Of Crystals (AREA)
- Treatment Of Steel In Its Molten State (AREA)
Claims (14)
- Procédé de passivation d'acier inoxydable, d'après lequel on soumet l'acier inoxydable- tout d'abord à un traitement chimique avec une solution aqueuse, qui contient au moins un agent complexant multi-denté pour le fer et au moins un agent oxydant, l'agent oxydant étant suffisant pour assurer dans la solution, un potentiel normal d'au moins +300 mV,- après cela, à une étape de rinçage avec de l'eau, et- ensuite, à un traitement thermique à une température d'au moins 80 °C dans une atmosphère renfermant de l'oxygène.
- Procédé selon la revendication 1, caractérisé en ce que l'on met en oeuvre une combinaison d'agents complexants, la combinaison d'agents complexants étant composée :- d'au moins un acide hydroxycarbonique avec 2 à 3 groupes hydroxyles et 2 à 3 groupes carboxyles, respectivement leur(s) sel(s),- d'au moins un acide diphosphonique de structure générale R"[-PO(OH)2]2 respectivement leur(s) sel(s), R" étant un reste divalent alkyle, hydroxyalkyle ou aminoalkyle, et- d'au moins un acide sulfonique de nitroaryle ou de nitroalkyle respectivement leur(s) sel(s).
- Procédé selon l'une des revendications 1 à 2, dans lequel l'agent oxydant comprend au moins un composé qui est choisi parmi le groupe constitué par le nitrate, peroxyde, persulfate, perborate, les percarboxylates, l'iodate et les composés de cérium(IV) sous la forme des acides et/ou sels respectifs.
- Procédé selon l'une des revendications 1 à 3, caractérisé en ce que la solution aqueuse comprend :- 0,5 à 10 % en poids d'au moins un acide hydroxycarbonique avec deux à trois groupes hydroxyles et deux à trois groupes carboxyles respectivement leur(s) sel(s),- 0,5 à 5,0 % en poids d'au moins un acide phosphonique de structure générale R"[-PO(OH)2]2 respectivement leur(s) sel(s), R" étant un reste divalent alkyle, hydroxyalkyle ou aminoalkyle,- 0,1 à 5,0 % en poids d'au moins un acide sulfonique de nitroaryle ou de nitroalkyle respectivement leur(s) sel(s),- 0,05 à 1,0 % en poids d'au moins un alkylglycol de structure générale H-(O-CHR-CH2)n-OH, R étant de l'hydrogène ou un reste alkyle avec 1 à 3 atomes de carbone, et n étant égal 1 à 5, et- 0,2 à 20 % en poids d'un agent oxydant, qui est suffisant pour assurer dans la solution, un potentiel normal d'au moins +300 mV,
le reste de la solution étant de l'eau à laquelle peuvent, en outre, encore être additionnés, éventuellement, un ou plusieurs épaississants. - Procédé selon l'une des revendications 1 à 4, dans lequel le traitement chimique est effectué dans une solution aqueuse, à une température d'au plus 70 °C.
- Procédé selon l'une des revendications 1 à 5, caractérisé en ce que le traitement chimique est effectué dans une solution aqueuse, pendant une durée de 1 à 4 heures.
- Procédé selon l'une des revendications 1 à 6, caractérisé en ce que le traitement thermique, qui suit, est effectué dans une atmosphère d'air, une atmosphère de vapeur d'eau ou dans un mélange d'air et de vapeur d'eau.
- Procédé selon l'une des revendications 1 à 7, caractérisé en ce que le traitement thermique, qui suit, est effectué à une température comprise dans une plage entre 80 °C et 280 °C.
- Procédé selon la revendication 8, caractérisé en ce que la température du traitement thermique, qui suit, se situe dans une plage entre 100 °C et 270 °C, de préférence entre 150 °C et 260 °C, lorsque l'acier inoxydable est un acier austénitique, qui présente une teneur de 16 à 20 % en poids de chrome et de 7 à 10 % en poids de nickel.
- Procédé selon la revendication 9, caractérisé en ce que la température lors du traitement thermique, qui suit, se situe dans une plage entre 100 °C et 190 °C, de préférence entre 120 °C et 160 °C, lorsque l'acier inoxydable est un acier ferritique, qui présente une teneur de 16 à 20 % en poids de chrome, et ne renferme sensiblement pas de nickel et/ou de molybdène.
- Procédé selon l'une des revendications 1 à 10, caractérisé en ce que le traitement thermique, qui suit, est effectué pendant une durée d'au moins 2 minutes.
- Procédé selon l'une des revendications 1 à 11, caractérisé en ce que le traitement thermique, qui suit, est effectué pendant une durée de 15 à 45 minutes.
- Utilisation d'un procédé selon l'une des revendications 1 à 12, pour augmenter la tenue à la corrosion de surfaces en acier inoxydable.
- Utilisation d'un procédé selon l'une des revendications 1 à 12, pour augmenter la capacité de résistance de surfaces en acier inoxydable, à l'encontre de changements de coloration d'origine thermique.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL08715970T PL2147131T3 (pl) | 2007-03-05 | 2008-02-22 | Sposób termochemicznej pasywacji stali szlachetnej |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102007010538A DE102007010538A1 (de) | 2007-03-05 | 2007-03-05 | Verfahren zum thermochemischen Passivieren von Edelstahl |
| PCT/EP2008/001419 WO2008107082A1 (fr) | 2007-03-05 | 2008-02-22 | Procédé de passivation thermochimique d'acier inoxydable |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2147131A1 EP2147131A1 (fr) | 2010-01-27 |
| EP2147131B1 true EP2147131B1 (fr) | 2011-08-17 |
Family
ID=39432890
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08715970A Active EP2147131B1 (fr) | 2007-03-05 | 2008-02-22 | Procédé de passivation thermochimique d'acier inoxydable |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US8430973B2 (fr) |
| EP (1) | EP2147131B1 (fr) |
| JP (1) | JP5222308B2 (fr) |
| AT (1) | ATE520802T1 (fr) |
| DE (1) | DE102007010538A1 (fr) |
| ES (1) | ES2370088T3 (fr) |
| PL (1) | PL2147131T3 (fr) |
| WO (1) | WO2008107082A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102014203412A1 (de) | 2013-02-25 | 2014-08-28 | Zschimmer & Schwarz Mohsdorf GmbH &Co.KG. | Verfahren und Formulierung zur gleichzeitigen Entschichtung und Passivierung von Edelstahloberflächen |
Families Citing this family (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2182095A1 (fr) * | 2008-10-29 | 2010-05-05 | Poligrat Gmbh | Procédé destiné au traitement de surfaces en acier inoxydable |
| US8906579B2 (en) * | 2009-05-14 | 2014-12-09 | GM Global Technology Operations LLC | Low contact resistance coated stainless steel bipolar plates for fuel cells |
| EP2617866A1 (fr) | 2012-01-23 | 2013-07-24 | Merz Pharma GmbH & Co. KGaA | Procédé et composition de préparation d'instruments médicaux |
| DE102012107807A1 (de) * | 2012-08-24 | 2014-02-27 | Paul Hettich Gmbh & Co. Kg | Verfahren zur Herstellung eines metallischen Bauteils eines Beschlages, Ofenbeschlag und Ofen mit Pyrolysereinigungsfunktion |
| CN103225087B (zh) * | 2013-04-26 | 2015-04-01 | 河南师范大学 | 一种不锈钢酸洗钝化膏及其制备方法 |
| EP3084035B1 (fr) * | 2013-12-18 | 2018-08-15 | SEPIES GmbH | Procédé de fabrication de surfaces en acier inoxydable colorées |
| US9202483B1 (en) * | 2015-01-02 | 2015-12-01 | HGST Netherlands B.V. | Iron-oxidized hard disk drive enclosure cover |
| EP3162558A1 (fr) | 2015-10-30 | 2017-05-03 | Outokumpu Oyj | Composant constitué d'un matériau composite métallique et procédé pour la fabrication du composant par formage à chaud |
| CN106637175B (zh) * | 2016-11-09 | 2019-02-22 | 深圳市麦滕医疗器械有限公司 | 外科手术器械用马氏体型抗菌不锈钢的表面钝化处理方法 |
| US10683576B2 (en) * | 2017-03-27 | 2020-06-16 | Baker Hughes, A Ge Company, Llc | Corrosion inhibitors for passivation of galvanized coatings and carbon steel |
| JP7299012B2 (ja) * | 2018-12-17 | 2023-06-27 | 株式会社Ihiインフラシステム | 不動態化処理方法、不動態化処理液及び不動態化処理容器 |
| CN114086189B (zh) * | 2021-11-24 | 2024-03-08 | 宁波吉海金属科技有限公司 | 一种环保型不锈钢酸洗钝化液 |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2601379A1 (fr) * | 1986-07-09 | 1988-01-15 | Commissariat Energie Atomique | Produit decapant pour pieces en acier et procede de decapage utilisant ce produit |
| DE3991748T1 (fr) * | 1989-09-21 | 1991-10-10 | ||
| US5354383A (en) | 1991-03-29 | 1994-10-11 | Itb, S.R.L. | Process for pickling and passivating stainless steel without using nitric acid |
| DE4237021C1 (de) * | 1992-11-02 | 1994-02-10 | Poligrat Gmbh | Mittel zum Beizen der Oberfläche von Chromnickelstählen und Chromstählen sowie Verwendung des Mittels |
| DE9214890U1 (de) * | 1992-11-02 | 1993-01-07 | Poligrat GmbH, 8000 München | Mittel zum Beizen und/oder Reinigen von Metalloberflächen |
| JP2941948B2 (ja) * | 1994-09-26 | 1999-08-30 | カルゴン ベスタル, インコーポレイテッド | ステンレス鋼酸処理 |
| IT1276954B1 (it) * | 1995-10-18 | 1997-11-03 | Novamax Itb S R L | Processo di decapaggio e di passivazione di acciaio inossidabile senza impiego di acido nitrico |
| AUPO371096A0 (en) * | 1996-11-18 | 1996-12-12 | Green, Bruce Phillip | Corrosion inhibiting composition |
| CA2253679A1 (fr) | 1998-01-26 | 1999-07-26 | Elf Atochem S.A. | Passivation des aciers inoxydables en milieu acide organosulfonique |
| AUPQ633200A0 (en) * | 2000-03-20 | 2000-04-15 | Commonwealth Scientific And Industrial Research Organisation | Process and solution for providing a conversion coating on a metallic surface I |
| US7524383B2 (en) * | 2005-05-25 | 2009-04-28 | Tokyo Electron Limited | Method and system for passivating a processing chamber |
| US20090120457A1 (en) * | 2007-11-09 | 2009-05-14 | Surface Chemistry Discoveries, Inc. | Compositions and method for removing coatings and preparation of surfaces for use in metal finishing, and manufacturing of electronic and microelectronic devices |
-
2007
- 2007-03-05 DE DE102007010538A patent/DE102007010538A1/de not_active Withdrawn
-
2008
- 2008-02-22 WO PCT/EP2008/001419 patent/WO2008107082A1/fr not_active Ceased
- 2008-02-22 JP JP2009552092A patent/JP5222308B2/ja not_active Expired - Fee Related
- 2008-02-22 AT AT08715970T patent/ATE520802T1/de active
- 2008-02-22 EP EP08715970A patent/EP2147131B1/fr active Active
- 2008-02-22 US US12/529,858 patent/US8430973B2/en not_active Expired - Fee Related
- 2008-02-22 ES ES08715970T patent/ES2370088T3/es active Active
- 2008-02-22 PL PL08715970T patent/PL2147131T3/pl unknown
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102014203412A1 (de) | 2013-02-25 | 2014-08-28 | Zschimmer & Schwarz Mohsdorf GmbH &Co.KG. | Verfahren und Formulierung zur gleichzeitigen Entschichtung und Passivierung von Edelstahloberflächen |
Also Published As
| Publication number | Publication date |
|---|---|
| DE102007010538A1 (de) | 2008-09-11 |
| US20100132844A1 (en) | 2010-06-03 |
| ATE520802T1 (de) | 2011-09-15 |
| ES2370088T3 (es) | 2011-12-12 |
| US8430973B2 (en) | 2013-04-30 |
| JP5222308B2 (ja) | 2013-06-26 |
| EP2147131A1 (fr) | 2010-01-27 |
| JP2010521581A (ja) | 2010-06-24 |
| WO2008107082A1 (fr) | 2008-09-12 |
| WO2008107082A8 (fr) | 2008-11-20 |
| PL2147131T3 (pl) | 2012-01-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2147131A1 (fr) | Procédé de passivation thermochimique d'acier inoxydable | |
| DE102007061193B4 (de) | Wälzbeanspruchtes Bauteil und Verfahren zur Oberflächenbehandlung eines wälzbeanspruchten Bauteils | |
| EP2255026B1 (fr) | Passivation optimisée à base de ti-zr de surfaces métalliques | |
| DE972727C (de) | Verfahren zur Behandlung von Metalloberflaechen vor dem Aufbringen von UEberzuegen | |
| DE102009044821B4 (de) | Behandlungslösung und Verfahren zur Beschichtung von Metalloberflächen | |
| DE3213384A1 (de) | Waessrige saure loesung und verfahren fuer die behandlung aufnahmefaehiger metallsubstrate zur verleihung eines passivierungsfilms | |
| DE4312417A1 (de) | Verfahren zur Erhöhung der Korrosionsbeständigkeit von nichtrostendem Stahl | |
| DE2904402A1 (de) | Phosphatierungsmittel | |
| DE1558628B2 (de) | Verfahren zur Herstellung einer oxidationsbestaendigen Kupferlegierung | |
| DE1182928B (de) | Verfahren und Loesung zum Nachbehandeln von Phosphatschichten | |
| DE3711095A1 (de) | Verfahren zur erzeugung von konversionsueberzuegen auf zink- oder zinklegierungsoberflaechen | |
| EP1678344A1 (fr) | Procede essentiellement exempt de chrome destine a la passivation de surfaces metalliques en zn, alliages de zn, al ou alliages d'al | |
| DE2315180C2 (de) | Phosphatierungslösung | |
| EP2352860B1 (fr) | Procédé destiné au traitement de surfaces en acier inoxydable | |
| EP1816234B1 (fr) | Procédé et composition aqueuse pour la passivation du zinc ou des alliages à base de zinc | |
| DE3232396C2 (fr) | ||
| DE3009931C2 (de) | Mittel zum Schützen von Stahloberflächen | |
| DE1295962B (de) | Verfahren und Zusatzmittel zur Herstellung von Boehmit auf Aluminiumoberflaechen | |
| DE3033961C2 (de) | Wäßriges Bad zum anodischen Entfernen von Metallüberzügen von einem davon verschiedenen Grundmetall sowie ein Verfahren zum anodischen Entfernen von Metallüberzügen unter Verwendung dieses Bades | |
| DE2715291A1 (de) | Verfahren zur herstellung amorpher, leichter, festhaftender phosphatueberzuege an eisenmetalloberflaechen | |
| DE102013107011A1 (de) | Verfahren zum Beschichten von Cu-Langprodukten mit einer metallischen Schutzschicht und mit einer metallischen Schutzschicht versehenes Cu-Langprodukt | |
| DE2239581C3 (de) | Lösung und Verfahren zum Aufbringen von Überzügen auf Zink oder Zinklegierungen | |
| DE102014203412B4 (de) | Verfahren, Formulierung und Verwendung der Formulierung zur gleichzeitigen Entschichtung und Passivierung von Edelstahloberflächen | |
| EP2821520A1 (fr) | Procédé de revêtement de produits plats en acier avec une couche de protection métallique et produits plats en acier revêtus d'une couche de protection métallique | |
| DE69330580T2 (de) | Eisen-Chrom-Legierung mit hoher Korrosionsbeständigkeit |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20090826 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA MK RS |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C23C 22/82 20060101ALI20110215BHEP Ipc: C23C 22/74 20060101ALN20110215BHEP Ipc: C23C 22/50 20060101AFI20110215BHEP |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 502008004523 Country of ref document: DE Representative=s name: WUESTHOFF & WUESTHOFF PATENT- UND RECHTSANWAEL, DE Ref country code: DE Ref legal event code: R082 Ref document number: 502008004523 Country of ref document: DE Representative=s name: WUESTHOFF & WUESTHOFF, PATENTANWAELTE PARTG MB, DE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502008004523 Country of ref document: DE Effective date: 20111117 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2370088 Country of ref document: ES Kind code of ref document: T3 Effective date: 20111212 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20110817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111217 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111117 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111219 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111118 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E013217 Country of ref document: HU |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 |
|
| 26N | No opposition filed |
Effective date: 20120521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120328 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502008004523 Country of ref document: DE Effective date: 20120521 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120229 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111117 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110817 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120222 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 502008004523 Country of ref document: DE Representative=s name: WUESTHOFF & WUESTHOFF, PATENTANWAELTE PARTG MB, DE Ref country code: DE Ref legal event code: R081 Ref document number: 502008004523 Country of ref document: DE Owner name: POLIGRAT DEUTSCHLAND GMBH, DE Free format text: FORMER OWNER: POLIGRAT GMBH, 81829 MUENCHEN, DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: BOVARD SA NEUCHATEL CONSEILS EN PROPRIETE INTE, CH Ref country code: CH Ref legal event code: PUE Owner name: POLIGRAT DEUTSCHLAND GMBH, DE Free format text: FORMER OWNER: POLIGRAT GMBH, DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A Owner name: POLIGRAT DEUTSCHLAND GMBH Effective date: 20190919 |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: FH1C Free format text: FORMER REPRESENTATIVE(S): DR. SVINGOR ADAM, DANUBIA SZABADALMI ES JOGI IRODA KFT., HU Representative=s name: DANUBIA SZABADALMI ES JOGI IRODA KFT., HU Ref country code: HU Ref legal event code: GB9C Owner name: POLIGRAT DEUTSCHLAND GMBH, DE Free format text: FORMER OWNER(S): POLIGRAT GMBH, DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: PD Owner name: POLIGRAT DEUTSCHLAND GMBH; DE Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), ASSIGNMENT; FORMER OWNER NAME: POLIGRAT GMBH Effective date: 20191010 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: PD Owner name: POLIGRAT DEUTSCHLAND GMBH; DE Free format text: DETAILS ASSIGNMENT: CHANGE OF OWNER(S), CESSION Effective date: 20191007 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: PC Ref document number: 520802 Country of ref document: AT Kind code of ref document: T Owner name: POLIGRAT DEUTSCHLAND GMBH, DE Effective date: 20191202 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20200213 AND 20200219 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20211220 Year of fee payment: 15 Ref country code: GB Payment date: 20211220 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20211229 Year of fee payment: 15 Ref country code: NL Payment date: 20211220 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20220216 Year of fee payment: 15 Ref country code: HU Payment date: 20220209 Year of fee payment: 15 Ref country code: FI Payment date: 20220215 Year of fee payment: 15 Ref country code: CH Payment date: 20220216 Year of fee payment: 15 Ref country code: AT Payment date: 20220216 Year of fee payment: 15 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20220216 Year of fee payment: 15 Ref country code: IT Payment date: 20220228 Year of fee payment: 15 Ref country code: ES Payment date: 20220318 Year of fee payment: 15 Ref country code: CZ Payment date: 20220211 Year of fee payment: 15 Ref country code: BE Payment date: 20220216 Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20230301 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 520802 Country of ref document: AT Kind code of ref document: T Effective date: 20230222 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20230228 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20230222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230223 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230228 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230228 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230301 Ref country code: HU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230223 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230228 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20240405 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230223 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230223 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230222 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20260217 Year of fee payment: 19 |