EP2182082A1 - Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier - Google Patents
Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier Download PDFInfo
- Publication number
- EP2182082A1 EP2182082A1 EP08105692A EP08105692A EP2182082A1 EP 2182082 A1 EP2182082 A1 EP 2182082A1 EP 08105692 A EP08105692 A EP 08105692A EP 08105692 A EP08105692 A EP 08105692A EP 2182082 A1 EP2182082 A1 EP 2182082A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- contact
- steel
- steel sheet
- contact plate
- temperature
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/62—Quenching devices
- C21D1/673—Quenching devices for die quenching
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21J—FORGING; HAMMERING; PRESSING METAL; RIVETING; FORGE FURNACES
- B21J1/00—Preparing metal stock or similar ancillary operations prior, during or post forging, e.g. heating or cooling
- B21J1/06—Heating or cooling methods or arrangements specially adapted for performing forging or pressing operations
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/34—Methods of heating
Definitions
- the invention relates to a method and a device for tempering a steel sheet body.
- metal sheets or sheet metal parts made of high-strength steel alloys are used, for example, in automobile bodies, which allow for the same strength a design with lower sheet thickness.
- high strength sheets sometimes do not have sufficient deformability on cold forming. Therefore, for forming workpieces made of high-strength metal sheets forming processes at elevated temperatures, ie hot forming processes, such as the so-called press hardening used.
- the sheet metal plates to be formed are fully austenitized by heating to a temperature above A c3 (so-called austenitization) and then placed in a pressing tool, transformed (so-called hot forming) and cooled in the tool and hardened (so-called direct press hardening).
- roller pass furnaces are used to heat the sheet steel body during austenitizing.
- the steel sheet body is placed in the oven and heated relatively slowly during the passage through the roller conveyor.
- the residence time of the steel sheet body within the furnace is typically about 5 to 10 minutes.
- the forming phase of the process is initiated, with the two halves of the tool being closed.
- the mold halves must be closed to the temperature of the martensitic microstructure transformation (approx. 400 ° C) before the sheet steel body cools down.
- the formed component remains in the mold and is further quenched, thereby completing the induced martensitic microstructure transformation and achieving the final properties of the component.
- the transport between the furnace and the pressing tool represents a fault-prone process step.
- the temperature of the sheet material can be limited control and control during transport, since the temporal and thermal conditions during the transfer of the steel sheet body from the furnace into a subsequent forming tool not exactly defined and can be safely reproduced. This can lead to uncontrollable changes in the properties of the sheet material and thus the Umform s.
- the sheet materials when they come out of the oven a relatively high temperature. This leads to an increased wear on the forming tool.
- the cycle times required for the hot forming increase, since a relatively long period of time is necessary for the cooling of the sheet material in the tool to a temperature that allows the demoulding.
- the object of the invention is to provide a method and a device for tempering at least one steel sheet body between austenitizing and hot working.
- the wear of the tools should be reduced by the smaller temperature gradients and less shrinkage of the steel sheet body in the tool.
- shortening the cycle times of the press should be achieved by reducing the cooling time in the mold.
- the steel sheet body located at austenitizing temperature is fixed in position, at least one first contact plate is brought into contact with at least one first surface portion of the steel sheet body and at least one second contact plate with at least one second Surface portion of the steel sheet body brought into contact.
- the contact plates are flat substantially or completely formed according to the contour of the surface portions of the sheet steel body and arranged in the state of contacting with the sheet steel body substantially parallel to each other. At least one contact plate has during the contacting of the steel sheet body with respect to the steel sheet body lower temperature.
- a sheet steel body here are both single substantially planar-shaped sheets and steel blanks, as well as three-dimensionally shaped sheet metal parts made of steel and also components that are composed of several such sheets understood.
- the austenitizing temperature is understood to mean the temperature above A c3 at which the steel sheet body was austenitized.
- the method according to the invention can be used variably.
- the temperature which the contact plate has or on which the steel sheet body is brought, as well as the period of time for which the contact between contact plates and steel sheet body, can be chosen almost arbitrarily.
- the contact between sheet steel body and contact plates may be formed such that the contact plates and the sheet steel body touch directly. However, it may also be an intermediate layer, such as a contact agent, which improves the temperature balance between the contact plate and sheet steel body, be present.
- the area associated with the contact plates surface portions can both extend over large parts of the sheet steel body or completely cover this and form only small, localized areas of the sheet steel body. If only locally limited areas are connected to the contact plates, a local thermal treatment of the steel sheet body can be carried out.
- a sheet metal plate made of a steel of the composition 22MnB5 and having an AlSi10 coating as steel sheet body located at austenitizing temperature is fixed between a first contact plate and a second contact plate.
- the contact plates have a temperature between 400 ° C and 600 ° C. After the sheet steel body has been contacted by the contact plates for a period of, for example, 10 seconds to 120 seconds, it is placed in a forming tool and hot worked.
- the device according to the invention is designed to carry out the method according to the invention and has a first surface formed contact plate, a second flat contact plate, which is arranged substantially parallel to the first contact plate, at least one heat source, which is in communication with at least one of the contact plates, and a closing device for varying the distance of the mutually parallel contact plates.
- the contact plates can both be made of the same material as well as of different materials.
- contact plates that are heated made of a metallic material, such as steel.
- Contact plates that are not heated may preferably be made of both metallic and non-metallic materials. In a particularly advantageous manner, contact plates that are not heated, made of an insulating material. This has the advantage that the heat loss is reduced.
- the contact plates may have an insulating layer. Also, the heat loss can be reduced thereby.
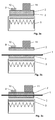
- Fig. 1 shows a schematic sectional view of an embodiment of the method according to the invention.
- the steel sheet body 1 has been brought by the displacement of the first contact plate 2 by means of the closing device 11 in the direction 4 with the first contact plate 2 in contact.
- a first surface portion 6 of the sheet steel body 1 is in communication with the first contact plate 2.
- the first surface section 6 lies on the upper side of the sheet metal and the second surface section 7 is located on the underside of the sheet metal.
- first surface portion 6 and the second surface portion 7 correspond to a portion of the top or bottom of the flat sheet steel body 1.
- first surface portion 6 and the second surface portion 7 of the entire bottom or the entire top of a flat sheet steel body 1 correspond.
- the contact plates 2, 3 are formed flat in accordance with the contour of the surface sections 6, 7 of the steel sheet body 1 and are arranged running parallel to one another in the state of contacting with the metal body 1.
- the contacting can be designed such that the first contact plate 2 and the second contact plate 3 are brought into contact with the steel sheet body 1 simultaneously. But it can also first a contact plate. 2 be brought into contact with the sheet steel body 1 and only later, a second contact plate 3 added.
- the second contact plate 3 is or was brought by an energy source 5 to a relative to the steel sheet body 1 lowered temperature.
- the contact plate 3 is brought to a temperature which is above room temperature but below the austenitizing temperature.
- Energy source 5 is understood below to mean any device that can be used to heat objects.
- a cooling device This can either be mounted in the immediate vicinity of one or both of the contact plates 2, 3 or integrated in them.
- 2.3 cooling channels can be introduced into one or both contact plates. This allows the passage of liquid or gaseous coolants through the contact plates 2,3, resulting in a particularly accurate cooling.
- the cooling device can thus regulate the temperature of the contact plates 2.3 particularly precisely.
- the contact plates 2, 3 are arranged running parallel to one another.
- the second contact plate 3 has an insulation layer 8. By this insulating layer 8, the heat or cooling loss can be reduced.
- the temperature of the steel sheet body 1 can be kept constant. However, it is also possible to vary the temperature of the steel sheet body 1 in the course of contacting by the defined change in the temperatures of the contact plates 2.3. Thus, a very variable adaptation of the temperature-time curve is possible.
- the temperature profile along a contact plate 2, 3 can be designed such that an almost constant temperature is established over the entire contact plate 2, 3.
- the contact plate 2, 3 can also be heated or cooled in such a way that regions with different temperatures form within the contact plate 2, 3.
- the first surface portion 6 brought into contact with the contact plates 2, 3 and the second surface portion 7 of the sheet steel body 1 may be the same size. However, they can also have different sizes (not shown).
- a temperature control device 9 and a temperature control device 10 may be attached on the contact plate 2. Furthermore, a temperature sensor element (not shown) may also be attached. This allows the measurement of the temperature of the steel sheet body 1 and / or the contact plates 2,3. The temperature measured in this way can serve, for example, as an input variable for the temperature control device 9 and / or the temperature control device 10, which controls and / or controls or controls the temperature-time profile of the thermal treatment.
- the temperature control device 9 can in this case control both the energy source 5 and the cooling device and thus ensure a particularly accurate temperature control of the contact plates 2.3 and thus the sheet steel body 1.
- the method can also be configured such that a plurality of steel sheet bodies 1 are simultaneously brought into contact with at least one first and / or one at least one second contact plate simultaneously.
- Fig. 2 shows a schematic sectional view of another embodiment of the method according to the invention.
- the steel sheet body 1 was brought by moving the first contact plate 2 with this and a second contact plate 3 in contact.
- the displacement of the two contact plates 2, 3 arranged parallel to one another takes place through the closing device 11.
- the first contact plate 2 is or has been brought to a temperature reduced relative to the steel sheet body by an energy source 5 and a cooling device (not shown).
- the second contact plate 3 is or was brought by a further energy source 5 and a further cooling device (not shown) to a relative to the steel sheet body elevated temperature.
- the first contact plate 2 and the second contact plate 3 can be brought by the energy sources 5 and the cooling devices both to the same temperature and to different temperatures.
- Fig. 3a shows a schematic sectional view of a first process step to a temperature of the contact plates.
- the first contact plate 2 and the second contact plate 3 are brought into mutual contact with each other before contacting with the steel sheet body.
- the second contact plate 3 is heated by the power source 5 to a temperature which is above room temperature and below the Austenitmaschinestemperatur.
- the temperature is subsequently transferred to the first contact plate 2 which is in contact with the second contact plate 3.
- Fig. 3b shows a schematic sectional view of a second method step to an application of the contact plates, which conform to the in Fig. 3a followed by the process step.
- the first contact plate 2 and the second contact plate 3 are separated from each other.
- the steel sheet body 1 located at austenizing temperature is introduced between the separate contact plates 2, 3.
- Fig. 3c shows a schematic sectional view of a third method step for an application of the contact plates 2 and 3, which conform to the in Fig. 3b followed by the process step.
- the first contact plate 2 and the second contact plate 3 were brought into contact with the steel sheet body 1 by closing the closing device 11. In this case, both the first contact plate 2 and the second contact plate 2 have a relation to the steel sheet body 1 lowered temperature.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Articles (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP08105692.1A EP2182082B2 (fr) | 2008-10-29 | 2008-10-29 | Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier |
| PCT/DE2009/075064 WO2010048951A1 (fr) | 2008-10-29 | 2009-10-28 | Procédé et dispositif de régulation de température d'un corps de tôle d'acier |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP08105692.1A EP2182082B2 (fr) | 2008-10-29 | 2008-10-29 | Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP2182082A1 true EP2182082A1 (fr) | 2010-05-05 |
| EP2182082B1 EP2182082B1 (fr) | 2013-12-25 |
| EP2182082B2 EP2182082B2 (fr) | 2018-01-24 |
Family
ID=40512180
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08105692.1A Not-in-force EP2182082B2 (fr) | 2008-10-29 | 2008-10-29 | Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP2182082B2 (fr) |
| WO (1) | WO2010048951A1 (fr) |
Cited By (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2547798A1 (fr) | 2010-03-16 | 2013-01-23 | Gestamp HardTech AB | Installation de trempe sur presse et procédé de trempe sur presse d'un flanc de tôle d'acier |
| EP2639536A2 (fr) | 2012-03-15 | 2013-09-18 | Benteler Automobiltechnik GmbH | Installation de four et procédé de fonctionnement de l'installation de four |
| DE102012102193A1 (de) | 2012-03-15 | 2013-09-19 | Benteler Automobiltechnik Gmbh | Ofenanlage sowie Verfahren zum Betreiben der Ofenanlage |
| WO2013140072A1 (fr) * | 2012-03-23 | 2013-09-26 | Herakles | Outillage de maintien pour traitement thermique de pieces metalliques |
| EP2455741A3 (fr) * | 2010-10-27 | 2013-10-23 | Schuler SMG GmbH & Co. KG | Procédé et dispositif destinés à la détermination de la dureté d'un composant durci à la presse |
| EP2730665A1 (fr) * | 2012-11-07 | 2014-05-14 | Benteler Automobiltechnik GmbH | Ligne moulée à chaud et procédé de fabrication d'un composant de véhicule automobile déformé à chaud et durci à la presse |
| EP2730346A1 (fr) * | 2012-11-07 | 2014-05-14 | Benteler Automobiltechnik GmbH | Ligne moulée à chaud pour la fabrication de produits de tôle d'acier moulés à chaud et durcis à la presse |
| DE102013101489B3 (de) * | 2013-02-14 | 2014-06-05 | Benteler Automobiltechnik Gmbh | Wärmebehandlungslinie und Verfahren zum Betreiben der Wärmebehandlungslinie |
| CN104946861A (zh) * | 2014-03-28 | 2015-09-30 | 本特勒尔汽车技术有限公司 | 用于导电式加热金属板坯的加热装置 |
| DE102014104922A1 (de) | 2014-04-07 | 2015-10-08 | Voestalpine Stahl Gmbh | Vorrichtung und Verfahren zum Kühlen von Stahlblechplatinen |
| DE102014105519A1 (de) | 2014-04-17 | 2015-10-22 | Schuler Pressen Gmbh | Vorrichtung und Verfahren zum Vorkühlen von Stahlblechplatinen |
| EP2182082B2 (fr) † | 2008-10-29 | 2018-01-24 | Neue Materialien Bayreuth GmbH | Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier |
| EP3141619B1 (fr) | 2015-09-08 | 2019-04-17 | ThyssenKrupp Steel Europe AG | Procédé et dispositif de réglage d'une propriété mécanique d'une pièce usinée en acier |
| EP2905346B1 (fr) * | 2014-01-23 | 2020-09-02 | Schwartz GmbH | Procede de traitement de la chaleur |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102013108972B4 (de) * | 2013-08-20 | 2016-03-17 | Benteler Automobiltechnik Gmbh | Temperierstation mit Induktorerwärmung |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102007009937A1 (de) | 2007-03-01 | 2008-09-04 | Schuler Smg Gmbh & Co. Kg | Verfahren zur Umformung einer Platine und Kühlvorrichtung für eine Platine |
| EP2014777A1 (fr) * | 2007-07-11 | 2009-01-14 | Neue Materialien Bayreuth GmbH | Procede et dipositif pour le traitement thermique d une tole metallique |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5435378A (en) † | 1991-06-04 | 1995-07-25 | Process And Equipment Development, Inc. | Apparatus for accurately heating and cooling articles |
| EP2182082B2 (fr) † | 2008-10-29 | 2018-01-24 | Neue Materialien Bayreuth GmbH | Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier |
-
2008
- 2008-10-29 EP EP08105692.1A patent/EP2182082B2/fr not_active Not-in-force
-
2009
- 2009-10-28 WO PCT/DE2009/075064 patent/WO2010048951A1/fr not_active Ceased
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102007009937A1 (de) | 2007-03-01 | 2008-09-04 | Schuler Smg Gmbh & Co. Kg | Verfahren zur Umformung einer Platine und Kühlvorrichtung für eine Platine |
| EP2014777A1 (fr) * | 2007-07-11 | 2009-01-14 | Neue Materialien Bayreuth GmbH | Procede et dipositif pour le traitement thermique d une tole metallique |
Cited By (31)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2182082B2 (fr) † | 2008-10-29 | 2018-01-24 | Neue Materialien Bayreuth GmbH | Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier |
| EP2547798A1 (fr) | 2010-03-16 | 2013-01-23 | Gestamp HardTech AB | Installation de trempe sur presse et procédé de trempe sur presse d'un flanc de tôle d'acier |
| EP2455741A3 (fr) * | 2010-10-27 | 2013-10-23 | Schuler SMG GmbH & Co. KG | Procédé et dispositif destinés à la détermination de la dureté d'un composant durci à la presse |
| EP2639536A2 (fr) | 2012-03-15 | 2013-09-18 | Benteler Automobiltechnik GmbH | Installation de four et procédé de fonctionnement de l'installation de four |
| DE102012102193A1 (de) | 2012-03-15 | 2013-09-19 | Benteler Automobiltechnik Gmbh | Ofenanlage sowie Verfahren zum Betreiben der Ofenanlage |
| DE102012102193B4 (de) * | 2012-03-15 | 2017-04-13 | Benteler Automobiltechnik Gmbh | Ofenanlage sowie Verfahren zum Betreiben der Ofenanlage |
| CN104245969A (zh) * | 2012-03-23 | 2014-12-24 | 赫拉克勒斯公司 | 用于金属部件的热处理的固定工具 |
| WO2013140072A1 (fr) * | 2012-03-23 | 2013-09-26 | Herakles | Outillage de maintien pour traitement thermique de pieces metalliques |
| FR2988401A1 (fr) * | 2012-03-23 | 2013-09-27 | Snecma Propulsion Solide | Outillage de maintien pour traitement thermique de pieces metalliques |
| US9903656B2 (en) | 2012-03-23 | 2018-02-27 | Airbus Safran Launchers Sas | Tooling for supporting metal parts during heat treatment |
| RU2630075C2 (ru) * | 2012-03-23 | 2017-09-05 | Эйрбас Сафран Лончерз Сас | Фиксирующий инструмент для термической обработки металлических деталей |
| CN104245969B (zh) * | 2012-03-23 | 2017-03-08 | 赫拉克勒斯公司 | 用于金属部件的热处理的固定工具 |
| EP2730346A1 (fr) * | 2012-11-07 | 2014-05-14 | Benteler Automobiltechnik GmbH | Ligne moulée à chaud pour la fabrication de produits de tôle d'acier moulés à chaud et durcis à la presse |
| EP2977472A1 (fr) * | 2012-11-07 | 2016-01-27 | Benteler Automobiltechnik GmbH | Station de chauffage de platines en tole |
| EP2730665A1 (fr) * | 2012-11-07 | 2014-05-14 | Benteler Automobiltechnik GmbH | Ligne moulée à chaud et procédé de fabrication d'un composant de véhicule automobile déformé à chaud et durci à la presse |
| CN103805761A (zh) * | 2012-11-07 | 2014-05-21 | 本特勒尔汽车技术有限公司 | 热成型加工线和利用它制造钢板制品的方法 |
| CN103805762A (zh) * | 2012-11-07 | 2014-05-21 | 本特勒尔汽车技术有限公司 | 热成型且加压淬火的汽车构件的制造方法和热成型生产线 |
| US9694408B2 (en) | 2012-11-07 | 2017-07-04 | Benteler Automobiltechnik Gmbh | Hot forming line and method for producing a hot formed and press hardened motor vehicle part |
| CN106755861A (zh) * | 2012-11-07 | 2017-05-31 | 本特勒尔汽车技术有限公司 | 用于对金属板坯进行调温的调温站 |
| EP2767599A1 (fr) * | 2013-02-14 | 2014-08-20 | Benteler Automobiltechnik GmbH | Ligne de traitement thermique et procédé de fonctionnement de la ligne de traitement thermique |
| CN103993137A (zh) * | 2013-02-14 | 2014-08-20 | 本特勒尔汽车技术有限公司 | 热处理作业线和操作热处理作业线的方法 |
| DE102013101489B3 (de) * | 2013-02-14 | 2014-06-05 | Benteler Automobiltechnik Gmbh | Wärmebehandlungslinie und Verfahren zum Betreiben der Wärmebehandlungslinie |
| EP2905346B1 (fr) * | 2014-01-23 | 2020-09-02 | Schwartz GmbH | Procede de traitement de la chaleur |
| CN104946861A (zh) * | 2014-03-28 | 2015-09-30 | 本特勒尔汽车技术有限公司 | 用于导电式加热金属板坯的加热装置 |
| WO2015155136A1 (fr) | 2014-04-07 | 2015-10-15 | Voestalpine Stahl Gmbh | Dispositif et procédé de refroidissement de flans en tôle d'acier |
| DE102014104922B4 (de) * | 2014-04-07 | 2017-10-19 | Voestalpine Stahl Gmbh | Vorrichtung und Verfahren zum Kühlen von Stahlblechplatinen |
| DE102014104922A1 (de) | 2014-04-07 | 2015-10-08 | Voestalpine Stahl Gmbh | Vorrichtung und Verfahren zum Kühlen von Stahlblechplatinen |
| DE102014105519B4 (de) * | 2014-04-17 | 2016-05-12 | Schuler Pressen Gmbh | Vorrichtung und Verfahren zum Vorkühlen von Stahlblechplatinen |
| WO2015158568A2 (fr) | 2014-04-17 | 2015-10-22 | Voestalpine Metal Forming Gmbh | Dispositif et procédé de pré-refroidissement de flans de tôle d'acier |
| DE102014105519A1 (de) | 2014-04-17 | 2015-10-22 | Schuler Pressen Gmbh | Vorrichtung und Verfahren zum Vorkühlen von Stahlblechplatinen |
| EP3141619B1 (fr) | 2015-09-08 | 2019-04-17 | ThyssenKrupp Steel Europe AG | Procédé et dispositif de réglage d'une propriété mécanique d'une pièce usinée en acier |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2182082B2 (fr) | 2018-01-24 |
| WO2010048951A1 (fr) | 2010-05-06 |
| EP2182082B1 (fr) | 2013-12-25 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2182082B1 (fr) | Procédé et dispositif destinés à l'équilibrage de la température d'un corps en tôle d'acier | |
| EP2182081B1 (fr) | Procédé destiné au traitement thermique d'un corps en tôle d'acier revêtu | |
| EP2014777B1 (fr) | Procédé et dispositif pour le traitement thermique d'une tôle métallique | |
| EP2324938B1 (fr) | Procédé et installation de formage à chaud destinés à la fabrication d'une pièce usinée durcie et déformée à chaud | |
| EP2473297B1 (fr) | Procédé et dispositif pour produire un composant métallique et utilisation d'un tel composant métallique | |
| DE102005032113B3 (de) | Verfahren und Vorrichtung zum Warmumformen und partiellen Härten eines Bauteils | |
| EP2233593B1 (fr) | Procédé et station de déformage à chaud pour la fabrication de composants de formage en tôle d'acier durcis par presse | |
| EP2143808B1 (fr) | Formage et durcissement à chaud partiels à l'aide d'un échauffement de lampes infrarouges | |
| DE102009015013B4 (de) | Verfahren zum Herstellen partiell gehärteter Stahlbauteile | |
| EP2497840B2 (fr) | Système de four pour le réchauffage partiel d'ébauches métalliques | |
| EP1426454A1 (fr) | Procédé de fabrication d'une piéce de forme avec au moins deux régions de structure de ductilité differente et four continu associé | |
| EP2710157A1 (fr) | Traitement thermique de pièces en tôle pouvant être trempées | |
| DE102011078075A1 (de) | Durch Warmbehandlungsnachbearbeitung passendgemachte Eigenschaften | |
| EP2931453B1 (fr) | Dispositif et procédé de formage à chaud | |
| EP2730346B2 (fr) | Ligne moulée à chaud pour la fabrication de produits de tôle d'acier moulés à chaud et durcis à la presse | |
| DE102008055980A1 (de) | Verfahren und Durchlaufofen zum Erwärmen von Werkstücken | |
| DE102017109613B3 (de) | Warmformlinie mit Temperierstation sowie Verfahren zum Betreiben | |
| DE102011056444B3 (de) | Verfahren und Vorrichtung zum partiellen Härten von Blechbauteilen | |
| DE102012012518A1 (de) | Warmumformwerkzeug zur Herstellung von Formteilen | |
| EP2883967B1 (fr) | Procédé et dispositif de post-traitement d'un élément de formage métallique durci au moyen du chauffage par résistance électrique | |
| WO2011082934A1 (fr) | Procédé et dispositif pour chauffer et refroidir partiellement des pièces dans un four continu | |
| DE102005055494B3 (de) | Verfahren zum Herstellen von einem Bauteil aus einem metallischen Flachprodukt durch Pressumformen | |
| EP2679692A1 (fr) | Procédé de fabrication d'un composant de formage en tôle d'acier durci par une presse | |
| DE102017201674B3 (de) | Verfahren zur Herstellung eines pressgehärteten Bauteils sowie Pressform | |
| DE102014104922A1 (de) | Vorrichtung und Verfahren zum Kühlen von Stahlblechplatinen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA MK RS |
|
| 17P | Request for examination filed |
Effective date: 20100928 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20110131 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B21J 1/06 20060101ALI20130806BHEP Ipc: C21D 1/673 20060101ALI20130806BHEP Ipc: C21D 9/46 20060101AFI20130806BHEP Ipc: C21D 1/34 20060101ALI20130806BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20131010 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 646702 Country of ref document: AT Kind code of ref document: T Effective date: 20140115 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502008011120 Country of ref document: DE Effective date: 20140213 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140325 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20131225 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140425 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140428 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 502008011120 Country of ref document: DE |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: BENTELER AUTOMOBILTECHNIK GMBH/ VOESTALPINE METAL Effective date: 20140925 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R026 Ref document number: 502008011120 Country of ref document: DE Effective date: 20140925 |
|
| PLAF | Information modified related to communication of a notice of opposition and request to file observations + time limit |
Free format text: ORIGINAL CODE: EPIDOSCOBS2 |
|
| PLBP | Opposition withdrawn |
Free format text: ORIGINAL CODE: 0009264 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20141029 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141031 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141029 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 646702 Country of ref document: AT Kind code of ref document: T Effective date: 20141029 |
|
| TPAC | Observations filed by third parties |
Free format text: ORIGINAL CODE: EPIDOSNTIPA |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20141029 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140326 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20081029 Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20131225 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| PUAH | Patent maintained in amended form |
Free format text: ORIGINAL CODE: 0009272 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT MAINTAINED AS AMENDED |
|
| 27A | Patent maintained in amended form |
Effective date: 20180124 |
|
| AK | Designated contracting states |
Kind code of ref document: B2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R102 Ref document number: 502008011120 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 502008011120 Country of ref document: DE Representative=s name: BOCKERMANN KSOLL GRIEPENSTROH OSTERHOFF, DE Ref country code: DE Ref legal event code: R081 Ref document number: 502008011120 Country of ref document: DE Owner name: BENTELER AUTOMOBILTECHNIK GMBH, DE Free format text: FORMER OWNER: NEUE MATERIALIEN BAYREUTH GMBH, 95448 BAYREUTH, DE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20181203 AND 20181205 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20211028 Year of fee payment: 14 Ref country code: GB Payment date: 20211022 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20211022 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502008011120 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20221029 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221031 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230503 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221029 |