EP2320441A1 - Aide au montage pour paquets de tôles de découpe - Google Patents
Aide au montage pour paquets de tôles de découpe Download PDFInfo
- Publication number
- EP2320441A1 EP2320441A1 EP10188988A EP10188988A EP2320441A1 EP 2320441 A1 EP2320441 A1 EP 2320441A1 EP 10188988 A EP10188988 A EP 10188988A EP 10188988 A EP10188988 A EP 10188988A EP 2320441 A1 EP2320441 A1 EP 2320441A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- slugs
- geometry
- sheets
- slug
- holes
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000003475 lamination Methods 0.000 title description 2
- 238000000034 method Methods 0.000 claims abstract description 15
- 238000004519 manufacturing process Methods 0.000 claims abstract description 3
- 241000237858 Gastropoda Species 0.000 claims description 22
- 239000002184 metal Substances 0.000 claims description 3
- 230000002093 peripheral effect Effects 0.000 claims description 2
- 238000011112 process operation Methods 0.000 abstract 2
- 239000002131 composite material Substances 0.000 description 7
- 210000001331 nose Anatomy 0.000 description 5
- 238000004080 punching Methods 0.000 description 3
- 238000005520 cutting process Methods 0.000 description 2
- 230000001419 dependent effect Effects 0.000 description 2
- 238000004049 embossing Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 229910000976 Electrical steel Inorganic materials 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 238000007373 indentation Methods 0.000 description 1
- 239000002905 metal composite material Substances 0.000 description 1
- 230000000750 progressive effect Effects 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
- 230000002123 temporal effect Effects 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D39/00—Application of procedures in order to connect objects or parts, e.g. coating with sheet metal otherwise than by plating; Tube expanders
- B21D39/03—Application of procedures in order to connect objects or parts, e.g. coating with sheet metal otherwise than by plating; Tube expanders of sheet metal otherwise than by folding
- B21D39/031—Joining superposed plates by locally deforming without slitting or piercing
- B21D39/032—Joining superposed plates by locally deforming without slitting or piercing by fitting a projecting part integral with one plate in a hole of the other plate
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D28/00—Shaping by press-cutting; Perforating
- B21D28/02—Punching blanks or articles with or without obtaining scrap; Notching
- B21D28/14—Dies
- B21D28/145—Dies with means for slug retention, e.g. a groove
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D43/00—Feeding, positioning or storing devices combined with, or arranged in, or specially adapted for use in connection with, apparatus for working or processing sheet metal, metal tubes or metal profiles; Associations therewith of cutting devices
- B21D43/20—Storage arrangements; Piling or unpiling
- B21D43/22—Devices for piling sheets
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F41/00—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties
- H01F41/02—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties for manufacturing cores, coils, or magnets
- H01F41/0206—Manufacturing of magnetic cores by mechanical means
- H01F41/0233—Manufacturing of magnetic circuits made from sheets
- H01F41/024—Manufacturing of magnetic circuits made from deformed sheets
Definitions
- the invention relates to a method for improving the accuracy of stanzp elected laminated cores, in particular of stanzp elected electrical steel cores.
- the punching package of sheets is a example of the EP0133858 A1 Known method for producing laminated cores in a single operation.
- the individual sheets cut out in a known progressive tool are stacked on top of one another and joined together by an integrated method described in more detail below in the tool.
- slugs are punched by an embossing process, leaving a slug hole in the form of a blind hole in the single sheet. In this hole, the slugs of the individual sheet produced in the next punching are pressed during the cutting process.
- the strength of the resulting composite sheet is dependent on the clamping force with which the slugs sit in the Butzenlöchern, which in turn depends on the dimensions of slugs and Butzenlöchern. These dimensions must be in close tolerances and their temporal consistency depends on various factors such as tool wear and tolerances in the material properties of the sheets. In addition, the slugs must be manufactured and joined with sufficient positioning accuracy with respect to the slug holes. If the rigorous Gebung from Butzen to Butzenloch too low, the composite sheet can separate again.
- the invention is therefore an object of the invention to improve the process of Stanzbierens such that the committee or the required rework is minimized by mutually releasing sheets and non-plane-parallel laminated cores.
- the slugs can be pre-embossed for better dimensional stability, the slug holes are pre-punched accordingly.
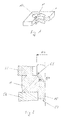
- Fig. 1 is an advantageous embodiment of a located in a first side of a single sheet Butzenlochs (10) with three distributed over the outer circumference, in the otherwise circular cross-section of the Butzenlochs protruding lugs (11) to see.
- a circular slug (15) can be seen on the opposite second side of the single sheet.
- Fig. 2 is a section of a Butzen- or Butzenlochgargestation a follow-on composite tool for producing inventive single sheets with a recess (53) for forming a nose (11) providing embossing punch (50), a hold-down (55) and a male (56) to see ,
- the single sheet (1) lies above the bore (57) in the male part (56).
- the pressure of the descending stamping die (50) of the slug (15) and the slug hole (10) is embossed.
- the diameter of the bore (57) and thus the outer diameter of the slugs (15) is greater than the pitch circle diameter (54) of the lugs, but smaller than the foot diameter (12) of the Butzenlochs (10).
- the slugs (15) clamp on the lugs (11), which they plastically deform when pressed in the nerierstation the follow-on composite tool (not shown).
- the noses (11) can thereby flow into the gap, which results from the difference between the outer diameter of the Butzens and the base diameter (12) of the Butzenlochs (10).
- Fig. 3 schematically shows a laminated core, which consists of the stamping of the slugs (15) in the corresponding slug holes (10) interconnected individual sheets.
- Fig. 4 shows a section of a single sheet with embossed Butzenloch (10) and three evenly distributed over the hole circumference lugs (11) in plan view. Evident are the foot diameter (12) and pitch circle diameter (54).
- Fig. 5 is the corresponding die (50) of the follow-on composite tool with recesses (53) to see the formation of the noses.
- the invention is not limited to the embodiment with lugs (11) in the slotted hole (10).
- lugs (11) in the slotted hole (10).
- a Dahlberggeometrie in Butzenloch denkar instead of the noses a Dahlberggeometrie in Butzenloch denkar. It is also conceivable to attach the toothing on the outer diameter of the Butzens 15 and to equip the Butzenloch circular or also with a tooth geometry.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE200910051271 DE102009051271A1 (de) | 2009-10-29 | 2009-10-29 | Montagehilfe zum Stanzpaketieren |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP2320441A1 true EP2320441A1 (fr) | 2011-05-11 |
Family
ID=43769046
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP10188988A Withdrawn EP2320441A1 (fr) | 2009-10-29 | 2010-10-27 | Aide au montage pour paquets de tôles de découpe |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP2320441A1 (fr) |
| DE (1) | DE102009051271A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ITMI20120356A1 (it) * | 2012-03-07 | 2013-09-08 | Corrada Spa | Stampo di tranciatura con dispositivo di frenatura antigrippaggio |
| CN105689541A (zh) * | 2014-12-16 | 2016-06-22 | 铃木株式会社 | 机械连接用冲头、机械连接装置以及机械连接构件 |
| DE102015121951A1 (de) | 2015-12-16 | 2017-06-22 | Kiekert Ag | Verfahren zur Herstellung eines Kraftfahrzeugtürverschlusses |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102018107916A1 (de) * | 2018-04-04 | 2019-10-10 | Iav Gmbh Ingenieurgesellschaft Auto Und Verkehr | Verfahren und Vorrichtung zur Herstellung eines Elektrobleches einer elektrischen Maschine |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0133858A1 (fr) | 1983-08-12 | 1985-03-13 | Essa Fabrique de Machines S.A. | Procédé et dispositif pour fabriquer des paquets composés de lames de tôle pour des noyaux magnétiques de machines électriques |
| US4728842A (en) * | 1986-09-29 | 1988-03-01 | Carbet Corporation | Laminated assembly for a dynamoelectric machine and method for manufacturing laminated assemblies having ridges formed on projections which interlock with recesses of adjacent laminations |
| US4809429A (en) * | 1986-09-29 | 1989-03-07 | Carbet Corporation | Apparatus for manufacturing laminated assemblies having ridges formed on projections which interlock with recesses of adjacent laminations |
| US5230136A (en) * | 1992-05-04 | 1993-07-27 | Savair Inc. | Punch and die set for sheet metal clinching |
| WO1999016092A1 (fr) | 1997-09-19 | 1999-04-01 | Vacuumschmelze Gmbh | Procede et dispositif de fabrication de paquets formes de lames de toles pour noyaux magnetiques |
| WO2003041889A1 (fr) * | 2001-11-13 | 2003-05-22 | Empresa Brasileira De Compressores S/A - Embraco | Tole metallique, empilement de toles metalliques et procede d'assemblage |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2671951A (en) * | 1949-10-03 | 1954-03-16 | Jefferson Electric Co | Transformer core and method of making same |
| DE1021516B (de) * | 1956-04-28 | 1957-12-27 | Kloeckner Moeller Elektrizit | Verfahren zur Herstellung von Wechselstrommagnetkernen |
| US2975312A (en) * | 1958-03-07 | 1961-03-14 | Globe Union Inc | Laminated magneto components |
| GB2206453B (en) * | 1987-06-22 | 1992-01-02 | Linton & Hirst Ltd | Pack of laminations and forming projections and depressions |
-
2009
- 2009-10-29 DE DE200910051271 patent/DE102009051271A1/de not_active Withdrawn
-
2010
- 2010-10-27 EP EP10188988A patent/EP2320441A1/fr not_active Withdrawn
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0133858A1 (fr) | 1983-08-12 | 1985-03-13 | Essa Fabrique de Machines S.A. | Procédé et dispositif pour fabriquer des paquets composés de lames de tôle pour des noyaux magnétiques de machines électriques |
| US4728842A (en) * | 1986-09-29 | 1988-03-01 | Carbet Corporation | Laminated assembly for a dynamoelectric machine and method for manufacturing laminated assemblies having ridges formed on projections which interlock with recesses of adjacent laminations |
| US4809429A (en) * | 1986-09-29 | 1989-03-07 | Carbet Corporation | Apparatus for manufacturing laminated assemblies having ridges formed on projections which interlock with recesses of adjacent laminations |
| US5230136A (en) * | 1992-05-04 | 1993-07-27 | Savair Inc. | Punch and die set for sheet metal clinching |
| WO1999016092A1 (fr) | 1997-09-19 | 1999-04-01 | Vacuumschmelze Gmbh | Procede et dispositif de fabrication de paquets formes de lames de toles pour noyaux magnetiques |
| WO2003041889A1 (fr) * | 2001-11-13 | 2003-05-22 | Empresa Brasileira De Compressores S/A - Embraco | Tole metallique, empilement de toles metalliques et procede d'assemblage |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ITMI20120356A1 (it) * | 2012-03-07 | 2013-09-08 | Corrada Spa | Stampo di tranciatura con dispositivo di frenatura antigrippaggio |
| EP2636464A1 (fr) * | 2012-03-07 | 2013-09-11 | Corrada S.p.A | Ensemble de matrice de découpage avec dispositif de freinage anti-grippage |
| CN105689541A (zh) * | 2014-12-16 | 2016-06-22 | 铃木株式会社 | 机械连接用冲头、机械连接装置以及机械连接构件 |
| DE102015121951A1 (de) | 2015-12-16 | 2017-06-22 | Kiekert Ag | Verfahren zur Herstellung eines Kraftfahrzeugtürverschlusses |
Also Published As
| Publication number | Publication date |
|---|---|
| DE102009051271A1 (de) | 2011-05-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69211411T2 (de) | Vorrichtung und Verfahren um gestapelte Lamellen einer dynamo-elektrischen Maschine auszurichten | |
| EP1016105B1 (fr) | Procede et dispositif de fabrication de paquets formes de lames de toles pour noyaux magnetiques | |
| DE102014104084A1 (de) | System zur elastischen mittelnden Ausrichtung, Verfahren zum Herstellen desselben und Schneidstempel dafür | |
| DE112018006953T5 (de) | Vorrichtung zum Herstellen und Verfahren zum Herstellen eines geschichteten Eisenkerns | |
| EP3360144B1 (fr) | Procede et dispositif de liaison d'elements de tole a des paquets de toles | |
| GB2125321A (en) | Improvements in or relating to methods of manufacturing stacked lamination assemblies for armatures of electric machines | |
| DE112006000245T5 (de) | Stanzvorrichtung, Stanzverfahren und Stanzprodukt | |
| EP3736062A1 (fr) | Procédé d'assemblage par boutonnage d'éléments de tôle à des paquets de tôle | |
| EP0133858B1 (fr) | Procédé et dispositif pour fabriquer des paquets composés de lames de tôle pour des noyaux magnétiques de machines électriques | |
| DE102015211190A1 (de) | Verfahren zum Herstellen eines laminierten Eisenkerns | |
| DE102009051271A1 (de) | Montagehilfe zum Stanzpaketieren | |
| EP3741032B1 (fr) | Procédé d'assemblage d'éléments de tôle à des paquets de tôle | |
| WO2001076788A1 (fr) | Procede et outil permettant de produire des liaisons d"assemblage par pression | |
| EP3741033B1 (fr) | Procédé de liaison de parties en tôle à un empilage de tôles | |
| EP0325947A2 (fr) | Procédé et outil progressif pour pièces estampées | |
| EP4170875A1 (fr) | Procédé de fabrication d'au moins un canal de liquide dans un paquet de tôles et paquet de tôles ainsi fabriqué | |
| EP1775042B1 (fr) | Procédé et dispositif de poinçonnage d'une tôle | |
| DE102015208870A1 (de) | Verfahren zur Herstellung eines Blechpakets | |
| JP3948575B2 (ja) | 異形部材の製造方法 | |
| DE102015008171A1 (de) | Vorrichtung und Verfahren zum Bearbeiten eines Blechbauteils | |
| DE102020128367B4 (de) | Anordnung mit einem aus mindestens drei aufeinanderliegenden Blechlagen zusammengefügten Blechstapel, elektrischer Kontakt umfassend diese Anordnung und Verfahren zum Durchsetzfügen eines Blechstapels | |
| WO2024089268A1 (fr) | Procédé de liaison de pièces en tôle pour former au moins un empilement de tôles | |
| EP3898023A1 (fr) | Poinçonnage d'au moins deux tôles métalliques agencées l'une au-dessus de l'autre | |
| DE3016168C2 (de) | Gesamtverbundschneid- und Biegewerkzeug | |
| DE3203123A1 (de) | Verfahren zum herstellen eines lamellenpaketes fuer anker elektrischer maschinen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20111112 |