EP2390110A1 - Verfahren und System zur Bildung von Tesseraemosaikplatten - Google Patents
Verfahren und System zur Bildung von Tesseraemosaikplatten Download PDFInfo
- Publication number
- EP2390110A1 EP2390110A1 EP10163961A EP10163961A EP2390110A1 EP 2390110 A1 EP2390110 A1 EP 2390110A1 EP 10163961 A EP10163961 A EP 10163961A EP 10163961 A EP10163961 A EP 10163961A EP 2390110 A1 EP2390110 A1 EP 2390110A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- tesserae
- mosaic
- adhesive
- adhesive substrate
- sheets
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000000034 method Methods 0.000 title claims abstract description 28
- 230000008569 process Effects 0.000 title claims abstract description 21
- 230000015572 biosynthetic process Effects 0.000 title claims abstract description 12
- 230000000181 anti-adherent effect Effects 0.000 claims abstract description 29
- 239000000758 substrate Substances 0.000 claims abstract description 26
- 238000005304 joining Methods 0.000 claims abstract description 12
- 239000003292 glue Substances 0.000 claims abstract description 10
- 239000000853 adhesive Substances 0.000 claims description 35
- 230000001070 adhesive effect Effects 0.000 claims description 35
- 238000004806 packaging method and process Methods 0.000 claims description 6
- 238000011179 visual inspection Methods 0.000 claims description 5
- 230000000875 corresponding effect Effects 0.000 description 18
- 238000004026 adhesive bonding Methods 0.000 description 8
- 238000004140 cleaning Methods 0.000 description 3
- 238000000151 deposition Methods 0.000 description 3
- 239000012530 fluid Substances 0.000 description 3
- 238000012423 maintenance Methods 0.000 description 3
- 230000007306 turnover Effects 0.000 description 3
- 230000000007 visual effect Effects 0.000 description 3
- 230000007547 defect Effects 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 229920002635 polyurethane Polymers 0.000 description 2
- 239000004814 polyurethane Substances 0.000 description 2
- 230000009471 action Effects 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 230000002596 correlated effect Effects 0.000 description 1
- 230000002950 deficient Effects 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000008030 elimination Effects 0.000 description 1
- 238000003379 elimination reaction Methods 0.000 description 1
- 238000003780 insertion Methods 0.000 description 1
- 230000037431 insertion Effects 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000012795 verification Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C3/00—Processes, not specifically provided for elsewhere, for producing ornamental structures
- B44C3/12—Uniting ornamental elements to structures, e.g. mosaic plates
- B44C3/126—Devices for making mosaic constructs automatically
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C3/00—Processes, not specifically provided for elsewhere, for producing ornamental structures
- B44C3/12—Uniting ornamental elements to structures, e.g. mosaic plates
- B44C3/123—Mosaic constructs
Definitions
- the present invention relates to the formation of sheets of tesserae of mosaic designed to be laid for the decorative coating of mural structures, floors, pavements, and the like.
- Sheets of this sort normally have standardized dimensions, and the number of the tesserae of each sheet, arranged in orderly fashion to form a chequered pattern, is evidently correlated to their dimensions. For example, with square tesserae having side of 2 cm, each sheet, which is also square, may include typically 15 rows by 15 columns of tesserae.
- the tesserae of mosaic are initially located within the trays with the respective front decorative faces, i.e., the faces that in the condition where the sheets are laid will be in view, facing upwards to enable visual verification of the integrity thereof.
- the groups of tesserae of mosaic thus composed are turned over so as to position the base or back faces of the tesserae upwards.
- the joining adhesive is then applied from above on the back faces of the tesserae, normally using a mechanized dispenser that is equipped with nozzles for dosage of the adhesive and can be displaced according to paths corresponding to the rows and columns of tesserae.
- a flexible covering sheet of anti-adhesive material typically siliconed paper.
- the sheets of tesserae of mosaic are picked up from the corresponding trays and then transferred into packaging boxes.
- the adhesive applied from above while it is still hot and in the fluid state on the back faces of the tesserae can penetrate into the areas of intersection between contiguous tesserae and, particularly in the case of tesserae of small thickness, can become visible on their front faces with evident aesthetic drawbacks.
- a further drawback of this methodology lies in the difficulty of managing and checking the thickness of the adhesive applied from above and in particular the homogeneity of height in so far as, once deposited and exposed to the ambient atmosphere, the adhesive immediately starts to solidify. Notwithstanding the use of squeezing and levelling rollers, at the end of its application, stretches of adhesive having different contact times with the atmosphere will have different hardening times before being subjected to the action of the rollers, with consequent lack of uniformity.
- a second type of methodology which also envisages initial insertion of the tesserae into the containment trays with the corresponding front faces facing upwards.
- Each tray containing the tesserae can then be inspected visually to check the integrity of the corresponding front faces, and is then turned upside down so as to place the tesserae in a second tray in order to position the back faces thereof upwards.
- the next step is the operation of gluing, which envisages providing a sheet of paper rendered anti-adhesive and cut to size and positioning it on top of a device for dispensing the adhesive equipped with nozzles for delivering the adhesive from beneath upwards against the under face of the sheet of paper, also in this case according to a predetermined path.
- the sheet of paper is deposited against the back faces of the tesserae of mosaic positioned in the underlying containment tray, thus obtaining mutual joining thereof.
- the sheet is then pressed with a constant pressure against the back faces of tesserae so as to obtain a homogeneous thickness of the adhesive applied.
- a further drawback of this type of process lies in the impossibility of verifying visually that all the tesserae of mosaic adhere properly to the sheet of paper with the adhesive and, also in this case, that the front faces of the tesserae themselves remain intact at the end of the gluing step.
- An object of the present invention is to overcome the drawbacks of the current methodologies and more in particular to provide a process for formation of sheets of tesserae of mosaic, as well as a system for implementation of the process, which will enable the operation of turning over of the tesserae of mosaic prior to the gluing step to be avoided, eliminating both the need for resources and the problems that derive therefrom.
- Another object of the invention is to provide a process and a system for the formation of sheets of tesserae of mosaic that will enable a constant and efficient visual check of quality to be obtained before, during, and after the gluing step, thus ensuring the quality of the sheets of tesserae of mosaic formed and at the same time increasing efficiency and productivity by reducing or even eliminating the production of defective sheets.
- the above objects are achieved thanks to a process of the type defined in the preamble of Claim 1, the peculiar characteristic of which lies in the fact that the step of joining envisages application from above of the glue on an anti-adhesive substrate and positioning of the group of tesserae on the glue applied on said anti-adhesive substrate, keeping the front faces of the tesserae facing upwards so as to cause the glue to adhere to the back faces of the tesserae.
- the anti-adhesive substrate is constituted by a regenerable endless belt.
- the anti-adhesive substrate can be constituted by a discrete flexible plate.
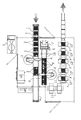
- the system is moreover provided with a series of visual-inspection stations, not illustrated in detail in so far as they are within the reach of the person skilled in the branch, typically constituted by video cameras operatively connected to a pre-programmed image-processing system for comparing the images detected with reference images and verifying the congruity thereof.
- the video cameras will be positioned in such a way as to film both the groups of tesserae of mosaic each time located in the corresponding containment trays 2 as they advance on the conveyor 1, and the area of application of the adhesive on the anti-adhesive substrate, constituted, as has been said, by the belt 6 or alternatively by the plates 10 each time positioned thereon, as well as the sheets F subsequently transferred to the packaging line 11.
- the tesserae of mosaic are, as has been said, positioned within the respective containment trays 2 in an orderly way to form a chequered pattern, with the corresponding front faces facing upwards. Then, whilst the trays 2 are transferred from the feeder 1 to the area where the manipulator robot 8 picks up the tesserae, the corresponding front faces are inspected by the video-camera system so as to verify not only the correct positioning thereof but also the absence of surface defects or anomalies.
- the gluing robot 3 proceeds to application of the fluid adhesive on the anti-adhesive substrate constituted by the surface of the regenerable belt 6 or, alternatively, by the plates 10 each time deposited thereon.
- the adhesive is applied by the dispenser robot 4 from above downwards and in a generally conventional way according to paths defining a grid - either continuous or in stretches - corresponding to the arrangement in rows and columns of the groups of tesserae within the corresponding containment trays 2.
- the manipulator robot 8 picks up, via the corresponding suction device 9, each group of tesserae 2 from the corresponding containment tray 2 on the feeder 1 and transfers it onto the grid of adhesive just applied on the anti-adhesive substrate.
- the group of tesserae is then deposited, in the same configuration in which it has been picked up, i.e., with the front faces of the tesserae facing upwards, on the grid of adhesive, thus obtaining joining therewith of the corresponding back faces.
- each sheet F thus formed is picked up from the belt 6 by the same manipulator robot 8 and then transferred to the packaging line 11 for being boxed.
- the tesserae of mosaic remain constantly oriented with the corresponding front decorative faces facing upwards. This enables the system of visual inspection to check constantly not only the presence and correct positioning of the tesserae but also the integrity and the absence of surface defects of said front faces, together with proper dispensing of the adhesive each time applied on the anti-adhesive substrate.
- each sheet F will be constituted only by the tesserae and by the grid of adhesive that joins the back faces thereof in the case where the anti-adhesive substrate is constituted by the surface of the regenerable belt 6, or else will include also the plate 10 in the alternative case where this is used for constituting the anti-adhesive substrate.
- an auxiliary anti-adhesive plate may then be inserted, with separating function, between each sheet F each time introduced into the box 12 along the packaging line 11 and the underlying sheet F.
Landscapes
- Lining Or Joining Of Plastics Or The Like (AREA)
- Folding Of Thin Sheet-Like Materials, Special Discharging Devices, And Others (AREA)
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP10163961A EP2390110A1 (de) | 2010-05-26 | 2010-05-26 | Verfahren und System zur Bildung von Tesseraemosaikplatten |
| EP11726193.3A EP2576241A1 (de) | 2010-05-26 | 2011-05-26 | Verfahren und system zur bildung von tesseraemosaik-blättern |
| PCT/IB2011/052302 WO2011148338A1 (en) | 2010-05-26 | 2011-05-26 | Process and system for the formation of sheets of tesserae of mosaic |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP10163961A EP2390110A1 (de) | 2010-05-26 | 2010-05-26 | Verfahren und System zur Bildung von Tesseraemosaikplatten |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP2390110A1 true EP2390110A1 (de) | 2011-11-30 |
Family
ID=42734064
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP10163961A Withdrawn EP2390110A1 (de) | 2010-05-26 | 2010-05-26 | Verfahren und System zur Bildung von Tesseraemosaikplatten |
| EP11726193.3A Withdrawn EP2576241A1 (de) | 2010-05-26 | 2011-05-26 | Verfahren und system zur bildung von tesseraemosaik-blättern |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP11726193.3A Withdrawn EP2576241A1 (de) | 2010-05-26 | 2011-05-26 | Verfahren und system zur bildung von tesseraemosaik-blättern |
Country Status (2)
| Country | Link |
|---|---|
| EP (2) | EP2390110A1 (de) |
| WO (1) | WO2011148338A1 (de) |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104527295A (zh) * | 2014-12-31 | 2015-04-22 | 佛山为尔电子科技有限公司 | 一种铺贴马赛克预设图案的方法及装置 |
| CN104786723A (zh) * | 2015-03-24 | 2015-07-22 | 辽宁省交通高等专科学校 | 一种马赛克自动拼装机 |
| CN105856943A (zh) * | 2016-04-15 | 2016-08-17 | 佛山博文机器人自动化科技有限公司 | 一种马赛克自动铺贴设备及铺贴方法 |
| CN107499048A (zh) * | 2017-09-29 | 2017-12-22 | 浙江卡莎罗新型装饰材料有限公司 | 一种玻璃马赛克自动铺贴装置 |
| IT201700025807A1 (it) * | 2017-03-08 | 2018-09-08 | Fabrizio Stefani | Procedimento per la realizzazione di mosaici |
| DE102019005505A1 (de) * | 2019-08-06 | 2021-02-11 | Lohmann Gmbh & Co. Kg | Verfahren zur Herstellung und Befestigung von Fliesen- oder Mosaiknetzen |
| CN113815294A (zh) * | 2021-09-23 | 2021-12-21 | 佛山市南海风靡建材有限公司 | 一种马赛克背网的铺贴线 |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106696580B (zh) * | 2016-12-01 | 2022-06-17 | 佛山科学技术学院 | 单色马赛克的对称分布式自动铺贴设备及其铺贴方法 |
| CN111038166A (zh) * | 2019-12-27 | 2020-04-21 | 珠海市白兔陶瓷有限公司 | 瓷砖铺贴线 |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4218496A (en) * | 1978-03-16 | 1980-08-19 | Savignac Manuel E | Natural stone panel and method of making same |
| IT1244110B (it) * | 1990-11-20 | 1994-07-05 | Bisazza Spa | Procedimento per la produzione di pannelli in tessere di mosaico |
| WO2005084822A1 (en) * | 2004-02-27 | 2005-09-15 | System S.P.A. | A device and process for depositing drops of adhesive material on a surface in a predetermined distribution pattern |
| WO2009150174A2 (en) * | 2008-06-11 | 2009-12-17 | Ergun Limited | Method and machine to make a modular covering panel and modular panel thus made |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE29708102U1 (de) * | 1997-05-05 | 1997-07-10 | Lutzke, Werner, 86316 Friedberg | Vorrichtung zum Auftragen von Klebstoff |
| ITMO20060197A1 (it) * | 2006-06-16 | 2007-12-17 | Kemac S P A | Iniettore per fluidi viscosi |
-
2010
- 2010-05-26 EP EP10163961A patent/EP2390110A1/de not_active Withdrawn
-
2011
- 2011-05-26 EP EP11726193.3A patent/EP2576241A1/de not_active Withdrawn
- 2011-05-26 WO PCT/IB2011/052302 patent/WO2011148338A1/en not_active Ceased
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4218496A (en) * | 1978-03-16 | 1980-08-19 | Savignac Manuel E | Natural stone panel and method of making same |
| IT1244110B (it) * | 1990-11-20 | 1994-07-05 | Bisazza Spa | Procedimento per la produzione di pannelli in tessere di mosaico |
| WO2005084822A1 (en) * | 2004-02-27 | 2005-09-15 | System S.P.A. | A device and process for depositing drops of adhesive material on a surface in a predetermined distribution pattern |
| WO2009150174A2 (en) * | 2008-06-11 | 2009-12-17 | Ergun Limited | Method and machine to make a modular covering panel and modular panel thus made |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104527295A (zh) * | 2014-12-31 | 2015-04-22 | 佛山为尔电子科技有限公司 | 一种铺贴马赛克预设图案的方法及装置 |
| CN104786723A (zh) * | 2015-03-24 | 2015-07-22 | 辽宁省交通高等专科学校 | 一种马赛克自动拼装机 |
| CN104786723B (zh) * | 2015-03-24 | 2017-11-28 | 辽宁省交通高等专科学校 | 一种马赛克自动拼装机 |
| CN105856943A (zh) * | 2016-04-15 | 2016-08-17 | 佛山博文机器人自动化科技有限公司 | 一种马赛克自动铺贴设备及铺贴方法 |
| IT201700025807A1 (it) * | 2017-03-08 | 2018-09-08 | Fabrizio Stefani | Procedimento per la realizzazione di mosaici |
| CN107499048A (zh) * | 2017-09-29 | 2017-12-22 | 浙江卡莎罗新型装饰材料有限公司 | 一种玻璃马赛克自动铺贴装置 |
| DE102019005505A1 (de) * | 2019-08-06 | 2021-02-11 | Lohmann Gmbh & Co. Kg | Verfahren zur Herstellung und Befestigung von Fliesen- oder Mosaiknetzen |
| DE102019005505B4 (de) | 2019-08-06 | 2022-08-11 | Lohmann Gmbh & Co. Kg | Verfahren zur Herstellung und Befestigung von Fliesen- oder Mosaiknetzen |
| CN113815294A (zh) * | 2021-09-23 | 2021-12-21 | 佛山市南海风靡建材有限公司 | 一种马赛克背网的铺贴线 |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2011148338A1 (en) | 2011-12-01 |
| EP2576241A1 (de) | 2013-04-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| WO2011148338A1 (en) | Process and system for the formation of sheets of tesserae of mosaic | |
| DK175952B1 (da) | Fremgangsmåde til sortering af belægningssten | |
| KR101749241B1 (ko) | 보호필름 부착장치 | |
| US11472139B2 (en) | Automated composite fabrication systems and methods | |
| EP1927068A2 (de) | Verfahren zum bestücken eines teppichs bwz. eines flächenförmigen trägers mit elektronischen bauteilen, vorrichtung hierzu, sowie teppich bzw. flächenförmiger träger mit elektronischen bauteilen | |
| US20130081360A1 (en) | Corner protector placement system and method and related pallet wrapping system and method | |
| US20080075907A1 (en) | Method for preparing tiles or sheets consisting of mosaic pieces and tiles obtained therewith | |
| DE1298653T1 (de) | Herstellungseinrichtung und herstellungsverfahren für optische platten | |
| US9744683B2 (en) | V groove insulation machine | |
| DE3338994A1 (de) | Plaettchen-befestigungsvorrichtung | |
| DE19500560A1 (de) | Verfahren zum Transportieren von Druckprodukten zwischen weiterverarbeitenden Buchbindemaschinen und Vorrichtung zur Durchführung des Verfahrens | |
| KR20200078931A (ko) | 물티슈 포장용기의 뚜껑 자동 부착장치 | |
| KR20180066326A (ko) | 물티슈 커버 부착 장치 및 방법 | |
| US20250002272A1 (en) | Device and method for producing solar modules | |
| JPH06312834A (ja) | タイル配列方法 | |
| KR101186122B1 (ko) | 보호필름 가박리 장치 | |
| JPH0340578Y2 (de) | ||
| CN100528560C (zh) | 用于制造感光层叠体的装置和方法 | |
| EP1586722B1 (de) | Verfahren zum Verbinden einzelner Keramikteile durch ein gemeinsames Substrat | |
| JPH10225908A (ja) | 単板積層材の製造装置 | |
| DE102010017497A1 (de) | Vorrichtung und Verfahren zum Be-und Entladen von Substratträgerarrays | |
| JP2773064B2 (ja) | タイル検査装置 | |
| JPS63152503A (ja) | 小袋包装された菓子をトレ−上に配列せしめる装置 | |
| JPH07132915A (ja) | 長尺物載置装置 | |
| KR100625841B1 (ko) | 반도체 포장용 튜브의 플러그 자동 삽입 장치 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME RS |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20120531 |