EP2542363B1 - Verfahren und vorrichtung zum ziehen und beschneiden von platinen - Google Patents
Verfahren und vorrichtung zum ziehen und beschneiden von platinen Download PDFInfo
- Publication number
- EP2542363B1 EP2542363B1 EP11707623.2A EP11707623A EP2542363B1 EP 2542363 B1 EP2542363 B1 EP 2542363B1 EP 11707623 A EP11707623 A EP 11707623A EP 2542363 B1 EP2542363 B1 EP 2542363B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cutting
- contour
- die
- cutting edge
- drawing punch
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000000034 method Methods 0.000 title claims description 23
- 238000009966 trimming Methods 0.000 title claims description 19
- 229910052751 metal Inorganic materials 0.000 title claims description 4
- 239000002184 metal Substances 0.000 title claims description 4
- 238000005520 cutting process Methods 0.000 claims description 145
- 229910000831 Steel Inorganic materials 0.000 claims description 5
- 239000010959 steel Substances 0.000 claims description 5
- 230000006835 compression Effects 0.000 claims description 2
- 238000007906 compression Methods 0.000 claims description 2
- 238000000926 separation method Methods 0.000 description 4
- 230000015572 biosynthetic process Effects 0.000 description 3
- 238000004519 manufacturing process Methods 0.000 description 3
- 239000000463 material Substances 0.000 description 2
- 238000007493 shaping process Methods 0.000 description 2
- 229910052782 aluminium Inorganic materials 0.000 description 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 239000011159 matrix material Substances 0.000 description 1
- 230000001617 migratory effect Effects 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D24/00—Special deep-drawing arrangements in, or in connection with, presses
- B21D24/16—Additional equipment in association with the tools, e.g. for shearing, for trimming
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D22/00—Shaping without cutting, by stamping, spinning, or deep-drawing
- B21D22/20—Deep-drawing
- B21D22/21—Deep-drawing without fixing the border of the blank
Definitions
- the invention relates to a device for drawing components from a metal circuit board with a drawing punch and a die, wherein the drawing punch has a cutting edge for trimming the board during the drawing process and in the die an inlet contour is provided. Moreover, the invention relates to a method for pulling a circuit board using the device according to the invention and to an inventive use of the method.
- the cutting edge of the drawing punch is simultaneously used to co-determine the contour of the drawn component and / or to compress the component, for example.
- An inclination of this cutting edge is therefore not possible in the rule.
- a reduction of the cutting forces without changing the contour of the drawn component is therefore not readily possible.
- the inlet contour is the area of the die, in which the actual mold cavity of the die merges into the frame.
- inlet contour the largest possible radius is provided to facilitate the drawing process, so that the material flow of the board does not have to be made over a narrow radius.
- the object of the invention is to provide a device and a method with which the cutting forces during integrated drawing and trimming can be reduced without influencing the contour of the component.
- the present invention has the object to provide a corresponding manufacturing method available.
- the above-described object is achieved in a generic device in that the inlet contour of the die is formed such that the cutting edge and the inlet contour in the Ziehstkovposition are only partially in cutting engagement at the beginning of the cutting process along the cutting line.
- the inlet contour of the die which serves to facilitate the drawing process, is usually formed as a larger radius, which is usually formed identically along the cutting line, to facilitate the pulling uniformly along the entire Einlaufrundung.
- the cutting engagement of the cutting edge takes place simultaneously along the entire cutting line.
- the inlet contour according to the invention is designed such that the cutting edge of the drawing punch at the beginning of the cutting process only a partial cutting engagement of the cutting edge generated so that not the entire cutting line is simultaneously in cutting engagement on the cutting edge.
- the minimum requirement for a clean trim of the board is that the infeed contour of the die provides the cutting engagement at at least one point relative to the die position in which the cutting operation begins.
- the inlet contour can ensure this, for example, by using different radii along the cutting line, so that at different positions along the cutting line, the inlet contour at different heights relative to the bottom of the die already has the final shape of the die and thus allows the cutting engagement only in areas or points , Due to the resulting, along the cutting line migratory cutting engagement, the cutting forces and wear of the device, in particular the cutting edge are significantly reduced.
- the device is designed for pulling steel blanks.
- specific steel grades must be provided on the cutting edge and / or the dimensions of the die and the drawing punch to be adapted to the flow behavior of the material to be formed.
- the cutting edge of the drawing punch is formed at the same time for forming the finished contour of the component and optionally extends in a plane perpendicular to the pulling movement of the drawing punch.
- the finished contour of the component is also compressed by the cutting edge of the drawing punch. Since, according to the invention, the formation of the cutting edge can be shaped almost independently of the cutting engagement to be realized, it can be adapted without problems to the respective component geometry and used for shaping the drawn component, in particular the end face of the frames of a drawn component. This is achieved in that the inlet contour of the die ensures the function of the wandering cutting engagement of the cutting edge.
- a particularly simple cutting edge can then be provided by the cutting edge running perpendicular to the pulling movement of the drawing punch in a plane.
- this also results in a flat component in the region of the shaping of the cutting edge or the end faces of the frames of the component.
- a uniform cutting process ensures a further advantageous embodiment of the device according to the invention characterized in that the inlet contour along the cutting line is formed varying.
- "Varying" in the sense of the present Invention means that the cutting process, as the position of the drawing punch changes, moves along the cutting line after the start of the cutting operation until the complete separation from the trimming is achieved.
- the inlet contour in the direction of the cutting line is step-shaped, so that in each case regions of the cutting line are in cutting engagement simultaneously with the cutting edge and simultaneously separated.
- the cutting engagement can take place simultaneously at different points on the cutting line and a continuous trimming at several points of the cutting line take place simultaneously.
- the inlet contour Due to the shape of the inlet contour, it has at least one point along the cutting line in which the cutting process begins, i. at which the inlet contour with respect to the drawing punch position first passes into the matrix form.
- the trimming of the board continues continuously in the direction of the lowest point of the inlet contour.
- the cutting edge of the drawing punch simultaneously engages the drawn board at several points and begins the cutting process.
- the cutting angle between the cutting edge and the inlet contour can be 1 ° to 5 ° to achieve good cutting results.
- the above object is achieved procedurally using the device according to the invention in that the cutting edge of the drawing die and the inlet contour of the die in the drawing punch position at the beginning of the cutting along the cutting line only partially and at least at one point of the cutting line are in cutting engagement and the board is continuously cut by the movement of the drawing die into the die starting from the cutting engagement point or the cutting engagement points along the cutting line.
- the method according to the invention not only achieves a clean trimming of the board during the drawing process, but also effectively reduces the cutting forces, so that the wear on the cutting edge is reduced and the cutting process is clearly harmonized. Overall, an improved method is available which is suitable for drawing and simultaneously trimming high numbers of boards.
- the inventive method can be further improved by the fact that the cutting edge of the drawing punch forms the contour of the component in the region of the cutting edge when reaching its end position and / or performs a compression of the component.
- the design of the cutting edge can be designed so that the contour of the component in the region of the cutting edge, for example in a cup-like component, the front edge of the frame of the component is formed, regardless of the realization of a continuation of the trimming during the drawing process.
- the end faces of the frames of the drawn component are flat and formed in a plane in order to ensure a connection possibility of the component over the end faces of the frames.
- the use of the method according to the invention is advantageous for the production of drawn steel components for motor vehicles. Regularly high volumes are required at low cost but high quality in motor vehicle parts.
- the use of the method according to the invention for the production of components for motor vehicles not only in one step components with high quality, but due to the reduced wear of the device according to the invention also allow high volumes of these components.
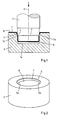
- a first embodiment of the device according to the invention shows Fig. 1 in a schematic sectional view.
- the device comprises a drawing punch 2, which pulls the board 1 using the die 3 to an example cup-like component and simultaneously cuts.
- the cutting edge 4 of the drawing punch 2 causes during the drawing process on the one hand, that for the board 1 from a certain drawing position of the drawing punch 2 in the die 3, the cutting process begins.
- the inlet contour 5 is designed so that it has an eccentricity with respect to the axis of symmetry 6 of the drawing punch 2 and thus also with respect to the axis of symmetry of the contour of the die 3.
- the cutting line 7, which marks the cutting engagement between cutting edge and inlet contour of the die, has a height profile.
- the cutting engagement of the cutting edge 4 initially takes place at a point of the drawing punch 2 at point 7a, since here the inlet contour merges into the final contour 8 of the die 3 even at a low drawing depth. If the drawing punch 2 is moved further in the direction of the die 3, the cutting edge 4 of the drawing punch 2 continuously cuts the drawn blank 1 starting from the cutting line point 7a until the cut at point 7b has completely separated the drawn part of the blank 1a from the cut 1b. This ensures that the cutting process during the drawing is introduced only partially and at least at one point 7a. Trimming the board while it is being pulled does not require high forces anymore, because not the complete cutting line in the cutting engagement of the cutting edge 4 and the die 3 is.
- the complete separation of the drawn part of the board 1a and the trimming 1b must have taken place at the latest when the drawing punch 2 has reached its end position.
- the trimming is carried out before reaching the end position of the drawing punch 2, in order to form over the cutting edge 4, the end faces of the frames of the finished component and optionally to compress.
- the formation of the die of the embodiment Fig. 1 shows in a perspective view the Fig. 2 ,
- the die 3 has an inlet contour 5, which merges with respect to the pulling direction at different heights in the final contour 8 of the die 3.
- these points are labeled 5a and 5b.
- the inlet contour 5 of the die for example, already at a lower depth of draw of the drawing punch 2 in the final contour 8 of the die 3, so that the cutting engagement between the cutting edge 4 and board 1 is already at a lower draw depth.
- the cut then continues from point 5a until it reaches the cutting point 5b circumferentially in both directions.
- the inlet contour 5 of the die 3 finally merges into the final contour 8 of the die, so that the cutting engagement between the cutting edge and the board takes place last.
- the cutting edge can be formed in a straight line due to the formation of the inlet contour 5 of the die 3 and yet a continuous cutting process is possible, which requires only low cutting forces.
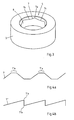
- FIG. 3 Now another embodiment of the die 3 is shown in a perspective view.
- the inlet contour 5 is formed along the cutting line 7 with a tooth-like height profile, so that the cutting line at the cutting point 7a marks the beginning of the cutting engagement between the cutting edge and the circuit board.
- the trimming of the board therefore begins at point 7a and continues on further displacement of the position of the drawing punch in the die to the lowest point of the cutting line 7b.
- the cutting engagement takes place simultaneously in the board at several points of the cutting line 7.
- the trimming then continues from these points of the cutting line 7a to the lower points of the cutting line 7b, 7c, as the drawing punch moves deeper into the die 3 becomes.
- the board is thus partially and simultaneously at several points in cutting engagement with the cutting edge of the drawing punch and cut continuously when relocating the drawing punch into the die into it.
- Fig. 4a and Fig. 4b Profiles of the inlet contour, which represent the height profile of the transition of the inlet contour in the final contour of the die.
- the cutting lines 7 'and 7 "of Fig. 4a) and 4b ) indicate the height profile of the inlet contour 5 of the die 3.
- the cutting line 7 ' shows that regions 7'a initiate the cutting process in regions when the drawing punch is immersed.
- the cutting line 7 "again shows a tooth-like course, wherein the cutting engagement in each case takes place at the highest points 7" a and then continues to the lowest point 7 "b.
- Fig. 4a ) and b) are exemplary embodiments of the inlet contour of the die 3 a Device according to the invention.
- the inlet contour may also be wave-like, for example sinusoidal or have other height gradients.
- the invention is not limited to the cup-shaped, flangeless component shown, but is also applicable to deep-drawn parts of any kind and shape, especially on flanged components.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Shaping Metal By Deep-Drawing, Or The Like (AREA)
- Punching Or Piercing (AREA)
Description
- Die Erfindung betrifft eine Vorrichtung zum Ziehen von Bauteilen aus einer Platine aus Metall mit einem Ziehstempel und einer Matrize, wobei der Ziehstempel eine Schneidkante zum Beschneiden der Platine während des Ziehvorganges aufweist und in der Matrize eine Einlaufkontur vorgesehen ist. Darüber hinaus betrifft die Erfindung ein Verfahren zum Ziehen einer Platine unter Verwendung der erfindungsgemäßen Vorrichtung sowie eine erfindungsgemäße Verwendung des Verfahrens.
- Es ist bekannt, Platinen aus einem Metall, insbesondere Stahl oder Aluminium zu ziehen und während des Ziehvorgangs gleichzeitig ein Besäumen bzw. Beschneiden des gezogenen Teils durchzuführen. So ist beispielsweise aus der gattungsgemäßen japanischen Patentanmeldung
JP 01034525 - Ferner ist bekannt, die Matrize einer Vorrichtung zum Ziehen von Platinen mit einer Einlaufkontur zu versehen. Die Einlaufkontur ist der Bereich der Matrize, in welchem die eigentliche Formvertiefung der Matrize in die Zarge übergeht. Als Einlaufkontur wird zur Erleichterung des Ziehvorganges ein möglichst großer Radius vorgesehen, so dass der Materialfluss der Platine nicht über einen engen Radius erfolgen muss.
- Hiervon ausgehend liegt der Erfindung die Aufgabe zugrunde, eine Vorrichtung und ein Verfahren zur Verfügung zu stellen, mit welchem die Schneidkräfte beim integrierten Ziehen und Beschneiden verringert werden können, ohne die Kontur des Bauteils zu beeinflussen. Darüber hinaus liegt der vorliegenden Erfindung die Aufgabe zugrunde, ein entsprechendes Herstellverfahren zur Verfügung zu stellen.
- Gemäß einer ersten Lehre der vorliegenden Erfindung wird die oben aufgezeigte Aufgabe bei einer gattungsgemäßen Vorrichtung dadurch gelöst, dass die Einlaufkontur der Matrize derart ausgebildet ist, dass die Schneidkante und die Einlaufkontur in der Ziehstempelposition zu Beginn des Schneidvorgangs entlang der Schneidlinie nur bereichsweise im Schneideingriff stehen.
- Die Einlaufkontur der Matrize, welche dazu dient, den Ziehvorgang zu erleichtern, ist in der Regel als größerer Radius ausgebildet, welcher üblicherweise entlang der Schneidlinie identisch ausgebildet ist, um das Ziehen entlang der gesamten Einlaufrundung gleichmäßig zu erleichtern. Bei dieser Ausprägung der Einlaufkontur findet der Schneideingriff der Schneidkante entlang der gesamten Schneidlinie gleichzeitig statt. Demgegenüber ist die erfindungsgemäße Einlaufkontur derart ausgebildet, dass die Schneidkante des Ziehstempels zu Beginn des Schneidprozesses nur einen bereichsweisen Schneideingriff der Schneidkante erzeugt, so dass nicht die gesamte Schneidlinie gleichzeitig über die Schneidkante im Schneideingriff steht. Die Minimalvoraussetzung für einen sauberen Beschnitt der Platine besteht darin, dass die Einlaufkontur der Matrize den Schneideingriff, bezogen auf die Ziehstempelposition in der der Schneidvorgang beginnt, an mindestens einem Punkt bereitstellt. Von diesem Punkt ausgehend wandert der Schneideingriff der Schneidkante bei weiterer Abwärtsbewegung entlang der Schneidlinie bis es zur vollständigen Trennung der gezogenen Platine von dem Beschnitt kommt. Die Einlaufkontur kann dies beispielsweise durch die Verwendung unterschiedlicher Radien entlang der Schneidlinie gewährleisten, so dass an verschiedenen Positionen entlang der Schneidlinie die Einlaufkontur in unterschiedlichen Höhen relativ zum Boden der Matrize bereits die endgültige Form der Matrize aufweist und so den Schneideingriff nur bereichs- oder punktweise zulässt. Durch den daraus resultierenden, entlang der Schneidlinie wandernden Schneideingriff werden die Schneidkräfte und auch der Verschleiß der Vorrichtung, insbesondere der Schneidkante deutlich verringert.
- Bevorzugt ist die Vorrichtung zum Ziehen von Platinen aus Stahl ausgelegt. Hierzu müssen beispielsweise spezifische Stahlgüten an der Schneidkante vorgesehen und/oder die Abmessungen der Matrize und des Ziehstempels auf das Fließverhalten des umzuformenden Werkstoffs angepasst werden.
- Gemäß einer ersten vorteilhaften Ausgestaltung der erfindungsgemäßen Vorrichtung ist die Schneidkante des Ziehstempels gleichzeitig zur Formung der Fertigkontur des Bauteils ausgebildet und verläuft optional in einer Ebene senkrecht zur Ziehbewegung des Ziehstempels. Gegebenenfalls wird die Fertigkontur des Bauteils auch durch die Schneidkante des Ziehstempels gestaucht. Da erfindungsgemäß die Ausbildung der Schneidkante nahezu unabhängig von dem zu realisierenden Schneideingriff geformt werden kann, kann diese ohne Probleme an die jeweilige Bauteilgeometrie angepasst werden und zur Formgebung des gezogenen Bauteils, insbesondere der Stirnfläche der Zargen eines gezogenen Bauteils genutzt werden. Dies wird dadurch erreicht, dass die Einlaufkontur der Matrize die Funktion des wandernden Schneideingriffs der Schneidkante gewährleistet. Eine besonders einfache Schneidkante kann dann dadurch bereitgestellt werden, dass die Schneidkante senkrecht zur Ziehbewegung des Ziehstempels in einer Ebene verläuft. Beim Ausformen des gezogenen Bauteils ergibt sich dadurch ebenfalls ein ebenes Bauteil im Bereich der Formgebung der Schneidkante bzw. der Stirnflächen der Zargen des Bauteils.
- Einen gleichmäßigen Schneidvorgang gewährleistet eine weitere vorteilhafte Ausführungsform der erfindungsgemäßen Vorrichtung dadurch, dass die Einlaufkontur entlang der Schneidelinie variierend ausgebildet ist. "Variierend" im Sinne der vorliegenden Erfindung bedeutet, dass der Schneidvorgang bei Veränderung der Position des Ziehstempels nach dem Beginn des Schneidvorgangs entlang der Schneidlinie wandert, bis die vollständige Trennung vom Beschnitt erreicht wird. Gemäß einer weiteren vorteilhafte Ausführungsform ist die Einlaufkontur in Richtung der Schneidlinie stufenförmig ausgebildet, so dass jeweils Bereiche der Schneidlinie simultan mit der Schneidkante im Schneideingriff stehen und gleichzeitig abgetrennt werden.
- Weist die Einlaufkontur gemäß einer weiteren bevorzugte Ausführungsform der erfindungsgemäßen Vorrichtung einen zahnartigen oder wellenartigen Verlauf entlang der Schneidlinie auf, kann der Schneideingriff gleichzeitig an verschiedenen Punkten der Schneidlinie erfolgen und ein fortlaufender Beschnitt an mehreren Stellen der Schneidlinie gleichzeitig erfolgen.
- Aufgrund der Form der Einlaufkontur weist diese entlang der Schneidlinie mindestens einen Punkt auf, in welchem der Schneidvorgang beginnt, d.h. an welchem die Einlaufkontur bezogen auf die Ziehstempelposition zuerst in die Matrizenform übergeht.
- Von dieser Position aus setzt sich der Beschnitt der Platine fortlaufend in Richtung tiefster Stelle der Einlaufkontur fort. Bei einem Mehrfacheingriff greift die Schneidkante des Ziehstempels gleichzeitig an mehreren Punkten in die gezogene Platine ein und beginnt den Schneidvorgang.
- Der Schneidwinkel zwischen Schneidkante und der Einlaufkontur kann 1° bis 5° betragen, um gute Schnittergebnisse zu erzielen.
- Gemäß einer zweiten Lehre der vorliegenden Erfindung wird die oben aufgezeigte Aufgabe verfahrensmäßig unter Verwendung der erfindungsgemäßen Vorrichtung dadurch gelöst, dass die Schneidkante des Ziehstempels und die Einlaufkontur der Matrize in der Ziehstempelposition zu Beginn des Schneidvorgangs entlang der Schneidlinie nur bereichsweise und mindestens an einem Punkt der Schneidlinie im Schneideingriff stehen und die Platine durch die Bewegung des Ziehstempels in die Matrize ausgehend von dem Schneideingriffspunkt oder den Schneideingriffspunkten entlang der Schneidlinie fortlaufend geschnitten wird.
- Wie bereits zuvor ausgeführt, wird durch das erfindungsgemäße Verfahren nicht nur ein sauberer Beschnitt der Platine während des Ziehvorgangs erreicht, sondern es werden auch effektiv die Schneidkräfte gesenkt, so dass der Verschleiß an der Schneidkante verringert und der Schneidvorgang deutlich harmonisiert wird. Insgesamt steht ein verbessertes Verfahren zur Verfügung, welches für das Ziehen und gleichzeitige Beschneiden hoher Stückzahlen an Platinen geeignet ist.
- Das erfindungsgemäße Verfahren kann dadurch weiterverbessert werden, dass die Schneidkante des Ziehstempels bei Erreichen dessen Endposition die Kontur des Bauteils im Bereich der Schnittkante ausformt und/oder eine Stauchung des Bauteils durchführt. Da bereits mit der Einlaufkontur der Matrize die unterschiedlichen Schneideingriffspunkte festgelegt werden, kann die Ausbildung der Schneidkante darauf ausgelegt werden, dass die Kontur des Bauteils im Bereich der Schnittkante, beispielsweise bei einem napfartigen Bauteil die Stirnkante der Zargen des Bauteils, ausgeformt wird und zwar unabhängig von der Realisierung eines Fortlaufens des Beschnittes während des Ziehvorgangs. Vorzugsweise werden die Stirnflächen der Zargen des gezogenen Bauteils flach und in einer Ebene geformt, um eine Anbindungsmöglichkeit des Bauteils über die Stirnflächen der Zargen zu gewährleisten.
- Schließlich ist die Verwendung des erfindungsgemäßen Verfahrens vorteilhaft für die Herstellung von gezogenen Bauteilen aus Stahl für Kraftfahrzeuge. Regelmäßig werden bei Kraftfahrzeugteilen hohe Stückzahlen mit geringen Kosten aber hoher Qualität gefordert. Die Verwendung des erfindungsgemäßen Verfahrens zur Herstellung von Bauteilen für Kraftfahrzeuge kann nicht nur in einem Arbeitsschritt Bauteile mit hoher Qualität, sondern aufgrund des verringerten Verschleißes der erfindungsgemäßen Vorrichtung auch hohe Stückzahlen dieser Bauteile ermöglichen.
- Im Weiteren soll die Erfindung anhand einer Zeichnung in Verbindung mit Ausführungsbeispielen näher erläutert werden. Die Zeichnung zeigt in
- Fig. 1
- eine Schnittansicht eines ersten Ausführungsbeispiels einer erfindungsgemäßen Vorrichtung,
- Fig. 2
- in einer perspektivischen Darstellung die Matrize gemäß dem ersten Ausführungsbeispiel,
- Fig. 3
- in einer perspektivischen Darstellung eines zweiten Ausführungsbeispiels und
- Fig. 4a), b)
- eine schematische Darstellung des Verlaufs der Einlaufkontur zweier weiterer Ausführungsbeispiele entlang der Schneidlinie einer Matrize.
- Ein erstes Ausführungsbeispiel der erfindungsgemäßen Vorrichtung zeigt
Fig. 1 in einer schematischen Schnittansicht. Die Vorrichtung umfasst einen Ziehstempel 2, welcher die Platine 1 unter Verwendung der Matrize 3 zu einem beispielsweise napfartigen Bauteil zieht und gleichzeitig beschneidet. Die Schneidkante 4 des Ziehstempels 2 bewirkt während des Ziehvorgangs einerseits, dass für die Platine 1 ab einer gewissen Ziehposition des Ziehstempels 2 in der Matrize 3 der Schneidvorgang beginnt. Die Einlaufkontur 5 ist dabei so ausgebildet, dass sie in Bezug auf die Symmetrieachse 6 des Ziehstempels 2 und damit auch in Bezug auf die Symmetrieachse der Kontur der Matrize 3 eine Exzentrizität aufweist. Die Schneidlinie 7, welche den Schneideingriff zwischen Schneidkante und Einlaufkontur der Matrize markiert, weist einen Höhenverlauf auf. In dem vorliegenden Ausführungsbeispiel findet der Schneideingriff der Schneidkante 4 ab einer Position des Ziehstempels 2 zunächst im Punkt 7a statt, da hier die Einlaufkontur bereits bei geringerer Ziehtiefe in die Endkontur 8 der Matrize 3 übergeht. Wird der Ziehstempel 2 weiter in Richtung Matrize 3 bewegt, schneidet die Schneidkante 4 des Ziehstempels 2 beginnend vom Schneidlinienpunkt 7a die gezogene Platine 1 fortlaufend, bis der Schnitt am Punkt 7b die vollständige Trennung des gezogenen Teils der Platine 1a vom Beschnitt 1b vollzogen hat. Dies gewährleistet, dass der Schneidvorgang während des Ziehens lediglich bereichsweise und mindestens an einem Punkt 7a eingeleitet wird. Das Beschneiden der Platine während des Ziehens erfordert dann keine hohen Kräfte mehr, da nicht die vollständige Schneidlinie im Schneideingriff der Schneidkante 4 und der Matrize 3 steht. - Die vollständige Trennung von dem gezogenen Teil der Platine 1a und dem Beschnitt 1b muss spätestens dann erfolgt sein, wenn der Ziehstempel 2 seine Endposition erreicht hat. Vorzugsweise wird der Beschnitt aber vor Erreichen der Endposition des Ziehstempels 2 durchgeführt, um über die Schneidkante 4 die Stirnflächen der Zargen des fertigen Bauteils auszuformen und gegebenenfalls zu stauchen.
- Die Ausbildung der Matrize des Ausführungsbeispiels aus
Fig. 1 zeigt in einer perspektivischen Darstellung dieFig. 2 . Die Matrize 3 weist eine Einlaufkontur 5 auf, welche in Bezug auf die Ziehrichtung in unterschiedlichen Höhen in die Endkontur 8 der Matrize 3 übergeht. In derFig. 2 sind diese Punkte mit 5a und 5b gekennzeichnet. Im Punkt 5a geht die Einlaufkontur 5 der Matrize 3 beispielsweise bereits bei geringerer Ziehtiefe des Ziehstempels 2 in die Endkontur 8 der Matrize 3 über, so dass der Schneideingriff zwischen Schneidkante 4 und Platine 1 bereits bei geringerer Ziehtiefe erfolgt. Der Schnitt setzt sich dann vom Punkt 5a fort, bis er umlaufend in beide Richtungen den Schneidpunkt 5b erreicht. Am Punkt 5b der Schneidlinie geht die Einlaufkontur 5 der Matrize 3 zuletzt in die Endkontur 8 der Matrize über, so dass hier der Schneideingriff zwischen Schneidkante und Platine zuletzt erfolgt. Die Schneidkante kann aufgrund der Ausbildung der Einlaufkontur 5 der Matrize 3 geradlinig ausgebildet sein und dennoch wird ein fortlaufender Schneidvorgang ermöglicht, der nur geringe Schneidkräfte erfordert. - In
Fig. 3 ist nun ein weiteres Ausführungsbeispiel der Matrize 3 in einer perspektivischen Ansicht dargestellt. Die Einlaufkontur 5 ist entlang der Schneidlinie 7 mit einem zahnartigen Höhenprofil ausgebildet, so dass die Schneidlinie am Schneidpunkt 7a den Beginn des Schneideingriffs zwischen Schneidkante und Platine markiert. Das Beschneiden der Platine beginnt daher am Punkt 7a und setzt sich bei weiterer Verlagerung der Position des Ziehstempels in die Matrize zum tiefsten Punkt der Schneidlinie 7b. Wie an dem Beispiel ausFig. 3 zu erkennen ist, erfolgt der Schneideingriff in die Platine gleichzeitig an mehreren Punkten der Schneidlinie 7. Der Beschnitt setzt sich dann von diesen Punkten der Schneidlinie 7a zu den tiefer gelegenen Punkten der Schneidlinie 7b, 7c fort, wenn der Ziehstempel tiefer in die Matrize 3 bewegt wird. Die Platine wird also bereichsweise und gleichzeitig an mehreren Punkten im Schneideingriff mit der Schneidkante des Ziehstempels stehen und fortlaufend bei Verlagerung des Ziehstempels in die Matrize hinein beschnitten. - Schematisch zeigen
Fig. 4a) und Fig. 4b ) Profile der Einlaufkontur, welche den Höhenverlauf des Übergangs der Einlaufkontur in die Endkontur der Matrize darstellen. Die Schneidlinien 7' und 7" derFig. 4a) und 4b ) zeigen den Höhenverlauf der Einlaufkontur 5 der Matrize 3 an. Die Schneidlinie 7' zeigt, dass Bereiche 7'a beim Eintauchen des Ziehstempels den Schneidvorgang bereichsweise einleiten. Die Schneidlinie 7" zeigt wiederum einen zahnartigen Verlauf, wobei der Schneideingriff jeweils an den höchsten Punkten 7"a erfolgt und sich dann bis zum tiefsten Punkt 7"b fortsetzt.Fig. 4a ) und b) sind erfindungsgemäße Ausführungsbeispiele der Einlaufkontur der Matrize 3 einer erfindungsgemäßen Vorrichtung. Selbstverständlich kann die Einlaufkontur auch wellenartig beispielsweise sinusförmig sein oder andere Höhenverläufe aufweisen. - Die Erfindung ist nicht auf das gezeigte napfförmige, flanschlose Bauteil beschränkt, sondern ist auch auf Tiefziehteile jeglicher Art und Form, insbesondere auf flanschbehaftete Bauteile anwendbar.
Claims (7)
- Vorrichtung zum Ziehen von Bauteilen aus einer Platine (1) aus Metall mit einem Ziehstempel (2) und einer Matrize (3), wobei der Ziehstempel (2) eine Schneidkante (4) zum Beschneiden der Platine (1) während des Ziehvorganges aufweist und in der Matrize (3) eine Einlaufkontur (5) vorgesehen ist,
dadurch gekennzeichnet, dass
die Einlaufkontur (5) der Matrize (3) derart ausgebildet ist, dass die Schneidkante (4) und die Einlaufkontur (5) in der Ziehstempelposition zu Beginn des Schneidvorgangs entlang der Schneidlinie (7) nur bereichsweise im Schneideingriff stehen. - Vorrichtung nach Anspruch 1,
dadurch gekennzeichnet, dass
die Schneidkante (4) des Ziehstempels (2) gleichzeitig zur Formung und/oder Stauchung der Fertigkontur des Bauteils ausgebildet ist und optional in einer Ebene senkrecht zur Ziehbewegung des Ziehstempels (2) verläuft. - Vorrichtung nach Anspruch 1 oder 2,
dadurch gekennzeichnet, dass
die Einlaufkontur (5) entlang der Schneidelinie (7) variierend oder stufenförmig ausgebildet ist. - Vorrichtung nach einem der Ansprüche 1 bis 3,
dadurch gekennzeichnet, dass
die Einlaufkontur (5) entlang der Schneidlinie (7) einen zahnartigen oder wellenartigen Verlauf aufweist. - Verfahren zum Ziehen von Bauteilen aus einer Platine (1) unter Verwendung einer Vorrichtung nach einem der Ansprüche 1 bis 4 mit einem Ziehstempel (2) mit Schneidkante (4) und einer Matrize (3) mit Einlaufkontur (5),
dadurch gekennzeichnet, dass
die Schneidkante (4) des Ziehstempels (2) und die Einlaufkontur (5) der Matrize (3) in der Ziehstempelposition zu Beginn des Schneidvorgangs entlang der Schneidlinie (7) nur bereichsweise und mindestens an einem Punkt der Schneidlinie (7) im Schneideingriff stehen und die Platine (1) durch die Bewegung des Ziehstempels (2) in die Matrize (3) ausgehend von dem Schneideingriffspunkt oder den Schneideingriffspunkten entlang der Schneidelinie (7) fortlaufend geschnitten wird. - Verfahren nach Anspruch 5,
dadurch gekennzeichnet, dass
die Schneidkante (4) des Ziehstempels (2) bei Erreichen dessen Endposition die Kontur des Bauteils im Bereich der Schnittkante ausformt und/oder eine Stauchung der Fertigkontur des Bauteils durchführt. - Verwendung eines Verfahrens nach einem der Ansprüche 5 oder 6 zur Herstellung von Bauteilen für Kraftfahrzeuge aus Stahl.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102010000608A DE102010000608B3 (de) | 2010-03-02 | 2010-03-02 | Verfahren und Vorrichtung zum Ziehen und Beschneiden von Platinen |
| PCT/EP2011/052880 WO2011107414A2 (de) | 2010-03-02 | 2011-02-28 | Verfahren und vorrichtung zum ziehen und beschneiden von platinen |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2542363A2 EP2542363A2 (de) | 2013-01-09 |
| EP2542363B1 true EP2542363B1 (de) | 2014-01-08 |
Family
ID=43525429
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP11707623.2A Not-in-force EP2542363B1 (de) | 2010-03-02 | 2011-02-28 | Verfahren und vorrichtung zum ziehen und beschneiden von platinen |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US9669447B2 (de) |
| EP (1) | EP2542363B1 (de) |
| JP (1) | JP5801825B2 (de) |
| DE (1) | DE102010000608B3 (de) |
| WO (1) | WO2011107414A2 (de) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102011050002A1 (de) * | 2011-04-29 | 2012-10-31 | Thyssenkrupp Steel Europe Ag | Verfahren und Vorrichtung zur Herstellung flanschbehafteter Ziehteile mit gleichzeitigem Beschnitt |
| DE102011050001A1 (de) * | 2011-04-29 | 2012-10-31 | Thyssenkrupp Steel Europe Ag | Verfahren und Vorrichtung zur Herstellung von flanschlosen Ziehteilen |
| DE102012100230B4 (de) | 2012-01-12 | 2017-10-19 | Thyssenkrupp Steel Europe Ag | Vorrichtung und Verfahren zur Herstellung von Schalenteilen |
| EP2857004B1 (de) | 2013-10-07 | 2018-07-04 | The Procter and Gamble Company | Haarglättungsverfahren mit reduzierenden Zuckern |
| GB2551514B (en) * | 2016-06-20 | 2019-09-18 | Crown Packaging Technology Inc | A method of manufacturing a metal cup using a draw die having a variable transition surface |
| KR102473320B1 (ko) * | 2022-05-09 | 2022-12-02 | 디에스 (주) | 스크랩 배출방법 및 이를 구현한 플랜지 절단장치 |
| CA3253940A1 (en) | 2022-06-30 | 2024-01-04 | Cleveland-Cliffs Steel Properties Inc. | METHOD FOR PREVENTING PREMATURE EDGE FRACTURE AT THE LEVEL OF A RETAINING RIB |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1665203A (en) * | 1926-02-26 | 1928-04-10 | Joseph Pavelka | Die |
| US2237069A (en) * | 1940-08-16 | 1941-04-01 | Gustaf O Christenson | Draw punch |
| CS224368B1 (en) * | 1981-06-03 | 1984-01-16 | Tomasek Jiri | Flangeless shell drawing apparatus |
| JPS6028921U (ja) * | 1983-07-29 | 1985-02-27 | 日野自動車株式会社 | トリミングダイ |
| JP2745505B2 (ja) * | 1987-04-23 | 1998-04-28 | トヨタ自動車株式会社 | 薄肉カツプ端面のプレス切断方法 |
| JPS6434525A (en) * | 1987-07-29 | 1989-02-06 | Toshiba Corp | Drawing method having edge punching stage |
| JP3156092B2 (ja) * | 1991-08-22 | 2001-04-16 | 中村製作所株式会社 | プレス加工方法 |
| JP3518004B2 (ja) * | 1994-12-19 | 2004-04-12 | 株式会社デンソー | 環状加工品の端面切断方法およびその端面切断方法に用いる端面成形用金型 |
| US5630337A (en) * | 1995-09-07 | 1997-05-20 | Werth; Elmer D. | Apparatus and method for forming a container |
| JP3239764B2 (ja) | 1996-07-17 | 2001-12-17 | 株式会社ニコン | Cmp用研磨装置及び研磨ポリシャ |
| US6981327B2 (en) * | 2003-01-10 | 2006-01-03 | Greenlee Textron Inc. | Two piece punch with pilot hole locator |
| US20080229802A1 (en) * | 2004-01-28 | 2008-09-25 | Glud & Marstrand A/S | Method of Forming a Metal Sheet Blank |
| DE102009059197A1 (de) * | 2009-12-17 | 2011-06-22 | ThyssenKrupp Steel Europe AG, 47166 | Verfahren und Vorrichtung zur Herstellung eines Halbschalenteils |
-
2010
- 2010-03-02 DE DE102010000608A patent/DE102010000608B3/de not_active Expired - Fee Related
-
2011
- 2011-02-28 EP EP11707623.2A patent/EP2542363B1/de not_active Not-in-force
- 2011-02-28 JP JP2012555373A patent/JP5801825B2/ja not_active Expired - Fee Related
- 2011-02-28 WO PCT/EP2011/052880 patent/WO2011107414A2/de not_active Ceased
-
2012
- 2012-08-08 US US13/569,525 patent/US9669447B2/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| WO2011107414A2 (de) | 2011-09-09 |
| US20130019648A1 (en) | 2013-01-24 |
| JP5801825B2 (ja) | 2015-10-28 |
| WO2011107414A3 (de) | 2011-11-10 |
| JP2013521130A (ja) | 2013-06-10 |
| EP2542363A2 (de) | 2013-01-09 |
| US9669447B2 (en) | 2017-06-06 |
| DE102010000608B3 (de) | 2011-03-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2701861B1 (de) | Verfahren und vorrichtung zur herstellung von flanschlosen ziehteilen | |
| EP2512702B1 (de) | Verfahren und vorrichtung zur herstellung eines halbschalenteils | |
| DE102008037612B4 (de) | Verfahren und Werkzeugsatz zur Herstellung von flanschbehafteten, hoch maßhaltigen und tiefgezogenen Halbschalen | |
| EP1820577B1 (de) | Profile mit in Längsrichtung veränderlichem Querschnitt | |
| EP2802425B1 (de) | Vorrichtung und verfahren zum tiefziehen von schalenteilen mit integriertem kopf- und zargenbeschnitt | |
| EP2259883B1 (de) | Verfahren zur materialflusssteuerung beim tiefziehen eines werkstücks und tiefziehvorrichtung | |
| DE102010000608B3 (de) | Verfahren und Vorrichtung zum Ziehen und Beschneiden von Platinen | |
| EP2701862B1 (de) | Verfahren und vorrichtung zur herstellung flanschbehafteter ziehteile mit gleichzeitigem beschnitt | |
| DE102016101150A1 (de) | Prallträger und Verfahren zur Herstellung eines Prallträgers | |
| EP2108467B1 (de) | Verfahren zur Herstellung von hochmaßhaltigen Halbschalen | |
| DE102017118295A1 (de) | Formpresswerkzeug | |
| DE102013112123B4 (de) | Metallhülse und Verfahren zu deren Herstellung | |
| EP2357048B1 (de) | Verfahren und Vorrichtung zum Beeinflussen der Schnitt- und Funktionsfläche an feingeschnittenen Fertigteilen | |
| EP0370562A2 (de) | Verfahren und Vorrichtung zur Umformung von Zahnflanken pulvermetallurgisch hergestellter Kupplungskörper | |
| DE102011102288B4 (de) | Vorrichtung und Verfahren zur Herstellung eines Stirnrads mit einer Schrägverzahnung | |
| WO2007115949A1 (de) | Verfahren zur herstellung von strukturierten hohlprofilen | |
| EP3478426B1 (de) | Verfahren zur herstellung von zierleisten und unter verwendung des verfahrens hergestellte zierleisten | |
| DE102014108726A1 (de) | Verfahren zur Herstellung einer Funktions- oder Zierleiste | |
| EP3190306B1 (de) | Verfahren und vorrichtung zur herstellung einer lagerbuchse | |
| EP1321202B1 (de) | Fertigungsverfahren und Innenhochdruckumformwerkzeug zur Durchführung des Fertigungsverfahrens | |
| EP1741497B9 (de) | Verfahren und Werkzeug zur spanlosen Herstellung von Werkstücken mit einer Kerbe und Werkstück mit einer Kerbe | |
| DE102019119849A1 (de) | Werkzeug und Verfahren zum Bearbeiten von plattenförmigen Werkstücken | |
| DE10328901B4 (de) | Verfahren zur Herstellung eines Stützblechs für eine Automobilkarosse sowie Vorformling für ein Stützblech | |
| DE102005017763B4 (de) | Verfahren zur Herstellung eines Profilstabs | |
| DE10307534A1 (de) | Verfahren zum Herstellen eines Rollenkörpers |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20120806 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20130801 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 648366 Country of ref document: AT Kind code of ref document: T Effective date: 20140215 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502011002002 Country of ref document: DE Effective date: 20140220 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20140108 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140508 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140408 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140508 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| BERE | Be: lapsed |
Owner name: THYSSENKRUPP STEEL EUROPE A.G. Effective date: 20140228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502011002002 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| 26N | No opposition filed |
Effective date: 20141009 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502011002002 Country of ref document: DE Effective date: 20141009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140409 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20110228 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20140228 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 648366 Country of ref document: AT Kind code of ref document: T Effective date: 20160228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160228 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20140108 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20200218 Year of fee payment: 10 Ref country code: DE Payment date: 20200219 Year of fee payment: 10 Ref country code: SE Payment date: 20200219 Year of fee payment: 10 Ref country code: IT Payment date: 20200224 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20200219 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502011002002 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20210228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210901 Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210301 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210228 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210228 |