EP2815859B1 - Längsschneideranordnung einer Längschneiderwickel einer Faserbahn-Herstellungslinie - Google Patents
Längsschneideranordnung einer Längschneiderwickel einer Faserbahn-Herstellungslinie Download PDFInfo
- Publication number
- EP2815859B1 EP2815859B1 EP13172648.1A EP13172648A EP2815859B1 EP 2815859 B1 EP2815859 B1 EP 2815859B1 EP 13172648 A EP13172648 A EP 13172648A EP 2815859 B1 EP2815859 B1 EP 2815859B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- slitter
- positioning arrangement
- winder
- support element
- slitters
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/26—Means for mounting or adjusting the cutting member; Means for adjusting the stroke of the cutting member
- B26D7/2628—Means for adjusting the position of the cutting member
- B26D7/2635—Means for adjusting the position of the cutting member for circular cutters
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D2007/0012—Details, accessories or auxiliary or special operations not otherwise provided for
- B26D2007/0043—Details, accessories or auxiliary or special operations not otherwise provided for the cutting machine comprising a linear motor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/26—Means for mounting or adjusting the cutting member; Means for adjusting the stroke of the cutting member
- B26D2007/2657—Auxiliary carriages for moving the tool holders
Definitions
- the present invention relates to a slitter-winder of a fiber web production line in general and in particular to a slitter positioning arrangement of a slitter-winder of a fiber web production line according to the preamble part of claim 1.
- a fiber web e.g. paper
- a fiber web is manufactured in machines which together constitute a paper-manufacturing line which can be hundreds of metres long.
- Modern paper machines can produce over 450,000 tons of paper per year.
- the speed of the paper machine can exceed 2,000 m/min and the width of the fiber web can be more than 11 metres.
- a fiber web completing in the paper machine is reeled by a reel-up around a reeling shaft i.e. a reel spool into a parent roll the diameter of which can be more than 5 metres and the weight more than 160 tons.
- the purpose of reeling is to modify the fiber web manufactured as planar to a more easily processable form.
- the continuous process of the paper machine breaks for the first time and shifts into periodic operation.
- the web of parent roll produced in paper machine is full-width and even more than 100 km long so it must be slit into partial webs with suitable width and length for the customers of the paper mill and wound around cores into so-called customer rolls before delivering them from the paper mill.
- This slitting and winding up of the web takes place as known in an appropriate separate machine i.e. a slitter-winder.
- the parent roll On the slitter-winder, the parent roll is unwound, the wide web is slit on the slitting section into several narrower partial webs which are wound up on the winding section around winding cores, such as spools, into customer rolls.
- the slitter-winder is stopped and the wound rolls i.e. the so-called set is removed from the machine. Then, the process is continued with the winding of a new set.
- a fiber web is slit in the longitudinal direction into several partial webs with rotating shear slitters, which form a slitter pair, comprising a top slitter blade and a bottom slitter band.
- the bottom slitter band with an adapter is mounted on a shaft of an AC-drive motor and its counter slitter, the top slitter blade, is mounted on a separate top slitter holder.
- top slitter top slitter blade with top slitter holder and with term “bottom slitter” is meant bottom slitter band with its drive motor.
- Term “slitter” means either “top slitter” or “bottom slitter” and in plural “slitters” both slitters.
- the width of the partial webs to be slit by the slitters and thus the position of the slitters can vary to a great extent when different trim settings are used, depending on the set widths of the rolls to be produced.
- the slitters have to be positioned and moved, in the cross direction of the web, into the right slitting position corresponding to the desired roll widths.
- the slitters of the slitter-winder are spaced apart as desired in the cross direction of the paper or board web, i.e. a trim change is carried out.
- slitter positioning equipment in which transfer bars with one or two gear jacks driven by a motor are used to move all slitter pairs.
- the slitter carriages, on which slitters are mounted, will grip to the transfer bars and the transfer bars are moved in reciprocating motion in their operating area.
- slitter positioning equipment based on a cogged belt or a wire rope, which is moved and the slitter carriages are attached to it.
- each slitter carriage with its own transfer device that takes care of moving the slitter to the desired position.
- EP patent publication 1390180B1 is disclosed a method for positioning slitters of a slitter-winder and in CN publication 102729286 is disclosed an automatic slitter positioning system.
- DE application publication 102007047890 is disclosed a device that has a magnetic measuring system, in which the position detection devices are connected with the carriages of the slitters, and a magnetic band extends over the path for the carriages.
- Each slitter has its own carriage and the carriages for top slitters have a common drive unit with a drive and a transmission unit.
- EP publications 1716985A1 and 1935818B1 are disclosed slitter-winders, in which energy transmission is provided by sliding contact element for the energy supply of the slitters in EP 1716985A1 and of the winding stations in EP 1935818B1 .
- EP 1716985A1 also the information transmission is provided by sliding contact element.
- a web-severing system which includes a support over which the web is arranged to move longitudinally, first and second shearing members supported respectively on first and second carrier members on opposite sides of the web, the carrier members in turn being supported by first and second guide members for transverse movement with respect to the web, and the transverse positions of both of the carrier members along the guide members being remotely controllable by a power-actuated unit.
- EP publication 1245354A1 is disclosed a device for the positioning of cutting tools for the lengthwise cutting of weblike material, comprising: a slide which is movable in a direction for positioning the cutting tools; on said slide, a gripping member for the cutting tools; a sensor for identifying the position of the cutting tools, movable together with said slide; a means for moving the slide in the positioning direction.
- a device for longitudinal cutting of a continuous web material comprising: at least a first series of slides each carrying a respective cutting tool, said slides being adjustable and clampable in pre-established positions along a first beam extending substantially transversely with respect to the direction of feed of the web material; a clamping system of the slides along said beam; a translation member to translate and position said slides along the beam.
- an apparatus for cutting a moving receiver comprising: a plurality of cutting devices, each comprising two parallel cutting wheels and a pressure wheel arranged so that the cutting wheels are pressed laterally against the pressure wheel to form two cutting areas and a chad area arranged laterally between the cutting areas; a drive mechanism for rotating the cutting wheels or pressure wheel of two or more of the plurality of cutting devices so that the rotating cutting wheels engage the moving receiver to cut the moving receiver parallel to its feed direction in the cutting areas.
- edge trim remaining at the edge of the fiber web is guided through an edge trim chute into a pulper.
- the width of the edge trim may, of course, also change.
- the untrimmed neck remaining between the edge trims according to a new and an old trim has been torn manually in order to enable the edge trim to be passed through the edge trim chute into the pulper.
- An object of the invention is to provide an easy-to-use and reliably operating slitter positioning arrangement of a slitter-winder of a fiber web production line.
- An object of the invention is to provide a slitter positioning arrangement of a slitter-winder of a fiber web production line that is in particular suitable for rebuild of a slitting section of an already existing slitter-winder.
- Another object of the invention is to accomplish rebuild of a slitter-winder as fast as possible and requiring as little changes as possible.
- the slitter positioning arrangement of a slitter-winder of a fiber web production line is mainly characterized by the features of claim 1.
- the slitter positioning arrangement comprises a support element for guides and also position-measurement means, which forms a slitter support module with the slitter carriages.
- the guides and advantageously a magnetic track for linear motors and the position-measurement means are constructed as parts of the slitter support module such that an independent unit is formed.
- the slitter support module can be pre-assembled and tight tolerances can be used.
- the independent pre-assembled slitter support modules are then assembled onto the frame beams of the slitter-winder in connection with rebuild of the slitting section of the slitter-winder.
- the frame beams of slitting section of the slitter-winder can be used as such, since the support element provides for the assembling joint surfaces and accuracy needed and thus it is in-built to the slitter support module.
- the testing and adjusting can be done also in connection with the pre-assembling work.
- the slitter carriages of the slitters are bearing mounted on the support element and the slitters are supported on the carriages in the manner known as such to one skilled in the art.
- the slitter positioning arrangement comprises a stand-alone control system, which thus needs no adapting work to other control systems of the slitter-winder or to the fiber web machine.
- the slitter positioning arrangement comprises in the slitter support module slitter carriages with a linear motor as the motor for moving the slitter carriages with high speed; typically the speed is 200 - 1000 mm/s.
- a linear motor as the motor for moving the slitter carriages with high speed; typically the speed is 200 - 1000 mm/s.
- Each slitter carriage for top and bottom slitter comprises its own linear motor and thus the time needed for positioning and moving the slitters to next slitting position for the next trim of customer rolls is reduced to 5 seconds and even less.
- the magnetic track for the linear motors is extending in cross direction, i.e. in longitudinal direction of the support element, and located in the slitter support element.
- the motor is an electric motor by which the time needed for positioning and moving the slitters to next slitting position for the next trim of customer rolls can also be reduced to 5 seconds and even less.
- electric motors or other types of motors other than linear motors are used, no magnetic tracks are needed in the slitter support module.
- the support element is made of steel.
- protective bellows between adjacent slitter carriages are located to close the support element such that the operating parts inside the support element are protected from dust and other foreign particles.
- the energy transmission to the carriages of the slitters is provided by spiral cable draws or by energy transfer chains or by bus bars.
- the position measurement means are optical or capacitive measurement means.
- Method for rebuild of a slitting section of a slitter-winder is characterized by features of claim 12.
- the new construction of slitters' support as the slitter support module using the support element makes it also possible to use a new method for edge trimming.
- the method for edge trimming of a fiber web in a slitter-winder is characterized by features of claim 14. According to the new method the edge trimming is done while the partial webs are still moving, when the machine is slowed down for the set change and the trim change. The outermost slitters in cross direction at both edges of the web are moved to the next position for the next trim of customer rolls and thus the edge trimming is achieved simultaneously and the operator does not need to go to the slitting section for manual edge trimming and thus time is saved.
- figure 1 is shown a schematical example of a slitting section of a slitter-winder in accordance with prior art.
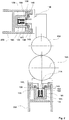
- figure 2 is shown schematically an example of a slitting section of a slitter winder according to an advantageous example of the invention.
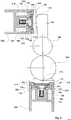
- figure 3 is shown schematically another example of a slitting section of a slitter winder according to an advantageous example of the invention.
- slitters are in pairs, one top slitter and one bottom slitter form a pair of slitters. Each pair slits one longitudinal cut to the fiber web.
- top and bottom do not necessarily have any correspondence to the location of the slitters in the slitting section of the slitter-winder; it can be that the top slitter is actually in reality below the bottom slitter.
- parts and part components and component assemblies relating to the bottom slitter are indicated by letter A after the corresponding reference numeral and parts relating to the top slitter are indicated by letter B after the corresponding reference numeral.
- FIG 1 is an example of a slitting section of a slitter-winder according to prior art.
- the slitting section comprises a frame beam 20A for bottom slitters 10A and a frame beam 20 B for top slitters 10B.
- the frame beams 20A, 20B extend longitudinally in cross section of the web.
- Each frame beam 20A; 20B comprises guides 21 A, 22A, 21B, 22B for slitter carriages 11 A; 11B of the slitters 10A; 10B.
- One of each guide pair 21 A, 22A; 21 B, 22B is a round bar 22A, 22B and the other one of each guide pair 21A, 22A; 21B, 22B is a flat bar 21A, 21B.
- the guides can be of different types and/or designs. For accurate positioning of slitter pairs 10A, 10B these guides are made under tight tolerances. For positioning and moving the slitter pairs 10A, 10B to the next slitting position for the next trim of customer rolls, the slitter pairs 10A, 10B are moved in their carriages 11 A, 11B along the guides 21 A, 22A; 21 B, 22B.
- each slitter 10A, 10B is supported on the slitter carriage 11 A, 11 B.
- For top slitters 10B in the slitting section is upper frame beam 20B and for bottom slitters 10A is lower frame beam 20A.
- a support element 19A, 19B is supported on the frame beam 20A, 20B.
- the support element 19A, 19B is a longitudinally in extending profile type element that has a generally U-type form with collars 31 A, 31B, by which the support element 19A, 19B is supported to the frame beam 20A, 20B.
- the support element also has shoulders 32A, 32B.
- Each slitter carriage 11A, 11B has its own motor 17A, 17B, which in this example is a linear motor 17A, 17B located movably on a magnetic track 18A, 18B for the linear motors 17A, 17B.
- the magnetic track 18A, 18B is located onto the bottom of the generally U-formed support element 19A, 19B.
- Linear guides 13A, 13B for the linear bearings 14A, 14B of the carriages 11 A, 11 B are located on the shoulders 32A, 32B of the support element 19A, 19B.
- a brake 15A, 15B for stopping the corresponding carriage 11A, 11 B and a position measurement means 16A, 16B for defining the correct position of the slitters 10A, 10B.
- the energy transmission to the carriages 11 A, 11B of the slitters 10A, 10B is provided by spiral cable draws or by energy transfer chains or by bus-bars.
- the position measurement means 16A, 16B are optical or capacitive.
- the example in the figure 3 is similar with the example in figure 2 and the only difference is that in figure 3 is shown bellows 12A, 12B, which is located between adjacent slitter carriages on top part of the support element 19A, 19B for protecting the inside of the support element 19A, 19B against dust and foreign particles.
- the support element 19A, 19B and the slitter carriage 11 A, 11B with the motor 17A, 17B, the guides 13A, 13B, the brake 15A, 15B and the position-measurement means 16A, 16B form a slitter support module.
- the guides 13A, 13B, the brake 15A, 15B and the position-measurement means 16A, 16B are constructed as parts of the support element 19A, 19B in the slitter support module such that an independent unit is formed.
- the independent pre-assembled slitter support module is assembled onto the frame beam 20A, 20B of the slitter-winder in connection with rebuild of the slitting section of the slitter-winder.
- the slitter-winder is the type presented in figure 1 the flat and the round bars 21A, 22A; 21 B, 22B are removed from the frame beam 20A, 20B and the support element 19A, 1B is located into support of the frame beam 20A, 20B.
- the frame beam 20A, 20B of the slitting section of the slitter-winder can be used as such, since the support element 19A, 19B provides for the assembling needed accuracy and joint surfaces.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Forests & Forestry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Winding Of Webs (AREA)
- Nonmetal Cutting Devices (AREA)
- Registering, Tensioning, Guiding Webs, And Rollers Therefor (AREA)
- Details Of Cutting Devices (AREA)
Claims (14)
- Längsschneiderpositionieranordnung eines Rollenschneiders einer Faserbahnherstellungslinie, die in einer Längsschneiderpartie des Rollenschneiders für Längsschneider (10a,10b) angeordnet ist, welche Längsschneiderpaare eines unteren Längsschneiders (10a) und eines oberen Längsschneiders (10b) bilden, wobei die Längsschneiderpartie Rahmenträger (20a,20b) für die Längsschneider (10a,110b) aufweisen, auf denen jeder Längsschneider (10a,10b) abgestützt positioniert und mittels Schlitten (11a,11b) auf Führungen beweglich ist, wobei in der Längsschneiderpositionieranordnung jeder Schlitten für die Längsschneider (10a,10b) mit einem Motor (17a,17b) versehen ist, und wobei die Längsschneiderpositionieranordnung ein Tragelement (19a,19b) aufweist,
dadurch gekennzeichnet, dass
die Längsschneiderpositionieranordnung eine Positionsmesseinrichtung (16a,16b) aufweist, die in dem Längsschneider-Tragelement (19a,19b) angeordnet ist und ein Längsschneidertragmodul mit den Längsschneiderschlitten (11a,11b) bildet, und dass die Führungen (13a,13b) und die Positionsmesseinrichtung (16a,16b) als Teile des Längsschneidertragmoduls konstruiert sind, so dass eine unabhängige Einheit gebildet ist, wobei das Längsschneidertragmodul vormontiert und dann auf dem Rahmenträger des Rollenschneiders montiert werden kann. - Längsschneiderpositionieranordnung nach Anspruch 1,
dadurch gekennzeichnet, dass
die Längsschneiderpositionieranordnung eine Bremse (15a,15b) aufweist, die in dem Längsschneidertragelement (19a,19b) angeordnet ist. - Längsschneiderpositionieranordnung nach Anspruch 1 oder 2,
dadurch gekennzeichnet, dass
die Längsschneiderschlitten (11a,11b) der Längsschneider (10a,10b) auf dem Tragelement (19a,19b) montiert gelagert und auf Linearführungen (13a,13b), die in dem Tragelement (19a,19b) vorgesehen sind, mittels Linearlager (14a,14b) beweglich sind. - Längsschneiderpositionieranordnung nach einem der Ansprüche 1 bis 3,
dadurch gekennzeichnet, dass
die Längsschneiderpositionieranordnung ein eigenständiges Steuersystem aufweist. - Längsschneiderpositionieranordnung nach einem der Ansprüche 1 bis 4,
dadurch gekennzeichnet, dass
der Motor (17a,17b) ein Linearmotor zum Bewegen der Längsschneiderschlitten (11a,11b) mit hoher Geschwindigkeit ist. - Längsschneiderpositionieranordnung nach einem der Ansprüche 1 bis 4,
dadurch gekennzeichnet, dass
der Motor (17a,17b) ein Elektromotor zum Bewegen der Längsschneiderschlitten (11a,11b) mit hoher Geschwindigkeit ist. - Längsschneiderpositionieranordnung nach Anspruch 5,
dadurch gekennzeichnet, dass
die Längsschneiderpositionieranordnung eine Magnetspur (18a,18b) für die Linearmotoren (17a,17b) aufweist, wobei die Magnetspur in den Längsschneidertragelementen (19a,19b) angeordnet ist. - Längsschneiderpositionieranordnung nach einem der Ansprüche 1 bis 7,
dadurch gekennzeichnet, dass
zwischen benachbarten Längsschneiderschlitten Schutzbälge (12a,12b) angeordnet sind, um die Tragelemente (19a,19b) derart zu schließen, dass die Innenseiten der Tragelemente von Staub und anderen Fremdpartikeln geschützt sind. - Längsschneiderpositionieranordnung nach einem der Ansprüche 1 bis 8,
dadurch gekennzeichnet, dass
eine Energieübertragung zu den Schlitten (11 a,11 b) der Längsschneider (10a,10b) durch Spiralkabelzüge oder durch Energietransferketten oder durch Sammel- bzw. Stromschienen vorgesehen ist. - Längsschneiderpositionieranordnung nach Anspruch 1,
dadurch gekennzeichnet, dass
die Positionsmesseinrichtung (16a,16b) eine optische oder kapazitive Messeinrichtung ist. - Längsschneiderpositionieranordnung nach einem der Ansprüche 1 bis 10,
dadurch gekennzeichnet, dass
das Tragelement ein sich in Längsrichtung erstreckendes Profiltypelement ist, das im Wesentlichen eine U-artige Form mit Krägen (31 a,31 b) aufweist, mittels welchem das Tragelement (19a,19b) an dem Rahmenträger (20a,20b) abgestutzt ist, und dass das Tragelement Schultern (32a,32b) aufweist. - Verfahren zur Wiederherstellung bzw. Umkonstruktion einer Längsschneiderpartie eines Rollenschneiders, wobei in dem Verfahren eine Längsschneiderpositionieranordnung gemäß einem der vorhergehenden Ansprüche vorgesehen ist, wobei das Tragelement (19a,19b) auf den Rahmenträgern der Längsschneiderpartie des wiederherzustellenden bzw. umzukonstruierenden Rollenschneiders als ein vormontiertes Längsschneidertragmodul montiert wird.
- Verfahren nach Anspruch 12,
dadurch gekennzeichnet, dass
das Längsschneidertragmodul vormontiert und dann auf dem Rahmenträger des Rollenschneiders in Verbindung mit der Wiederherstellung bzw. Umkonstruktion der Längsschneiderpartie des Rollenschneiders montiert wird. - Verfahren zum Kantenbeschneiden einer Faserbahn in einem Rollenschneider, der eine Längsschneiderpositionieranordnung nach einem der vorhergehenden Ansprüche aufweist, wobei in dem Verfahren das Kantenbeschneiden durchgeführt wird, während die Teilbahnen sich noch bewegen und der Rollenschneider für den Beschneidewechsel verlangsamt wird, und zwar durch Bewegen der äußersten Längsschneider in Querrichtung an beiden Rändern der Bahn zu der nächsten Position für das nächste Beschneiden von Kundenrollen.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP13172648.1A EP2815859B1 (de) | 2013-06-19 | 2013-06-19 | Längsschneideranordnung einer Längschneiderwickel einer Faserbahn-Herstellungslinie |
| CN201420321632.3U CN203903613U (zh) | 2013-06-19 | 2014-06-17 | 纤维幅材生产线的分切复卷机的切刀定位装置 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP13172648.1A EP2815859B1 (de) | 2013-06-19 | 2013-06-19 | Längsschneideranordnung einer Längschneiderwickel einer Faserbahn-Herstellungslinie |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2815859A1 EP2815859A1 (de) | 2014-12-24 |
| EP2815859B1 true EP2815859B1 (de) | 2016-04-27 |
Family
ID=48655987
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP13172648.1A Active EP2815859B1 (de) | 2013-06-19 | 2013-06-19 | Längsschneideranordnung einer Längschneiderwickel einer Faserbahn-Herstellungslinie |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP2815859B1 (de) |
| CN (1) | CN203903613U (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP4065322B1 (de) * | 2019-11-26 | 2025-04-23 | Grafotronic SP. Z O.O. | System zur positionierung eines werkzeugs auf einer welle und eine bahnschneidevorrichtung, die dieses system zur positionierung eines werkzeugs auf einer welle umfasst |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110834993B (zh) * | 2018-08-15 | 2023-03-24 | 金红叶纸业集团有限公司 | 分切装置和复卷机 |
| DE102022108688A1 (de) * | 2022-04-11 | 2023-10-12 | Voith Patent Gmbh | Verfahren und Vorrichtung zur Positionierung von Randschneidevorrichtungen einer Längsschneidevorrichtung für eine Materialbahn in einer Rollenschneidemaschine |
| DE102022108690A1 (de) * | 2022-04-11 | 2023-10-12 | Voith Patent Gmbh | Verfahren zur Positionierung von Schneidevorrichtung einer Längsschneidevorrichtung für eine Materialbahn in einer Rollenschneidemaschine |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3176566A (en) * | 1961-06-02 | 1965-04-06 | Beloit Eastern Corp | Remotely positioned slitter system |
| DE60108474T2 (de) * | 2001-03-26 | 2006-03-23 | A. Celli Nonwovens S.P.A., Porcari | Vorrichtung zur Verstellung von Schneidwerzeugen, Schneideanlage mit einer solchen Vorrichtung sowie Umspuler mit einer solchen Schneideanlage |
| FI20011005A7 (fi) | 2001-05-14 | 2002-11-15 | Metso Paper Inc | Menetelmä paperi- tai kartonkikoneen pituusleikkurin asetteen teossa |
| BRPI0520056B1 (pt) * | 2005-02-28 | 2019-04-30 | A. Celli Nonwovens S.P.A. | Dispositivo para corte longitudinal de um material em tela contínua e máquina possuindo o dito dispositivo |
| DE102005000049A1 (de) | 2005-04-29 | 2006-11-02 | Voith Patent Gmbh | Schneidanordnung zum Schneiden einer Materialbahn |
| DE202006019435U1 (de) | 2006-12-23 | 2007-03-01 | Voith Patent Gmbh | Vorrichtung zum Wickeln von Teilmaterialbahnen |
| DE102007000685A1 (de) | 2007-08-31 | 2009-03-05 | Voith Patent Gmbh | Rollenschneidmaschine, insbesondere Längsschneidemaschine |
| DE102007047890A1 (de) | 2007-11-29 | 2009-06-04 | Voith Patent Gmbh | Positioniereinrichtung und Verwendung einer Positioniereinrichtung |
| US8312798B2 (en) * | 2010-05-18 | 2012-11-20 | Eastman Kodak Company | Slitter with translating cutting devices |
| CN102729286B (zh) | 2012-06-11 | 2015-05-20 | 杭州大华工控技术有限公司 | 一种高速智能型分切机自动排刀系统 |
-
2013
- 2013-06-19 EP EP13172648.1A patent/EP2815859B1/de active Active
-
2014
- 2014-06-17 CN CN201420321632.3U patent/CN203903613U/zh not_active Expired - Lifetime
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP4065322B1 (de) * | 2019-11-26 | 2025-04-23 | Grafotronic SP. Z O.O. | System zur positionierung eines werkzeugs auf einer welle und eine bahnschneidevorrichtung, die dieses system zur positionierung eines werkzeugs auf einer welle umfasst |
Also Published As
| Publication number | Publication date |
|---|---|
| CN203903613U (zh) | 2014-10-29 |
| EP2815859A1 (de) | 2014-12-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US9138905B2 (en) | Method for calibrating the position of the slitter blades of a slitter-winder | |
| EP3243778B1 (de) | Maschine zur herstellung von spulen mit system zur ausrichtung von längsschneidklingen und des weges der längsstreifen, die durch schneiden mit den klingen erzeugt werden, und zugehöriges verfahren | |
| JP7208673B2 (ja) | ポアソン比計算装置を備えた巻取り装置及び関連する方法 | |
| EP2769813B1 (de) | Verfahren zur Kalibrierung der Position der Rollenschneidklingen eines Rollenschneiders | |
| EP2815859A1 (de) | Längsschneideranordnung einer Längschneiderwickel einer Faserbahn-Herstellungslinie | |
| EP3144132B1 (de) | Automatische vorrichtung zum querschneiden von verstärkten gummibahnen | |
| EP3867711B1 (de) | Wickelmaschine mit einem auswertesystem für das zu verarbeitende bahnmaterial und verfahren | |
| CA2700438A1 (en) | Web inspection and repair machine with rotary razor slitting | |
| KR101725674B1 (ko) | 고무 호스를 절단하는 장치 및 방법 | |
| CN213387076U (zh) | 分切机 | |
| KR102309248B1 (ko) | 철판 슬릿팅 절단장비의 사이드 가이드 | |
| EP2653422B1 (de) | Verfahren und Vorrichtung zum Wickeln von Faserbahnen, insbesondere von Teilbahnen aus Papier und Pappe | |
| CN204322548U (zh) | 用于切割帘线带的纵断机 | |
| CN216027193U (zh) | 一种开卷纵剪收卷线 | |
| EP2666739A1 (de) | Verfahren zum Aufbringen von Klebstoff in einer Rollenschneid- und Wickelmaschine von einer Faserbahnmaschine | |
| WO2012143112A1 (en) | Side trimming apparatus for trimming longitudinal edges of a metal strip | |
| CN203680382U (zh) | 用于切割帘线带的纵断机 | |
| KR101726072B1 (ko) | 스트립 유도 장치 | |
| CN101541654B (zh) | 纤维幅材机的分切卷绕机 | |
| US10252437B2 (en) | Line for processing a continuous web material and related method | |
| EP2495195B1 (de) | Anordnung bei der Behandlung von Bahnrollen | |
| KR102219005B1 (ko) | 코드 밴드 절단용 슬리터 | |
| JP4816090B2 (ja) | 金属板の製造方法及びその製造装置 | |
| ITMI20000645U1 (it) | Apparecchiatura per il taglio a misura di materiali nastriformi | |
| EP2543616B1 (de) | Anordnung in einer Rollenschneid- und Wickelmaschine für eine Faserbahnmaschine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20130619 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| R17P | Request for examination filed (corrected) |
Effective date: 20150604 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B26D 7/26 20060101AFI20151119BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20151210 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 794207 Country of ref document: AT Kind code of ref document: T Effective date: 20160515 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602013006884 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20160427 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 794207 Country of ref document: AT Kind code of ref document: T Effective date: 20160427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160727 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160728 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160829 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602013006884 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20170228 |
|
| 26N | No opposition filed |
Effective date: 20170130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160630 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160630 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160619 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20170619 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170619 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20130619 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: MT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160630 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160619 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160427 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20250627 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250618 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250624 Year of fee payment: 13 |