EP3124665B1 - Tissu non tissé, articles fabriqués à partir de celui-ci et procédé de production de ce tissu non-tissé - Google Patents
Tissu non tissé, articles fabriqués à partir de celui-ci et procédé de production de ce tissu non-tissé Download PDFInfo
- Publication number
- EP3124665B1 EP3124665B1 EP15002277.0A EP15002277A EP3124665B1 EP 3124665 B1 EP3124665 B1 EP 3124665B1 EP 15002277 A EP15002277 A EP 15002277A EP 3124665 B1 EP3124665 B1 EP 3124665B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- nonwoven fabric
- fibers
- fiber
- pla
- layer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/42—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties characterised by the use of certain kinds of fibres insofar as this use has no preponderant influence on the consolidation of the fleece
- D04H1/4382—Stretched reticular film fibres; Composite fibres; Mixed fibres; Ultrafine fibres; Fibres for artificial leather
- D04H1/43835—Mixed fibres, e.g. at least two chemically different fibres or fibre blends
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/42—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties characterised by the use of certain kinds of fibres insofar as this use has no preponderant influence on the consolidation of the fleece
- D04H1/4326—Condensation or reaction polymers
- D04H1/435—Polyesters
Definitions
- the invention refers to a nonwoven fabric comprising polylactide fibers and articles made thereof.
- the invention further refers to a method for producing the nonwoven fabric.
- a nonwoven fabric is a textile-like material made from long fibers, entangled and bonded by chemical, mechanical, heat or solvent treatment etc.
- Nonwoven materials denote fabrics which are neither woven nor knitted like felt, for example.
- Nonwoven fabrics may be engineered for absorbency, liquid repellence, resilience, stretch, softness, strength, flame retardancy, washability, cushioning, thermal insulation, acoustic insulation, filtration, use as a bacterial barrier and sterility.
- Nonwoven materials are used in numerous applications like medical applications, filters, geotextiles, and other applications, such as diapers, feminine hygiene, and other absorbent materials, disposable clothing (foot coverings, coveralls), and cleanroom or cosmetic wipes, for example.
- small fibers are put together in form of a sheet, forming a precursor web and bonded together.
- Bonding of the fibers may be performed either via an adhesive, thermally by applying binder (in the form of powder, paste, or polymer melt) and melting the binder onto and into the web by increasing temperature, or mechanically - by interlocking the fibers with serrated needles such that the inter-fiber friction results in a stronger fabric as given for felts, for example.
- An alternative mechanical method regarding needlepunching is spunlacing (hydroentanglement) employing jets of water on a formed web (usually air-laid or wet-laid, but sometimes spun-bond or melt-blown, etc.) to entangle fibers and thereby provide fabric integrity.
- the spunlace fabrics have characteristic softness, drape, conformability, and relatively high strength and sturdiness.
- Fiber properties comprise fineness, profile, length and wettability.
- isotropic or anisotropic characteristics may be achieved by different forming processes as air laying systems for isotropic character and carding for products with high MD strength (machine direction) than CD strength (cross direction), for example.
- absorbency capacity and hydroentangling energy the higher the hydroentangling energy, the lower the absorbency capacity and absorbency rate.
- PLA polylactic acid or polylactide
- PLA is a biodegradable thermoplastic aliphatic polyester which is produced by polymerization of lactic acid or lactide, the cyclic di-ester thereof.
- One production route is the ring-opening polymerization of lactide, the other route is condensation of lactic acid monomers.
- Lactic acid or lactide for polymerization derive from renewable resources, such as corn starch, tapioca roots, chips or starch, or sugarcane. Processing of PLA into fibers is performed by conventional melt spinning processes.
- nonwovens containing PLA fibers are known in producing tea bags and the like as disclosed in WO 2012 027 539 A2 , for example.
- a disposable absorbent article containing natural and / or biodegradable compounds.
- the top sheet of the article may be a nonwoven fabric containing PLA and the back sheet of the article may be a waterproof film containing PLA, or a polyethylene film containing PLA, laminated with a nonwoven fabric containing PLA.
- the article may be used as superabsorbent materials, fastening systems, and barrier cuffs.
- the invention refers to a nonwoven fabric containing PLA fibers and further fibers of at least a second fiber type, which is eucalyptus fiber.
- the relatively high hydrophilicity of PLA fibers - when compared with thermoplastic polymer fibers - contributes to a good wettability of the fibers and humidity transmission and transport, which is enhanced by the cross-shaped profile of the PLA fibers with the cross lobes forming grooves in between. Water may be transported along these grooves.
- the eucalyptus fibers have humidity managing characteristics as well and provide enhanced humidity retention.
- the PLA fibers may have micro-engravings on their surface, wherein these micro-engravings extend along the fiber's length direction.
- the micro-engravings allow a quick migration of the liquid along the axis of the fiber and therefore enable removing the liquid away from the liquid receiving surface as fast as possible.
- distribution of the liquid on a largest possible surface is supported and/or transport of the liquid to the other side of the nonwoven enabled. So, the liquid receiving surface of the nonwoven fabric may be kept comfortably dry in case of skin contact for hygiene purposes.
- the ratio of the PLA fibers can be at least 20 % by weight and up to 50 % by weight with reference to the total weight of the nonwoven fabric. The ratio may depend on the article which is made from the nonwoven fabric. A PLA fiber portion of 20 to 30 % by weight with reference to the total weight of the nonwoven fabric may be preferred. These 20 to 30 % by weight PLA allow an optimum speed of the production equipment at the textile mill during production of the nonwoven fabric, with minimum heat generation caused by friction of the fibers.
- the post-life composting of the nonwoven fabric is also more effective, when the portion of PLA fiber is 20 to 30% by weight with reference to the total weight of the nonwoven fabric, as the respective portion of eucalyptus fibers will add humidity to the composting process.
- the nonwoven fabric comprises further fibers of a third fiber type, which may be alginate fiber.
- a third fiber type which may be alginate fiber. Due to their ion-exchange and gel-forming capability, alginate fibers made from sodium alginate are known for their use in treating wounds. Sodium alginate is a polymer derived from brown seaweeds. Furthermore, alginate fibers are capable of absorbing humidity and have anti-microbial properties.
- the third fiber type in an inventive nonwoven could be a chitosan containing fiber.
- Chitosan is a polyaminosaccharide which is produced commercially by deacetylation of chitin. Natural origins of chitin are the exoskeletons of crustaceans (such as crabs and shrimps) and cell walls of fungi. Due to structural similarity with cellulose, chitosan may be blended with cotton or viscose in forming fibers. Chitosan in fibers accounts for a strong antibacterial and fungicide effects combined with high humidity absorption. Like in eucalyptus fibers, antibacterial and antimicrobial performance is associated with the inhibition of growth of bacteria combined with an anti-smell function.
- All fiber types used in the inventive nonwoven fabric exhibit good biocompatibility (antiallergic properties) and biodegradability.
- an inventive nonwoven fabric based on PLA fibers and eucalyptus fibers may comprise both, alginate and chitosan containing fibers.
- the ratio of the alginate fibers and/or chitosan containing fibers in the nonwoven fabric may not exceed 20 % by weight with reference to the total weight of the nonwoven fabric.
- the nonwoven fabric may have a surface weight of about 35 g/m 2 to 100 g/m 2 .
- the nonwoven fabric may be produced by spunlacing/hydroentanglement and may be manufactured with a substantially plain or corrugated surface, which may be perforated or not.
- Another matter of the invention is a multilayer nonwoven fabric having at least two differing layers, which stick together without chemical bonding as provided by adhesives, for example.
- At least one first layer is an inventive nonwoven fabric comprising the PLA fibers and the further fibers of the at least second fiber type, which is eucalyptus fiber.
- At least one second layer which is an inner or lower layer, comprises no PLA fibers but said further fibers of the at least second fiber type, which is eucalyptus fiber.
- the first layer or one of the first layers is a surface layer of the multilayer nonwoven fabric and may provide an application surface of the multilayer nonwoven fabric, i. e. the surface contacting skin, for example.
- moisture can be removed from the surface into the core of the nonwoven fabric and retained by the eucalyptus fibers - or inversely moisture stored in the inner of the fabric by the eucalyptus fibers may be provided at the surface, depending on the type of destined application of the nonwoven fabric.
- the multilayer nonwoven fabric may have at each surface first layers, with at least one second layer in between. Both, the first and second layer may comprise further fibers of the third fiber type. Optionally, more than two differing layers are possible, too.
- An additional first layer which is not a surface layer could comprise PLA fibers and further fibers of the at least second fiber type in an alternate ratio or PLA fibers in combination with fibers of the third fiber type, for example.
- Each layer may have a thickness of about 1 to 3 mm.
- Another subject matter of the invention is an article made of an inventive nonwoven fabric or an inventive multilayer nonwoven fabric.
- the article may be a disposable garment, a cosmetic or hygiene product, or a diaper.
- a method according to the invention comprises the steps of providing the PLA fibers with a cross-shaped profile by extrusion and providing further fibers of at least a second fiber type, wherein the second fiber type is eucalyptus fiber.
- the next step is forming a precursor web with the PLA fibers and the further fibers followed by bonding the fibers together by spunlacing / hydroentangling of the precursor web for obtaining the nonwoven fabric.
- "Web" should not be understood as a product being made by weaving but rather as a textile panel.
- micro-engravings may be generated on the PLA fibers' surface with the micro-engravings extending along the PLA fibers' length direction.
- the micro-engravings are generated by means of an adapted extrusion die with four branches for forming the cross-shaped profile and respective micro-protusions, leading to the micro-engravings.
- the PLA fiber After the melted PLA is extruded into the fiber with definite cross-shaped profile and micro-engravings, the PLA fiber may be cooled, drawn to reach the final denier, crimped (thermosetting) and finally cut in staple fibers.
- hydrophilicity of the fibers used in the invention supports hydroentanglement, since the hydrophilic fibers show an enhanced wettability and therefore engagement with the water jets resulting in in a higher degree of entanglement. Prior to hydroentanglement in the formation of the precursor web, hydrophilicity facilitates uniform fiber dispersion in wet-laid fabrics.
- a further step may be providing further fibers of a third fiber type which is alginate fiber and/or chitosan containing fiber in forming the precursor web.
- a method for producing an inventive multilayer nonwoven fabric comprises the above steps of producing a nonwoven fabric containing PLA fibers, wherein the forming step of the precursor web comprises the forming of a multilayer structure with at least two layers, wherein at least a first layer, which is an inventive layer comprising PLA fiber and further fibers of the at least second fiber type, is arranged as a surface layer, and wherein a second layer, which is arranged as a lower or inner layer comprises no PLA fibers, but further fibers of the at least second fiber type.
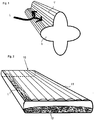
- the invention refers to nonwoven fabrics comprising PLA fibers, which have a cross-shaped profile as illustrated by fiber 1 in Fig. 9.
- the four lobes of the cruciform shape define four grooves respectively, which enhance humidity transport along the fiber, indicated by arrow L.
- Micro-engravings 1° on the surface of the fiber support migration of the liquid along the fiber length.
- the second fiber type which is comprised in an inventive nonwoven fabric is eucalyptus fiber.
- the eucalyptus fiber is an environmentally friendly fiber made from eucalyptus wood pulp. Production of eucalyptus fibers comprises sustainable agriculture with significant less water consumption than cotton.
- the eucalyptus fibers exhibit superior softness combined with odor resistance, i. e. in utilization no smell is developed over a long time. Further benefit is bacteriostaticity of the fabric, which is inherent to both, the PLA fibers and the eucalyptus fibers.
- the ratio of the PLA fibers in the nonwoven fabric is at least 20 % by weight and up to 50 % by weight with reference to the total weight of the nonwoven fabric.
- a nonwoven fabric comprises the two fiber types only, so the remaining ratio of 80 to 50 % by weight consists of eucalyptus fibers.
- a nonwoven fabric may comprise not only PLA and eucalyptus fibers, but further fibers of a third fiber type.
- This third fiber type may be alginate fibers or chitosan containing fibers, which both are excellent in biodegradability, biocompatibility, and humidity absorption, and show bacteriostatic effect as well.
- An example for chitosan containing fibers is known under the name Crabyon, which is a composite fiber of chitosan and cellulose.
- the ratio of the third fibers in the nonwoven fabric is not exceeding 20 % by weight with reference to the total weight of the nonwoven fabric. So with 20 to 50 % by weight PLA fibers, the remainder is at least 60 to 30 % by weight eucalyptus fibers.
- the nonwoven fabric has a surface weight of about 35 g/m 2 to 100 g/m 2 .
- the surface weight may be adjusted suitably depending on the intended use of the nonwoven fabric in an article like a disposable garment, cosmetic product (tissues or wipes) or hygiene product (sanitary towel), or a diaper, i. e. articles with contact to the human skin.
- an inventive nonwoven fabric may be used for other applications as for producing seed mats (with the seeds incorporated in the fabric, which will be degraded after being covered with soil) or cleaning wipes with enhanced biodegradability.
- PLA fibers with a cross-shaped profile are provided by extrusion.
- micro-engravings extending along the fibers' length may be generated on the fibers' surface during extrusion.
- the further fibers which are eucalyptus fibers (and optionally alginate fibers and/or chitosan containing fibers) are provided prior to forming a precursor web.
- Web should not be understood as a product being made by weaving but rather as a textile panel.
- the formation of the precursor web may be air-laid, wet-laid, spun-bond or melt-blown, for example.
- the bonding of the fibers for obtaining the nonwoven fabric is carried out mechanically without adhesives or binders by spunlacing / hydroentangling of the precursor web.
- Chosen process parameters in respect of web forming and fiber bonding depend among others on the target surface weight of the finished product.
- the surface may be perforated or left plain depending on the intended use. For filtering purposes the surface may be perforated whereas for commodity plain surfaces may be preferred.
- a nonwoven fabric according to the invention has a multilayer structure with at least two layers sticking together without chemical or mechanical bonding.
- An example of a multilayer nonwoven fabric with two layers is depicted in Fig. 2 . It is noted that this example shall not be understood to restrict the scope of the invention.
- a multilayer nonwoven fabric according the invention may comprise three or more layers, in which every layer may be different from the others in respect of fiber composition, fiber lengths, fiber direction, or layer thickness, for example. On the other hand, it is absolutely possible that some layers match each other or may have corresponding compositions, but differ in another parameter like layer thickness. The order of layers may be symmetric in respect to a center layer of the fabric, or asymmetric.
- the forming of the precursor web is carried out by laying the fibers in different compositions (and/or lengths, directions, thicknesses%), successively in layers.
- a first layer is formed by laying PLA, fiber and eucalyptus fibers (and optionally further fibers).
- a second layer is formed on the first layer by laying eucalyptus fibers only, so that PLA fibers are only present in the first layer.
- fiber bonding takes place by spunlacing/hydroentanglement, so the layers of the multilayer nonwoven fabric are mechanically interlaced without any chemical or adhesives.
- Fiber length etc. may not only differ in various layers, it is also possible that the length of differing fiber types differ within one layer.
- the eucalyptus fibers could be short-cut (also referred to as chopped) and the PLA fibers could be long fibers.
- the short-cut fibers may be added to only one side of the nonwoven and may be randomly orientated distributed, thereby constructing a surface structure that creates an uneven surface as in Fig. 2 , reducing the migration of fluids and improving the penetration of the fluids into the absorption core of the fabric. This could be referred to as "liquid stopper" effect, as the top layer of this example consist of small barriers.
- the length of short-cut fibers may vary from 3 mm to 40 mm and may depend on the web forming process. Maximum fiber length for air laid process is about 12 mm and for wet laid processes about 40 mm. For dry laid processes fibers may be as long as 12 cm, whereas spunbond, meltblown and electrospun processes use continuous filaments.
- the first layer 11 at the surface of the multilayer nonwoven fabric 10 comprises the PLA and eucalyptus fibers (and optionally further fibers of a third type) and the second layer 12, which is a lower layer here, comprises no PLA fibers but eucalyptus fibers (and optionally further fibers of a third type).
- the thickness of each layer is about 1 to 3 mm.
- the first layer 11 of the multilayer nonwoven fabric 10 is already a multilayer structure consisting of several sub-layers (for example five sub-layers, wherein each may have 7 g/m 2 ). In each sub-layer, the orientation of long PLA fibers 1 is essentially parallel, since longer fibers tend to lay down in the machine direction. The long fiber orientations of adjacent sub-layers are crossed, to create a criss-cross structure.
- the second layer 12 is a random fiber storage web. Both layers 11, 12 constitute the double layer mechanically interlaced carded web.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Nonwoven Fabrics (AREA)
Claims (13)
- Tissu non-tissé comprenant des fibres PLA,
caractérisé en ce que
les fibres PLA ont un profilé cruciforme et le tissu non-tissé comprend des fibres supplémentaires d'au moins un deuxième type de fibres, qui est de la fibre d'eucalyptus. - Tissu non-tissé selon la revendication 1,
dans lequel
les fibres PLA ont des micro-gravures (1') sur leur surface, avec les micro-gravures (1') s'étendant le long de la direction en longueur des fibres PLA. - Tissu non-tissé selon la revendication 1 ou 2,
dans lequel
le rapport des fibres PLA dans le tissu non-tissé est au moins de 20 % en poids et jusqu'à 50 % en poids en référence au poids total du tissu non-tissé. - Tissu non-tissé selon l'une quelconque des revendications 1 à 3,
dans lequel
le tissu non-tissé comprend des fibres supplémentaires d'un troisième type de fibres qui est de la fibre d'alginate et/ou de la fibre contenant du chitosane. - Tissu non-tissé selon la revendication 4,
dans lequel
le rapport des fibres d'alginate et/ou des fibres contenant du chitosane dans le tissu non-tissé ne dépasse pas 20 % en poids en référence au poids total du tissu non-tissé. - Tissu non-tissé selon l'une quelconque des revendications 1 à 5,
dans lequel
le tissu non-tissé présente un poids de surface d'environ 35 g/m2 à 100 g/m2. - Tissu non-tissé multicouches présentant au moins deux couches différentes de tissus non-tissés,
caractérisé en ce
qu'au moins une première couche est un tissu non-tissé selon l'une quelconque des revendications 1 à 6, dans lequel l'au moins une première couche est une couche de surface du tissu non-tissé multicouches, et
au moins une seconde couche qui est une couche intérieure ou inférieure, ne comprend pas de fibres PLA mais les fibres supplémentaires de l'au moins un deuxième type de fibres, qui est de la fibre d'eucalyptus,
dans lequel les au moins deux couches du tissu non-tissé multicouches collent ensemble sans liaison chimique. - Tissu non-tissé multicouches selon la revendication 7,
dans lequel
chaque couche présente une épaisseur d'environ 1 à 3 mm. - Article en tissu non-tissé,
caractérisé en ce
que l'article est fait d'un tissu non-tissé selon l'une quelconque des revendications 1 à 6 ou est fait d'un tissu non-tissé multicouches selon la revendication 7 ou 8, dans lequel l'article est un vêtement jetable, un produit de cosmétique ou d'hygiène, ou une couche-culotte. - Procédé de production d'un tissu non-tissé contenant des fibres PLA selon l'une quelconque des revendications 1 à 6,
comprenant les étapes de- doter les fibres PLA d'un profilé cruciforme par extrusion,- doter des fibres supplémentaires d'au moins un deuxième type de fibres, dans lequel le deuxième type de fibre est de la fibre d'eucalyptus,- former un noyau précurseur avec les fibres PLA et les fibres supplémentaires,- lier les fibres ensemble par hydroliage/liage par jet d'eau du noyau précurseur pour obtenir le tissu non-tissé. - Procédé selon la revendication 10,
dans lequel
durant l'étape d'extrusion des fibres PLA avec un profilé cruciforme, des micro-gravures (1') sont générées sur la surface des fibres PLA, avec les micro-gravures (1') s'étendant le long de la direction en longueur des fibres PLA. - Procédé selon la revendication 10 ou 11,
comprenant l'étape- de doter des fibres supplémentaire d'un troisième type de fibres qui est de la fibre d'alginate et/ou de la fibre contenant du chitosane dans la formation du noyau précurseur. - Procédé de production d'un tissu non-tissé multicouches selon les revendications 7 ou 8,
comprenant les étapes de- production d'un tissu non-tissé contentant des fibres PLA avec un procédé selon l'une quelconque des revendications 10 à 12, dans lequeldans l'étape de formation du noyau précurseur, une structure multicouches est formée avec au moins deux couches, dans lequel au moins une première couche, qui est agencée pour résulter en une couche de surface, comprend la fibre PLA et des fibres supplémentaires de l'au moins un second type de fibres, et au moins une seconde couche, qui est agencée en tant que
couche intérieure ou inférieure, ne comprend pas de fibres PLA mais les fibres supplémentaires de l'au moins un deuxième type de fibres.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP15002277.0A EP3124665B1 (fr) | 2015-07-31 | 2015-07-31 | Tissu non tissé, articles fabriqués à partir de celui-ci et procédé de production de ce tissu non-tissé |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP15002277.0A EP3124665B1 (fr) | 2015-07-31 | 2015-07-31 | Tissu non tissé, articles fabriqués à partir de celui-ci et procédé de production de ce tissu non-tissé |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3124665A1 EP3124665A1 (fr) | 2017-02-01 |
| EP3124665B1 true EP3124665B1 (fr) | 2017-10-04 |
Family
ID=53773148
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP15002277.0A Active EP3124665B1 (fr) | 2015-07-31 | 2015-07-31 | Tissu non tissé, articles fabriqués à partir de celui-ci et procédé de production de ce tissu non-tissé |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP3124665B1 (fr) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108286132A (zh) * | 2018-03-27 | 2018-07-17 | 界首市圣通无纺布有限公司 | 一种具有抗菌功能的易降解无纺布加工方法 |
| US10590577B2 (en) | 2016-08-02 | 2020-03-17 | Fitesa Germany Gmbh | System and process for preparing polylactic acid nonwoven fabrics |
| US20210330032A1 (en) * | 2020-04-27 | 2021-10-28 | Allbirds, Inc. | Knit athletic shoes with continuous upper portion |
| US11441251B2 (en) | 2016-08-16 | 2022-09-13 | Fitesa Germany Gmbh | Nonwoven fabrics comprising polylactic acid having improved strength and toughness |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| USD1010280S1 (en) | 2020-04-27 | 2024-01-09 | Allbirds, Inc. | Shoe |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| MX2008006155A (es) | 2008-05-09 | 2009-11-09 | Grupo P I Mabe Sa De C V | Articulo absorbente desechable, amigable con el medio ambiente. |
| JP5585001B2 (ja) * | 2009-05-25 | 2014-09-10 | 東レ株式会社 | ニードルパンチ不織布の製造方法 |
| US8828895B2 (en) | 2010-08-25 | 2014-09-09 | Nonwoven Network LLC | Webs of bi-component and mono-component Co-PLA fibers |
| JP2015510555A (ja) * | 2012-02-10 | 2015-04-09 | キンバリー クラーク ワールドワイド インコーポレイテッド | 改質ポリ乳酸繊維 |
| EP3033449B1 (fr) * | 2013-08-16 | 2018-12-19 | GPCP IP Holdings LLC | Substrat enchevêtré de fibres libériennes individualisées courtes |
-
2015
- 2015-07-31 EP EP15002277.0A patent/EP3124665B1/fr active Active
Non-Patent Citations (1)
| Title |
|---|
| None * |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US10590577B2 (en) | 2016-08-02 | 2020-03-17 | Fitesa Germany Gmbh | System and process for preparing polylactic acid nonwoven fabrics |
| US11441251B2 (en) | 2016-08-16 | 2022-09-13 | Fitesa Germany Gmbh | Nonwoven fabrics comprising polylactic acid having improved strength and toughness |
| CN108286132A (zh) * | 2018-03-27 | 2018-07-17 | 界首市圣通无纺布有限公司 | 一种具有抗菌功能的易降解无纺布加工方法 |
| US20210330032A1 (en) * | 2020-04-27 | 2021-10-28 | Allbirds, Inc. | Knit athletic shoes with continuous upper portion |
| US11849804B2 (en) * | 2020-04-27 | 2023-12-26 | Allbirds, Inc. | Knit athletic shoes with continuous upper portion |
Also Published As
| Publication number | Publication date |
|---|---|
| EP3124665A1 (fr) | 2017-02-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| Das et al. | Composite nonwovens | |
| EP2540892B1 (fr) | Tissu non tissé dispersible dans l'eau | |
| US11674248B2 (en) | Nonwoven fabrics comprising polylactic acid having improved strength and toughness | |
| KR102240716B1 (ko) | 오일 흡수 능력이 향상된 부직포 셀룰로오스 섬유 직물 | |
| KR102240747B1 (ko) | 광학적으로 투명한 습식 부직포 셀룰로오스 섬유 직물 | |
| EP3124665A1 (fr) | Tissu non tissé, articles fabriqués à partir de celui-ci et procédé de production de ce tissu non-tissé | |
| EP2193229A1 (fr) | Non-tissé provenant d'un câble de filaments texturés | |
| CA2921537C (fr) | Substrat enchevetre de fibres liberiennes individualisees courtes | |
| KR20240039199A (ko) | 스테이플 섬유를 갖는 코폼 재료 및 코폼 재료 형성 공정 | |
| CN109563662A (zh) | 用于制备聚乳酸非织造织物的系统和方法 | |
| US20220331176A1 (en) | A hygiene article | |
| JP2015048569A (ja) | 不織布及び該不織布の製造方法 | |
| JP2024539638A (ja) | エアレイド不織布 | |
| CN101060822B (zh) | 起圈的非织造纤维网、其制造方法以及包含该纤维网的制品 | |
| US20220064850A1 (en) | Nonwoven fabric having improved fluid management properties | |
| Bhat et al. | Biodegradable materials for nonwovens | |
| JP4854214B2 (ja) | 吸水性不織布積層体 | |
| ES2382791T3 (es) | Tela no tejida biodegradable de copoliéster | |
| CN106178071A (zh) | 一种超吸水敷料及其制备方法 | |
| Ferdousi et al. | Non-woven | |
| JP5235783B2 (ja) | ポリ乳酸系潜在捲縮繊維 | |
| KR20140116598A (ko) | 스펀레이스 부직포, 이를 포함하는 물티슈 및 그 제조방법 | |
| JP6053353B2 (ja) | 積層不織布の製造方法 | |
| EP3385432A1 (fr) | Tissu de fibres de cellulose non tissé ayant une très faible teneur en métaux lourds | |
| WO2025248849A1 (fr) | Tissu non tissé et son procédé de fabrication |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20160219 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20170504 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 934142 Country of ref document: AT Kind code of ref document: T Effective date: 20171015 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602015005053 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20171004 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 934142 Country of ref document: AT Kind code of ref document: T Effective date: 20171004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180104 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180204 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180105 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180104 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602015005053 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| 26N | No opposition filed |
Effective date: 20180705 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20180925 Year of fee payment: 5 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20180731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20190731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190731 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20150731 Ref country code: MK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20171004 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180731 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250819 Year of fee payment: 11 |