EP3204555B1 - A system and a method for producing a molded article, such as a tray - Google Patents
A system and a method for producing a molded article, such as a tray Download PDFInfo
- Publication number
- EP3204555B1 EP3204555B1 EP15778606.2A EP15778606A EP3204555B1 EP 3204555 B1 EP3204555 B1 EP 3204555B1 EP 15778606 A EP15778606 A EP 15778606A EP 3204555 B1 EP3204555 B1 EP 3204555B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- pulp
- mold part
- hollow
- pressure
- male
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21J—FIBREBOARD; MANUFACTURE OF ARTICLES FROM CELLULOSIC FIBROUS SUSPENSIONS OR FROM PAPIER-MACHE
- D21J3/00—Manufacture of articles by pressing wet fibre pulp, or papier-mâché, between moulds
Definitions
- tray-shaped articles made from pulp would, for environmental reasons, be a highly desirable alternative to plastic containers, one reason for the limited popularity of such articles is believed to be their high costs arising from the relatively high demand for energy required during the production thereof, particularly during the dewatering of the pulp material. The relatively high production time is also a factor as often a processing in a separate drying station of the molded article is required.
- US 2004/0041305 A1 discloses a system for producing a molded article according to the premable of claim 1.
- the present invention relates to a system for producing a molded article, in particular a tray-shaped article, from pulp, said system comprising:
- said pressing tool has a hollow and an expandable male mold part, said system further comprising an expanding device configured for expanding said expandable male mold part by establishing an inside pressure in said hollow of said expandable pressing tool.
- Said female mold part may comprise a casing for enclosing said one or more further cavities.
- a system as described above may include a wall separating said first cavity from said one or more cavities, said wall having said first surface, an opposite second surface of said wall being oriented towards said one or more further cavities.
- Said one or more cavities may be in an open-celled porous material.
- said wall and said one or more further cavities may be an integral structure.
- said heating device and said expanding device may supply a hot fluid heating medium to said hollow, for said heating and expanding of said expandable male part.
- Embodiments comprising an expandable male mold may further comprise a control device operable to establish simultaneously at the most the same elevated pressure in said one or more further cavities as said inside pressure in said hollow.
- said heating device may be located in said hollow, and preferably heating by microwaves.
- the method may comprise the further steps of:
- the method may comprise, before said step b, a step of draining said one or more further cavities.
- said inside pressure in said hollow established in step b is higher than 4 bar, said heating in step d being so as to superheat liquid only in a portion of said layer nearest said male part.
- Said elevated fluid pressure may be between 70% and 100%, preferably between 90% and 100%, of said inside pressure in said hollow, said heating in step d being so as to superheat liquid contained in said pulp only in a portion of said layer nearest said male part.
- Said inside pressure established in step b may be higher than 6 bar, preferably between 7-8 bar, said pressure established in said one or more further cavities in said step c being identical, or substantially identical, to said inside pressure inside said hollow established in step b.
- said system includes a wall separating said first cavity from said one or more cavities, said wall having said first surface, an opposite second surface of said wall being oriented towards said one or more further cavities.
- the present invention is concerned with the making of articles from a fibrous pulp material, in particular tray-shaped articles such as the article 5 shown in fig. 1a , which article may have a bottom and a peripheral side wall.
- the side wall may be composed of sides meeting at an angle, as shown in fig. 1a , or may be round.
- the side wall may also present any type of surface irregularities, such as ribs, that may conveniently result from the pressing method discussed in the following with reference to preferred embodiments of the invention.
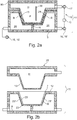
- a predetermined amount of pulp slurry in the form of a water dispersion of pulp fibre, such as wood pulp, and, if necessary, other components/additives is contained in a first, central or interior cavity 21 of a split mold 11, shown in a closed configuration in fig. 2a .
- the other components/additives may e.g. be clay, biobased or non-biobased fibres, colorants, and process catalysts.
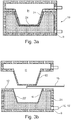
- the pulp slurry has been previously applied as a layer 7 onto an inwardly oriented first surface 23' of a female mold part 12 of the split mold 11, when the latter is in its open configuration shown in fig. 2b .
- This application or depositing may, by way of example, be either by using an insertable tubular pulp delivery device 15 (see fig. 3b ) or by dipping the female mold part 12 in the pulp slurry.
- the mold may e.g. be made from polymer, ceramic or metal, such as aluminium.
- the amount of solid fibre material in the pulp slurry should be chosen so that it has a pumpable consistency. It should e.g. be above 0 up to 10 weight percent, such as up to 4 weight percent.
- the split mold 11 of the system 10 has apart from the female mold part 12 a pressing tool 25 having a hollow H defined by a casing 90 and an impermeable expandable male mold part 13 tightly connected to the casing 90 to depend therefrom, as best seen in fig. 2b .
- the expandable male part 13 as such is shown in fig. 1b in its slack state and is formed with an overall shape which essentially corresponds or conforms to the overall outline of the recess of the female mold part 12. This recess is defined by the inwardly oriented surface 23' and into which the male mold part 13 is inserted to delimit the first cavity 21.
- the term "expandable" as used herein should be understood in the way that the male mold part 13 may expand elastically on application of a pressure P in the hollow H.
- the male mold part 13 When expanded the male mold part 13 will press against the layer 7 of pulp with a uniform pressure corresponding to the aforementioned pressure P.
- the split mold 11 Normally, in the present invention the split mold 11 will be brought to assume its closed configuration with no pressure being applied in the hollow H such that during this operation, the male mold part 13 is in the slack state. In this state, it will largely not contact the layer 7 of pulp on the surface 23' during its insertion into the female mold 12.
- Such a contact if the male mold part 13 were a solid structure or already expanded on insertion into the female mold part 12 could damage the inner surface of the article 5 to be molded, and/or drive some of the pulp material towards the bottom of the recess of the female mold 12.
- a pressure perpendicular to the surface 23' By applying a pressure perpendicular to the surface 23', a higher strength of the molded article can be obtained for a given amount of pulp material. Alternatively, a lower amount of material may be used without compromising a given desired strength.
- an expandable male mold part 13 allows for a great versatility in that complex articles may be molded where the male mold part 13 through its expansion may be brought to form article portions having faces oriented towards the bottom of the article.
- the male mold part 13 may by way of example be made of silicone rubber or any other elastic material capable of withstanding relatively high temperatures while at the same time conforming essentially to the shape of the inner cavity 21.
- a heating device 30 is arranged inside the hollow H to provide for a heating of the male mold part 13 and, hence, the layer 7 of pulp.
- This heating device 30 may operate on the basis of irradiation.
- fluid supplied via a port in the pressing tool 25 to the hollow H for setting up the pressure P may be heated by an external heating device to a desired temperature, such that this fluid serves also the purpose of heating the male mold part 13.
- the female mold part 12 also comprises one or more further cavities 24.
- the aforementioned first surface 23' allows fluid contained in the layer 7 of pulp to flow into the one or more further cavities 24.
- the female mold part 12 is shown as having a casing 9 which delimits two such cavities 24 separated by a wall structure W, each cavity 24 being connected to a first compressor 16 and a draining pump 16'.
- the compressors 16 connected to the one or more further cavities 24 are configured for establishing, in one mode of operation of the system 10, a temporary elevated fluid pressure of more than 1 bar in the one or more further cavities 24 in the female mold part 12 and the draining pump 16' for evacuating the one or more further cavities in another mode of operation of the system 10.
- the first, inwardly oriented surface 23' is such as to allow fluid, in gas or liquid form, to pass between the one or more cavities 24 of the female mold part 12 and the central or first cavity 21 between the male mold part 13 and the female mold part 12.
- a wall 23 with through-going bores B separates the first cavity 21 from the one or more further cavities 24 within the female mold part 12 and has a surface 23" facing the one or more further cavities 24, opposite the first surface 23'.
- the female mold part 12 may be of an open-celled porous material, such as of a sintered material, having the inwardly oriented first surface 23'.
- the porous material is such that fluid may pass through the surface 23' and flow between the first cavity 21 and a compressor 16/pump 16' connected to the female mold part 12 as was the case in the first embodiment.
- the inwardly oriented first surface 23' may be defined by a netted structure N applied onto the sintered material portion.
- the wall 23 may be integral with the open-celled porous material and may not be distinguishable.
- a netted structure N as mentioned may also have been applied onto the wall 23 in the first embodiment of fig.
- the purpose of the netted structure N is generally to act as a filter restricting or preventing pulp fibres in the pulp layer 7 from ingressing into the female part 12.
- Such an net and/or the mold could e.g. be made by 3D-printing and sintering. Other methods of making these components will be well known to a person skilled in the art.
- the determination of an actual size of the porosity can be based on parameters such as the desired surface pattern and the risk of clogging for a given pulp composition and process parameters used. An optimal choice may e.g. be determined by experimentation.
- an external heating device generating a hot, pressurised fluid, such as a liquid, such as hot oil at a temperature of, by way of example, 100 °C to 350°C, such as 100 °C to 140 °C, or a gas, and being coupled to a second compressor 17 delivering this fluid to the pressing tool 25 to set up in the hollow H a pressure P, such as 1-30 bar, or even 70-100 bar, via a port in the pressing tool 25.
- a hot, pressurised fluid such as a liquid, such as hot oil at a temperature of, by way of example, 100 °C to 350°C, such as 100 °C to 140 °C, or a gas
- a second compressor 17 delivering this fluid to the pressing tool 25 to set up in the hollow H a pressure P, such as 1-30 bar, or even 70-100 bar, via a port in the pressing tool 25.
- the aforementioned pressure P is selected such that on the one hand the deposited pulp material 7 is not damaged by an excessive pressure applied by the expanded male part 13 and, preferably, on the other hand such that the pulp material is sufficiently pressed by the expanded male part 13 against the interior first surface 23' to give rise to an initial dewatering.
- This dewatering is obtained by water in the pulp being pressed out of the pulp and through the aforementioned channels B or open pores of the female mold part 12.
- Evacuation or draining of the female mold part 12 by means of the pump 16' may be terminated immediately prior to the temperature of the deposited pulp having reached a pre-set threshold temperature, or when a certain initial dewatering of the deposited pulp has occurred.
- the control device C is preferably configured to provide for an abrupt decrease in the elevated fluid pressure in the female mold part 12, to bring about evaporation of the superheated water. This evaporation will occur where the layer of pulp is at the highest temperature, viz. where it contacts or is closest to the pressing tool; i.e. near the expanded male mold part 13 located inside the first, interior cavity 21. Vapour in this portion of the layer 7 of pulp will seek to escape, and with the male mold part 13 on one side the only route of escape is through the surface 23'. The vapour drives in this process all or much of the remaining water in the layer 7 of pulp into the exterior cavity 24 from which it is subsequently drained by pump 16'.
- the optimal process parameters and the control thereof for a given product being manufactured can be determined experimentally, possibly in combination with computer modelling. It may furthermore be possible to use input from sensors arranged in the mold to optimize the process.
- the followings method steps are taken, using a system 10 as discussed above: First, a layer 7 of the pulp is deposited onto the first surface 23', following which the expandable male part 13 is inserted into the female mold part 12. Then an inside pressure P inside the male mold part 13 is established using the compressor 17 to press the expandable male part 13 against the layer 7 of pulp. As a next step, using the first compressor 16 connected to a port of the female mold part 12, a positive elevated fluid pressure of more than 1 bar is established in the one or more further cavities 24. This elevated pressure is, by way of example, between 70% and 100% of the aforementioned pressure P inside the male mold part 13 previously established.
- the pressure in the one or more further cavities 24 may be four bar.
- the elevated pressure in the one or more further cavities 24 may be in the order of 10%-90% of the aforementioned pressure P.
- the heating device 30 is activated to heat the expanded male mold part 13 which is pressing against the layer 7 of pulp, and to superheat some of the water of the pulp. Then the pressure inside the one or more further cavities 24 is released by disconnecting the compressor 16 while maintaining a higher inside pressure inside the expanded male mold part 13 pressing against the layer 7 of pulp.
- the heating device 30 is deactivated and the male mold part 13 is withdrawn from the first, central cavity 21, preferably after release of the pressure P to bring it into the slack state. The molded article 5 is then removed from the split mold 20.
- the inside pressure P inside the expandable expansion member 25 generated by the second compressor 17 is higher than 4 bar.
- this size of the pressure has been found as providing the desired surface roughness and compression of the fibres.
- other pressures will also be covered by the scope of the invention and may be more appropriate for other types of pulps, product dimensions and desired surface appearances.
- the heating is so as to superheat liquid only in a portion of the layer 7 of pulp nearest the expandable male part 13.
- this superheated liquid in the pulp nearest the male part 13 drives liquid/water in the liquid phase into the one or more further cavities 24.
- the inside pressure P is higher than 6 bar, preferably between 7-8 bar, and the elevated fluid pressure established in the one or more further cavities 24 may be less than or identical therewith.
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Paper (AREA)
- Containers Having Bodies Formed In One Piece (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| HRP20181857TT HRP20181857T1 (hr) | 2014-10-08 | 2015-10-08 | Sustav i postupak za proizvodnju lijevanog proizvoda poput plitke posude |
| SI201530473T SI3204555T1 (sl) | 2014-10-08 | 2015-10-08 | Sistem in metoda za proizvodnjo odlitega artikla, kot na primer pladnja |
| SM20180583T SMT201800583T1 (it) | 2014-10-08 | 2015-10-08 | Un sistema e un metodo per produrre un articolo stampato, come una vaschetta |
| RS20181310A RS57861B1 (sr) | 2014-10-08 | 2015-10-08 | Sistem i postupak za proizvodnju livenog proizvoda poput plitke posude |
| PL15778606T PL3204555T3 (pl) | 2014-10-08 | 2015-10-08 | System i sposób do wytwarzania formowanego artykułu, takiego jak taca |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP14188123 | 2014-10-08 | ||
| PCT/DK2015/050301 WO2016055072A1 (en) | 2014-10-08 | 2015-10-08 | A system and a method for producing a molded article, such as a tray |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3204555A1 EP3204555A1 (en) | 2017-08-16 |
| EP3204555B1 true EP3204555B1 (en) | 2018-08-15 |
Family
ID=51687873
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP15778606.2A Active EP3204555B1 (en) | 2014-10-08 | 2015-10-08 | A system and a method for producing a molded article, such as a tray |
Country Status (13)
| Country | Link |
|---|---|
| EP (1) | EP3204555B1 (lt) |
| CY (1) | CY1120999T1 (lt) |
| DK (1) | DK3204555T3 (lt) |
| ES (1) | ES2694634T3 (lt) |
| HR (1) | HRP20181857T1 (lt) |
| HU (1) | HUE041850T2 (lt) |
| LT (1) | LT3204555T (lt) |
| PL (1) | PL3204555T3 (lt) |
| PT (1) | PT3204555T (lt) |
| RS (1) | RS57861B1 (lt) |
| SI (1) | SI3204555T1 (lt) |
| SM (1) | SMT201800583T1 (lt) |
| WO (1) | WO2016055072A1 (lt) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US12060682B2 (en) | 2018-07-19 | 2024-08-13 | Celwise Ab | Laminated structure and method of its production |
Families Citing this family (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| PL3512701T3 (pl) * | 2016-09-14 | 2026-04-13 | PackBenefit S.L. | Proces wytwarzania tacki formowanej z masy celulozowej |
| EP3519628A1 (en) | 2016-09-27 | 2019-08-07 | Carlsberg Breweries A/S | Plant fiber pulp closure for a container and method for manufacturing a plant fiber pulp container with a closure |
| EP3418446A1 (en) | 2017-06-21 | 2018-12-26 | BillerudKorsnäs AB | Pulp mixture |
| JP2019043630A (ja) * | 2017-09-04 | 2019-03-22 | 日本モウルド工業株式会社 | パルプモールド製容器 |
| DE102019104369B3 (de) * | 2019-02-21 | 2020-06-04 | Technische Universität Dresden | Verfahren und Vorrichtung zur Herstellung eines Formteils aus einem Faserwerkstoff |
| WO2022066149A1 (en) * | 2020-09-22 | 2022-03-31 | Hewlett-Packard Development Company, L.P. | Transfer screens to be 3d fabricated with determined pore placements |
| EP4067571A1 (en) | 2021-03-31 | 2022-10-05 | BillerudKorsnäs AB | A method for coating a hollow container comprising molded pulp |
| EP4067572A1 (en) | 2021-03-31 | 2022-10-05 | BillerudKorsnäs AB | A method for providing a non-uniform barrier coating on a hollow container comprising molded pulp |
| ES1281036Y (es) * | 2021-10-21 | 2022-01-28 | Munne Josep Soteras | Bandeja de pintor biodegradable |
| DE102022108122A1 (de) * | 2022-04-05 | 2023-10-05 | Kiefel Gmbh | Verfahren zur regelung einer heisspresseinrichtung, werkzeugkomponente für eine heisspresseinrichtung und heisspresseinrichtung |
| WO2025171224A1 (en) * | 2024-02-09 | 2025-08-14 | Graphic Packaging International, Llc | Method and system for forming articles |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB550058A (en) | 1941-09-09 | 1942-12-21 | Harold Holmyard Beasley | Improved method of and means for moulding containers and other articles from pulp, and/or the treatment of containers and other articles |
| EP1288369B1 (en) * | 2000-04-18 | 2009-10-07 | Kao Corporation | Method of producing pulp moldings |
| JP3415607B2 (ja) * | 2001-07-24 | 2003-06-09 | 花王株式会社 | 繊維成形体の製造方法 |
| CN102725448A (zh) | 2009-11-27 | 2012-10-10 | Pakit国际贸易股份有限公司 | 在模制纤维产品上施加阻挡的方法以及通过所述方法制造的产品 |
-
2015
- 2015-10-08 PT PT15778606T patent/PT3204555T/pt unknown
- 2015-10-08 HU HUE15778606A patent/HUE041850T2/hu unknown
- 2015-10-08 SM SM20180583T patent/SMT201800583T1/it unknown
- 2015-10-08 EP EP15778606.2A patent/EP3204555B1/en active Active
- 2015-10-08 LT LTEP15778606.2T patent/LT3204555T/lt unknown
- 2015-10-08 ES ES15778606.2T patent/ES2694634T3/es active Active
- 2015-10-08 DK DK15778606.2T patent/DK3204555T3/en active
- 2015-10-08 WO PCT/DK2015/050301 patent/WO2016055072A1/en not_active Ceased
- 2015-10-08 PL PL15778606T patent/PL3204555T3/pl unknown
- 2015-10-08 SI SI201530473T patent/SI3204555T1/sl unknown
- 2015-10-08 RS RS20181310A patent/RS57861B1/sr unknown
- 2015-10-08 HR HRP20181857TT patent/HRP20181857T1/hr unknown
-
2018
- 2018-11-08 CY CY181101179T patent/CY1120999T1/el unknown
Non-Patent Citations (1)
| Title |
|---|
| None * |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US12060682B2 (en) | 2018-07-19 | 2024-08-13 | Celwise Ab | Laminated structure and method of its production |
Also Published As
| Publication number | Publication date |
|---|---|
| HUE041850T2 (hu) | 2019-05-28 |
| ES2694634T3 (es) | 2018-12-26 |
| SI3204555T1 (sl) | 2018-12-31 |
| DK3204555T3 (en) | 2018-12-03 |
| SMT201800583T1 (it) | 2019-01-11 |
| WO2016055072A1 (en) | 2016-04-14 |
| HRP20181857T1 (hr) | 2018-12-28 |
| RS57861B1 (sr) | 2018-12-31 |
| EP3204555A1 (en) | 2017-08-16 |
| PL3204555T3 (pl) | 2019-01-31 |
| PT3204555T (pt) | 2018-11-23 |
| LT3204555T (lt) | 2018-11-26 |
| CY1120999T1 (el) | 2019-12-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DK3204555T3 (en) | SYSTEM AND PROCEDURE FOR MANUFACTURING A FORMATED ITEM, LIKE A DISH | |
| EP3204556B1 (en) | A system and a method for producing a molded article, such as a bottle | |
| RU2722790C2 (ru) | Способ изготовления детали из композиционного материала | |
| JP6691126B2 (ja) | 複合材料製耐火性部品の製造方法 | |
| US10954169B2 (en) | Process for manufacturing a ceramic composite material part by pressurized injection of a loaded slurry into a porous mould | |
| CN113272495B (zh) | 用于由纸浆浆料来生产3d模制产品的拾取压制装置和方法 | |
| EP1266998B1 (en) | Method of manufacturing pulp mold formed body | |
| EP2582877A1 (en) | Method and apparatus for forming an article from pulped material | |
| CN112513372A (zh) | 用于生产3d模制纸浆产品的方法 | |
| US20190134848A1 (en) | A method of fabricating a composite material part by injecting a filled slurry into a fiber texture | |
| JP2011506136A5 (lt) | ||
| CA1053048A (en) | Method of pulp molding | |
| CN1207464C (zh) | 纤维成形体的制造方法及装置 | |
| CA3068744A1 (en) | Method and equipment for producing a part by injecting resin into a woven fibre preform | |
| JP2000034699A (ja) | パルプモウルド成形品の加熱プレス用型及びパルプモウルド成形品の製造方法 | |
| KR100877008B1 (ko) | 압축하는 동안 펄프-성형된 산출물들의 잔여 수분을감소시키는 주형 공동부 장치 | |
| US7059845B2 (en) | Moulding element for forming articles by slip casting with clay or the like and a method for its manufacture | |
| JP3973368B2 (ja) | パルプモールド成形体製造用中子 | |
| JP2003306898A (ja) | パルプモールド成形方法及び抄紙装置 | |
| CN202644310U (zh) | 纸浆模塑制品的生产系统中的干燥装置 | |
| JP2009293157A (ja) | パルプ繊維製半球状容器の製造方法 | |
| KR200207189Y1 (ko) | 통기성이 양호한 도자기 용기 성형용 금형장치 | |
| Ong | Modelling and simulation of drying process for ceramic membrane fabrication | |
| JP4039765B2 (ja) | 成形体の製造方法及び成形機 | |
| JP2005179885A (ja) | パルプモールド中空成形体の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20170505 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20180222 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: GB Ref legal event code: FG4D Ref country code: AT Ref legal event code: REF Ref document number: 1029908 Country of ref document: AT Kind code of ref document: T Effective date: 20180815 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602015014906 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: HR Ref legal event code: TUEP Ref document number: P20181857 Country of ref document: HR |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Ref document number: 3204555 Country of ref document: PT Date of ref document: 20181123 Kind code of ref document: T Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20181108 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20181030 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: HR Ref legal event code: ODRP Ref document number: P20181857 Country of ref document: HR Payment date: 20181121 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 Effective date: 20181126 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2694634 Country of ref document: ES Kind code of ref document: T3 Effective date: 20181226 |
|
| REG | Reference to a national code |
Ref country code: HR Ref legal event code: T1PR Ref document number: P20181857 Country of ref document: HR |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20181030 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: EE Ref legal event code: FG4A Ref document number: E016466 Country of ref document: EE Effective date: 20181112 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: T2 Effective date: 20180815 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GR Payment date: 20181115 Year of fee payment: 4 Ref country code: LT Payment date: 20181113 Year of fee payment: 4 Ref country code: EE Payment date: 20181025 Year of fee payment: 4 Ref country code: NO Payment date: 20181101 Year of fee payment: 4 Ref country code: RO Payment date: 20181113 Year of fee payment: 4 Ref country code: PT Payment date: 20181122 Year of fee payment: 4 Ref country code: CZ Payment date: 20181227 Year of fee payment: 4 Ref country code: MC Payment date: 20181025 Year of fee payment: 4 Ref country code: FI Payment date: 20181025 Year of fee payment: 4 Ref country code: PL Payment date: 20181115 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AL Payment date: 20181120 Year of fee payment: 4 Ref country code: RS Payment date: 20181115 Year of fee payment: 4 Ref country code: SM Payment date: 20181113 Year of fee payment: 4 Ref country code: HR Payment date: 20181121 Year of fee payment: 4 Ref country code: BG Payment date: 20181023 Year of fee payment: 4 Ref country code: MT Payment date: 20181026 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: T3 Ref document number: E 29226 Country of ref document: SK |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20180403295 Country of ref document: GR Effective date: 20190320 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CY Payment date: 20181114 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602015014906 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E041850 Country of ref document: HU |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: MK Payment date: 20181108 Year of fee payment: 4 Ref country code: HU Payment date: 20181203 Year of fee payment: 4 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SK Payment date: 20181112 Year of fee payment: 4 |
|
| 26N | No opposition filed |
Effective date: 20190516 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: UEP Ref document number: 1029908 Country of ref document: AT Kind code of ref document: T Effective date: 20180815 |
|
| REG | Reference to a national code |
Ref country code: HR Ref legal event code: PBON Ref document number: P20181857 Country of ref document: HR Effective date: 20191008 |
|
| REG | Reference to a national code |
Ref country code: FI Ref legal event code: MAE |
|
| REG | Reference to a national code |
Ref country code: EE Ref legal event code: MM4A Ref document number: E016466 Country of ref document: EE Effective date: 20191031 |
|
| REG | Reference to a national code |
Ref country code: NO Ref legal event code: MMEP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191031 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20191101 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: MM4A Ref document number: E 29226 Country of ref document: SK Effective date: 20191008 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MM4D Effective date: 20191008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191031 Ref country code: LT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200506 Ref country code: NO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191031 Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191031 Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: RS Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191031 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: CY Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: HU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191009 Ref country code: SM Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200507 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191101 Ref country code: BG Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200531 Ref country code: SK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 Ref country code: LV Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200805 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20191008 Ref country code: AL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20211022 Year of fee payment: 7 Ref country code: AT Payment date: 20211021 Year of fee payment: 7 Ref country code: DK Payment date: 20211022 Year of fee payment: 7 Ref country code: ES Payment date: 20211224 Year of fee payment: 7 Ref country code: DE Payment date: 20211020 Year of fee payment: 7 Ref country code: SE Payment date: 20211020 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20211028 Year of fee payment: 7 Ref country code: FR Payment date: 20211022 Year of fee payment: 7 Ref country code: BE Payment date: 20211020 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20191008 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602015014906 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP Effective date: 20221031 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 1029908 Country of ref document: AT Kind code of ref document: T Effective date: 20221008 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20221031 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20221008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221031 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230503 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221008 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221008 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221008 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221031 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20231127 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221009 |