EP3205593A1 - Behälter, der einen warmgeformten körper und eine banderole umfasst - Google Patents
Behälter, der einen warmgeformten körper und eine banderole umfasst Download PDFInfo
- Publication number
- EP3205593A1 EP3205593A1 EP17155357.1A EP17155357A EP3205593A1 EP 3205593 A1 EP3205593 A1 EP 3205593A1 EP 17155357 A EP17155357 A EP 17155357A EP 3205593 A1 EP3205593 A1 EP 3205593A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- streamer
- container
- end portion
- container according
- fastening
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 239000012815 thermoplastic material Substances 0.000 claims abstract description 19
- 239000000463 material Substances 0.000 claims description 13
- 238000004804 winding Methods 0.000 claims description 12
- 239000000853 adhesive Substances 0.000 claims description 6
- 230000001070 adhesive effect Effects 0.000 claims description 6
- 230000014759 maintenance of location Effects 0.000 claims description 2
- 238000003856 thermoforming Methods 0.000 description 10
- 230000006835 compression Effects 0.000 description 8
- 238000007906 compression Methods 0.000 description 8
- 239000003292 glue Substances 0.000 description 7
- 230000037431 insertion Effects 0.000 description 4
- 238000003780 insertion Methods 0.000 description 4
- 235000013618 yogurt Nutrition 0.000 description 3
- 239000004793 Polystyrene Substances 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 229920002223 polystyrene Polymers 0.000 description 2
- 230000001737 promoting effect Effects 0.000 description 2
- 239000007787 solid Substances 0.000 description 2
- 208000031968 Cadaver Diseases 0.000 description 1
- 238000004026 adhesive bonding Methods 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 235000013336 milk Nutrition 0.000 description 1
- 239000008267 milk Substances 0.000 description 1
- 210000004080 milk Anatomy 0.000 description 1
- 235000011837 pasties Nutrition 0.000 description 1
- 239000003208 petroleum Substances 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 231100000241 scar Toxicity 0.000 description 1
- 238000007789 sealing Methods 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
- 238000004513 sizing Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D1/00—Rigid or semi-rigid containers having bodies formed in one piece, e.g. by casting metallic material, by moulding plastics, by blowing vitreous material, by throwing ceramic material, by moulding pulped fibrous material or by deep-drawing operations performed on sheet material
- B65D1/22—Boxes or like containers with side walls of substantial depth for enclosing contents
- B65D1/26—Thin-walled containers, e.g. formed by deep-drawing operations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D25/00—Details of other kinds or types of rigid or semi-rigid containers
- B65D25/34—Coverings or external coatings
- B65D25/36—Coverings or external coatings formed by applying sheet material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D85/00—Containers, packaging elements or packages, specially adapted for particular articles or materials
- B65D85/70—Containers, packaging elements or packages, specially adapted for particular articles or materials for materials not otherwise provided for
- B65D85/72—Containers, packaging elements or packages, specially adapted for particular articles or materials for materials not otherwise provided for for edible or potable liquids, semiliquids, or plastic or pasty materials
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2203/00—Decoration means, markings, information elements, contents indicators
- B65D2203/02—Labels
Definitions
- the present disclosure relates to a container comprising a body of thermoformed thermoplastic material and a streamer wrapped around the body so as to surround the body.
- Containers of this type are known, serving for example to contain a liquid or pasty product, such as yogurt, milk product in general, compote, or the like.
- a liquid or pasty product such as yogurt, milk product in general, compote, or the like.
- the inner face of the streamer is glued on its entire surface, in particular by being coated with a heat-sealable product, and thus adheres to the body of the container by gluing.
- the pre-bonded streamer is arranged wound on itself in a thermoforming chamber, and the material of the container body is thermoformed in this chamber, so that the heat released by this material activates the heat-sealable product, and the streamer thus adheres to the body of the container when, under the effect of thermoforming, it is pressed against the streamer.
- the body of the container having an open end and a bottom opposite this open end, it is considered that the direction which goes from this open end to the bottom of the body (corresponding to the direction of the thermoforming piston which serves to repel the thermoplastic material during thermoforming) is the vertical direction, which is transverse to the winding direction of the streamer.
- thermoplastic material Even if there is a tendency to use non-petroleum thermoplastic materials, this trend is not widespread, and such materials may be difficult to thermoform or not to ensure the desired holding, including vertical compression. Consequently, having to have such a quantity of thermoplastic material is unecological.
- the present disclosure aims to provide a container whose streamer can better contribute to the holding of the container, in particular its resistance to vertical compression.
- a container comprising a body of thermoformed thermoplastic material and a streamer wrapped around the body so as to surround the body, container in which, among the two end portions of the streamer at least the first end portion has a fastening configuration comprising at least one fastening aperture which cooperates with the second end portion of the streamer to fix between them said first and second ends.
- the two end portions of the streamer cooperate with one another, via the fastening configuration comprising the fastening opening, and also cooperate with the body of the container. Therefore, to form the streamer, a thicker and more mechanically strong material can be chosen than in the state of the art.
- the streamer constitutes an object having its own behavior, which makes it possible to produce a container having at least the same resistance to vertical compression as the containers of the prior art, with a thickness of less wall and, therefore, with less thermoplastic material.
- the streamer has a retaining edge cooperating mechanically inlay with the body of the container.
- the wall of the container body is embedded in the at least one attachment opening.
- This incrustation of the wall of the container body in the fastening opening contributes to the mechanical connection between the body of the container and the streamer, and thus contributes to locally stiffening the container body which promotes its mechanical strength, particularly its strength. to compression.
- the first end portion has one or more attachment apertures, while the second end portion is solid, and thus forms a solid band glued only on a small surface.
- the second end portion is directly secured to the body of the container by glue, in a small quantity, passing through the one or more attachment openings, and the first end portion is also perfectly secured to the body of the container being sandwiched between the body and the second end portion.
- the adhesive on the inner face of the second end portion may also contribute to the attachment of the first and second end portions therebetween.
- the first end portion has a row of attachment openings disposed transversely to the winding direction of the streamer and the inner face of the second end portion has a band of glue covering said row.
- the first and second end portions of the streamer are mechanically fixed to each other by insertion of the fastening tab into the fastening opening.
- the presence of this tab and its insertion into this opening promote the mechanical strength of the streamer, in particular its resistance to vertical compression.
- At least one of the edges of the fixing lug has a notch promoting the retention of the fixing lug in the slot-shaped fastening opening.
- said at least one bracket is embedded in the wall of the container body.
- the fastening tab inserted in the slot-shaped fastening opening forms a relief on the inner side of the streamer.
- this tab is embedded in the wall of the body of the container. This promotes the mechanical strength between the streamer and the container body, and also promotes the mechanical strength of the container body, in particular its resistance to vertical compression.
- the streamer has at least one wedging opening, located between said first and second end portions and wherein the wall of the body of the vessel is inlaid.
- the wall of the container body penetrates into the setting opening, which can also be configured to contribute to a decorative effect given by the streamer, and the inlay thus produced promotes the mechanical strength of fixing between the streamer and the wall of the container body.
- the setting opening can also be configured to contribute to a decorative effect given by the streamer, and the inlay thus produced promotes the mechanical strength of fixing between the streamer and the wall of the container body.
- the streamer has a height, measured transversely to its winding direction, which is at least equal to the height of the body of the container.
- the streamer contributes to the mechanical strength of the container body over the entire height of this body.
- the container has a thermoformed flange integral with the body, and the body is suspended in the streamer by the rim.
- the streamer which ensures the mechanical strength of the container, and in particular its resistance to vertical compression.
- the streamer is made of cardboard material having a basis weight of 150 to 250 g / cm 2 .
- the streamer has a thickness of between 200 ⁇ m and 800 ⁇ m, advantageously between 200 ⁇ m and 400 ⁇ m, more advantageously between 200 ⁇ m and 300 ⁇ m.
- the streamer has a compressive strength of between 15 and 25 daN, advantageously between 18 and 22 daN, the compressive strength being measured according to the height of the streamer, transversely to its direction of winding.
- the thickness of the thermoplastic material of the container body is of the order of 85 microns, while that of the streamer provided with the fixing configuration is of the order of 220 microns, ie a total thickness of the order 305 ⁇ m.
- the expression “of the order of” means “equal”, subject to a manufacturing tolerance, which is generally 5%.
- the figure 1 which illustrates the first embodiment, shows a container 10 comprising a thermoformed body 12 (whose contour is shown in dashed lines) and a rim 14 thermoformed in one piece with this body.
- the body defines a fastening plane for a cover, such as a peelable strip, glued to the flange.
- the container 10 also comprises a streamer 16 wound around the body 12 so as to surround it.
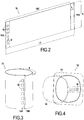
- the first end portion 16A of the streamer which is covered by its second end portion 16B, is shown in dashed lines. It can be seen that the first end portion 16A comprises fastening apertures 18 which cooperate with the second end portion 16B. More precisely, in the openings 18, the inner face of the second end portion 16B is in contact with the body of the container which is thus fixed to said second end portion 16B, thereby promoting the attachment cooperation between said first and second ends.
- this strip 16 has the first end portion 16A with the openings 18, the second end portion 16B and a common portion 16C which extends from the free end of the first end portion 16A, at the second end portion 16B.
- the figure 2 shows the face of the band which, when the band is formed, will be the inside of this band.
- only the second end portion 16B has a glued inner face thus forming a glued strip extending over the entire height H of the strip and the band, this height H being measured, transversely to the direction of the band.
- winding S of the streamer in the direction of the depth of the container body.
- the length L of this adhesive strip measured in the winding direction S of the streamer, represents between 3 and 20% of the total length LT of the strip, preferably between 4 and 10% of this length LT, more preferably between 4 and 7% of this length LT.
- the fastening openings 18 form a row of fastening apertures arranged transversely to the winding direction S of the streamer, said row of fastening openings being inscribed in a length of streamer having the same length L as the glue strip located at the second end portion 16B. So, as we see on the figure 3 when the streamer is wound on itself so that the first end portion 16A is covered by the second end portion 16B, the attachment openings 18 are completely covered by said second end portion 16B.
- the fixing openings shown in the figures by way of examples are circular, knowing however that another shape, for example an oblong shape, could be envisaged.
- the streamer has a total length LT of the order of 16 to 20 cm.
- the length L of the adhesive strip may be of the order of 7 mm and the diameter D of the fastening openings may be of the order of 5 mm.
- the second end portion 16B covers the first end portion 16A, and the second end portion 16B is secured to the body 12 of the container 10 by the glue passing through the fastening openings 18.
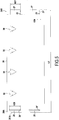
- the figure 5 shows, flat, a strip 26 for forming a streamer around a container according to a second embodiment.
- This strip / banner 26 has the same overall dimensions as the strip / banner 16 of the preceding figures, but the one or more fastening apertures 28 are slit-shaped. In this case, two slot-shaped fastening apertures 28 are shown.
- the first portion of the end 26A of the streamer 26 is thus provided with fixing slots.
- the second end portion 26B of this streamer 26 is in this case provided with two attachment lugs 27 intended to be inserted into the slots 28.
- the height H27 of the lugs 27 is slightly smaller than the height H28 of the slits 28. We see on the figure 5 at the base of the tabs 27, notches 29.
- the sum of the height H27 of a tab 27 and the height H29 of the notch 29 located at its base is equal to or very slightly less than the height H28 of the slot 28 in which this tab is intended to be inserted.
- the base 27 'of the tab 27 is substantially aligned with the lower edge 28' of the corresponding mounting slot 28, so that when the tab is inserted into the slot, this tab naturally descends to the bottom of this slot so that the notch 29 is attached to the lower edge of the slot.
- the free end of the first end portion has slight protrusions 26'A which locally extend the length of the streamer.
- the tabs 27 are inserted into the slots 28 from the outer face of the streamer 26, so that, once the vessel is manufactured, the legs 27 are on the inner side of the streamer. the banner, against the body of the container.
- This embodiment may allow to secure the streamer 26 to the body 12 of the container, without the inner face of the streamer being glued.
- the streamer has wedging openings 30 which, in this case, are regularly distributed along the length LT of the streamer. These openings are thus formed in a current portion of the streamer, at a distance from these end portions 26A and 26B.
- the wall of the body 12 of the container is embedded in these wedging openings, which further contributes to the mechanical strength between the streamer and the body of the container.
- These wedging openings may have any suitable shape, to form the decor patterns for the container. In the example shown, the wedging openings are only present towards the upper end portion of the streamer, but it should be understood that they may be present in other areas.
- the streamer 16 or 26 has a height H which is at least equal to or slightly greater than the height HC of the body 12 of the container.
- the height H exceeds the height HC by a value between 0 and 2 mm, so that the body 12 of the container is suspended in the streamer 16 or 26 by its flange 14.
- the streamer may be made of a cardboard type material, particularly ecological natural fiber. This material can impart the desired mechanical strength to the container, in particular its compressive strength, and advantageously has a basis weight of the order of 150 to 250 g / cm 2 .
- the streamer advantageously has a thickness of between 200 ⁇ m and 800 ⁇ m, advantageously between 200 ⁇ m and 400 ⁇ m, more advantageously between 200 ⁇ m and 300 ⁇ m.
- it not only exhibits the desired mechanical strength but, moreover, the incrustation phenomena previously described contribute effectively to the mechanical strength of the connection between the streamer and the container body as they operate over the entire thickness of the the banner.
- the thickness of the thermoplastic material of the body is, for example, of the order of 60 ⁇ m to 100 ⁇ m, advantageously of the order of 80 ⁇ m to 90 ⁇ m. This thickness can therefore be significantly lower than that found for containers of the state of the art. This results in a substantial saving in thermoplastic material.
- thermoplastic material of the body of the container is embedded in the opening or openings of the streamer, whether fixing or wedging opening. Conversely, when the streamer has a fixing lug projecting on its inner face, because of its insertion into the fixing slot, this time this tab is embedded in the thermoplastic material of the body of the container.
- the plastic material of the body of the thermoformed container and a retaining edge of the streamer cooperate with each other in incrustation to achieve a mechanical connection .
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Ceramic Engineering (AREA)
- Details Of Rigid Or Semi-Rigid Containers (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR1651005A FR3047472A1 (fr) | 2016-02-09 | 2016-02-09 | Recipient comprenant un corps thermoforme et une banderole |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP3205593A1 true EP3205593A1 (de) | 2017-08-16 |
Family
ID=55759815
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17155357.1A Withdrawn EP3205593A1 (de) | 2016-02-09 | 2017-02-09 | Behälter, der einen warmgeformten körper und eine banderole umfasst |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP3205593A1 (de) |
| FR (1) | FR3047472A1 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2022106725A3 (en) * | 2020-11-23 | 2022-07-07 | Compagnie Gervais Danone | Pet cup containers and process of making the same |
| WO2024261303A1 (fr) * | 2023-06-22 | 2024-12-26 | Synerlink | Pot alimentaire |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE8906782U1 (de) * | 1989-06-02 | 1989-07-20 | Starringer, Helmut, 7980 Ravensburg | Verpackung für pastöses Füllgut |
| DE3913468A1 (de) * | 1989-04-24 | 1990-10-25 | Zott Kg | Kunststoffbehaelter, insbesondere becher |
| EP2338804A1 (de) * | 2009-12-23 | 2011-06-29 | Optipack GmbH | Verpackungsbehälter |
| US20140367294A1 (en) * | 2013-06-18 | 2014-12-18 | Huhtamaki, Inc. | Container having rotating label with window |
| US20150096976A1 (en) * | 2013-10-09 | 2015-04-09 | Conagra Foods Rdm, Inc. | Microwavable food container with at least one removable microwave-interactive robe |
-
2016
- 2016-02-09 FR FR1651005A patent/FR3047472A1/fr not_active Withdrawn
-
2017
- 2017-02-09 EP EP17155357.1A patent/EP3205593A1/de not_active Withdrawn
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3913468A1 (de) * | 1989-04-24 | 1990-10-25 | Zott Kg | Kunststoffbehaelter, insbesondere becher |
| DE8906782U1 (de) * | 1989-06-02 | 1989-07-20 | Starringer, Helmut, 7980 Ravensburg | Verpackung für pastöses Füllgut |
| EP2338804A1 (de) * | 2009-12-23 | 2011-06-29 | Optipack GmbH | Verpackungsbehälter |
| US20140367294A1 (en) * | 2013-06-18 | 2014-12-18 | Huhtamaki, Inc. | Container having rotating label with window |
| US20150096976A1 (en) * | 2013-10-09 | 2015-04-09 | Conagra Foods Rdm, Inc. | Microwavable food container with at least one removable microwave-interactive robe |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2022106725A3 (en) * | 2020-11-23 | 2022-07-07 | Compagnie Gervais Danone | Pet cup containers and process of making the same |
| CN116888051A (zh) * | 2020-11-23 | 2023-10-13 | 达能日尔维公司 | Pet杯子容器及其制造方法 |
| WO2024261303A1 (fr) * | 2023-06-22 | 2024-12-26 | Synerlink | Pot alimentaire |
| FR3150186A1 (fr) * | 2023-06-22 | 2024-12-27 | Synerlink | Pot alimentaire |
Also Published As
| Publication number | Publication date |
|---|---|
| FR3047472A1 (fr) | 2017-08-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2554487B1 (de) | Laschendichtung zum Verschliessen eines Behälters mit Stöpsel oder Kapsel und entsprechendes Herstellungsverfahren | |
| EP2872409B1 (de) | Kastenförmige verpackung aus zwei materialien zum verpacken eines produktes, und herstellungsverfahren | |
| FR2531659A1 (fr) | Procede pour la fabrication par emboutissage d'un recipient conique en materiau synthetique avec un rebord d'ouverture depassant vers l'exterieur | |
| FR2916157A1 (fr) | Procede pour la realisation d'un joint scellable pour l'obturation d'un recipient a fermeture par bouchon ou capsule | |
| EP3019414B1 (de) | Verpackungsstruktur zur lagerung und verteilung eines schüttgutes | |
| EP2956292A1 (de) | Konditionierung einer gruppe von mindestens zwei kunststoffbehältern | |
| FR2915973A1 (fr) | Boite d'emballage pour flacons et decoupes correspondantes. | |
| FR2975973A1 (fr) | Procede de fabrication d'une barquette etanche en carton pour la realisation d'un emballage permettant le conditionnement de produits | |
| FR3047472A1 (fr) | Recipient comprenant un corps thermoforme et une banderole | |
| EP2905240B1 (de) | Lebensmittelverpackung mit wiederverschließbarem Deckel | |
| FR2976923A1 (fr) | Element de fond bi-matieres pour un emballage etanche | |
| EP3552526B1 (de) | Halter für blumenkomposition | |
| FR2972958A1 (fr) | Procede pour la fabrication d'une barquette bi-composants | |
| EP2226258A1 (de) | Lebensmittelverpackung mit einer umgebenden Hülle für einen Behälter mit Deckel, und Verfahren zu deren Herstellung | |
| EP2008948B1 (de) | Element zur Ausführung der Verpackung eines Lebensmittelprodukts, entsprechende Verpackung, und Einheit, die diese Verpackung und ein Lebensmittelprodukt umfasst | |
| EP4043356B1 (de) | Doppelmaterial-verpackung aus kunststoff und karton oder einem anderen biobasierten material mit deckel | |
| FR2585986A2 (fr) | Bande composite a couvercles pour recipients thermoplastiques et procede, dispositif et installation de fabrication d'une telle bande composite | |
| EP3530582B1 (de) | Verpackungsträger und herstellungsverfahren | |
| FR2962718A1 (fr) | Barquette a usage alimentaire a deux elements | |
| FR2990198A1 (fr) | Emballage pour produit alimentaire a deux parties scellees ensemble en leurs rebords, et son procede de fabrication. | |
| FR2865192A1 (fr) | Systeme de fermeture pour dispositif d'emballage ou de sur-emballage | |
| FR3012799A1 (fr) | Opercule pelable pour l'obturation d'un recipient, et joint d'etancheite comprenant un tel opercule | |
| EP4650290A2 (de) | Wasserdichter papierbehälter, insbesondere für blumensträusse mit wasservorrat | |
| FR2975083A1 (fr) | Barquette renforcee a faible impact environnemental | |
| FR3115773A3 (fr) | Emballage destiné à contenir des œufs |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20180131 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20210901 |