EP3248773A1 - Système de déchargement automatique pour machines de fabrication de sacs - Google Patents
Système de déchargement automatique pour machines de fabrication de sacs Download PDFInfo
- Publication number
- EP3248773A1 EP3248773A1 EP17173149.0A EP17173149A EP3248773A1 EP 3248773 A1 EP3248773 A1 EP 3248773A1 EP 17173149 A EP17173149 A EP 17173149A EP 3248773 A1 EP3248773 A1 EP 3248773A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- bags
- package
- unloading system
- spreader
- packages
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B70/00—Making flexible containers, e.g. envelopes or bags
- B31B70/74—Auxiliary operations
- B31B70/92—Delivering
- B31B70/98—Delivering in stacks or bundles
- B31B70/986—Stacking bags by means of a rotary stacking drum
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H31/00—Pile receivers
- B65H31/04—Pile receivers with movable end support arranged to recede as pile accumulates
- B65H31/06—Pile receivers with movable end support arranged to recede as pile accumulates the articles being piled on edge
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H31/00—Pile receivers
- B65H31/30—Arrangements for removing completed piles
- B65H31/3036—Arrangements for removing completed piles by gripping the pile
- B65H31/3045—Arrangements for removing completed piles by gripping the pile on the outermost articles of the pile for clamping the pile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H33/00—Forming counted batches in delivery pile or stream of articles
- B65H33/02—Forming counted batches in delivery pile or stream of articles by moving a blade or like member into the pile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H5/00—Feeding articles separated from piles; Feeding articles to machines
- B65H5/006—Feeding stacks of articles to machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/30—Orientation, displacement, position of the handled material
- B65H2301/33—Modifying, selecting, changing orientation
- B65H2301/332—Turning, overturning
- B65H2301/3322—Turning, overturning according to a determined angle
- B65H2301/33222—90°
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2701/00—Handled material; Storage means
- B65H2701/10—Handled articles or webs
- B65H2701/19—Specific article or web
- B65H2701/191—Bags, sachets and pouches or the like
Definitions
- the present Patent for Industrial Invention relates to an automatic unloading system at the outlet of machines for producing paper bags or paper and plastic film bags.
- the present automatic unloading system is the missing element in the production lines of paper bags or also paper bags with a transparent strip; such a system performs the automatic unloading in "packages" of desired dimensions or number of bags, generally from 50 to 100 pieces each, automatically, i.e. without the presence of an operator. Indeed, currently one or also two operators are to be present in line on the bag making machine to remove the packages of bags produced and then bind them manually or with manual strapping tools or with simple elastic rings of the traditional type.
- bag making machines start from the simple general paper tape or with a strip of transparent plastic film, during the path that starts from the roll of paper to the formed bag, bag making machines perform a series of processing operations of pre-perforation, forming the tubular body, and both longitudinal and transverse gluing, up to the complete production of the finished paper bag, then at the end of the processing path, the finished bag is stacked according to a horizontal axis on an unloading plane in almost radial direction with respect to the forming drum of the machine.
- a continuous stack of bags arranged orthogonally to the support plane is formed with the opening of the bags upwards; to allow the successive taking at the outlet by an operator, at the wanted number of bags, for example, every fifty bags, the fifty-first, by means of a suitable preset counter, is released by the pliers of the drum slightly in advance and is unloaded into the stacker, protruding from the stack itself like a bookmark, the reason for which a characteristic horizontal stack is formed with said "bookmarks" clearly visible to the operators appointed to unloading, who remove them in packages equal to the distance between one bookmark and the next, and equal, like in the example mentioned, to the number of fifty bags each.
- Another element of difficulty in packing the final production of these bags is the presence in many current productions of long and narrow bags, such as for example the ones intended for packaging bread such as traditional baguettes, which are difficult to keep stacked also for very short stacking paths.
- the present system resolves both the noted problem of high production speeds and of the dimensions of said long bags with a single solution by operating both quickly and while not undergoing any conditioning due to the length.
- the present automatic unloading system is combined with a traditional bag making machine and in particular, in the final area, immediately after the outlet drum of the bags, where normally a plate with wheels with abutment pins is arranged, where the bags just formed are collected.
- a spreader equipped with two oscillating movements, a primary one for positioning the whole system and a secondary one for opening two shaped plates such as to separate the end of one package just produced from the beginning of the following one, all during the continuous production of the bags outcoming from the drum.
- the whole set carrying the spreader is also provided with a vertical movement for allowing the cycle start repositionings.
- pliers with shaped teeth are inserted into the spreader between two separate packages of bags, i.e. the flat teeth of the pliers find room between similar alternate teeth of the spreader so as to seize, from below, the stacked bags with glued bottom downwards.
- the pliers begin spacing themselves apart from the new package being formed by moving towards the outlet of the machine with the pliers upwards, i.e. in the same direction towards which they were detached.
- a transverse cylinder sends the package towards an automatic binding device. Due to reasons of practicality in the successive handling operations, said packages are made with a number of bags varying from 50 to 100 pieces, generally the bags are made of paper or of paper and transparent film so the contents may be viewed.
- the spreader passing below the package being produced, is repositioned towards the drum where the bags produced continuously are formed and are outlet, waiting for the set quantity to be made and also for the pliers, which are arranged on a linear actuator, they also oscillating downwards, to return below the package being produced in open position to seize the new package formed at the proper count.
- the device herein referred to as a spreader is fundamental to the present unloading system, which spreader divides two adjacent packages with certainty, the spreader being provided with two oscillations which are fundamental to the whole assembly, a primary one where the whole spreader is arranged towards the drum behind the first bag of the package being produced, and a secondary one where at the end of the package, moved forwards, it opens on itself like scissors to allow the gripping of the pliers.
- the present spreader depicts the operating fulcrum of the present automatic unloading system because it decides on the order and operating frequency between the production drum and the packages of bags outcoming from the machine.
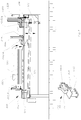
- Fig. 1 From this first assembly, the operating principle and concept of the subject of the present Patent may be traced back to, which, arranged in line with machine 500 that produces the bags (herein depicted only in the final area, i.e. at the end of the production of the bags themselves) on the unloading drum 510 where there are arranged the pliers of the drum itself which squeeze, transversely to the tubular body, the glued and closed bottom of the bag, up to the collection guides and table.
- said machines may work with productions which reach even 800 bags per minute, unloading them continuously with a bag serving as a bookmark protruding at the end of each package, a package formed usually by a number varying between 50 and 100 pieces.
- the present automatic unloading system replaces the operators who manually take the packages while binding them in different manners to tie them with elastics or strapping or automatic binding while always manually supporting the bundle.
- said automatic unloading system consists of two sets which are complementary to each other, i.e. the first, spreader 300 dimensionally prepares the package of bags produced outcoming from the machine, generally it separates from 50 to 100 pieces thereof, holds them vertically, even if they have an increased length like the bags intended for fresh French bread, or baguette, also up to 70-75 cm, then once the number of pieces is reached, it "detaches" the completed package from the one being formed and therefore allows the gripping of the first by the pliers set 200 provided with the transport movement, thus causing the package to slide on a specific table 230 up to a final area where an actuator or a general transverse pusher moves it towards a binding system, as used in these processing operations.
- the first, spreader 300 dimensionally prepares the package of bags produced outcoming from the machine, generally it separates from 50 to 100 pieces thereof, holds them vertically, even if they have an increased length like the bags intended for fresh French bread, or baguette, also up to 70-75 cm, then once
- the successive table no. 2 in Fig. 2 notes the assembly mounted in perspective view with all the actuators applied in 300 itself to provide a complete comprehensive depiction of the present set 300, while the successive Fig. 3 shows the three fundamental graphic views, where there are noted all the actuators selected for the movements, for example of 310, opening/closing with 315, oscillating on 316 by means of 312 of 310, oscillating the whole set by means of 325 and finally, raining/lowering always the whole set by means of 305.
- the shape of 310, spreader plates or planes, which are hollowed out in the lower area, towards 316, may also be noted, in order to allow the passage of the gripping teeth of the pliers 210 when they grip the bottom of the complete package 400 of the bags outlet from the forming machine.
- the successive Fig. 4 is dedicated to the gripping pliers 210 with the different devices and actuators which characterize it both in the gripping, 211, and in the transport 221, indeed, starting from the right, where the spreader can be recognized, the pliers 210 may be recognized facing upwards, 215/A, in the specific function of gripping and seizing of 400 just formed. Then it moves towards plane 230 in position 215/B, taking gripped with it package 400 to rotate it, spreading it out, over plane 230 itself and pulling it up to releasing it in position 215/C of the trolley itself.
- the present transport system allows also working on very long packages of bags which, as disclosed below, are carried vertically by a containment feeler, therefore by releasing them therefrom, they rest on plane 230 to be easily unloaded onto a side of the plane for either a manual but also automatic binding into bundles, as used and required in this field.
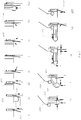
- Step I shows spreader 300 towards the drum waiting for the load of bags outcoming from the bag making machine
- II shows the pliers 210 open at the bottom and the plates 310 closed in top position
- III the formation of package 400 and the plates 310 stopped up high up to the completion of 400.
- the plates are rotated by the cylinders 312 and rotate to contain the end of the formation of 400 and allow the start of a new package 410 continuously but separately from the preceding one, like in V, then the cylinders 315 spread the plates 310 as much as required to separate the bottom of the bags, position VI. Then in VII and VIII, while more bags continue reaching the rack of the drum, cylinder 222 is raised with the pliers 210 while 325 executes the primary rotation of spreader 300.
- step IX there is the seizing by the gripping pliers of package 400 with feeler 600 which ensures the support towards the outlet of 400 itself, therefore in X, 210 retracts and with the aid of 600, the bags are sent to rotate to the right, towards the drum, as shown in X. Then in XI, the gripped pliers 210 rotate by 90° towards the drum, actuator 216, while supporting package 400 on plane 230, and then 310 they are closed by means of the cylinders 315 and are lowered through the movement of the cylinders 305.
- a new bundle 410 is being formed which increments up to the end of step XII, indeed at positions XII and XIII, while the pliers move away with 400, the lowered spreader rotates by means of 325 towards the drum and is raised again, repositioning itself behind the new package 410 in formation to begin a new cycle of separating the packages, while in XIV the pliers 210 continue their operation, releasing their gripping of package 400 which in XV is unloaded transversely by a pusher 650 to be bound or strapped here or also simply packaged outside the line for forming the various packages 400.
- 210 rotates by means of cylinder 216 (position XVI ) and travelling plane 230 (in XVII ), is repositioned in the "low" gripping position (in XVIII ) with cylinder 222 and the electromechanical actuator 221, which are arranged like in position II, waiting for the unloading of the bags from the bag making machine to be completed to form a package 400 and therefore resume the taking and transport cycle of this package 400.
- this packaging system apparently resolves the problem of the long and narrow bags contained here, at the time of unloading they are pulled by feeler 600 in the high and open area of the bag and by the pliers 210 from below, by individual package 400, towards the unloading system, while folding themselves naturally during the rotation and pulling as is clearly noted in positions X and XI of Fig. 5 , moreover, said rotation of 210 occurs at 250 mm from the start of the pulling of the bags which are supported on plane 230.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Basic Packing Technique (AREA)
- Control And Other Processes For Unpacking Of Materials (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ITUA2016A004420A ITUA20164420A1 (it) | 2016-05-27 | 2016-05-27 | Scarico automatico per macchine sacchettatrici |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3248773A1 true EP3248773A1 (fr) | 2017-11-29 |
| EP3248773B1 EP3248773B1 (fr) | 2019-01-02 |
Family
ID=56990892
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17173149.0A Active EP3248773B1 (fr) | 2016-05-27 | 2017-05-26 | Système de déchargement automatique pour machines de fabrication de sacs |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP3248773B1 (fr) |
| IT (1) | ITUA20164420A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110562537A (zh) * | 2018-06-06 | 2019-12-13 | 东洋自动机株式会社 | 袋输送方法和袋输送装置 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0337039A1 (fr) * | 1988-04-13 | 1989-10-18 | C.E.E.- Compagnie Europeenne Des Emballages Robert Schisler | Machine pour la manutention d'articles plats, notamment sacs ou sachets, à la sortie d'une machine de fabrication |
| EP1050501A2 (fr) * | 1999-04-28 | 2000-11-08 | Castaldini S.r.L. | Méthode et dispositif pour empiler des articles, en particulier des sacs en papier ou similaires |
-
2016
- 2016-05-27 IT ITUA2016A004420A patent/ITUA20164420A1/it unknown
-
2017
- 2017-05-26 EP EP17173149.0A patent/EP3248773B1/fr active Active
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0337039A1 (fr) * | 1988-04-13 | 1989-10-18 | C.E.E.- Compagnie Europeenne Des Emballages Robert Schisler | Machine pour la manutention d'articles plats, notamment sacs ou sachets, à la sortie d'une machine de fabrication |
| EP1050501A2 (fr) * | 1999-04-28 | 2000-11-08 | Castaldini S.r.L. | Méthode et dispositif pour empiler des articles, en particulier des sacs en papier ou similaires |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110562537A (zh) * | 2018-06-06 | 2019-12-13 | 东洋自动机株式会社 | 袋输送方法和袋输送装置 |
| EP3581506A1 (fr) * | 2018-06-06 | 2019-12-18 | Toyo Jidoki Co., Ltd. | Procédé de transport de sacs et appareil de transport de sacs |
Also Published As
| Publication number | Publication date |
|---|---|
| EP3248773B1 (fr) | 2019-01-02 |
| ITUA20164420A1 (it) | 2017-11-27 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN211996366U (zh) | 一种全自动双工位套袋封口包装机 | |
| CA3025685C (fr) | Tete de saisie et de pliage d'encarts, dispositif d'encartage, station de remplissage et procede de saisie, pliage et chargement d'encart | |
| US5353576A (en) | Device for packaging printed matter | |
| KR101932738B1 (ko) | 미용 마스크 팩 자동 폴딩장치 | |
| CN1081573C (zh) | 包装扁平物品的方法和设备 | |
| CZ295538B6 (cs) | Plnicí zařízení pro plnění měkkých pytlíků | |
| BR112013006603B1 (pt) | Dispositivo de transporte para o deslocamento de uma sucessão de feixes e máquina de percintagem | |
| CN108069074A (zh) | 食品容器供给装置 | |
| EP3177533B1 (fr) | Appareil pour emballer un produit avec un film extensible | |
| IT201900012273A1 (it) | Metodo e macchina per il confezionamento di prodotti in fogli di incarto | |
| US6238173B1 (en) | Apparatus for placing groups of products on pallets | |
| CN204846508U (zh) | 袋子对折包装的装置 | |
| CN104093656B (zh) | 在包装机中收集扁平对象的样品的收集方法和用于执行所述收集方法的包装机 | |
| JP7198765B2 (ja) | プリメイドパッケージ内に製品をパッケージングする装置及び方法 | |
| WO2006010732A1 (fr) | Procede et machine de fabrication de sacs a provisions en papier | |
| CN118083284A (zh) | 传送折指装置及手套自动装袋系统 | |
| EP3248773B1 (fr) | Système de déchargement automatique pour machines de fabrication de sacs | |
| JP6810880B1 (ja) | 内袋敷設装置 | |
| EP0734948A1 (fr) | Machine pour l'emballage automatique d'objets dans des récipients obtenus à partir de flans tubulaires | |
| JP6781558B2 (ja) | 製袋装置およびこれを有する梱包箱内袋敷設装置 | |
| US4442874A (en) | Automatic valve bag placer | |
| DE202010014192U1 (de) | Vorrichtung zur Entnahme und Übergabe von flachliegenden Beutelpaketen | |
| US4778438A (en) | Fabric stacking device | |
| RU2507132C2 (ru) | Способ и устройство для упаковки порционных продуктов в заготовку для упаковки | |
| KR102755316B1 (ko) | 다중 그리퍼 및 이를 포함하는 포장 장치 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20180521 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B31B 70/98 20170101AFI20180615BHEP Ipc: B65H 15/02 20060101ALI20180615BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20180802 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: AT Ref legal event code: REF Ref document number: 1083821 Country of ref document: AT Kind code of ref document: T Effective date: 20190115 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602017001653 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20190102 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1083821 Country of ref document: AT Kind code of ref document: T Effective date: 20190102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190402 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190502 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190502 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190403 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190402 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602017001653 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| 26N | No opposition filed |
Effective date: 20191003 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20190531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190526 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190526 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200531 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20170526 Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190102 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250528 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20250527 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250530 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250527 Year of fee payment: 9 |