EP3468882B1 - Verfahren und vorrichtung zum herstellen einer verpackung und so hergestellte verpackung - Google Patents
Verfahren und vorrichtung zum herstellen einer verpackung und so hergestellte verpackung Download PDFInfo
- Publication number
- EP3468882B1 EP3468882B1 EP17734790.3A EP17734790A EP3468882B1 EP 3468882 B1 EP3468882 B1 EP 3468882B1 EP 17734790 A EP17734790 A EP 17734790A EP 3468882 B1 EP3468882 B1 EP 3468882B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cardboard
- parts
- manufacturing
- window
- conveyor belt
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D15/00—Containers having bodies formed by interconnecting or uniting two or more rigid, or substantially rigid, sections made of different materials
- B65D15/22—Containers having bodies formed by interconnecting or uniting two or more rigid, or substantially rigid, sections made of different materials of polygonal cross-section
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D5/00—Rigid or semi-rigid containers of polygonal cross-section, e.g. boxes, cartons or trays, formed by folding or erecting one or more blanks made of paper
- B65D5/32—Rigid or semi-rigid containers of polygonal cross-section, e.g. boxes, cartons or trays, formed by folding or erecting one or more blanks made of paper having bodies formed by folding and interconnecting two or more blanks
- B65D5/326—Rigid or semi-rigid containers of polygonal cross-section, e.g. boxes, cartons or trays, formed by folding or erecting one or more blanks made of paper having bodies formed by folding and interconnecting two or more blanks at least one container body part formed by folding a single blank to a permanently assembled tube
- B65D5/327—Rigid or semi-rigid containers of polygonal cross-section, e.g. boxes, cartons or trays, formed by folding or erecting one or more blanks made of paper having bodies formed by folding and interconnecting two or more blanks at least one container body part formed by folding a single blank to a permanently assembled tube at least two container body parts, each formed by folding a single blank to a permanently assembled tube
- B65D5/328—Rigid or semi-rigid containers of polygonal cross-section, e.g. boxes, cartons or trays, formed by folding or erecting one or more blanks made of paper having bodies formed by folding and interconnecting two or more blanks at least one container body part formed by folding a single blank to a permanently assembled tube at least two container body parts, each formed by folding a single blank to a permanently assembled tube and the tubular body parts being alligned axially to form a container
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D5/00—Rigid or semi-rigid containers of polygonal cross-section, e.g. boxes, cartons or trays, formed by folding or erecting one or more blanks made of paper
- B65D5/42—Details of containers or of foldable or erectable container blanks
- B65D5/4204—Inspection openings or windows
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2105/00—Rigid or semi-rigid containers made by assembling separate sheets, blanks or webs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2105/00—Rigid or semi-rigid containers made by assembling separate sheets, blanks or webs
- B31B2105/002—Making boxes characterised by the shape of the blanks from which they are formed
- B31B2105/0022—Making boxes from tubular webs or blanks, e.g. with separate bottoms, including tube or bottom forming operations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2110/00—Shape of rigid or semi-rigid containers
- B31B2110/30—Shape of rigid or semi-rigid containers having a polygonal cross section
- B31B2110/35—Shape of rigid or semi-rigid containers having a polygonal cross section rectangular, e.g. square
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B50/00—Making rigid or semi-rigid containers, e.g. boxes or cartons
- B31B50/74—Auxiliary operations
- B31B50/81—Forming or attaching accessories, e.g. opening devices, closures or tear strings
- B31B50/82—Forming or attaching windows
Definitions
- the present invention relates to the field of cardboard and more particularly cardboard packaging having a plastic window or a flexible, transparent material.
- the window is advantageously transparent. It can be cut from PVC, PET, PP, cardboard or any other material.
- WO2007116150 offers a single-piece blank in corrugated cardboard for the manufacture of a display case comprising a belt comprising at least four main rectangular flaps, linked together in pairs by parallel fold lines, and provided with two series of flaps located on both sides, suitable for forming at least partially respectively the bottom and the top of the body, characterized in that the belt comprises a precut transverse line making it possible to split the blank into two half blanks, said transverse line determining on the part and on the other and for each parallel fold line, two separate fold line portions offset relative to each other to allow at least partially the catching up of the cardboard thicknesses during the coating of the second half blank on the first half blank around a mandrel.
- This patent application also describes a process for the production of a polygonal section packing case from a single blank in a sheet of corrugated cardboard, comprising a belt comprising at least four main rectangular flaps, linked together in pairs by parallel fold lines, and provided with two series of flaps located on either side, suitable for respectively forming at least partially the bottom and the top of the body, said belt comprising a precut transverse line making it possible to split the blank into two half blanks, characterized in that after unstacking the blank, the two half blanks are separated, the first half blank is deposited in a transfer channel, the second half blank being held in a plane greater than that of said transfer channel, the first half blank is transferred to a mandrel by gluing it in passing, the first half blank is wrapped around the mandrel, the transfer channel then being configured to allow the transfer of the second half blank, we lower said second half blank onto the channel, we transfer the second half blank to the mandrel and we wrap it around the first half blank itself coated around said mandrel,
- the patent application US2139626 provides a method of manufacturing a paper container, which includes folding a rectangular blank, applying an adhesive to a side portion thereof, folding the edges of the blank, so that the adhesive-treated edge overlaps the opposite edge of the blank, exerting external pressure
- the folded blank to permanently seal its overlapping edges, open the folded blank in a tubular state, form a rectangular blank to provide end closure for body structure.
- the end closure blank has foldable marginal portions projecting therefrom, the ends of said folded blank The marginal portions being separated from each other by V-shaped spaces, said shaped spaces of V being formed by making an acute angular cut at each corner of the blank, folding the marginal parts to provide recesses, applying an adhesive to the recessed parts of the finishing closure, assemble the end closure to body structure by inserting the end of said body structure into the recesses of the formed end closure and applying By exerting external pressure to permanently seal said parts together.
- the patent application 3372796 describes a package formed by an article having opposite end portions with dissimilar contours, a pair of capsules surrounding respective end portions of said article.
- the packaging comprises means for retaining said caps in leaktight manner against said end portions.
- the purpose of the present invention is to provide a solution for flexible and reliable manufacturing of such packaging.
- the blank is deposited on a conveyor belt so that the center line passing through the breakable zones is oriented perpendicular to the direction of movement of said conveyor belt, and in that said pressure rollers are arranged transversely.
- the method according to the invention controls the slowing down of the rear roller to cause the rupture of the connection zone and create a longitudinal offset between the two parts separated by a distance corresponding to the height of the window.
- the method comprises a step of repositioning the two parts separated by a jogging module to ensure the realignment of the two parts.
- the invention also relates to equipment for the manufacture of a packaging consisting of two cardboard bottoms and a transparent window extending on the lateral faces between said cardboard bottoms, characterized in that it comprises a conveyor belt and two rollers pressers whose rotation is controlled to cause the slowing of one of the rollers in contact with one of the parts relative to the roller in contact with the other part to cause the rupture of said breakable zones, and reposition the two parts by deviating by a distance corresponding to the height of the transparent window as well as a means of removing a transparent window and gluing the edges to the corresponding edges of the parts thus repositioned.
- the equipment for manufacturing a packaging according to the invention further comprises a destacker for depositing the sides on the conveyor belt and a destacker for delivering the windows.
- the equipment further comprises a jogger for realigning the cut and repositioned parts.
- the invention also relates to a package comprising two cardboard bottoms, between which it has a plastic window, characterized in that it is produced in accordance with the above-mentioned process.
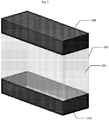
- the figure 1 shows an example of packaging comprising two cardboard bottoms (100, 200) and a window (300) disposed between the two cardboard bottoms (100, 200).
- the window (300) is typically cut from a PVC sheet, on which a groove (302) is applied to facilitate folding and prevent the PVC sheet, which is more rigid than the cardboard, from tearing the cardboard at the edge, during the forming of the cardboard and PVC bonding area.
- the transparent window (300) can also have notches (301) on the edges, at the level of the fold lines (302), to prevent the stiffness of the PVC from creating a deformation exerting on the cardboard a pressure which can lead to a tear. local.
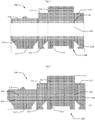
- the figure 2 represents the assembly between the cardboard blanks (100; 200) and the window (300) before shaping.
- the manufacture of a packaging box according to the invention comprises the following main steps: First of all, a series of cuts is cut from a cardboard sheet formed by two blanks (100, 200) separated by a transverse space (150) and punctually connected by breakable zones (160), and these cuts are stacked on a destacker.
- the cardboard blanks are then driven, one by one, on a conveyor belt, to a blank processing station.
- the cardboard blank is wedged, at least for part of its movement, between the conveyor belt and a pair of rollers supported on the upper surface of the blank.
- the rollers initially rotate at a synchronous speed with the belt so as to ensure the movement of the cut without speed differential between the lower part and the upper part.
- traction is then exerted on each of the blanks (100, 200), in opposite directions perpendicular to the median of the transverse space (150).
- This traction is achieved by modifying the speed of the two rollers, when positioned on either side of the breakable area (160) of the cutout. For example, the roller is slowed down behind this breakable zone, so as to create a force in a direction perpendicular to the breakable line.
- This effort causes the breakable zones (160) to rupture and makes it possible to separate the two blanks (100, 200), in order to position them one opposite the other with an offset corresponding to the transparent sheet (300).
- a window is then transported in superposition with the two edges of the blanks (100, 200), an adhesive is deposited on the edge of the strips (110, 210) and the window is deposited on the glued area.
- the figure 4 illustrates a particular example of equipment for implementing the method according to the invention.
- the equipment comprises a suction conveyor (1) running longitudinally.
- the cutout (2) is deposited on this suction belt (1) by a destacker, and slides under pressure rollers (3 to 5).
- the cutout (2) is then driven between the belt (1) and a motorized transverse roller (6).
- a belting module (7) ensures the separation of the two blanks (100, 200) of the cutout (2).
- the purpose of the equipment is to detach and separate, parallel to a predefined distance, the cutout (2) cardboard made up of two or three pieces held in them by breakable zones (160).
- a belt-retaining device (7) realigns the cardboard cut-outs (100, 200) in parallel with the suction mat (1) and ensures also the correct pre-programmed distance of the cutouts (100, 200) between them.
- the pressure rollers (6) slow down while the front blank (200) of the cardboard blank (2) continues to advance at the same speed as the suction belt (1) and is kept under pressure by the pressure rollers (3 to 5 ) on the mat (1).
- the rollers (6) accelerate to return at the same speed as the belt (1) at a very precise moment, determined beforehand by the separation length of the two cutouts (100, 200).
- the separate blanks (100, 200) advance to the belting module (7).
- the blanks (100, 200) are then realigned by pushing and retaining the straight edges of the two cardboard blanks (100, 200).
- a motorized toothed belt provided with a welded cleat and synchronized with the advance movement of the blanks (100, 200), ensures braking and acceleration of the blanks (100, 200) on the suction mat (1), which also allows to finalize with precision, the spacing of the two blanks (100, 200).
- the belt retractor module (7) consists of two belt carriages mounted in parallel.
- the two notched belts are motorized by a splined shaft with ball bushing, allowing lateral adjustment of each carriage.
- Each of the toothed belts is fitted with a welded cleat.
- Each belt has a micro adjustment device, which allows the two tabs to be aligned in parallel or to make an angular correction of the cardboard cutouts.
- the settings for synchronizing the tabs / at the cutout position can be configured on the machine console.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Making Paper Articles (AREA)
Claims (8)
- Verfahren zur Herstellung einer Verpackung, die aus zwei Kartonböden und einem Fenster besteht, das sich an den Seitenflächen zwischen den Kartonböden erstreckt, wobei:- Kartonzuschnitte (2) hergestellt werden, indem aus einem Bogen zwei Teile (100, 200) ausgeschnitten werden, die der Form des ersten bzw. des zweiten Kartonbodens entsprechen und durch brechbare Verbindungsbereiche (160) verbunden sind- der Zuschnitt auf einem Förderband mit einem Paar motorisierter Walzen, die auf der Oberseite des Zuschnitts abgestützt sind, durchgeführt wird- eine der Walzen, die mit einem der Teile (200) in Kontakt steht, relativ zu der Walze, die mit dem anderen Teil (100) in Kontakt steht, verlangsamt wird, um das Abreißen der brechbaren Bereiche (160) zu bewirken- das Fenster (300) entfernt wird, um die Kanten an die entsprechenden Kanten der so neu positionierten Teile (100, 200) zu kleben.
- Verfahren zur Herstellung einer Verpackung nach Anspruch 1, dadurch gekennzeichnet, dass der Zuschnitt (2) so auf einem Förderband (1) abgelegt ist, dass die durch die brechbaren Bereiche (160) verlaufende Mittellinie senkrecht zur Bewegungsrichtung des Förderbandes (1) ausgerichtet ist, und dass die Druckwalzen quer angeordnet sind.
- Verfahren zur Herstellung einer Verpackung nach Anspruch 2, dadurch gekennzeichnet, dass die hintere Walze verlangsamt wird, um das Abreißen des Verbindungsbereiches (160) zu bewirken und einen Längsversatz zwischen den beiden Teilen (100, 200) zu erzeugen, die durch einen der Höhe des Fensters (300) entsprechenden Abstand getrennt sind.
- Verfahren zur Herstellung einer Verpackung nach Anspruch 1, dadurch gekennzeichnet, dass es einen Schritt des Neupositionierens der zwei Teile (100, 200) umfasst, die durch ein Neupositionierungsmodul getrennt sind, um die Neuausrichtung der zwei getrennten Teile (100, 200) zu gewährleisten.
- Vorrichtung zur Herstellung einer Verpackung, die aus zwei Kartonböden (100, 200) und einem transparenten Fenster (300) besteht, das sich an den Seitenflächen zwischen den Kartonböden (100, 200) erstreckt, dadurch gekennzeichnet, dass sie ein Förderband (1) und zwei Druckwalzen umfasst, deren Drehung gesteuert wird, um die Verlangsamung einer der Walzen, die mit einem der Teile (100) in Kontakt steht, relativ zu der Walze, die mit dem anderen Teil (200) in Kontakt steht, zu bewirken, um das Abreißen der brechbaren Bereiche (160) zu bewirken und die beiden Teile (100, 200) neu zu positionieren, indem sie um einen Abstand verschoben werden, der der Höhe des Fensters (300) entspricht, sowie ein Mittel zum Entfernen eines Fensters (300) und Kleben der Kanten an die entsprechenden Kanten der so neu positionierten Teile (100, 200).
- Vorrichtung zur Herstellung einer Verpackung gemäß dem vorhergehenden Anspruch, dadurch gekennzeichnet, dass sie ferner einen Entstapler zum Ablegen der Seiten auf dem Förderband und einen Entstapler zum Liefern der Fenster (300) umfasst.
- Vorrichtung zur Herstellung einer Verpackung nach Anspruch 5 oder 6, dadurch gekennzeichnet, dass sie ferner einen Umsetzer zum Neuausrichten der geschnittenen und neu positionierten Teile (100, 200) umfasst.
- Schachtel mit zwei Kartonböden, zwischen denen sich ein Kunststofffenster befindet, dadurch gekennzeichnet, dass sie aus einem Kartonzuschnitt (2) hergestellt ist, der aus einem Bogen gebildet ist, der aus zwei Teilen (100, 200) besteht, die der Form des ersten bzw. des zweiten Kartonbodens entsprechen und durch brechbare Verbindungsbereiche (160) verbunden sind, wobei die Herstellung nach dem Verfahren gemäß einem der Ansprüche 1 bis 5 durchgeführt wird.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR1655280A FR3052389B1 (fr) | 2016-06-09 | 2016-06-09 | Procede et equipement pour la fabrication d'un emballage et emballage ainsi realise |
| PCT/FR2017/051445 WO2017212176A1 (fr) | 2016-06-09 | 2017-06-08 | Procédé et équipement pour la fabrication d'un emballage et emballage ainsi réalisé |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3468882A1 EP3468882A1 (de) | 2019-04-17 |
| EP3468882B1 true EP3468882B1 (de) | 2020-05-20 |
Family
ID=57045079
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17734790.3A Active EP3468882B1 (de) | 2016-06-09 | 2017-06-08 | Verfahren und vorrichtung zum herstellen einer verpackung und so hergestellte verpackung |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US20190144160A1 (de) |
| EP (1) | EP3468882B1 (de) |
| CN (1) | CN109311562B (de) |
| FR (1) | FR3052389B1 (de) |
| WO (1) | WO2017212176A1 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11185058B2 (en) * | 2017-03-01 | 2021-11-30 | Alan J. Cohen | Ornament assembly |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2507155A1 (fr) * | 1981-06-05 | 1982-12-10 | Babey Marie Edith | Boite d'emballage ou de presentation realisee a partir d'une decoupe en matiere transparente et au moins une decoupe en carton |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2139626A (en) * | 1935-10-04 | 1938-12-06 | Specialty Automatic Machine Co | Paper container for fluid |
| US2143957A (en) * | 1937-04-27 | 1939-01-17 | Noel A Petter | Display package |
| US3372796A (en) * | 1967-01-13 | 1968-03-12 | Container Corp | Interchangeable cap for package |
| DE3737968A1 (de) * | 1987-11-07 | 1989-05-18 | Kohmann Gmbh Co Maschbau | Verfahren zur herstellung von folienzuschnitten fuer faltschachteln mit winkelfenstern bzw. solcher faltschachteln und entsprechende vorrichtung |
| ITBO20060214A1 (it) * | 2006-03-29 | 2006-06-28 | Gd Spa | Metodo per la produzione di materiale da sovraincarto e confezione dotata del materiale cosi' prodotto. |
| FR2899873B1 (fr) * | 2006-04-12 | 2008-07-11 | Otor Sa | Flan mono piece, caisse presentoir, procede et dispositif pour la fabrication d'une telle caisse a partir dudit flan |
-
2016
- 2016-06-09 FR FR1655280A patent/FR3052389B1/fr not_active Expired - Fee Related
-
2017
- 2017-06-08 US US16/308,787 patent/US20190144160A1/en not_active Abandoned
- 2017-06-08 EP EP17734790.3A patent/EP3468882B1/de active Active
- 2017-06-08 CN CN201780035164.XA patent/CN109311562B/zh active Active
- 2017-06-08 WO PCT/FR2017/051445 patent/WO2017212176A1/fr not_active Ceased
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2507155A1 (fr) * | 1981-06-05 | 1982-12-10 | Babey Marie Edith | Boite d'emballage ou de presentation realisee a partir d'une decoupe en matiere transparente et au moins une decoupe en carton |
Also Published As
| Publication number | Publication date |
|---|---|
| FR3052389A1 (fr) | 2017-12-15 |
| CN109311562B (zh) | 2020-06-02 |
| CN109311562A (zh) | 2019-02-05 |
| FR3052389B1 (fr) | 2018-05-18 |
| EP3468882A1 (de) | 2019-04-17 |
| WO2017212176A1 (fr) | 2017-12-14 |
| US20190144160A1 (en) | 2019-05-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0086153B1 (de) | Maschine zum Falten von Platten | |
| EP2007635B1 (de) | Schauschachtel mit stülpdeckel | |
| EP2240316A1 (de) | Verfahren und vorrichtung zur herstellung von schachteln aus einem satz von rohlingen | |
| EP3033223B1 (de) | Verfahren und vorrichtung zur anbringung von verstärkungen an einem kartonverpackungszuschnitt | |
| EP3038954B1 (de) | Verfahren zum transportieren und drehen flacher gegenstände | |
| EP1640146B1 (de) | Vorrichtung zum Zusammensetzen von Zuschnitten in einer Maschine zum Herstellen von Schachteln | |
| WO1999024245A1 (fr) | Procede et machine a barillet pour la mise en volume de caisses ou analogue a partir d'une decoupe a plat en carton | |
| EP1171355A1 (de) | Faltschachtel, zuschnitte, verfahren zur öffnung einer faltschachtel sowie verfahren und maschine zum herstellen von einer solchen faltschachtel | |
| EP0146482A1 (de) | Verfahren und Vorrichtung zum Anbringen von Griffen oder Versteifungselementen auf schlauchartigen Bändern | |
| EP1093433B1 (de) | Schachtel und kartonzuschnitt mit einem aufreisswandteil | |
| EP3526025B1 (de) | Vorrichtung und verfahren zur entfernung einer schachtel von einem dorn | |
| WO2015040332A1 (fr) | Flan de matiere en feuille avec languettes de centrage, boite et procede mettant en oeuvre un tel flan | |
| WO2017212176A1 (fr) | Procédé et équipement pour la fabrication d'un emballage et emballage ainsi réalisé | |
| WO2018069614A1 (fr) | Procede et dispositif de mise en forme d'un flan autour d'un mandrin | |
| EP3472056B1 (de) | Verfahren zur herstellung einer kartonschachtel | |
| EP1725393B1 (de) | Maschine und verfahren zur herstellung einer platte durch verwendung eines dorns | |
| FR2496052A1 (fr) | Procede et dispositif de fabrication d'une boite de presentation et boite ainsi obtenue | |
| FR3012800A1 (fr) | Emballage comprenant un element en materiau semi-rigide et des feuilles auto-scellantes de protection et de maintien des articles conditionnes | |
| WO1999024247A1 (fr) | Procede et machine a barillet pour la mise en volume de caisses tambour ou analogue a partir de decoupes en carton | |
| EP0387171A1 (de) | Verfahren zum Herstellen eines schlauchförmigen Verpackungskörpers, sowie damit erhaltene Verpackung und Vorrichtung für dieses Verfahren | |
| FR3077276A1 (fr) | Emballage de type pret a vendre realise en deux elements dont les fonds sont superposes. | |
| FR3012066A1 (fr) | Module de pliage pour machine de fabrication de plis courriers et machine obtenue | |
| CH435958A (fr) | Procédé pour l'encollage de flans en carton et appareil pour la mise en oeuvre de ce procédé | |
| WO2015192863A1 (fr) | Procede, dispositif de rotation d'objets plans, module et machine de traitement ainsi equipee | |
| EP1362689A2 (de) | Verfahren und Vorrichtung zum kontinuierlichen Aufrichten von Packungen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20181127 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R079 Ref document number: 602017017054 Country of ref document: DE Free format text: PREVIOUS MAIN CLASS: B65D0008000000 Ipc: B65D0005320000 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B65D 5/32 20060101AFI20191121BHEP Ipc: B31B 105/00 20170101ALI20191121BHEP Ipc: B31B 110/35 20170101ALI20191121BHEP Ipc: B65D 5/42 20060101ALI20191121BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20191213 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602017017054 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1272471 Country of ref document: AT Kind code of ref document: T Effective date: 20200615 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20200520 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200820 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200821 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200921 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200920 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200820 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1272471 Country of ref document: AT Kind code of ref document: T Effective date: 20200520 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602017017054 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200608 |
|
| 26N | No opposition filed |
Effective date: 20210223 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200608 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200630 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20200520 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20220518 Year of fee payment: 6 Ref country code: GB Payment date: 20220519 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20220523 Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20230630 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20230608 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230608 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230608 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250520 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250521 Year of fee payment: 9 |