EP3632582B1 - Verfahren zur multimodalen herstellung von metallbändern und -platten - Google Patents
Verfahren zur multimodalen herstellung von metallbändern und -platten Download PDFInfo
- Publication number
- EP3632582B1 EP3632582B1 EP19208335.0A EP19208335A EP3632582B1 EP 3632582 B1 EP3632582 B1 EP 3632582B1 EP 19208335 A EP19208335 A EP 19208335A EP 3632582 B1 EP3632582 B1 EP 3632582B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- plates
- slab
- rolling
- process according
- production
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/46—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling metal immediately subsequent to continuous casting
- B21B1/463—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling metal immediately subsequent to continuous casting in a continuous process, i.e. the cast not being cut before rolling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/46—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling metal immediately subsequent to continuous casting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B13/00—Metal-rolling stands, i.e. an assembly composed of a stand frame, rolls, and accessories
- B21B13/22—Metal-rolling stands, i.e. an assembly composed of a stand frame, rolls, and accessories for rolling metal immediately subsequent to continuous casting, i.e. in-line rolling of steel
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B2265/00—Forming parameters
- B21B2265/14—Reduction rate
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/02—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for lubricating, cooling, or cleaning
- B21B45/0203—Cooling
- B21B45/0209—Cooling devices, e.g. using gaseous coolants
- B21B45/0215—Cooling devices, e.g. using gaseous coolants using liquid coolants, e.g. for sections, for tubes
- B21B45/0218—Cooling devices, e.g. using gaseous coolants using liquid coolants, e.g. for sections, for tubes for strips, sheets, or plates
Definitions
- the present invention concerns a process for the continuous or batch production of hot rolled strips and plates, in a wide size range with high plant productivity and cost effectiveness and high product quality.
- EP 1558408 the so-called "cast-rolling" technology is used which unites the continuous casting of a thin slab with liquid core reduction (LCR) to a first roughing rolling step through a high-reduction mill (HRM) or roughing mill that achieves an intermediate product which, after a heating phase in an induction heater and subsequent descaling, is further processed in a second phase of finishing rolling.
- LCR liquid core reduction
- HRM high-reduction mill
- EP 1868748 teaches some improvements from the point of view of plant compactness and energy saving, providing that the continuous casting is directly connected with a rolling step in a single manufacturing step without solution of continuity. In practice there are no longer two separate rolling steps, roughing and finishing, but a single rolling step and the distance between the outlet of the continuous casting and the first stand of the rolling mill will not be greater than 50 m in order to limit the temperature losses of the slab.
- EP 1868748 also provides the production of plates only with "endless" mode and using the same cooling system used for coils, a solution which has proved to be not optimal for the production of plates since the "endless" mode works better for coils and the optimal cooling parameters for plates are significantly different from those for coils.
- the cast slab has a maximum thickness of 50 mm prior to the liquid core reduction that takes it to 40 mm and it undergoes a maximum thickness reduction of 3 mm performed by the pinch rolls located just downstream from the casting machine.
- a roughing mill is arranged just downstream from the casting machine to perform a slab thickness reduction up to 70%, but in case of problems along the subsequent rolling line said thickness reduction can temporarily be reduced down to zero.
- the preamble of claim 1 is based on DE 102011004245 .
- the aim of the present invention is therefore to provide a solution for the production of continuously hot rolled strips or plates with strip thickness from 0,6 mm to 12 mm and plate thickness from 12 mm to 50 mm or in any case half of whatever may be the slab thickness at the exit of the continuous caster with liquid core reduction, said thickness having a minimum value of 80 mm, with maximum width at least 2100 mm or whatever may be the maximum mould width foreseen, with plate and strip quality the same or better, lower energy consumption, lower impact on the environment, higher productivity and flexibility compared with the afore-mentioned prior art.
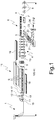
- a plant performing the process according to the present invention conventionally includes a continuous caster 1 followed at a certain distance by an induction heater 2, with a pendulum shear 3 therebetween, and then a rolling mill 4 followed by a rotary shear 5 and a run out table with a cooling device 6 and a pusher or pusher/piler 7 for plates and finally a high-speed shear 8 before the down coilers 9.
- caster 1 includes a mould followed by a curved liquid core reduction section to produce a slab with a minimum thickness of 80 mm, e.g. 100 mm x 2100 mm, at a casting speed up to 9 m/min. Said slab is then heated by the induction heater 2, comprising four coils in the illustrated example, prior to entering the finishing rolling mill 4, comprising up to seven stands as in the illustrated example, in which the slab undergoes a progressive thickness reduction with decreasing reduction rates, e.g. 58%; 52%; 47%; 43%; 40%; 35%; 30% and work rolls of larger diameter in the initial stands (e.g. the first two in the illustrated example).
- the induction heater 2 comprising four coils in the illustrated example, prior to entering the finishing rolling mill 4, comprising up to seven stands as in the illustrated example, in which the slab undergoes a progressive thickness reduction with decreasing reduction rates, e.g. 58%; 52%; 47%; 43%; 40%; 35%; 30% and work rolls of larger diameter in the initial stands (e
- the finishing rolling mill 4 may also include, at any position after the first two stands, cooling and/or heating devices (e.g. gas or induction heaters) located between the rolling stands so as to be able to better control the rolling conditions by adapting the temperature of the material being rolled to its specific characteristics and needs.
- cooling and/or heating devices e.g. gas or induction heaters
- the resulting strip is then cooled by the cooling device 6 and finally coiled by the down coilers 9 and cut by the high speed shear 8 when the coil has reached the intended weight.
- the slab is then cut into plates by the rotary shear 5 and said plates are moved out of the line by the pusher or pusher/piler 7, possibly after having been cooled in the first section of the cooling device 6.
- a first novel aspect of the present invention resides in the presence of a so-called "kiss pass" stand 10 between the continuous caster 1 and the pendulum shear 3, said stand 10 performing a thickness reduction of only about 10%, and in any case not more than 20%, therefore starting from a minimum reduction of about 8 mm, that has a metallurgical rather than a mechanical purpose.
- this minimum reduction is aimed at the optimisation of the crystalline structure of the slab surface by recrystallizing the coarse grains coming out of the caster in order to obtain smaller grains which are less prone to detach from each other in the actual rolling step carried out in the rolling mill 4.
- the plant also preferably includes, between caster 1 and stand 10, an additional induction heater 11, comprising two coils in the illustrated example, and a descaler 12 so as to: a) avoid the ductility draft temperature ranges, b) keep segregating elements in solution, and c) improve the result of the "kiss pass" reduction (similarly, a further descaler 13 preferably precedes the rolling mill 4).
- the presence in the cast alloy of low-melting elements e.g. copper and tin as in the steel produced from scrap in an EAF
- low-melting elements e.g. copper and tin as in the steel produced from scrap in an EAF
- the recomposition and refining of these grains achieved through this "light" reduction pass provides the double advantage of being able to: a) apply a higher reduction rate in the subsequent first actual reduction step without breaking the material at the surface, and b) obtaining strips/plates of the same high quality even using cheaper and lower-quality scrap, i.e. scrap containing higher concentrations of impurities such as copper and tin.
- the "kiss pass" stand 10 preferably includes working cylinders of smaller diameter with respect to the first stand in the rolling mill 4, since it must apply a minimum reduction while cooling the slab as little as possible, whereby a smaller arc of contact is sufficient and preferable with the advantage that tension stresses at the surface of the rolled stock are minimized.
- Another advantage obtained by arranging the "kiss pass" stand 10 between the continuous caster 1 and the pendulum shear 3, as mentioned above, is the creation of a "mechanical filter” between said two components so as to avoid any disturbance in caster 1 when the slab is cut by shear 3 in case of emergency if there is a cobble in the portion of plant downstream from shear 3.
- a second novel aspect of the present invention resides in the presence of an edger 14, i.e. a narrow face vertical rolling stand, that is preferably positioned immediately upstream from the "kiss pass" stand 10 and preferably preceded by an induction edge heater 15, i.e. a heater with C-shaped coils that heat only the edges of the slab.
- edger 14 could also be arranged immediately upstream from the rolling mill 4 together with its corresponding induction edge heater 15 that could be arranged adjacent to the induction heater 2 on any side thereof.
- edger 14 allows to recrystallize the slab edges, which are the coldest parts and therefore those most sensitive to the formation of cracks, to shape them for minimizing the tension stresses in the subsequent rolling step and to improve the width tolerances. Moreover, edger 14 can reduce the slab width on each side by up to 50 mm whereby a narrower strip/plate can be obtained without any intervention on the mould and thus without reducing the plant productivity.
- a third novel aspect of the present invention resides in the presence, between the "kiss pass" stand 10 and the induction heater 2, of an interconnecting furnace 16 suitable to allow the introduction/removal and the controlled advancement of slabs S.
- an interconnecting furnace 16 suitable to allow the introduction/removal and the controlled advancement of slabs S.
- a typical example is a gas-heated roller hearth furnace or walking beam furnace, usually about 30 m long, but other equivalent types of furnace can obviously be used.
- Said furnace 16 is immediately preceded by an additional pendulum shear 17 so that, as previously mentioned, the present plant not only makes possible to evacuate through a piler 18 re-usable slabs in the case of unavailability of the rolling mill 4, but also to select between the "endless” and “batch/combined” operating modes, as well as to load into the interconnecting furnace 16 (through a loading station 19) slabs at ambient temperature that have been bought on the market.
- the furnace 16 also acts as a buffer to hold and then subsequently load to the rolling line the hot slabs produced and stored in the furnace because of a cobble in the rolling mill 4, once the latter is available again.
- the "kiss pass” stand 10 is located between the continuous caster 1 and the additional pendulum shear 17 therefore it acts as a "mechanical filter", as mentioned above, also between said two components so as to avoid any disturbance in caster 1 when the slab is cut by shear 17 to select the "batch/combined" mode.
- the "kiss pass" stand 10 can be used as a first rolling pass upstream from furnace 16 exactly because it performs a thickness reduction of about 10%, and not more than 20% in any case. Such a reduction is much smaller than the thickness reduction in a roughing mill or in the first stand of a finishing rolling mill according to the prior art, which is in the order of 50-70%, that would result in an unacceptable length of furnace 16.
- the furnace must be sized to hold a slab of a weight corresponding to the weight of a finished coil of strip or a stack of plates to be produced in a batch production cycle, whereby an excessively thinned slab would have an unacceptable length to obtain the required weight.
- a fourth novel aspect of the present invention resides in the fact that the cooling device 6 may include a first cooling section capable of performing an ultra-fast cooling of the plates that corresponds to a quenching thereof. A subsequent tempering at a later working step will provide plates having a higher quality with respect to those produced with prior art plants whose cooling sections are only optimized for strips.
- a plate-specific cooling device 20 may be arranged offline such that the plates removed by the pusher or pusher/piler 7 undergo a multi-stage high-pressure cooling, i.e. each intense cooling stage is followed by an interval in which the temperature of the plate has the time to become substantially homogeneous prior to the successive cooling.
- the cooling device 20 may be followed by a tempering furnace 21, a further controlled cooling 22, a skin pass stand 23 and a roller leveller 24 for a complete treatment of the plates (either cooled in the specific cooling device 20 or in the above-mentioned ultra-fast cooling section of the cooling device 6).
- Another possibility is to provide a cooling device 6 that can be easily adjusted to a plate-specific setting, and in such a case it is obvious that the pusher/piler 7 or an additional pusher/piler 7' would be located between the cooling device 6 and coilers 9. In this way the cooling device 6 can be properly used for the cooling of both high-quality strips and high-quality plates.
- the above-described process according to the present invention is therefore suitable for producing both high-quality strips and high-quality plates, either in "endless” mode with no solution of continuity of the slab between caster 1 and rolling mill 4 (i.e. the entry speed of the rolling mill 4 is linked to the casting speed through the speed increase in the kiss pass stand), or in "batch/combined” mode with the slab that enters the rolling mill 4 which is disconnected from the slab in caster 1.
- Such a process can use as starting material also slabs coming from the interconnecting furnace 16, either loaded at ambient temperature through the loading station 19 or held at high temperature in furnace 16 itself when used as a buffer.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Metal Rolling (AREA)
- Continuous Casting (AREA)
Claims (10)
- Verfahren zur kontinuierlichen oder chargenweisen Herstellung von Bändern und Platten aus heißgewalztem Stahl mit einer Dicke von 0,6 mm bis 50 mm oder der halben maximalen Dicke einer gegossenen Bramme, umfassend das kontinuierliche Stranggießen (1) mit Reduzierung des flüssigen Kerns einer dünnen Bramme (S) mit einer minimalen Dicke von 80 mm, gefolgt von einem Aufheizen in einer Induktionsheizeinrichtung (2), einem ersten Schneiden (3) in dem Fall einer chargenweisen Herstellung, einem Fertigbearbeitungswalzen (4), einem kontrollierten Abkühlen (6) auf einem Auslauftisch, und einem zweiten Schneiden (5), gefolgt von einer Entnahme durch einen Schieber/Stapler (7) in dem Fall der Herstellung von Platten, oder einem Aufwickeln (9), gefolgt von einem abschließenden Schneiden (8) in dem Fall der Herstellung von Bändern, wobei es ferner ein anfängliches Walzen (10) mit einer Dickenreduzierung der Bramme (S) vor der Erwärmung in der Induktionsheizeinrichtung (2) umfasst, dadurch gekennzeichnet, dass die Dickenreduzierung der Bramme während des anfänglichen Walzens nur etwa 10% und jedenfalls nicht mehr als 20% beträgt, beginnend bei einer Dickenreduzierung von etwa 8 mm.
- Verfahren gemäß Anspruch 1, dadurch gekennzeichnet, dass dem anfänglichen Walzen (10) ein Aufheizen in einer zusätzlichen Induktionsheizeinrichtung (11) und eine Entzunderung (12) vorausgeht.
- Verfahren gemäß Anspruch 1 oder 2, dadurch gekennzeichnet, dass es ferner ein vertikales Walzen (14) der schmalen Seiten der Bramme mit einer möglichen Reduzierung der Breite von bis zu 50 mm auf jeder Seite umfasst, wobei das besagte vertikale Walzen (14) unmittelbar vor dem anfänglichen Walzen (10) oder dem Fertigbearbeitungswalzen (4) stattfindet.
- Verfahren gemäß dem vorhergehenden Anspruch, dadurch gekennzeichnet, dass dem vertikalen Walzen (14) ein Aufheizen der Brammenkanten in einer Induktionskantenheizeinrichtung (15) vorausgeht.
- Verfahren gemäß einem der Ansprüche von 1 bis 4, dadurch gekennzeichnet, dass in dem Fall der Herstellung von Platten das kontrollierte Abkühlen (6) ein ultraschnelles Abkühlen der Platten umfasst, welches einem Abschrecken derselben entspricht.
- Verfahren gemäß einem der Ansprüche von 1 bis 4, dadurch gekennzeichnet, dass es in dem Fall der Herstellung von Platten ferner die Entnahme (7) der Platten nach dem Fertigbearbeitungswalzen (4) und ein mehrstufiges Hochdruckabkühlen der Platten in einer plattenspezifischen Offline-Kühleinrichtung umfasst.
- Verfahren gemäß Anspruch 5 oder 6, dadurch gekennzeichnet, dass es ferner der Reihe nach ein Temperieren (21), ein kontrolliertes Abkühlen (22), ein Dressieren (23) und ein Nivellieren (24) der Platten nach deren ultraschnellem oder mehrstufigen Hochdruckabkühlen umfasst.
- Verfahren gemäß einem der Ansprüche 1 bis 4, dadurch gekennzeichnet, dass in dem Fall der Herstellung von Platten das kontrollierte Abkühlen (6) auf eine plattenspezifische Einstellung eingerichtet ist und die Entnahme (7') der Platten nach dem kontrollierten Abkühlen (6) erfolgt.
- Verfahren gemäß einem der Ansprüche von 1 bis 8, dadurch gekennzeichnet, dass es ferner einen Schritt des Nutzens einer Bramme (S) aus einem Verbindungs-Schmelzofen (16), der sich zwischen dem Walzgerüst (10) für das anfängliche Walzen und der Induktionsheizeinrichtung (2) befindet und derart dimensioniert ist, um eine Bramme (S) aufzunehmen mit einem Gewicht entsprechend dem Gewicht einer fertigen Wickelrolle eines Bandes oder eines Stapels von Platten, welche in einem chargenweisen Produktionszyklus hergestellt werden, als Ausgangsmaterial umfasst, wobei die besagte Bramme (S) entweder über eine Ladestation (19) bei Umgebungstemperatur in den Schmelzofen (16) geladen wird oder in dem Schmelzofen (16) selbst bei einer hohen Temperatur gehalten wird, wenn sie als Puffer verwendet wird.
- Verfahren gemäß einem der Ansprüche von 1 bis 9, dadurch gekennzeichnet, dass es ferner einen Schritt des Schneidens der Brammen (S) mit einer vierten Schneideinrichtung (17) umfasst, welche dem Verbindungs-Schmelzofen unmittelbar vorausgehend angeordnet ist, und das Entfernen derselben aus dem Verbindungs-Schmelzofen (16) mittels eines Staplers (18) in dem Fall von Störungen in einem dem besagten Verbindungs-Schmelzofen (16) nachgelagerten Bereich der Anlage.
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT102017000039423A IT201700039423A1 (it) | 2017-04-10 | 2017-04-10 | Impianto e procedimento per la produzione in molteplici modalita' di nastri e lamiere d’acciaio |
| PCT/IB2018/052459 WO2018189652A1 (en) | 2017-04-10 | 2018-04-09 | Plant and process for multi-mode manufacturing of metal strips and plates |
| EP18718524.4A EP3606681B1 (de) | 2017-04-10 | 2018-04-09 | Anlage und verfahren zur mehrmodenherstellung von metallbändern und -platten |
Related Parent Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP18718524.4A Division-Into EP3606681B1 (de) | 2017-04-10 | 2018-04-09 | Anlage und verfahren zur mehrmodenherstellung von metallbändern und -platten |
| EP18718524.4A Division EP3606681B1 (de) | 2017-04-10 | 2018-04-09 | Anlage und verfahren zur mehrmodenherstellung von metallbändern und -platten |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3632582A1 EP3632582A1 (de) | 2020-04-08 |
| EP3632582B1 true EP3632582B1 (de) | 2021-06-09 |
Family
ID=59521593
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19208335.0A Active EP3632582B1 (de) | 2017-04-10 | 2018-04-09 | Verfahren zur multimodalen herstellung von metallbändern und -platten |
| EP18718524.4A Active EP3606681B1 (de) | 2017-04-10 | 2018-04-09 | Anlage und verfahren zur mehrmodenherstellung von metallbändern und -platten |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP18718524.4A Active EP3606681B1 (de) | 2017-04-10 | 2018-04-09 | Anlage und verfahren zur mehrmodenherstellung von metallbändern und -platten |
Country Status (12)
| Country | Link |
|---|---|
| EP (2) | EP3632582B1 (de) |
| JP (2) | JP7095071B2 (de) |
| KR (1) | KR102435246B1 (de) |
| CN (1) | CN110573269B (de) |
| ES (2) | ES2887184T3 (de) |
| IT (1) | IT201700039423A1 (de) |
| MA (1) | MA47042B1 (de) |
| MX (2) | MX2019012216A (de) |
| MY (1) | MY199097A (de) |
| PH (1) | PH12019502312A1 (de) |
| RU (1) | RU2752592C2 (de) |
| WO (1) | WO2018189652A1 (de) |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114746196B (zh) * | 2020-05-22 | 2024-09-06 | 株式会社Tmeic | 切割位置控制装置 |
| IT202000016120A1 (it) * | 2020-07-03 | 2022-01-03 | Arvedi Steel Eng S P A | Impianto e procedimento per la produzione in continuo di nastri d’acciaio ultrasottili laminati a caldo |
| TWI899413B (zh) * | 2021-12-29 | 2025-10-01 | 義大利商阿維迪鋼鐵工程股份公司 | 用於連續生產熱軋超薄鋼帶之設備和方法 |
| WO2026022726A1 (en) * | 2024-07-24 | 2026-01-29 | Acciaieria Arvedi S.P.A. | Plant and process for the multiple-mode production of steel strips |
| WO2026028390A1 (en) * | 2024-08-01 | 2026-02-05 | Primetals Technologies Japan, Ltd. | Manufacturing method for rolled metal strip and rolling facility |
| EP4721889A1 (de) | 2024-10-04 | 2026-04-08 | Primetals Technologies Austria GmbH | Anlage und verfahren zum herstellen eines metallbandes im endlosbetrieb oder im batchbetrieb |
Family Cites Families (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5276952A (en) * | 1992-05-12 | 1994-01-11 | Tippins Incorporated | Method and apparatus for intermediate thickness slab caster and inline hot strip and plate line |
| CN1062196C (zh) * | 1994-10-20 | 2001-02-21 | 曼内斯曼股份公司 | 具有冷轧性能的带钢制造方法和设备 |
| US6309482B1 (en) * | 1996-01-31 | 2001-10-30 | Jonathan Dorricott | Steckel mill/on-line controlled cooling combination |
| NL1007739C2 (nl) * | 1997-12-08 | 1999-06-09 | Hoogovens Staal Bv | Werkwijze en inrichting voor het vervaardigen van een stalen band met hoge sterkte. |
| SK286108B6 (sk) * | 1996-12-19 | 2008-03-05 | Corus Staal B.V. | Spôsob výroby oceľového pásu alebo plechu |
| DE19713604A1 (de) * | 1997-04-02 | 1998-10-08 | Schloemann Siemag Ag | Einer Fertigstraße für stranggegossenes Bandmaterial vorgeordnetes positionsgeregeltes Stauchgerüst |
| KR100863557B1 (ko) * | 2002-07-31 | 2008-10-15 | 주식회사 포스코 | 폭 압연의 슬래브 뒤틀림 방지 장치 |
| ITMI20021996A1 (it) * | 2002-09-19 | 2004-03-20 | Giovanni Arvedi | Procedimento e linea di produzione per la fabbricazione di nastro a caldo ultrasottile sulla base della tecnologia della bramma sottile |
| BRPI0513754B1 (pt) * | 2005-04-07 | 2018-10-23 | Arvedi Giovanni | processo para fabricar tiras de metal de espessura, e, usina para fabricar tiras de metal |
| ITRM20050523A1 (it) * | 2005-10-21 | 2007-04-22 | Danieli Off Mecc | Processo e impianto per la produzione di nastro metallico. |
| DE102008020412A1 (de) * | 2007-08-24 | 2009-02-26 | Sms Demag Ag | Verfahren und Vorrichtung zum Herstellen eines Metallbandes durch Gießwalzen |
| DE102008003222A1 (de) * | 2007-09-13 | 2009-03-19 | Sms Demag Ag | Kompakte flexible CSP-Anlage für Endlos-, Semi-Endlos- und Batchbetrieb |
| IT1400002B1 (it) * | 2010-05-10 | 2013-05-09 | Danieli Off Mecc | Procedimento ed impianto per la produzione di prodotti laminati piani |
| DE102011004245A1 (de) * | 2010-10-07 | 2012-04-12 | Sms Siemag Ag | Verfahren und Vorrichtung zum Herstellen eines Metallbandes durch Gießwalzen |
| DE102013019698A1 (de) * | 2013-05-03 | 2014-11-06 | Sms Siemag Ag | Verfahren zur Herstellung eines metallischen Bandes |
| CN106244916B (zh) * | 2016-09-18 | 2018-05-08 | 武汉钢铁有限公司 | 高品质薄规格热轧合金工具钢及其csp生产工艺 |
-
2017
- 2017-04-10 IT IT102017000039423A patent/IT201700039423A1/it unknown
-
2018
- 2018-04-09 JP JP2020504467A patent/JP7095071B2/ja active Active
- 2018-04-09 MA MA47042A patent/MA47042B1/fr unknown
- 2018-04-09 KR KR1020197033306A patent/KR102435246B1/ko active Active
- 2018-04-09 ES ES19208335T patent/ES2887184T3/es active Active
- 2018-04-09 RU RU2019135817A patent/RU2752592C2/ru active
- 2018-04-09 MY MYPI2019005963A patent/MY199097A/en unknown
- 2018-04-09 CN CN201880024408.9A patent/CN110573269B/zh active Active
- 2018-04-09 MX MX2019012216A patent/MX2019012216A/es unknown
- 2018-04-09 EP EP19208335.0A patent/EP3632582B1/de active Active
- 2018-04-09 ES ES18718524T patent/ES2866154T3/es active Active
- 2018-04-09 WO PCT/IB2018/052459 patent/WO2018189652A1/en not_active Ceased
- 2018-04-09 EP EP18718524.4A patent/EP3606681B1/de active Active
-
2019
- 2019-10-09 PH PH12019502312A patent/PH12019502312A1/en unknown
- 2019-10-10 MX MX2024001387A patent/MX2024001387A/es unknown
-
2022
- 2022-05-20 JP JP2022082806A patent/JP2022107666A/ja active Pending
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| KR20190134776A (ko) | 2019-12-04 |
| CN110573269A (zh) | 2019-12-13 |
| IT201700039423A1 (it) | 2018-10-10 |
| ES2887184T3 (es) | 2021-12-22 |
| JP2022107666A (ja) | 2022-07-22 |
| MY199097A (en) | 2023-10-12 |
| CN110573269B (zh) | 2022-01-04 |
| ES2866154T3 (es) | 2021-10-19 |
| EP3606681A1 (de) | 2020-02-12 |
| RU2019135817A3 (de) | 2021-06-04 |
| EP3632582A1 (de) | 2020-04-08 |
| MA47042B1 (fr) | 2022-01-31 |
| RU2019135817A (ru) | 2021-05-11 |
| EP3606681B1 (de) | 2021-01-27 |
| KR102435246B1 (ko) | 2022-08-22 |
| JP2020516466A (ja) | 2020-06-11 |
| MX2024001387A (es) | 2024-02-27 |
| WO2018189652A1 (en) | 2018-10-18 |
| JP7095071B2 (ja) | 2022-07-04 |
| RU2752592C2 (ru) | 2021-07-29 |
| MA47042A1 (fr) | 2020-12-31 |
| PH12019502312A1 (en) | 2020-10-12 |
| MX2019012216A (es) | 2019-11-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3606681B1 (de) | Anlage und verfahren zur mehrmodenherstellung von metallbändern und -platten | |
| CN1103647C (zh) | 制造热轧钢带的方法和设备 | |
| EP2957358B2 (de) | Verfahren und anlage zur herstellung von flachgewalzten produkten | |
| RU2271256C2 (ru) | Способ и установка для изготовления лент и листов из стали | |
| KR100960096B1 (ko) | 중판 연속 주조 및 압연 방법 | |
| RU2491356C1 (ru) | Способ и устройство для получения микролегированной стали, в частности трубной стали | |
| TW200927313A (en) | Method and apparatus for producing strips of silicon steel or multi-phase steel | |
| EP0726101A1 (de) | Mitteldicken- und Mehrofen-Produktionslinie mit Brammenlagerung und -zuordnung | |
| CN112024595A (zh) | 一种薄带钢连铸连轧无头轧制方法及其轧制生产线 | |
| EP2580002B1 (de) | Walzverfahren für flache produkte und zugehörige walzanlage | |
| RU2750305C2 (ru) | Способ бесконечного изготовления смотанной горячекатаной полосы в комбинированной установке для разливки и прокатки, способ пуска комбинированной установки для разливки и прокатки и комбинированная установка для разливки и прокатки | |
| CN101304819A (zh) | 用于制造热轧制钢带的方法和用于执行该方法的联合浇铸轧制设备 | |
| CN101848776A (zh) | 用于连续作业、半连续作业和间歇作业的灵活而结构紧凑的csp设备 | |
| KR20150119437A (ko) | 주조 및 압연을 통한 금속 스트립 제조 방법 | |
| RU2537629C2 (ru) | Способ и устройство для изготовления металлической полосы бесслитковой прокаткой | |
| TWI615210B (zh) | 根據csp-槪念的設備以及用於操作此種設備的方法 | |
| JPH06320203A (ja) | 鋳造熱間圧延連続設備 | |
| RU2368438C2 (ru) | Компактная установка для получения горячекатаной стальной полосы | |
| RU2679159C1 (ru) | Способ производства особо тонких горячекатаных полос на широкополосном стане литейно-прокатного комплекса | |
| WO2000051755A1 (en) | Method of manufacturing hot rolled steel sheet using mini mill process | |
| WO2022043871A1 (en) | Process and apparatus for producing metallurgical products, in particular of the merchant type, in particular in an endless mode | |
| CN116511247A (zh) | 生产金属带材的方法及实施所述方法的生产设备 | |
| JPH07204708A (ja) | ホットコイルの製造方法 | |
| none | Discussion on rolling operations |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AC | Divisional application: reference to earlier application |
Ref document number: 3606681 Country of ref document: EP Kind code of ref document: P |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20200911 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20201222 |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: ARVEDI, GIOVANNI Inventor name: BIANCHI, ANDREA TEODORO |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AC | Divisional application: reference to earlier application |
Ref document number: 3606681 Country of ref document: EP Kind code of ref document: P |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1400039 Country of ref document: AT Kind code of ref document: T Effective date: 20210615 Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602018018513 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210909 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210910 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210909 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2887184 Country of ref document: ES Kind code of ref document: T3 Effective date: 20211222 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20211011 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: UEP Ref document number: 1400039 Country of ref document: AT Kind code of ref document: T Effective date: 20210609 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602018018513 Country of ref document: DE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| 26N | No opposition filed |
Effective date: 20220310 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20220409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220409 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220430 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220409 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220409 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230527 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20180409 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210609 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20250418 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250422 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20250530 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20250418 Year of fee payment: 8 Ref country code: IT Payment date: 20250402 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250425 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20250423 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20250403 Year of fee payment: 8 |