EP3656521A1 - Dispositif d'application de glacure en poudre pour la décoration de carreaux ou dalles céramiques - Google Patents
Dispositif d'application de glacure en poudre pour la décoration de carreaux ou dalles céramiques Download PDFInfo
- Publication number
- EP3656521A1 EP3656521A1 EP19202323.2A EP19202323A EP3656521A1 EP 3656521 A1 EP3656521 A1 EP 3656521A1 EP 19202323 A EP19202323 A EP 19202323A EP 3656521 A1 EP3656521 A1 EP 3656521A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- powder
- aforementioned
- enamel
- applicator device
- decoration
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B11/00—Apparatus or processes for treating or working the shaped or preshaped articles
- B28B11/04—Apparatus or processes for treating or working the shaped or preshaped articles for coating or applying engobing layers
- B28B11/044—Apparatus or processes for treating or working the shaped or preshaped articles for coating or applying engobing layers with glaze or engobe or enamel or varnish
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C—APPARATUS FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C19/00—Apparatus specially adapted for applying particulate materials to surfaces
- B05C19/04—Apparatus specially adapted for applying particulate materials to surfaces the particulate material being projected, poured or allowed to flow onto the surface of the work
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B11/00—Apparatus or processes for treating or working the shaped or preshaped articles
- B28B11/04—Apparatus or processes for treating or working the shaped or preshaped articles for coating or applying engobing layers
- B28B11/047—Apparatus or processes for treating or working the shaped or preshaped articles for coating or applying engobing layers by pooring, e.g. curtain coating
Definitions
- the present invention is part of the technical sector concerning the machinery used in the ceramic industry for the decoration of ceramic tiles or slabs.
- the powder glaze is introduced into a hopper arranged above the conveyor line with which the ceramic tiles or slabs are advanced.
- the hopper is extended transversely to the direction of feed, for example with a width equal to that of said tiles or ceramic slabs, and is inferiorly affected by a blade slit, suitably calibrated, from which emerges a so-called "dust curtain" which deposits on the underlying tile or ceramic slab in transit.
- hoppers which provide, in correspondence with the blade slit, a battery of shutters intended to be selectively controlled by an electronic control unit, on the basis of a memorized mapping, to dispense dosed quantities of enamel having unit width equal to that of the shutter, or to prevent its exit.
- a variant embodiment of the described solutions provides that the hopper deposits the powdered enamel on a mobile belt placed between the hopper itself and the underlying ceramic tile or slab; the same carpet then deposits on the latter, in a more downstream position.
- An object of the present invention is therefore to propose a powder glaze applicator device for the decoration of ceramic tiles or slabs which allows to overcome the technical limits of the known solutions and consequently increases the possibility of realizing designs or decorations of high complexity , with qualitatively optimal results.
- Another object of the invention is to provide an applicator device with high reliability and operating precision, without requiring too frequent maintenance interventions.
- Another object of the invention is to propose an applicator device in which there are no organs subject to the abrasive action of the enamel powder, so as to guarantee constant operating results over time and avoid expensive replacement of parts.
- a further object of the invention provides that the applicator device is made with relatively simple technical solutions, which can be easily integrated into normal production lines both as regards assembly and operation.
- a powder glaze applicator device for the decoration of ceramic tiles or slabs, with said powder glaze provided to reproduce a predetermined design or decoration, a variable quantity of the same powder glaze being intended to be deposited at selected portions of the surface of said ceramic tile or plate, with the latter moved horizontally along a conveyor line below said applicator device, which comprises:
- reference number 1 indicates, as a whole, a powder glaze applicator device S for the decoration of ceramic tiles or slabs PL.
- the powder glaze S must be suitably distributed, according to variable quantities, in correspondence with selected portions of the surface of said tile or ceramic plate PL, to reproduce a predetermined design or decoration D.
- the ceramic tile or plate PL with the design or decoration D still in the powder state will be introduced, according to the known technique, into a baking oven (not shown), in which the powder glaze S will be melted and incorporated permanently in the material of the tile or PL ceramic plate, becoming a single body with it.
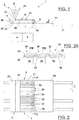
- the applicator device 1 comprises dispensing means 2, which comprise a tray 20 for containing the powder enamel S.
- the tray 20 is advantageously shaped like a hopper and is provided with a lower blade opening 21, extended transversely to the ceramic tile or plate PL, for the gravity release of the aforementioned powder enamel S.
- the tray 20, and the relative lower blade opening 21, have a width preferably equal to that of the ceramic tile or plate PL ( Fig. 2 ).
- a metering unit 3 in which a plurality of conveyor elements 30 are arranged, arranged side by side and oriented according to the transport direction F of said tile or ceramic plate PL, and able to define in their part above a mobile resting surface 31 of predefined width, preferably equal to or greater than those of the tray 20 as well as of the ceramic tile or plate PL.
- the mobile resting surface 31 is intended to receive the powder glaze S released by the blade opening 21 of the tray 20, so that a layer H of said powder glaze S continuously forms.
- Said layer H of powdered enamel S preferably, although not necessarily, has a uniform thickness.
- the blade opening 21 is advantageously arranged a few millimeters above the mobile resting surface 31, so as to limit the outflow of the powder enamel S.
- each of said conveyor elements 30 there are associated respective power members 32 ( Fig. 2A ), consisting for example of known electric stepper motors or the like, optionally provided with encoders, electronically controlled and capable of accurately performing rotations of amplitude predetermined angle, also very small.
- power members 32 consisting for example of known electric stepper motors or the like, optionally provided with encoders, electronically controlled and capable of accurately performing rotations of amplitude predetermined angle, also very small.
- the applicator device 1 also comprises an electronic processing unit 4, in which a drawing or decoration scheme D provided for the ceramic tile or plate PL is stored in digital form.
- this drawing or decoration scheme D comprises a two-dimensional matrix, the entire surface of the aforementioned ceramic tile or plate PL is divided into cells C with a predetermined unit surface, and to each cell C is associated with an element of this matrix.
- instructions relating to the presence or absence of enamel in the corresponding cell C, and possibly the quantity of enamel to be applied to the same, are recorded with appropriate coding.
- the entire matrix therefore contains sufficient information to reproduce the predetermined design or decoration D on the entire PL tile or slab.
- the applicator device 1 further comprises an actuation unit 5, electrically connected to the electronic processing unit 4 and controlled by it according to actuation sequences defined by a program residing therein, according to the aforementioned drawing or decoration scheme D.
- the unit drive 5 is provided to operate, in a suitable phase relationship with the advancement of the conveyor line T, the power members 32 of each conveyor element 30 present in said metering unit 3, as better specified below.
- the power members 32 can be activated simultaneously, to move all the conveyor elements 30 in a direction concordant with that of advancement of the same ceramic tile or plate PL, in a phase of formation of said layer H of enamel powder S, or selectively for imparting at least one conveyor element 30 a predetermined incremental advance, such that a metered quantity of powder glaze S is induced to fall, by gravity, onto the underlying ceramic tile or plate PL, in the underlying transit.
- one or more longitudinal strips of said continuous layer H are made to advance more, by a predetermined quota, with respect to the front of the continuous layer H, until it exceeds the front limit of the mobile resting surface 31, so that predetermined quantities of glaze fall onto the ceramic tile or plate PL and, at the end of the phase, in each of the aforementioned cells C of the same, the quantity of glaze is deposited in powder S, with the necessary thickness, in accordance with the provisions of the aforementioned cell matrix for the realization of the predetermined design or decoration D ( Fig. 8 ).
- each conveyor element 30 can be operated with adjustable speed, so as to deposit, in the unit of time, different quantities of enamel in powder form on the cell C of tile or slab PL.
- the said plurality of conveyor elements 30 is constituted by a series of belts 33, wound in a closed loop on a respective pair of pulleys 34, 35.
- Each belt 33 has a section such that its external side 33E is flat and of a width not exceeding that of one of the aforementioned cells C of the matrix ( Fig. 2A ).
- the belts 33 are mutually close to each other in sufficient numbers to cover at least the width of said ceramic tile or plate PL, and their upper horizontal branches are adapted to define said mobile resting surface 31.
- the relative electric motors 32 are associated with the downstream pulleys 35, and are preferably contained within them, without protruding laterally (see again Fig. 2A ).
- a collection plate 36 is provided, positioned immediately below said upper horizontal branches of the belts 33, intended to retain any powder enamel S drawn between one belt 33 and the other avoiding the fall on the underlying PL ceramic tile or plate ( Fig. 1 ).
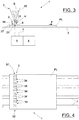
- the said plurality of conveyor elements 30 is constituted by a drum 37 with a horizontal axis formed by disks 38 side by side and mutually close together, in sufficient number to cover at least the width of said ceramic tile or plate PL ( Fig. 4 ).
- each disk 38 is not greater than the width of one of the aforementioned cells C of the matrix, while the mobile resting surface 31 is constituted by an upper portion of the circumference of said drum 37.
- each disc 38 (not shown in the figures) is preferably contained within it, without protruding laterally.
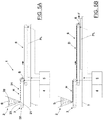
- an intermediate horizontal belt 6 is provided between the aforesaid metering unit 3 and the underlying ceramic tile or plate PL.
- the intermediate belt 6 extends longitudinally for a length greater than or equal to that of the ceramic tile or slab PL, is provided with actuator means - not shown as having a known structure - independent of those which actuate the conveyor elements 30 and the conveyor line T, and is intended to be operated in advance in phase relation with the metering unit 3, to receive the entire design or decoration D constituted by the enamel powder S supplied by the same metering unit 3 on its upper branch 6S Fig. 5A ), then in phase relation with the transport line T of the ceramic tile or plate PL, to transfer said design or decoration D to the latter ( Fig. 5B ).
- Fig. 6 schematically illustrates an optional divider unit 7, associated with the metering unit 3, with the latter indifferently of the type with belts 33 (as illustrated by way of example) or drum 37.
- the partitioning device 7 is positioned in the area of the conveyor elements 30 where the aforementioned gravity fall of the powder enamel S takes place, and comprises at least one nozzle 70 for ejection of compressed air for each of said conveyor elements 30, which can be operated in relation to phase with the activation of the latter to reduce the amount of falling enamel powder S, directing an excess part Se towards a recovery tile 71 suitably arranged nearby.
- the battery of nozzles 70 is arranged under the conveyor elements 30, in the space between these and the transiting tile or ceramic slab PL; the ejection of compressed air occurs towards the front with respect to the motion of the latter, and slightly upwards, so that said excess part of enamel powder S can be directed and collected by the aforementioned recovery tile 71.
- a very advantageous aspect lies in the fact that the powdered enamel is not induced to pass through metering elements such as shutters and the like, necessarily of small if not very small dimensions, and therefore subject to clogging and wear, consequently high reliability and precision of operation, without requiring frequent maintenance.
- the embodiments of the powder glaze applicator device are relatively simple for those skilled in the art, easy to construct and can be easily integrated into normal production lines, both as regards assembly and operation.
Landscapes
- Engineering & Computer Science (AREA)
- Structural Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Mechanical Engineering (AREA)
- Devices For Post-Treatments, Processing, Supply, Discharge, And Other Processes (AREA)
- Finishing Walls (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT102018000009274A IT201800009274A1 (it) | 2018-10-09 | 2018-10-09 | Dispositivo applicatore di smalto in polvere per la decorazione di piastrelle o lastre ceramiche |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3656521A1 true EP3656521A1 (fr) | 2020-05-27 |
| EP3656521B1 EP3656521B1 (fr) | 2022-08-24 |
Family
ID=64755648
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19202323.2A Active EP3656521B1 (fr) | 2018-10-09 | 2019-10-09 | Dispositif d'application d'émail en poudre pour la décoration de carreaux ou dalles céramiques |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP3656521B1 (fr) |
| ES (1) | ES2929446T3 (fr) |
| IT (1) | IT201800009274A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112372810A (zh) * | 2020-10-13 | 2021-02-19 | 陈国奇 | 一种瓷瓶自动涂釉装置 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH329122A (fr) * | 1955-10-17 | 1958-04-15 | Changewood Corp | Procédé pour déposer des éléments fibreux sur une surface, et appareil pour la mise en oeuvre de ce procédé |
| EP2760594B1 (fr) * | 2011-09-26 | 2015-11-18 | SACMI Cooperativa Meccanici Imola Società Cooperativa | Dispositif et méthode de distribution de matériau solide en vrac |
-
2018
- 2018-10-09 IT IT102018000009274A patent/IT201800009274A1/it unknown
-
2019
- 2019-10-09 EP EP19202323.2A patent/EP3656521B1/fr active Active
- 2019-10-09 ES ES19202323T patent/ES2929446T3/es active Active
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH329122A (fr) * | 1955-10-17 | 1958-04-15 | Changewood Corp | Procédé pour déposer des éléments fibreux sur une surface, et appareil pour la mise en oeuvre de ce procédé |
| EP2760594B1 (fr) * | 2011-09-26 | 2015-11-18 | SACMI Cooperativa Meccanici Imola Società Cooperativa | Dispositif et méthode de distribution de matériau solide en vrac |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112372810A (zh) * | 2020-10-13 | 2021-02-19 | 陈国奇 | 一种瓷瓶自动涂釉装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| ES2929446T3 (es) | 2022-11-29 |
| EP3656521B1 (fr) | 2022-08-24 |
| IT201800009274A1 (it) | 2020-04-09 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| RU2495383C2 (ru) | Способ и устройство для распределения твердых сыпучих материалов | |
| EP2892657B1 (fr) | Procédé et machine pour la décoration numérique de produits avec des matières granulaires et similaires | |
| EP2065150B1 (fr) | Dispositif pour fabriquer des veines continues ayant des modèles désirés et traversant l'épaisseur totale d'un produit et son procédé de préparation | |
| EP3622824B1 (fr) | Tamis pour matériau d'aspersion | |
| CN113165205B (zh) | 用于瓷砖的干法装饰的机器 | |
| WO2019171166A1 (fr) | Machine et procédé pour le compactage d'un matériau en poudre | |
| EP3656521B1 (fr) | Dispositif d'application d'émail en poudre pour la décoration de carreaux ou dalles céramiques | |
| EP2318189B1 (fr) | Système de charge de presses pour produits en céramique | |
| CN113165206A (zh) | 在厚度上装饰陶瓷板的方法 | |
| EP0492733B1 (fr) | Dispositif et méthode pour la fabrication de carreaux en céramique | |
| CN112805129A (zh) | 用于将粒状材料给送至用于生产板或砖的设施的设备和方法 | |
| EP0941826A2 (fr) | Méthode pour la fabrication d'un carreau décoré , dispositif correspondant pour l'alimentation des moules de pressage et carreau ainsi obtenu | |
| EP0940235A2 (fr) | Dispositif pour la production de carreaux avec différentes colorations | |
| EP1802430B1 (fr) | Appareil servant a repartir, dans une couche mince, un melange a base de ceramique ou pierre agglomeree | |
| EP1905563A2 (fr) | Dispositif pour remplir la cavité d'un moule avec un matériau en poudre et dalle obtenue selon un procédé de pressage de matériau en poudre | |
| EP1773553B1 (fr) | Installation pour l'apport d'une double couche de poudre ou de materiau granulaire dans la cavite d'un moule pour la production de carreau de ceramique | |
| EP1358983B1 (fr) | Dispositif pour le remplissage des moules d'une presse pour la fabrication des carreaux | |
| EP1225016A2 (fr) | Procédé pour le remplissage des moules d'une presse utilisée dans la fabrication de carreaux en céramique, moyens de mise en oeuvre correspondants et carreaux ainsi fabriqués | |
| CN121152713A (zh) | 在陶瓷制品上分配粉末产品的装置 | |
| IT201800001893A1 (it) | Macchina per la preparazione e la distribuzione a disegno di polveri per la produzione di piastrelle e lastre con decori a tutto spessore | |
| RU2755189C1 (ru) | Машина и способ уплотнения порошкового материала | |
| HK1054526A1 (en) | Tile forming equipment | |
| CN121079187A (zh) | 用于在陶瓷制品上分配粉末状产品的设备 | |
| ITMO980223A1 (it) | Dispositivo per l'alimentazione di una cavita' di formatura di unostampo per prodotti ceramici | |
| ITBO20060351A1 (it) | Metodo per l'applicazione di prodotti granulari e/o polverulenti su un articolo, e dispositivo che attua tale metodo |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20201127 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B05C 19/04 20060101ALI20220315BHEP Ipc: B28B 11/04 20060101AFI20220315BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20220419 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1513343 Country of ref document: AT Kind code of ref document: T Effective date: 20220915 Ref country code: DE Ref legal event code: R096 Ref document number: 602019018594 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2929446 Country of ref document: ES Kind code of ref document: T3 Effective date: 20221129 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20220824 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20221226 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20221124 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1513343 Country of ref document: AT Kind code of ref document: T Effective date: 20220824 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20221224 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20221125 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602019018594 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20221031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221009 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221031 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221024 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230503 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221031 |
|
| 26N | No opposition filed |
Effective date: 20230525 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20221009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20191009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20231009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20231009 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220824 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20251028 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20251105 Year of fee payment: 7 |