EP4005757A1 - Procédé et installation de fabrication de panneaux de matière - Google Patents
Procédé et installation de fabrication de panneaux de matière Download PDFInfo
- Publication number
- EP4005757A1 EP4005757A1 EP21203626.3A EP21203626A EP4005757A1 EP 4005757 A1 EP4005757 A1 EP 4005757A1 EP 21203626 A EP21203626 A EP 21203626A EP 4005757 A1 EP4005757 A1 EP 4005757A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- composite strand
- profiling
- continuous press
- material panels
- coating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N3/00—Manufacture of substantially flat articles, e.g. boards, from particles or fibres
- B27N3/08—Moulding or pressing
- B27N3/18—Auxiliary operations, e.g. preheating, humidifying, cutting-off
- B27N3/183—Forming the mat-edges, e.g. by cutting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N3/00—Manufacture of substantially flat articles, e.g. boards, from particles or fibres
- B27N3/08—Moulding or pressing
- B27N3/18—Auxiliary operations, e.g. preheating, humidifying, cutting-off
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27C—PLANING, DRILLING, MILLING, TURNING OR UNIVERSAL MACHINES FOR WOOD OR SIMILAR MATERIAL
- B27C5/00—Machines designed for producing special profiles or shaped work, e.g. by rotary cutters; Equipment therefor
- B27C5/08—Rounding machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27D—WORKING VENEER OR PLYWOOD
- B27D3/00—Veneer presses; Press plates; Plywood presses
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27D—WORKING VENEER OR PLYWOOD
- B27D3/00—Veneer presses; Press plates; Plywood presses
- B27D3/04—Veneer presses; Press plates; Plywood presses with endless arrangement of moving press plates, belts, or the like
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27D—WORKING VENEER OR PLYWOOD
- B27D5/00—Other working of veneer or plywood specially adapted to veneer or plywood
- B27D5/003—Other working of veneer or plywood specially adapted to veneer or plywood securing a veneer strip to a panel edge
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27M—WORKING OF WOOD NOT PROVIDED FOR IN SUBCLASSES B27B - B27L; MANUFACTURE OF SPECIFIC WOODEN ARTICLES
- B27M1/00—Working of wood not provided for in subclasses B27B - B27L, e.g. by stretching
- B27M1/08—Working of wood not provided for in subclasses B27B - B27L, e.g. by stretching by multi-step processes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N3/00—Manufacture of substantially flat articles, e.g. boards, from particles or fibres
- B27N3/02—Manufacture of substantially flat articles, e.g. boards, from particles or fibres from particles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N3/00—Manufacture of substantially flat articles, e.g. boards, from particles or fibres
- B27N3/08—Moulding or pressing
- B27N3/24—Moulding or pressing characterised by using continuously acting presses having endless belts or chains moved within the compression zone
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N5/00—Manufacture of non-flat articles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N7/00—After-treatment, e.g. reducing swelling or shrinkage, surfacing; Protecting the edges of boards against access of humidity
- B27N7/005—Coating boards, e.g. with a finishing or decorating layer
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/08—Accessory tools, e.g. knives; Mountings therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/32—Discharging presses
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/34—Heating or cooling presses or parts thereof
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B5/00—Presses characterised by the use of pressing means other than those mentioned in the preceding groups
- B30B5/04—Presses characterised by the use of pressing means other than those mentioned in the preceding groups wherein the pressing means is in the form of an endless band
- B30B5/06—Presses characterised by the use of pressing means other than those mentioned in the preceding groups wherein the pressing means is in the form of an endless band co-operating with another endless band
Definitions
- the invention relates to a process for the production of material panels, in which particles are pressed in a continuous press between two circulating belts with the supply of heat to form a composite strand and the composite strand emerging from the continuous press is then cut into material panels of the desired size and with a profiling process to achieve a non-rectangular material plate cross-section.
- the invention also relates to a system for producing material panels with a heatable continuous press, a cutting device for producing material panels from a composite strand of pressed particles emerging from the continuous press, and a profiling device for achieving a non-rectangular material panel cross-section.
- Material boards are primarily understood to mean wood material boards that have already been produced in a preferably continuous press and subsequently cut with saws.
- Chipboard, MDF or OSB boards come into consideration here, with the particles mentioned in the introduction then essentially being wood fibers or wood chips that have been provided with a binding agent.
- other lignocellulosic materials for example the fibers of annual plants (e.g. from rice straw) have also been used for pressing material boards.
- material boards can also be insulating boards, gypsum boards, plastic boards or other material boards, the particles of which have been pressed by means of circulating belts in a continuous press with the application of heat. Such a press is at the Applicant marketed with the name ContiRoll.
- Binding agents are usually added to the particles before the continuous press, so that the material panels have a high level of stability.
- the composite strand of the possible particles mentioned which is produced in this way in the continuous press and emerges from the continuous press can, of course, be described as clearly flat in cross-section in the context of the production of material panels by subsequent cutting processes. As a rule, the height of the composite strand emerging from the press is not even a hundredth of its width.
- the profiling process mentioned in the preamble is primarily a contouring, in particular at the edge of a material panel, which can be reached by cutting or milling tools. However, within the scope of the invention, the profiling should not be limited to the edge.
- coatings are also known for chipboard or MDF boards. Coatings made of (resin-soaked) paper, linoleum or plastic foils are mentioned here as examples.
- the finished panels often have similar edge shapes. Such panels are found, for example, in the furniture industry, where, depending on customer requirements, such edge shapes are incorporated into the material panels using cutting or milling tools.
- the object of the invention is to simplify the process for producing profiled material panels.
- the object is achieved by the features of the first claim and in particular by the fact that the profiling process takes place before the material panels have cooled to ambient temperature.
- the profiling can already be carried out on the edges of the composite strand, which is later cut into material panels, as long as this has not yet cooled down.
- the material panels at least do not have to be reprofiled on the side that was previously the longitudinal side of the composite strand.
- the trimming device and the profiling device can be combined into one processing unit.
- One - as is customary today - later-acting assembly group for profiling can be omitted completely or at least made significantly smaller.
- the profiling process takes place before the material panels have cooled to the mean temperature between the temperature of the composite strand at the outlet of the continuous press and the ambient temperature.
- the profiling of the composite strand can also be carried out without difficulty at temperatures above the temperature between the outlet temperature of the composite strand from the continuous press and the ambient temperature, without undesirable stresses subsequently occurring in the material panels.
- the profiling process is carried out between the exit of the composite strand from the continuous press and a saw for dividing the composite strand into individual sections.
- the individual sections which often already correspond to the later material plate size, then already have two profiled edges and no longer have to wait for the cooling process, for example in a star turner, before they are profiled.
- the time saving allows for either faster production or fewer post-processing machines.
- the profiling process preferably includes a partial round milling of the side edge of the composite strand.
- Partial round milling in particular is much more complex afterwards than if it is carried out directly behind the continuous press or a trimming device.
- the composite strand is coated on at least one side between the profiling process and the division of the composite strand into individual sections.
- coating can also take place before the composite strand is divided into individual sections, in a manner that simplifies the process.
- the coating preferably takes place with a paper or film lamination, the paper or film being connected, in particular glued, to at least one side of the composite strand.
- One side means the top or bottom of the flat composite strand.
- the coating material paper or film
- the coating material can, for example, be unwound from a roll and pressed onto the respective side.
- it is sprayed with an adhesive, for example.
- the new arrangement of the processing steps has the particular advantage that the bonded strand is still warm, which can have a very beneficial effect on the gluing process.
- the object is finally achieved in terms of system by the features of claim 8 and in particular by the fact that the profiling process is carried out by a profiling device which is arranged a maximum of 20 m behind the exit point of the composite strand from the continuous press.
- the expense for a separate profiling device after the composite strand has been divided into individual sections is eliminated or greatly reduced as a result.
- the profiling device can be combined with the trimming device after the press.
- the profiling device is located between the exit point of the composite strand from the continuous press and a saw for dividing the composite strand into individual sections.
- the profiling device already includes a rounding cutter.
- a coating device to be arranged between the profiling device and the saw.
- the coating device comprises a one-sided or two-sided unwind for papers or foils which can be connected to the composite strand as a coating.
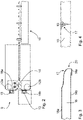
- FIG. 1 shows a plant for the production of a material panel 1 in a top view, wherein for reasons of clarity, both the representation of a composite strand and the representation of the cut material panel are omitted.
- the deflection arrows indicate that the installation in the top row continues in the bottom row.
- a composite strand is created between two circulating press belts by a mat of scattered particles that are in the Usually wetted with a binder, it is compacted under pressure and heat. In many cases, the particles are lignocellulosic fibers or wood chips, but should not be restricted to these within the scope of the invention.
- the mat emerges compacted as a composite strand at the outlet of the continuous press 2a with a temperature T2 and is brought to a trimming device 4 via only one conveyor track 3 (shown here as a roller carpet), where unclean edges or the desired width are cut with a trimming cutting tool 5.
- the composite strand retains its rectangular, flat cross-section.
- the profiling device 6 follows, in which, according to the invention, the composite strand is profiled, in particular at the edges, so that the composite strand no longer has a rectangular cross section.
- a partial round milling cutter 7 is provided for the edge 20 for this purpose.
- this profiling takes place well before the composite strand, which exits the press at a temperature T2, has reached the ambient temperature T1.
- the distance between the press outlet 2a and the profiling device is at least 20 m away and is in any case in front of a dividing saw, here in the form of a diagonal saw 11.
- the composite strand can even be so warm that it is even above that of the averaged Temperature is between the temperature at the outlet T2 from the continuous press 2a and the ambient temperature T1.
- the profiled composite strand is transported to a coating device 9 via a bridging conveyor 8 .
- a coating device 9 For the embodiment can be seen in particular considering the 2 at least one unwinding roll 12a with an upper coating material 18a, and alternatively or jointly at least one unwinding roll 12b for the lower one Coating Material 18b.
- Foils or (resin-impregnated) paper are customary and can be used as coating material.
- an upper paper web (upper coating material 18a) and a lower paper web (lower coating material 18b) is pulled off the unwinding rolls 12a, 12b, coated with adhesive by an adhesive supply 13 in each case and finally via pressable and possibly heatable pressure rollers 14 with the upper and lower side of the bonded strand.
- a finishing device for the coating 10 in which, for example, a wider upper coating web 18a is deflected around a rounded edge of the composite strand, for example, and the end is glued to the underside of the composite strand, for example overlapping with the lower coating material 18b.
- a wider upper coating web 18a is deflected around a rounded edge of the composite strand, for example, and the end is glued to the underside of the composite strand, for example overlapping with the lower coating material 18b.
- Such a (usually circular) saw runs at an angle over the continuous composite strand in order to thereby achieve a right-angled cut to the feed direction.
- FIG. 3 shows a typical embodiment of a gypsum plasterboard in section, with the figure focusing on the design of the edge 20, ie the profiling. In addition, it is indicated how an upper coating paper 18a and a lower coating paper 18b on the
- Composite strand 16 is bonded.
- the upper coating paper 18a is guided around the milled edge 20 in the finishing device for coatings 10 down to the underside of the composite strand 16 and on the underside overlaps with the lower coating paper 18b.
- the edge 20 itself was created beforehand in the profiling device 6 with a milling cutter 7 which is suitable for producing the desired curves 17 and bevels.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Wood Science & Technology (AREA)
- Forests & Forestry (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Dry Formation Of Fiberboard And The Like (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102020006861.8A DE102020006861A1 (de) | 2020-11-09 | 2020-11-09 | Verfahren und Anlage zur Herstellung von Werkstoffplatten |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP4005757A1 true EP4005757A1 (fr) | 2022-06-01 |
| EP4005757B1 EP4005757B1 (fr) | 2025-10-15 |
| EP4005757C0 EP4005757C0 (fr) | 2025-10-15 |
Family
ID=78332593
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP21203626.3A Active EP4005757B1 (fr) | 2020-11-09 | 2021-10-20 | Procédé et installation de fabrication de panneaux de matière |
Country Status (3)
| Country | Link |
|---|---|
| US (1) | US11794374B2 (fr) |
| EP (1) | EP4005757B1 (fr) |
| DE (1) | DE102020006861A1 (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2024191652A1 (fr) * | 2023-03-10 | 2024-09-19 | Louisiana-Pacific Corporation | Procédé de production de panneaux en bois finis en usine |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2357051A1 (de) * | 1973-11-15 | 1975-05-28 | Klessmann Ima Norte Maschfab | Verfahren und vorrichtung zum beschichten von holz- oder holzwerkstoffplatten mit abgerundeten kanten |
| WO2004089585A2 (fr) * | 2003-04-07 | 2004-10-21 | Fritz Egger Gmbh & Co. | Plaque de serrage et procede pour produire une plaque de serrage |
| DE102011015195A1 (de) * | 2011-03-25 | 2012-09-27 | Fritz Egger Gmbh & Co. Og | Verfahren und Vorrichtung zum Bekanten von Holzwerkstoffplatten sowie Holzwerkstoffplatten |
| DE102015107376A1 (de) | 2015-05-11 | 2016-11-17 | Dieffenbacher Maschinenfabrik Gmbh, Zaisenhausen | Vorrichtung und Verfahren zur Kühlung von Werkstoffplatten |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3577936A (en) * | 1969-01-10 | 1971-05-11 | William M Emery | Stool or leg rest |
| EP1322453B1 (fr) * | 2000-10-06 | 2008-09-10 | MiTek Holdings, Inc. | Systeme de formation d'elements de bois d'oeuvre a extremites arrondies |
| CN109500976B (zh) * | 2018-11-30 | 2021-06-22 | 大亚木业(江苏)有限公司 | 一种高强度低醛刨花板的生产工艺 |
| BE1026957B1 (nl) * | 2019-01-09 | 2020-08-14 | Ivc Bvba | Methode voor het vervaardigen van een vloer- of wandpaneel |
-
2020
- 2020-11-09 DE DE102020006861.8A patent/DE102020006861A1/de active Pending
-
2021
- 2021-10-20 EP EP21203626.3A patent/EP4005757B1/fr active Active
- 2021-11-07 US US17/520,692 patent/US11794374B2/en active Active
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2357051A1 (de) * | 1973-11-15 | 1975-05-28 | Klessmann Ima Norte Maschfab | Verfahren und vorrichtung zum beschichten von holz- oder holzwerkstoffplatten mit abgerundeten kanten |
| WO2004089585A2 (fr) * | 2003-04-07 | 2004-10-21 | Fritz Egger Gmbh & Co. | Plaque de serrage et procede pour produire une plaque de serrage |
| DE102011015195A1 (de) * | 2011-03-25 | 2012-09-27 | Fritz Egger Gmbh & Co. Og | Verfahren und Vorrichtung zum Bekanten von Holzwerkstoffplatten sowie Holzwerkstoffplatten |
| DE102015107376A1 (de) | 2015-05-11 | 2016-11-17 | Dieffenbacher Maschinenfabrik Gmbh, Zaisenhausen | Vorrichtung und Verfahren zur Kühlung von Werkstoffplatten |
Also Published As
| Publication number | Publication date |
|---|---|
| DE102020006861A1 (de) | 2022-05-12 |
| US20220143863A1 (en) | 2022-05-12 |
| EP4005757B1 (fr) | 2025-10-15 |
| US11794374B2 (en) | 2023-10-24 |
| EP4005757C0 (fr) | 2025-10-15 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69511242T2 (de) | Verfahren zum herstellen von lignocelluloseplatten | |
| EP2623282B1 (fr) | Procédé d'imprégnation de plaques de matière première | |
| EP2451655B1 (fr) | Panneau composite stratifié et procédé de production | |
| EP2514585B1 (fr) | Presse continue | |
| DE60319615T2 (de) | Verfahren zur Herstellung von gewölbten Möbelkomponenten, insbesondere Möbeltüren sowie Gegenstand, der mit diesem Verfahren hergestellt wurde | |
| EP2688722B1 (fr) | Procédé façonnage des bords de panneaux en matériau dérivé du bois | |
| EP3028829B1 (fr) | Installation pour la fabrication d'un panneau en bois agglomeré | |
| EP4005757B1 (fr) | Procédé et installation de fabrication de panneaux de matière | |
| EP1792723B1 (fr) | Procédé et dispositif destinés à la fabrication d'un panneau de construction léger | |
| EP2020195B1 (fr) | Procédé de fabrication d'un panneau pliable | |
| DE69510544T2 (de) | Gewelltes bauelement und verfahren zu seiner herstellung | |
| DE19957610A1 (de) | Verfahren, Anlage und taktweise arbeitende Prägepresse zur Herstellung von Holzwerkstoffplatten mit strukturierten Oberflächen | |
| EP2873522A1 (fr) | Plaque composite en matériau bois et son procédé de fabrication | |
| DE4306559C2 (de) | Verfahren zum kontinuierlichen Beschichten von Holzwerkstoffplatten | |
| WO2005009702A1 (fr) | Procede et dispositif pour produire des panneaux en materiau derive du bois | |
| EP3909733B1 (fr) | Procédé et système de fabrication d'une plaque déformée tridimensionnelle | |
| DE69600789T2 (de) | Verfahren und vorrichtung zur herstellung eines wabenförmigen kernes für wabenförmige verbundplatten | |
| EP1886778B1 (fr) | Procédé et dispositif destinés à la fabrication d'un panneau de laminé | |
| AT505855A1 (de) | Verfahren und vorrichtung zur herstellung von endlos-brettern | |
| WO2008055460A2 (fr) | Procédé et dispositif de réalisation en continu de préimprégnés | |
| DE19952271A1 (de) | Verfahren und Anlage zur Herstellung von überbreiten Furnierschichtplatten | |
| EP3653353A1 (fr) | Dispositif et procédé de revêtement d'une pièce | |
| WO2016180881A1 (fr) | Procédé et dispositif pour disperser un mat au cours de la fabrication de panneaux de matériaux et panneau de matériau | |
| EP3768522A1 (fr) | Panneau de postformage | |
| DE1703352A1 (de) | Parkettplatte sowie ein Verfahren und eine Vorrichtung zu ihrer Herstellung |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20220630 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20250605 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH Ref country code: CH Ref legal event code: F10 Free format text: ST27 STATUS EVENT CODE: U-0-0-F10-F00 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20251015 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502021008965 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| U01 | Request for unitary effect filed |
Effective date: 20251016 |
|
| U07 | Unitary effect registered |
Designated state(s): AT BE BG DE DK EE FI FR IT LT LU LV MT NL PT RO SE SI Effective date: 20251022 |
|
| U20 | Renewal fee for the european patent with unitary effect paid |
Year of fee payment: 5 Effective date: 20260107 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20251015 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20260115 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20251015 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20260115 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20260215 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20251015 |