EP4509328A1 - Procédé de fabrication d'un document de valeur et document de valeur - Google Patents
Procédé de fabrication d'un document de valeur et document de valeur Download PDFInfo
- Publication number
- EP4509328A1 EP4509328A1 EP24193933.9A EP24193933A EP4509328A1 EP 4509328 A1 EP4509328 A1 EP 4509328A1 EP 24193933 A EP24193933 A EP 24193933A EP 4509328 A1 EP4509328 A1 EP 4509328A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- substrate body
- film element
- ink
- front side
- digital printing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/40—Manufacture
- B42D25/45—Associating two or more layers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/20—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof characterised by a particular use or purpose
- B42D25/29—Securities; Bank notes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41M—PRINTING, DUPLICATING, MARKING, OR COPYING PROCESSES; COLOUR PRINTING
- B41M3/00—Printing processes to produce particular kinds of printed work, e.g. patterns
- B41M3/14—Security printing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/30—Identification or security features, e.g. for preventing forgery
- B42D25/324—Reliefs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/30—Identification or security features, e.g. for preventing forgery
- B42D25/36—Identification or security features, e.g. for preventing forgery comprising special materials
- B42D25/378—Special inks
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/40—Manufacture
- B42D25/405—Marking
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/40—Manufacture
- B42D25/405—Marking
- B42D25/425—Marking by deformation, e.g. embossing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/40—Manufacture
- B42D25/45—Associating two or more layers
- B42D25/455—Associating two or more layers using heat
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/40—Manufacture
- B42D25/45—Associating two or more layers
- B42D25/46—Associating two or more layers using pressure
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42D—BOOKS; BOOK COVERS; LOOSE LEAVES; PRINTED MATTER CHARACTERISED BY IDENTIFICATION OR SECURITY FEATURES; PRINTED MATTER OF SPECIAL FORMAT OR STYLE NOT OTHERWISE PROVIDED FOR; DEVICES FOR USE THEREWITH AND NOT OTHERWISE PROVIDED FOR; MOVABLE-STRIP WRITING OR READING APPARATUS
- B42D25/00—Information-bearing cards or sheet-like structures characterised by identification or security features; Manufacture thereof
- B42D25/40—Manufacture
- B42D25/45—Associating two or more layers
- B42D25/465—Associating two or more layers using chemicals or adhesives
- B42D25/47—Associating two or more layers using chemicals or adhesives using adhesives
Definitions
- the invention relates to a method for producing a value document, such as a banknote, a check, a credit or other payment card, an identification card or the like, wherein a substrate body having a front and a back is provided as a web element, a film element is provided as a web element, and the film element is pressed against the front of the substrate body in a roll process, wherein the film element partially or completely covers the substrate body and is laminated to the substrate body.
- a value document such as a banknote, a check, a credit or other payment card, an identification card or the like
- a print image is transferred directly from a file in a control unit to a printing machine. In the digital printing process, no static printing form is required.
- Types of digital printing processes are electrophotography, laser printing or inkjet printing. What all types have in common is that the print image is transferred with low mechanical pressure or, for example, in the case of inkjet printing, even without contact (non-impact printing).
- a laser exposure unit writes a print image onto a photo exposure cylinder, where an electrostatic charge image is initially created.
- the electrically charged liquid ink is fed to the photo exposure cylinder via ink form rollers and colors the exposed areas.
- the then visible print image is transferred to a rubber blanket cylinder. and is completely transferred to the printing material, which is mounted on a counter-pressure cylinder. There it dries and solidifies immediately. After all the colors have been applied, the printing sheet is ready for further processing.
- the durability of this printing process is, however, problematic for security printing.
- Dry toner processes are also known, in which a liquid toner consisting of plastic (PET) particles and a dye is thermally fixed. However, it can be assumed that this process does not achieve the durability required for banknotes.
- PET plastic
- a constant challenge is to increase the security against forgery of a security document.
- this is mainly achieved through complex combinations of printing processes.
- These complex printing processes require many separate work steps when producing a single sheet of paper, which has a negative impact on the economic efficiency of the process.
- the invention is based on the object of specifying a method for producing a value document and a value document which improves the durability of the printed image and is at the same time more economically attractive than previously known solutions.
- a method for producing a value document such as a banknote, a check, a credit or other payment card, an identification card or the like.
- a substrate body having a front and a back side is provided as a web element.
- a film element is provided as a web element and the film element is pressed against the front side of the substrate body in a rolling process, wherein the film element at least partially covers the substrate body and is laminated to the substrate body.
- the substrate body is not designed as a printed sheet, but as a web element.
- the substrate body is therefore a film web that is pulled over rollers in a machine as a single web element and is processed there step by step - one work step follows the next on the same film web - the individual valuable documents are only separated from the film web in the last work step.
- the film element is also designed analogously as a web element.
- Polymer substrates such as PET substrates, paper substrates or combined paper and polymer substrates can be used as substrate bodies.
- the film element is applied to the substrate body in such a way that it at least partially covers the substrate body - the film element can therefore be applied to the entire surface of the substrate body, but it can also be applied in such a way that it does not cover the entire width of the substrate body (for example as a strip).
- the film element consists of PP, PET, PE, LDPE, LLDPE, PA, PC, POPP, PVC, PU, polyurethane acrylates, cellophane, UV-crosslinked lacquer layers (radically crosslinking or cationically crosslinking) or natural bipolymers.
- the film element can also be a mixture of one or more of the above-mentioned polymers.
- the film element is preferably transparent or translucent.
- the film element has a thickness of 2 ⁇ m to 40 ⁇ m, preferably from 2 ⁇ m to 12 ⁇ m, particularly preferably from 2 ⁇ m to 6 ⁇ m.
- a digital printing layer with an ink is printed onto the front of the substrate body so that the digital printing layer is embedded between the substrate body and the film element in the subsequent laminating step.
- the inks used for digital printing can be divided into three main categories: latex inks, solvent/eco-solvent inks (i.e. solvent-based or water-based inks) and UV-curing inks.
- the electrically charged liquid inks mentioned at the beginning are particularly preferred.
- the film element is laminated onto the substrate body in a roll process in a laminating step.
- film lamination processes are possible, in particular a pressure lamination process, a gap lamination process, or an air lamination process.
- the film element can be heated before it is applied to the substrate body, for example with a hot air blower and/or pressure can be applied - for example in a thermal lamination process; in the thermal lamination process, no adhesive is required for lamination.
- a wet adhesive (wet lamination process) or a dry adhesive (dry lamination process) can also be used to laminate the substrate body and the film element.
- a further digital printing layer is printed with the ink onto the back of the substrate body.
- a further film element is provided as a web element and pressed against the back of the substrate body in a roll process, whereby the further film element is laminated to the substrate body so that the further digital printing layer is embedded between the substrate body and the further film element.
- the method according to the invention relates to the production of a value document directly at the substrate manufacturer.
- the production of the value document according to the invention takes place directly in the roll process; i.e. the digital printing layer is printed directly onto the substrate body, which is designed as a web element - i.e. represents a roll product.
- the film element is also provided and laminated in the roll process as a web element, i.e. as a roll product. All process steps take place in the roll process, so that all process steps can be carried out in a single machine and in work steps that follow one another directly. This reduces the production effort, thus reducing costs, and therefore makes the process more economically attractive than previously known processes.
- the substrate body is printed with the digital printing layer using digital printing, for example using inkjet printing or liquid toner processes.
- Standard colors and effect colors can be used here.
- a liquid toner color similar to OVI (optically variable ink) can be used as an effect color. It preferably consists of a carrier liquid containing resin elements in which the pigments are embedded, and thus represents an electrically charged liquid color.
- the digital printing technology used also provides advantageous possibilities for individualization, because digital printing enables to individually design each individual value document on the film web using a roll process.
- each value document on the film web can contain a slightly different grid that functions as a digital watermark - 2D barcodes are also possible. But different motifs are also possible, even the numbering could be applied in the first printing step.
- the digital printing layer particularly preferably has a graphic coding that luminesces when illuminated with radiation from the UV range and is transparent in the entire visible spectral range.
- thermochromic, photochromic, piezochromic or magnetochromic features are also easier to implement within the composite of foil element, digital printing layer and substrate body, as the required durability is achieved due to the lamination that follows the printing. This means that thermochromic, photochromic, piezochromic or magnetochromic features can also be printed using the ink as a digital printing layer.
- the film element is embossed after the lamination step in a roll process, whereby a relief structure is created on the front, but this is not caused by a layer of color, in order to be able to carry out the embossing on the same film web in a roll process.
- the laminated substrate body is provided with appropriate microstructures by embossing rollers - a relief structure is created on the front.
- a final matting of the film element can preferably be carried out This embossing is done so that no greasy impression is created and so-called BPS capability is ensured (in a BPS system, the authenticity and circulation stability of valuable documents is checked).
- the embossing preferably provides the same or a similar tactile (not optical) impression as the gravure printing, which is not currently being carried out.
- the digital printing layer is particularly preferably applied using a raster print. An accurate registration of the embossing with the areas printed with the digital printing layer is possible.
- the embossing step can be carried out in the same machine on the same film web using a roll process as the previously explained process steps, which further reduces production costs and thus further improves the cost-effectiveness of the process.
- the film element is at least partially printed with an ink-receiving layer after the laminating step.
- This printing step is particularly preferably carried out using a roll process - i.e. on the same film web in the same machine, which in turn saves manufacturing costs.
- the ink-receiving layer can be applied to the entire surface of the value document, or only partially.
- a value document such as a banknote, a check, a credit or other payment card, an identification card or the like.
- the value document has a substrate body which has a front and a back, and a film element which at least partially covers the substrate body and is laminated in a roll process at least against the front of the substrate body.
- the value document has a digital printing layer which is printed with an ink on the front side of the substrate body, wherein the digital printing layer is embedded between the substrate body and the film element. It is understood that the value document can be modified in the same ways as the method for producing a value document already described.
- value documents can be produced using the method according to the invention for producing a value document:
- a so-called hybrid value document is created.
- a multi-color print is carried out as a digital print layer on a paper roll as the substrate body.
- the multi-color print has fluorescence, optically variable effect pigments, a 2D barcode and/or individual designs - the printed elements can differ from value document to value document on the paper roll.
- lamination takes place and thus the increased and necessary protection of the printing elements.
- This process example enables cost-effective production with short set-up times, less material required and lower hourly rates, so that this process is also suitable for short runs such as commemorative notes, numbering, or cost-effective subsequent numbering when continuous/gapless numbering is required.
- At least one of the printing processes used is digital printing - i.e. printing the digital print layer (in particular, numbering is applied).
- Digital printing particularly preferably produces the entire print image of each individual value document on the paper roll.
- a security document made from a paper substrate is laminated with a polymer film
- printing on roll goods is a It is a cost-effective option to produce banknotes that are very stable in circulation (e.g. they have low circulation values with low security) and/or it is also possible to produce small runs at low cost, which might not be worthwhile for the banknote printer.
- the hybrid film i.e. the value document, can also be printed at least partially with a transparent/translucent ink-receiving layer, e.g. to achieve a matting effect or a more appealing feel.
- a hybrid or polymer value document is provided.
- a multi-color print is carried out as a digital print layer on a roll-shaped substrate body.
- the multi-color print has fluorescence, optically variable effect pigments, a 2D barcode and/or individual designs.
- At least one of the printing processes used is digital printing, with which in particular a numbering is applied.
- lamination takes place, in which the film element is applied to the digital print layer, thus ensuring increased and necessary protection of the printing elements.
- Subsequent embossing is carried out using embossing rollers.
- the haptic structures are thus created by depressions embossed into the substrate body - and not by a structured color layer, as with embroidery, which is explicitly not carried out. This embossing complements a clearly perceptible haptic and can be used as a separate security element. Even after the substrate body has been laminated with the film element, the front can be printed again, for example at least partially with an ink acceptance layer.
- a polymer security document is produced.
- Digital printing on polymer films is a sensible option, especially for small runs of security documents, such as banknotes for island states. especially since an ink-receiving layer is printed at the same time in digital printing.
- Polymer films also include film composites.
- the digital print is embedded between film layers and is therefore extremely durable.
- Multilayer composites made of different polymer materials can be used (for example PET and BOPP); the outer film may only serve as protection. Films pre-treated with a print-receiving layer can also be used and are available at reasonable prices. Duplex or triplex composites are conceivable.
- a patch can also be integrated between the films.
- this printed and laminated roll product can optionally be embossed.
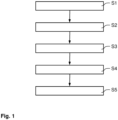
- Fig. 1 shows a flow chart of a method for producing a value document 1.
- a substrate body 2 which has a front side 3 and a back side 4, is provided as a web element.
- a digital printing layer 6 with an ink 10 is printed onto the front side 3 of the substrate body 2.
- a film element 8 is provided as a web element.
- the film element 8 is pressed against the front side 3 of the substrate body 2.
- the film element 8 is laminated to the substrate body 2, the digital printing layer 6 being embedded between the substrate body 2 and the film element 8.
- the film element 8 covers the substrate body 2 completely or only partially, for example in the form of a strip.
- the value document 1 can be embossed, a relief structure being created on the front side 3.
- the value document 1 can also be partially or fully printed with an ink-accepting layer in the fifth step S5.
- the embossing and the printing with the ink-accepting layer can also both be carried out one after the other on the same value document 1.
- All process steps S1 to S5 are carried out using the roll process.
- the substrate body 2 is, for example, unrolled from a roll and guided through a machine as a web element and processed one after the other in steps S1 to S5 without the machine having to be converted.
- the roll process thus proves to be particularly economical because the manufacturing effort is significantly reduced and the film element 8 applied as a lamination in the fourth step S4 improves the durability of the digital printing layer 6.
- Fig. 2 shows a value document 1, which was created using the procedure whose flow chart is shown in Fig. 1 is shown. However, the fifth step S5 in the production was omitted.
- the value document has the substrate body 2, the digital layer 6 and the film element 8, wherein the substrate body 2 has a front side 3 and a back side 4 and the digital printing layer 6 is printed on the front side 3. It is coated with the film element 8 and is thus protected from external influences and particularly resistant to circulation.
- Fig. 3 shows an ink 10 which is used in digital printing, with which the digital printing layer 6 is applied. It is an "electro ink", i.e. an electrically charged liquid ink with a liquid toner which contains electrically charged particles.
- a carrier liquid 12 there are particles 15 (“electro ink particle") in which pigments 16 are surrounded by a resin element 14.
- the particles 15 have particle sizes of 1 ⁇ m to 2 ⁇ m.
- the electrically charged liquid ink (ink 10) is used in digital printing and is not so durable that it would be suitable for banknote printing - due to the lamination of the digital printing layer 6 in the fourth step S4, however, the durability in circulation of the value document 1 is improved, so that this ink 10 is also made accessible for banknote printing - the digital printing layer 6 can no longer detach from the value document 1 in circulation due to the lamination with the film element 8.
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Health & Medical Sciences (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- General Health & Medical Sciences (AREA)
- Toxicology (AREA)
- Business, Economics & Management (AREA)
- Accounting & Taxation (AREA)
- Finance (AREA)
- Credit Cards Or The Like (AREA)
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102023122098.5A DE102023122098A1 (de) | 2023-08-17 | 2023-08-17 | Verfahren zur Herstellung eines Wertdokuments und Wertdokument |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP4509328A1 true EP4509328A1 (fr) | 2025-02-19 |
Family
ID=92300782
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP24193933.9A Pending EP4509328A1 (fr) | 2023-08-17 | 2024-08-09 | Procédé de fabrication d'un document de valeur et document de valeur |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP4509328A1 (fr) |
| CN (1) | CN119489635A (fr) |
| DE (1) | DE102023122098A1 (fr) |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO1995006564A1 (fr) * | 1993-09-03 | 1995-03-09 | Rexham Graphics Incorporated | Procede de production d'image a jet d'encre et element d'enregistrement |
| WO2002018151A1 (fr) | 2000-09-03 | 2002-03-07 | Hewlett-Packard Indigo B.V. | Impression d'images plastifiees |
| AT505007A4 (de) * | 2007-04-30 | 2008-10-15 | Oesterreichische Staatsdrucker | Verwendung eines leuchtstoffs als sicherheitsmerkmal, sicherheitsdruckfarbe, verfahren und vorrichtung zum überprüfen eines dokumentes sowie dokument und sicherheitsmerkmal |
| DE102007044482A1 (de) * | 2007-09-18 | 2009-03-19 | Giesecke & Devrient Gmbh | Sicherheitselement mit Tamper Evident-Effekt |
| DE102009020846A1 (de) * | 2009-05-12 | 2010-11-25 | Giesecke & Devrient Gmbh | Farbannahmeschicht mit Aussparung |
-
2023
- 2023-08-17 DE DE102023122098.5A patent/DE102023122098A1/de active Pending
-
2024
- 2024-08-09 EP EP24193933.9A patent/EP4509328A1/fr active Pending
- 2024-08-13 CN CN202411103499.9A patent/CN119489635A/zh active Pending
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO1995006564A1 (fr) * | 1993-09-03 | 1995-03-09 | Rexham Graphics Incorporated | Procede de production d'image a jet d'encre et element d'enregistrement |
| WO2002018151A1 (fr) | 2000-09-03 | 2002-03-07 | Hewlett-Packard Indigo B.V. | Impression d'images plastifiees |
| AT505007A4 (de) * | 2007-04-30 | 2008-10-15 | Oesterreichische Staatsdrucker | Verwendung eines leuchtstoffs als sicherheitsmerkmal, sicherheitsdruckfarbe, verfahren und vorrichtung zum überprüfen eines dokumentes sowie dokument und sicherheitsmerkmal |
| DE102007044482A1 (de) * | 2007-09-18 | 2009-03-19 | Giesecke & Devrient Gmbh | Sicherheitselement mit Tamper Evident-Effekt |
| DE102009020846A1 (de) * | 2009-05-12 | 2010-11-25 | Giesecke & Devrient Gmbh | Farbannahmeschicht mit Aussparung |
Also Published As
| Publication number | Publication date |
|---|---|
| DE102023122098A1 (de) | 2025-02-20 |
| CN119489635A (zh) | 2025-02-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE69117756T2 (de) | Verbesserungen für unterschriftsstreifen | |
| EP1156927B1 (fr) | Procede de fabrication de produits de securite multicouches et produit de securite fabrique selon ce procede | |
| EP3802144B1 (fr) | Procédé de fabrication d'un élément stratifié et d'un film stratifié ainsi qu'élément stratifié et film stratifié | |
| EP2430237B1 (fr) | Couche réceptrice d'encre pourvue d'un évidement | |
| EP2857218B1 (fr) | Procédé de création d'une caractéristique de sécurité avec des structures tactiles pour documents de valeur | |
| DE10255639A1 (de) | Sicherheitselement und Verfahren zur Herstellung desselben | |
| EP2590822B2 (fr) | Document de valeur avec une couche d'absorption transparente et avec une couche d'absorption opaque | |
| EP3441234A1 (fr) | Procédé de transfert de films à froid et film de transfert | |
| DE102010048240B4 (de) | Druckträgerverbundmaterial für Mehrfarbendruckkarten | |
| DE102015015908A1 (de) | Folien-Verbundsubstrat mit taktil erfassbaren Element | |
| EP1558448A1 (fr) | Document de valeur | |
| DE102023122098A1 (de) | Verfahren zur Herstellung eines Wertdokuments und Wertdokument | |
| EP1767377B1 (fr) | Feuilles polymériques pour marquage individuel, méthodes pour leur fabrication et produits resultants | |
| WO2011160781A2 (fr) | Procédé pour produire un document d'identification | |
| EP3256329B1 (fr) | Produit de valeur ou de sécurité et procédé de fabrication de celui-ci avec individualisation décentralisée | |
| EP3135495B1 (fr) | Élément de sécurité imprimé | |
| EP2878455B1 (fr) | Caractéristique de sécurité tactilement identifiable pour des documents de valeur | |
| EP2974877B1 (fr) | Procede de fabrication d'un document de valeur ayant un effet de transmission/réflexion visuelle | |
| EP3326833B1 (fr) | Impression en sérigraphie de couleurs à effet sur des documents de valeur | |
| DE102018115748A1 (de) | Verfahren und Vorrichtung zur Druckveredelung | |
| EP4219185A1 (fr) | Film, bande de film, document de valeur et procédé de fabrication | |
| DE10339065A1 (de) | Verfahren zur Herstellung von Ausweiskarten und dessen Produkt | |
| EP4520544A1 (fr) | Document de valeur et procédé de fabrication d'un document de valeur |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20250806 |