EP4520671A1 - Orales produkt in beutelform - Google Patents
Orales produkt in beutelform Download PDFInfo
- Publication number
- EP4520671A1 EP4520671A1 EP23196221.8A EP23196221A EP4520671A1 EP 4520671 A1 EP4520671 A1 EP 4520671A1 EP 23196221 A EP23196221 A EP 23196221A EP 4520671 A1 EP4520671 A1 EP 4520671A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- inclined transverse
- packaging material
- filling material
- travel
- seal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
- B65B9/10—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs
- B65B9/20—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs the webs being formed into tubes in situ around the filling nozzles
- B65B9/2056—Machines for packages of special type or form
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B29/00—Packaging of materials presenting special problems
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B51/00—Devices for, or methods of, sealing or securing package folds or closures; Devices for gathering or twisting wrappers, or necks of bags
- B65B51/10—Applying or generating heat or pressure or combinations thereof
- B65B51/26—Devices specially adapted for producing transverse or longitudinal seams in webs or tubes
- B65B51/30—Devices, e.g. jaws, for applying pressure and heat, e.g. for subdividing filled tubes
- B65B51/306—Counter-rotating devices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B51/00—Devices for, or methods of, sealing or securing package folds or closures; Devices for gathering or twisting wrappers, or necks of bags
- B65B51/10—Applying or generating heat or pressure or combinations thereof
- B65B51/22—Applying or generating heat or pressure or combinations thereof by friction or ultrasonic or high-frequency electrical means
- B65B51/225—Applying or generating heat or pressure or combinations thereof by friction or ultrasonic or high-frequency electrical means by ultrasonic welding
Definitions
- the present disclosure relates to an oral pouched product. It further relates to an apparatus for producing oral pouched products and a method for producing an oral pouched product.
- Pouched smokeless low-tobacco-containing products for oral use may contain added nicotine, i.e. nicotine in addition to the nicotine of the tobacco. Alternatively, they contain no added nicotine and the nicotine is provided solely by the tobacco in the product.
- US 4,703,765 discloses a device for packaging precise amounts of finely divided tobacco products, such as snuff tobacco or the like, in a tubular packaging material into which snuff portions are injected via a fill tube, the tubular packing material thereby having a vertical orientation. Downstream from the tube, sealing means are positioned for transverse sealing of the packaging material, as well as cutting means for severing the packaging material in the area of the transverse seal to thus form discrete or individual portion packages.
- finely divided tobacco products such as snuff tobacco or the like
- each final pouched product When manufacturing individual pouched smokeless products for oral use, they may be sealed and cut apart thereby forming rectangular "pillow shaped" pouched products.
- each final pouched product includes parallel transverse seals at opposite ends and a longitudinal seal orthogonal to the transverse seals. The seals must be of sufficient strength to preserve the integrity of the pouched product during use, though without disturbing the consumer's experience.
- An object of the present disclosure is to overcome or ameliorate at least one of the disadvantages of the prior art, or to provide a useful alternative.
- the present disclosure provides an oral pouched product according to claim 1.
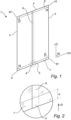
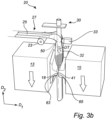
- the oral pouched product comprises a filling material and a saliva-permeable pouch of packaging material enclosing the filling material, the oral pouched product having two longitudinal sides extending in a longitudinal direction LD and two inclined transverse end sides extending in an inclined transverse direction ITD. At least one of the two longitudinal sides is a fold in the packaging material.
- the inclined transverse direction ITD is non-perpendicular to the longitudinal direction LD, which inclined transverse end sides are sealed edges forming inclined transverse end seals of the packaging material. Both the longitudinal sides may be folds in the packaging material.
- a pouch comprising two inclined transverse end sides which are sealed edges forming inclined transverse end seals may reduce the risk that the end seals become weakened during manufacturing.
- the end seal is inclined, the influence of the filling material when impacting the end seal during filling may be reduced since the impact force may be distributed over a larger surface area. Consequently, a stronger seal strength may be achieved in the inclined transverse end sides.
- the oral pouched product may have a shape that will be appreciated by the user. It will fit well in the mouth of the user, such as between the upper or lower gum and the lip.
- the oral pouched product as disclosed herein has a shape that may be easy to produce in an effective manner and may have relatively strong sealed ends.
- the filling material may be distributed in a suitable way.
- the two longitudinal sides may be opposite sides of the pouched product.
- the two longitudinal sides may be parallel.
- the two inclined transverse end sides may be opposite sides of the pouched product.
- the two inclined transverse end sides may also be parallel.
- the oral pouched product has the shape of a rhombus or a rhomboid.
- the filling material may comprise a smokeless tobacco or a tobacco-free material, which may be nicotine-containing or nicotine free.
- the filling material may thus contain an active agent which may be nicotine.
- the filling material may also be referred to as filling composition.
- the oral pouched product may comprise a longitudinal seal in the longitudinal direction LD.
- Longitudinal seals of pouched products facilitate the production of the pouched products.
- both longitudinal sides may be folds in the packaging material.
- a weak region may be present in the overlapping part as a result of some of a sealing agent or a material that provides sealability having been consumed during a first sealing step. Consequently, the strength of the seal may be reduced. This may affect the next sealing step when there is less sealing agent in the overlapping part of the longitudinal seal and the transverse seal. In the overlapping part, the strength of the seal may be weaker.
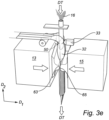
- the filling material will impact an inclined transverse seal, which is non perpendicular to a direction of travel of the packaging material during filling and sealing, since the impact force on the inclined transverse seal will be reduced compared to the impact force on a seal which is perpendicular to the direction of travel DT.
- the impact force on the inclined transverse seal will be reduced since the inclined transverse seal will be longer than a seal which is perpendicular to the direction of travel.
- the filling material will thus impact a larger area and the force will be spread over a larger area and will therefore be lower on a transverse inclined seal compared to a perpendicular seal. This may further result in an improved seal strength.
- the filler material may for example be pneumatically assisted in the supply into the pouched product and the seal may be damaged by the filling material impacting the end seal. Such problems may be avoided with the product of the disclosure.
- the longitudinal seal may be located between the two longitudinal sides. This location of the longitudinal seal provides an oral pouched product which provides a pleasant mouth comfort and mouthfeel.
- the longitudinal seal may be located centrally between the two longitudinal sides. This has been found to hinder deformation of the pouched product.
- the centrally located longitudinal seal may resist skewing of the pouched product.
- the oral pouched product may comprise two diagonally opposite corners, each may have an angle ⁇ of 30 to 70° and two diagonally opposite corners, each may have an angle ⁇ of 110 to 150°. ⁇ may be 180 minus ⁇ °.
- the angle 30 to 70° has been shown to provide a good filling performance of the filling material in the oral pouched product.
- the oral pouched product may have a rhombus form or a rhomboid form.
- the four sides of the oral pouched product may have a rhombus form or a rhomboid form.
- each of the two longitudinal sides may have a length of 20 to 45 mm and each of the two inclined transverse end sides may have length of 20 to 45 mm.
- the two longitudinal sides may be longer than the two inclined transverse end sides.
- the inclined transverse end seals may have a measured maximum value of shear seal strength of from 30 to 45 N, determined with the ASTM F88 method for seal strength. The method will be referred to below together with results achieved by the seal strength test. Different nonwoven materials than the one tested below in the Examples may obtain different values. Higher values may for example be obtained.
- the packaging material may comprise a nonwoven material.
- the nonwoven material may comprise cellulose fibres, such as regenerated cellulose fibres, and a sealing agent.
- the regenerated cellulose fibres may be viscose fibres or lyocell fibres.
- Sealing of the pouched product for oral use may for example be performed by means of heat sealing or by ultrasonic sealing. It may be desirable that the pouch material comprises a component, a sealing agent, which is reactive to the heat or ultrasonic energy, such that this component contributes to the sealing of the pouch.
- sealing agent refers to an adhesive substance, generally a polymer, such as a polymer having long chains, in solid form, such as powder, film or fibre, or as a foam, or in a liquid form, such as an emulsion, dispersion or solution, used for sealability between for example two nonwoven layers.
- the sealing agent may be a fibrous sealing agent or a non-fibrous sealing agent.
- fibrous sealing agent refers to thermoplastic fibres used for thermal sealing, e.g., of materials comprising fibres of a higher softening point or non-melting fibres.
- the fibrous sealing agent may be thermoplastic fibres.
- the thermoplastic fibres may be used for providing sealability, such as for heat sealing or ultrasoncic sealing.
- the thermoplastic fibres may be selected from the group consisting of polypropylene (PP), polyethylene (PE), polylactic acid (PLA), polyethylene terephthalate (PET), polyhydroxyalkanoate (PHA), polybutylene succinate (PBS) and any combination thereof.
- the fibres may be referred to as homofibres.
- the thermoplastic material may be bicomponent fibres, wherein one component of the fibres may be thermoplastic.
- Bicomponent fibres may be selected from PP/PE, e.g., with PP in the core and PE in the sheath, and PLA/co-PLA, e.g., with PLA in the core and co-PLA in the sheath.
- the bicomponent fibres may be combined with the thermoplastic homofibres mentioned herein.
- the non-fibrous sealing agent may be a polymer non-fibrous sealing agent.
- the polymer non-fibrous sealing agent may be selected from the group consisting of the polymers polypropylene (PP), polyethylene (PE), polylactic acid (PLA), polyethylene terephthalate (PET), polyhydroxyalkanoate (PHA), polybutylene succinate (PBS), vinyl acetate polymer, acrylate polymer, vinyl acrylate polymer, vinyl acetate ethylene copolymers, styrenebutadiene copolymers and vinyl acetate ethylene copolymers and any combination thereof.
- the polymer non-fibrous sealing agent may be thermoplastic.
- the polymer non-fibrous sealing agent may be selected from solution based sealing agents, liquid based sealing agents, liquid dispersions and adhesive.
- the heat applied or the ultrasonic energy will melt thermoplastic fibres or thermoplastic polymers, which will then solidify.
- the heat sealing or ultrasonic sealing may be used for thermal bonding of thermoplastic fibres or thermoplastic polymers. Further, when a non-thermoplastic non-fibrous sealing agent is used, a cross-linking reaction may be performed. The heat applied or the ultrasonic energy may contribute to the sealing of the non-thermoplastic non-fibrous sealing agent.
- a facilitated production may thus be attained for producing the oral pouch product.
- Seals in the form of heat seals made by heat sealing or ultrasonic sealing may be used for production of the oral pouched product.
- the inclined transverse seals may be sealed by heat sealing or ultrasonic sealing.
- the longitudinal seal may also be sealed by heat sealing or ultrasonic sealing. Heat sealing may be preferred for the sealing of the longitudinal seal.
- the step of filling may take place after an inclined transverse end seal of the pouch has been made.
- the inclined transverse end seal may still be warm or uncured and may be sensitive to the force from the filling material supplied and impacting the transverse end seal. Since the seal has an inclined transverse direction, the force from the filling material on the inclined transverse end seal will be lower compared to the force on an end seal in a perpendicular direction in relation to the direction of travel of the packaging material during filling and sealing.
- seals may be needle punching or by gluing with adhesive.
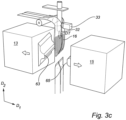
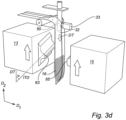
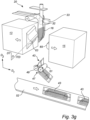
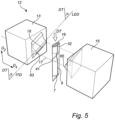
- the present disclosure provides an apparatus for producing oral pouched products, the oral pouched products comprising a packaging material and filling material enclosed by the packaging material, the apparatus comprising:
- Inclined transverse end seals of oral pouched products may be formed.
- the direction of travel DT is preferably substantially vertical.
- the direction of travel DT extends between the anvil and the horn.
- the direction of travel extends between the operation surface of the anvil and the operation surface of the horn.
- the first operation surface and the second operation surface may be sealing surfaces. Further, at least one of the first operation surface and the second operation surface may comprise a cutting portion for cutting a seal.
- the apparatus is used for producing oral pouched products.
- the oral pouched products may be produced by sealing and cutting a packaging material comprising a filling material.
- the sealing may be performed in an inclined transverse direction ITD which will be advantageous for the reasons explained above.
- the apparatus may comprise a forming unit for forming a tubular web of the web of the packaging material.
- a production step may be facilitated by the possibility to form a tubular web of the packaging material.
- the apparatus may comprise at least a second sealing device for making a longitudinal seal in a direction of travel DT.
- the longitudinal seal may extend in a direction parallel to the longitudinal side edges of the pouched product.
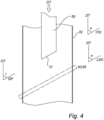
- the length extension direction LED may form an angle ⁇ of 30 to 70° with the direction of travel DT.
- the angle 30 to 70° has been shown to provide a good filling performance of the filling material in the oral pouched product.
- the oral pouched product has also shown improved sealing strength with angles of 30 to 70°.
- the angle ⁇ may be 35 to 65°.
- the filling material supply unit may comprise a dosing tube having a length extending in the direction of travel DT.
- the dosing tube may have a longitudinal axis extending in the direction of travel DT.
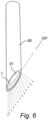
- the dosing tube may comprise an opening, extending in a plane OP that is non-perpendicular to the direction of travel DT.
- the supply of the filling material When the dosing tube has an inclined opening, the supply of the filling material will be supplied with a force which will be directed not only in the direction of travel DT, but also in an inclined or transverse direction.
- An inclined opening may yield a less focused stream since the supply of the filling material may also be directed in transversal directions or inclined transversal directions and not only in the direction of travel DT. This may reduce the force acting on the transverse end seal. This may further enhance the seal strength.
- the plane OP of the opening may form an angle ⁇ of 30 to 70° with the direction of travel DT.
- the angle ⁇ may be 35 to 65°.
- the plane OP of the opening may be substantially parallel to the length extension direction LED.
- the plane of the opening of the dosing tube and the length direction of the first operation surface and the second operation surface need not be parallel.
- the sealing device may be a heat sealing device or an ultrasonic sealing device.
- the present disclosure provides a method for producing an oral pouched product comprising a filling material and a saliva-permeable pouch enclosing the filling material, the method comprising
- a plurality of pouches may be provided with the method.
- a seal may be created in which two opposite longitudinal edges of the web are faced towards each other so that the inner surface of one edge is faced to the outer surface of one edge.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP23196221.8A EP4520671A1 (de) | 2023-09-08 | 2023-09-08 | Orales produkt in beutelform |
| PCT/EP2024/074707 WO2025051791A1 (en) | 2023-09-08 | 2024-09-04 | An oral pouched product |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP23196221.8A EP4520671A1 (de) | 2023-09-08 | 2023-09-08 | Orales produkt in beutelform |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP4520671A1 true EP4520671A1 (de) | 2025-03-12 |
Family
ID=88016269
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP23196221.8A Withdrawn EP4520671A1 (de) | 2023-09-08 | 2023-09-08 | Orales produkt in beutelform |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP4520671A1 (de) |
| WO (1) | WO2025051791A1 (de) |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4703765A (en) | 1983-09-09 | 1987-11-03 | United States Tobacco Company | Precise portion packaging machine |
| US8608381B2 (en) * | 2005-05-26 | 2013-12-17 | General Mills, Inc. | Easy pour bag |
| WO2017093487A1 (en) * | 2015-12-02 | 2017-06-08 | Swedish Match North Europe Ab | Method for producing an oral pouched snuff product |
-
2023
- 2023-09-08 EP EP23196221.8A patent/EP4520671A1/de not_active Withdrawn
-
2024
- 2024-09-04 WO PCT/EP2024/074707 patent/WO2025051791A1/en active Pending
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4703765A (en) | 1983-09-09 | 1987-11-03 | United States Tobacco Company | Precise portion packaging machine |
| US8608381B2 (en) * | 2005-05-26 | 2013-12-17 | General Mills, Inc. | Easy pour bag |
| WO2017093487A1 (en) * | 2015-12-02 | 2017-06-08 | Swedish Match North Europe Ab | Method for producing an oral pouched snuff product |
| US20180257801A1 (en) * | 2015-12-02 | 2018-09-13 | Swedish Match North Europe Ab | Method for producing an oral pouched snuff product |
Non-Patent Citations (1)
| Title |
|---|
| S. RUSSEL: "Handbook of Nonwovens", 2007, WOODHEAD PUBL. LTD. |
Also Published As
| Publication number | Publication date |
|---|---|
| WO2025051791A1 (en) | 2025-03-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3548385B1 (de) | Verfahren und anordnung zur portionsverpackung eines oralen schnupfprodukts in beutelform | |
| EP3383746B1 (de) | Dichtungsvorrichtung | |
| RU2409506C2 (ru) | Упаковка для сыпучих материалов, в частности мешок из синтетической пленки | |
| US8402724B2 (en) | Method and apparatus for product in seal deflection | |
| MX2011002839A (es) | Dispositivo de cierre para cerrar envases unitarios que preferentemente tienen forma de bolsa. | |
| WO2000027721A9 (en) | Touch fasteners, their manufacture, and products incorporating them | |
| JP2014030755A (ja) | 薬剤包装袋及びその袋用シート | |
| CN107416352B (zh) | 膜包装件以及用于在膜包装件中包装产品的方法 | |
| WO2010140242A1 (ja) | 抽出バッグの製造方法 | |
| WO2025051791A1 (en) | An oral pouched product | |
| TW201130590A (en) | Method of closing a sack body | |
| WO2016089975A1 (en) | Apparatus, processes and systems for heat sealing | |
| JP2017019513A (ja) | 超音波溶着溶断装置及び包装体 | |
| KR20260061407A (ko) | 경구용 파우치형 제품 | |
| JP4763162B2 (ja) | 製袋充填機 | |
| US20080072545A1 (en) | Continuous motion wrapping method and apparatus | |
| US11845578B2 (en) | Pouched product for oral use, sealing method, sealing device, method and apparatus for manufacturing a pouched product for oral use | |
| GB1561817A (en) | Pouches | |
| EP1681155A2 (de) | Haftverschlüsse und deren Herstellung | |
| JP2015063329A (ja) | インフレーションフィルムを用いた縦型充填包装機、および内容物入りフィルム包装袋の製造方法 | |
| EP1612144A1 (de) | Verfahren und Vorrichtung zum Verpacken eines Produktes in Beuteln | |
| WO2025133623A1 (en) | Pouched products and their manufacture | |
| CN1906094A (zh) | 具有整体系紧条的塑料袋 | |
| WO2009122244A1 (en) | A method of producing multiple packages and corresponding package | |
| RU2021127231A (ru) | Упаковочный материал и пакетированный продукт в виде снаффа, предназначенный для орального применения |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20250913 |