EP4570935A1 - Plaque en alliage d'aluminium pour couvercle de canette - Google Patents
Plaque en alliage d'aluminium pour couvercle de canette Download PDFInfo
- Publication number
- EP4570935A1 EP4570935A1 EP24792662.9A EP24792662A EP4570935A1 EP 4570935 A1 EP4570935 A1 EP 4570935A1 EP 24792662 A EP24792662 A EP 24792662A EP 4570935 A1 EP4570935 A1 EP 4570935A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- mass
- less
- aluminum alloy
- content
- sheet
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/06—Alloys based on aluminium with magnesium as the next major constituent
- C22C21/08—Alloys based on aluminium with magnesium as the next major constituent with silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22F—CHANGING THE PHYSICAL STRUCTURE OF NON-FERROUS METALS AND NON-FERROUS ALLOYS
- C22F1/00—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working
- C22F1/04—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon
- C22F1/047—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon of alloys with magnesium as the next major constituent
Definitions
- the present disclosure relates to an aluminum alloy sheet for a can lid.
- Production of the primary aluminum requires a large amount of electricity in its refining process, which leads to large CO 2 emissions.
- reducing an amount of blending the primary aluminum and increasing a closed recycling rate lead to reduction of CO 2 emissions in production of the aluminum alloy sheet.
- CO 2 emissions can be reduced to approximately one-thirtieth when aluminum scraps are re-melted for casting compared to a case where the primary aluminum is produced.
- an amount of aluminum alloy sheets produced for beverage cans, which are widely used around the world, is very large.
- further improvement in the closed recycling rate has great significance in reducing the burden on the environment.
- a can lid made of 5182 aluminum alloy (AA5182 alloy) has lower upper compositional limits of Si, Fe, Cu, Mn, and the like than those of a can body made of 3104 aluminum alloy (AA3104 alloy). Thus, it is difficult to blend scraps derived from can stock containing the 3104 aluminum alloy.
- an aluminum alloy sheet for a can lid is adjusted to include a composition of the 5182 aluminum alloy by using a large amount of primary metal compared to an aluminum alloy sheet for a can body, resulting in a lower recycling rate.
- the alloy for a can lid is changed to an alloy having a composition in which more 3104 aluminum alloy can be blended, the usage rate of the primary metal for a can lid can be greatly reduced.
- Patent Documents 1 to 5 disclose aluminum alloy sheets for can lids excellent in recyclability and each having a composition relatively closer to that of the 3104 aluminum alloy.
- Problems in making an alloy for a can lid similar in composition to the 3104 aluminum alloy include reduction in a buckling pressure (pressure resistance) of the can lid and toughness of a material.
- the buckling pressure of the can lid is an internal pressure value when the can lid bulges (buckles) under a pressure inside the can, which is a resistance value when the internal pressure of the can accidentally increases due to changes in the external environment.
- high buckling pressure is required.
- the buckling pressure increases as the strength of the material increases and the sheet thickness increases.
- the buckling pressure thereof is greatly reduced, and it is highly possible that the lid bulges and the content leaks when the internal pressure of the can is unexpectedly increased. If the sheet thickness is greatly increased to improve the buckling pressure, the weight and cost of the lid are increased.
- the toughness of a material affects the formability and the opening property of a lid. If the toughness of the materials is low, a molding crack may occur especially in a rivet part and a countersink part of the lid. In addition, when the internal pressure of the can is unexpectedly increased, a crack may occur in a score part, and it is highly possible that the content of the can leaks. In particular, these cracks occur along a rolling direction of the alloy sheet. Thus, toughness is required against tensile stress and bending stress in a direction perpendicular to the rolling direction.
- the conventional aluminum alloy sheets for can lids each having a composition relatively close to the composition of the 3104 aluminum alloy do not satisfy either or both of the above two problems: the strength of the material (that is, buckling pressure of the lid) and the toughness of the material (that is, formability and opening property).
- One aspect of the present disclosure is an aluminum alloy sheet for a can lid, the sheet comprising: a silicon (Si) content of 0.20 mass % or more and 0.47 mass % or less; an iron (Fe) content of 0.30 mass % or more and 0.59 mass % or less; a copper (Cu) content of 0.11 mass % or more and 0.40 mass % or less; a manganese (Mn) content of 0.70 mass % or more and 0.98 mass % or less, and a magnesium (Mg) content of 1.1 mass % or more and 3.7 mass % or less, and a balance consisting of or including aluminum (Al) and inevitable impurities, wherein, in each of 0°, 45°, and 90° directions to a rolling direction of the alloy sheet, a minimum evaluation value S min , which is a minimum value among evaluation values S calculated by a following formula (1) using a 0.2% yield strength ⁇ 0.2 , a tensile strength ⁇ B , and an average value ⁇ f
- An aluminum alloy sheet for a can lid of the present disclosure (hereinafter, also simply referred to as “alloy sheet”) comprises aluminum (Al), silicon (Si), iron (Fe), copper (Cu), manganese (Mn), and magnesium (Mg).
- the lower limit of Si content is 0.20 mass %, and preferably, 0.30 mass %. If the Si content is less than 0.20 mass %, an amount of Si precipitation by processing heat during cold rolling, which is conducted after hot rolling and solution heat treatment, may decrease and the strength of the alloy sheet may be insufficient.
- the average value of Si component specified for 3104 aluminum alloy according to JIS-H-4000:2014 is 0.30 mass %.
- Si content 0.30 mass % or more, a larger amount of scraps of 3104 aluminum alloy can be blended.
- the upper limit of the Si content is 0.47 mass %, and preferably 0.39 mass %, and more preferably, 0.35 mass %. If the Si content is more than 0.47 mass %, more Mg 2 Si particles are formed, and the toughness of the alloy sheet decreases.
- the lower limit of Fe content is 0.30 mass %, and preferably, 0.40 mass %.
- the average value of Fe component specified for 3104 aluminum alloy is 0.40 mass %. Thus, by setting the Fe content to 0.40 mass % or more, a larger amount of scraps of 3104 aluminum alloy can be blended.
- the upper limit of the Fe content is 0.59 mass %. If the Fe content is more than 0.59 mass %, more Al-Fe-Mn base or Al-Fe-Mn-Si base intermetallic compounds (that is, second phase particles) are formed. As a result, a crack propagation path is generated, and the toughness of the alloy sheet decreases.
- the lower limit of Cu content is 0.11 mass %, and preferably 0.15 mass %, and more preferably 0.20 mass %. If the Cu content is less than 0.11 mass %, there is insufficient Cu to enhance the strength by solid solution or precipitation, and the strength of the alloy sheet decreases. The strength of the alloy sheet significantly increases by precipitating Cu in the process of the cold rolling after the hot rolling and the solution heat treatment.
- the average value of Cu component specified for 3104 aluminum alloy is 0.15 mass %. Thus, by setting the Cu content to 0.15 mass % or more, a larger amount of scraps of 3104 aluminum alloy can be blended.
- the upper limit of the Cu content is 0.40 mass %, and preferably 0.25 mass %. If the Cu content is more than 0.40 mass %, the toughness of the alloy sheet decreases.
- the lower limit of Mn content is 0.70 mass %, and preferably 0.75 mass %. If the Mn content is less than 0.70 mass %, there is insufficient Mn to enhance the strength by solid solution or precipitation, and the average strength of the alloy sheet decreases.
- the average value of Mn component specified for 3104 aluminum alloy is 1.1 mass %, and the average value of the Mn component specified for 5182 aluminum alloy is 0.35 mass %.
- Mn content 0.75 mass % or more, a larger amount of scraps of 3104 aluminum alloy can be blended compared to the conventional 5182 aluminum alloy.
- the upper limit of the Mn content is 0.98 mass %, and preferably, 0.90 mass %. If the Mn content is more than 0.98 mass %, more Al-Fe-Mn base or Al-Fe-Mn-Si base intermetallic compounds (that is, second phase particles) are formed. As a result, a crack propagation path is generated, and the toughness of the alloy sheet is reduced.
- the lower limit of Mg content is 1.1 mass %, and preferably 1.4 mass %. If the Mg content is less than 1.1 mass %, there is insufficient Mg to enhance the strength by solid solution, and the average strength of the alloy sheet decreases. The strength of the alloy sheet significantly increases by precipitating Mg in the process of the cold rolling after the hot rolling and the solution heat treatment.
- the upper limit of the Mg content is 3.7 mass %, and preferably 3.1 mass %.
- the average value of Mg component specified for 3104 aluminum alloy is 1.05 mass %, and the average value of the Mg component specified for 5182 aluminum alloy is 4.5 mass %.
- the Mg content is set to 3.7 mass % or less, it is possible to use a larger amount of scraps of 3104 aluminum alloy and to reduce the amount of blending additional Mg-containing raw material.
- the alloy sheet may comprise titanium (Ti).
- the upper limit of Ti content is preferably 0.10 mass %. If Ti is contained, an ingot structure of the alloy sheet is refined.
- the alloy sheet may also comprise zinc (Zn).
- the upper limit of Zn content is preferably 0.25 mass %.
- the alloy sheet may comprise chromium (Cr).
- the upper limit of Cr content is preferably 0.10 mass %.
- the alloy sheet may comprise inevitable impurities to the extent that the performance of the alloy sheet is not significantly impaired. That is, the alloy sheet contains Si, Fe, Cu, Mn, Mg, Ti, Zn and Cr in the above-mentioned respective ranges, and a balance consists of or includes aluminum and inevitable impurities. The upper limit of the total amount of the inevitable impurities is preferably 0.15 mass %. The balance may contain substances other than aluminum and the inevitable impurities.
- a rolled aluminum alloy sheet has material anisotropy, and the strength shows different values in 0°, 45°, and 90° directions to a rolling direction of the alloy sheet.
- deformation begins in the direction with the least strength.
- S ⁇ fm / ⁇ 0.2 / ⁇ B
- a buckling pressure value of a lid made of aluminum alloy has a strong positive correlation with a value V obtained from the following formula (2) that is empirically expressed by the minimum evaluation value S min and sheet thickness t of the aluminum alloy sheet.
- V t 2.27 ⁇ S min
- the minimum evaluation value S min of the alloy sheet is preferably 360 MPa or more.
- the buckling pressure of the lid can be further increased.
- the minimum evaluation value S min exceeds 410 MPa, the material strength becomes excessively high and the toughness of the material decreases. That is, shear bands are more likely to occur on the materials due to tensile stress and bending stress during forming, and forming breakage is likely to occur.
- the minimum evaluation value S min is 410 MPa or less, it is possible to achieve both the strength of the material (that is, buckling pressure of the lid) and the toughness of the material (that is, formability and opening property).
- the 0.2% yield strength ⁇ 0.2 and the tensile strength ⁇ B in the formula (1) are measured by a method specified in JIS-Z-2241:2011.
- the sheet thickness t is measured, for example, with a micro gauge.
- the toughness of the aluminum alloy sheet affects the formability of a lid and a force (i.e. an opening force) required to open a score part.
- a cyclic bending test is one of the evaluation indices of the toughness of an aluminum alloy sheet.
- the cyclic bending test is performed by the following procedure. For example, a test piece cut into a strip with 12.5 mm in width and 200 mm in length is arranged so that a bending ridge line is parallel to a rolling direction D of the alloy sheet. Both ends of this test piece are fixed with chucks, and the test piece is tensioned with a load of 200 N.
- a jig having a bending radius R 2.0 mm is placed at a position 150 mm in a longitudinal direction of the test piece from the end of the test piece fixed with a stationary chuck, and with the jig as a fulcrum, the other chuck is rotated 90° to the left and the right, thereby the test piece is bent repeatedly. The number of bending is measured until the test piece breaks.
- N N 0 + ⁇ / 90
- a normalized number of cyclic bending N s is obtained by the following formula (4) based on a sheet thickness of 0.235 mm.
- t a sheet thickness of the test piece.
- N s N ⁇ t / 0.235
- the aluminum alloy sheet of the present disclosure has the normalized number of cyclic bending N s of 18 or more.
- the toughness is affected by strength and distribution of second phase particles. That is, as the strength is higher and the density of the second phase particles is higher, the toughness decreases. In particular, if the Mg content and the Si content are increased, Mg 2 Si particles are easily formed. As a result, the Mg 2 Si particles may become a starting point or a propagation path of a crack, and affect the decrease in toughness.
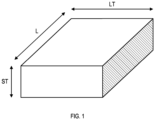
- a ratio of a total area in the L-ST cross section of the Mg 2 Si particles each having an area of 0.3 ⁇ m 2 or more is 0.2% or less.
- “L” indicates a longitudinal direction
- “ST” indicates a sheet thickness direction
- “LT” indicates the width direction of the alloy sheet.
- the ratio of the area of the Mg 2 Si particles can be measured by the following method, for example. First, a measurement sample is cut, and a surface to be measured (i.e., the L-ST cross section) is mechanically polished to a mirror finish. Then, the polished surface (i.e., the L-ST cross-section) is observed using a scanning electron microscope (SEM), and 10 fields of view are obtained in a central region of the sheet thickness.
- the accelerating voltage of the SEM is set to 15 kV, the magnification of the SEM is set to 1000 times and a range of one field of view is set to 0.012 mm 2 , and imaging is performed. Then, a COMPO image (a backscattered electron composition image) is obtained.
- the obtained COMPO image is analyzed by image analysis software "ImageJ". Specifically, the most frequent brightness value of the image in 256 shades is used as a background brightness, and particles with brightness of less than a value obtained by subtracting 30 from the most frequent brightness value is determined to be the Mg 2 Si particles.
- a total area of particles each having an area of 0.3 ⁇ m 2 or more is calculated. Then, the obtained value is divided by an imaged area of the 10 fields of view (i.e., an imaged total area). Thereby, the ratio of the total area of the Mg 2 Si particles each having the area of 0.3 ⁇ m 2 or more in the L-ST cross-section is calculated.
- the Mg 2 Si particles that become a starting point and a propagation path of a crack and affect the decrease in toughness are re-solutionized in the process of the homogeneous heat treatment of the ingot.
- a solidus temperature is higher than a solid solutionizing temperature of Mg 2 Si, and it is further preferable that a difference between the solidus temperature and the solid solutionizing temperature of Mg 2 Si is 30°C or more.
- the crystallization temperature of the primary crystal that is, Al 6 (Mn, Fe)
- the crystallization temperature of the primary crystal is lower than the solidification start temperature of aluminum.
- the solid solutionizing temperature of Mg 2 Si herein indicates the highest temperature at which Mg 2 Si can exist in the equilibrium diagram, and is the lowest temperature at which a liquid phase can exist.
- the solidification start temperature of aluminum indicates the highest temperature at which solid Al can exist in the equilibrium diagram, and the crystallization temperature of the primary crystal is the highest temperature at which Al 6 (Mn, Fe) can exist.
- the solid solutionizing temperature of Mg 2 Si, the solidus temperature, the solidification start temperature of aluminum and the crystallization temperature of the primary crystal can be obtained from the equilibrium diagram of the aluminum alloy calculated using a thermodynamics calculation software.
- the solid solutionizing temperature of Mg 2 Si, the solidus temperature, the solidification start temperature of aluminum and the crystallization temperature of the primary crystal are uniquely determined by the composition of the aluminum alloy.
- the method for calculating these boundary temperatures from the alloy composition includes calculating thermodynamic quantities required for respective calculations using the CALPHAD method.
- thermodynamic calculations for multi-component alloy can be performed using a commercially available system software (for example, "JMatPro” developed by Sente Software Ltd.) which includes a thermodynamic database required for the calculations, an interface, and a phase diagram creation function.
- JMatPro developed by Sente Software Ltd.
- the solid solutionizing temperature of Mg 2 Si is lower than the solidus temperature, and the crystallization temperature of the primary crystal is lower than the solidification start temperature of Al.
- Mg 2 Si is re-solutionized, and the Mg 2 Si particles that become a starting point and a propagation path of a crack, and affect the decrease in toughness can be reduced.
- cold rolling reduction materials with low cold rolling reduction
- a material in which annealing is performed on a rolled sheet during cold rolling using a continuous annealing line (CAL) so that the final cold rolling reduction (that is, cold rolling reduction after annealing) is reduced has high toughness.
- CAL continuous annealing line
- the higher the cold rolling reduction the greater the 0.2% yield strength ⁇ 0.2_90° in the 90° direction to the rolling direction compared to the 0.2% yield strength ⁇ 0.2_0° in the 0° direction to the rolling direction.
- a difference in the 0.2% yield strength between the 0° direction to the rolling direction and the 90° direction to the rolling direction that is, the strength anisotropy, can be associated with the cold rolling reduction of the material.
- a value D obtained by subtracting the 0.2% yield strength ⁇ 0.2_90° in the 90° direction to the rolling direction from the 0.2% yield strength ⁇ 0.2_0° in the 0° direction to the rolling direction, using the formula (5), is -13 MPa or more and 13 MPa or less.
- D ⁇ 0.2 _ 0 ° ⁇ ⁇ 0.2 _ 90 °
- the metallographic meaning of the strength anisotropy obtained by subtracting the 0.2% yield strength ⁇ 0.2_90° in the 90° direction to the rolling direction from the 0.2% yield strength ⁇ 0.2_0° in the 0° direction to the rolling direction can be explained as follows.
- the material after hot rolling or annealing is in a recrystallized state, and has high degree of integration of isotropic Cube orientation. From here, by plastic deformation due to cold rolling, Cube orientation transforms into a rolling texture having anisotropy in the rolling direction. Moreover, the higher the cold rolling reduction, the more elongated the crystal grains in the rolling direction. Thus, while diameters of the crystal grains along the 0° direction to the rolling direction increase, the change in diameters of the crystal grains along the 90° direction to the rolling direction decreases compared to that in the 0° direction to the rolling direction.
- the resistance ⁇ has different values. This is because the degree of integration of the rolling texture having anisotropy in the rolling direction increases as the cold rolling reduction increases, causing changes in resistance to the crystal grain boundary sliding depending on the tensile direction.
- the crystal grains are elongated and the diameters increase as the cold rolling reduction increases in the 0° direction to the rolling direction, the change in the crystal grain diameter with respect to the cold rolling reduction is relatively small in the 90° direction to the rolling direction. Accumulation of these effects results in strength anisotropy with respect to the increase in the cold rolling reduction.
- the aluminum alloy sheet of the present disclosure can be produced, for example, by the following procedure. First, an aluminum alloy having a composition same as that of the aluminum alloy sheet of the present disclosure is subjected to a semi-continuous casting (i.e. Direct Chill (DC) casting) in a normal manner to produce an ingot.
- a semi-continuous casting i.e. Direct Chill (DC) casting
- the temperature in the homogenizing treatment is preferably, for example, 470°C or higher and 620°C or lower.
- the duration of the homogenizing treatment is preferably, for example, one hour or longer and 20 hours or shorter.
- the temperature in the homogenizing treatment is 400°C or higher, segregation in the ingot structure can be easily resolved. Furthermore, if the temperature in the homogenizing treatment is 450°C or higher, the Mg 2 Si particles are re-solutionized, and the strength and toughness of the alloy sheet can be improved. Moreover, if the temperature in the homogenizing treatment is 470°C or higher, and more preferably the solid solutionizing temperature of Mg 2 Si or higher, re-solutionization of the Mg 2 Si particles is promoted and the strength and toughness of the alloy sheet can be further improved. On the other hand, if the temperature in the homogenizing treatment is 620°C or lower, local melting of the aluminum alloy is less likely to occur.
- the duration of the homogenizing treatment is one hour or longer, the temperature of the entire slab becomes uniform, segregation of the ingot structure is easily resolved, and the Mg 2 Si particles can be easily re-solutionized.
- the hot rolling process comprises a rough rolling process and a finish rolling process.
- the ingot is processed into a plate material having a thickness of approximately several tens of millimeters by reverse rolling.
- the finish rolling process the thickness of the plate material is reduced to approximately several millimeters by, for example, tandem rolling or the like, and the plate material is coiled to form a hot-rolled coil.
- a total rolling reduction in the finish rolling is high, a recrystallization texture is formed after coiling, and an integration degree of isotropic Cube orientation can be increased. If a coiling temperature in the finish rolling is high, the recrystallization texture is formed after coiling, and the integration degree of Cube orientation can be increased.
- the sheet material is subjected to cold rolling.
- the hot-rolled coil is rolled until a product sheet thickness is achieved.
- the cold rolling may be either single cold rolling or tandem cold rolling. In the single cold rolling, the rolling is preferably divided into several times and performed in two or more rolling passes.
- the solution heat treatment is performed on the coil during the cold rolling, and Mg and the like are re-solutionized. Thereby, while increasing the strength of the material, it is possible to reduce the final cold rolling reduction and obtain an alloy sheet with reduced material anisotropy.
- a continuous annealing line (CAL) is used to perform a heat treatment (i.e. annealing) at a target peak metal temperature of 440°C or higher followed by forced cooling such as air-cooling, whereby the strength of the alloy sheet can be effectively increased.
- CAL continuous annealing line
- a cold rolling reduction is preferably 80% or more.
- the strength of the alloy sheet can be increased.
- the cold rolling reduction is preferably 92% or less.
- the cold rolling reduction after the solution heat treatment is preferably 50% or more.
- the strength of the alloy sheet can be increased even if the cold rolling reduction is low.
- the cold rolling reduction is preferably 80% or less.
- the cold rolling reduction R (%) is obtained by the following formula (7), where "t 0 " is a sheet thickness (mm) of a sheet after the hot rolling or solution heat treatment, and "t 1 " is a product sheet thickness (mm) after the cold rolling.
- R t 0 ⁇ t 1 / t 0 ⁇ 100
- the product sheet thickness can be selected as appropriate so that a desired buckling pressure is obtained. As shown in the above-described formula (2), the buckling pressure increases as the sheet thicknesses increases.
- the product sheet thickness can be selected in accordance with the value V of the formula (2).
- the value V is preferably 13.0 or more, and more preferably 14.0 or more. As described above, with the aluminum alloy sheet of the present disclosure, it is possible to avoid increasing the sheet thickness to maintain the buckling pressure high.
- the coil that has been cold-rolled to have a product sheet thickness is precoated on a coating line or the like.
- the surface(s) of the cold-rolled coil is subjected to degreasing, cleaning, and chemical conversion treatment, followed by paint coating and paint baking treatment.
- a chemical solution such as a chromate based solution and a zirconium based solution is used.
- the paint to be used may include an epoxy based paint and a polyester based paint. These can be selected according to applications.
- the coil is heated at a peak metal temperature (PMT) of 220C° or higher and 270C° or lower for approximately 30 seconds or shorter. At this time, the recovery of the material is inhibited at lower PMT, and thus, high strength of the alloy sheet can be maintained.
- PMT peak metal temperature
- both the high strength and high toughness of the aluminum alloy sheet can be achieved while blending scrap materials derived from can stock. That is, a certain amount of scraps derived from 3104 aluminum alloy for a can body can be blended, thereby reducing the usage rate of the primary metal and the amount of CO 2 emissions. Furthermore, it is possible to obtain a highly formable aluminum alloy sheet for a can lid that can be used for positive pressure can lids in which high buckling pressure is required.
- the present disclosure also includes various forms other than the aluminum alloy sheet of the above-described embodiment, such as a member comprising this aluminum alloy sheet and a production method of this aluminum alloy sheet.
- a function of a single component in the aforementioned embodiments may be distributed to a plurality of components, and functions of a plurality of components may be achieved by a single component.
- a part of the configuration of each of the aforementioned embodiments may be omitted.
- At least one part of the configuration of the aforementioned embodiments may be added to or replaced with the configuration of another embodiment or other embodiments of the aforementioned embodiments. All the modes that are encompassed in the technical idea defined by the language in the claims are embodiments of the present disclosure.
- ingots each comprising components (mass %) specified by alloy numbers 1 to 9 shown in Table 3 and a balance consisting of aluminum and inevitable impurities were produced by a semi-continuous casting method.
- Each ingot includes 0.10 mass % or less of Ti, 0.25 mass % or less of Zn, 0.10 mass % or less of Cr, and 0.15 mass % or less of inevitable impurities.
- each ingot was scalped. Then, the ingot was placed in the furnace, and subjected to homogenizing treatment. The temperature of the homogenizing treatment is shown in Table 1. After the homogenizing treatment, the ingot was removed from the furnace and hot rolling was immediately started to thereby obtain a rolled sheet.
- the hot-rolled sheet was cold-rolled without being annealed.
- the target cold rolling reduction in the cold rolling is shown in Table 1.
- the product sheet thickness of the aluminum alloy sheets of S1 to S17 (i.e. "t 1 " in formula (7)) after the cold rolling is within a range of approximately 0.235 ⁇ 0.03 mm.
- the aluminum alloy sheets of S1 to S17 were each milled to form three test pieces No. 5 specified in JIS-Z-2241:2011. Longitudinal directions of the three test pieces extend in respective directions forming angles of 0°, 45°and 90° to the rolling direction.
- test pieces were subjected to a tensile test according to JIS-Z-2241:2011, and 0.2% yield strength and tensile strength were measured.
- Tables 1 and 2 show the measurement results of the 0.2% yield strength ⁇ 0.2 and the tensile strength ⁇ B , and the average values ⁇ fm of the 0.2% yield strength and the tensile strength.
- evaluation values S were calculated from the measurement results of the respective tensile tests in the 0° direction, 45° direction, and 90° direction to the rolling direction and the formula (1).
- Table 2 shows a minimum evaluation value S min , which is the minimum value of these evaluation values S.
- Table 3 shows the solid solutionizing temperature of Mg 2 Si, the solidus temperature, the solidification start temperature of aluminum and the crystallization temperature of the primary crystal (that is, Al 6 (Mn, Fe)), calculated based on the components (mass %) specified by the alloy numbers 1 to 9.
- Each boundary temperature was calculated based on the equilibrium diagram obtained based on the five main components (Si, Fe, Cu, Mn, and Mg) using "JMatPro".
- the effects of Ti, Zn, Cr and the inevitable impurities are not taken into consideration.
- the aluminum alloy sheet marked " ⁇ 50" means that 50 mass % or more of 3104 aluminum alloy can be blended in the sheet.
- the possible blending ratio of the scraps of 3104 aluminum alloy is determined based on Table 4.
- Table 4 shows the correspondence between the blending ratio of 3104 aluminum alloy and 5182 aluminum alloy and the average values of the components.
- the first line of Table 4 shows the average values of the components of 3104 aluminum alloy, and the second line shows the average values of the components of 5182 aluminum alloy.
- the average value of Si is 0.20 mass %
- the average value of Fe is 0.29 mass %
- the average value of Cu is 0.11 mass %
- the average value of Mn is 0.7 mass %
- the average value of Mg is 2.8 mass %.
- the ratios of the respective components in the aluminum alloy sheets are equal to or more than the above-described values of Si, Fe, Cu, Mn, and Mg, these sheets have 50 mass % or more of the possible blending ratio of 3104 aluminum alloy sheet.
- the blending ratio of 3104 aluminum alloy increases, the contents of Si, Fe, Cu and Mn increase, and the content of Mg decreases.
- 50 mass % or more of the scraps of 3104 aluminum alloy can be blended.
- the aluminum alloy sheets of S1 to S15 have higher strength (that is, S min ) than the aluminum alloy sheet of S16.
- S min strength
- the Mg content was low compared to the 5182 aluminum alloy for conventional can lids shown in S17, but the equivalent strength was achieved.
- the cold rolling reduction has decreased through the intermediate annealing process.
- the alloy sheets of S1 to S7 have less strength anisotropy compared to the alloy sheets of S8 to S13 with the cold rolling reduction exceeding 80%.
- the strength anisotropy is associated with the cold rolling reduction.
- both high strength and high toughness that is, high number of cyclic bending are achieved compared to the alloy sheets of S8 to S13 with the cold rolling reduction exceeding 80%.
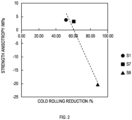
- the strength anisotropy has a negative correlation with the cold rolling reduction.
- an absolute value of the strength anisotropy is considered to be maximum at the cold rolling reduction of 80% in the negative direction.
- the strength anisotropy at the cold rolling reduction of 80% is estimated to be -13 MPa, and thus it is said that the lower limit of the strength anisotropy is -13 MPa.
- the absolute value of the strength anisotropy is considered to be maximum at the cold rolling reduction of 50% in the positive direction. From the trend in FIG. 2 , the strength anisotropy at the cold rolling reduction of 50% is estimated to be 7 MPa. On the other hand, referring to the strength anisotropy of the alloy sheets of S3, S5, and so on, it can be seen that some variation in strength anisotropy is unavoidable. Thus, the appropriate strength anisotropy at the cold rolling reduction of 50% is considered to be around 13 MPa.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Metal Rolling (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023067145A JP7473707B1 (ja) | 2023-04-17 | 2023-04-17 | 缶蓋用アルミニウム合金板 |
| PCT/JP2024/015113 WO2024219388A1 (fr) | 2023-04-17 | 2024-04-16 | Plaque en alliage d'aluminium pour couvercle de canette |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4570935A1 true EP4570935A1 (fr) | 2025-06-18 |
| EP4570935A4 EP4570935A4 (fr) | 2025-10-01 |
Family
ID=90735681
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP24792662.9A Pending EP4570935A4 (fr) | 2023-04-17 | 2024-04-16 | Plaque en alliage d'aluminium pour couvercle de canette |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US20260009110A1 (fr) |
| EP (1) | EP4570935A4 (fr) |
| JP (1) | JP7473707B1 (fr) |
| WO (1) | WO2024219388A1 (fr) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2025142252A1 (fr) * | 2023-12-28 | 2025-07-03 | 株式会社Uacj | Plaque en alliage d'aluminium pour couvercle de canette non-revêtu |
| WO2025169925A1 (fr) * | 2024-02-06 | 2025-08-14 | 東洋製罐株式会社 | Couvercle de canette en alliage d'aluminium et feuille en alliage d'aluminium pour un couvercle de canette |
| WO2026095010A1 (fr) * | 2024-10-31 | 2026-05-07 | 株式会社Uacj | Feuille d'alliage d'aluminium pour couvercles de boîte |
| WO2026095012A1 (fr) * | 2024-10-31 | 2026-05-07 | 株式会社Uacj | Feuille d'alliage d'aluminium destinée à des couvercles de canette |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01269594A (ja) | 1988-04-21 | 1989-10-27 | Fuji Photo Film Co Ltd | 平版印刷版用版面保護剤 |
| JP3523692B2 (ja) * | 1994-08-23 | 2004-04-26 | 住友軽金属工業株式会社 | 曲げ加工性に優れた缶蓋材およびその製造方法 |
| JP3059083B2 (ja) | 1995-09-01 | 2000-07-04 | スカイアルミニウム株式会社 | リサイクルに好適な缶蓋用アルミニウム合金積層板およびその製造方法 |
| JP3411840B2 (ja) | 1998-11-27 | 2003-06-03 | 住友軽金属工業株式会社 | 缶エンド用アルミニウム合金板 |
| JP4077997B2 (ja) | 1999-09-03 | 2008-04-23 | 古河スカイ株式会社 | 缶蓋用アルミニウム合金硬質板の製造方法 |
| JP2002180173A (ja) * | 2000-12-11 | 2002-06-26 | Mitsubishi Alum Co Ltd | エンド部用樹脂被覆アルミニウム合金板 |
| JP6058050B2 (ja) | 2015-03-04 | 2017-01-11 | 株式会社神戸製鋼所 | 負圧缶蓋用アルミニウム合金板 |
| CN105568085A (zh) * | 2015-12-21 | 2016-05-11 | 山东南山铝业股份有限公司 | 一种3104铝合金易拉罐罐盖材料及其生产方法 |
| PL3601626T3 (pl) * | 2017-03-23 | 2022-07-18 | Novelis, Inc. | Odlewanie złomu aluminiowego z recyklingu |
| FR3122666B1 (fr) * | 2021-05-04 | 2024-06-21 | Constellium Neuf Brisach | FEUILLES D’ALUMINIUM 5xxx POUR FABRICATION DE CANETTES |
| JPWO2023095859A1 (fr) * | 2021-11-25 | 2023-06-01 | ||
| JP7652730B2 (ja) * | 2022-03-09 | 2025-03-27 | 株式会社Uacj | 缶蓋用アルミニウム合金板 |
-
2023
- 2023-04-17 JP JP2023067145A patent/JP7473707B1/ja active Active
-
2024
- 2024-04-16 US US19/104,012 patent/US20260009110A1/en active Pending
- 2024-04-16 EP EP24792662.9A patent/EP4570935A4/fr active Pending
- 2024-04-16 WO PCT/JP2024/015113 patent/WO2024219388A1/fr not_active Ceased
Also Published As
| Publication number | Publication date |
|---|---|
| JP7473707B1 (ja) | 2024-04-23 |
| EP4570935A4 (fr) | 2025-10-01 |
| JP2024153327A (ja) | 2024-10-29 |
| US20260009110A1 (en) | 2026-01-08 |
| WO2024219388A1 (fr) | 2024-10-24 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP4394068A1 (fr) | Plaque en alliage d'aluminium pour opercule de canette | |
| US20260009110A1 (en) | Aluminum alloy sheet for can lid | |
| EP4570937A1 (fr) | Plaque en alliage d'aluminium pour opercule de canette | |
| EP4570936A1 (fr) | Plaque en alliage d'aluminium pour couvercle de canette | |
| EP4610388A1 (fr) | Procédé de fabrication d'une feuille d'alliage d'aluminium pour couvercle de canette | |
| EP4570938A1 (fr) | Feuille d'alliage d'aluminium pour languette | |
| EP4582575A1 (fr) | Feuille d'alliage d'aluminium pour languettes | |
| WO2025142690A1 (fr) | Plaque en alliage d'aluminium pour couvercle de canette non-revêtu | |
| JP2025105155A (ja) | 未塗装の缶蓋用アルミニウム合金板 | |
| JP2025105154A (ja) | 未塗装の缶蓋用アルミニウム合金板 | |
| JP2025105153A (ja) | 未塗装の缶蓋用アルミニウム合金板 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20250311 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20250901 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C22C 21/06 20060101AFI20250826BHEP Ipc: C22F 1/00 20060101ALI20250826BHEP Ipc: C22F 1/047 20060101ALI20250826BHEP Ipc: C22C 21/08 20060101ALI20250826BHEP |