JP2007144485A - 超音波溶着器 - Google Patents
超音波溶着器 Download PDFInfo
- Publication number
- JP2007144485A JP2007144485A JP2005343989A JP2005343989A JP2007144485A JP 2007144485 A JP2007144485 A JP 2007144485A JP 2005343989 A JP2005343989 A JP 2005343989A JP 2005343989 A JP2005343989 A JP 2005343989A JP 2007144485 A JP2007144485 A JP 2007144485A
- Authority
- JP
- Japan
- Prior art keywords
- welding
- anvil
- handpiece
- ultrasonic
- lever
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000003466 welding Methods 0.000 claims abstract description 33
- 230000010355 oscillation Effects 0.000 claims abstract description 19
- 230000007547 defect Effects 0.000 abstract description 4
- 230000002950 deficient Effects 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 239000000155 melt Substances 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/84—Specific machine types or machines suitable for specific applications
- B29C66/861—Hand-held tools
- B29C66/8614—Tongs, pincers or scissors
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
- B29C65/08—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using ultrasonic vibrations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/01—General aspects dealing with the joint area or with the area to be joined
- B29C66/05—Particular design of joint configurations
- B29C66/10—Particular design of joint configurations particular design of the joint cross-sections
- B29C66/11—Joint cross-sections comprising a single joint-segment, i.e. one of the parts to be joined comprising a single joint-segment in the joint cross-section
- B29C66/112—Single lapped joints
- B29C66/1122—Single lap to lap joints, i.e. overlap joints
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/40—General aspects of joining substantially flat articles, e.g. plates, sheets or web-like materials; Making flat seams in tubular or hollow articles; Joining single elements to substantially flat surfaces
- B29C66/41—Joining substantially flat articles ; Making flat seams in tubular or hollow articles
- B29C66/43—Joining a relatively small portion of the surface of said articles
- B29C66/431—Joining the articles to themselves
- B29C66/4312—Joining the articles to themselves for making flat seams in tubular or hollow articles, e.g. transversal seams
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/73—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/739—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/7392—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic
- B29C66/73921—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic characterised by the materials of both parts being thermoplastics
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/82—Pressure application arrangements, e.g. transmission or actuating mechanisms for joining tools or clamps
- B29C66/822—Transmission mechanisms
- B29C66/8221—Scissor or lever mechanisms, i.e. involving a pivot point
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/82—Pressure application arrangements, e.g. transmission or actuating mechanisms for joining tools or clamps
- B29C66/824—Actuating mechanisms
- B29C66/8242—Pneumatic or hydraulic drives
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/83—General aspects of machine operations or constructions and parts thereof characterised by the movement of the joining or pressing tools
- B29C66/832—Reciprocating joining or pressing tools
- B29C66/8322—Joining or pressing tools reciprocating along one axis
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/87—Auxiliary operations or devices
- B29C66/874—Safety measures or devices
- B29C66/8748—Safety measures or devices involving the use of warnings
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/90—Measuring or controlling the joining process
- B29C66/92—Measuring or controlling the joining process by measuring or controlling the pressure, the force, the mechanical power or the displacement of the joining tools
- B29C66/922—Measuring or controlling the joining process by measuring or controlling the pressure, the force, the mechanical power or the displacement of the joining tools by measuring the pressure, the force, the mechanical power or the displacement of the joining tools
- B29C66/9221—Measuring or controlling the joining process by measuring or controlling the pressure, the force, the mechanical power or the displacement of the joining tools by measuring the pressure, the force, the mechanical power or the displacement of the joining tools by measuring the pressure, the force or the mechanical power
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/90—Measuring or controlling the joining process
- B29C66/96—Measuring or controlling the joining process characterised by the method for implementing the controlling of the joining process
- B29C66/961—Measuring or controlling the joining process characterised by the method for implementing the controlling of the joining process involving a feedback loop mechanism, e.g. comparison with a desired value
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Fluid Mechanics (AREA)
- Pressure Welding/Diffusion-Bonding (AREA)
- Lining Or Joining Of Plastics Or The Like (AREA)
- Apparatuses For Generation Of Mechanical Vibrations (AREA)
Abstract
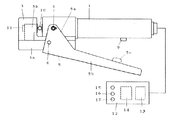
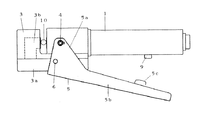
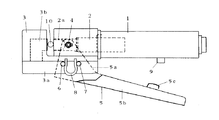
【解決手段】 超音波溶着装置において1はハンドピース、2は超音波振動子、2aはホーン、3はアンビル部、3aは摺動部材、3bはアンビル、4は回動軸、5は回動部材、5aは三角部材、5bはレバー、6は駆動軸、7は支持軸、8はU字状のバネ、9は発振スイッチ、10は被溶着物である。ハンドピースの側部に発振スイッチ9が装着され、又、レバー5bに突出部5cが装着され、アンビル部のアンビル3bにセンサ11が装着され、ハンドピース1に制御装置12が接続され、制御装置12に発振器13、判定回路14、溶着中の表示灯15、溶着完了の表示灯16、溶着不良の表示灯17が装着されている。そして溶着時の振動とセンサ圧力をセンサで検出し、その強さで溶着時期を判定し、発振器を停止する。
【選択図】図1
Description
2 超音波振動子
3 アンビル部
10 被溶着物
11 センサ
12 制御装置
13 発振器
14 判定回路
15 溶着中の表示灯
16 溶着完了の表示灯
17 溶着不良の表示灯
Claims (3)
- 超音波振動子を内蔵し、該超音波振動子のホーンの先端が端部に突出したハンドピースと、該ハンドピースの側部に摺動部材を装着し、該摺動部材から突出するアンビルの接触部が前記超音波振動子のホーンと対向するように装着したアンビル部と、該アンビル部の前記アンビルに装着されたセンサと、前記ハンドピースの両側部に装着された回動軸に三角部材の頂点近傍に回動可能に装着され、前記三角部材から前記ケースから離れる方向にレバーを設けた回動部材と、該回動部材の前記レバーの中間部に固着した突出部と、該突出部で作動され、前記ハンドピースの側部に装着された発振スイッチと、該発振スイッチによって前記超音波振動子に発振出力を印加する発振器を内蔵する制御装置を前記ハンドピースに接続することを特徴とするの超音波溶着器。
- 前記センサで検出した振動及び圧力信号によって、溶着完了を判定する判定回路を前記制御装置に装着することを特徴とする請求項1記載の超音波溶着器。
- 前記制御装置に溶着中、溶着完了及び溶着不可を表示する表示灯を装着することを特徴とする請求項1記載の超音波溶着器。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2005343989A JP4904473B2 (ja) | 2005-11-29 | 2005-11-29 | 超音波溶着器 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2005343989A JP4904473B2 (ja) | 2005-11-29 | 2005-11-29 | 超音波溶着器 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2007144485A true JP2007144485A (ja) | 2007-06-14 |
| JP4904473B2 JP4904473B2 (ja) | 2012-03-28 |
Family
ID=38206507
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2005343989A Expired - Fee Related JP4904473B2 (ja) | 2005-11-29 | 2005-11-29 | 超音波溶着器 |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP4904473B2 (ja) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101543936B (zh) * | 2009-05-04 | 2011-06-15 | 宁波中望电子科技有限公司 | 超声波铜管剪切封口机及剪切封口方法 |
| CN113399813A (zh) * | 2021-07-13 | 2021-09-17 | 北京半导体专用设备研究所(中国电子科技集团公司第四十五研究所) | 适用于压焊机的超声波换能装置 |
| JP2023091469A (ja) * | 2021-12-20 | 2023-06-30 | 日本アビオニクス株式会社 | 超音波溶断装置 |
| CN120115811A (zh) * | 2025-05-15 | 2025-06-10 | 珠海灵科自动化科技有限公司 | 焊接机头组件和焊接装置 |
| US12539557B2 (en) | 2021-07-29 | 2026-02-03 | Lg Energy Solution, Ltd. | Ultrasonic welding apparatus and ultrasonic welding method |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH11197854A (ja) * | 1998-01-20 | 1999-07-27 | Olympus Optical Co Ltd | 超音波溶着装置及び超音波溶着装置における溶着状態 検査方法 |
| JP2000202912A (ja) * | 1999-01-18 | 2000-07-25 | Kyoshin Sekkei:Kk | 超音波溶着装置 |
-
2005
- 2005-11-29 JP JP2005343989A patent/JP4904473B2/ja not_active Expired - Fee Related
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH11197854A (ja) * | 1998-01-20 | 1999-07-27 | Olympus Optical Co Ltd | 超音波溶着装置及び超音波溶着装置における溶着状態 検査方法 |
| JP2000202912A (ja) * | 1999-01-18 | 2000-07-25 | Kyoshin Sekkei:Kk | 超音波溶着装置 |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101543936B (zh) * | 2009-05-04 | 2011-06-15 | 宁波中望电子科技有限公司 | 超声波铜管剪切封口机及剪切封口方法 |
| CN113399813A (zh) * | 2021-07-13 | 2021-09-17 | 北京半导体专用设备研究所(中国电子科技集团公司第四十五研究所) | 适用于压焊机的超声波换能装置 |
| CN113399813B (zh) * | 2021-07-13 | 2022-05-03 | 北京半导体专用设备研究所(中国电子科技集团公司第四十五研究所) | 适用于压焊机的超声波换能装置 |
| US12539557B2 (en) | 2021-07-29 | 2026-02-03 | Lg Energy Solution, Ltd. | Ultrasonic welding apparatus and ultrasonic welding method |
| JP2023091469A (ja) * | 2021-12-20 | 2023-06-30 | 日本アビオニクス株式会社 | 超音波溶断装置 |
| JP7742297B2 (ja) | 2021-12-20 | 2025-09-19 | 日本アビオニクス株式会社 | 超音波溶断装置 |
| CN120115811A (zh) * | 2025-05-15 | 2025-06-10 | 珠海灵科自动化科技有限公司 | 焊接机头组件和焊接装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP4904473B2 (ja) | 2012-03-28 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP2017136642A (ja) | 超音波溶接品質判断装置および方法 | |
| US11660707B2 (en) | Welding quality inspection apparatus and method of the same | |
| JP2011093082A5 (ja) | ||
| JP4904473B2 (ja) | 超音波溶着器 | |
| KR20180059943A (ko) | 마찰 교반 점 접합 장치 및 마찰 교반 점 접합 방법 | |
| JP4809455B2 (ja) | 溶接状態の異常判別装置 | |
| JP3772175B2 (ja) | 超音波溶着装置 | |
| JP2008272767A (ja) | レーザ溶接装置及びレーザ溶接の品質管理方法 | |
| JP2006153710A (ja) | 溶接検査用プローブ及びそれを用いた溶接検査システム | |
| JPH05115986A (ja) | 超音波溶接のモニタ方法 | |
| JP5205926B2 (ja) | 溶接品質検査装置および溶接品質検査方法 | |
| US20110173819A1 (en) | Operating method for a power tool, especially a hand-held power tool | |
| JPH11197854A (ja) | 超音波溶着装置及び超音波溶着装置における溶着状態 検査方法 | |
| EP4196310A1 (en) | Self leveling stack assembly with front-loaded amplitude uniform ultrasonic welding horn | |
| KR100790775B1 (ko) | 마찰교반 점용접장치 | |
| JP2010110796A (ja) | レーザ加工モニタリング方法および装置 | |
| JP2007175876A (ja) | 超音波溶着器 | |
| JP2009222642A (ja) | 溶接検査システム | |
| JP2003205379A (ja) | レーザ溶接方法及びレーザ溶接用出射装置 | |
| JP2007075857A (ja) | シーム溶接機 | |
| JPH0360881A (ja) | 超音波溶接機 | |
| KR20040092263A (ko) | 용접물의 불량 검사 장치 | |
| JP2007175878A (ja) | 超音波溶着器 | |
| KR200408413Y1 (ko) | 청소가 용이한 스트립 용접부 감지장치 | |
| JP2009018314A (ja) | 非消耗電極アーク溶接装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20081031 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20110217 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20110309 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20110509 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20110707 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20110829 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20111117 |
|
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20111213 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20150120 Year of fee payment: 3 |
|
| R150 | Certificate of patent or registration of utility model |
Free format text: JAPANESE INTERMEDIATE CODE: R150 Ref document number: 4904473 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| LAPS | Cancellation because of no payment of annual fees |