JP2009187724A - Winding type lithium ion secondary battery - Google Patents
Winding type lithium ion secondary battery Download PDFInfo
- Publication number
- JP2009187724A JP2009187724A JP2008024745A JP2008024745A JP2009187724A JP 2009187724 A JP2009187724 A JP 2009187724A JP 2008024745 A JP2008024745 A JP 2008024745A JP 2008024745 A JP2008024745 A JP 2008024745A JP 2009187724 A JP2009187724 A JP 2009187724A
- Authority
- JP
- Japan
- Prior art keywords
- positive electrode
- separator
- lithium ion
- ion secondary
- secondary battery
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
- HBBGRARXTFLTSG-UHFFFAOYSA-N Lithium ion Chemical compound [Li+] HBBGRARXTFLTSG-UHFFFAOYSA-N 0.000 title claims abstract description 48
- 229910001416 lithium ion Inorganic materials 0.000 title claims abstract description 48
- 238000004804 winding Methods 0.000 title description 9
- 230000003068 static effect Effects 0.000 claims abstract description 27
- 239000011888 foil Substances 0.000 claims description 18
- 229910052751 metal Inorganic materials 0.000 claims description 11
- 239000002184 metal Substances 0.000 claims description 11
- 229920000098 polyolefin Polymers 0.000 abstract description 5
- 229910052782 aluminium Inorganic materials 0.000 description 12
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 11
- 239000000203 mixture Substances 0.000 description 11
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 9
- -1 lithium hexafluorophosphate Chemical compound 0.000 description 8
- 239000011889 copper foil Substances 0.000 description 7
- 229910052744 lithium Inorganic materials 0.000 description 7
- 230000002093 peripheral effect Effects 0.000 description 6
- 229910052723 transition metal Inorganic materials 0.000 description 6
- 239000000463 material Substances 0.000 description 5
- SECXISVLQFMRJM-UHFFFAOYSA-N N-Methylpyrrolidone Chemical compound CN1CCCC1=O SECXISVLQFMRJM-UHFFFAOYSA-N 0.000 description 4
- 239000011230 binding agent Substances 0.000 description 4
- 238000004519 manufacturing process Methods 0.000 description 4
- 239000007773 negative electrode material Substances 0.000 description 4
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 3
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 3
- WHXSMMKQMYFTQS-UHFFFAOYSA-N Lithium Chemical compound [Li] WHXSMMKQMYFTQS-UHFFFAOYSA-N 0.000 description 3
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 description 3
- 239000002033 PVDF binder Substances 0.000 description 3
- 229910003481 amorphous carbon Inorganic materials 0.000 description 3
- 239000013078 crystal Substances 0.000 description 3
- 239000008151 electrolyte solution Substances 0.000 description 3
- 238000011156 evaluation Methods 0.000 description 3
- 229920002981 polyvinylidene fluoride Polymers 0.000 description 3
- 239000007774 positive electrode material Substances 0.000 description 3
- 239000011347 resin Substances 0.000 description 3
- 229920005989 resin Polymers 0.000 description 3
- 238000012360 testing method Methods 0.000 description 3
- 238000003466 welding Methods 0.000 description 3
- 239000004698 Polyethylene Substances 0.000 description 2
- 239000011248 coating agent Substances 0.000 description 2
- 238000000576 coating method Methods 0.000 description 2
- 239000004020 conductor Substances 0.000 description 2
- 229910052802 copper Inorganic materials 0.000 description 2
- 239000010949 copper Substances 0.000 description 2
- QHGJSLXSVXVKHZ-UHFFFAOYSA-N dilithium;dioxido(dioxo)manganese Chemical compound [Li+].[Li+].[O-][Mn]([O-])(=O)=O QHGJSLXSVXVKHZ-UHFFFAOYSA-N 0.000 description 2
- 239000006185 dispersion Substances 0.000 description 2
- 238000001035 drying Methods 0.000 description 2
- 238000009413 insulation Methods 0.000 description 2
- 229910052742 iron Inorganic materials 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 229910052759 nickel Inorganic materials 0.000 description 2
- 239000011255 nonaqueous electrolyte Substances 0.000 description 2
- 229920000573 polyethylene Polymers 0.000 description 2
- 239000002904 solvent Substances 0.000 description 2
- 229920002943 EPDM rubber Polymers 0.000 description 1
- KMTRUDSVKNLOMY-UHFFFAOYSA-N Ethylene carbonate Chemical compound O=C1OCCO1 KMTRUDSVKNLOMY-UHFFFAOYSA-N 0.000 description 1
- 229910013870 LiPF 6 Inorganic materials 0.000 description 1
- PWHULOQIROXLJO-UHFFFAOYSA-N Manganese Chemical compound [Mn] PWHULOQIROXLJO-UHFFFAOYSA-N 0.000 description 1
- 239000004642 Polyimide Substances 0.000 description 1
- 239000004743 Polypropylene Substances 0.000 description 1
- 239000004820 Pressure-sensitive adhesive Substances 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 239000002390 adhesive tape Substances 0.000 description 1
- 229910021383 artificial graphite Inorganic materials 0.000 description 1
- 239000003575 carbonaceous material Substances 0.000 description 1
- 229910052804 chromium Inorganic materials 0.000 description 1
- 238000003776 cleavage reaction Methods 0.000 description 1
- CKFRRHLHAJZIIN-UHFFFAOYSA-N cobalt lithium Chemical compound [Li].[Co] CKFRRHLHAJZIIN-UHFFFAOYSA-N 0.000 description 1
- 239000000571 coke Substances 0.000 description 1
- 238000002485 combustion reaction Methods 0.000 description 1
- 230000000052 comparative effect Effects 0.000 description 1
- 230000008602 contraction Effects 0.000 description 1
- 238000002788 crimping Methods 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 230000006866 deterioration Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- IEJIGPNLZYLLBP-UHFFFAOYSA-N dimethyl carbonate Chemical compound COC(=O)OC IEJIGPNLZYLLBP-UHFFFAOYSA-N 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 229910002804 graphite Inorganic materials 0.000 description 1
- 239000010439 graphite Substances 0.000 description 1
- 239000007770 graphite material Substances 0.000 description 1
- 230000001678 irradiating effect Effects 0.000 description 1
- RSNHXDVSISOZOB-UHFFFAOYSA-N lithium nickel Chemical compound [Li].[Ni] RSNHXDVSISOZOB-UHFFFAOYSA-N 0.000 description 1
- 229910003002 lithium salt Inorganic materials 0.000 description 1
- 159000000002 lithium salts Chemical class 0.000 description 1
- 230000007257 malfunction Effects 0.000 description 1
- 229910052748 manganese Inorganic materials 0.000 description 1
- 239000011572 manganese Substances 0.000 description 1
- 239000012046 mixed solvent Substances 0.000 description 1
- 229910021382 natural graphite Inorganic materials 0.000 description 1
- 239000010450 olivine Substances 0.000 description 1
- 229910052609 olivine Inorganic materials 0.000 description 1
- 239000002245 particle Substances 0.000 description 1
- 238000007747 plating Methods 0.000 description 1
- 229920001721 polyimide Polymers 0.000 description 1
- 229920001155 polypropylene Polymers 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 230000002265 prevention Effects 0.000 description 1
- 238000012827 research and development Methods 0.000 description 1
- 230000007017 scission Effects 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 229910052596 spinel Inorganic materials 0.000 description 1
- 239000011029 spinel Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
Images


Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/50—Manufacturing or production processes characterised by the final manufactured product
Landscapes
- Cell Separators (AREA)
- Secondary Cells (AREA)
- Connection Of Batteries Or Terminals (AREA)
Abstract
【課題】ダイレクトタブにねじれを生じても正負電極間の短絡を抑制することができる捲回式リチウムイオン二次電池を提供する。
【解決手段】リチウムイオン二次電池は、有底円筒状の電池容器を有している。電池容器には電極群が収容されている。電極群は、正極板17と負極板18とがこれら両極板が直接接触しないように、セパレータ16を介して軸芯の周囲に捲回されている。正極板17から延出した正極ダイレクトタブ2は、延出端部が正極集電リング4の鍔部周縁に接合されている。セパレータ16には、静摩擦係数が0.6以下の多孔質ポリオレフィン系フィルムが使用されている。正極ダイレクトタブ2がねじれを生じてセパレータ16に接触しても、正極ダイレクトタブ2がセパレータ16の表面を滑る。
【選択図】図2Provided is a wound lithium ion secondary battery capable of suppressing a short circuit between positive and negative electrodes even when a direct tab is twisted.
A lithium ion secondary battery has a bottomed cylindrical battery container. An electrode group is accommodated in the battery container. In the electrode group, the positive electrode plate 17 and the negative electrode plate 18 are wound around the shaft core via the separator 16 so that the two electrode plates do not directly contact each other. The positive electrode direct tab 2 extending from the positive electrode plate 17 has an extended end portion joined to the periphery of the flange portion of the positive electrode current collecting ring 4. For the separator 16, a porous polyolefin film having a static friction coefficient of 0.6 or less is used. Even if the positive electrode direct tab 2 is twisted and contacts the separator 16, the positive electrode direct tab 2 slides on the surface of the separator 16.
[Selection] Figure 2
Description
本発明は捲回式リチウムイオン二次電池に係り、特に、金属箔の長手方向端部に集電用のダイレクトタブが形成された正負電極をセパレータを介して捲回した電極群を備えた捲回式リチウムイオン二次電池に関する。 The present invention relates to a wound-type lithium ion secondary battery, and more particularly, a winding provided with an electrode group in which positive and negative electrodes each having a current collecting direct tab formed at a longitudinal end portion of a metal foil are wound through a separator. The present invention relates to a rotary lithium ion secondary battery.
正負電極がセパレータを介して捲回された捲回式リチウムイオン二次電池は、さまざまな用途で使用されている。中でも、高エネルギー密度であるメリットを活かして、VTRカメラやノート型パソコン、携帯電話等のポータブル機器に使用されている。一方、電気自動車用や電力貯蔵用として高容量、高出力、更には高出力密度を目的とする大型の捲回式リチウムイオン二次電池の研究開発が活発に行われている。特に、自動車産業界においては、環境問題に対応すべく、動力源としてモータを用いる方式の電気自動車や内燃機関とモータとの両方を用いるハイブリッド方式の電気自動車の開発が進められており、その一部は既に実用化されている。このような電気自動車用の電源としても、捲回式リチウムイオン二次電池が注目されている。 A wound lithium ion secondary battery in which positive and negative electrodes are wound through a separator is used in various applications. Above all, taking advantage of the high energy density, it is used in portable devices such as VTR cameras, notebook computers and mobile phones. On the other hand, research and development of large-scale wound lithium ion secondary batteries for high-capacity, high-power, and high-power density are being actively conducted for electric vehicles and power storage. In particular, in the automobile industry, development of electric vehicles using a motor as a power source and hybrid electric vehicles using both an internal combustion engine and a motor is underway in order to deal with environmental problems. The part has already been put to practical use. As such a power source for an electric vehicle, a wound lithium ion secondary battery has attracted attention.
高出力を目的とした大型の捲回式リチウムイオン二次電池では、出力特性を向上させるために集電部分を含む電池内部の抵抗を低減することが重要となる。集電部分の抵抗を低減するためには金属箔の長手方向端部に形成されたダイレクトタブを用いて集電することが有効である(例えば、特許文献1参照)。 In a large-sized wound lithium ion secondary battery intended for high output, it is important to reduce the internal resistance of the battery including the current collecting portion in order to improve output characteristics. In order to reduce the resistance of the current collecting portion, it is effective to collect current using a direct tab formed at the end in the longitudinal direction of the metal foil (see, for example, Patent Document 1).
しかしながら、集電にダイレクトタブを用いた場合、ダイレクトタブが製造工程での捲回時や電池の充放電に伴う電極の膨張収縮等でねじれを生じる可能性がある。ダイレクトタブに一定以上のねじれが加わるとセパレータを圧迫し破損させることがある。この場合、正負電極間が短絡をおこす可能性があり、電池特性の著しい低下や機能停止にいたることとなる。さらに、短絡による発熱で電池内部の圧力が上昇し、高温の電解液等が電池外部に排出される可能性もある。 However, when a direct tab is used for current collection, the direct tab may be twisted during winding in the manufacturing process or due to expansion / contraction of the electrode accompanying charging / discharging of the battery. If a certain level of twist is applied to the direct tab, the separator may be pressed and damaged. In this case, there is a possibility that the positive and negative electrodes are short-circuited, leading to a significant deterioration in battery characteristics and a malfunction. Furthermore, the pressure inside the battery rises due to heat generated by the short circuit, and there is a possibility that a high-temperature electrolytic solution or the like is discharged outside the battery.
本発明は上記事案に鑑み、ダイレクトタブにねじれを生じても正負電極間の短絡を抑制することができる捲回式リチウムイオン二次電池を提供することを課題とする。 An object of the present invention is to provide a wound lithium ion secondary battery that can suppress a short circuit between positive and negative electrodes even if the direct tab is twisted.
上記課題を解決するために、本発明は、金属箔の長手方向端部に集電用のダイレクトタブが形成された正負電極をセパレータを介して捲回した電極群を備えた捲回式リチウムイオン二次電池において、前記セパレータの静摩擦係数が0.6以下であることを特徴とする。 In order to solve the above problems, the present invention provides a wound lithium ion comprising an electrode group in which positive and negative electrodes each having a current collecting direct tab formed on a longitudinal end of a metal foil are wound through a separator. In the secondary battery, the separator has a static friction coefficient of 0.6 or less.
本発明では、セパレータの静摩擦係数を0.6以下に設定することで、正負電極の捲回時や充放電時にダイレクトタブがねじれを生じてセパレータに接触しても、ダイレクトタブがセパレータの表面を滑りセパレータの破損が抑制されるため、正負電極間の短絡を抑制することができる。 In the present invention, by setting the coefficient of static friction of the separator to 0.6 or less, even if the direct tab twists and contacts the separator when the positive and negative electrodes are wound or charged / discharged, the direct tab does not touch the surface of the separator. Since the slip separator is prevented from being damaged, a short circuit between the positive and negative electrodes can be suppressed.
この場合において、セパレータの静摩擦係数を0.39以下とすることが好ましい。また、正極のダイレクトタブが、金属箔側の一部がセパレータを介して負極と対向していてもよい。 In this case, it is preferable that the static friction coefficient of the separator be 0.39 or less. In addition, the direct tab of the positive electrode may have a part on the metal foil side facing the negative electrode via a separator.
本発明によれば、セパレータの静摩擦係数を0.6以下に設定することで、正負電極の捲回時や充放電時にダイレクトタブがねじれを生じてセパレータに接触しても、ダイレクトタブがセパレータの表面を滑りセパレータの破損が抑制されるため、正負電極間の短絡を抑制することができる、という効果を得ることができる。 According to the present invention, by setting the coefficient of static friction of the separator to 0.6 or less, even if the direct tab twists and contacts the separator when the positive and negative electrodes are wound or charged / discharged, the direct tab is separated from the separator. Since the breakage of the separator is suppressed by sliding the surface, an effect that a short circuit between the positive and negative electrodes can be suppressed can be obtained.
以下、図面を参照して、本発明に係る捲回式リチウムイオン二次電池の実施の形態について説明する。 Hereinafter, embodiments of a wound lithium ion secondary battery according to the present invention will be described with reference to the drawings.
(構成)
図1に示すように、本実施形態の捲回式リチウムイオン二次電池20は、帯状の正負極板がセパレータを介して断面渦巻状に捲回された電極群6を備えている。電極群6は、有底円筒状でニッケルメッキが施された鉄製の電池容器7に収容されている。
(Constitution)
As shown in FIG. 1, the wound lithium ion
電極群6の上側には、中空状の軸芯1のほぼ延長線上に正極板からの電位を集電するためのアルミニウム製の正極集電リング4が配置されている。正極集電リング4は、軸芯1の上端部に固定されている。正極集電リング4の周囲から一体に張り出している鍔部周縁には、正極板から延出した正極ダイレクトタブ2の端部が超音波溶接で接合されている。正極集電リング4の上方には、正極外部端子となる円盤状の電池蓋が配置されている。電池蓋は、アルミニウム製の蓋ケース12と、蓋キャップ13と、気密を保つ弁押え14と、内圧上昇により開裂する開裂弁11とで構成されており、これらが積層されて蓋ケース12の周縁をカシメ固定することで組立てられている。正極集電リング4の上部には複数枚のアルミニウム製リボンを重ね合わせて構成した2本の正極リード板9のうち1本の一端が固定されており、蓋ケース12の下面には他の1本の一端が溶接されている。2本の正極リード板9の他端同士は溶接で接続されている。
On the upper side of the
一方、電極群6の下側には負極板からの電位を集電するための銅製の負極集電リング5が配置されている。負極集電リング5の内周面には軸芯1の下端部外周面が固定されている。負極集電リング5の外周縁には、負極板から延出した負極ダイレクトタブ3の端部が溶接されている。負極集電リング5の下部には電気的導通のための銅製の負極リード板8が溶接されており、負極リード板8は電池容器7の内底部に溶接されている。電池容器7の寸法は、本例では、高さ108.0mm、外径40mm、内径39mmに設定されている。
On the other hand, a copper negative electrode current collecting
電池蓋は、絶縁性及び耐熱性のEPDM樹脂製ガスケット10を介して電池容器7の上部にカシメ固定されている。このため、リチウムイオン二次電池20の内部は密封されている。また、電池容器7内には、図示を省略した非水電解液が注液されている。非水電解液には、エチレンカーボネートとジメチルカーボネートとの体積比1:1の混合溶媒中にリチウム塩として6フッ化リン酸リチウム(LiPF6)を1モル/リットル溶解したものが用いられている。
The battery lid is caulked and fixed to the upper part of the
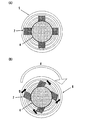
図2(A)に示すように、電極群6は、正極板17と負極板18とがこれら両極板が直接接触しないように、セパレータ16を介して捲回されている。このとき、正極ダイレクトタブ2と負極ダイレクトタブ3とが、それぞれ電極群6の互いに反対側の両端面に位置するように捲回されている。捲回方向は、正極ダイレクトタブ2側から見て左周りに設定されている。図3(A)に示すように、正極ダイレクトタブ2は、捲回された電極群6の端面で内周〜外周にわたる各位置の正極板から延出しており、各延出端部が正極集電リング4の鍔部周縁近傍に集められて鍔部周縁に接合されている(図1も参照)。本例では、正極集電リング4の鍔部周縁の4箇所に正極ダイレクトタブ2が接合されている(負極ダイレクトタブ3についても同様。)。
As shown in FIG. 2A, in the
また、図2(A)に示すように、セパレータ16は、端部が正極板17、負極板18の端部からはみ出して(正極集電リング4側に)位置するように配置されている。負極板18は、端部が正極板17の端部からはみ出して位置するように配置されている。このため、正極ダイレクトタブ2は、正極板17側の一部(符号2a参照)、すなわち、正極板17を構成するアルミニウム箔(金属箔)側の近傍がセパレータ16を介して負極板18と対向している。セパレータ16には、セパレータ16同士を2枚重ね合わせ、日本工業規格(JIS−K7125)に準じて測定したセパレータ・セパレータ間の静摩擦係数が0.6以下のものが使用されている。セパレータ16は、本例では、幅が90.5mm、厚さが16μmに設定されており、例えば、ポリエチレンフィルムに代表される多孔質ポリオレフィン系フィルムが使用されている。
Further, as shown in FIG. 2A, the
また、電極群6および正極集電リング4の鍔部周面全周には、絶縁被覆が施されている。絶縁被覆には、ポリイミド製の基材の片面にヘキサメタアクリレートの粘着剤が塗布された粘着テープが用いられている。粘着テープは鍔部周面から電極群6の外周面に亘って一重以上巻かれている。正極板17、負極板18、セパレータ16の長さを調整することで、電極群6の直径が38±0.1mmに設定されている。
In addition, an insulation coating is applied to the entire circumference of the collar portion peripheral surface of the
電極群6を構成する負極板18は、負極集電体として厚さ10μmの圧延銅箔(金属箔)を有している。圧延銅箔の両面には、負極活物質としてリチウムイオンを吸蔵、放出可能な非晶質炭素粉末を含む負極合剤が塗着されている。負極合剤には、例えば、非晶質炭素粉末の90重量部に対して、バインダ(結着材)のポリフッ化ビニリデン(以下、PVDFと略記する。)の10重量部が配合されている。圧延銅箔に負極合剤を塗着するときには、分散溶媒のN−メチル−2−ピロリドン(以下、NMPと略記する。)が用いられる。圧延銅箔の長手方向端部には、幅30mmの負極合剤の未塗着部が形成されている。未塗着部は櫛状(矩形状)に切り欠かれており、切り欠き残部で負極ダイレクトタブ3が形成されている。隣り合う負極ダイレクトタブ3の間隔が50mm、負極ダイレクトタブ3の幅が5mmに設定されている。換言すれば、負極ダイレクトタブ(切り欠き残部)3は、圧延銅箔の長手方向と交差する方向に圧延銅箔端部から延出している。負極板18は、乾燥後、厚さが70μmとなるように、加熱可能なロールプレス機でプレス加工され、幅が88mmに裁断されている。
The
一方、正極板17は、正極集電体として厚さ20μmのアルミニウム箔(金属箔)を有している。アルミニウム箔の両面には、正極活物質としてマンガン酸リチウム等のリチウム遷移金属複酸化物を含む正極合剤が塗着されている。正極合剤には、例えば、リチウム遷移金属複酸化物の100重量部に対して、導電材の鱗片状黒鉛の10重量部およびバインダのPVDFの5重量部が配合されている。アルミニウム箔に正極合剤を塗着するときには、分散溶媒のNMPが用いられる。アルミニウム箔の長手方向端部には、負極板18と同様に幅30mmの正極合剤の未塗着部が形成されており、正極ダイレクトタブ2が形成されている。隣り合う正極ダイレクトタブ2の間隔が50mm、正極ダイレクトタブ2の幅が5mmに設定されている。換言すれば、正極ダイレクトタブ(切り欠き残部)2は、アルミニウム箔の長手方向と交差する方向にアルミニウム箔端部から延出している。正極板17は、乾燥後、厚さが90μmとなるように、負極板18と同様にプレス加工され、幅が84mmに裁断されている。
On the other hand, the
(電池組立)
リチウムイオン二次電池20の組立は以下の手順で行う。すなわち、正極板17および負極板18をセパレータ16を介して軸芯1の周囲に捲回装置で捲回し電極群6を作製する。このとき、正極ダイレクトタブ2の一部がセパレータ16を介して負極板18と対向する。電極群6の両端面からそれぞれ延出している正極ダイレクトタブ2および負極ダイレクトタブ3を正極集電リング4および負極集電リング5にそれぞれ溶接した後、電池容器7内に電極群6を挿入する。負極集電リング5に予め溶接した負極リード板8を電池容器7の内底部に溶接する。電池容器7の上端部から9mm分下側の位置に電池蓋をカシメ固定するため、段付け加工を施して段付け部を形成する。正極集電リング4および電池蓋を正極リード板9で接続した後、電池容器7内に非水電解液を軸芯1の中空部分から注液して電極群6を非水電解液に浸潤させる。その後、ガスケット10と電池蓋とを段付け部の上にカシメ固定することで、リチウムイオン二次電池20の組立を完成させる。
(Battery assembly)
The lithium ion
次に、本実施形態のリチウムイオン二次電池20の作用等について、セパレータ16の作用を中心に説明する。
Next, the operation of the lithium ion
本実施形態のリチウムイオン二次電池20では、正極ダイレクトタブ2が形成された正極板17および負極ダイレクトタブ3が形成された負極板18がセパレータ16を介して捲回された電極群6を備えている。電池組立時に電極群6を作製するときや、電池の充放電に伴い正極板17および負極板18が膨張収縮することで体積変化を生じたとき等には、正極ダイレクトタブ2、負極ダイレクトタブ3にねじれを生じることとなる。すなわち、図3(B)に示すように、電極群6を正極集電リング4側からみたときは、電極群6に対して、電池組立時や充放電時に右回り(図の矢印A方向)の力が加わると、正極ダイレクトタブ2にねじれを生じる。このとき、正極ダイレクトタブ2がセパレータ16に対して直角ではなく斜めに接触してセパレータ16を圧迫する(図の矢印B方向)。そうすると、図2(B)に示すように、正極ダイレクトタブ2がセパレータ16や負極板18の端部を変形させる。
The lithium ion
このような場合、従来の捲回式リチウムイオン二次電池では、正極ダイレクトタブに一定量以上のねじれを生じると、金属製の正極ダイレクトタブが樹脂製フィルムのセパレータを破損することがある。セパレータが破損すると電極群内で正極板および負極板間の短絡が発生し、電池性能の低下、ひいては、電池機能の停止に至り、電池の信頼性を損なうこととなる。 In such a case, in the conventional wound type lithium ion secondary battery, when the positive electrode direct tab is twisted more than a certain amount, the metal positive electrode direct tab may damage the resin film separator. When the separator is broken, a short circuit occurs between the positive electrode plate and the negative electrode plate in the electrode group, resulting in a decrease in battery performance and, consequently, a battery function stop, which impairs battery reliability.
ここで、ダイレクトタブがセパレータに斜めに接触するときの力のかかり方について説明する。一般に、物体が平面に一定の力で斜めに押し当てられたときは、物体から平面に与えられる力を当該平面に直交する直交成分と当該平面に沿う水平成分とに分解することができる。水平成分の力が、垂直成分の力と平面の静摩擦係数との積(垂直成分の力×静摩擦係数)より大きくなると物体が平面上を滑ることとなる。換言すれば、セパレータの静摩擦係数を小さくすると、ダイレクトタブがセパレータに斜めに接触してもセパレータの表面を滑りやすくなる。 Here, how to apply a force when the direct tab contacts the separator obliquely will be described. In general, when an object is pressed obliquely against a plane with a constant force, the force applied from the object to the plane can be decomposed into an orthogonal component orthogonal to the plane and a horizontal component along the plane. When the force of the horizontal component becomes larger than the product of the force of the vertical component and the static friction coefficient of the plane (vertical component force × static friction coefficient), the object slides on the plane. In other words, when the coefficient of static friction of the separator is reduced, the surface of the separator is easily slid even if the direct tab contacts the separator obliquely.
本実施形態では、セパレータ16として静摩擦係数が0.6以下の多孔質ポリオレフィン系フィルムが使用されている。このため、正極板17および負極板18の捲回時や電池の充放電時に、正極ダイレクトタブ2や負極ダイレクトタブ3がねじれを生じてセパレータ16に接触しても、正極ダイレクトタブ2、負極ダイレクトタブ3がセパレータ16の表面を滑ることとなる。これにより、セパレータ16の破損が抑制されるので、正極板17および負極板18間の短絡を抑制することができ、電池の信頼性を確保することができる。
In this embodiment, a porous polyolefin film having a static friction coefficient of 0.6 or less is used as the
また、本実施形態では、負極板18の端部が正極板17の端部からはみ出して位置するように配置されており、正極ダイレクトタブ2の正極板17側の一部がセパレータ16を介して負極板18と対向している(図2(A)の符号2a参照)。正極ダイレクトタブ2が正極合剤の未塗着部に形成されているため、正極ダイレクトタブ2とセパレータ16との間に空隙が形成される。この空隙の分で、正極ダイレクトタブ2がねじれを生じても、セパレータ16を圧迫する力を低減することができる。これにより、セパレータ16の破損が抑制されるので、正極板17および負極板18間の短絡を抑制し電池機能を確保することができる。
Further, in the present embodiment, the end of the
なお、本実施形態では、セパレータ16として静摩擦係数を0.6以下とする例を示したが、セパレータ16の破損抑制を確実にし、電池信頼性を向上させることを考慮すれば、静摩擦係数を0.39以下とすることが好ましい。また、本実施形態では、セパレータの材質としてポリエチレンフィルムを例示したが、本発明はこれに限定されるものではなく、静摩擦係数が0.6以下であればいかなる材質のものも使用することができる。このような材質として、例えば、ポリプロピレンフィルム等のポリオレフィン系フィルムを挙げることができる。
In the present embodiment, an example in which the static friction coefficient is set to 0.6 or less is shown as the
また、本実施形態では、アルミニウム箔の正極合剤の未塗着部および圧延銅箔の負極合剤の未塗着部をそれぞれ櫛状に切り欠くことにより正極ダイレクトタブ2および負極ダイレクトタブ3を形成する例を示したが、本発明はこれに制限されるものではなく、例えば、三角状等としてもよい。また、正極ダイレクトタブ2、負極ダイレクトタブ3の幅や間隔等にも制限のないことはもちろんである。
Further, in this embodiment, the positive electrode
更に、本実施形態では、円筒型のリチウムイオン二次電池20を例示したが、本発明は電池形状に制限されるものではなく、正極板および負極板が捲回された捲回式のリチウムイオン二次電池に適用することができる。円筒型以外の電池形状として、例えば、角型等の多角形状の電池に適用することもできる。
Furthermore, in the present embodiment, the cylindrical lithium ion
また更に、本実施形態では、正極活物質にマンガン酸リチウム、負極活物質に非晶質炭素をそれぞれ例示したが、本発明はこれらに限定されるものではない。正極活物質としては、例えば、コバルト酸リチウムに代表されるリチウムコバルト複酸化物、ニッケル酸リチウムに代表されるリチウムニッケル複酸化物等のリチウム遷移金属複酸化物を用いることができる。また、結晶中のリチウムやマンガン等の遷移金属元素の一部をFe、Co、Ni、Cr、Al、Mg等の遷移金属元素で置換またはドープしたリチウム遷移金属複酸化物を用いてもよい。更に、結晶構造についても特に制限はなく、スピネル型、層状型、オリビン型のいずれの結晶構造を有していてもよい。一方、負極活物質としては、リチウムイオン二次電池に通常用いられる炭素材を用いることができる。本実施形態以外の負極活物質としては、例えば、天然黒鉛や人造黒鉛の各種黒鉛材やコークス等を挙げることができ、その粒子形状においても、鱗片状、球状、繊維状、塊状等、特に制限されるものではない。また、導電材やバインダ等についても特に制限はなく、通常、リチウムイオン二次電池に使用される材料を用いてもよい。 Furthermore, in the present embodiment, lithium manganate is exemplified as the positive electrode active material and amorphous carbon is exemplified as the negative electrode active material, but the present invention is not limited to these. As the positive electrode active material, for example, lithium transition metal double oxides such as lithium cobalt double oxide typified by lithium cobaltate and lithium nickel double oxide typified by lithium nickelate can be used. Alternatively, a lithium transition metal double oxide in which a part of a transition metal element such as lithium or manganese in the crystal is substituted or doped with a transition metal element such as Fe, Co, Ni, Cr, Al, or Mg may be used. Further, there is no particular limitation on the crystal structure, and the crystal structure may be any of spinel type, layered type, and olivine type. On the other hand, as a negative electrode active material, the carbon material normally used for a lithium ion secondary battery can be used. Examples of the negative electrode active material other than the present embodiment include natural graphite and various graphite materials such as artificial graphite, coke, and the like, and the particle shape is also particularly limited, such as scaly, spherical, fibrous, or massive. Is not to be done. Moreover, there is no restriction | limiting in particular about a electrically conductive material, a binder, etc., You may use the material normally used for a lithium ion secondary battery.
次に、本実施形態に従い作製したリチウムイオン二次電池20の実施例について説明する。なお、比較のために作製した比較例についても併記する。
Next, examples of the lithium ion
下表1に示すように、本実施例では、静摩擦係数の異なる6種類のポリオレフィン系フィルムのセパレータを用いた。静摩擦係数は、同一のセパレータを2枚重ね合わせ、セパレータ・セパレータ間の静摩擦係数を日本工業規格(JIS−K7125)に準じた方法で測定したものである。各セパレータの静摩擦係数は、セパレータ1では0.28、セパレータ2では0.32、セパレータ3では0.39、セパレータ4では0.55、セパレータ5では0.60、セパレータ6では0.78であった。
As shown in Table 1 below, in this example, six types of polyolefin film separators having different static friction coefficients were used. The static friction coefficient is obtained by overlapping two identical separators and measuring the static friction coefficient between the separator and the separator by a method according to Japanese Industrial Standard (JIS-K7125). The static friction coefficient of each separator was 0.28 for separator 1, 0.32 for

(電池作製)
各セパレータをそれぞれ用いた電極群6をセパレータ毎に10個ずつ作製した。電極群6の両端面からそれぞれ延出している正極ダイレクトタブ2および負極ダイレクトタブ3を正極集電リング4および負極集電リング5にそれぞれ溶接した後、セパレータ毎に作製した10個の電極群6のうち5個については、正極集電リング4を固定し電極群6を正極集電リング側から見て右回りに45°回転させることで、正極ダイレクトタブ2にねじれを加えた。得られた電極群6を用いてリチウムイオン二次電池を作製した。
(Battery production)
Ten
(試験評価1)
作製した電池を0.1Cの電流値で4.1Vまで充電した後、25℃の恒温槽内に3日間放置した。放置後の電池電圧を測定し、4.0V以下に電圧が低下した電池数をカウントした。セパレータ毎にねじれを加えた場合と加えていない場合とで電圧低下を生じた電池の割合を百分率で求めた。求めた電圧低下電池の割合を下表2に示す。
(Test evaluation 1)
The produced battery was charged to 4.1 V with a current value of 0.1 C, and then left in a thermostat at 25 ° C. for 3 days. The battery voltage after standing was measured, and the number of batteries whose voltage dropped to 4.0 V or less was counted. The percentage of the battery that caused a voltage drop was calculated as a percentage when the twist was applied to each separator and when it was not added. Table 2 shows the obtained ratio of the voltage drop battery.
表2に示すように、ねじれを加えなかった場合は、いずれのセパレータを用いても、全てのリチウムイオン二次電池で電圧低下が発生しなかった。ところが、ねじれを加えた場合は、静摩擦係数が0.6以下のセパレータ1〜セパレータ5を用いたリチウムイオン二次電池では電圧低下が発生しなかったのに対し、静摩擦係数が0.78のセパレータ6を用いたリチウムイオン二次電池では40%の割合で電圧低下が発生した。電圧低下が発生したリチウムイオン二次電池を解体し、電圧低下の原因を調べたところ、電圧低下の発生した全てのリチウムイオン二次電池で正極ダイレクトタブによる短絡の発生が確認された。このことから、静摩擦係数が0.6以下のセパレータを用いることで正極ダイレクトタブ2による正極板17および負極板18間の短絡を抑制できることが判明した。
As shown in Table 2, when no twist was applied, no voltage drop occurred in all lithium ion secondary batteries, regardless of which separator was used. However, when a twist is applied, a voltage drop does not occur in the lithium ion secondary battery using the separators 1 to 5 having a static friction coefficient of 0.6 or less, whereas a separator having a static friction coefficient of 0.78. In the lithium ion secondary battery using 6, voltage drop occurred at a rate of 40%. When the lithium ion secondary battery in which the voltage drop occurred was disassembled and the cause of the voltage drop was examined, occurrence of a short circuit due to the positive electrode direct tab was confirmed in all the lithium ion secondary batteries in which the voltage drop occurred. From this, it was found that the short circuit between the
(試験評価2)
試験評価1の電池電圧の測定後、各リチウムイオン二次電池を2.7Vまで放電し、解体した。正極板の捲き終わりから10本目の正極ダイレクトタブの内側に対向する部分のセパレータを電池毎に取り出した。取り出したセパレータを紫外線硬化樹脂に包埋し、紫外線を照射して硬化させた後、正極ダイレクトタブが接していた部分を正極ダイレクトタブに対して垂直方向に切断し断面を観察し、正極ダイレクトタブによってつけられたキズの深さが8μm以上の電池本数をカウントした。セパレータ毎にねじれを加えた場合と加えていない場合とで正極ダイレクトタブによる深さ8μm以上のキズの割合を百分率で求めた。求めたキズの割合を下表3に示す。
(Test evaluation 2)
After measuring the battery voltage in Test Evaluation 1, each lithium ion secondary battery was discharged to 2.7 V and disassembled. The separator of the part facing the inner side of the tenth positive electrode direct tab from the end of the positive electrode plate was taken out for each battery. The separator taken out was embedded in an ultraviolet curable resin and cured by irradiating with ultraviolet rays, and then the portion where the positive electrode direct tab was in contact was cut in a direction perpendicular to the positive electrode direct tab, and the cross section was observed. The number of batteries with a scratch depth of 8 μm or more was counted. The percentage of scratches with a depth of 8 μm or more due to the positive electrode direct tab was determined as a percentage depending on whether or not twist was added for each separator. The obtained scratch ratio is shown in Table 3 below.
表3に示すように、ねじれを加えなかった場合は、いずれのセパレータを用いても、全てのリチウムイオン二次電池で深さ8μm以上のキズが発生しなかった。ところが、ねじれを加えた場合は、深さ8μm以上のキズの発生が認められ、その割合は、静摩擦係数が0.55のセパレータ4を用いたリチウムイオン二次電池で20%、静摩擦係数が0.60のセパレータ5を用いたリチウムイオン二次電池で40%、静摩擦係数が0.78のセパレータ6を用いたリチウムイオン二次電池で80%であった。これに対して、静摩擦係数が0.39以下のセパレータ1〜セパレータ3を用いたリチウムイオン二次電池では、深さ8μm以上のキズの発生が認められなかった。このことから、静摩擦係数0.39以下のセパレータを用いることで一層安全で信頼性に優れるリチウムイオン二次電池を得ることができることが明らかとなった。
As shown in Table 3, when no twist was applied, no cracks having a depth of 8 μm or more were generated in all lithium ion secondary batteries, regardless of which separator was used. However, when twist is applied, scratches with a depth of 8 μm or more are observed, and the ratio is 20% for the lithium ion secondary battery using the
本発明はダイレクトタブにねじれを生じても正負電極間の短絡を抑制することができる捲回式リチウムイオン二次電池を提供するため、捲回式リチウムイオン二次電池の製造、販売に寄与するので、産業上の利用可能性を有する。 The present invention provides a wound type lithium ion secondary battery that can suppress a short circuit between positive and negative electrodes even if the direct tab is twisted, and thus contributes to the manufacture and sale of a wound type lithium ion secondary battery. So it has industrial applicability.
2 正極ダイレクトタブ
2a 正極ダイレクトタブの一部(金属箔側の一部)
3 負極ダイレクトタブ
6 電極群
16 セパレータ
17 正極板
18 負極板
20 捲回式リチウムイオン二次電池
2 Positive electrode
3 Negative electrode
Claims (3)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008024745A JP2009187724A (en) | 2008-02-05 | 2008-02-05 | Winding type lithium ion secondary battery |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2008024745A JP2009187724A (en) | 2008-02-05 | 2008-02-05 | Winding type lithium ion secondary battery |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| JP2009187724A true JP2009187724A (en) | 2009-08-20 |
Family
ID=41070768
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2008024745A Pending JP2009187724A (en) | 2008-02-05 | 2008-02-05 | Winding type lithium ion secondary battery |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP2009187724A (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2009295389A (en) * | 2008-06-04 | 2009-12-17 | Hitachi Vehicle Energy Ltd | Lithium-ion secondary battery |
| US9017859B2 (en) | 2011-04-19 | 2015-04-28 | Industrial Technology Research Institute | Secondary battery structure |
| US9088023B2 (en) | 2011-03-29 | 2015-07-21 | Industrial Technology Research Institute | End cover assembly of battery |
| JP2023174383A (en) * | 2022-05-27 | 2023-12-07 | 旭化成株式会社 | Separator for power storage devices and power storage devices including the same |
| JP2024092194A (en) * | 2022-12-26 | 2024-07-08 | プライムアースEvエナジー株式会社 | Nonaqueous secondary battery and method for manufacturing the same |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0992335A (en) * | 1995-09-27 | 1997-04-04 | Sony Corp | Cylindrical secondary battery |
| JPH11111261A (en) * | 1997-09-30 | 1999-04-23 | Sanyo Electric Co Ltd | Manufacture of cylindrical non-aqueous electrolyte secondary battery |
| JPH11115084A (en) * | 1997-10-14 | 1999-04-27 | Ube Ind Ltd | Laminated porous film |
| JPH11185726A (en) * | 1997-12-17 | 1999-07-09 | Sanyo Electric Co Ltd | Cylindrical battery |
| JP2002117825A (en) * | 2000-10-06 | 2002-04-19 | Denso Corp | Method for manufacturing flat-shaped wound electrode body |
| JP2002190314A (en) * | 2000-12-20 | 2002-07-05 | Nissan Motor Co Ltd | Battery |
| JP2005171230A (en) * | 2003-11-05 | 2005-06-30 | Toray Ind Inc | Biaxially oriented microporous film and method for producing the same |
| JP2007165117A (en) * | 2005-12-14 | 2007-06-28 | Hitachi Vehicle Energy Ltd | Secondary battery |
-
2008
- 2008-02-05 JP JP2008024745A patent/JP2009187724A/en active Pending
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH0992335A (en) * | 1995-09-27 | 1997-04-04 | Sony Corp | Cylindrical secondary battery |
| JPH11111261A (en) * | 1997-09-30 | 1999-04-23 | Sanyo Electric Co Ltd | Manufacture of cylindrical non-aqueous electrolyte secondary battery |
| JPH11115084A (en) * | 1997-10-14 | 1999-04-27 | Ube Ind Ltd | Laminated porous film |
| JPH11185726A (en) * | 1997-12-17 | 1999-07-09 | Sanyo Electric Co Ltd | Cylindrical battery |
| JP2002117825A (en) * | 2000-10-06 | 2002-04-19 | Denso Corp | Method for manufacturing flat-shaped wound electrode body |
| JP2002190314A (en) * | 2000-12-20 | 2002-07-05 | Nissan Motor Co Ltd | Battery |
| JP2005171230A (en) * | 2003-11-05 | 2005-06-30 | Toray Ind Inc | Biaxially oriented microporous film and method for producing the same |
| JP2007165117A (en) * | 2005-12-14 | 2007-06-28 | Hitachi Vehicle Energy Ltd | Secondary battery |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2009295389A (en) * | 2008-06-04 | 2009-12-17 | Hitachi Vehicle Energy Ltd | Lithium-ion secondary battery |
| US9088023B2 (en) | 2011-03-29 | 2015-07-21 | Industrial Technology Research Institute | End cover assembly of battery |
| US9017859B2 (en) | 2011-04-19 | 2015-04-28 | Industrial Technology Research Institute | Secondary battery structure |
| JP2023174383A (en) * | 2022-05-27 | 2023-12-07 | 旭化成株式会社 | Separator for power storage devices and power storage devices including the same |
| JP2024092194A (en) * | 2022-12-26 | 2024-07-08 | プライムアースEvエナジー株式会社 | Nonaqueous secondary battery and method for manufacturing the same |
| JP7675695B2 (en) | 2022-12-26 | 2025-05-13 | トヨタバッテリー株式会社 | Nonaqueous secondary battery and method for manufacturing the same |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5274026B2 (en) | Square battery | |
| JP5242364B2 (en) | Flat secondary battery | |
| CN103477490B (en) | Rolled electrode assembly pattern-coated with active material and secondary battery including same | |
| JP5257700B2 (en) | Lithium secondary battery | |
| US20090297940A1 (en) | Prismatic battery | |
| KR101629499B1 (en) | Electrode assembly and secondary battery comprising the same | |
| CN101599555A (en) | Lithium secondary battery | |
| JP2009289672A (en) | Wound type power storage device | |
| JP2012190739A (en) | Secondary battery | |
| JP5334429B2 (en) | Lithium secondary battery | |
| WO2014188501A1 (en) | Nonaqueous electrolyte secondary cell | |
| JP5232751B2 (en) | Lithium ion secondary battery | |
| JP5433164B2 (en) | Lithium ion secondary battery | |
| CN111480250B (en) | Positive electrode for lithium ion secondary battery and lithium ion secondary battery using same | |
| JP2006012703A (en) | Secondary battery | |
| JP2003243036A (en) | Cylindrical lithium secondary battery | |
| JP3511476B2 (en) | Lithium secondary battery | |
| JP2006040772A (en) | Lithium ion battery | |
| JP2007123009A (en) | Wound type battery | |
| JP5776948B2 (en) | Lithium secondary battery and manufacturing method thereof | |
| JP2000182656A (en) | Lithium secondary battery | |
| JP5254910B2 (en) | Lithium ion secondary battery | |
| KR20230054267A (en) | Lithium secondary battery | |
| JP4548070B2 (en) | Secondary battery | |
| JP4876380B2 (en) | Method for manufacturing lithium secondary battery |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20100219 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20120425 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20120515 |
|
| A521 | Request for written amendment filed |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20120621 |
|
| A02 | Decision of refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A02 Effective date: 20120731 |