JP2020171955A - Continuous steel casting method - Google Patents
Continuous steel casting method Download PDFInfo
- Publication number
- JP2020171955A JP2020171955A JP2019076463A JP2019076463A JP2020171955A JP 2020171955 A JP2020171955 A JP 2020171955A JP 2019076463 A JP2019076463 A JP 2019076463A JP 2019076463 A JP2019076463 A JP 2019076463A JP 2020171955 A JP2020171955 A JP 2020171955A
- Authority
- JP
- Japan
- Prior art keywords
- molten steel
- long nozzle
- tundish
- steel
- opening hole
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Landscapes
- Continuous Casting (AREA)
- Casting Support Devices, Ladles, And Melt Control Thereby (AREA)
Abstract
【課題】ロングノズルの損傷、溶鋼漏れ等のトラブルを生じさせずに、また、溶鋼歩留りも悪化させることなく、非金属介在物の除去を十分に行うことができ、清浄度の高い鋼鋳片を製造可能な鋼の連続鋳造方法を提供する。【解決手段】ロングノズル20は、底面部23に開口する底面開口孔24と、側面に開口する側面開口孔25と、を有しており、底面部23の全面積をS(m2)、底面開口孔24の開口面積をSB(m2)、側面開口孔25の総開口面積をST(m2)、定常時におけるロングノズル20内の流速をv(m/s)とした場合に、(1)式:0.14≦SB/S、(2)式:0<SB/(SB+ST)≦0.55、(3)式:v2×(S−SB)≧0.0035、を満足するとともに、定常鋳造時における底面開口孔24からの溶鋼流出量が3t/minを超えないように、ロングノズル20を介して、取鍋からタンディッシュに向けて溶鋼を注入する。【選択図】図2[Problem] To sufficiently remove non-metallic inclusions without causing troubles such as damage to a long nozzle and leakage of molten steel, and without deteriorating the yield of molten steel, and having a high degree of cleanliness. To provide a continuous casting method for steel capable of producing A long nozzle (20) has a bottom opening hole (24) opening to a bottom part (23) and a side opening hole (25) opening to a side surface. When the opening area of the opening holes 24 is SB (m2), the total opening area of the side opening holes 25 is ST (m2), and the flow velocity in the long nozzle 20 at steady state is v (m/s), (1) Formula: 0.14 ≤ SB / S, Formula (2): 0 < SB / (SB + ST) ≤ 0.55, Formula (3): v2 × (S - SB) ≥ 0.0035, and steady Molten steel is poured from the ladle toward the tundish through the long nozzle 20 so that the molten steel flow rate from the bottom opening 24 during casting does not exceed 3 t/min. [Selection drawing] Fig. 2
Description
本発明は、取鍋からタンディッシュに向けて溶鋼を注入し、このタンディッシュから連続鋳造用鋳型に前記溶鋼を供給し、鋳片を連続的に鋳造する鋼の連続鋳造方法に関するものである。 The present invention relates to a method for continuously casting steel by injecting molten steel from a ladle toward a tundish, supplying the molten steel from the tundish to a mold for continuous casting, and continuously casting slabs.
例えば、自動車用外板向け極低炭素鋼板、缶用低炭ブリキ鋼板向けの低炭アルミキルド鋼板、鋼管向け熱延鋼板、自動車用の構造部材等に用いられるハイテン鋼においては、高加工性や良好な表面形状が求められる。
これらの高加工性や良好な表面形状を実現するためには、鋼中の非金属介在物およびそれらを含む表面や内部欠陥が大きな課題となる。したがって、高加工性、良好な表面形状が必要な場合、溶鋼から非金属介在物を除去して清浄性を高めることが必要である。
For example, ultra-low carbon steel sheets for outer panels for automobiles, low-carbon aluminum killed steel sheets for low-carbon tin steel sheets for cans, hot-rolled steel sheets for steel pipes, high-tensile steel used for structural members for automobiles, etc. A good surface shape is required.
In order to realize these high workability and good surface shape, non-metal inclusions in steel and surface and internal defects containing them are major issues. Therefore, when high workability and good surface shape are required, it is necessary to remove non-metal inclusions from the molten steel to improve the cleanliness.
従来は、タンディッシュに堰を設けて溶鋼の上昇流を形成したり、連続鋳造の鋳型内で電磁ブレーキを用いて浸漬ノズルからの吐出流を制動させたりすることで、非金属介在物の浮上除去を行っていたが、十分に除去されておらず、非金属介在物が最終成品である薄鋼板まで持ち込まれ、有害なアルミナクラスターや、非金属介在物が一定量残存している。 Conventionally, non-metal inclusions have floated by providing a weir in the tundish to form an ascending flow of molten steel or by using an electromagnetic brake to brake the discharge flow from the immersion nozzle in a continuously cast mold. Although it was removed, it was not sufficiently removed, and non-metal inclusions were brought to the final product, thin steel sheet, and harmful alumina clusters and non-metal inclusions remained in a certain amount.
そこで、非金属介在物のさらなる除去を行うために、例えば、特許文献1〜4に示すように、タンディッシュ内の溶鋼において非金属介在物の浮上分離を促進する技術が提案されている。
特許文献1においては、スラグ・非金属介在物起因の欠陥を生じさせないために、タンディッシュの注入流落下領域に凹部を形成して撹拌することによって、スラグの浮上を図るものである。
Therefore, in order to further remove the non-metal inclusions, for example, as shown in
In
特許文献2においては、タンディッシュに溶鋼を注入するロングノズルについて底部を持つ構造とするとともに横方向に開口した横孔を形成し、この横孔から溶鋼を吐出することによって上昇流を生じさせ、タンディッシュ内での非金属介在物の浮上を効果的に行う溶鋼注入方法を提案している。
特許文献3においては、特許文献2と同様に、ロングノズルの下端部を閉塞し、側面に上向きの吐出口を持つロングノズルを提案し、タンディッシュ内における溶鋼の滞留時間を長くし、非金属介在物の浮上分離を効果的に行うものとしている。
特許文献4においては、特許文献2、3と同様の考え方をもつものであり、ノズルに底とその周面に形成された吐出用開口部1個を持つロングノズルを提案することで、タンディッシュ内において溶鋼中の介在物が浮上するのに十分な時間を確保するようにしている。
In
Similar to
ところで、特許文献1のように、タンディッシュに凹部を形成した場合には、連続鋳造が終わった後、タンディッシュ内に残存する溶鋼量が多くなり、溶鋼歩留の低下に繋がるため、実生産プロセスとしては、コスト的に成り立たない。
また、特許文献2〜4に示すように、ロングノズルの下端を閉塞した場合には、取鍋から溶鋼の注入を開始する際に、大きな溶鋼静圧を持った運動量の大きな溶鋼落下によって大きな衝撃力がかかり、ロングノズルが損傷し、損傷したロングノズルの破片がタンディッシュ内に落下するトラブルが発生するおそれがあった。また、上述の衝撃力がロングノズルを把持する把持力よりも大きくなってロングノズルと取鍋下部に隙間があき、隙間から溶鋼が漏れるおそれがあった。このように、操業上の問題があるため、実用化が出来ていない。
By the way, as in
Further, as shown in
本発明は、前述した状況に鑑みてなされたものであって、ロングノズルの損傷、溶鋼漏れ等のトラブルを生じさせずに、また、溶鋼歩留りも悪化させることなく、非金属介在物の除去を十分に行うことができ、清浄度の高い鋼鋳片を製造可能な鋼の連続鋳造方法を提供することを目的とする。 The present invention has been made in view of the above-mentioned situation, and removes non-metal inclusions without causing troubles such as damage to a long nozzle and leakage of molten steel, and without deteriorating the yield of molten steel. It is an object of the present invention to provide a continuous casting method of steel which can be sufficiently performed and can produce steel slabs having high cleanliness.
上記課題を解決するために、本発明者らが鋭意検討した結果、以下に示すような知見を得た。
本発明者らは、上記課題を解決するためには、ロングノズルを活用することが重要であると考えた。すなわち、ロングノズル内で溶鋼を乱流、撹拌状態に保ち、微細な非金属介在物の凝集を促進する機能を持たせることを、損傷、溶鋼漏れ等のトラブルを生じさせずに活用する方法を見つけ出すことである。ロングノズル内で非金属介在物を凝集させて浮上しやすくすれば、タンディッシュに凹部を形成する必要がなくなるため、溶鋼歩留りも悪化させることなく、非金属介在物の除去を行うことができる。
そこで、ロングノズルの下方の溶鋼の吐出口を変化させて、ロングノズルの損傷、溶鋼漏れ等のトラブルを生じさせることなく、ロングノズル内の乱流、撹拌エネルギーを用いることによって、非金属介在物の凝集を促進して、非金属介在物を効率的に浮上分離して個数密度を減少させることができる、ロングノズルの形状を解明することを試みた。
As a result of diligent studies by the present inventors in order to solve the above problems, the following findings were obtained.
The present inventors considered that it is important to utilize a long nozzle in order to solve the above problems. That is, a method of utilizing the function of keeping the molten steel in a turbulent flow and stirring state in the long nozzle and promoting the aggregation of fine non-metal inclusions without causing troubles such as damage and leakage of the molten steel. To find out. If the non-metal inclusions are aggregated in the long nozzle to facilitate floating, it is not necessary to form a recess in the tundish, so that the non-metal inclusions can be removed without deteriorating the molten steel yield.
Therefore, by changing the discharge port of the molten steel below the long nozzle and using the turbulent flow and stirring energy in the long nozzle without causing troubles such as damage to the long nozzle and leakage of molten steel, non-metal inclusions Attempts have been made to elucidate the shape of long nozzles, which can promote agglomeration of non-metal inclusions and efficiently levitate and separate to reduce the number density.
本発明者は、連続鋳造装置において低炭アルミキルド鋼を鋳造する際に、ロングノズル内溶鋼流速v(m/s)、および、ロングノズルの下方の溶鋼の吐出口を変化させて、取鍋、タンディッシュ、鋳片で、溶鋼メタルのサンプリング、鋳片サンプルの採取を行い、それらの成分分析、非金属介在物の調査、解析を詳細に行った。非金属介在物の調査は、スライム抽出法で行った。鋳片の表層から60mm程度の深さの位置にある介在物の集積帯位置から、サンプルを切り出して30μm以上の大きさの非金属介在物を捕集する網の中で、塩化第一鉄水溶液中で約500g電気分解を行って非金属介在物を電解抽出しスライムとして捕集した。捕集したスライムを水簸(水洗しながら非金属介在物のみを分離捕集すること)、分級したのちに、非金属介在物の粒径分布、最大粒径を求めた。 When casting low-carbon aluminum killed steel in a continuous casting apparatus, the present inventor changes the flow velocity v (m / s) of molten steel in a long nozzle and the discharge port of molten steel below the long nozzle to create a ladle. We sampled molten steel metal and sampled slabs from tundish and slabs, and analyzed their components, investigated and analyzed non-metal inclusions in detail. The investigation of non-metal inclusions was carried out by the slime extraction method. An aqueous solution of ferrous chloride in a net that collects non-metallic inclusions with a size of 30 μm or more by cutting out a sample from the position of the accumulation zone of inclusions at a depth of about 60 mm from the surface layer of the slab. About 500 g of the non-metal inclusions were electrolyzed and collected as slime. After elutriation (separation and collection of only non-metal inclusions while washing with water) and classification of the collected slime, the particle size distribution and maximum particle size of the non-metal inclusions were determined.
鋭意研究の結果、取鍋下部に設置したロングノズル下方の溶鋼の吐出口に開口孔を有する底面部を設けることで、取鍋の溶鋼がロングノズル内を落下してくる運動エネルギーを止めることになり、その急激な運動エネルギーの変化がロングノズルの内部の溶鋼を乱流撹拌状態にして、非金属介在物の凝集を促進できるとともに、底面部に設けた開口孔の分、溶鋼の衝突力を低減することができ、ロングノズルの損傷や溶鋼漏れを防止できることを知見した。
また、底面開口孔の開口面積を大きくしすぎると、ロングノズル内での溶鋼の乱流状態が不十分になり、底面開口孔の開口面積を小さくしすぎると、溶鋼が落下する運動エネルギーによる衝突力で、ロングノズルが損傷したり、溶鋼漏れが発生したりして、操業トラブルとなるため、両者を両立するためには底面開口孔の開口面積を適正化することが重要であることを知見した。
As a result of diligent research, we decided to stop the kinetic energy of the molten steel of the ladle falling in the long nozzle by providing a bottom part with an opening hole at the discharge port of the molten steel below the long nozzle installed at the bottom of the ladle. The sudden change in kinetic energy makes the molten steel inside the long nozzle turbulent and agitated, which can promote the aggregation of non-metal inclusions and the collision force of the molten steel due to the opening hole provided in the bottom surface. It was found that it can be reduced and damage to the long nozzle and leakage of molten steel can be prevented.
Further, if the opening area of the bottom opening hole is made too large, the turbulent flow state of the molten steel in the long nozzle becomes insufficient, and if the opening area of the bottom opening hole is made too small, the molten steel collides with the falling kinetic energy. It was found that it is important to optimize the opening area of the bottom opening hole in order to achieve both, because the long nozzle may be damaged by force or molten steel leakage may occur, causing operational troubles. did.
さらに、タンディッシュ内の底部に沿った流れによって、非金属介在物が鋳型に直接流入する現象を抑制する為に、ロングノズルの側面に側面開口孔を設けて、直接、底面開口孔から流出する溶鋼量を制限することで、最終成品である薄鋼板まで持ち込まれる非金属介在物量、大きさを、品質に必要な値を超えないように鋳造することができることを知見した。
こうして、ロングノズルの破損、溶鋼漏れ等のトラブルを引き起こすことなく、非金属介在物の十分な除去が可能で、高品質の鋼鋳片を鋳造することができる、ロングノズルを用いた鋼の連続鋳造方法を見出した。
Further, in order to suppress the phenomenon that the non-metal inclusions directly flow into the mold due to the flow along the bottom in the tundish, a side opening hole is provided on the side surface of the long nozzle, and the non-metal inclusions flow out directly from the bottom opening hole. By limiting the amount of molten steel, it was found that the amount and size of non-metal inclusions brought into the final product, the thin steel sheet, can be cast so as not to exceed the values required for quality.
In this way, non-metal inclusions can be sufficiently removed without causing troubles such as breakage of the long nozzle and leakage of molten steel, and high quality steel slabs can be cast. Continuous steel using the long nozzle. I found a casting method.
本発明は、上述の知見に基づいてなされたものであって、本発明の鋼の連続鋳造方法は、取鍋からタンディッシュへ溶鋼を注入し、このタンディッシュから連続鋳造用鋳型に前記溶鋼を供給し、鋳片を連続的に鋳造する鋼の連続鋳造方法であって、前記取鍋の下端に、有底筒状のロングノズルが配設され、このロングノズルを介して、前記取鍋から前記タンディッシュへの前記溶鋼が注入される構成とされており、前記ロングノズルは、底面部に開口する底面開口孔と、側面に開口する側面開口孔と、を有しており、前記ロングノズルの前記底面部の全面積をS(m2)、前記底面開口孔の面積をSB(m2)、前記側面開口孔の総開口面積をST(m2)、定常時における前記ロングノズル内の流速をv(m/s)とした場合に、以下の(1)〜(3)式を満足するとともに、
(1)式:0.14≦SB/S
(2)式:0<SB/(SB+ST)≦0.55
(3)式:v2×(S−SB)≧0.0035
定常鋳造時における前記底面開口孔からの溶鋼流出量が3t/minを超えないように、前記取鍋から前記タンディッシュに向けて前記溶鋼を注入することを特徴としている。
The present invention has been made based on the above findings, and in the method for continuous casting of steel of the present invention, molten steel is injected from a ladle into a tundish, and the molten steel is cast from the tundish into a mold for continuous casting. It is a continuous casting method of steel that is supplied and continuously casts slabs. A long nozzle with a bottomed cylinder is arranged at the lower end of the ladle, and the long nozzle is used to the ladle. The molten steel is injected into the tundish, and the long nozzle has a bottom opening hole that opens to the bottom surface and a side opening hole that opens to the side surface, and the long nozzle has the long nozzle. The total area of the bottom surface portion is S (m 2 ), the area of the bottom surface opening hole is SB (m 2 ), the total opening area of the side surface opening hole is ST (m 2 ), and the inside of the long nozzle in a steady state. When the flow velocity is v (m / s), the following equations (1) to (3) are satisfied and the flow velocity is satisfied.
Equation (1): 0.14 ≤ SB / S
Equation (2): 0 <SB / (SB + ST) ≤ 0.55
Equation (3): v 2 × (S-SB) ≧ 0.0035
It is characterized in that the molten steel is injected from the ladle toward the tundish so that the amount of molten steel flowing out from the bottom opening hole during steady casting does not exceed 3 t / min.
この構成の鋼の連続鋳造方法によれば、取鍋からタンディッシュに対して溶鋼の注入を開始する際に、大きな溶鋼静圧を持った運動量の大きな溶鋼落下によっても、ロングノズルの破損、溶鋼漏れ等のトラブルの発生を抑制でき、安定して鋳造を行うことができる。また、底面部を有することでロングノズル内の溶鋼が乱流状態となり、非金属介在物を効率的に凝集させることができ、かつ、側面開口孔からの吐出流によって温度差による対流を促し、非金属介在物の浮上分離を促進することができ、清浄度が十分に高い鋼鋳片を製造することが可能となる。 According to the continuous casting method of steel having this configuration, when the injection of molten steel from the ladle into the tundish is started, the long nozzle is damaged and the molten steel is damaged even if the molten steel with a large static pressure and a large momentum falls. The occurrence of troubles such as leakage can be suppressed, and stable casting can be performed. Further, by having the bottom surface portion, the molten steel in the long nozzle becomes a turbulent flow state, non-metal inclusions can be efficiently aggregated, and convection due to a temperature difference is promoted by the discharge flow from the side opening hole. Floating separation of non-metal inclusions can be promoted, and steel slabs having sufficiently high cleanliness can be produced.
また、本発明の鋼の連続鋳造方法においては、前記タンディッシュ内の前記溶鋼の湯面を、フラックス及び不活性ガスの一方又は両方で覆う構成とすることが好ましい。
この場合、前記タンディッシュ内の前記溶鋼の湯面を、フラックス及び不活性ガスで覆うことにより、タンディッシュ内の溶鋼の酸化を抑制でき、非金属介在物の生成を抑制することが可能となる。よって、さらに清浄度が十分に高い鋼鋳片を製造することが可能となる。
Further, in the continuous steel casting method of the present invention, it is preferable that the molten steel surface of the molten steel in the tundish is covered with one or both of the flux and the inert gas.
In this case, by covering the molten steel surface of the molten steel in the tundish with a flux and an inert gas, the oxidation of the molten steel in the tundish can be suppressed, and the formation of non-metal inclusions can be suppressed. .. Therefore, it is possible to manufacture a steel slab having a sufficiently high cleanliness.
上述のように、本発明によれば、ロングノズルの損傷、溶鋼漏れ等のトラブルを生じさせずに、また、溶鋼歩留りも悪化させることなく、非金属介在物の除去を十分に行うことができ、清浄度の高い鋼鋳片を製造可能な鋼の連続鋳造方法を提供することができる。 As described above, according to the present invention, it is possible to sufficiently remove non-metal inclusions without causing troubles such as damage to the long nozzle and leakage of molten steel, and without deteriorating the yield of molten steel. It is possible to provide a continuous casting method of steel capable of producing steel slabs having high cleanliness.
以下に、本発明の実施形態について、添付した図面を参照して説明する。なお、本発明は、以下の実施形態に限定されるものではない。 Hereinafter, embodiments of the present invention will be described with reference to the accompanying drawings. The present invention is not limited to the following embodiments.
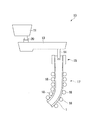
図1に示す連続鋳造装置10においては、取鍋11によって転炉から溶鋼を移送し、ロングノズル20を介してタンディッシュ13に溶鋼2を注入し、このタンディッシュ13において大きな介在物を浮上分離した後、浸漬ノズル14を介して鋳型15に溶鋼を供給し、鋳型15内で凝固シェルを形成し、得られた鋳片1を連続的に鋳造するものである。そして、鋳型15から製出された鋳片1は、複数のサポートロール18からなるサポートロール群17によって引き抜かれ、2次冷却手段(図示なし)によってさらに冷却することで凝固シェルを成長させて完全凝固させる。
In the
そして、本発明の実施形態である鋼の連続鋳造方法においては、取鍋11からタンディッシュ13へ溶鋼を注入する際に用いられるロングノズル20に特徴を有している。図2に、本発明の実施形態である鋼の連続鋳造方法において用いられるロングノズル20を示す。
The continuous steel casting method according to the embodiment of the present invention is characterized by the
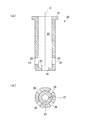
本実施形態におけるロングノズル20は、図2に示すように、有底筒状をなし、具体的には、概略円筒形状をなしており、その上端に、取鍋へ取り付けるためのフランジ部21が形成されている。
また、ロングノズル20は、軸線O沿って延在する溶鋼経路22を有しており、この溶鋼経路22の下端に底面部23が形成されている。そして、ロングノズル20には、底面部23に開口する底面開口孔24と、溶鋼経路22の側面に開口する側面開口孔25と、が設けられている。なお、側面開口孔25は、周方向に間隔をあけて複数設けられており、本実施形態では、図2(b)に示すように、4つの側面開口孔25が周方向に等間隔に配設されている。
As shown in FIG. 2, the
Further, the
ここで、ロングノズル20においては、底面部23の内面積をS(m2)、底面開口孔24の面積をSB(m2)、側面開口孔25の総開口面積をST(m2)、定常時における前記ロングノズル内の流速をv(m/s)とした場合に、以下の(1)式〜(3)式を満足するように構成されている。なお、(3)式の左辺を攪拌パラメータ指数と定義する。
(1)式:0.14≦SB/S
(2)式:0<SB/(SB+ST)≦0.55
(3)式:v2×(S−SB)≧0.0035
Here, in the
Equation (1): 0.14 ≤ SB / S
Equation (2): 0 <SB / (SB + ST) ≤ 0.55
Equation (3): v 2 × (S-SB) ≧ 0.0035
さらに、本実施形態では、定常鋳造時における底面開口孔24からの溶鋼流出量が3t/minを超えないように、取鍋11からタンディッシュ13への溶鋼の注入量を制御するように構成されている。
なお、底面開口孔24からの溶鋼流出量は、全体の溶鋼流量に全ての開口孔の面積に対する底面開口孔24の面積の割合(SB/(SB+ST))を乗じて算出されるものである。
Further, in the present embodiment, the amount of molten steel injected from the
The amount of molten steel flowing out from the
以下に、本実施形態において、上述の(1)〜(3)式、及び、定常鋳造時における底面開口孔24からの溶鋼流出量、を規定した理由について説明する。
Hereinafter, the reasons for defining the above-mentioned equations (1) to (3) and the amount of molten steel flowing out from the
本実施形態においては、ロングノズル20の溶鋼流路22の下端に、底面部23を設けることで、ロングノズル20の内部(溶鋼経路22内)を乱流攪乱状態にして、非金属介在物を凝集させ、非金属介在物の浮上分離の促進を図っている。
また、底面部23に底面開口孔24を設けることにより、鋳造開始時の取鍋開孔時の溶鋼落下による衝突力を低減することにより、ロングノズル20の損傷や、ロングノズル20の位置ずれによる溶鋼漏れ等の大きな操業トラブルの抑制を図っている。
そこで、実験を繰り返して、上述のトラブルを回避するために必要な底面開口孔の条件について検討した。
In the present embodiment, by providing the
Further, by providing the
Therefore, the experiment was repeated to examine the conditions of the bottom opening hole necessary for avoiding the above-mentioned trouble.
図3に、取鍋11の下部に設置してタンディッシュ13へ注入するロングノズル20の底面部への衝撃力を説明する概略図を示す。
取鍋11からタンディッシュ13に溶鋼注入を開始するときに、取鍋11の下部にあるスラインディングノズルを開放する。溶鋼は、取鍋11の溶鋼高さH(m)による溶鋼静圧Pから求められる初速度v0でロングノズル20内(溶鋼経路22)を自由落下する。ロングノズル20内(溶鋼経路22)を自由落下した溶鋼は、重力加速度gを受けて加速し、ロングノズル20の底面部へ衝突する。
FIG. 3 shows a schematic view for explaining the impact force on the bottom surface of the
When starting molten steel injection from the
溶鋼流出初速度v0、溶鋼流出初期流量Q0(kg/s)とすると、
Q0(kg/s)=ロングノズル断面積×v0×溶鋼密度
ロングノズル20の下端での出口溶鋼流出速度vとすると、
v=v0+g×t,x=v0×t+0.5×g×t2
ロングノズルの長さLとし、x=Lを代入することで、ロングノズル20の上部から下端までの落下時間t(s)が求まり、v(m/s)が求まる。さらに、ロングノズル20の下端での溶鋼流出流量Q(kg/s)が求まる。
Assuming that the initial velocity of molten steel outflow is v 0 and the initial flow rate of molten steel outflow is Q 0 (kg / s),
Q 0 (kg / s) = long nozzle cross-sectional area x v 0 x molten steel density If the outlet molten steel outflow velocity v at the lower end of the
v = v 0 + g × t, x = v 0 × t + 0.5 × g × t 2
By setting the length L of the long nozzle and substituting x = L, the fall time t (s) from the upper end to the lower end of the
ロングノズル20の下端における溶鋼流の衝撃力Fは、以下の式で算出される。
衝撃力F(N)=溶鋼流出流量Q(kg/s)×溶鋼流出速度v(m/s)
取鍋11の溶鋼高さH(m)は、製鋼工場によって異なるため、初速度v0が変わり、ロングノズル20の底面部への衝突力Fも変わる。
The impact force F of the molten steel flow at the lower end of the
Impact force F (N) = molten steel outflow flow rate Q (kg / s) x molten steel outflow velocity v (m / s)
Since the molten steel height H (m) of the
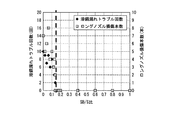
本実施形態においては、取鍋11内の溶鋼量が約100tから400tの異なる製鋼工場で、底面部の全面積S(m2)と前記底面開口孔の面積SB(m2)を変えたロングノズルを用いて実機実験を行った。その時の、ロングノズル20の損傷状況、溶鋼漏れ状況を確認し、図4を実験的に得た。横軸に、各製鋼工場で用いて実験を行ったロングノズル20のSB/Sを取り、その時の溶鋼漏れトラブル回数と、ロングノズル20の損傷本数を縦軸に取って示した。
この結果から、溶鋼漏れトラブルを発生させることが無く、かつ、ロングノズル20の損傷を発生させることのない条件として、SB/S≧0.14を得た。
In the present embodiment, the total area S (m 2 ) of the bottom surface portion and the area SB (m 2 ) of the bottom surface opening hole are changed in the steelmaking factories in which the amount of molten steel in the
From this result, SB / S ≧ 0.14 was obtained under the condition that the molten steel leakage trouble did not occur and the
次に、溶鋼漏れ、ロングノズル20の損傷トラブルを生じさせないSB/S≧0.14の範囲で、非金属介在物の凝集効果を十分に得るために必要な要件について、検討を行った。
ここで、本実施形態においては、「撹拌エネルギー指数v2×(S−SB)」を考案した。その定義は、開口のある底面部23において遮蔽され、下向きに流れていた溶鋼流が反対方向(上向き)の流れに変えられ、消失した運動エネルギーを指数とした。下向き運動エネルギーの消失した分が、ロングノズル20の内部の溶鋼に撹拌エネルギーとして働くと考察した。すなわち、底面部23から流出しようとした溶鋼流にせん断力が働き、そのせん断力の大小によって、非金属介在物の凝集エネルギーの大小を指数化しようと考察したものである。
Next, the requirements necessary to sufficiently obtain the agglomeration effect of the non-metal inclusions within the range of SB / S ≧ 0.14 that does not cause molten steel leakage and damage trouble of the
Here, in the present embodiment, "stirring energy index v 2 × (S-SB)" is devised. The definition is that the molten steel flow that was shielded at the
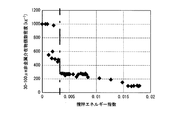
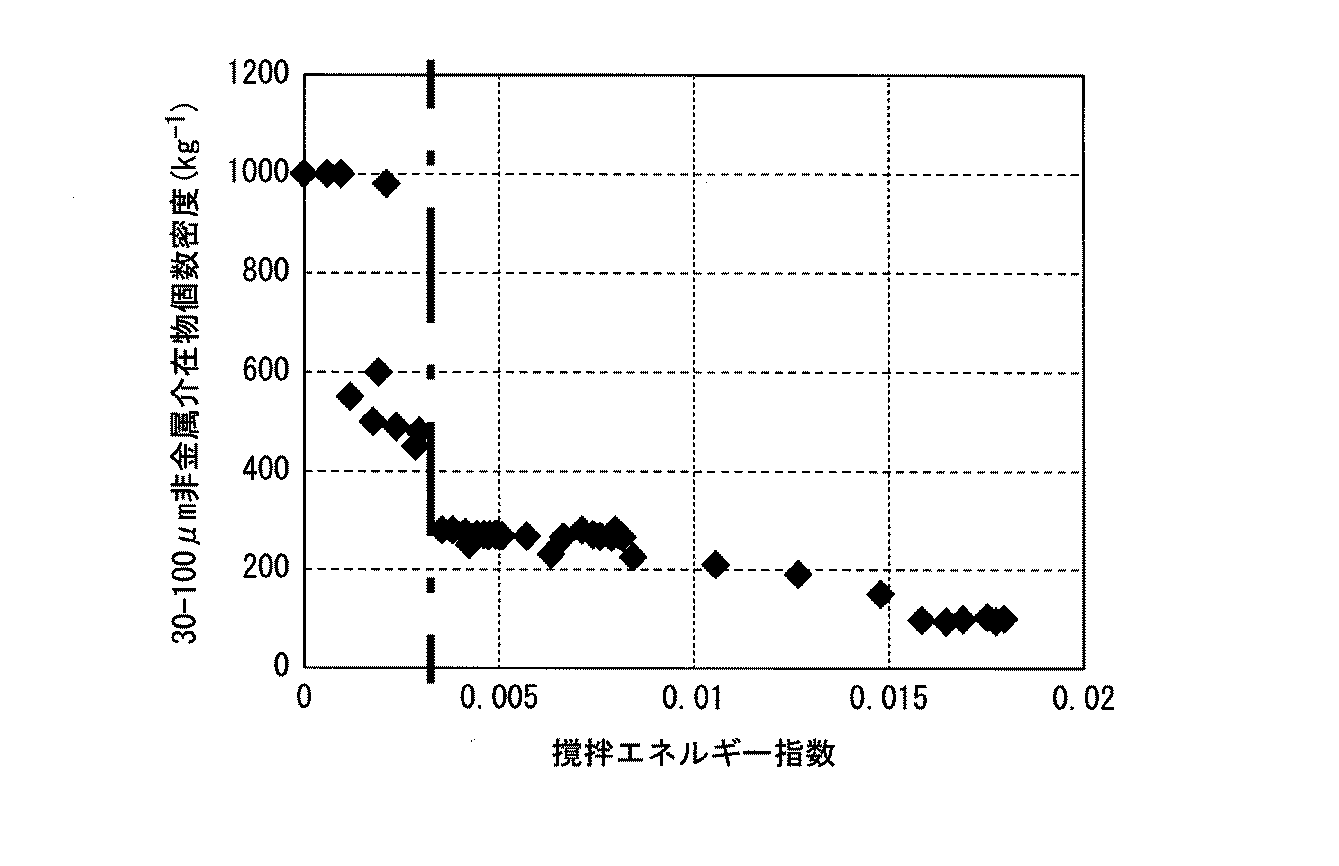
この指数で整理した結果を図5に示す。ロングノズル20内の撹拌エネルギー指数と凝集効果が働く100μm以下の非金属介在物の個数密度の関係である。
図5に示すように、撹拌エネルギー指数v2×(S−SB)≧0.0035とすることで、非金属介在物の凝集効果を十分に得られることを確認した。
The results organized by this index are shown in FIG. It is the relationship between the stirring energy index in the
As shown in FIG. 5, it was confirmed that the aggregating effect of the non-metal inclusions could be sufficiently obtained by setting the stirring energy index v 2 × (S-SB) ≧ 0.0035.
本実施形態においては、上述のように、ロングノズル20の損傷、溶鋼漏れ等のトラブルを発生させず、非金属介在物の凝集効果を得るために、底面部23に底面開口孔24を設けることを考案した。底面開口孔24があることで、ロングノズル20の損傷は免れるが、底面開口孔20の開口面積SBの増大に従い、従来のストレート型のノズルのように、タンディッシュ13の底部を這って、直接鋳型に流れ込む溶鋼流れによって、比較的大きな非金属介在物が流入する課題が残った。
これについては、本実施形態においては、ロングノズル20の底面部23に設けた底面開口孔24とロングノズル20の側面に設けた側面開口孔25で、溶鋼流を適切に分配することで解決した。この時、底面開口孔24の開口面積SBと側面開口孔25の総開口面積STとの比は、次のような実験で求めた。
In the present embodiment, as described above, the
This has been solved in the present embodiment by appropriately distributing the molten steel flow through the
側面開口孔25からの流出する溶鋼流が大きくなるとタンディッシュ13内で上向きの流れが生じ、比較的大きな非金属介在物が浮上除去されやすくなると考えられる。
そこで、底面開口孔24と側面開口孔25のそれそれから流出する溶鋼流の分配比を示す指標として、SB/(SB+ST)を定義し、SB/(SB+ST)を変化させたロングノズル20を用いて連続鋳造を行い、鋳片1中の非金属介在物の最大径を調査した。図6に、SB/(SB+ST)に対する非金属介在物最大径の関係を示す。
SB/(SB+ST)を0.55以下に制御することで、鋳片1に巻き込まれる非金属介在物を100μm程度まで小さくすることができることがわかった。
It is considered that when the molten steel flow flowing out from the
Therefore, SB / (SB + ST) is defined as an index showing the distribution ratio of the molten steel flow flowing out from the
It was found that by controlling SB / (SB + ST) to 0.55 or less, the non-metal inclusions involved in the
一方、底面開口孔24からの溶鋼流出流量が大きくなると、直接、鋳型15に流れ込む非金属介在物が多くなる。そこで、底面開口孔24からの溶鋼流出流量と、特に製品で問題となる鋳片1中の100μm超の非金属介在物の個数密度の関係を調査した。図7に、底面開口孔24からの溶鋼流出流量と100μm超の非金属介在物の個数密度の関係を示す。ここで、底面開口孔24からの溶鋼流出流量は、全溶鋼流出流量に全ての開口孔の面積に対する底面開口孔24の面積の割合(SB/(SB+ST))を乗じて求める。
底面開口孔24からの溶鋼流出流量が3t/minを超えないように制御することで、100μm超の非金属介在物の個数密度を小さくすることが可能なことを知見した。
On the other hand, as the flow rate of molten steel flowing out from the
It was found that the number density of non-metal inclusions exceeding 100 μm can be reduced by controlling the flow rate of molten steel outflow from the
以上のような実験結果から、本実施形態では、上述の(1)〜(3)式、及び、定常鋳造時における底面開口孔24からの溶鋼流出量、を規定した。
From the above experimental results, in the present embodiment, the above-mentioned equations (1) to (3) and the amount of molten steel flowing out from the
また、本実施形態においては、ロングノズル20からタンディッシュ13内に溶鋼が流れ出た後の再酸化を防ぐために、タンディッシュ13の溶鋼表面をタンディッシュ13内の大気雰囲気から遮断して酸素濃度を低減することが好ましい。
このため、タンディッシュ13内の溶鋼の湯面を、フラックス及び不活性ガスの一方又は両方で覆うことが好ましい。高級鋼においては、不活性ガスシールとフラックスシールの両方を適用することが望ましい。低級鋼においては、不活性ガスシールもしくは、フラックスシールのどちらかによって、確実にシールできることが望ましい。
Further, in the present embodiment, in order to prevent reoxidation after the molten steel flows out from the
Therefore, it is preferable to cover the molten steel surface in the
フラックスにはCaO−Al2O3−SiO2系をベースとした、低融点組成で、溶鋼温度で十分溶融し、溶鋼表面を覆うことが可能なものを用いることが望ましい。
こうして、非金属介在物を凝集合体させ浮上を強化させるような高清浄鋼の溶製においては、溶鋼表面の酸素濃度を制御して再酸化を抑制しつつ、非金属介在物の除去を図ることで、大きなアルミナクラスターの低減効果を得ることができる。なお、酸素濃度は、酸素分圧でPO2=10−14(atm)以下とすることが好ましい。
It is desirable to use a flux having a low melting point composition based on the CaO-Al 2 O 3- SiO 2 system, which can sufficiently melt at the molten steel temperature and cover the surface of the molten steel.
In this way, in the melting of high-clean steel in which non-metal inclusions are agglutinated and coalesced to strengthen levitation, the non-metal inclusions should be removed while controlling the oxygen concentration on the surface of the molten steel to suppress reoxidation. Therefore, the effect of reducing large alumina clusters can be obtained. The oxygen concentration is preferably at an oxygen partial pressure P O2 = 10 -14 (atm) or less.
以上のような構成とされた本実施形態である鋼の連続鋳造方法によれば、底面部23に開口する底面開口孔24と、側面に開口する側面開口孔25と、を有するロングノズル20を用いて、上述の(1)〜(3)式を満足するとともに、定常鋳造時における底面開口孔24からの溶鋼流出量が3t/minを超えないように、取鍋11からタンディッシュ13に向けて溶鋼を注入する構成とされているので、取鍋11からタンディッシュ13に対して溶鋼の注入を開始する際に、大きな溶鋼静圧を持った運動量の大きな溶鋼落下によっても、ロングノズル20の破損、位置ずれに溶鋼漏れの発生を抑制でき、安定して鋳造を行うことができる。
また、底面部23を有することでロングノズル20内の溶鋼が乱流状態となり、非金属介在物を効率的に凝集させることができ、かつ、側面開口孔25からの吐出流によって温度差による対流を促し、非金属介在物の浮上分離を促進することができ、清浄度が十分に高い鋳片1を製造することが可能となる。
According to the steel continuous casting method of the present embodiment having the above-described configuration, the
Further, by having the
また、本実施形態において、タンディッシュ13内の溶鋼の湯面を、フラックス及び不活性ガスの一方又は両方で覆う構成とした場合には、タンディッシュ13内の溶鋼の酸化を抑制でき、非金属介在物の生成を抑制することが可能となる。よって、さらに清浄度の高い鋳片を製造することが可能となる。
Further, in the present embodiment, when the molten steel surface in the
以上、本発明の実施形態である鋼の連続鋳造方法について、具体的に説明したが、本発明はこれに限定されることはなく、その発明の技術的思想を逸脱しない範囲で適宜変更可能である。 Although the continuous steel casting method according to the embodiment of the present invention has been specifically described above, the present invention is not limited to this and can be appropriately changed without departing from the technical idea of the invention. is there.
例えば、本実施形態では、側面開口孔を4つ設けたものとして説明したが、これに限定されることはなく、側面開口孔の個数は4,6,8,・・・のように偶数個設けることが好ましい。
タンディッシュから2つのストランドに溶鋼を供給する場合、側面開口孔を、タンディッシュの長手方向別に半分ずつ(2,3,4,・・・)、かつ、両ストランド左右で対照に配置することにより、両ストランドに対照な流れを得て、なおかつタンディッシュの壁に直接向かう流れや、鋳型内に直接向かう直送流を避けることが可能となる。
For example, in the present embodiment, it has been described that four side opening holes are provided, but the present invention is not limited to this, and the number of side opening holes is an even number such as 4, 6, 8, ... It is preferable to provide.
When supplying molten steel from the tundish to two strands, by arranging the side opening holes in half (2, 3, 4, ...) in each longitudinal direction of the tundish and in contrast on the left and right sides of both strands. It is possible to obtain a contrasting flow in both strands and avoid a flow directly toward the wall of the tundish or a direct flow directly into the mold.
また、本実施形態においては、側面開口孔の吐出角度について言及していないが、タンディッシュ底に這う流れが生じることをさらに抑制するためには、側面開口孔の吐出角度を水平面(上向き0°)とすることが好ましい。 Further, in the present embodiment, the discharge angle of the side opening hole is not mentioned, but in order to further suppress the flow that crawls on the bottom of the tundish, the discharge angle of the side opening hole is set to a horizontal plane (upward 0 °). ) Is preferable.
本発明の効果について検証するために実施した検証試験について説明する。
自動車用に用いられる低炭アルミキルド鋼を転炉出鋼、RH二次精錬工程で、脱ガス処理を行い、その後、表1に示す条件のロングノズルを用いて、表1に示す溶鋼流量で取鍋からタンディッシュに溶鋼を注入し、連続鋳造を行った。なお、ロングノズルは、いずれも側面開口孔が4個水平面に開口しているものを用いた。
The verification test carried out for verifying the effect of the present invention will be described.
Low-carbon aluminum killed steel used for automobiles is degassed in the converter steelmaking and RH secondary refining process, and then taken at the molten steel flow rate shown in Table 1 using a long nozzle under the conditions shown in Table 1. Molten steel was injected into the tundish from the pan and continuous casting was performed. As the long nozzle, four side opening holes were used in the horizontal plane.
鋳造途中でのノズル破損、溶鋼漏れのトラブルが発生したものは、トラブル発生時点で鋳造を中止し、非金属介在物の調査は実施しなかった。トラブルなく鋳造できた鋳片については、非金属介在物の調査を前述したスライム抽出法で行い、非金属介在物の粒径分布、最大粒径を求めた。鋳片サンプルの採取を行い、スライム法を用いて、非金属介在物個数密度を調査した。試験結果を表2に示す。 For nozzles that had problems such as nozzle breakage or molten steel leakage during casting, casting was stopped at the time of the trouble, and non-metal inclusions were not investigated. For the slabs that could be cast without trouble, the non-metal inclusions were investigated by the slime extraction method described above, and the particle size distribution and maximum particle size of the non-metal inclusions were determined. A slab sample was taken and the density of non-metal inclusions was investigated using the slime method. The test results are shown in Table 2.
No.1〜14は発明例であり、ノズル破損や溶鋼漏れのトラブルなく鋳造でき、非金属介在物個数密度も少なく、直径200μmを超えるような粗大な介在物も見られなかった。
No.15〜17はSB/Sが小さすぎる比較例であり、ロングノズル底面開口孔が小さすぎるためにノズル破損や溶鋼漏れのトラブルが発生した。
No.18〜20は撹拌エネルギーが小さすぎる比較例であり、500個/kgを超える直径30〜100μmの非金属介在物が存在した。
No.21〜23はSB/(SB+ST)が大きすぎる比較例であり、直径200μmを超える非金属介在物が存在した。
No.24〜26は、底面開口孔からの溶鋼流出流量が3.0t/minを超える比較例であり、直径100μm超の大きな非金属介在物が10個/kg以上存在した。
No. Examples 1 to 14 are examples of the invention, in which casting can be performed without troubles of nozzle breakage and molten steel leakage, the number density of non-metal inclusions is low, and no coarse inclusions having a diameter of more than 200 μm are observed.
No. Reference examples 15 to 17 are comparative examples in which the SB / S is too small, and the nozzle breakage and molten steel leakage problems occur because the long nozzle bottom opening hole is too small.
No. 18 to 20 are comparative examples in which the stirring energy is too small, and there were non-metal inclusions having a diameter of 30 to 100 μm exceeding 500 pieces / kg.
No. 21 to 23 are comparative examples in which SB / (SB + ST) is too large, and non-metallic inclusions having a diameter of more than 200 μm were present.
No. Reference examples 24 to 26 are comparative examples in which the flow rate of molten steel flowing out from the bottom opening hole exceeds 3.0 t / min, and there are 10 or more large non-metal inclusions having a diameter of more than 100 μm.
1 鋳片
10 連続鋳造装置
11 取鍋
13 タンディッシュ
15 鋳型
20 ロングノズル
22 溶湯経路
23 底面部
24 底面開口孔
25 側面開口孔
1
Claims (2)
前記取鍋の下端に、有底筒状のロングノズルが配設され、このロングノズルを介して、前記取鍋から前記タンディッシュへの前記溶鋼が注入される構成とされており、
前記ロングノズルは、底面部に開口する底面開口孔と、側面に開口する側面開口孔と、を有しており、
前記ロングノズルの前記底面部の全面積をS(m2)、前記底面開口孔の面積をSB(m2)、前記側面開口孔の総開口面積をST(m2)、定常時における前記ロングノズル内の流速をv(m/s)とした場合に、以下の(1)〜(3)式を満足するとともに、
(1)式:0.14≦SB/S
(2)式:0<SB/(SB+ST)≦0.55
(3)式:v2×(S−SB)≧0.0035
定常鋳造時における前記底面開口孔からの溶鋼流出量が3t/minを超えないように、前記取鍋から前記タンディッシュに向けて前記溶鋼を注入することを特徴とする鋼の連続鋳造方法。 It is a continuous casting method of steel in which molten steel is injected from a ladle into a tundish, the molten steel is supplied from the tundish to a mold for continuous casting, and slabs are continuously cast.
A bottomed tubular long nozzle is arranged at the lower end of the ladle, and the molten steel is injected from the ladle into the tundish through the long nozzle.
The long nozzle has a bottom opening hole that opens on the bottom surface and a side opening hole that opens on the side surface.
The total area of the bottom surface of the long nozzle is S (m 2 ), the area of the bottom surface opening is SB (m 2 ), the total opening area of the side surface opening is ST (m 2 ), and the long in a steady state. When the flow velocity in the nozzle is v (m / s), the following equations (1) to (3) are satisfied, and the following equations (1) to (3) are satisfied.
Equation (1): 0.14 ≤ SB / S
Equation (2): 0 <SB / (SB + ST) ≤ 0.55
Equation (3): v 2 × (S-SB) ≧ 0.0035
A method for continuous casting of steel, which comprises injecting the molten steel from the ladle toward the tundish so that the amount of molten steel flowing out from the bottom opening hole during steady casting does not exceed 3 t / min.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2019076463A JP7200811B2 (en) | 2019-04-12 | 2019-04-12 | Steel continuous casting method |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2019076463A JP7200811B2 (en) | 2019-04-12 | 2019-04-12 | Steel continuous casting method |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2020171955A true JP2020171955A (en) | 2020-10-22 |
| JP7200811B2 JP7200811B2 (en) | 2023-01-10 |
Family
ID=72829654
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2019076463A Active JP7200811B2 (en) | 2019-04-12 | 2019-04-12 | Steel continuous casting method |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP7200811B2 (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2022189431A (en) * | 2021-06-11 | 2022-12-22 | 日本製鉄株式会社 | Continuous casting method of steel |
| JP2024085133A (en) * | 2022-12-14 | 2024-06-26 | 日本製鉄株式会社 | Ladle injection nozzle and continuous casting method |
| JP2024085132A (en) * | 2022-12-14 | 2024-06-26 | 日本製鉄株式会社 | Continuous casting method and pouring nozzle for ladle |
| JPWO2024232222A1 (en) * | 2023-05-10 | 2024-11-14 |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS6325255U (en) * | 1986-08-02 | 1988-02-19 | ||
| JPH0691355A (en) * | 1992-09-14 | 1994-04-05 | Toshiba Ceramics Co Ltd | Casting nozzle |
| JP2001113347A (en) * | 1999-10-19 | 2001-04-24 | Sumitomo Metal Ind Ltd | Hot water supply device and continuous casting method for steel |
| JP2013529551A (en) * | 2010-07-02 | 2013-07-22 | ベスビウス クルーシブル カンパニー | Immersion nozzle |
| JP2013208643A (en) * | 2012-03-30 | 2013-10-10 | Nisshin Steel Co Ltd | Continuous casting method |
| JP2013208641A (en) * | 2012-03-30 | 2013-10-10 | Nisshin Steel Co Ltd | Continuous casting method |
| JP2015066559A (en) * | 2013-09-27 | 2015-04-13 | 日新製鋼株式会社 | Continuous casting method |
-
2019
- 2019-04-12 JP JP2019076463A patent/JP7200811B2/en active Active
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS6325255U (en) * | 1986-08-02 | 1988-02-19 | ||
| JPH0691355A (en) * | 1992-09-14 | 1994-04-05 | Toshiba Ceramics Co Ltd | Casting nozzle |
| JP2001113347A (en) * | 1999-10-19 | 2001-04-24 | Sumitomo Metal Ind Ltd | Hot water supply device and continuous casting method for steel |
| JP2013529551A (en) * | 2010-07-02 | 2013-07-22 | ベスビウス クルーシブル カンパニー | Immersion nozzle |
| JP2013208643A (en) * | 2012-03-30 | 2013-10-10 | Nisshin Steel Co Ltd | Continuous casting method |
| JP2013208641A (en) * | 2012-03-30 | 2013-10-10 | Nisshin Steel Co Ltd | Continuous casting method |
| JP2015066559A (en) * | 2013-09-27 | 2015-04-13 | 日新製鋼株式会社 | Continuous casting method |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2022189431A (en) * | 2021-06-11 | 2022-12-22 | 日本製鉄株式会社 | Continuous casting method of steel |
| JP7663809B2 (en) | 2021-06-11 | 2025-04-17 | 日本製鉄株式会社 | Continuous casting method for steel |
| JP2024085133A (en) * | 2022-12-14 | 2024-06-26 | 日本製鉄株式会社 | Ladle injection nozzle and continuous casting method |
| JP2024085132A (en) * | 2022-12-14 | 2024-06-26 | 日本製鉄株式会社 | Continuous casting method and pouring nozzle for ladle |
| JPWO2024232222A1 (en) * | 2023-05-10 | 2024-11-14 | ||
| WO2024232222A1 (en) * | 2023-05-10 | 2024-11-14 | Jfeスチール株式会社 | Nozzle for continuous casting, continuous casting apparatus, tundish, and continuous casting method |
| JP7772234B2 (en) | 2023-05-10 | 2025-11-18 | Jfeスチール株式会社 | Continuous casting device and continuous casting method |
| TWI917930B (en) | 2023-05-10 | 2026-03-11 | 日商杰富意鋼鐵股份有限公司 | Continuous casting apparatus and continuous casting method |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7200811B2 (en) | 2023-01-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5807719B2 (en) | High cleanliness steel slab manufacturing method and tundish | |
| JP7200811B2 (en) | Steel continuous casting method | |
| JP2011143449A (en) | Method for removing inclusion in tundish for continuous casting | |
| KR20050021961A (en) | Method for producing ultra low carbon steel slab | |
| Miyazawa | Continuous casting of steels in Japan | |
| JP4411945B2 (en) | Slab continuous casting method for ultra-low carbon steel | |
| JP5751078B2 (en) | Manufacturing method of high cleanliness steel slab by continuous casting | |
| JP2023066986A (en) | nozzle system | |
| JP5556465B2 (en) | Manufacturing method of high cleanliness steel slab by continuous casting | |
| JP7663809B2 (en) | Continuous casting method for steel | |
| JP4998705B2 (en) | Steel continuous casting method | |
| JP4474948B2 (en) | Steel continuous casting method | |
| TWI805110B (en) | Steel continuous casting method | |
| JP5831138B2 (en) | Manufacturing method of high cleanliness steel slab by continuous casting | |
| JP4220848B2 (en) | Tundish for continuous casting of steel with heating function | |
| JP3558815B2 (en) | High cleanliness steel continuous casting method with tundish equipped with fixed weir with closed bottom | |
| JP5044981B2 (en) | Steel continuous casting method | |
| JP2009090323A (en) | Continuous casting apparatus and continuous casting method | |
| JPH10249498A (en) | High cleanliness steel continuous casting method with tundish equipped with fixed weir with closed bottom | |
| JPH11320054A (en) | Continuous casting machine and continuous casting method | |
| JP6904132B2 (en) | Tandish for continuous casting | |
| JPH09164455A (en) | Method for removing non-metallic inclusions in molten metal | |
| JP2008087065A (en) | Tundish for continuous casting | |
| JPS61140356A (en) | Electromagnetic stirring method in continuous casting machine | |
| JP2024043884A (en) | nozzle system |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A621 | Written request for application examination |
Free format text: JAPANESE INTERMEDIATE CODE: A621 Effective date: 20211206 |
|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20221107 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20221122 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20221205 |
|
| R151 | Written notification of patent or utility model registration |
Ref document number: 7200811 Country of ref document: JP Free format text: JAPANESE INTERMEDIATE CODE: R151 |