JP3552939B2 - 溶着部とこれを備えた超音波溶着装置 - Google Patents
溶着部とこれを備えた超音波溶着装置 Download PDFInfo
- Publication number
- JP3552939B2 JP3552939B2 JP01960399A JP1960399A JP3552939B2 JP 3552939 B2 JP3552939 B2 JP 3552939B2 JP 01960399 A JP01960399 A JP 01960399A JP 1960399 A JP1960399 A JP 1960399A JP 3552939 B2 JP3552939 B2 JP 3552939B2
- Authority
- JP
- Japan
- Prior art keywords
- welding
- welded
- ultrasonic
- section
- horn
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000003466 welding Methods 0.000 title claims abstract description 76
- 230000002093 peripheral effect Effects 0.000 claims description 4
- 230000010355 oscillation Effects 0.000 claims description 3
- 238000003754 machining Methods 0.000 abstract description 4
- 238000012545 processing Methods 0.000 description 8
- 239000000463 material Substances 0.000 description 5
- 229920005989 resin Polymers 0.000 description 5
- 239000011347 resin Substances 0.000 description 5
- WABPQHHGFIMREM-UHFFFAOYSA-N lead(0) Chemical compound [Pb] WABPQHHGFIMREM-UHFFFAOYSA-N 0.000 description 3
- 229920008790 Amorphous Polyethylene terephthalate Polymers 0.000 description 2
- 239000004743 Polypropylene Substances 0.000 description 2
- 238000013459 approach Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 239000004800 polyvinyl chloride Substances 0.000 description 2
- 229920000915 polyvinyl chloride Polymers 0.000 description 2
- 238000007789 sealing Methods 0.000 description 2
- 229920005992 thermoplastic resin Polymers 0.000 description 2
- 239000004793 Polystyrene Substances 0.000 description 1
- 238000007796 conventional method Methods 0.000 description 1
- 230000020169 heat generation Effects 0.000 description 1
- 238000003780 insertion Methods 0.000 description 1
- 230000037431 insertion Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 239000005022 packaging material Substances 0.000 description 1
- 229920000139 polyethylene terephthalate Polymers 0.000 description 1
- 239000005020 polyethylene terephthalate Substances 0.000 description 1
- -1 polypropylene Polymers 0.000 description 1
- 229920001155 polypropylene Polymers 0.000 description 1
- 229920002223 polystyrene Polymers 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/83—General aspects of machine operations or constructions and parts thereof characterised by the movement of the joining or pressing tools
- B29C66/836—Moving relative to and tangentially to the parts to be joined, e.g. transversely to the displacement of the parts to be joined, e.g. using a X-Y table
- B29C66/8362—Rollers, cylinders or drums moving relative to and tangentially to the parts to be joined
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
- B29C65/08—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using ultrasonic vibrations
- B29C65/083—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using ultrasonic vibrations using a rotary sonotrode or a rotary anvil
- B29C65/086—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using ultrasonic vibrations using a rotary sonotrode or a rotary anvil using a rotary anvil
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/74—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by welding and severing, or by joining and severing, the severing being performed in the area to be joined, next to the area to be joined, in the joint area or next to the joint area
- B29C65/745—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by welding and severing, or by joining and severing, the severing being performed in the area to be joined, next to the area to be joined, in the joint area or next to the joint area using a single unit having both a severing tool and a welding tool
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/01—General aspects dealing with the joint area or with the area to be joined
- B29C66/05—Particular design of joint configurations
- B29C66/10—Particular design of joint configurations particular design of the joint cross-sections
- B29C66/11—Joint cross-sections comprising a single joint-segment, i.e. one of the parts to be joined comprising a single joint-segment in the joint cross-section
- B29C66/112—Single lapped joints
- B29C66/1122—Single lap to lap joints, i.e. overlap joints
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/01—General aspects dealing with the joint area or with the area to be joined
- B29C66/05—Particular design of joint configurations
- B29C66/20—Particular design of joint configurations particular design of the joint lines, e.g. of the weld lines
- B29C66/21—Particular design of joint configurations particular design of the joint lines, e.g. of the weld lines said joint lines being formed by a single dot or dash or by several dots or dashes, i.e. spot joining or spot welding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/40—General aspects of joining substantially flat articles, e.g. plates, sheets or web-like materials; Making flat seams in tubular or hollow articles; Joining single elements to substantially flat surfaces
- B29C66/41—Joining substantially flat articles ; Making flat seams in tubular or hollow articles
- B29C66/43—Joining a relatively small portion of the surface of said articles
- B29C66/431—Joining the articles to themselves
- B29C66/4312—Joining the articles to themselves for making flat seams in tubular or hollow articles, e.g. transversal seams
- B29C66/43121—Closing the ends of tubular or hollow single articles, e.g. closing the ends of bags
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/814—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8141—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined
- B29C66/81411—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat
- B29C66/81421—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat being convex or concave
- B29C66/81422—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat being convex or concave being convex
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/814—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8141—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined
- B29C66/81433—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined being toothed, i.e. comprising several teeth or pins, or being patterned
- B29C66/81435—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined being toothed, i.e. comprising several teeth or pins, or being patterned comprising several parallel ridges, e.g. for crimping
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/816—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the mounting of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8167—Quick change joining tools or surfaces
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/82—Pressure application arrangements, e.g. transmission or actuating mechanisms for joining tools or clamps
- B29C66/822—Transmission mechanisms
- B29C66/8221—Scissor or lever mechanisms, i.e. involving a pivot point
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/82—Pressure application arrangements, e.g. transmission or actuating mechanisms for joining tools or clamps
- B29C66/822—Transmission mechanisms
- B29C66/8226—Cam mechanisms; Wedges; Eccentric mechanisms
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/82—Pressure application arrangements, e.g. transmission or actuating mechanisms for joining tools or clamps
- B29C66/822—Transmission mechanisms
- B29C66/8227—Transmission mechanisms using springs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/84—Specific machine types or machines suitable for specific applications
- B29C66/861—Hand-held tools
- B29C66/8614—Tongs, pincers or scissors
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/71—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the composition of the plastics material of the parts to be joined
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/73—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/737—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the state of the material of the parts to be joined
- B29C66/7377—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the state of the material of the parts to be joined amorphous, semi-crystalline or crystalline
- B29C66/73771—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the state of the material of the parts to be joined amorphous, semi-crystalline or crystalline the to-be-joined area of at least one of the parts to be joined being amorphous
- B29C66/73772—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the state of the material of the parts to be joined amorphous, semi-crystalline or crystalline the to-be-joined area of at least one of the parts to be joined being amorphous the to-be-joined areas of both parts to be joined being amorphous
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/73—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/739—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/7392—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic
- B29C66/73921—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic characterised by the materials of both parts being thermoplastics
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Package Closures (AREA)
Description
【発明の属する技術分野】
本発明は溶着部とこれを備えた超音波溶着装置に関し、詳しくは、樹脂包装材などに対するスポットあるいはシームのいずれの溶着も可能な溶着部とこれを備えた超音波溶着装置に関する。
【0002】
【従来の技術】
内容物を収納した樹脂製容器などの開口縁部を部分的に固着したり、袋体の入口全体を封緘したりするのに、超音波を利用した溶着装置がその手軽さから広く利用されている。例えば、PET等の熱可塑性樹脂の開口縁部をスポット溶着して固着する装置として、特開平10−44243号に開示されているものがある。又、袋体の入口全体をシーム溶着して封緘する装置として、登録実用新案第3024720号に記載されているものがある。
【0003】
【発明が解決しようとする課題】
しかしながら、上記いずれの装置も夫々スポット溶着またはシーム溶着のいずれかのみが可能になるのであって、被溶着物の溶着要求により別々の装置を用いる必要があり、タイプの異なる2種の装置を用意する必要があって不都合かつ不経済であった。しかも、後者のシーム溶着する装置は床に設置される設置型のものであり、容易に持ち運びできる可搬性に優れたものではない。従って、手軽に被溶着物のある場所まで移動でき、被溶着物の溶着用途に応じてスポットあるいはシーム溶着のいずれも適用可能な超音波溶着装置はこれまでなかった。
【0004】
そこで、本発明の目的は、上記従来等技術の有する問題点に鑑みて、スポットあるいはシームのいずれの溶着も可能で、しかも持ち運び容易で可搬性に優れた溶着部とこれを備えた超音波溶着装置を提供することにある。
【0005】
【課題を解決するための手段】上記目的は各請求項記載の発明により達成される。すなわち、本発明に係る溶着部の特徴構成は、超音波振動子と、この超音波振動子の発する振動を増幅すると共に端部に加工面を有するホーン部と、このホーン部の加工面との間で被溶着物を挟持可能な支持部と、この支持部を前記被溶着物の挟持位置と非挟持位置とに位置変更可能なレバー部とを有していて、前記支持部が前記レバー部とは別体の、異なる支点周りに回動可能な支持アーム部を介して前記レバー部を動作して位置変更可能になっていると共に、前記支持部が前記被溶着物の溶着方向に向けて回動可能になっており、前記被溶着物を挟持した際、前記被溶着物の先端と接当して溶着位置を定めると共に、前記支持部の回動に伴い回動する鍔状のストッパー部が形成されていることにある。
【0006】
この構成によれば、被溶着物を挟持して超音波溶着する際に、支持部が被溶着物の溶着方向に向けて回動可能になっていることから、溶着部を被溶着物の溶着方向に移動させる(あるいは被溶着物を溶着方向とは反対方向に移動させる)ことによりシーム溶着することができると共に、溶着部を被溶着物の溶着方向に移動させずに挟持位置でスポット溶着することもできる。しかも、レバー部の操作により支持部を前記被溶着物の挟持位置と非挟持位置とに位置変更可能な構成となっているので、装置全体を小型化でき、持ち運び容易で可搬性のよい構成とすることができる。その結果、本発明によれば、スポットあるいはシームのいずれも溶着可能で、しかも持ち運び容易で可搬性に優れた溶着部を提供することができた。
【0007】
前記支持部は、前記ホーン部の加工面との間で前記被溶着物を挟持して接当する部位に凸面が形成されて構成されていることが好ましい。この構成によれば、シーム溶着する際に、溶着部を把持する手で溶着された部分を確認しながら溶着部(あるいは被溶着物)を移動でき、溶着作業が安定するので都合がよい。もっとも、凸面は支持部表面に一定のピッチで複数個形成されていることがより好ましい。この場合、被溶着部に応じてピッチを適宜選択することにより、溶着された部分における、連続発熱によるひずみの発生を少なくできて都合がよいからであり、又剥離したい場合には剥離容易となって都合がよいからである。
【0008】
前記ホーン部の加工面の周囲縁部が曲面に形成されていることが好ましい。この構成によれば、シーム溶着する際に、溶着部(あるいは被溶着物)の移動を、被溶着物の表面を傷つけることなく円滑に行うことができて都合がよい。ホーン部加工面の縁部の曲面は、少なくとも被溶着物の溶着方向に対向する縁部に形成されていればよい。
【0009】
前記支持部は、前記被溶着物を挟持した際、前記被溶着物の先端と接当して溶着位置を定めるストッパー部が形成されていることが好ましい。この構成によれば、シーム溶着する際に、被溶着物の溶着位置を定めることができるので、溶着部(あるいは被溶着物)の移動を安定して行うことができて都合がよい。
【0010】
又、本発明に係る超音波溶着装置の特徴構成は、前記溶着部と、超音波発振機能を有する電源制御部とを備えたことにある。この構成によれば、スポットあるいはシームのいずれも溶着可能で、しかも溶着部、電源制御部のいずれも小型で構成でき、持ち運び容易で可搬性に優れた超音波溶着装置を提供することができる。
【0011】
超音波溶着装置として、前記電源制御部がタイマー機構を有することが好ましい。この構成によれば、被溶着物の材質、形状などに応じて好ましい加工(溶着)時間を選択できるので、確実な溶着箇所を形成できて都合がよい。
【0012】
【発明の実施の形態】
本発明の実施の形態を、図面を参照して詳細に説明する。図1は、本実施形態に係る超音波溶着装置Aの部分断面構造を示す。この超音波溶着装置Aは、超音波振動子3などを備え、各種熱可塑性樹脂などの被溶着物を挟持して溶着する機能を備えた溶着部1と、超音波を所定時間発生させるための超音波発振機能を備えた電源制御部2とからなっている。
【0013】
溶着部1は、片手で操作可能なように、把持部1aと、超音波振動子3を収納したヘッド部1bと、被溶着物を挟持する挟持部4と、この挟持部4の開閉を手で操作するレバー部5と、電源制御部2と接続するリード線L等とから構成されている。挟持部4は、通常、被溶着物を挟持し易くするため、板バネ(図示省略)によって開口状態にかるよう付勢されているが、被溶着物を所定位置に配置した後、把持部1aとレバー部5とを片手で握ると、後述するように、挟持部4が被溶着物を挟持するようになっている。従って、図1はバネの付勢力に抗して把持部1aとレバー部5とを接近させた状態を示すものである。把持部1aとレバー部5とを片手で握ることにより被溶着物を挟持完了すると、図示はしないが、溶着部1内部に設けられているリミット・スイッチが作用して通電されるようになっていて、把持部1aとレバー部5との把持力を緩めて、レバー部5を下方に下げるに任せるとリミット・スイッチが解除され、通電が遮断されるようになっている。
【0014】
尚、図番12は、溶着部1を一時的に作業場壁面などに設けられた吊り下げフック(図示略)に引っ掛けて吊り下げ可能にする引っ掛け部である。この引っ掛け部12は全体が略C字状をしていて、自由端側が溶着部1の尾部(リード線Lの挿入部近傍)に形成された穴に挿入されて、溶着部1に取り外し可能に取り付けられている。従って、引っ掛け部12は前記穴の周りに回動自在になっているので、この引っ掛け部12の長さを前記穴から長く突出するような大きさに形成すると、引っ掛け部12を前記穴周りに下方に回動すると共にレバー部5をその下方への付勢力に抗して上方に引上げ、この状態で引っ掛け部12によりレバー部5の自由端部を引っ掛けることができる。その結果、搬送時に全体の嵩を小さくまとめることができて都合がよい。
【0015】
前記挟持部4は、超音波振動子3に接続され超音波を増幅すると共に先細り状の先端に加工面6aを有するホーン部6と、このホーン部6の加工面6aとの間で被溶着物を挟持する支持部7とから構成されている。そして、把持部1aとレバー部5とを片手で握り、バネの付勢力に抗して両者を接近させる方向に力を入れると、レバー部5がその支点5a周りに上方に回動し、支点5aから幾分離れた位置に図1の紙面に対して垂直方向に差し渡されている棒状ピン5bが、支持部7に接続する支持アーム10を押し上げる。つまり、この支持アーム10はその支点10a周りに上方に押し上げられ、支点10aとは反対側に位置する支持アーム10の他端部に取り付けられている支持部7を押し上げて、結局、支持部7をホーン部6の加工面6aに接近させる。このようにして、加工面6aと支持部7との間に配置される被溶着物を挟持する。
【0016】
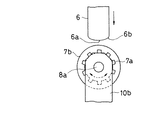
次に支持部7を、図2、3を参照して詳細に説明する。図2は、挟持部4により被溶着物Bである樹脂製袋体の開口部を溶着すべく挟持した状態を示す。支持部7は、前記支持アーム10の他端部に挿入されビス11で固着された略L字状の補助支持アーム10bに取り付けられている。つまり、支持部7は略円筒状に形成されていて、補助支持アーム10bに取り付けられたビス8の軸8a周りに回動可能に遊嵌されている。支持部7には、被溶着物Bと接する箇所として、図3に示すように、補助支持アーム10bに対面する側の外周面に沿って凹凸状に加工された凸部7aが10個形成されている。従って、被溶着物Bの挟持はホーン部6の加工面6aと前記凸部7aとの間で行われることになる。又、ビス8の他端側にはナット9が螺着されていて、ビス8が補助支持アーム10bに確実に固着されている。尚、図3は、ナット9を取り外した状態の側面構造を示す。
【0017】
更に、補助支持アーム10bと対向する側とは反対側の支持部7の端部には、支持部外周面から張り出して被溶着物Bの端部と接当する鍔状のストッパー部7bが形成されている。このようになっていると、被溶着物Bの端部をストッパー部7bに接当させることにより、被溶着物Bの溶着位置を端部から一定の位置に定めることができて好ましい。又、ホーン部6の加工面6aの縁部6bは、図3に示すように、シーム溶着する方向に曲面が形成されており、これにより縁部が尖鋭になって被溶着物Bの表面を傷つけたり、溶着部1の移動が円滑になり難くなるのを回避できるようになっている。もっとも、ホーン部6の加工面6aの縁部全周が全て曲面になっていてもよい。
【0018】
一方、電源制御部2は、スイッチ部2aと、溶着部1のリード線Lと接続可能なアウトプット部2bと、タイマー機構2cと、外部AC電源と接続するコード線2d等とから構成されている。このようにタイマー機構2cを備えていることにより、被溶着物Bの材質、形状などに応じて加工時間を変化させ、常に最適な溶着状態を達成できるようになっている。
【0019】
次に、上記超音波溶着装置Aを用いて、被溶着物Bを溶着する方法を説明する。予め被溶着物Bの材質、形状などにより溶着時間を、電源制御部2のタイマー機構2cを用いて設定する。スイッチ部2aをONにした後、図4(a)に示すような開口している挟持部4に被溶着物Bを挿入し、被溶着物Bの端部を支持部のストッパー部7bに接当させた状態でレバー部5と把持部1aとを片手で把持する。図4(b)に示すように、支持部7がホーン部6の加工面6aに上昇接近する。その結果、図2に示すように、被溶着物Bが挟持部4に挟持される。この状態で、シーム溶着する場合には、被溶着物Bを溶着部1に対して相対移動させればよい。スポット溶着する場合は、レバー部5と把持部1aとを片手で把持するだけでよい。
【0020】
〔別実施の形態〕
(1)上記実施形態では、被溶着物と接当する支持部の表面に歯車状の凹凸を形成し、その凸部と被溶着物の底面が接当するようにした例を示したが、支持部表面の凹凸の形状、ピッチ等は特に限定されず、互いに交差する刻み目を支持部の接当箇所である円周面に刻印したようなものでもよいし、円周面とせず多角形状に接当箇所を形成してもよい。又、支持部表面を、凹凸を形成しない平滑な円周面としてもよい。
【0021】
(2)本発明に適用できる被溶着物としては、A−PET(非晶質ポリエチレンテレフタレート)、PVC(ポリ塩化ビニル)、PP(ポリプロピレン)、OPS(延伸ポリスチレン)等の各種樹脂製容器、袋体などのみならず、樹脂製のリボン、シート製品など、超音波溶着可能な各種材質のものを挙げることができる。
【図面の簡単な説明】
【図1】本発明に係る超音波溶着装置の全体構成を示す正面一部断面図
【図2】図1の超音波溶着装置の使用状態を説明する挟持部近傍の正面断面図
【図3】図1の超音波溶着装置の挟持部近傍の右側面図
【図4】図1の超音波溶着装置の動作を説明する斜視図
【符号の説明】
1 溶着部
2 電源制御部
3 超音波振動子
5 レバー部
6 ホーン部
6a 加工面
7 支持部
7b ストッパー部
B 被溶着物
Claims (5)
- 超音波振動子と、この超音波振動子の発する振動を増幅すると共に端部に加工面を有するホーン部と、このホーン部の加工面との間で被溶着物を挟持可能な支持部と、この支持部を前記被溶着物の挟持位置と非挟持位置とに位置変更可能なレバー部とを有していて、前記支持部が前記レバー部とは別体の、異なる支点周りに回動可能な支持アーム部を介して前記レバー部を動作して位置変更可能になっていると共に、前記支持部が前記被溶着物の溶着方向に向けて回動可能になっており、前記被溶着物を挟持した際、前記被溶着物の先端と接当して溶着位置を定めると共に、前記支持部の回動に伴い回動する鍔状のストッパー部が形成されている溶着部。
- 前記支持部は、前記ホーン部の加工面との間で前記被溶着物を挟持して接当する部位に凸面が形成されて構成されている請求項1の溶着部。
- 前記ホーン部の加工面の周囲縁部が曲面に形成されている請求項1又は2の溶着部。
- 請求項1〜3のいずれか1の溶着部と、超音波発振機能を有する電源制御部とを備えた超音波溶着装置。
- 前記電源制御部がタイマー機構を有する請求項4の超音波溶着装置。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP01960399A JP3552939B2 (ja) | 1999-01-28 | 1999-01-28 | 溶着部とこれを備えた超音波溶着装置 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP01960399A JP3552939B2 (ja) | 1999-01-28 | 1999-01-28 | 溶着部とこれを備えた超音波溶着装置 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2000219215A JP2000219215A (ja) | 2000-08-08 |
| JP3552939B2 true JP3552939B2 (ja) | 2004-08-11 |
Family
ID=12003794
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP01960399A Expired - Fee Related JP3552939B2 (ja) | 1999-01-28 | 1999-01-28 | 溶着部とこれを備えた超音波溶着装置 |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP3552939B2 (ja) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5421578B2 (ja) * | 2008-12-04 | 2014-02-19 | 三愛工業株式会社 | 超音波溶着機 |
| JP7316864B2 (ja) * | 2018-07-27 | 2023-07-28 | Asti株式会社 | 超音波ホッチキスと超音波溶着方法 |
-
1999
- 1999-01-28 JP JP01960399A patent/JP3552939B2/ja not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| JP2000219215A (ja) | 2000-08-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP3854283B2 (ja) | 剥離式キャップの矯正開蓋装置 | |
| CN115593815A (zh) | 密封装置及袋状膜体 | |
| JP2003205912A (ja) | 袋取り出し装置、袋又はシートの吸着取り出し手段における吸引口の構造 | |
| JP2000219215A (ja) | 溶着部とこれを備えた超音波溶着装置 | |
| JP3479035B2 (ja) | 超音波溶着装置 | |
| CN110525754A (zh) | 带体回收装置 | |
| JP7316864B2 (ja) | 超音波ホッチキスと超音波溶着方法 | |
| EP4610181A1 (en) | Tape-adhering apparatus and computer program | |
| JP4390432B2 (ja) | 剥離工具及び剥離装置 | |
| CN119275150B (zh) | 用于晶圆盒的夹具及搬运机器人 | |
| KR101584103B1 (ko) | 아크용접봉 홀더 | |
| JP3321150B1 (ja) | プラスチック容器の蝶番部切り離し用紐掛け装置 | |
| JP7665458B2 (ja) | シート剥離装置およびシート剥離方法 | |
| JPH1158522A (ja) | 超音波溶着機 | |
| JP2003220648A (ja) | 超音波シール装置 | |
| CN217036283U (zh) | 连接插针焊接系统及其物料翻转组件 | |
| JP2020196488A (ja) | 帯掛け包装装置 | |
| CN217397587U (zh) | 一种汽车饰件v型卡扣自动送料振动盘 | |
| JP7421528B2 (ja) | テープ材貼付け機およびコンピュータプログラム | |
| JP2009274811A (ja) | シート剥離装置及び剥離方法 | |
| JP2020117291A (ja) | ラベル貼り付けシステム | |
| JP2002258491A (ja) | 画像記録装置及びそのプレート取り付け方法 | |
| JP7330479B2 (ja) | 帯巻き包装装置、包装方法 | |
| JP2004231774A (ja) | 部品の剥離方法及び剥離装置 | |
| JPH0977031A (ja) | シール貼り装置 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20040129 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20040205 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20040402 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20040427 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20040427 |
|
| R150 | Certificate of patent or registration of utility model |
Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20080514 Year of fee payment: 4 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20090514 Year of fee payment: 5 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20100514 Year of fee payment: 6 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20110514 Year of fee payment: 7 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20110514 Year of fee payment: 7 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20120514 Year of fee payment: 8 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20130514 Year of fee payment: 9 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20140514 Year of fee payment: 10 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| R250 | Receipt of annual fees |
Free format text: JAPANESE INTERMEDIATE CODE: R250 |
|
| LAPS | Cancellation because of no payment of annual fees |