JP4205652B2 - 割れの少ないブルーム鋳片の製造方法 - Google Patents
割れの少ないブルーム鋳片の製造方法 Download PDFInfo
- Publication number
- JP4205652B2 JP4205652B2 JP2004303261A JP2004303261A JP4205652B2 JP 4205652 B2 JP4205652 B2 JP 4205652B2 JP 2004303261 A JP2004303261 A JP 2004303261A JP 2004303261 A JP2004303261 A JP 2004303261A JP 4205652 B2 JP4205652 B2 JP 4205652B2
- Authority
- JP
- Japan
- Prior art keywords
- slab
- pitch
- roll
- cracks
- bloom
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000004519 manufacturing process Methods 0.000 title claims description 10
- 238000009749 continuous casting Methods 0.000 claims description 16
- 230000005499 meniscus Effects 0.000 claims description 14
- 238000000034 method Methods 0.000 claims description 13
- 229910000831 Steel Inorganic materials 0.000 claims description 10
- 239000010959 steel Substances 0.000 claims description 10
- 239000000498 cooling water Substances 0.000 claims description 8
- 238000007711 solidification Methods 0.000 description 30
- 230000008023 solidification Effects 0.000 description 30
- 238000005336 cracking Methods 0.000 description 12
- 239000002436 steel type Substances 0.000 description 9
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 8
- 229910052799 carbon Inorganic materials 0.000 description 8
- 230000007704 transition Effects 0.000 description 8
- 238000005204 segregation Methods 0.000 description 5
- 238000011144 upstream manufacturing Methods 0.000 description 5
- 238000001816 cooling Methods 0.000 description 4
- 230000000694 effects Effects 0.000 description 4
- 230000009467 reduction Effects 0.000 description 4
- 238000005266 casting Methods 0.000 description 3
- 239000007790 solid phase Substances 0.000 description 3
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 3
- VEXZGXHMUGYJMC-UHFFFAOYSA-N Hydrochloric acid Chemical compound Cl VEXZGXHMUGYJMC-UHFFFAOYSA-N 0.000 description 2
- 229910001209 Low-carbon steel Inorganic materials 0.000 description 2
- 230000009471 action Effects 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 238000005260 corrosion Methods 0.000 description 1
- 230000007797 corrosion Effects 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 238000007689 inspection Methods 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 230000005855 radiation Effects 0.000 description 1
- 238000005096 rolling process Methods 0.000 description 1
- 230000035945 sensitivity Effects 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 230000003068 static effect Effects 0.000 description 1
Images




Landscapes
- Continuous Casting (AREA)
Description
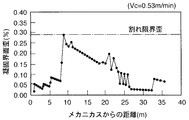
εc=φ(dε/dt)m/(ΔT)n…(1)
但し、φ:0.02821
m:0.3131
n:0.8638
dε/dt:歪速度
ΔT:固相率fs=0.9〜0.99までの温度範囲

断面が600mm×380mmのブルーム鋳片を、分塊工場にて断面155mm×155のビレットまで圧延した後、長さ10mのビレットを試料とし、磁分探傷装置によって表面割れを目視にて確認した。そして、各面の割れの合計数が50個以上発生したときは表面割れ有り(「×」印)と判定し、それ未満のときを割れ無し(「○」印)と判定した。
鋳造したブルーム鋳片(図5)から、各断面[C断面、L断面:図6(a),(b)]に相当するサンプルを採取し、その検査面に塩酸を塗布して腐食させ、各断面おいて鋳片上面および下面から夫々60〜100mmの範囲に相当する位置に発生する割れを目視にて確認した[図6(a)中G1〜G3、図(b)G4,G5にて示す]。そして確認できる割れの総長さ(mm)を夫々の面について求め[G1+G2+G3、G4+G5(mm)]、この値がC断面について50mm以上、L断面で70mm以上となったときに割れ有り(「×」印)と判定し、それ未満のときを割れ無し(「○」印)と判定した。
Claims (2)
- C含有量が0.99質量%の軸受鋼であり、軸直角断面形状が厚み:300〜400mm、幅:500〜650mmであるブルーム鋳片を連続鋳造法によって製造するに当たり、引き抜き速度を0.50〜0.90m/min、二次冷却水量を0.2〜0.5L/kgとし、鋳型内メニスカスからの距離で少なくとも8.0〜14.0mの位置に存在するロールのピッチを400〜500mmとして操業することを特徴とする割れの少ないブルーム鋳片の製造方法。
- 更に、14.0超〜20.0mの位置に存在するロールのピッチを400〜500mmとして操業する請求項1に記載の製造方法。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2004303261A JP4205652B2 (ja) | 2004-10-18 | 2004-10-18 | 割れの少ないブルーム鋳片の製造方法 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2004303261A JP4205652B2 (ja) | 2004-10-18 | 2004-10-18 | 割れの少ないブルーム鋳片の製造方法 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| JP2006110618A JP2006110618A (ja) | 2006-04-27 |
| JP4205652B2 true JP4205652B2 (ja) | 2009-01-07 |
Family
ID=36379562
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| JP2004303261A Expired - Fee Related JP4205652B2 (ja) | 2004-10-18 | 2004-10-18 | 割れの少ないブルーム鋳片の製造方法 |
Country Status (1)
| Country | Link |
|---|---|
| JP (1) | JP4205652B2 (ja) |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP4704980B2 (ja) * | 2006-09-05 | 2011-06-22 | 株式会社神戸製鋼所 | 大断面ブルーム連鋳における軸受鋼の中心偏析改善方法 |
| JP4704981B2 (ja) * | 2006-09-05 | 2011-06-22 | 株式会社神戸製鋼所 | 大断面ブルーム連鋳における機械構造用鋼の中心偏析改善方法 |
| JP4704982B2 (ja) * | 2006-09-05 | 2011-06-22 | 株式会社神戸製鋼所 | 大断面ブルーム連鋳におけるバネ用鋼の中心偏析改善方法 |
| JP4723451B2 (ja) * | 2006-10-12 | 2011-07-13 | 株式会社神戸製鋼所 | 復熱由来の内部割れに係る高炭素鋼の連続鋳造方法 |
| JP2009106967A (ja) * | 2007-10-30 | 2009-05-21 | Sumitomo Metal Ind Ltd | 鋼の連続鋳造方法 |
| CN114850423B (zh) * | 2022-05-21 | 2023-05-23 | 湖南华菱湘潭钢铁有限公司 | 一种中碳锰钢连铸大方坯角部裂纹的控制方法 |
-
2004
- 2004-10-18 JP JP2004303261A patent/JP4205652B2/ja not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| JP2006110618A (ja) | 2006-04-27 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6115735B2 (ja) | 鋼の連続鋳造方法 | |
| CN102398007B (zh) | 一种用于高铬合金钢大方坯连铸的轻压下工艺 | |
| JP6384679B2 (ja) | 熱延鋼板の製造方法 | |
| JP5835531B2 (ja) | 極厚鋼板用鋳片の連続鋳造方法 | |
| JP5085451B2 (ja) | ビレットの連続鋳造方法 | |
| JP6044614B2 (ja) | 鋼の連続鋳造方法 | |
| JP2006110618A (ja) | 割れの少ないブルーム鋳片の製造方法 | |
| JP6787359B2 (ja) | 鋼の連続鋳造方法 | |
| JP5825087B2 (ja) | 連続鋳造方法 | |
| CN109261920B (zh) | 小方坯连铸单辊压下方法和设备 | |
| JP5831118B2 (ja) | 鋼の連続鋳造方法及び装置 | |
| US20210138535A1 (en) | Continuous casting method of steel | |
| JP2001191158A (ja) | 鋼の連続鋳造方法 | |
| JP3619377B2 (ja) | ビレットの連続鋳造方法及び装置 | |
| JP4704979B2 (ja) | 連続鋳造における鋳片の軽圧下方法 | |
| JPH0890182A (ja) | 広幅薄鋳片の連続鋳造方法 | |
| JP2944476B2 (ja) | 鋳片の表面割れを防止した連続鍛圧法 | |
| JP6816523B2 (ja) | 鋼の連続鋳造方法 | |
| JP7817540B2 (ja) | 鋼の連続鋳造方法 | |
| JP2019076931A (ja) | 継目無鋼管用鋳片の連続鋳造方法 | |
| JP3524750B2 (ja) | 鋼の連続鋳造方法 | |
| JP5195636B2 (ja) | 連続鋳造鋳片の製造方法 | |
| JP4723451B2 (ja) | 復熱由来の内部割れに係る高炭素鋼の連続鋳造方法 | |
| JP3395674B2 (ja) | 連続鋳造方法 | |
| JP5691949B2 (ja) | 大断面鋳片の連続鋳造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| A977 | Report on retrieval |
Free format text: JAPANESE INTERMEDIATE CODE: A971007 Effective date: 20061016 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20061024 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20061221 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A821 Effective date: 20061221 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20070612 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20070808 |
|
| A131 | Notification of reasons for refusal |
Free format text: JAPANESE INTERMEDIATE CODE: A131 Effective date: 20070828 |
|
| A521 | Written amendment |
Free format text: JAPANESE INTERMEDIATE CODE: A523 Effective date: 20070927 |
|
| TRDD | Decision of grant or rejection written | ||
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 Effective date: 20081014 |
|
| A01 | Written decision to grant a patent or to grant a registration (utility model) |
Free format text: JAPANESE INTERMEDIATE CODE: A01 |
|
| A61 | First payment of annual fees (during grant procedure) |
Free format text: JAPANESE INTERMEDIATE CODE: A61 Effective date: 20081016 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20111024 Year of fee payment: 3 |
|
| R150 | Certificate of patent or registration of utility model |
Free format text: JAPANESE INTERMEDIATE CODE: R150 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20111024 Year of fee payment: 3 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20121024 Year of fee payment: 4 |
|
| FPAY | Renewal fee payment (event date is renewal date of database) |
Free format text: PAYMENT UNTIL: 20131024 Year of fee payment: 5 |
|
| LAPS | Cancellation because of no payment of annual fees |