TW202003183A - Workpiece processing method - Google Patents
Workpiece processing method Download PDFInfo
- Publication number
- TW202003183A TW202003183A TW108116990A TW108116990A TW202003183A TW 202003183 A TW202003183 A TW 202003183A TW 108116990 A TW108116990 A TW 108116990A TW 108116990 A TW108116990 A TW 108116990A TW 202003183 A TW202003183 A TW 202003183A
- Authority
- TW
- Taiwan
- Prior art keywords
- cutting
- workpiece
- height
- unit
- target
- Prior art date
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28D—WORKING STONE OR STONE-LIKE MATERIALS
- B28D5/00—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor
- B28D5/0058—Accessories specially adapted for use with machines for fine working of gems, jewels, crystals, e.g. of semiconductor material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28D—WORKING STONE OR STONE-LIKE MATERIALS
- B28D5/00—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor
- B28D5/0058—Accessories specially adapted for use with machines for fine working of gems, jewels, crystals, e.g. of semiconductor material
- B28D5/0064—Devices for the automatic drive or the program control of the machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28D—WORKING STONE OR STONE-LIKE MATERIALS
- B28D5/00—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor
- B28D5/0058—Accessories specially adapted for use with machines for fine working of gems, jewels, crystals, e.g. of semiconductor material
- B28D5/0076—Accessories specially adapted for use with machines for fine working of gems, jewels, crystals, e.g. of semiconductor material for removing dust, e.g. by spraying liquids; for lubricating, cooling or cleaning tool or work
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28D—WORKING STONE OR STONE-LIKE MATERIALS
- B28D5/00—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor
- B28D5/0058—Accessories specially adapted for use with machines for fine working of gems, jewels, crystals, e.g. of semiconductor material
- B28D5/0082—Accessories specially adapted for use with machines for fine working of gems, jewels, crystals, e.g. of semiconductor material for supporting, holding, feeding, conveying or discharging work
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28D—WORKING STONE OR STONE-LIKE MATERIALS
- B28D5/00—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor
- B28D5/02—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor by rotary tools, e.g. drills
- B28D5/022—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor by rotary tools, e.g. drills by cutting with discs or wheels
- B28D5/023—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor by rotary tools, e.g. drills by cutting with discs or wheels with a cutting blade mounted on a carriage
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28D—WORKING STONE OR STONE-LIKE MATERIALS
- B28D5/00—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor
- B28D5/02—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor by rotary tools, e.g. drills
- B28D5/022—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor by rotary tools, e.g. drills by cutting with discs or wheels
- B28D5/024—Fine working of gems, jewels, crystals, e.g. of semiconductor material; apparatus or devices therefor by rotary tools, e.g. drills by cutting with discs or wheels with the stock carried by a movable support for feeding stock into engagement with the cutting blade, e.g. stock carried by a pivoted arm or a carriage
-
- H—ELECTRICITY
- H10—SEMICONDUCTOR DEVICES; ELECTRIC SOLID-STATE DEVICES NOT OTHERWISE PROVIDED FOR
- H10P—GENERIC PROCESSES OR APPARATUS FOR THE MANUFACTURE OR TREATMENT OF DEVICES COVERED BY CLASS H10
- H10P52/00—Grinding, lapping or polishing of wafers, substrates or parts of devices
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Mechanical Treatment Of Semiconductor (AREA)
- Dicing (AREA)
- Electrical Discharge Machining, Electrochemical Machining, And Combined Machining (AREA)
- Constituent Portions Of Griding Lathes, Driving, Sensing And Control (AREA)
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
- Milling Processes (AREA)
Abstract
[課題]提供一種可以不使產量大幅降低,而能適當地調整切割刀片高度的工件加工方法。[解決手段]一種工件加工方法,其包含:基準設定步驟,設定切割單元的作為基準的高度;目標設定步驟,以使切割刀片切入到切割膠膜的預定深度的方式,來設定切割單元的作為目標的高度;第一切割步驟,在將切割單元定位在作為目標的高度的狀態下,藉由使切割單元與卡盤台做相對移動來切割加工工件;修正值取得步驟,基於切割刀片在切割膠膜上形成之接觸痕跡的長度,取得修正值;以及第二切割步驟,切割單元定位在依據修正值修正後之作為目標的高度的狀態下,藉由使切割單元與卡盤台做相對移動來切割加工工件。[Problem] To provide a workpiece processing method that can appropriately adjust the height of the cutting blade without greatly reducing the output. [Solution] A workpiece processing method, including: a reference setting step to set the height of the cutting unit as a reference; a target setting step to set the cutting unit as a way of cutting the cutting blade to a predetermined depth of the cutting film The height of the target; the first cutting step, in the state where the cutting unit is positioned at the height of the target, the workpiece is cut by relatively moving the cutting unit and the chuck table; the correction value obtaining step is based on the cutting blade The length of the contact trace formed on the adhesive film to obtain the correction value; and the second cutting step, the cutting unit is positioned at the height of the target after correction according to the correction value, by relatively moving the cutting unit and the chuck table To cut the workpiece.
Description
本發明係關於一種工件的加工方法,切割加工黏貼有切割膠膜的板狀工件。The invention relates to a processing method of a workpiece, which cuts and processes a plate-shaped workpiece adhered with a cutting glue film.
當加工代表半導體晶圓或封裝基板的板狀工件時,例如,使用在主軸上安裝有環狀切割刀片的切割裝置。一面使主軸旋轉並使切割刀片切入工件,一面使主軸以及切割刀片與工件做相對移動,藉此可以沿著此相對移動的方向切割加工工件。When processing a plate-shaped workpiece representing a semiconductor wafer or a package substrate, for example, a cutting device with a ring-shaped cutting blade mounted on a main shaft is used. While rotating the main shaft and cutting the cutting blade into the workpiece, the main shaft and the cutting blade and the workpiece are relatively moved, whereby the workpiece can be cut and processed along the direction of this relative movement.
可是,以如上述的切割裝置切割加工工件,切割刀片就會發生磨損,其直徑將會逐漸變小。若繼續使用直徑因磨損而變小的切割刀片,則切割刀片對於工件的切入就會變淺,無法適當地切割加工工件。However, when cutting the workpiece with the cutting device as described above, the cutting blade will wear out and its diameter will gradually become smaller. If the cutting blade whose diameter becomes smaller due to wear continues to be used, the cutting blade will cut into the workpiece shallower, and the workpiece cannot be properly cut and processed.
於是,下述方法被實用化:在任意時間點檢測切割刀片前端(下端)的位置,以此前端的位置為基準,來控制切割刀片對於工件的切入的方法(例如,參照專利文獻1)。此方法係為,使切割刀片侵入設置於切割裝置上的光學式感測器,藉由切割刀片遮斷感測器內的光路,檢測切割刀片前端的位置。 [習知技術文獻] [專利文獻]Therefore, the following method has been put into practical use: A method of detecting the position of the front end (lower end) of the cutting blade at an arbitrary point in time and using the position of the front end as a reference to control the cutting of the cutting blade into the workpiece (for example, see Patent Document 1). This method is to make the cutting blade invade the optical sensor provided on the cutting device, and block the optical path in the sensor by the cutting blade to detect the position of the front end of the cutting blade. [Conventional Technical Literature] [Patent Literature]
[專利文獻1]日本特開2001-298001號公報[Patent Document 1] Japanese Patent Laid-Open No. 2001-298001
[發明所欲解決的課題] 近幾年,伴隨著從工件切出之晶片的小型化等,設定於此工件上的加工預定線(切割道)的數量也增加。因此,容易發生下述狀況:在切割加工一片工件的途中,切割刀片大幅磨損,必須確認切割刀片前端的位置來調整切割刀片的高度。[Problems to be solved by the invention] In recent years, along with the miniaturization of wafers cut from workpieces, etc., the number of processing lines (dicing lanes) set on the workpieces has also increased. Therefore, the following situation is likely to occur: the cutting blade is greatly worn out during the cutting of a workpiece, and the height of the cutting blade must be adjusted by confirming the position of the front end of the cutting blade.
一旦發生這種狀況,就要停止工件的切割加工,以上述的感測器檢測切割刀片前端的位置後,調整切割刀片的高度,並重新開始切割加工。然而,這種情況下,必須使切割刀片在工件與感測器之間做相對移動,所以產量容易降低。Once this happens, the cutting process of the workpiece must be stopped. After detecting the position of the front end of the cutting blade with the sensor described above, the height of the cutting blade is adjusted, and the cutting process is restarted. However, in this case, the cutting blade must be relatively moved between the workpiece and the sensor, so the yield is easily reduced.
本發明是鑑於這種問題點而完成的發明,作為其目的,係提供一種可以不使產量大幅降低就能適當地調整切割刀片高度的工件加工方法。The present invention is made in view of such a problem, and as its object, it is to provide a workpiece processing method that can appropriately adjust the height of the cutting blade without greatly reducing the output.
[解決課題的技術手段] 根據本發明的一態樣,係為一種工件加工方法,其使用切割裝置對黏貼切割膠膜的工件進行切割加工,該切割膠膜貼在環狀框架開口上,該切割裝置包含:保持工件之卡盤台;切割單元,安裝有切割刀片,該切割刀片對保持在該卡盤台上的該工件進行切割加工;以及設定單元,基於該切割刀片外周前端的高度,設定該切割單元的作為基準的高度;該工件加工方法包含以下步驟:基準設定步驟,基於該切割刀片外周前端的高度,設定該切割單元的作為該基準的高度;目標設定步驟,以使該切割刀片切入到該切割膠膜的預定深度的方式,來設定該切割單元的作為目標的高度;第一切割步驟,在將該切割單元定位在作為該目標的高度的狀態下,藉由使該切割單元與該卡盤台做相對移動來切割加工該工件;修正值取得步驟,與該第一切割步驟同時,或在該第一切割步驟之後,基於該切割刀片在該切割膠膜上形成之接觸痕跡的長度,取得用於修正該切割單元的作為該目標的高度的修正值;以及第二切割步驟,在將該切割單元定位於依據該修正值修正作為該目標的高度後而得到的高度之狀態下,藉由使該切割單元與該卡盤台做相對移動來切割加工該工件。[Technical means to solve the problem] According to one aspect of the present invention, it is a workpiece processing method that uses a cutting device to perform cutting processing on a workpiece to which a cutting adhesive film is attached. The cutting adhesive film is attached to an opening of a ring frame. The cutting device includes: holding the workpiece A chuck table; a cutting unit installed with a cutting blade that cuts the workpiece held on the chuck table; and a setting unit that sets the cutting unit as a reference based on the height of the front end of the outer periphery of the cutting blade The height of the workpiece; the workpiece processing method includes the following steps: a reference setting step, based on the height of the outer peripheral front end of the cutting blade, setting the height of the cutting unit as the reference; a target setting step so that the cutting blade cuts into the cutting film The predetermined height of the cutting unit is used to set the target height of the cutting unit; the first cutting step, in the state of positioning the cutting unit at the target height, by making the cutting unit and the chuck table do Relatively move to cut and process the workpiece; the correction value acquisition step, at the same time as the first cutting step, or after the first cutting step, based on the length of the contact marks formed on the cutting film by the cutting blade, is used for A correction value of the height of the cutting unit as the target; and a second cutting step, by positioning the cutting unit at a height obtained by correcting the height of the target according to the correction value, by making the The cutting unit moves relative to the chuck table to cut and process the workpiece.
在本發明的一態樣中,也可以該第一切割步驟中,使該切割單元在該工件與該框架之間的該切割膠膜露出的第一區域下降,下降到作為該目標的高度後,以使該切割刀片相對於該工件移動,移動至與該第一區域相反側之該切割膠膜露出的第二區域為止的方式,藉由使該切割單元與該卡盤台做相對移動,於切割加工該工件的同時,在該切割膠膜上形成該接觸痕跡。In one aspect of the present invention, in the first cutting step, the cutting unit may be lowered in the first area exposed by the cutting glue film between the workpiece and the frame, and then lowered to the height as the target , By moving the cutting blade relative to the workpiece to the second area on the opposite side of the first area from which the cutting glue film is exposed, by relatively moving the cutting unit and the chuck table, While cutting the workpiece, the contact marks are formed on the cutting adhesive film.
此外,在本發明的一態樣中,更可以包含接觸痕跡形成步驟,其在第一切割步驟之後,該修正值取得步驟之前,使該切割單元在該工件與該框架之間的該切割膠膜之露出區域下降,藉由下降到作為該目標的高度,在該切割膠膜上形成該接觸痕跡。In addition, in one aspect of the present invention, a contact mark forming step may be further included, which is to make the cutting unit cut the glue between the workpiece and the frame after the first cutting step and before the correction value obtaining step The exposed area of the film descends, and by descending to the height as the target, the contact mark is formed on the dicing adhesive film.
此外,在本發明的一態樣中,可以在該修正值取得步驟中,基於由從該接觸痕跡的長度與該切割刀片的外徑算出之接觸痕跡的深度,取得該修正值。Furthermore, in one aspect of the present invention, in the correction value obtaining step, the correction value may be obtained based on the depth of the contact mark calculated from the length of the contact mark and the outer diameter of the cutting blade.
[發明功效] 在關於本發明一態樣的工件加工方法中,基於切割刀片在切割膠膜上形成之接觸痕跡的長度,取得用於修正切割單元的作為目標的高度的修正值,其後,將切割單元定位於依據此修正值修正後的高度來切割加工工件。[Effect of invention] In the workpiece processing method according to an aspect of the present invention, based on the length of the contact mark formed by the cutting blade on the cutting adhesive film, a correction value for correcting the target height of the cutting unit is obtained, and thereafter, the cutting unit is positioned Based on the height corrected by this correction value, the workpiece is cut and processed.
因此,每當切割刀片磨損時,即使不用設定單元檢測切割刀片外周前端的高度,也可以適當地調整切割單元的高度。即,當調整切割刀片的高度時,切割刀片相對移動的距離不需要如以往那麼大即可完成,所以可以不使產量大幅降低而適當地調整切割刀片的高度。Therefore, whenever the cutting blade is worn, the height of the cutting unit can be adjusted appropriately even without using the setting unit to detect the height of the front end of the outer periphery of the cutting blade. That is, when the height of the cutting blade is adjusted, the relative moving distance of the cutting blade does not need to be as large as in the past, so the height of the cutting blade can be adjusted appropriately without greatly reducing the output.
茲參照附圖,就關於本發明一態樣的實施方式進行說明。圖1為表示利用本實施方式的工件加工方法來進行切割加工之工件11等的構成例的立體圖。如圖1所示,工件11為,例如,使用矽(Si)等半導體材料所形成之圓盤狀的晶圓。The embodiment of the present invention will be described with reference to the drawings. FIG. 1 is a perspective view showing a configuration example of a
此工件11的正面11a側為,由互相交叉的多條加工預定線(切割道)13劃分成多個小區域,各小區域上形成有IC(Integrated Circuit;積體電路)等的元件15。於工件11的背面11b側,黏貼有直徑大於工件11之切割膠膜21的第一面21a側。The
此外,切割膠膜21的第一面21a側的外周部分黏貼於具有大致圓形開口23a的環狀框架23上。即,在工件11的背面11b側,黏貼有貼於環狀框架23之開口23a上的切割膠膜21,工件11透過此切割膠膜21而為框架23所支撐。In addition, the outer peripheral portion of the
再者,在本實施方式中,雖然將以矽等半導體材料形成之圓盤狀的晶圓作為工件11,但對工件11的材質、形狀、構造、大小等並無限制。例如,也可以將以其他的半導體、陶瓷、樹脂、金屬等材料形成之基板等用作工件11。同樣地,對元件15的種類、數量、形狀、構造、大小、配置等亦無限制。工件11上也可以未形成元件15。In addition, in this embodiment, although a disc-shaped wafer formed of a semiconductor material such as silicon is used as the
再者,在本實施方式中,雖然就將切割膠膜21黏貼於工件11的背面11b側,再從正面11a側切割加工工件11的例子進行說明,但也可以將切割膠膜21黏貼於工件11的正面11a側。這種情況,工件11就變成要從背面11b側來切割加工。In addition, in this embodiment, although the example where the
在關於本實施方式的工件加工方法中,首先,進行用於以切割裝置切割加工上述工件11的準備。圖2為表示在關於本實施方式的工件加工方法中所使用的切割裝置2之構成例的立體圖。再者,圖2中以功能方塊表示一部分的構成要素。如圖2所示,切割裝置2具備支撐各構成要素的基台4。In the workpiece processing method according to the present embodiment, first, preparation for cutting and processing the
在基台4前方的角落形成有開口4a,此開口4a內設有利用升降機構(未圖示)進行升降的卡匣升降機6。卡匣升降機6的上表面放置有卡匣8,該卡匣8係用於容納透過切割膠膜21而為框架23所支撐之狀態的工件11。再者,圖2中為了說明方便起見,只顯示卡匣8的輪廓。An opening 4a is formed in a corner in front of the
在卡匣升降機6的側面方向,於X軸方向上(前後方向、加工進給方向)形成有長的開口4b。開口4b內配置有滾珠螺桿式的X軸移動機構(加工進給機構)10,以及覆蓋X軸移動機構10上部的蛇腹狀罩蓋12。X軸移動機構10具備X軸移動台(未圖示),使此X軸移動台在X軸方向上移動。再者,此X軸移動台的上部為工作台罩蓋10a所覆蓋。In the lateral direction of the
X軸移動台上配置有用於透過切割膠膜21來保持工件11的卡盤台(保持台)14,該卡盤台14係為從工作台罩蓋10a露出的態樣。卡盤台14連結有馬達等旋轉驅動源(未圖示),圍繞與Z軸方向(垂直方向)大致平行的旋轉軸來旋轉。此外,卡盤台14藉由上述之X軸移動機構10,與X軸移動台共同在X軸方向上移動(加工進給 )。A chuck table (holding table) 14 for holding the
卡盤台14上表面的一部分為用於保持工件11的保持面14a。保持面14a係在相對X軸方向以及Y軸方向上(左右方向、分度進給方向)大致平行地形成,透過於卡盤台14內部形成之吸引通路14b(參照圖4(A))等而被吸引源(未圖示)所連接。此外,卡盤台14的周圍設置有4個夾具16,該夾具16係用於從四個方向固定支撐工件11的環狀框架23。A part of the upper surface of the chuck table 14 is a
在開口4b的上方配置有搬送單元(未圖示),該搬送單元係用於將上述工件11(框架23)往卡盤台14等搬送。以搬送單元搬送的工件11,例如以正面11a側往上方露出的方式,放置於卡盤台14的保持面14a上。即,在本實施方式中,黏貼於工件11之背面11b側的切割膠膜21會接觸卡盤台14的保持面14a。Above the opening 4b, a conveying unit (not shown) is arranged for conveying the workpiece 11 (frame 23) to the chuck table 14 or the like. The
在開口4b的側面方向配置有懸臂樑狀的支撐構造20,該支撐構造20係用於支撐切割工件11的切割單元18。在支撐構造20的前面上部,設置有使切割單元18在Y軸方向以及Z軸方向上移動的切割單元移動機構(分度進給機構、切入進給機構)22。A cantilever-
切割單元移動機構22具備有配置於支撐構造20的前面且與Y軸方向大致平行的一對Y軸導軌24。在Y軸導軌24上安裝有可滑動之Y軸移動板26,該Y軸移動板26構成了切割單元移動機構22。The cutting
在Y軸移動板26的背面側(後面側)設置有螺母部(未圖示),與Y軸導軌24大致平行的Y軸滾珠螺桿28被旋入此螺母部。Y軸滾珠螺桿28的一端部連結有Y軸脈衝馬達(未圖示)。若以Y軸脈衝馬達使Y軸滾珠螺桿28旋轉,則Y軸移動板26會沿著Y軸導軌24在Y軸方向上移動。A nut portion (not shown) is provided on the back side (rear side) of the Y-
在Y軸移動板26的表面(前面)設置有與Z軸方向大致平行的一對Z軸導軌30。在Z軸導軌30上安裝有可滑動之Z軸移動板32。A pair of Z-axis guide rails 30 substantially parallel to the Z-axis direction are provided on the surface (front surface) of the Y-
在Z軸移動板32的背面側(後面側)設置有螺母部(未圖示),與Z軸導軌30平行的Z軸滾珠螺桿34被旋入此螺母部。 Z軸滾珠螺桿34的一端部連結有Z軸脈衝馬達36。若以Z軸脈衝馬達36使Z軸滾珠螺桿34旋轉,則Z軸移動板32會沿著Z軸導軌30在Z軸方向上移動。A nut portion (not shown) is provided on the back side (rear side) of the Z-
在Z軸移動板32的下部固定有構成切割單元18的筒狀主軸外殼38。在主軸外殼38內,容納有作為旋轉軸的主軸40(參照圖3)。主軸40的一端部從主軸外殼38的一端側露出於外部,此主軸40的一端部安裝有用於切割加工工件11的切割刀片42。主軸40的另一端側連結有馬達等的旋轉驅動源(未圖示)。A
在鄰接於切割單元18的位置,設置有攝影機(攝影單元)44,該攝影機(攝影單元)44係用於拍攝保持於卡盤台14上的工件11等。若以切割單元移動機構22使Y軸移動板26在Y軸方向上移動,則切割單元18以及攝影機44會在Y軸方向上移動(分度進給)。此外,若以切割單元移動機構22使Z軸移動板32在Z軸方向上移動,則切割單元18以及攝影機44會在Z軸方向上移動(切入進給)。At a position adjacent to the cutting
在開口4b的上方且低於切割單元18的位置配置有刀片位置檢測單元(設定單元)46,該刀片位置檢測單元(設定單元)46係用於檢測切割刀片42的刀鋒(外周的前端)之Z軸方向的位置(高度)。此外,在相對於開口4b和開口4a為相反側的位置形成有開口4c。在開口4c內配置有清洗單元48,該清洗單元48係用於清洗切割加工後的工件11等。Above the
控制單元(設定單元)50連接有X軸移動機構10、切割單元18、切割單元移動機構22、攝影機44、刀片位置檢測單元46等各構成要素。控制單元50為,例如,對照工件11的加工條件等來控制切割裝置2的各構成要素。The control unit (setting unit) 50 is connected to the
圖3為切割單元18以及刀片位置檢測單元46的放大立體圖。再者,圖3中省略了切割單元18的一部分構成要素。如圖3所示,刀片位置檢測單元46具備位於切割單元18下方的檢測器54。檢測器54為,例如,包含以大致長方體狀構成的支撐部54a,以及設置於支撐部54a後端側(X軸方向的任一方側)上方的檢測部54b。FIG. 3 is an enlarged perspective view of the cutting
檢測部54b的上端部形成有已切出槽口的刀片侵入部54c,該刀片侵入部54c以切割刀片42可侵入之態樣所形成。刀片侵入部54c具備在Y軸方向上互相面對的一對內側面,在此一對內側面中,分別配置有構成光學式感測器的發光部56與受光部58。即,發光部56與受光部58隔著刀片侵入部54c而面對著。The upper end portion of the
位於檢測部54b前方側(X軸方向的另一方側)之支撐部54a的上表面,設置有兩支空氣供給噴嘴60,該空氣供給噴嘴60係用於供應空氣給發光部56與受光部58。此外,在空氣供給噴嘴60的前方,設置有兩支液體供給噴嘴62,該兩支液體供給噴嘴62係用於供應水等液體給發光部56與受光部58。例如,藉由從液體供給噴嘴62供應的液體清洗發光部56與受光部58後,利用從空氣供給噴嘴60供應的空氣乾燥發光部56與受光部58。Two
在檢測器54的後端面,透過以鉸鏈等形成的連結器64來安裝長方體狀的罩蓋66。此罩蓋66的內部為空洞。因此,例如,以連結器64為中心而使罩蓋66旋轉,藉此可將檢測部54b、空氣供給噴嘴60、液體供給噴嘴62等容納於罩蓋66的內部。A
另一方面,當要以刀片位置檢測單元46檢測切割刀片42外周前端的位置時,使罩蓋66旋轉到圖3所示的位置,而使得檢測部54b、空氣供給噴嘴60、液體供給噴嘴62等露出。藉此,就變得可以使切割刀片42侵入刀片侵入部54c的方式,檢測其外周前端的位置。On the other hand, when the position of the outer peripheral front end of the
在關於本實施方式的工件加工方法中,首先,基於上述切割刀片42外周前端的高度,將切割單元18的作為基準的高度(基準高度H0
)設定於切割裝置2(基準設定步驟)。具體而言,首先,將已使其旋轉之切割刀片42定位於刀片位置檢測單元46的檢測器54上方。然後,如圖3所示,在使光從發光部56放射的狀態下,使切割單元18下降,使已使其旋轉的切割刀片42侵入刀片侵入部54c(發光部56與受光部58之間)。In the workpiece processing method of the present embodiment, first, based on the height of the front end of the outer periphery of the
藉此,從發光部56往受光部58放射之光線,因切割刀片42而被部分地遮擋,受光部58的受光量會逐漸降低。控制單元50監視受光部58的受光量(相當於受光量的電壓值等),以及切割單元18的高度,例如,將受光部58的受光量降低到預定閾值時之切割單元18的高度作為基準高度H0
,使其記憶於控制單元50內的記憶部。As a result, the light radiated from the light-emitting
在本實施方式中,係將切割刀片42外周的前端與卡盤台14的保持面14a接觸時之切割單元18的高度設定為基準高度H0
。即,以設定此基準高度H0
的方式,調整受光部58的受光量閾值等。但是,基準高度H0
也可以不一定要以切割刀片42的外周前端與卡盤台14的保持面14a接觸的方式來設定。In the present embodiment, the height of the cutting
再者,在本實施方式中,雖然就使用上述刀片位置檢測單元46以非接觸設定基準高度H0
的例子進行了說明,但對基準高度H0
的設定方法並無限制。例如,也可以利用下述方法設定基準高度H0
:在卡盤台14與切割刀片42之間形成電位差,使此等構件接觸並確認導通。Furthermore, in the present embodiment, although the example in which the above-mentioned blade
設定基準高度H0
後,以能適當地切斷為卡盤台14所保持之工件11的方式,將切割單元18的作為目標的高度(目標高度H1
)設定於切割裝置2 (目標設定步驟)。更具體而言,以能夠使切割刀片42切入至與工件11共同保持於卡盤台14之切割膠膜21的預定深度的方式,設定目標高度H1
。After setting the reference height H 0 , the target height (target height H 1 ) of the cutting
例如,切割膠膜21的厚度為T0
,希望使切割刀片42切入至離此切割膠膜21的第一面21a之深度為D0
的位置時(即,第一面21a與切割刀片42之最下點的距離為D0
時),目標高度H1
係成為H0
+T0
-D0
。For example, if the thickness of the cutting
控制單元50使所得到的目標高度H1
記憶於控制單元50內的記憶部。再者,用於算出目標高度H1
的深度D0
,其較佳為5μm~35μm,具代表性的則為10μm程度。但是,深度D0
的值在可適當地切斷工件11的範圍內,可以任意調整。The
設定基準高度H0
與目標高度H1
後,切割加工工件11(第一切割步驟)。圖4(A)以及圖4(B)為表示切割加工工件11之情況的局部剖面側視圖。具體而言,首先,使黏貼於工件11的背面11b側的切割膠膜21接觸卡盤台14的保持面14a,使吸引源的負壓起作用。同時,以夾具16固定框架23。藉此,工件11以正面11a側往上方露出的狀態被保持。After setting the reference height H 0 and the target height H 1 , the
其次,例如,使卡盤台14旋轉,並使對象的加工預定線13與切割裝置2之X軸方向一致。此外,使卡盤台14以及切割單元18做相對移動,使切割刀片42的位置與對象的加工預定線13的延長線上方一致。Next, for example, the chuck table 14 is rotated, and the
然後,如圖4(A)所示,一面使切割刀片42旋轉,一面使切割單元18下降至目標高度H1
。其結果,切割刀片42在工件11與框架23之間的切割膠膜21露出的第一區域,切入切割膠膜21。Then, as shown in FIG. 4(A), while the
其後,使卡盤台14在X軸方向上移動。具體而言,如圖4(A)以及圖4(B)所示,以使切割刀片42相對移動到對於工件11和第一區域相反側之第二區域的方式,使卡盤台14在X軸方向上移動。Thereafter, the chuck table 14 is moved in the X-axis direction. Specifically, as shown in FIGS. 4(A) and 4(B), the chuck table 14 is positioned at X in such a manner that the
藉此,沿著對象的加工預定線13切割加工工件11。再者,此第二區域也和第一區域同樣,露出切割膠膜21。在本實施方式中,設卡盤台14在X軸方向上移動的距離(使切割刀片42做相對移動的距離)為x0
。Thereby, the
圖5(A)為表示被切割加工後之工件11等的俯視圖。上述切割加工的結果,工件11上會形成沿著對象的加工預定線13切斷工件11之態樣的切口((kerf)11c。在本實施方式中,一面使切割刀片42對切割膠膜21做切入,一面使其從第一區域相對移動至第二區域。因此,如圖5(A)所示,在切割膠膜21上也會形成藉由與切割刀片42的接觸所造成的接觸痕跡21b。FIG. 5(A) is a plan view showing the
例如,在沿著對象的加工預定線13切割加工工件11的同時,在切割膠膜21上形成接觸痕跡21b後,取得用於修正上述目標高度H1
的修正值(修正值取得步驟)。在本實施方式中,以基於由接觸痕跡21b的長度與切割刀片42的外徑(直徑)算出之接觸痕跡21b的深度,取得修正值。For example, while cutting the
再者,此處為了說明方便起見,雖然就沿著一條加工預定線13切割加工工件11後,取得修正值的例子進行說明,但也可以在沿著多條加工預定線13切割加工工件11後,取得修正值。在取得修正值之前,被切割加工之加工預定線13的數量(即,在第一切割步驟要被切割加工之加工預定線的數量)等,可按照切割刀片42磨損的狀況等進行調整。In addition, for the sake of convenience of explanation, although an example in which the correction value is obtained after cutting the processed
圖5(B)為表示使切割刀片42當場切入時(即,不使切割刀片42在X軸方向上做相對移動時),所形成之接觸痕跡的深度D的概念圖。從圖5(B)所示的幾何學上的關係來看,切割刀片42當場切入時,所形成之接觸痕跡的深度D可作為切割刀片42的直徑d,此接觸痕跡的長度(X軸方向的長度)則作為L0
,並以算式(1)表示。FIG. 5(B) is a conceptual diagram showing the depth D of the contact trace formed when the
【數學式1】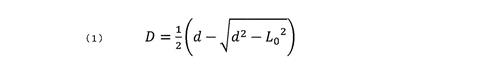
如上述,在本實施方式中,為了形成接觸痕跡21b,將切割刀片42相對移動的距離設定為x0
。因此,若設接觸痕跡21b的長度(X軸方向的長度)為L1
,則L0
成為L1
-x0
。即,接觸痕跡21b的深度D1
(≒D)可變成用接觸痕跡21b的長度L1
,以算式(2)表示。As described above, in the present embodiment, in order to form the
【數學式2】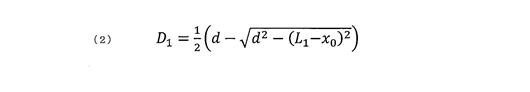
因此,要取得修正值時,首先,取得接觸痕跡21b的長度L1
。在本實施方式中,以攝影機44拍攝接觸痕跡21b而形成圖像,基於映現於此圖像上的接觸痕跡21b,控制單元50算出長度L1
。再者,接觸痕跡21b的影像以及長度L1
的取得也可以與上述工件11的切割加工同時進行。於此情況,就變成修正值取得步驟的一部分與第一切割步驟同時進行。Therefore, to obtain the correction value, first, the length L 1 of the contact mark 21b is obtained. In this embodiment, the
切割刀片42的直徑d以及切割刀片42相對移動的距離x0
為已知。因此,利用算出接觸痕跡21b之長度L1
,可從上述算式(2)算出接觸痕跡21b的深度D1
。由於磨損等所造成之切割刀片42的直徑d的減少,對接觸痕跡21b的深度D1
幾乎沒有影響,所以可以忽略不計。The diameter d of the
控制單元50算出接觸痕跡21b的深度D1
後,基於此深度D1
取得修正值。在本實施方式中,在算出目標高度H1
時,將所使用的深度D0
與接觸痕跡21b的深度D1
之差D0
-D1
作為修正值。控制單元50取得修正值後,使其記憶於控制單元50內的記憶部。After calculating the depth D 1 of the
取得修正值後,將切割單元18定位於依據此修正值修正目標高度H1
後而得到之高度,切割加工工件11(第二切割步驟)。圖6(A)為表示切割加工工件11之情況的局部剖面側視圖,圖6(B)為表示被切割加工後之工件11等的俯視圖。After obtaining the correction value, the cutting
具體的切割加工程序與上述第一切割步驟相同。具體而言,首先,使卡盤台14以及切割單元18做相對移動,使切割刀片42的位置與對象的加工預定線13的延長線上方一致。再者,剛被切割加工完之加工預定線13的方向與對象之加工預定線13的方向不同時,必須旋轉卡盤台14,使對象的加工預定線13與切割裝置2的X軸方向一致。The specific cutting process is the same as the above-mentioned first cutting step. Specifically, first, the chuck table 14 and the cutting
其次,如圖6(A)所示,一面使切割刀片42旋轉,一面使切割單元18下降到預定的高度H2
。在本實施方式中,例如,將目標高度H1
與修正值D0
-D1
之差H1
-(D0
-D1
)當作預定的高度H2
使用。此為只有因切割刀片42的磨損而切入變淺的部分,意味著將切割單元18定位於較低的位置。Next, as shown in FIG. 6(A), while rotating the
然後,使卡盤台14在X軸方向上移動。藉此,工件11會沿著對象的加工預定線13而被切割加工。圖6(B)為表示被切割加工後之工件11等的俯視圖。上述切割加工的結果,工件11上會形成沿著對象的加工預定線13切斷工件11之態樣的切口(kerf)11d。Then, the chuck table 14 is moved in the X-axis direction. As a result, the
此處,由於按照上述程序取得之修正值來修正了目標高度H1
,即使在切割刀片42磨損時,也可以使此切割刀片42切入到適當的高度來切割加工工件11。再者,在之後的切割刀片42磨損等之場合,於再次進行修正值取得步驟而取得修正值後,進行更進一步的切割步驟即可。Here, since the target height H 1 is corrected according to the correction value obtained by the above procedure, even when the
如以上,在關於本實施方式之工件加工方法中,基於藉由切割刀片42於切割膠膜21上形成之接觸痕跡21b的長度,取得用於修正切割單元18的作為目標的高度的修正值,其後,將切割單元18定位於依據此修正值修正後之高度來切割加工工件11。As described above, in the workpiece processing method of the present embodiment, based on the length of the
因此,每當切割刀片42磨損時,即使不用刀片位置檢測單元(設定單元)46等檢測切割刀片42外周前端的高度,也可以適當地調整切割單元18的高度。即,當調整切割刀片42的高度時,切割刀片42相對移動的距離不需要如以往那麼大即可完成,所以可以不使產量大幅降低而適當地調整切割刀片42的高度。Therefore, whenever the
再者,本發明不受上述實施方式的記載限制,可進行各種變更而實施。例如,在上述實施方式中,雖然在切割加工工件11的第一切割步驟中,於工件11上形成切口(kerf)11c的同時,在切割膠膜21上形成接觸痕跡21b,但也可以在第一切割步驟後,以不同的步驟形成接觸痕跡(接觸痕跡形成步驟)。In addition, the present invention is not limited by the description of the above embodiment, and can be implemented with various changes. For example, in the above embodiment, in the first cutting step of cutting the
圖7為表示用與上述實施方式不同的步驟形成接觸痕跡21c的切割膠膜21等的俯視圖。要形成如這種接觸痕跡21c時,例如,在第一切割步驟中,沿著對象的加工預定線13切割加工工件11後,使切割刀片42切入比第二區域更外側(即框架23側)的第三區域。FIG. 7 is a plan view showing the dicing
即,在第一切割步驟中,切割加工工件11後,使切割單元18上升,再使卡盤台14在X軸方向上移動。具體而言,以切割刀片42相對移動至第三區域上方為止之方式,使卡盤台14在X軸方向上移動。That is, in the first cutting step, after the
然後,例如,在卡盤台14未移動的狀態下,使切割單元18下降至目標高度H1
。其結果,切割刀片42在工件11與框架23之間的切割膠膜21露出的第三區域,切入切割膠膜21。Then, for example, in a state where the chuck table 14 is not moved, the cutting
藉此,在切割膠膜21上形成接觸痕跡21c。如此,藉由使切割刀片42當場切入的程序,所形成之切割痕跡21c的長度(X軸方向的長度)L2
等於上述算式(1)之接觸痕跡的長度L0
。因此,控制單元50可從算式(1)算出接觸痕跡21c的深度D2
(=D))。With this, a
其他,關於上述實施方式的構造、方法等,只要不脫離本發明目的的範圍,就可以適當變更而實施。In addition, the structure, method, and the like of the above-described embodiment can be appropriately modified and implemented without departing from the scope of the object of the present invention.
11‧‧‧工件 11a‧‧‧正面 11b‧‧‧背面 11c、11d‧‧‧切口(kerf) 13‧‧‧加工預定線(切割道) 15‧‧‧元件 21‧‧‧切割膠膜 21a‧‧‧第一面 21b、21c接觸痕跡 23‧‧‧框架 23a‧‧‧開口 2‧‧‧切割裝置 4‧‧‧基台 4a、4b、4c‧‧‧開口 6‧‧‧卡匣升降機 8‧‧‧卡匣 10‧‧‧X軸移動機構(加工進給機構) 10a‧‧‧工作台罩蓋 12‧‧‧波紋狀罩蓋 14‧‧‧卡盤台(保持台) 14a‧‧‧保持面 14b‧‧‧吸引通路 16‧‧‧夾具 18‧‧‧切割單元 20‧‧‧支撐構造 22‧‧‧切割單元移動機構(分度進給機構、切入進給機構) 24‧‧‧Y軸導軌 26‧‧‧Y軸移動板 28‧‧‧Y軸滾珠螺桿 30‧‧‧Z軸導軌 32‧‧‧Z軸移動板 34‧‧‧Z軸滾珠螺桿 36‧‧‧Z軸脈衝馬達 38‧‧‧主軸外殼 40‧‧‧主軸 42‧‧‧切割刀片 44‧‧‧攝影機(攝影單元) 46‧‧‧刀片位置檢測單元(設定單元) 48‧‧‧清洗單元 50‧‧‧控制單元(設定單元) 54‧‧‧檢測器 54a‧‧‧支撐部 54b‧‧‧檢測部 54c‧‧‧刀片侵入部 56‧‧‧發光部 58‧‧‧受光部 60‧‧‧空氣供給噴嘴 62‧‧‧液體供給噴嘴 64‧‧‧連結器 66‧‧‧罩蓋11‧‧‧Workpiece 11a‧‧‧Front 11b‧‧‧Back 11c, 11d‧‧‧cut (kerf) 13‧‧‧Scheduled processing line (cutting path) 15‧‧‧ Components 21‧‧‧Cutting film 21a‧‧‧The first side 21b, 21c contact marks 23‧‧‧Frame 23a‧‧‧ opening 2‧‧‧Cutting device 4‧‧‧Abutment 4a, 4b, 4c‧‧‧ opening 6‧‧‧ cassette elevator 8‧‧‧Cassette 10‧‧‧X axis moving mechanism (processing feed mechanism) 10a‧‧‧Workbench cover 12‧‧‧Corrugated cover 14‧‧‧Chuck table (holding table) 14a‧‧‧Keep 14b‧‧‧Attraction 16‧‧‧Fixture 18‧‧‧Cutting unit 20‧‧‧Support structure 22‧‧‧Moving mechanism of cutting unit (indexing feed mechanism, cutting feed mechanism) 24‧‧‧Y axis guide 26‧‧‧Y axis moving board 28‧‧‧Y-axis ball screw 30‧‧‧Z axis guide 32‧‧‧Z moving plate 34‧‧‧Z-axis ball screw 36‧‧‧Z-axis pulse motor 38‧‧‧spindle housing 40‧‧‧spindle 42‧‧‧Cutting blade 44‧‧‧Camera (Photography unit) 46‧‧‧Blade position detection unit (setting unit) 48‧‧‧cleaning unit 50‧‧‧Control unit (setting unit) 54‧‧‧Detector 54a‧‧‧Support 54b‧‧‧Detection Department 54c‧‧‧Blade intrusion 56‧‧‧Lighting Department 58‧‧‧Receiving Department 60‧‧‧Air supply nozzle 62‧‧‧Liquid supply nozzle 64‧‧‧Connector 66‧‧‧Cover
圖1表示工件等構成例的立體圖。 圖2表示切割裝置之構成例的立體圖。 圖3為切割單元以及刀片位置檢測單元的放大立體圖。 圖4的圖4(A)以及圖4(B)表示切割加工工件之情況的局部剖面側視圖。 圖5的圖5(A)表示被切割加工後之工件等的俯視圖,圖5(B)表示接觸痕跡之深度的概念圖。 圖6的圖6(A)表示切割加工工件之情況的局部剖面側視圖,圖6(B)表示被切割加工後之工件等的俯視圖。 圖7表示用不同的步驟形成接觸痕跡之切割膠膜等的俯視圖。FIG. 1 shows a perspective view of a configuration example of a workpiece and the like. 2 is a perspective view showing a configuration example of a cutting device. 3 is an enlarged perspective view of a cutting unit and a blade position detection unit. 4(A) and 4(B) of FIG. 4 show a partial cross-sectional side view of a state where a workpiece is cut and processed. 5(A) of FIG. 5 shows a plan view of a workpiece and the like after being cut, and FIG. 5(B) shows a conceptual view of the depth of contact marks. 6(A) of FIG. 6 shows a partial cross-sectional side view of a state where a workpiece is cut and processed, and FIG. 6(B) shows a plan view of the workpiece and the like after being cut and processed. FIG. 7 shows a plan view of a dicing film or the like that forms contact marks in different steps.
11‧‧‧工件 11‧‧‧Workpiece
11a‧‧‧正面 11a‧‧‧Front
11c‧‧‧切口 11c‧‧‧Notch
13‧‧‧加工預定線 13‧‧‧Scheduled processing line
15‧‧‧元件 15‧‧‧ Components
21‧‧‧切割膠膜 21‧‧‧Cutting film
21a‧‧‧第一面 21a‧‧‧The first side
21b‧‧‧接觸痕跡 21b‧‧‧Contact marks
23‧‧‧框架 23‧‧‧Frame
23a‧‧‧開口 23a‧‧‧ opening
42‧‧‧切割刀片 42‧‧‧Cutting blade
L1‧‧‧長度 L 1 ‧‧‧ length
Claims (4)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2018097231A JP2019202356A (en) | 2018-05-21 | 2018-05-21 | Processing method for work piece |
| JP2018-097231 | 2018-05-21 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| TW202003183A true TW202003183A (en) | 2020-01-16 |
| TWI779194B TWI779194B (en) | 2022-10-01 |
Family
ID=68622443
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| TW108116990A TWI779194B (en) | 2018-05-21 | 2019-05-16 | Workpiece processing method |
Country Status (3)
| Country | Link |
|---|---|
| JP (1) | JP2019202356A (en) |
| CN (1) | CN110509444B (en) |
| TW (1) | TWI779194B (en) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP7463037B2 (en) * | 2020-08-26 | 2024-04-08 | 株式会社ディスコ | Testing board and testing method |
| JP7539813B2 (en) * | 2020-10-22 | 2024-08-26 | 株式会社ディスコ | Detection Method |
| JP7660973B2 (en) * | 2021-04-21 | 2025-04-14 | 株式会社ディスコ | Wafer cutting method |
| CN117790294B (en) * | 2023-12-29 | 2026-02-06 | 沈阳和研科技股份有限公司 | Cutting blade height adjusting method and device for dicing saw and dicing saw |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2662703B2 (en) * | 1988-10-28 | 1997-10-15 | 住友電気工業株式会社 | Semiconductor wafer dicing equipment |
| JPH0767692B2 (en) * | 1989-09-07 | 1995-07-26 | 株式会社東京精密 | Cutting method of slicing machine |
| JP3157751B2 (en) * | 1997-09-03 | 2001-04-16 | 山口日本電気株式会社 | Dicing method for semiconductor substrate |
| JP5858684B2 (en) * | 2011-08-15 | 2016-02-10 | 株式会社ディスコ | Cutting method |
| JP6251574B2 (en) * | 2014-01-14 | 2017-12-20 | 株式会社ディスコ | Cutting method |
| JP2015214002A (en) * | 2014-05-13 | 2015-12-03 | 株式会社ディスコ | Cutting method |
| JP2016192494A (en) * | 2015-03-31 | 2016-11-10 | 株式会社ディスコ | Wafer dividing method |
| JP6727699B2 (en) * | 2016-04-19 | 2020-07-22 | 株式会社ディスコ | How to set up cutting equipment |
-
2018
- 2018-05-21 JP JP2018097231A patent/JP2019202356A/en active Pending
-
2019
- 2019-05-16 TW TW108116990A patent/TWI779194B/en active
- 2019-05-20 CN CN201910417678.2A patent/CN110509444B/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| JP2019202356A (en) | 2019-11-28 |
| CN110509444B (en) | 2022-10-18 |
| CN110509444A (en) | 2019-11-29 |
| TWI779194B (en) | 2022-10-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| TWI653677B (en) | Alignment method | |
| TWI657494B (en) | Wafer processing method | |
| CN107210206B (en) | Cutting device and method of manufacturing a plurality of products by cutting objects to be cut | |
| JP7282461B2 (en) | Inspection equipment and processing equipment | |
| TWI606549B (en) | Suction cup table | |
| JP7062449B2 (en) | How to cut the workpiece | |
| CN111834254B (en) | Processing device and processing method of processed object | |
| TWI779194B (en) | Workpiece processing method | |
| CN105702627B (en) | Cutting device | |
| JP6415349B2 (en) | Wafer alignment method | |
| US9569852B2 (en) | Alignment method | |
| TWI713706B (en) | How to install the cutting device | |
| JP2018078145A (en) | Cutting equipment | |
| CN110893574B (en) | Edge trimming device | |
| CN103659002B (en) | Processing unit (plant) | |
| TW202234492A (en) | Method of processing workpiece | |
| CN110039674A (en) | The management method and cutting apparatus of cutting tool | |
| JP2012151225A (en) | Method for measuring cut groove | |
| TW202138114A (en) | Cutting apparatus | |
| CN110076917B (en) | Method for setting cutting device | |
| TWI754742B (en) | Processing method of fan-shaped wafer | |
| JP5356803B2 (en) | Wafer processing equipment | |
| CN105914164B (en) | Processing device | |
| JP7300938B2 (en) | Kerf recognition method | |
| JP2009206362A (en) | Method of cutting plate-like material |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GD4A | Issue of patent certificate for granted invention patent |