US3626821A - Method for making continuous form envelopes - Google Patents
Method for making continuous form envelopes Download PDFInfo
- Publication number
- US3626821A US3626821A US875289A US3626821DA US3626821A US 3626821 A US3626821 A US 3626821A US 875289 A US875289 A US 875289A US 3626821D A US3626821D A US 3626821DA US 3626821 A US3626821 A US 3626821A
- Authority
- US
- United States
- Prior art keywords
- web
- envelope
- sets
- assemblies
- series
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 38
- 230000000712 assembly Effects 0.000 claims abstract description 44
- 238000000429 assembly Methods 0.000 claims abstract description 44
- 239000000463 material Substances 0.000 claims abstract description 28
- 238000005520 cutting process Methods 0.000 claims abstract description 20
- 239000000853 adhesive Substances 0.000 claims description 41
- 230000001070 adhesive effect Effects 0.000 claims description 41
- 230000003313 weakening effect Effects 0.000 claims description 13
- 238000007789 sealing Methods 0.000 description 3
- 230000000717 retained effect Effects 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B70/00—Making flexible containers, e.g. envelopes or bags
- B31B70/26—Folding sheets, blanks or webs
- B31B70/262—Folding sheets, blanks or webs involving longitudinally folding, i.e. along a line parallel to the direction of movement
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2150/00—Flexible containers made from sheets or blanks, e.g. from flattened tubes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2155/00—Flexible containers made from webs
- B31B2155/001—Flexible containers made from webs by folding webs longitudinally
- B31B2155/0014—Flexible containers made from webs by folding webs longitudinally having their openings facing transversally to the direction of movement
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B2160/00—Shape of flexible containers
- B31B2160/10—Shape of flexible containers rectangular and flat, i.e. without structural provision for thickness of contents
- B31B2160/104—Shape of flexible containers rectangular and flat, i.e. without structural provision for thickness of contents obtained from rhombus shaped sheets
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B—MAKING CONTAINERS OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31B70/00—Making flexible containers, e.g. envelopes or bags
- B31B70/14—Cutting, e.g. perforating, punching, slitting or trimming
- B31B70/16—Cutting webs
- B31B70/18—Cutting webs longitudinally
Definitions
- each assembly is further separated into sets, each set including a plurality of envelopes joined together in end-to-end relation and having connecting strips at the opposite ends thereof.
- the sets are arranged with the connecting strips thereof longitudinally aligned and are joined together in series-connected relation by attaching a pair of spaced carrier strips to the connecting strips.
- This invention relates in general to continuous form envelopes and deals more particularly with improved continuous form envelope structure and methods for making same.
- continuous form envelopes are made by folding and joining portions of an advancing web of sheet material to simultaneously form two groups of series-connected envelope bodies and cutting the advancing web to simultaneously shape the envelope closing flaps and separate the envelope assemblies from each other.
- the envelopes comprising each assembly are further separated into sets, each set including a plurality of joined together in end-to-end relation.
- the sets are joined together in series-connected relation by applying spaced carrier strips thereto.
- FIG. 1 is a fragmentary plan view of an envelope assembly made in accordance with the present invention.
- FIG. 2 is a sectional view taken along the line 2-2 of FIG. 1.
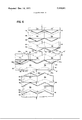
- FIG. 3 is a somewhat reduced plan view of a web of sheet material from which the envelope assembly of FIG. I is made and shows, from left to right, successive changes in the material as two envelope assemblies are simultaneously formed therefrom.
- FIG. 4 is a fragmentary plan view of another envelope assembly made in accordance with the invention.
- FIG. 5 is a generally similar to FIG. 3 but illustrates another method for simultaneously making two assemblies of seriesconnected envelopes.
- FIG. 6 is a fragmentary continuation of FIG. 5.
- a typical assembly of continuous form or series-connected envelopes made in accordance with a method of the present invention and indicated generally at 10 comprises a group of individual seamless envelopes l2, 12 connected together in end-to-end relation along lines of perforation or weakening I4, 14.
- Each envelope has a body defining a pocket and formed by a front panel 16 and a rear panel 18 connected to the lower edge of the front panel along a longitudinally extending fold line 20.
- the panels 16 and 18 are joined together in face-to-face relation near the lines of weakening I4, 14 which define the opposite ends thereof by lines of attachment defined by strips of adhesive 22, 22.
- the rear panel 18 has a line 23 imprinted thereon to simulate an envelope bottom panel of conventional folded type.
- Each envelope 12 also includes a triangular closing flap 24 connected to the upper edge of the front panel 16 along another longitudinally extending fold line 26.
- a chevronshaped line of adhesive 28 which may, for example, be of a remoistenable or pressure sensitive type is carried by the closing flap 24 for sealing the flap in engagement with the rear panel 18 to provide a closure for the mouth of the envelope.
- FIG. 3 A two-up method for simultaneously making two assemblies of series-connected envelopes l0, 10 from an advancing elongated web of sheet material or paper 30 is illustrated in FIG. 3.
- the illustrated method is particularly adapted to be practiced with a conventional automatic envelope making machine of the type capable of continuously advancing the web at high speed through a plurality of work stations where a variety of operations are performed thereon, as, for example, scoring, folding, gumming, cutting and imprinting messages or designs. However, for clarity of illustration, the machine is not shown.
- sequence of operations may vary and will, of course, depend upon the arrangement of the various work stations and the order in which these stations are encountered by the advancing web. A preferred sequence of operations is illustrated and will be evident from consideration of the web 30 as viewed from left to right in FIG. 3 or in the direction of web advance as indicated by the arrow.
- the parallel score or fold lines 20, 20 and 26, 26 are formed on the advancing web and separate marginal portions 32, 32 from a central portion 34 thereof.
- Each marginal portion 32 is folded inwardly or toward the other marginal portion and along a respectively associated fold line 20 to over lie the central portion 34.
- the bodies of the envelopes 12, 12 are formed by connecting each marginal portion 32 in face-to-face relation to an associated underlying part of the central portion 34 by the lines of adhesive 22, 22 which, as shown, are applied to each marginal portion before it is folded.
- Moist adhesive is preferably used and for this reason each line of adhesive 22 is spaced from its respectively associated fold line 20 by a small margin sufficient to accommodate a folding bar of a conventional envelope making machine without danger of the folding bar smearing the adhesive.
- the lines of adhesive 22, 22 applied to one marginal portion 32 are longitudinally offset with respect to the lines of adhesive 22, 22 applied to the opposite marginal portion.
- two assemblies or groups of envelope bodies are formed at opposite sides of the folded web, the envelope bodies in one group being longitudinally offset with respect to the envelope bodies in the other group.
- the two groups of envelope bodies are longitudinally offset with respect to each other a distance substantially equal to one-half the longitudinal dimension of an envelope body 12.
- Each group of envelope bodies is connected to the other by an intermediate portion of the web indicated at 36 and exposed between the longitudinally extending free or inner edges of the marginal portions 32, 32.
- Each marginal portion 32 forms the front panels l6, 16 of an associated group of envelope bodies, the back panels l8, 18 thereof being formed by an associated underlying part of the web central portion 34.
- the lines 23, 23 are imprinted on the lower surface of the web 30 before it is folded.
- Adhesive for sealing the envelope closing flaps is preferably applied to the intermediate portion 36 when the lines of adhesive 22, 22 are applied to the web.
- the flap adhesive may be applied in various continuous or interrupted patterns and may, if desired, cover the entire intermediate portion 36.
- a line of adhesive 37 is applied in a zigzag pattern to the intermediate portion 36 and extends in a generally longitudinal direction alternately traversing the intennediate portion in one and an opposite direction.
- the various lines of weakening 14, 14 are preferably formed on the folded web after the envelope bodies are formed. Each line of weakening 14 extends inwardly from an associated fold line 20 and terminates at or near a respectively associated one of the fold lines 26, 26.
- the various lines of weakening 14, 14 define the end portions of the envelope 12, 12, consequently, the line of weakening associated with one group of envelope bodies are longitudinally offset with respect to the lines of weakening on the opposite group of envelop bodies.
- the advancing web is cut to form the envelope closing flaps and simultaneously separate the two groups of series-connected envelopes from each other.
- the two envelope assemblies l0, 10 are separated from each other by cutting the advancing web along a parting line 38 which alternately traverses the intermediate portion 36 and forms an alternate series of junctures with the lines of weakening 14, 14 near the fold lines 26, 26.
- the parting cut is made along the line of adhesive 37.
- a plurality of substantially identical triangular-shaped envelope flaps 24, 24 are formed as the two envelope assemblies are separated, each flap being connected to an associated envelope panel 16 and carrying a chevron-shaped line of adhesive 28.
- the individual envelopes l2, 12 which comprise each group or assembly 10 may be further separated from each other along the various lines of weakening l4, l4.
- the envelope assemblies l0, 10 may, if desired, be formed with inserts therein, a typical insert being indicated at 40, 40 in FIG. 3.
- Each insert 40 is positioned on the web 30 before the marginal portions 32, 32 are folded inwardly.
- One or more spots of release-type adhesive such as indicated at 42, 42 may be employed if desired, to retain each insert in proper position while an associated envelope 12 is formed therearound.
- Each envelope 12 may also be provided with a window formed therein, such as indicated at 44, so that material printed on an associated insert 40 before assembly will be visible therethrough. The window also facilitates imprinting on the latter inserts at some later time.
- the envelope assembly 100 generally comprises a plurality of envelope sets 46, 46 joined together in longitudinal series.
- Each envelope set 46 includes tow or more envelopes 12a, 12a connected together in end-toend relation and has connecting strips 48, 48 extending outwardly from its opposite ends.
- the envelopes 12a, 120 are separated from each other and from the connecting strips 48, 48 by lines of weakening 14a, 14a.
- the sets 46, 46 are retained in series-connected relation by the carrier strips 50, 50 adhesively attached to the connecting strips 48, 48.
- Each carrier strip has a longitudinally spaced series of configurations or feed holes 52, 52 formed therein for cooperating with an as sociated feeding mechanism of the aforedescribed type.
- Each envelope 12a is substantially identical to the previous described envelope l2 and parts thereof which correspond to parts previously described bear the same reference numeral and a letter "a" suffix and will not be thereinafter further described.
- FIG. 5 A method for simultaneously making two assemblies of sefies-connected envelopes l, from an elongated web of sheet material or paper 30a is illustrated in FIG. 5.
- the envelopes which comprise the assemblies 10', 10' are in turn used in making the assembly 12a as illustrated in FIG. 6.
- a plurality of operations are simultaneously performed on the web 30a as it continuously advances in an automatic envelope making machine (not shown).
- FIG. 5 A preferred sequence of operation will be evident from FIG. 5 as viewed from left to right or in the direction of advance as indicated by the arrow thereof.
- each marginal portion 32a is folded inwardly or toward the other along a longitudinally extending fold or score line a.
- the width of the web 30a is substantially greater than the combined width of the two marginal portions 32a, 32a so that an intermediate portion of the web indicated at 36a is exposed between the free side edges of the two-folded marginal portions.
- each marginal portion 32a is joined to its associated underlying portion of the web along longitudinally spaced and generally transversely extending lines of attachment defined by lines of adhesive 22a, 22a.
- lines of adhesive 22a, 22a differs somewhat from the arrangement of the corresponding lines 22, 22 shown in FIG. 3. More specifically, the lines 220, 22a are arranged in longitudinal sets, each set being separated from the next successive one by a connecting portion of the web indicated at 54.
- each group comprises a plurality of sets of envelope bodies separated from each other by connecting portions 54, 54.
- Each set in turn comprises a plurality of individual envelope bodies joined together in end-to-end relation.
- Lines of weakening 14a, 14a, which, as shown, are formed on the web before it is folded, define the end portions of each envelope body.
- the sets which ultimately comprise one group or assembly 10' are longitudinally offset with respect to the sets comprising the other or opposite group.
- the sets are longitudinally offset with respect to each other a distance substantially equal to one-half the longitudinal dimension of an envelope body.
- Adhesive for sealing the envelope flaps 24a, 24a is preferably applied-to the intermediate portion 36a when the strips of adhesive 22a, 22a are applied to the web.
- a longitudinal series of strips of adhesive 37a, 37a is applied to the intermediate portion 36a and forms an interrupted patter thereon.
- Each line of adhesive 370 forms a generally longitudinally extending zigzag pattern traversing the intermediate portion 36a.
- the two groups of envelope assemblies 10', 10' are separated from each other and the envelope closing a. 24a, 24a are simultaneously shaped by cutting the web 30a along its intermediate portion 36a.
- the assemblies 10', 10' are separated and the flaps shaped by alternately cutting the intermediate portion 360 along parting lines 380, 38a and cutting portions 56, 56 from the web.
- Each cutout portion 56 extends from a connecting portion 54 on one side of the folded web to the next successive connecting portion 54 on the opposite side thereof.
- Each parting line 38a extends along an associated line of adhesive 37a.
- the two groups of series-connected envelopes are separated from each other while a plurality of triangular-shaped closing flaps 24a, 24:: are simultaneously formed, each closing flap carrying a chevron-shaped strip of adhesive 28a.
- the envelope sets 46, 46 in each group 10' are separated from each other by cutting the web 30a along lines of separation 58, 58 which extend tranversely of the connecting portions 54, 54 so that the connecting strips 48, 48 are formed. The latter cutting operation is preferably performed when the intermediate portion 360 is cut.
- each successive envelope set 46 is separated from the advancing web 30a, it is moved away from the web and in a direction transverse to the direction of web advance by an appropriate conveying means (not shown).
- the envelope sets 46, 46 which comprise one group 10 move away from the web in one direction whereas the envelope sets 46, 46 of the other group 10' move away from the web in the opposite direction.
- each envelope set 24 moves away from the web, it engages a portion of the conveying means which initially increases its speed of transverse movement causing it to move to closely spaced relation with the set which precedes it so that the flaps 24a, 24a of each envelope set 46 are brought into overlying relation with respectively associated portions of the back panels 18a, 18a of the preceding set.
- the envelope sets 46, 46 of each group are arranged in series with the connecting strips 48, 48 thereof generally aligned.
- Each assembly 10a is completed by attaching a carrier strip 50 to the aligned connecting strips 48, 48 at each end of the envelope sets 46, 46 as the sets are advanced and as shown in FIG. 4.
- a method for making continuous form envelope assemblies from an elongated web of sheet material comprising the steps of advancing said web in a longitudinal direction, folding one longitudinally extending marginal portion of said advancing web inwardly along one longitudinally extending fold line and into face-to-face relation with an associated underlying portion of said web, simultaneously folding the other longitudinally extending marginal portion of said web inwardly along another longitudinally extending fold line and into face-toface relation with another underlying portion of said web leaving a longitudinally extending intermediate portion of said web exposed between the longitudinally extending free edges of said marginal portions, joining said one marginal portion of said advancing web to its associated underlying portion along one longitudinal series of sets of longitudinally spaced and generally transversely extending lines of attachment, each set in said one series longitudinally spaced from the next successive set in said one series, said one marginal portion and its associated underlying portion cooperating to define one group of envelope bodies comprising one longitudinal series of sets of envelope bodies, each set of envelope bodies comprising said one group including at least one envelope body and separated from the next successive set of envelope bodies
- a method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the additional step of imprinting at least one line on each said marginal portions as said web advances to define a plurality of simulated envelope bottom panels, each of said simulated bottom panels being respectively associated with one of said envelope bodies.
- a method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of applying two transversely spaced apart sets of longitudinally spaced and generally transversely extending lines of adhesive to said web to define said lines of attachment before the step of folding said one and said other marginal portions and wherein the step of joining each of said marginal portions is further characterized as joining each of said marginal portions to its associated underlying portion by one of said sets of lines of adhesive.
- a method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of forming a longitudinally spaced series of lines of weakening extending generally transversely of at least each of said marginal portions and the respectively associated underlying portions of said web to define the end portions of each of said envelope bodies and along which each of said envelopes may be separated from the other and from the connecting portions after said intermediate portion has been cut.
- a method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of applying adhesive to said intermediate portion.
- a method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the additional steps of cutting said web along the connecting portions to separate each of said sets from the other and to define connecting strips at the opposite ends of each of said sets, each of said connecting strips being defined by a part of an associated connecting portion, arranging said generally aligned, and attaching a pair of spaced carrier strips to said connecting strips to form an assembly of series-connected envelope sets.
- a method for making envelope assemblies as set forth in claim 8 including the additional step of initially increasing the speed of transverse movement of each of said sets as its moves away from said web to cause each successive set to move into closely spaced relation with the set preceding it, said step of increasing the speed of transverse movement to be performed before the step of attaching said carrier strips.
- a method for making envelope assemblies as set forth in claim 9 wherein the step of increasing the speed of transverse movement is further characterized as increasing the speed of transverse movement to cause each successive set to move into closely spaced relation with the set which precedes it so that each successive set partially overlies a preceding set.
- a method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of positioning one longitudinal series of longitudinally spaced inserts on said web and disposed to one side of said intermediate portion, each of said inserts overlying an associated portion of said one fold line and positioning another longitudinal series of longitudinally spaced apart inserts on said web and disposed to the other side of said intermediate portion, each of said other inserts overlying an associated portion of said other fold line and wherein the step of folding said marginal portions is further characterized as simultaneously folding said one marginal portion and said one series of inserts along said one fold line and said other marginal portion and said other set of inserts along said other fold lines.
Landscapes
- Making Paper Articles (AREA)
Abstract
Two assemblies of continuous form or series-connected envelopes are simultaneously made by advancing an elongated web of sheet material in a longitudinal direction, folding opposite marginal portions of the advancing web inwardly toward each other, joining each marginal portion in face-to-face relation to an associated underlying portion of the web along longitudinally spaced generally transversely extending lines of attachment to form two assemblies of envelope bodies connected together by an exposed intermediate portion of the web, and cutting the advancing web along its intermediate portion to simultaneously form closing flaps for the envelopes comprising each of the assemblies and to separate the two assemblies from each other. In accordance with a further method of the invention the envelopes of each assembly are further separated into sets, each set including a plurality of envelopes joined together in end-to-end relation and having connecting strips at the opposite ends thereof. The sets are arranged with the connecting strips thereof longitudinally aligned and are joined together in series-connected relation by attaching a pair of spaced carrier strips to the connecting strips.
Description
United States Patent Allison et al 93/6] Primary Examiner -Bernard Stickney Attorney-McCormick, Paulding and Huber ABSTRACT: Two assemblies of continuous form or seriesconnected envelopes are simultaneously made by advancing an elongated web of sheet material in a longitudinal direction, folding opposite marginal portions of the advancing web inwardly toward each other, joining each marginal portion in face-to-face relation to an associated underlying portion of the web along longitudinally spaced generally transversely extending lines of attachment to form two assemblies of envelope bodies connected together by an exposed intermediate por tion of the web, and cutting the advancing web along its intermediate portion to simultaneously form closing flaps for the envelopes comprising each of the assemblies and to separate the two assemblies from each other. In accordance with a further method of the invention the envelopes of each assembly are further separated into sets, each set including a plurality of envelopes joined together in end-to-end relation and having connecting strips at the opposite ends thereof. The sets are arranged with the connecting strips thereof longitudinally aligned and are joined together in series-connected relation by attaching a pair of spaced carrier strips to the connecting strips.
Patented Dec. 14, 1971 3,626,823
3 SheetsSheet 1 Patented Dec. 14, 1971 3 Sheets-Sheet 2 omw Patented Dec. 14, 1971 3,626fi2i 3 Sheets-Sheet 3 FIG. 6
METHOD FOR MAKING CONTINUOUS FORM ENVELOPES BACKGROUND OF THE INVENTION This invention relates in general to continuous form envelopes and deals more particularly with improved continuous form envelope structure and methods for making same.
SUMMARY OF THE INVENTION In accordance with the present invention continuous form envelopes are made by folding and joining portions of an advancing web of sheet material to simultaneously form two groups of series-connected envelope bodies and cutting the advancing web to simultaneously shape the envelope closing flaps and separate the envelope assemblies from each other. The envelopes comprising each assembly are further separated into sets, each set including a plurality of joined together in end-to-end relation. The sets are joined together in series-connected relation by applying spaced carrier strips thereto.
BRIEF DESCRIPTION OF THE DRAWINGS FIG. 1 is a fragmentary plan view of an envelope assembly made in accordance with the present invention.
FIG. 2 is a sectional view taken along the line 2-2 of FIG. 1.
FIG. 3 is a somewhat reduced plan view of a web of sheet material from which the envelope assembly of FIG. I is made and shows, from left to right, successive changes in the material as two envelope assemblies are simultaneously formed therefrom.
FIG. 4 is a fragmentary plan view of another envelope assembly made in accordance with the invention.
FIG. 5 is a generally similar to FIG. 3 but illustrates another method for simultaneously making two assemblies of seriesconnected envelopes.
FIG. 6 is a fragmentary continuation of FIG. 5.
DETAILED DESCRIPTION OF THE PREFERRED EMBODIMENTS Turning now to the drawings and referring first particularly to FIGS. 1 and 2, a typical assembly of continuous form or series-connected envelopes made in accordance with a method of the present invention and indicated generally at 10 comprises a group of individual seamless envelopes l2, 12 connected together in end-to-end relation along lines of perforation or weakening I4, 14. Each envelope has a body defining a pocket and formed by a front panel 16 and a rear panel 18 connected to the lower edge of the front panel along a longitudinally extending fold line 20. The panels 16 and 18 are joined together in face-to-face relation near the lines of weakening I4, 14 which define the opposite ends thereof by lines of attachment defined by strips of adhesive 22, 22.
The rear panel 18 has a line 23 imprinted thereon to simulate an envelope bottom panel of conventional folded type. Each envelope 12 also includes a triangular closing flap 24 connected to the upper edge of the front panel 16 along another longitudinally extending fold line 26. A chevronshaped line of adhesive 28 which may, for example, be of a remoistenable or pressure sensitive type is carried by the closing flap 24 for sealing the flap in engagement with the rear panel 18 to provide a closure for the mouth of the envelope.
A two-up method for simultaneously making two assemblies of series-connected envelopes l0, 10 from an advancing elongated web of sheet material or paper 30 is illustrated in FIG. 3. The illustrated method is particularly adapted to be practiced with a conventional automatic envelope making machine of the type capable of continuously advancing the web at high speed through a plurality of work stations where a variety of operations are performed thereon, as, for example, scoring, folding, gumming, cutting and imprinting messages or designs. However, for clarity of illustration, the machine is not shown.
The sequence of operations may vary and will, of course, depend upon the arrangement of the various work stations and the order in which these stations are encountered by the advancing web. A preferred sequence of operations is illustrated and will be evident from consideration of the web 30 as viewed from left to right in FIG. 3 or in the direction of web advance as indicated by the arrow.
Further considering FIG. 3, the parallel score or fold lines 20, 20 and 26, 26 are formed on the advancing web and separate marginal portions 32, 32 from a central portion 34 thereof. Each marginal portion 32 is folded inwardly or toward the other marginal portion and along a respectively associated fold line 20 to over lie the central portion 34. The bodies of the envelopes 12, 12 are formed by connecting each marginal portion 32 in face-to-face relation to an associated underlying part of the central portion 34 by the lines of adhesive 22, 22 which, as shown, are applied to each marginal portion before it is folded. Moist adhesive is preferably used and for this reason each line of adhesive 22 is spaced from its respectively associated fold line 20 by a small margin sufficient to accommodate a folding bar of a conventional envelope making machine without danger of the folding bar smearing the adhesive. At this point, it should be noted that the lines of adhesive 22, 22 applied to one marginal portion 32 are longitudinally offset with respect to the lines of adhesive 22, 22 applied to the opposite marginal portion. Thus, two assemblies or groups of envelope bodies are formed at opposite sides of the folded web, the envelope bodies in one group being longitudinally offset with respect to the envelope bodies in the other group. Preferably and as shown, the two groups of envelope bodies are longitudinally offset with respect to each other a distance substantially equal to one-half the longitudinal dimension of an envelope body 12. Each group of envelope bodies is connected to the other by an intermediate portion of the web indicated at 36 and exposed between the longitudinally extending free or inner edges of the marginal portions 32, 32. Each marginal portion 32 forms the front panels l6, 16 of an associated group of envelope bodies, the back panels l8, 18 thereof being formed by an associated underlying part of the web central portion 34. In accordance with the illustrated method the lines 23, 23 are imprinted on the lower surface of the web 30 before it is folded.
Adhesive for sealing the envelope closing flaps is preferably applied to the intermediate portion 36 when the lines of adhesive 22, 22 are applied to the web. The flap adhesive may be applied in various continuous or interrupted patterns and may, if desired, cover the entire intermediate portion 36. In the illustrated case, a line of adhesive 37 is applied in a zigzag pattern to the intermediate portion 36 and extends in a generally longitudinal direction alternately traversing the intennediate portion in one and an opposite direction.
The various lines of weakening 14, 14 are preferably formed on the folded web after the envelope bodies are formed. Each line of weakening 14 extends inwardly from an associated fold line 20 and terminates at or near a respectively associated one of the fold lines 26, 26. The various lines of weakening 14, 14 define the end portions of the envelope 12, 12, consequently, the line of weakening associated with one group of envelope bodies are longitudinally offset with respect to the lines of weakening on the opposite group of envelop bodies.
In accordance with the present invention, the advancing web is cut to form the envelope closing flaps and simultaneously separate the two groups of series-connected envelopes from each other. In the illustrated case, the two envelope assemblies l0, 10 are separated from each other by cutting the advancing web along a parting line 38 which alternately traverses the intermediate portion 36 and forms an alternate series of junctures with the lines of weakening 14, 14 near the fold lines 26, 26. In the illustrated case the parting cut is made along the line of adhesive 37. Thus, a plurality of substantially identical triangular- shaped envelope flaps 24, 24 are formed as the two envelope assemblies are separated, each flap being connected to an associated envelope panel 16 and carrying a chevron-shaped line of adhesive 28. The individual envelopes l2, 12 which comprise each group or assembly 10 may be further separated from each other along the various lines of weakening l4, l4.
The envelope assemblies l0, 10 may, if desired, be formed with inserts therein, a typical insert being indicated at 40, 40 in FIG. 3. Each insert 40 is positioned on the web 30 before the marginal portions 32, 32 are folded inwardly. One or more spots of release-type adhesive such as indicated at 42, 42 may be employed if desired, to retain each insert in proper position while an associated envelope 12 is formed therearound. Each envelope 12 may also be provided with a window formed therein, such as indicated at 44, so that material printed on an associated insert 40 before assembly will be visible therethrough. The window also facilitates imprinting on the latter inserts at some later time.
Another assembly of series-connected envelopes made in accordance with another method of the present invention and particularly adapted to be advanced by a positive feed mechanism, such as a pinwheel feed device (not shown), is indicated generally at 10a in F IG. 4. The envelope assembly 100 generally comprises a plurality of envelope sets 46, 46 joined together in longitudinal series. Each envelope set 46 includes tow or more envelopes 12a, 12a connected together in end-toend relation and has connecting strips 48, 48 extending outwardly from its opposite ends. The envelopes 12a, 120 are separated from each other and from the connecting strips 48, 48 by lines of weakening 14a, 14a. The sets 46, 46 are retained in series-connected relation by the carrier strips 50, 50 adhesively attached to the connecting strips 48, 48. Each carrier strip has a longitudinally spaced series of configurations or feed holes 52, 52 formed therein for cooperating with an as sociated feeding mechanism of the aforedescribed type. Each envelope 12a is substantially identical to the previous described envelope l2 and parts thereof which correspond to parts previously described bear the same reference numeral and a letter "a" suffix and will not be thereinafter further described.
A method for simultaneously making two assemblies of sefies-connected envelopes l, from an elongated web of sheet material or paper 30a is illustrated in FIG. 5. The envelopes which comprise the assemblies 10', 10' are in turn used in making the assembly 12a as illustrated in FIG. 6. As in the previously described method, a plurality of operations are simultaneously performed on the web 30a as it continuously advances in an automatic envelope making machine (not shown). A preferred sequence of operation will be evident from FIG. 5 as viewed from left to right or in the direction of advance as indicated by the arrow thereof.
As the web advances, each marginal portion 32a is folded inwardly or toward the other along a longitudinally extending fold or score line a. The width of the web 30a is substantially greater than the combined width of the two marginal portions 32a, 32a so that an intermediate portion of the web indicated at 36a is exposed between the free side edges of the two-folded marginal portions. As in the previously described method, each marginal portion 32a is joined to its associated underlying portion of the web along longitudinally spaced and generally transversely extending lines of attachment defined by lines of adhesive 22a, 22a. It will be noted, however, that the arrangement of the lines of adhesive 22a, 22a differs somewhat from the arrangement of the corresponding lines 22, 22 shown in FIG. 3. More specifically, the lines 220, 22a are arranged in longitudinal sets, each set being separated from the next successive one by a connecting portion of the web indicated at 54.
When the marginal portions 32a, 32a are connected to the web central portion 340, two groups of series-connected envelope bodies are formed at opposite sides of the folded web and are connected together by the intermediate portion 36a. Each group comprises a plurality of sets of envelope bodies separated from each other by connecting portions 54, 54. Each set in turn comprises a plurality of individual envelope bodies joined together in end-to-end relation. Lines of weakening 14a, 14a, which, as shown, are formed on the web before it is folded, define the end portions of each envelope body. At this point, it should be noted that the sets which ultimately comprise one group or assembly 10' are longitudinally offset with respect to the sets comprising the other or opposite group. Preferably, and as shown, the sets are longitudinally offset with respect to each other a distance substantially equal to one-half the longitudinal dimension of an envelope body.
Adhesive for sealing the envelope flaps 24a, 24a is preferably applied-to the intermediate portion 36a when the strips of adhesive 22a, 22a are applied to the web. A longitudinal series of strips of adhesive 37a, 37a is applied to the intermediate portion 36a and forms an interrupted patter thereon. Each line of adhesive 370 forms a generally longitudinally extending zigzag pattern traversing the intermediate portion 36a.
The two groups of envelope assemblies 10', 10' are separated from each other and the envelope closing a. 24a, 24a are simultaneously shaped by cutting the web 30a along its intermediate portion 36a. In the illustrated case, the assemblies 10', 10' are separated and the flaps shaped by alternately cutting the intermediate portion 360 along parting lines 380, 38a and cutting portions 56, 56 from the web. Each cutout portion 56 extends from a connecting portion 54 on one side of the folded web to the next successive connecting portion 54 on the opposite side thereof. Each parting line 38a extends along an associated line of adhesive 37a. Thus, the two groups of series-connected envelopes are separated from each other while a plurality of triangular-shaped closing flaps 24a, 24:: are simultaneously formed, each closing flap carrying a chevron-shaped strip of adhesive 28a. The envelope sets 46, 46 in each group 10' are separated from each other by cutting the web 30a along lines of separation 58, 58 which extend tranversely of the connecting portions 54, 54 so that the connecting strips 48, 48 are formed. The latter cutting operation is preferably performed when the intermediate portion 360 is cut.
Referring now to FIG. 6, as each successive envelope set 46 is separated from the advancing web 30a, it is moved away from the web and in a direction transverse to the direction of web advance by an appropriate conveying means (not shown). The envelope sets 46, 46 which comprise one group 10 move away from the web in one direction whereas the envelope sets 46, 46 of the other group 10' move away from the web in the opposite direction. As each envelope set 24 moves away from the web, it engages a portion of the conveying means which initially increases its speed of transverse movement causing it to move to closely spaced relation with the set which precedes it so that the flaps 24a, 24a of each envelope set 46 are brought into overlying relation with respectively associated portions of the back panels 18a, 18a of the preceding set.'Thus, the envelope sets 46, 46 of each group are arranged in series with the connecting strips 48, 48 thereof generally aligned. Each assembly 10a is completed by attaching a carrier strip 50 to the aligned connecting strips 48, 48 at each end of the envelope sets 46, 46 as the sets are advanced and as shown in FIG. 4.
I claim:
1. A method for making continuous form envelope assemblies from an elongated web of sheet material comprising the steps of advancing said web in a longitudinal direction, folding one longitudinally extending marginal portion of said advancing web inwardly along one longitudinally extending fold line and into face-to-face relation with an associated underlying portion of said web, simultaneously folding the other longitudinally extending marginal portion of said web inwardly along another longitudinally extending fold line and into face-toface relation with another underlying portion of said web leaving a longitudinally extending intermediate portion of said web exposed between the longitudinally extending free edges of said marginal portions, joining said one marginal portion of said advancing web to its associated underlying portion along one longitudinal series of sets of longitudinally spaced and generally transversely extending lines of attachment, each set in said one series longitudinally spaced from the next successive set in said one series, said one marginal portion and its associated underlying portion cooperating to define one group of envelope bodies comprising one longitudinal series of sets of envelope bodies, each set of envelope bodies comprising said one group including at least one envelope body and separated from the next successive set of envelope bodies in said one group by a connecting portion, joining said other marginal portion of said advancing web to its associated underlying portion along another longitudinal series of sets of longitudinally spaced and generally transversely extending lines of attachment, each set in said other series longitudinally spaced from the next successive set in said other series, said other marginal portion and its underlying marginal portion cooperating to define another group of envelope bodies comprising another longitudinal series of sets of envelope bodies, each set of envelope bodies comprising said other group including at least one envelope body and separated from the next successive set of envelope bodies in said other group by a connecting portion, each of said envelope bodies defining a pocket having a longitudinally extending mouth, said sets of envelope bodies comprising said one group being longitudinally offset with respect to said sets of envelope bodies comprising said other group, and alternately cutting said intermediate portion along a parting line extending in a generally longitudinal direction and cutting a portion therefrom as said web advances to separate the sets of envelope bodies comprising said one group from the sets of envelope bodies comprising said other group and simultaneously shape a plurality of envelope closing flaps, each of said flaps being attached to a respectively associated one of said envelope bodies.
2. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the additional step of imprinting at least one line on each said marginal portions as said web advances to define a plurality of simulated envelope bottom panels, each of said simulated bottom panels being respectively associated with one of said envelope bodies.
3. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of applying two transversely spaced apart sets of longitudinally spaced and generally transversely extending lines of adhesive to said web to define said lines of attachment before the step of folding said one and said other marginal portions and wherein the step of joining each of said marginal portions is further characterized as joining each of said marginal portions to its associated underlying portion by one of said sets of lines of adhesive.
4. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of forming a longitudinally spaced series of lines of weakening extending generally transversely of at least each of said marginal portions and the respectively associated underlying portions of said web to define the end portions of each of said envelope bodies and along which each of said envelopes may be separated from the other and from the connecting portions after said intermediate portion has been cut.
5. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of applying adhesive to said intermediate portion.
6. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 5 wherein the step of applying adhesive is further characterized as applying a continuous line of adhesive to said intermediate portion and the step of cutting said intermediate portion along said parting line is further characterized as cutting said intermediate portion along said line of adhesive.
7. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the additional steps of cutting said web along the connecting portions to separate each of said sets from the other and to define connecting strips at the opposite ends of each of said sets, each of said connecting strips being defined by a part of an associated connecting portion, arranging said generally aligned, and attaching a pair of spaced carrier strips to said connecting strips to form an assembly of series-connected envelope sets.
8. A method for making envelope assemblies from an elongated web os sheet material as set forth in claim 7 wherein the step of separating each of said sets is further characterized as successively separating each of the sets in said one group from the other sets in said one group and successively separating each of the sets in said other group from the other sets in said other group and wherein the step of arranging said sets is further characterized as successively moving each of the sets in said one and said other groups in generally opposite transverse direction and away from said web as said sets are successively separated.
9. A method for making envelope assemblies as set forth in claim 8 including the additional step of initially increasing the speed of transverse movement of each of said sets as its moves away from said web to cause each successive set to move into closely spaced relation with the set preceding it, said step of increasing the speed of transverse movement to be performed before the step of attaching said carrier strips.
10. A method for making envelope assemblies as set forth in claim 9 wherein the step of increasing the speed of transverse movement is further characterized as increasing the speed of transverse movement to cause each successive set to move into closely spaced relation with the set which precedes it so that each successive set partially overlies a preceding set.
11. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 wherein the step of joining each of said marginal portions to its associated underlying portion is further characterized as applying one longitudinal series of lines of moist adhesive to a portion of said web disposed to one side of said intermediate portions and spaced from said one fold line and applying another longitudinal series of transversely extending lines of moist adhesive to another portion of said web disposed to the other side of said intermediate portion and spaced from said other fold line and joining said marginal portions to said underlying portions by said moist adhesive when said marginal portions are folded.
12. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of positioning one longitudinal series of longitudinally spaced inserts on said web and disposed to one side of said intermediate portion, each of said inserts overlying an associated portion of said one fold line and positioning another longitudinal series of longitudinally spaced apart inserts on said web and disposed to the other side of said intermediate portion, each of said other inserts overlying an associated portion of said other fold line and wherein the step of folding said marginal portions is further characterized as simultaneously folding said one marginal portion and said one series of inserts along said one fold line and said other marginal portion and said other set of inserts along said other fold lines.
t t IF 8' *zggg UNITED STATES PATENT OFFICE CERTIFICATE @F CURREQTEQN Patent No. 3,626,821 Dated December 14, 1971 Inventor(s) Wilfred H. Gendron It is certified that error appears in the above-identified patent and that said Letters Patent are hereby corrected as shown below:
Col. 1, line 18, after "of" insert --envel0pes-- C01. 1, line 36, after "is" delete "a". Col. 2, line 13, "over lie" should read --overlie- Col. 2, line 60, "line" should read,--lines--.
Col. 3; line 2 1, "tow" should read --'-two--.
Col. 4; line 19; after "closing" delete "a" and insert --f1aps Claim 7, line 10, after "said" insert --sets in series with said connecting strips--.
Claim 8, line 15, after "Web" "0s" should read --of--.
Signed and sealed this th day of July 1972.
(SEAL) Attest:
EDE'IARD I-I.FLETCHER, JR. ROBERT GOITSCHALK Attesting Officer Commissionerof Patents
Claims (12)
1. A method for making continuous form envelope assemblies from an elongated web of sheet material comprising the steps of advancing said web in a longitudinal direction, folding one longitudinally extending marginal portion of said advancing web inwardly along one longitudinally extending fold line and into face-to-face relation with an associated underlying portion of said web, simultaneously folding the other longitudinally extending marginal portion of said web inwardly along another longitudinally extending fold line and into face-to-face relation with another underlying portion of said web leaving a longitudinally extending intermediate portion of said web exposed between the longitudinally extending free edges of said marginal portions, joining said one marginal portion of said advancing web to its associated underlying portion along one longitudinal series of sets of longitudinally spaced and generally transversely extending lines of attachment, each set in said one series longitudinally spaced from the next successive set in said one series, said one marginal portion and its associated underlying portion cooperating to define one group of envelope bodies comprising one longitudinal series of sets of envelope bodies, each set of envelope bodies comprising said one group including at least one envelope body and separated from the next successive set of envelope bodies in said one group by a connecting portion, joining said other marginal portion of said advancing web to its associated underlying portion along another longitudinal series of sets of longitudinally spaced and generally transversely extending lines of attachment, each set in said other series longitudinally spaced from the next successive set in said other series, said other marginal portion and its underlying marginal portion cooperating to define another group of envelope bodies comprising another longitudinal series of sets of envelope bodies, each set of envelope bodies comprising said other group including at least one envelope body and separated from the next successive set of envelope bodies in said other group by a connecting portion, each of said envelope bodies defining a pocket having a longitudinally extending mouth, said sets of envelope bodies comprising said one grOup being longitudinally offset with respect to said sets of envelope bodies comprising said other group, and alternately cutting said intermediate portion along a parting line extending in a generally longitudinal direction and cutting a portion therefrom as said web advances to separate the sets of envelope bodies comprising said one group from the sets of envelope bodies comprising said other group and simultaneously shape a plurality of envelope closing flaps, each of said flaps being attached to a respectively associated one of said envelope bodies.
2. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the additional step of imprinting at least one line on each said marginal portions as said web advances to define a plurality of simulated envelope bottom panels, each of said simulated bottom panels being respectively associated with one of said envelope bodies.
3. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of applying two transversely spaced apart sets of longitudinally spaced and generally transversely extending lines of adhesive to said web to define said lines of attachment before the step of folding said one and said other marginal portions and wherein the step of joining each of said marginal portions is further characterized as joining each of said marginal portions to its associated underlying portion by one of said sets of lines of adhesive.
4. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of forming a longitudinally spaced series of lines of weakening extending generally transversely of at least each of said marginal portions and the respectively associated underlying portions of said web to define the end portions of each of said envelope bodies and along which each of said envelopes may be separated from the other and from the connecting portions after said intermediate portion has been cut.
5. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of applying adhesive to said intermediate portion.
6. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 5 wherein the step of applying adhesive is further characterized as applying a continuous line of adhesive to said intermediate portion and the step of cutting said intermediate portion along said parting line is further characterized as cutting said intermediate portion along said line of adhesive.
7. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the additional steps of cutting said web along the connecting portions to separate each of said sets from the other and to define connecting strips at the opposite ends of each of said sets, each of said connecting strips being defined by a part of an associated connecting portion, arranging said generally aligned, and attaching a pair of spaced carrier strips to said connecting strips to form an assembly of series-connected envelope sets.
8. A method for making envelope assemblies from an elongated web os sheet material as set forth in claim 7 wherein the step of separating each of said sets is further characterized as successively separating each of the sets in said one group from the other sets in said one group and successively separating each of the sets in said other group from the other sets in said other group and wherein the step of arranging said sets is further characterized as successively moving each of the sets in said one and said other groups in generally opposite transverse direction and away from said web as said sets are successively separated.
9. A method for making envelope assemblies as set forth in claim 8 including the additional step of initially increasing the speed of transverse movement of each of said seTs as its moves away from said web to cause each successive set to move into closely spaced relation with the set preceding it, said step of increasing the speed of transverse movement to be performed before the step of attaching said carrier strips.
10. A method for making envelope assemblies as set forth in claim 9 wherein the step of increasing the speed of transverse movement is further characterized as increasing the speed of transverse movement to cause each successive set to move into closely spaced relation with the set which precedes it so that each successive set partially overlies a preceding set.
11. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 wherein the step of joining each of said marginal portions to its associated underlying portion is further characterized as applying one longitudinal series of lines of moist adhesive to a portion of said web disposed to one side of said intermediate portions and spaced from said one fold line and applying another longitudinal series of transversely extending lines of moist adhesive to another portion of said web disposed to the other side of said intermediate portion and spaced from said other fold line and joining said marginal portions to said underlying portions by said moist adhesive when said marginal portions are folded.
12. A method for making envelope assemblies from an elongated web of sheet material as set forth in claim 1 including the step of positioning one longitudinal series of longitudinally spaced inserts on said web and disposed to one side of said intermediate portion, each of said inserts overlying an associated portion of said one fold line and positioning another longitudinal series of longitudinally spaced apart inserts on said web and disposed to the other side of said intermediate portion, each of said other inserts overlying an associated portion of said other fold line and wherein the step of folding said marginal portions is further characterized as simultaneously folding said one marginal portion and said one series of inserts along said one fold line and said other marginal portion and said other set of inserts along said other fold lines.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US87528969A | 1969-11-10 | 1969-11-10 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| US3626821A true US3626821A (en) | 1971-12-14 |
Family
ID=25365530
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US875289A Expired - Lifetime US3626821A (en) | 1969-11-10 | 1969-11-10 | Method for making continuous form envelopes |
Country Status (1)
| Country | Link |
|---|---|
| US (1) | US3626821A (en) |
Cited By (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3956049A (en) * | 1974-01-15 | 1976-05-11 | Johnsen Edward L | Continuous business form or the like adapted for subsequent processing into original indicia bearing lottery tickets, envelopes or the like |
| US3982473A (en) * | 1975-06-26 | 1976-09-28 | American Paper Products Company | Envelope-making method |
| US4063398A (en) * | 1974-05-13 | 1977-12-20 | Huffman Harold W | Multi-panel envelope form and method of producing same |
| US4071997A (en) * | 1976-04-27 | 1978-02-07 | Gunther Business Systems, Inc. | Mechanism and method of making an envelope |
| US4343129A (en) * | 1976-04-27 | 1982-08-10 | G.B.R., Ltd. | Mechanism of making an envelope |
| US4630310A (en) * | 1985-03-01 | 1986-12-16 | Winesett Franklin P | Off-set means for removing bags from connected plural rows |
| WO1988005410A1 (en) * | 1987-01-20 | 1988-07-28 | Avery International Corporation | Dual envelope sheet-fed assembly |
| US4915288A (en) * | 1989-04-27 | 1990-04-10 | Avery International Corporation | Envelope with single peel-off backing sheet to facilitate printing and copying |
| US4948028A (en) * | 1989-02-03 | 1990-08-14 | Avery International Corporation | Variable size envelope with single closure flap |
| US5904030A (en) * | 1994-09-05 | 1999-05-18 | Kavanagh; Conor | Process for making an envelope assembly with folded insert |
| US5971260A (en) * | 1995-03-06 | 1999-10-26 | Mertens; Luc | Continuous strip of detachably interconnected folded products |
| US20040016210A1 (en) * | 1996-03-06 | 2004-01-29 | Luc Mertens | Continuous strip of detachably interconnected folded products |
| US20130042444A1 (en) * | 2010-03-03 | 2013-02-21 | Evologics Gmbh | Release apparatus for a load on a device and underwater device |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US302690A (en) * | 1884-07-29 | stocking- | ||
| US2224513A (en) * | 1937-12-15 | 1940-12-10 | Maria Majen Lindgren | Method of making envelopes without side flaps |
| US3263904A (en) * | 1961-11-17 | 1966-08-02 | Flex O Glass Inc | Tear-off bag supply |
| US3327927A (en) * | 1965-04-01 | 1967-06-27 | Robert D Allison | Continuous envelope assembly |
-
1969
- 1969-11-10 US US875289A patent/US3626821A/en not_active Expired - Lifetime
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US302690A (en) * | 1884-07-29 | stocking- | ||
| US2224513A (en) * | 1937-12-15 | 1940-12-10 | Maria Majen Lindgren | Method of making envelopes without side flaps |
| US3263904A (en) * | 1961-11-17 | 1966-08-02 | Flex O Glass Inc | Tear-off bag supply |
| US3327927A (en) * | 1965-04-01 | 1967-06-27 | Robert D Allison | Continuous envelope assembly |
Cited By (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3956049A (en) * | 1974-01-15 | 1976-05-11 | Johnsen Edward L | Continuous business form or the like adapted for subsequent processing into original indicia bearing lottery tickets, envelopes or the like |
| US4063398A (en) * | 1974-05-13 | 1977-12-20 | Huffman Harold W | Multi-panel envelope form and method of producing same |
| US3982473A (en) * | 1975-06-26 | 1976-09-28 | American Paper Products Company | Envelope-making method |
| US4071997A (en) * | 1976-04-27 | 1978-02-07 | Gunther Business Systems, Inc. | Mechanism and method of making an envelope |
| US4343129A (en) * | 1976-04-27 | 1982-08-10 | G.B.R., Ltd. | Mechanism of making an envelope |
| US4630310A (en) * | 1985-03-01 | 1986-12-16 | Winesett Franklin P | Off-set means for removing bags from connected plural rows |
| WO1988005410A1 (en) * | 1987-01-20 | 1988-07-28 | Avery International Corporation | Dual envelope sheet-fed assembly |
| US4807805A (en) * | 1987-01-20 | 1989-02-28 | Avery International Corporation | Dual envelope sheet-fed assembly |
| US4948028A (en) * | 1989-02-03 | 1990-08-14 | Avery International Corporation | Variable size envelope with single closure flap |
| US4915288A (en) * | 1989-04-27 | 1990-04-10 | Avery International Corporation | Envelope with single peel-off backing sheet to facilitate printing and copying |
| US5904030A (en) * | 1994-09-05 | 1999-05-18 | Kavanagh; Conor | Process for making an envelope assembly with folded insert |
| US5971260A (en) * | 1995-03-06 | 1999-10-26 | Mertens; Luc | Continuous strip of detachably interconnected folded products |
| US20040016210A1 (en) * | 1996-03-06 | 2004-01-29 | Luc Mertens | Continuous strip of detachably interconnected folded products |
| US7100348B2 (en) | 1996-03-06 | 2006-09-05 | Megaspirea N.V. | Continuous strip of detachably interconnected folded products |
| US20060272295A1 (en) * | 1996-03-06 | 2006-12-07 | Luc Mertens | Continuous strip of detachably interconnected folded products |
| US7587881B2 (en) | 1996-03-06 | 2009-09-15 | Hersch Reich | Continuous strip of detachably interconnected folded products |
| US20130042444A1 (en) * | 2010-03-03 | 2013-02-21 | Evologics Gmbh | Release apparatus for a load on a device and underwater device |
| US9126662B2 (en) * | 2010-03-03 | 2015-09-08 | Evologics Gmbh | Release apparatus for a load on a device and underwater device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4063398A (en) | Multi-panel envelope form and method of producing same | |
| US3902655A (en) | Method of producing multi-panel mailing envelope forms in side-by-side interconnected series | |
| US3999746A (en) | Method of making a combined brochure and return envelope package | |
| US3554438A (en) | Correspondence assembly | |
| US3618284A (en) | Method for making envelope containing return envelope structure | |
| US3946938A (en) | Two piece mailer | |
| US2824685A (en) | Assembly of series-connected envelopes and method of making same | |
| US3743273A (en) | Continuous web forming of envelopes in pamphlets | |
| US3988971A (en) | Method of making envelope assembly | |
| US2722369A (en) | Series-connected envelopes and method of manufacturing | |
| CA1245243A (en) | Business mailer | |
| US3665817A (en) | Forming multiple page pamphlet | |
| US3482763A (en) | Continuous form envelopes with inserts | |
| US5221567A (en) | Packaging system | |
| US3593485A (en) | Method of forming envelopes having inserts therein from a moving blank web | |
| US5095682A (en) | Mailer and method and apparatus for making | |
| US3900159A (en) | Continuous form envelopes | |
| US3786984A (en) | Continuous strip envelopes | |
| US5064115A (en) | Mailer and method and apparatus for making | |
| US3790068A (en) | Continuous form envelope assembly | |
| US3733982A (en) | Machine for producing self-opening envelopes | |
| US3817445A (en) | Expandable mailing envelope assembly | |
| US3354798A (en) | Method of making envelopes | |
| US3339828A (en) | Individual envelope unit for use in tabulating and similar machines | |
| US3813028A (en) | Continuous web with separable segmented envelopes and order coupons |