WO1988006103A1 - Tissu tisse en mailles pour cadre d'impression - Google Patents
Tissu tisse en mailles pour cadre d'impression Download PDFInfo
- Publication number
- WO1988006103A1 WO1988006103A1 PCT/JP1987/000601 JP8700601W WO8806103A1 WO 1988006103 A1 WO1988006103 A1 WO 1988006103A1 JP 8700601 W JP8700601 W JP 8700601W WO 8806103 A1 WO8806103 A1 WO 8806103A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- mesh
- mesh fabric
- composite filament
- sheath
- fabric
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41N—PRINTING PLATES OR FOILS; MATERIALS FOR SURFACES USED IN PRINTING MACHINES FOR PRINTING, INKING, DAMPING, OR THE LIKE; PREPARING SUCH SURFACES FOR USE AND CONSERVING THEM
- B41N1/00—Printing plates or foils; Materials therefor
- B41N1/24—Stencils; Stencil materials; Carriers therefor
- B41N1/247—Meshes, gauzes, woven or similar screen materials; Preparation thereof, e.g. by plasma treatment
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41N—PRINTING PLATES OR FOILS; MATERIALS FOR SURFACES USED IN PRINTING MACHINES FOR PRINTING, INKING, DAMPING, OR THE LIKE; PREPARING SUCH SURFACES FOR USE AND CONSERVING THEM
- B41N1/00—Printing plates or foils; Materials therefor
- B41N1/24—Stencils; Stencil materials; Carriers therefor
-
- D—TEXTILES; PAPER
- D03—WEAVING
- D03D—WOVEN FABRICS; METHODS OF WEAVING; LOOMS
- D03D15/00—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used
- D03D15/20—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the material of the fibres or filaments constituting the yarns or threads
- D03D15/283—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the material of the fibres or filaments constituting the yarns or threads synthetic polymer-based, e.g. polyamide or polyester fibres
-
- D—TEXTILES; PAPER
- D03—WEAVING
- D03D—WOVEN FABRICS; METHODS OF WEAVING; LOOMS
- D03D15/00—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used
- D03D15/20—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the material of the fibres or filaments constituting the yarns or threads
- D03D15/292—Conjugate, i.e. bi- or multicomponent, fibres or filaments
-
- D—TEXTILES; PAPER
- D03—WEAVING
- D03D—WOVEN FABRICS; METHODS OF WEAVING; LOOMS
- D03D15/00—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used
- D03D15/30—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the structure of the fibres or filaments
- D03D15/37—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the structure of the fibres or filaments with specific cross-section or surface shape
-
- D—TEXTILES; PAPER
- D03—WEAVING
- D03D—WOVEN FABRICS; METHODS OF WEAVING; LOOMS
- D03D15/00—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used
- D03D15/50—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the properties of the yarns or threads
- D03D15/547—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the properties of the yarns or threads with optical functions other than colour, e.g. comprising light-emitting fibres
-
- D—TEXTILES; PAPER
- D03—WEAVING
- D03D—WOVEN FABRICS; METHODS OF WEAVING; LOOMS
- D03D15/00—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used
- D03D15/50—Woven fabrics characterised by the material, structure or properties of the fibres, filaments, yarns, threads or other warp or weft elements used characterised by the properties of the yarns or threads
- D03D15/573—Tensile strength
-
- D—TEXTILES; PAPER
- D03—WEAVING
- D03D—WOVEN FABRICS; METHODS OF WEAVING; LOOMS
- D03D9/00—Open-work fabrics
-
- D—TEXTILES; PAPER
- D10—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B2321/00—Fibres made from polymers obtained by reactions only involving carbon-to-carbon unsaturated bonds
- D10B2321/02—Fibres made from polymers obtained by reactions only involving carbon-to-carbon unsaturated bonds polyolefins
-
- D—TEXTILES; PAPER
- D10—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B2331/00—Fibres made from polymers obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds, e.g. polycondensation products
- D10B2331/02—Fibres made from polymers obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds, e.g. polycondensation products polyamides
- D10B2331/021—Fibres made from polymers obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds, e.g. polycondensation products polyamides aromatic polyamides, e.g. aramides
-
- D—TEXTILES; PAPER
- D10—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B2331/00—Fibres made from polymers obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds, e.g. polycondensation products
- D10B2331/04—Fibres made from polymers obtained otherwise than by reactions only involving carbon-to-carbon unsaturated bonds, e.g. polycondensation products polyesters, e.g. polyethylene terephthalate [PET]
-
- D—TEXTILES; PAPER
- D10—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B—INDEXING SCHEME ASSOCIATED WITH SUBLASSES OF SECTION D, RELATING TO TEXTILES
- D10B2401/00—Physical properties
- D10B2401/06—Load-responsive characteristics
- D10B2401/061—Load-responsive characteristics elastic
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/29—Coated or structually defined flake, particle, cell, strand, strand portion, rod, filament, macroscopic fiber or mass thereof
- Y10T428/2913—Rod, strand, filament or fiber
- Y10T428/2929—Bicomponent, conjugate, composite or collateral fibers or filaments [i.e., coextruded sheath-core or side-by-side type]
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T442/00—Fabric [woven, knitted, or nonwoven textile or cloth, etc.]
- Y10T442/10—Scrim [e.g., open net or mesh, gauze, loose or open weave or knit, etc.]
- Y10T442/102—Woven scrim
- Y10T442/105—Comprising a composite fiber
Definitions
- the present invention relates to a mesh fabric using a composite filament and suitable for a printing screen.
- Mesh fabrics made of silk or stainless steel have been widely used as textiles for printing screens, but silk has problems in strength and dimensional stability, and stainless steel has elastic recovery and instantaneousness.
- mesh fabrics made of polyester or nylon are increasingly used at present.
- polyester mesh fabrics are often used because of their excellent dimensional stability, but polyester screens have the following defects *.
- Japanese Patent Application Laid-Open No. 59-144,688 discloses an antistatic screen girder using a composite filament, which is used to prevent the screen girder from being charged.
- the purpose of this method is to use a thermoplastic synthetic polymer containing a conductive black, which has been used to improve printing accuracy and printing resistance. No solution was suggested for improving the properties.
- the present invention provides a printing screen which uses a composite filament and has all of dimensional stability, adhesion to an emulsion resin and elastic recovery, that is, excellent printing accuracy and printing resistance.
- the purpose of the present invention is to provide a mesh fabric for textiles. Disclosure of the invention
- the mesh fabric of the present invention is a mesh fabric using a composite filament, wherein the composite filament is made of a material having good adhesion to a screen emulsion or a resin, It is made of a core-in-sheath composite filament with a core that is excellent in dimensional stability and elastic surface resilience, and the above-mentioned woven fabric is used as a 5 cm wide test piece for label and strip.
- the composite filament is made of a material having good adhesion to a screen emulsion or a resin
- It is made of a core-in-sheath composite filament with a core that is excellent in dimensional stability and elastic surface resilience, and the above-mentioned woven fabric is used as a 5 cm wide test piece for label and strip.
- a polyester or polyolefin having excellent dimensional stability and elastic recovery is used as the core material of the composite filament to assure the dimensional stability of the screen.
- the use of a polyamide or a low-viscosity polyester with good adhesion to resin etc. as a sheath material prevents the generation of white powder scum during weaving, which is a drawback of ordinary polyester screens.
- the mesh fabric of the present invention has high productivity and can always be manufactured with high quality, and can be stably used as a screen having excellent printing accuracy, printing resistance, and the like.
- the woven fabric of the present invention can be used to select and use a composite filament as described above, and to perform an appropriate heat setting as necessary, thereby improving the strength and elongation of the woven fabric.
- the workability in the gauging process during screen production and the dimensional stability of the screen are significantly improved, It also improves the high-tension printing resistance of the plate in the printing process, making it applicable to precision printing.
- the relationship between the strength and elongation of the woven fabric in the present invention is such that while having an appropriate breaking elongation that cannot be expected with stainless steel, the breaking strength is the same as that of a conventional synthetic woven fabric.
- This is a curve that is significantly larger than the woven fabric, and has a reduced strength so that the stress' strain curve becomes Y ⁇ (X + 1) X5 / 3 when the strain is 5% or more. Therefore, it is possible to form a stable screen with very high tension and low elongation. For example, a high-tension screen with a tension of 0.76 mm or less from San Giken's tension gauge, which was not possible with conventional synthetic fabric fabrics, was impossible. Can be manufactured with good workability.
- the polyester and the polyolefin constituting the core component need to have an appropriate viscosity at the spinning temperature determined in relation to the ⁇ component at the time of the spinning.
- Lenterephthalate, copolymerized polyalkylene terephthalate, poly [1,4-cyclohexanediol 'terephthalate], etc. are used, but after weaving, in the heat setting at the processing stage.
- polyethylene terephthalate, polybutyrene terephthalate and poly [1,4-cyclohexanediol • terephthalate] which is particularly economical. It is best to use polyethylene terephthalate, which is readily available.
- Polyolefins such as polyethylene, polypropylene, and polybutene can be used, but from the viewpoint of spinning stability and ease of handling, polyethylene and polypropylene are preferred. In particular, it is preferable to use a polypropylene having an easy-to-select spinning temperature.
- Polyamides that constitute the sheath component include Nylon 6, Nylon 66, Nylon 610, Nylon 12 and Nylon laminocyclohexylmetane.
- Aliphatic polyamides such as polyamides condensed with dodecanoic acid
- Aromatic polyamides such as polystyrene, polyxylylene adipamide, and polyhexamethylene phthalamide can all be used, but Nylon 6 and Nylon 66 are preferred due to their ease of spinning and economy.
- the cross-sectional shape of the fiber may be an ordinary round cross-sectional shape, and the arrangement and shape of the core components are not particularly limited, and may be single-core, multi-core, round cross-section, irregular cross-section. Concentric or eccentric is possible. . However, in order to guarantee dimensional stability, a concentric single-core arrangement with a round cross section where stress is not dispersed or a multi-core arrangement with a round cross section is preferred.
- the ratio of the core component to the sheath component is preferably 1: 5 to 3: 1 by volume, and particularly preferably 1: 2 to 2: 1. If the amount of the sheath component is too small, the sheath film becomes too thin, causing uneven thickness during spinning, and the film tends to be broken, or the film is damaged due to external stress during weaving, gauging or printing. May be. Conversely, if the core component is too small, these disadvantages will not occur, but the resistance to tensile stress will be low, and the screen will lack dimensional stability.
- the composite filament may be a mono-filament or a multi-filament, but in order to obtain a screen with high printing accuracy, it is generally a mono-filament. It is preferable that the fineness is 1 d or more. The use of monofilaments of 5 to 50 d is particularly preferred.
- the fiber diameter is usually 100 ( "preferably less than or equal to”.
- the composite filament is usually used as a drawn yarn, but its strength is 5.5 g in order to guarantee dimensional stability as a screen. d or more, residual elongation is 30 to 50%.
- the stretching ratio and the heat setting temperature are preferably set at the time of stretching so that the boiling water shrinkage is 10% or less.
- the woven density of the woven fabric of the present invention is 10 to 600 Z-inches (that is, 10 to 600 mesh plain weave).
- An appropriate weaving density may be selected according to the application, that is, according to the supply amount of the ink and the line width of the picture. Usually, it is preferably 100 to 350 pliers.
- the woven fabric woven using the composite filament is washed with an aqueous solution of 60 to 80'c nonionic or anionic surfactant, and then heated to 100 to 190, and then heated to 100 to 190. It is set to a specified thickness and mesh number with a tension of 0 to 250 kg.
- the fabric of the present invention is made of any of aluminum-iron, wooden and resin frames. May be applied.
- the woven fabric of the present invention uses the conjugate fiber as described above, it does not change even after being spread, and is left for 24 hours before being subjected to the next photosensitive or heat-sensitive resin emulsion coating step. It can be also significantly toward the workability of manufacturing the disk Hiichin version; to above.
- any of commercially available photosensitive and heat-sensitive resin emulsions can be applied to the woven fabric of the present invention.
- photosensitive agent Dichromates such as ammonium dichromate, various diazo compounds, and emulsion resins such as gelatin, acacia, polyvinyl alcohol, vinyl acetate, acrylic resin, or a mixture thereof.
- emulsion resins such as gelatin, acacia, polyvinyl alcohol, vinyl acetate, acrylic resin, or a mixture thereof.
- Other additives such as emulsifiers and antistatic agents can also be used.
- the thickness of the emulsion applied to the mesh fabric varies depending on the intended use.
- the fabric of the present invention has a surface covered with a polyamide having good adhesion to the emulsion, the conventional polyester is used. It has remarkably excellent emulsion coating properties as compared to screens made of EVA, and can easily form a resin layer with a uniform thickness.
- a screen plate by applying an emulsion to a predetermined thickness, drying, exposing or heating, and printing the pattern using the emulsion to be used.
- a high-pressure mercury lamp, xenon lamp, etc. (about 4 kW) is used as a light source, and exposure is performed for 2 to 5 minutes from a distance of about 1 to 1.5 m. Sekimino amount at this time is 3 0 0-5 0 0 millimeter Juruno cm 2.
- the screen plate using the mesh fabric of the present invention has both dimensional stability, elastic recovery, etc., and is excellent in both printing accuracy and puncture resistance.
- At least the sheath of the composite filament is used to prevent halation from occurring during exposure and exposure by the plate-making method, so that the pattern printed on the screen is not blurred or fogged. It is preferred to treat the composite filament so that the surface is light absorbing for the light that is exposed during screen printing.
- the composite filament may be dyed after the production of the mesh fabric to impart the above-mentioned light-absorbing property, but the pigment or dye may be added to the sheath material of the composite filament. May be mixed with a stock solution, or an ultraviolet ray absorbing agent may be mixed.
- the use of ordinary polyester filament requires high-pressure dyeing, which not only impairs the workability of dyeing, but also causes heat shrinkage of the mesh fabric during dyeing and also reduces the surface of textile fabric. It is difficult for foreign materials to adhere to the surface and it is difficult to produce a screen pattern with a fine pattern with good performance.
- a screen plate can be dyed at normal pressure, and the heat shrinkage of the mesh fabric during dyeing and the adhesion of foreign substances to the fiber surface are relatively small.
- the anti-halation performance can be imparted to exposure at the time.
- the present invention only by mixing a pigment or an ultraviolet absorbent into the sheath material of the composite filament, it is possible to stably obtain the antihalation ability without dyeing after fabric production.
- the pigment or the like only needs to be mixed into the sheath material of the composite filament, so that the desired effect can be obtained in a very small diameter.
- the screen plate can be manufactured without causing adhesion of heat and shrinkage of the mesh fabric, so that even higher density and finer patterns than ever before can be screened with very high accuracy. It can be manufactured into a printed version.
- the wavelength of light used for photolithography has a peak in the range of 280 to 450 nm.
- the composite filament is preferably treated so as to have a light absorbing property for at least a part of the wavelength included in the range of 4450 nm.
- FIG. 1 shows a 150-mesh mesh fabric using a composite monofilament having a fiber diameter of 48 according to the present invention, and a polyester filament having a fiber diameter of 48. This is a graph comparing the stress-strain curves of the used 150-mesh mesh fabric.
- FIG. 2 shows a 200-mesh mesh fabric using a composite monofilament having a fiber diameter of 48 ⁇ > according to the present invention, and a polyester filament having a fiber diameter of 48.
- FIG. 4 is a graph showing a stress-strain curve of a 200-mesh woven fabric using the same.
- FIG. 3 shows a 250-mesh mesh fabric using a composite monofilament having a fiber diameter of 40 ′′ according to the present invention, and a polyester fiber having a weave diameter of 40 ⁇ . This is a graph showing the stress-strain curve of a 250-mesh mesh fabric using a lame.
- FIG. 4 shows a mesh fabric of 270 mesh using the composite monofilament having a fiber diameter of 3 according to the present invention, and a polyester filament having a fiber diameter of 34 ( "). This is a graph showing a comparison of stress-strain curves of the used mesh fabric of 270 mesh.
- FIG. 5 shows a 300-mesh mesh fabric using a composite monofilament having a fiber diameter of 34 according to the present invention, and a polyester film having a weave diameter of 34. This is a graph comparing stress-strain curves of a 300-mesh mesh fabric using a mesh.
- FIG. 6 is a graph showing a load-deformation relationship of a fiber.
- Fig. 7 is a photomicrograph (500X magnification) of a 250-mesh mesh fabric using the uncolored composite monofilament.
- Figure 8 shows a 250 mesh mesh using a composite monofilament. It is a micrograph (500 times) of the dyed material of the mesh fabric.
- Fig. 9 is a photomicrograph (500X magnification) of a dyed material of a 250-mesh mesh fabric using a polyester monofilament.
- Fig. 10 shows the results of using the uncolored composite monofilament.
- Fig. 11 is a photomicrograph (500-fold magnification) of a photomeshed plate of a 300-mesh woven fabric using a composite monofilament. It is a photomicrograph (500 times magnification) of a photomechanized plate of a 300-mesh dyed fabric using polyester monofilament. -- Figure 13 is a photomicrograph (500X magnification) of a photomeshed 300-mesh mesh fabric using uncolored composite monofilament.
- FIG. 14 is a photomicrograph (magnification: 500 ⁇ ) of a 300-mesh mesh fabric using a non-colored polyester monofilament after photoengraving.
- Nylon bellows polyethylene terephthalate as core, sheath: core volume ratio of 1: 1 circular concentric composite filament, spinning temperature 285 ° C, winding speed 1 , With the filament manufactured
- the stretch ratio was 3.90, the stretching temperature was 84 ° C, the stretching center temperature was 180 ° c, and the fiber diameter was 48 / ⁇ , 40 mm, and 34 m3.
- a variety of composite filaments were obtained.
- the woven fabrics A1 to A5 according to the present invention have an appropriate elongation, and the conventional screen materials B1 to It shows remarkably superior strength as compared with B5 and C1 to C5.
- the stress' strain curve of the woven fabrics A1 to A5 according to the present invention satisfies Y ⁇ (X + 1) X5-3 at elongation of 5% or more, whereas Inherited screen materials ⁇ 1 to ⁇ 5 and C1 to C5 all had low slope curves, far from the range of the above formula.
- Table 2 shows a comparison of white powder scum generation during weaving for woven fabrics A2, B2, A3, B3, A5, and B5 in Table 1.
- the woven fabrics A2 and B2 are 200-mesh woven fabrics woven at 18,800 yarns at a weft driving speed of 230 times.
- the woven fabrics A 3 and B 3 are 250 mesh woven fabrics woven at 23,500 warp yarns and at a weft driving speed of 230 times / min.
- the fabrics A5 and B5 are 300-mesh fabrics woven at a warp count of 28,200 and a weft driving speed of 210 times / min.
- ⁇ Residual rate of white powder scum, 20% or less.
- ⁇ White powder scum remaining rate, 20 to 50%.
- X Residual rate of white powder scum, 50% or more.
- the mesh fabrics of Example 1 were framed on an aluminum frame by a gauging machine. At this time, at the same time as measuring the compressor pressure of the gauging machine due to the change in the tension, mark the center of the mesh fabric at 5 Ocm intervals in the vertical and horizontal directions, and measure the elongation during this time. did.
- Table 3 shows the relationship between the tension, the compressor pressure of the stretcher and the elongation of the mesh fabric.
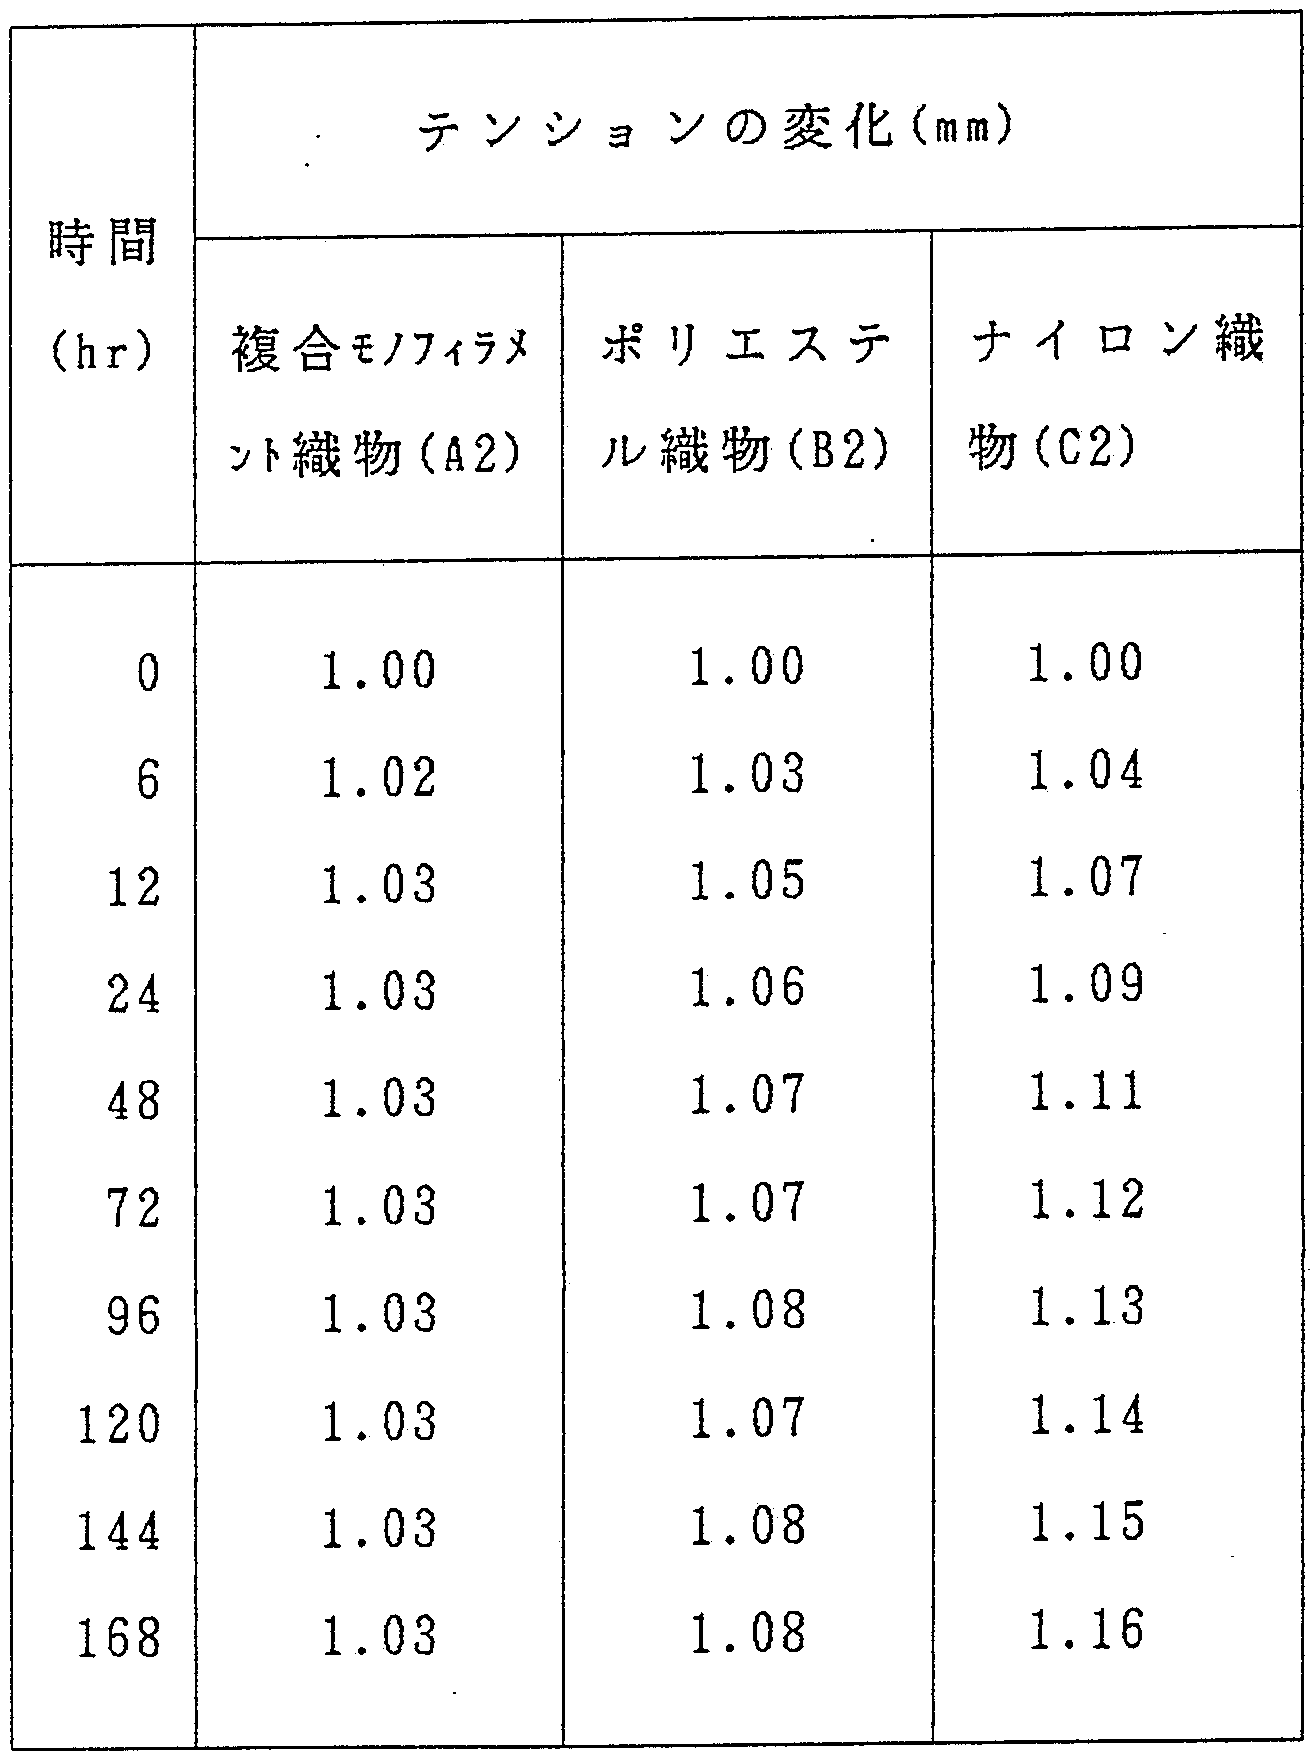
- Table 4 shows the temporal change of the tension after gauging.
- A2, A3, A5, B2, B3, B5, and C2 indicate the types of the mesh fabrics of Example 1.o.
- the equipment used for the test is as follows. -Baling machine: 3S made by Mino Group ⁇ Earth torture aluminum frame: 880 mm X 880 mm square
- the mesh fabric according to the present invention (A2, A 3, A5) shows that the workability is very good, and it is possible to stably lay the gauze at high tension.
- the elongation increases at a high tension at an accelerated rate, and it is difficult to form a stable gauze.
- the tension of the polyester mesh fabric (B2) and the nylon mesh fabric (C2) change significantly after swelling.
- the tension of Nylon mesh fabric (C 2) is not stable even after one week since the swelling.
- the mesh woven fabric of the present invention was tested for the friction band voltage, its half-life, and the leakage resistance, and was tested for ordinary polyester woven fabric, low-temperature plasma-treated polyester woven fabric, and antistatic treated polyester woven fabric. It was compared with the test result of the fabric. Table 5 shows the results.
- the test method is as follows.
- Friction band voltage Measured with a Kyoto University Chemical Research Type Rotary Stick Tester (Koa Shokai).
- Leakage resistance value Using the SM-5 type supermeter (Toa Denpa Kogyo)
- the woven fabric of the present invention can be stably used as a screen without causing a problem due to static electricity in a printing process or the like.
- Each mesh fabric after the formation of the photosensitive coating film was baked with a grid pattern of continuously changing size in 10 steps as described below.
- the baking was performed using a 4 kw high-pressure mercury lamp and exposing for 3 minutes at a distance of 1.5 m.
- Product Ki amount in this case was found to be 4 0 0 millimeter Joule ZCM 2.
- unexposed portions were removed by water spray.
- the mesh fabric thus baked with the grid pattern was subjected to a tape peeling test to measure the adhesive strength of the photosensitive coating film.
- A2A5 and B2B5 indicate the same woven fabric numbers as in Table 1 of Example 1.
- Example 5
- Figure 6 shows the load-deformation relationship between the first cycle and the nth cycle.
- A such as A L, indicates each energy value.
- a R for A L The ratio indicates the degree of recovery after conditioning, and is a function of speed and primary clip.
- a c a 0 ,
- the mesh fabrics (A 1, A 2, A 3,. A 4, A 5) according to the present invention have extremely excellent recoverability and a large load. Also ordinary polyester mesh fabrics (B1, B2, B3, B
- Example 1 Each of the fabrics of Example 1 was heat-set, then framed on an aluminum frame by a sizing machine, washed with water and dried, and then subjected to PVA-vinyl acetate photosensitive emulsion NK. — Apply 14 (manufactured by Carle Co., West Germany), dry, and apply repeatedly to make a film thickness of 12, and apply the following two patterns to each mesh fabric after forming the photosensitive film. Baked.
- test patterns each consisting of five lines of 150 0 ⁇ 2 0 ⁇ m. 250, u 300 m arranged at equal intervals. Observe the print misalignment when printing 1 000 times and 3 000 times with the pattern (I), and observe the reproducibility of fine lines with the pattern ( ⁇ ).
- the printing was performed using a 3 KW metal halide lamp at a distance of 80 era for 2 minutes. Then, after immersion in water for 3 minutes, unexposed areas were removed by water spray.
- Table 9 10 shows that the mesh fabric (A2, A3, A5) according to the present invention can be applied to high-density and high-precision printing with excellent printing precision and fine line printing. You can see that
- the ordinary polyester mesh fabrics (B2, B3, B5) have poor fine line print resolution, and the precision decreases markedly as the number of prints increases.
- the men's woven fabric (A2, A3, A5) according to the present invention has excellent E, P, C. and elongation modulus after printing, and the printing accuracy is high.
- the printing resistance was remarkably improved, and that it can be applied to high-density and high-precision printing.
- a yellow pigment (PID Yellow No. 83, manufactured by Repino Color Industrial Co., Ltd.) was added to the sheath material of the composite filament at a rate of 0.01% by weight, and used.
- mesh fabrics X1 to X5 composed of composite fibers whose sheath portion was colored yellow with a stock solution were obtained.
- the mesh fabrics A1 to A5 of Example 1 were dyed yellow under the conditions shown in Table 13 and the mesh fabrics Y1 to Y in which the sheath portion of the composite filament was dyed.
- the mesh fabrics of Nos. 1 to 5 of Example 1 were dyed yellow under the conditions shown in Table 13 to obtain yellow polyester mesh fabrics Nos. 1 to 5 I got
- each of the mesh fabrics thus obtained exhibits antihalation properties against exposure in photoengraving, but as shown in Table 13, the composite fabric using the uncolored sheath material as shown in Table 13
- the mesh fabrics X1 to X5 consisting of filaments do not need to use a dyeing process with poor workability. It can be seen that the mesh fabric can be applied to the production of screen stencils of any pattern without any heat shrinkage, etc., with extremely high quality. Further, even when dyed, the mesh fabrics Y1 to Y2 of the present invention do not require harsh dyeing conditions and can easily obtain the anti-halation property, and can be used for dyeing at the time of dyeing.
- FIGS. 7 to 9 Micrographs (magnification: 500 times) of X 3, Y 3 and Z 3 are shown in FIGS. 7 to 9.
- the mesh fabrics X1 to X5 using the uncolored composite monofilament according to the present invention have extremely clean surfaces
- the mesh fabrics Y1 to Y5 using the composite monofilament of the present invention are the mesh fabrics Z1 to Z5 using the polyester monofilament. It can be seen that the product is of good quality with less foreign matter adhesion compared to Fig. 5.
- Example 10 Example 10
- Mesh fabrics X1 to X5, Y1 to Y5 and Z1 to Z5 of Example 8 and mesh fabrics A1 to A5 and B1 to B of Example 1 which are not dyed 5 was washed with 0.2% aqueous neutral detergent solution and dried, then coated with PVA-vinyl acetate photosensitive felony NK-14 (manufactured by Hext Co.), dried, and coated again to form a film. It was 10 to 12 m.
- Table 15 shows the results of baking a fine pattern on each mesh fabric after the formation of the photosensitive coating film and observing it with an electronic microscope.
- Fig. 10 to Fig. 14 show micrographs (magnification: 500 times) of mesh fabrics X5, Y5, ⁇ 5, ⁇ 5, and ⁇ 5 on which the above pattern was baked.
- the mesh fabric according to the present invention can prevent halation very effectively by both dyeing and undiluted solution coloring, and can produce fine patterns. Can be reproduced on a screen version with high accuracy (see Fig. 10 and Fig. 11 and the columns ⁇ 1 to ⁇ '5 and ⁇ 1 to ⁇ 5 in Table 14).
- the antihalation effect can be obtained by dyeing, but the fiber surface becomes uneven as shown in Fig. 9 and Fig. 12 and the adhesive strength is reduced, resulting in a clear pattern. Is not obtained (see columns ⁇ 1 to ⁇ 5 in Table 14).
- the mesh fabric of the present invention has excellent dimensional stability and high strength. Because of its excellent adhesiveness with resin, it enables the production of a print screen with good workability and high accuracy. Further, since the mesh fabric of the present invention has excellent antistatic properties, the workability when used as a printing screen is markedly enhanced.
- the woven fabric of the present invention has good ink passing properties, enables the manufacture of a screen with very little change over time, and is free from irregularities. It will greatly improve the performance and make it possible to mass-produce screens that can be used stably for precision printing of electronic components such as printed circuit-multilayer boards and IC circuits at low cost with good workability.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Woven Fabrics (AREA)
- Printing Plates And Materials Therefor (AREA)
- Multicomponent Fibers (AREA)
Description
明 細 書 印捺スク リ ー ン用メ 'ン シュ織物 技術分野
本発明は、 複合フ ィ ラメ ン トを使用した、 印捺スク リ ーンに適し た、 メ 'ン シュ織物に関するものである。 背景技術
印捺スク リ ーン用の織物としては、 シルク又はステンレスからな るメ ツ シュ織物が広く使用されてきたが、 シルク は強度、 寸法安定 性に問題があり、 又、 ステンレスは弾性回復、 瞬発性に問題があり . しかも、 これらは共に高価であるため、 現在ではポリ エステル又は ナ イ ロ ンからなるメ ッ シュ織物が使用されることが多 く なつてきて いる。 特に、 ポリ ヱステル製のメ ッ シュ織物は寸法安定性に優れ るため、 多用されるが、 ポリ エステルスク リ ー ンには次のような欠 *があった。
a ) 製織時に白粉スカムが発生して種々の障害を引き起こ し易い、 b ) 乳剤の塗布性が悪い、
c ) 均一な膜厚を形成させるためには、 職人的な手法で数多 く の重 ね塗りを必要とする、
d ) 生産性が低い、
e ) メ ッ シュと乳剤樹脂との密着性が悪く 、 耐印刷性に劣る
などである。
従来、 これらの欠点を解决すべく 、 酸又はアルカ リ等による化学
処理、 火炎処理、 コロナ処理など種々の方法が検討されてきたが、 素材の強力低下を招く などの問題を生じ、 十分な効果は得られず、 実用的な改良がなされていないのが現状である。
しかし、 印刷分野の多様化に伴い、 印刷精度及び耐印刷性に対す る要望は益々強まり 、 ステ ン レススク リ ー ンの寸法安定性と、 ナ ィ ロ ンスク リ ーンの乳剤樹脂との密着性と、 ポリ エステルスクリ ー ン の弾性面復性を兼ね備えたスク リ 一 ンの開発が強く要望される。 特開昭 5 9 - 1 4 2 6 8 8号公報には、 複合フイ ラメ ン トを使用 した制電性スク リ一ン紗が開示されるが、 これはスク リ一ン紗の帯 電防止性の改良を目的とするものであって、 導電性力一ボンブラ ッ クを含有する熱可塑性合成重合体を使用することを特徴とするもの であり、 従来問題とされてきた印刷精度と耐印刷性の改良について ば何ら解決方法が示されていない。
本発明は、 複合フイ ラメ ン トを使用して、 寸法安定性、 乳剤樹脂 との密着性及び弾性回復性をすベて兼ね備えた、 即ち印刷精度及び 耐印刷性共に優れた、 印捺スクリ ―ン用のメ ツシュ織物を提供する ことを目的とする。 発明の開示
本発明のメ ッシュ織物は、 複合フ ィ ラメ ン トを使用したメ ッシュ 織物であって、 前記複合フイ ラメ ン トが、 スク リ ー ンの乳剤や樹脂 と接着性の良い素材を鞘とし、 寸法安定性及び弾性面復性に優れた 素材を芯とする芯鞘型複合フイ ラメ ン トからなること、 及び上記織 物を、 5 cm幅の試験片と して、 ラベル · ス ト リ ッ プ法で、 摑み間隔
2 0 cnvに設定してス ト レス · ス ト レイ ン曲線を測定した場合、 破断
伸度が 1 5 〜 4 0 %で、 破断強度が 2 5 kg f 以上であり、 かつ 5 % 以上の伸度において、 強度 Y (k g f ) と伸度 X ( % ) の関係が Y≥ ( X + 1 ) X 5 3であることを特徴とする。
即ち、 本発明は、 異なる合成繊維素材を組み合わせて、 複合フィ ラメ ン ト として使用することによって、 それぞれ素材の長所のみを 有効に発揮させ、 所望の目的を効果的に達成したものである。
例えば、 本発明では、 複合フイ ラメ ン トの芯素材として寸法安定 性及び弾性回復性に優れたポリ エステル又はポリオレフィ ンなどを '使用し、 ス ク リ ー ンの寸法安定性を保証し、 また、 鞘素材として樹 脂等と接着性の良いポリ ア ミ ド又は低粘度ボリ ヱステルなどを使用 することによって、 通常のポリ ヱステルスク リ ー ンの欠点である製 織時の白粉スカムの発生を防止し、 スク リ ー ンの強度、 乳剤の塗布 性、 ィ ンキの通過性等を改良するこ とができ る のである。
従って、 本発明のメ ッ シュ織物は生産性よ く 、 常に高品位に製造 でき、 しかも印刷精度、 耐印刷性等に優れたス ク リ ー ンとして安定 して使用できるものとなる。
更に、 本発明の織物は、 前述の如き複合フイ ラメ ン トを十分選択 して使用し、 必要に応じて適度の熱セ ッ トをするなどするこ とに よって、 織物の強度と伸度の関係を前述の如き特定の範囲に設計す るこ とによ って、 ス ク リ ー ン製造時の紗張り工程における作業性、 ス ク リ ―ンの寸法安定性を著し く 向上し、 また印刷工程での版の高 テ ン シ ョ ン耐印刷性をも向上し、 精密印刷への適用を可能とする も のである。
本発明における織物の強伸度の関係は、 ステ ン レスでは望めない 適度の破断伸度を有しながら、 破断強度は通常の合成織維製メ ツ
シュ織物より著しく大であり、 しかもス トレス ' ス ト レイ ン曲線が 5 %以上の伸度において Y≥ ( X + 1 ) X 5 / 3 となるように伸度 が抑えられ強度の勝った曲線となるものであり、 このため、 非常に 高テンショ ンで伸度少なく安定したスク リ一ンの形成が可能となる ものである。 例えば、 サン技研製 7 5 Β型テンショ ンゲ一ジによる テンショ ンが 0. 6 0以下という、 従来の合成織維製メ 'ン シュ織物で ば不可能であつた高テンショ ンのスク リ ーンをも、 作業性よ く製造 可能となる。
なお、 本発明において、 芯成分を構成するポリ エステル及びポリ ォレフィ ンは、 紡糸時に齄成分との関連で決まる紡糸温度で適当な 粘性を有する必要があるが、 例えばポリ エステルとしては、 ポリ ァ ルキ レンテレフタ レ一 ト、 共重合ポリ アルキレンテレフタ レー ト、 ポリ 〔 1 , 4—シク ロへキサンジオール ' テレフタ レ一 ト〕 等が使 用されるが、 製織後、 加工段階での熱セッ トにおける寸法安定性を 確実なものとするためには、 ポリ エチレンテレフタ レー ト、 ボリブ チレンテレフタ レー ト及びポリ 〔 1 , 4 ーシク ロへキサンジオール • テレフタ レー ト〕 の使用が好まし く 、 特に経済的に入手し易いポ リ エチレンテレフタ レー トの使用が最適である。 また、 ポリ オ レ フ ィ ンとしてはポリ エチレン、 ポリ プロ ピレン、 ポリ ブテン一 1等 が使用できるが、 紡糸時の安定性や取り扱い易さの点から、 ポリ ェ チレン、 ポリ プロピレンが好適であり、 特に紡糸温度の選択'の容易 なポリ プ口 ピレンの使用が好ましい。
また、 鞘成分を構成するポリア ミ ドとしては、 ナイ ロ ン 6、 ナイ ロ ン 6 6 、 ナイ ロ ン 6 1 0、 ナイ ロ ン 1 2 、 ノヽ 'ラァ ミ ノ シク ロへキ シルメ タ ンと ドデカンニ酸との縮合ポリ ア ミ ド等の脂肪族ポリ ア ミ
ド、 ボリ キシリ レンアジパミ ド、 ポ リ へキサメ チレンフタルア ミ ド 等の芳香族ポリ ア ミ ドがいずれも使用できるが、 紡糸の容易さ及び 経済性などから、 ナイ ロ ン 6及びナイ ロ ン 6 6 の使用が好適である なお、 複合フィ ラメ ン トの形態は、 繊維横断面の全周にわたって 鞘成分が連続して存在し、 芯成分が露出していないことが重要であ る。 繊維の横断面の形状は、 通常の丸断面形状でよ く 、 また芯成分 の配置及び形状は特に限定されず、 単芯、 多芯、 丸断面、 異形断面. 同心、 偏心いずれも可能である。 しかし、 寸法安定性を保証するた めには、 応力が分散しない丸断面の同心的単芯配置、 又は丸断面の 多芯配置が好ま しい。
芯成分と鞘成分の比率は,、 容量比率で 1 : 5 〜 3 : 1 であるのが 好ま し く 、 特に 1 : 2 〜 2 : 1 であるのがよい。 鞘成分が少なすぎ ると、 鞘の被膜が薄く なりすぎて、 紡糸時に厚み斑が生じ、 被膜が 破れ易く なつたり、 製織時、 紗張り時又は印刷時に外部応力を受け て、 被膜が破れたりするこ とがある。 逆に芯成分が少なすぎると、 これらの欠点は生じないが、 引っ張り応力に対する抵抗が小となり、 スク リ 一ンとしての寸法安定性に欠けることとなる。
複合フ ィ ラメ ン ト は、 モノ フ ィ ラメ ン ト及びマルチフ ィ ラメ ン ト いずれでもよいが、 印刷精度のあるスク リ ー ンを得るためには、 一 般的にモノ フ ィ ラメ ン トであるのが好適であり、 その繊度は 1 d以 上あればよい。 5 〜 5 0 dのモノ フィ ラメ ン トの使用が特に好ま し い。 なお、 繊維径は通常 1 0 0 ( "以下であるのが好ま しい。
本発明のメ ッ シュ織物の製織に当たっては、 当該複合フィ ラメ ン トは通常延伸糸として用いるが、 スク リ ー ンと しての寸法安定性を 保証するため、 その強度は 5. 5 gノ d以上、 残伸度は 3 0 〜 5 0 % .
沸水収縮率は 1 0 %以下となるように延伸時に延伸倍率及び熱セ ッ ト温度が設定されるのがよい。 特に強度 6 g Z d以上、 残伸度 3 5 〜 4 5 %、 沸水収縮率は 9 %以下の延伸糸の使用が好ましい。
また、 一般に、 本発明の織物の織り密度は 1 0〜 6 0 0本 Zイ ン チ (即ち 1 0〜 6 0 0 メ ッ シュの平織) とされるが、 スク リ ーンと しての用途に応じて、 即ちィ ンキの供給量や絵柄の線幅等に応じて, 適当な織り密度が選択されればよい。 通常 1 0 0〜 3 5 0本ノイ ン チであるのが好ましい。
複合フイ ラメ ン トを使用して製織した生織は 6 0〜 8 0 'cの非ィ オンまたばァニォン系界面活性剤水溶液で洗浄した後 1 0 0〜 1 9 0 でに加熱し 1 0 0〜 2 5 0 k gのテンショ ンをかけて所定の厚み とメ ッ シュ数にセッ トされる。
セッ ト後、 メ ツシュ織物は表面を洗浄、 乾燥した後、 枠にメ ッ シュ織物を張る紗張り工程に供されるが、 本発明の織物はアルミ製- 鉄製、 木製、 樹脂製いずれの枠に適用されてもよい。
本発明の織物は、 前述の如き複合繊維を使用するため、 紗張り し た後も錢時変化がなく、 2 4時間放置した後に、 次の感光性または 感熱性樹脂乳剤の塗布工程に供することができ、 スク ひ一ン版の製 造の作業性をも著しく向 ;上させる。
これに対して、 従来のナイ ロ ン製メ ッシュ織物は、 柽時変化が悪 いため、 精密印刷には適用できず、 またポリ エステル製メ ッ シュ織 物も紗張り後の径時変化のため、 7 2時間以上ば放置しなければな らなかったのである。
スク リ一ン版の製造に当たって、 本発明の織物に対しては、 市販 の感光性及び感熱性樹脂乳剤がいずれも適用できる。 例えば感光剤
としては重クロム酸アンモニユウム塩等の重ク ロム酸塩類、 各種の ジァゾ化合物、 乳剤樹脂としてはゼラチン、 アラビアゴム、 ポ リ ビ ニールアルコ ール、 酢酸ビニール、 ァク リル系樹脂又はこれらの混 合物が使用でき、 こ の他乳化剤、 帯電防止剤などの添加剤も添加使 用できる。
なお、 メ ッ シュ織物に対する乳剤の塗布厚さは目的とする用途に よって異なるが、 本発明の織物は表面が乳剤と接着性の良いポリ ア ミ ドで覆われているため、 従来のポリ エステル製のスク リ ー ンに比 して乳剤塗布性に著し く 優れ、 均一な膜厚の樹脂層を容易に形成で さる。
所定の膜厚になるように乳剤を塗布した後、 乾燥し、 露光または 加熱によって、 スク リ —ン版が製造されることは常法通りであり、 また、 パター ンの焼付けは使用する乳剤等によって異なるが、 通常 高圧水銀ラ ンプ、 キセノ ンラ ンプ等 ( 4 k w程度) を、 光源に用い、 1 〜 1. 5 m程度の距離から 2 〜 5分間露光する。 この時の積箕光量 は 3 0 0 〜 5 0 0 ミ リ ジュールノ c m 2 である。
このようにして、 本発明のメ ッ シュ織物を使用したスク リ ー ン版 は、 寸法安定性、 弾性回復性などを兼ね備えた、 印刷精度及び耐印 刺性共に優れたものとなるが、 写真製版法による感光 · 露光の際に ハレー シ ョ ンを生じて、 スク リ ーン上に焼付けたパター ンに、 ぼけ やかぶりを生じないように、 複合フィ ラメ ン トの少な く とも鞘素表 面が、 スク リ ーン版製造時に露光される光に対して光吸収性を示す ように、 複合フィ ラメ ン トを処理するのが好ま しい。
複合フイ ラメ ン トには、 メ ッ シュ織物製造後に染色して上記光吸 収性を付与してもよいが、 複合フィ ラメ ン トの鞘素材に顔料や染料
を混入して原液着色したり、 又は紫外.線吸収剤を混入してもよい。 通常のボリエステルフィ ラメ ン トを使用したものでは、 高圧染色 を必要とするため、 染色な作業性が悪いだけでな く 、 染色時にメ ツ シュ織物に熱収縮を生じたり、 また織維表面に異物が付着したり し やすく 、 緻密なパター ンのスク リ ー ン版を性能よ く製造することは 困難であるが、 本究明の製品では、 複合鐡維の鞘素材として染色性 に優れるポリてミ ドを使用できるため、 常圧で染色でき、 染色時の メ ッ シュ織物の熱収縮や繊維表面への異物の付着が比較的少ない状 態で、 写真製版法によるスク リ —ン版製造時の露光に対するハレ一 ショ ン防止性能を付与できる。
更に、 本発明では、 複合フイ ラメ ン トの鞘素材に顔料や紫外線吸 収剤を混入するだけで、 織物製造後に染色する必要なく 、 安定して ハレーショ ン防止能を得ることもできる。 この方法は、 複合フィ ラ メ ン トの鞘素材のみに顔料等を混入すればよいため、 非常に径済的 に所望の效果を得ることができるものであり、 また、 織維表面に異 物が付着したり、 メ ッ シュ織物に熱収縮を生じたりすることなく、 ス ク リ ーン版を製造できるため、 従来になく高密度で微細なバタ一 ンをも非常に精度よ く スク リ ーン版に製造できるものとなる。
なお、 一般に、 写'真製版に使用される光の波長は 2 8 0〜 4 5 0 nmの範囲にピークを有するものであるので、 写真製版に使用される 光に対応して、 2 8 0〜 4 5 0 nmの範囲に含まれる少なく とも一部 の波長の光に対して光吸収性を有するように、 複合フイ ラメ ン トは 処理されるのが好ましい。
図面の簡単な説明
第 1図は、 本発明による繊維径 4 8 の複合モノ フィ ラメ ン トを 使用した 1 5 0 メ ッ シュ のメ ッ シュ織物と、 繊維径 4 8 のポ リ エ ステルフ ィ ラ メ ン ト を使用した 1 5 0 メ ッ シュ のメ ッ シュ織物のス ト レス — ス ト レイ ン曲線を比較して示すグラ フである。
第 2図は、 本発明による繊維径 4 8 < "の複合モノ フ ィ ラ メ ン トを 使用した 2 0 0 メ ッ シュ のメ ッ シュ織物と、 繊維径 4 8 のポリエ ステルフ ィ ラ メ ン トを使用した 2 0 0 メ ッ シュ のメ ッ シュ織物のス ト レス ー ス ト レイ ン曲線を比較して示すグラフである。
第 3図は、 本発明による繊維径 4 0 « " の複合モノ フィ ラ メ ン トを 使用した 2 5 0 メ ッ シュ のメ ッ シュ織物と、 織維径 4 0 ^ のポ リ エ ステルフ ィ ラ メ ン トを使用した 2 5 0 メ ッ シュ のメ ッ シュ織物のス ト レス — ス ト レイ ン曲線を比較して示すグラ フである。
第 4図は、 本発明による繊維径 3 の複合モノ フィ ラメ ン トを 使用した 2 7 0 メ ッ シュ のメ ッ シュ織物と、 繊維径 3 4 ( " のポリ エ ステルフ ィ ラ メ ン トを使用した 2 7 0 メ ッ シュ のメ ッ シュ織物のス ト レス ー ス ト レイ ン曲線を比較して示すグラ フである。
第 5図は、 本発明による繊維径 3 4 の複合モノ フ ィ ラ メ ン トを 使用した 3 0 0 メ ッ シュ のメ ッ シュ織物と、 織維径 3 4 のポ リ ェ スチルフ ィ ラ メ ン トを使用した 3 0 0 メ ッ シュ のメ ッ シュ織物のス ト レス — ス ト レイ ン曲線を比較して示すグラ フである。
第 6図は、 繊維の荷重-変形の関係を示すグラ フである。
第 7図は、 原液着色した複合モノ フ ィ ラ メ ン トを使用した 2 5 0 メ 'ン シュのメ ッ シ ュ織物の顕微鏡写真 ( 5 0 0倍) である。
第 8図は、 複合モノ フ ィ ラメ ン トを使用した 2 5 0 メ ッ シュ の
メ ッシュ織物の染色物の顕微鏡写真 ( 5 0 0倍) である。
第 9図ば、 ポリ エステルモノ フ ィ ラメ ン トを使用した 2 5 0 メ ッ シュのメ ッ シュ織物の染色物の顕微鏡写真 ( 5 0 0倍) である。
第 1 0図は、 原液着色した複合モノ フィ ラメ ン トを使用した 3 0
0 メ ッ シュのメ ッ シュ織物の写真製版後の顕微鏡写真 ( 5 0 0倍) である。
第 1 1図は、 複合モノ フ ィ ラメ ン トを使用した 3 0 0 メ ッ シュの メ ッシュ織物染色物の写真製版後の顕微鏡写真 ( 5 0 0倍) である , 第 1 2図は、 ポリ エステルモノ フ ィ ラメ ン トを使用した 3 0 0 メ ッ シュのメ ツ シュ織物染色物の写真製版後の顕微鏡写真 ( 5 0 0 倍) である。 - - 第 1 3図ば、 未着色の複合モノ フィ ラメ ン トを使用した 3 0 0 メ ッシュのメ ッ シュ織物の写真製版後の顕微鏡写真 ( 5 0 0倍) で ある。
第 1 4図は、 未着色のポリ エステルモノ フィ ラメ ン トを使用した 3 0 0 メ ッ シュのメ ッ シュ織物の写真製版後の顕微鏡写真 ( 5 0 0 倍) である。 発明を実施するための最良の形態
次に、 本発明の実施例を示すが、 本 ¾明ばこれらに限定されるも のではない。
実施例 1 .
6 ナイ ロ ンを鞴、 ポリ エチレンテレフタ レー トを芯とし、 鞘 : 芯 の容量比率が 1 : 1 の円形同心複合フ イ ラメ ン トを、 紡糸温度 2 8 5 'C、 巻き取り速度 1 , 0 0 0 mノ分で製造し、 このフィ ラメ ン ト
を延伸倍率 3. 9 0、 延伸温度 8 4 °c、 延伸セ 'ン ト温度 1 8 0 'cで延 伸し、 織維径が 4 8 /^ 、 4 0 M m 、 3 4 m の 3種の複合フイ ラ メ ン トを得た。
これらの複合フィ ラメ ン トを用いて、 表 1 の 5種のメ ッ シュ織物 A 1 〜 A 5を製造し、 熱セ ッ ト した後、 それぞれの強伸度を試験し た。 その結果を、 同一繊維径、 同一メ ッ シュのポ リ エステル製メ ッ シュ織物 B 1 〜 B 5 の結果と比較して表 1 に示す。
表 1

試験方法 : J I S L 1 0 6 8 〜 : L 9 6 4
ラベル ド . ス ト リ ップ法
試験機 : 定速緊張形試験機
(島津製作所製 S - 5 0 0型)
試験条件 : 2 0 で、 R.H. 6 5 ¾
試験幅 5 cm、 摑み間隔 2 0 cm
引張速度 1 0 cm/min
試験回数: 5 0回
なお、 表 1 のメ ッ シュ織物 A 1 〜 A 5及び B 1 〜 5、 並びに従来 のナイ ロ ンメ ッ シュ織物 C 1 〜 C 5 に関するス ト レス ' ス ト レイ ン 曲線を第 1図〜第 5図に示す。 試験条件は前記同様であり、 また メ フ シュ織物 C 1 〜 C 5 の素材及びメ 、フシュ数は次の通りである。
C 1 δ θ ^πι ナイ ロ ンモノ フ ィ ラメ ン ト による 1 5 0 メ ッ シュ の織物
C 2 5 0 m ナイ ロ ンモノ フ ィ ラメ ン ト による 2 0 0 メ ッ シュ の織物
C 3 3 9 〃 m ナイ ロ ンモノ フ ィ ラメ ン トによる 2 5 0 メ ッ シュ の織物
C 4 3 9 m ナイ ロ ンモノ フ ィ ラメ ン ト による 2 7 0 メ ッ シュ の織物
C 5 3 9 /im ナ イ ロ ンモノ フ ィ ラメ ン ト による 3 0 0 メ ッ シュ の織物
表 1及び第 1図〜第.5図から明らかなように、 本発明に従った A 1 〜 A 5 の織物は、 適度の伸度を有し、 しかも従来のスク リ ー ン 素材 B 1 〜 B 5及び C 1 〜 C 5 に比して著しく優れた強度を示す。 また、 本発明に従つた A 1 〜 A 5の織物のス ト レス ' ス ト レイ ン曲 線は伸度 5 %以上で Y≥ ( X + 1 ) X 5ノ 3を満足する のに対し、 徒来のスク リ一ン素材 Β 1 〜 Β 5及び C 1 〜 C 5 はいずれも勾配の 低い曲線となり、 上式の範囲に遠く及ばないものであった。
次に、 表 1 の織物 A 2、 B 2、 A 3、 B 3、 A 5、 B 5 について 製織時の白粉スカムの発生状態を比較して表 2 に示す。
織物 A 2及び B 2 は、 柽糸本数 1 8 , 8 0 0本、 緯糸打ち込み速 度 2 3 0回ノ分で製織した 2 0 0 メ ッ シュの織物であり、
織物 A 3及び B 3 は、 経糸本数 2 3 , 5 0 0本、 緯糸打ち込み速 度 2 3 0回/分で製織した 2 5 0 メ ッ シュの織物であり、
織物 A 5及び B 5 は、 経糸本数 2 8 , 2 0 0本、 緯糸打ち込み速 度 2 1 0回/分で製織した 3 0 0 メ 'ン シュの織物である。
いずれの織物も、 スルーザ一織機を用いて、 製織中スカムが目立 つ所で箴をエア 一ガ ンでふき、 スカ ムを落としながら製織した。
表 2 · 織物の種類 稼動 白粉スカム
葳先い I 判
No 繊維素材 (%) (m/ 回) 定
A2 ¾ ^"モノフィラメント 96 5, 000
B2 ボ エステルモノフィラメント 91 300 〇
A3 H モノフィラメント 97 4,500 ◎
B3 ボリエステ モノフィラメント 92 180 厶
A5 モノフィラメント 98 3, 000 ◎
B5 ポリエステル ΐノフィラメント 90 140 X 判定 ◎ : 白粉スカムがほとんど発生しない。
〇 : 白粉スカムの残存率、 2 0 %以下。
△ : 白粉スカムの残存率、 2 0 〜 5 0 %。
X : 白粉スカムの残存率、 5 0 %以上。
表 2 の結果から、 本発明に従った織物 A 2、 A 3 、 A 5 は白粉ス
L4
カムがほとんど発生することなく、 非常に品質よ く織成されること がわかる。
実施例 2
実施例 1 のメ ッ シュ織物をそれぞれ熱セッ ト した後、 紗張り機に てアルミ製の枠に枠張り した。 この際、 テ ンシ ョ ンの変化に伴う 紗張り機のコ ンプレ ッ サ圧を測定すると同時に、 メ ッ シュ織物の中 央に縦横方向それぞれ 5 O cm間隔に印を付け、 この間の伸びを測定 した。
テンショ ンと、 紗張り機のコ ンプレッサ圧及びメ ッ シュ織物の伸 率の関係を、 表 3 に示す。 また、 紗張り後のテ ンショ ンの柽時変化 を表 4に示す。 表 3及び 4において、 A 2、 A 3、 A 5、 B 2、 B 3、 B 5、 及び C 2 とあるのは、 実施例 1 のメ ッ シュ織物の種類を 示す o .
なお、 試験に使用した機器は下記の通りである。 - 紗張り機 : みのグループ製の 3 S ヱアース ト レツチヤ ー アルミ枠 : 8 8 0 mm X 8 8 0 mm角
枠材の 畐 4 0 mm、 厚み 2 5 mm
テ ンシ ョ ンメ ータ ー : サン技研製 7 5 B型テンシ ョ ンゲージ

D I · 0 Q
0.90 6.8 7.0 5.2 9.6
0.80 7.3 8.3 6.2 10.4
0.70 8.3 9.0 7.6 12.7
0.60 9.0 破断 8.8 破断
A 5 B 5 A 5 B 5
1.00 6.2 6.8 5.0 8.3
0.90 7.0 8.0 5.8 10.5
0.80 8.0 8.6 7.2 12.5
0.70 8.5 破断 8.4 破断
0,60 9.5 9.0 表 4
実施例 3
本発明のメ ッ シュ織物の摩擦帯電圧及びその半減期、 並びに漏洩 抵抗を試験し、 通常のポリエステルメ ッシュ織物、 低温プラズマ処 理したポリエステルメ ッ シュ織物及び帯電防止加工したポリ エステ ルメ ッ シュ織物の試験結果と比較した。 その結果を表 5 に示す。 試験方法は次の通りである。
摩擦帯電圧 : 京大化研式ロータ リ ースティ ッ ク テスタ ー (興亜 商会) によつて測定した。
摩擦対象布 綿金巾 3号
回転数 4 5 0 rpm
荷重 5 Q 0 g
摩擦時間 6 0 sec
漏洩抵抗値 : S M - 5型超铯緣計 (東亜電波工業) を用いて、
2 0 で、 R H 4 0 %で、 J I S G— 1 0 2 6 に 従って測定した。
表 5

この結果より、 本発明の織物は、 ス ク リ ー ンと して印刷工程など において静電気による問題を生ずることな く 、 安定して使用できる こ とがわかる。
実施例 4
実施例 1·の表 1 に示す各メ ッ シュ織物を 0. 2 %の中性洗剤水溶液 で洗浄、 乾燥した後、 P V A -酢酸ビニル系の感光性乳剤 N K — 1 4 (西独、 カー レ一社製) を塗布、 乾燥し、 重ね塗りによって膜厚 を 1 0 〜 1 2 とした。
感光性塗膜形成後の各メ ッ シュ織物に、 下記の通り 1 0段階で連 続的に大きさの変化する碁盤目パター ンを焼付けた。
No. 碁盤目の大きさ ίτ Ε. 個数
1 0.1 mm X 0.1 mm 20 10 200
2 0.2 mm X 0.2 mm 20 10 200
3 0.3 mm X 0.3 mm 20 10 200
4 0.4 mm X 0.4 mm 20 10 200
5 0.5 mm x 0.5 mm 20 10 200
6 0.6 mm x 0.6 mm 20 10 200
7 0.7 mm x 0.7 mm 10 10 100
8 0.8 mm x 0.8 mm 10 10 100
9 0.9 mm 0. mm 10 10 100
10 1.0 mmxl.0 mm 10 10 100
焼付けは、 4kwの高圧水銀ラ ンプを用い、 1. 5 mの距離で 3分間露 光して実施した。 この場合の積箕光量は 4 0 0 ミ リ ジュール Zcm2 であつた。 次いで、 水に 3分間浸漬した後、 水スプレーによって未 感光部分を除去した。
このようにして碁盤目パタ -ンを焼付けたメ ッ シュ織物について. テープ引き剥がしテス トを実施して、 感光性塗膜の接着強度を測定 した。
テス ト方法
各メ ッ シュ織物のパターン上に、 住友スリ ーェム ¾のフィ ラメ ン トテ一ブせ 8 1 0を張り付けた後、 このテープを引き剝がすという 操作を、 同一面に 3回繰り返して実施し、 テープに付着した碁盤目 の数を記録する。
その結果を、 表 6'に示す。 表 6 に、 ^_ _として示される数値は、
1回巨のテープ張り付けによって剝がれた碁盤目の数であり、 M 及び 3西として示される数値は、 それぞれ 2回目及び 3 HI目のテー ブ張り付け後に、 剝がれている碁盤百の総数である。
表 6 碁盤目 No. 1 2 3 4 5 6 7 8 9 10
1 凹
A L 0 4 0 0 0 0 0 0 0 0 0
16 4 2 2 1 0 0 0 0 0
ώ 凹
A2 4 1 0 0 0 0 0 0 0 0
碁 B 2 26 4 4 2 2 1 0 0 0 0
0 4 2 0 0 0 0 0 0 0 0
o ά 48 20 8 6 6 4 1 0 0 0
1 回
曰 A o 2 0 1 0 0 0 0 0 0 0
r> o 14 8 2 4 1 0 0 0 0 0
回
の A3 2 0 1 0 0 0 0 0 0 0
B 3 22 15 8 4 2 1 0 0 0 0
凹
剝 A 0
6 2 1 1 0 0 0 0 0 0 0
40 17 10 6 4 2 0 0 0 0 力、 1 回
A 4 A 2 0 0 0 0 0 0 0 0 0
b 4 15 8 2 2 0 1 0 0 0 0
れ 2 回
A4 2 0 0 0 0 0 0 0 0 0
B 4 24 9 7 5 0 1 1 0 0 0
数 3回 n
A4 2 0 1 U U U υ υ u u
B 4 30 17 7 5 1 1 1 0 0 0
1 回
A5 4 0 0 0 0 0 0 0 0 0
B 5 16 9 10 2 0 0 0 0 0 0
2回
A5 4 0 0 0 0 0 0 0 0 0
B 5 18 11 10 2 1 0 0 0 0 0
3回
A5 4 1 0 0 0 0 0 0 0 0
B 5 33 11 10 2 2 1 0 0 0 0
但し) A 2 A 5及び B 2 B 5 はそれぞれ実施 例 1 の表 1 と 同様の織物 No. を示す。
実施例 5
実施例 1 の表 1 に示す各メ ッ シュ織物を熱セ ッ ト した後、 それぞ れの E . P . C . 並びに伸長弾性率を試験し、 通常のポリ エステル メ ッ シュ織物の試験結果と比較した。 その結果を表 7、 表 8 に示す, E, P . C .
Elastic Performance Coefficients t VZ ^ 繊維が機械的な作用 を受けた後の回復性も考慮に入れた物性を示す。
第 1回サイ クルと第 n回サイ クルにおける荷重—変形関係を求め て第 6図の様に示す。
L o 初めの荷重曲線
L c コ ンデショユングされたときの荷重曲線
R o 初めの回復曲線
R c コ ンデショ ユングされたときの面復曲線
a o 初めの荷重時の変形量
a c コ ンデショ ユングしたときのコ ンデショ ユング荷重に対す る変形量
A L など Aのついたのはそれぞれのエネルギー値を示す。
A R の A L。 比はコ ンデショユングしたときの回復の程度を示 すもので、 速度、 一'次クリ ープの関数となる。
また、 a。2 ZA L。 は初めのサイ クルに対して全変形に対する' エネルギーの吸収の尺度を示し、 また a c z/A L。 は同様にコ ンデ ショ ニングサイ クルにおける変形エネルギー量に対するエネルギー 吸収の尺度を示す。 これらの比に対して、 A R。 /A L。 の補正項 を考慮して、 E , P . C . は次の式で表される。
A R
A L A L
E . P C =
A L o
回復可能な場合 A R o = A L o であり a o = a c >
A L o = A L c , A R = A R a であれば当然 E . P . C . = 1
非回復の場合 A R = 0 , A R c = A L o . a c = a 0 ,
E . P . C = 0
になる。 (昭和 4 5年 3月 1 0 日丸善株式会社発行の 「繊維物理 学」 第 2 5 4 - 2 5 5買参照) · - 伸長弾性率
J I S L 1 0 9 6 による。
自動記録装置付定速伸長形引張試験機を用い、 摑み間の距離を 20 cm . 引張速度を 1分間当たり摑み間隔の 10 %の速度で、 一定荷重ま で引き伸ばし、 次いで、 同じ速度で除重し、 再び同じ速度で一定荷 重まで引き伸ばす。 記録した荷重 -伸長曲線から残留伸びを計り、 次式より伸長弾性率を算出する。
L 一 L !
伸長弾性率 (%) = X 100
L
L : 一定荷重下の伸び (mm )
L : 一定荷重下の残留伸び (mm )
なお、 E . P . C . 及び伸長弾性率の測定はいずれも下記の条件 で実施した。
試験方法 : J I S L 1 0 6 8 - 1 9 6 4 ラベル ド ' ス ト リ ツプ法
試験機 : 定速緊張形試験機 (島津製作所 3 - 5 0 0型) 試験条件 : 2 0 。c、 R . H . 6 5 ¼
試験幅 5 cm. 摑み間隔 2 0 on
■ 引張逮度 1 0 cm / m i n .
サイ ク ル 2 0回
試験回数 : 5 0面
表 7
iHJ Ε . Ρ . C .
b f i Τί¾δ ciチ / 5 / st ポ リ て ス f てノフィフヌ ホ リ エスァ ^モノフィラメ ポリ エステ ント織物(Al) ル織物(B1) ント織物(A2) ル織物(B2) ント織物 (A3) ル織物 (B3) 丄 * U U 1.00 1.00 1.00 1 - 00
10 0.98 0.79 1.00 0.90 1.00 0.93
15 0,93 0.67 0.92 0.79 0.94 0.80
L si η υ , ο PR ο υ . ο ο 0.85 0.61 0.88 0.70
L υ , ο丄 0.81 0.54 0.81
Qfl 0.66 υ . ί ο 0.74
¾ς 0.45 0.75 0.44
Π R 0.66 0.40 0.70
Λ υ · ϋ 11 0.59 0.65
½ v口^S F; Τ *ί τフ t 不 05 Jリ! 丄 人 ァ ΐί¾ 不 - 5 Iリt 丄 "T ス ァ
ント織物(Α4) ル織物 (Β4) ント織物(A5) ル織物(B5)
5 1,00 1.00 1.00 1.00
10 0.97 0.75 1.00 0.81
15 0.94 0.64 0.96 0.69
20 0.88 0.52 0.90 0.56.
25 0.80 0.43 0.83 0.48
30 0.73 0.77
35 0.66 0.70
40 0.64
表 8
1HJ 伸 長 m †生 M
b f ポ' リ エステ モノフィラメ ポ リ エステ ' ¾ ¾ノフィラメ ポ リ エステ ント織物 (Al) ル織物(B1) ント織 (Α2) ル織物(Β2) ント織物(A3) ル織物 (B3)
100 0 100 0 100 0 100 0 100.0
10 99.1 89.8 100.0 93.3 100.0 95.0
15 96.8 82.0 97.7 86.9 98.6 87.3 on 70 0 93.2 79 4 92.5 74.5
OR «« β 65 3 88.8 68 2 89 2 68.5
R?♦ 7 f 82.2 60 1 82 6 60.2
•i
o 74.6 51 75 5
70 0 69.9 70.3 口 *■ ポ リ エ ス テ モノフィラメ ポ リ エ ス テ
ント織物(Α4) ル織物(B4) ント織物(Α5) ル織物(Β5)
5 100.0 100.0 100.0
10 98.3 94.0 100.0 94.1
15 95.7 87.5 97.9 88.0
20 91.1 80.9 93.5 76.0
25 88.4 68.8 88.0 64.0
30 83.6 83.2
35 75.9 76.1
40 70.4
表 7、 表 8 の結果から、 本発明に従ったメ ッ シュ織物 (A 1 , A 2 , A 3 , . A 4 , A 5 ) は、 非常に回復性に優れ、 荷重が大き く なっても通常のポリ エステルメ ッ シュ織物 ( B 1 , B 2 , B 3 , B
4 , B 5 ) より変化は少な く 、 弾性回復率並びに機械的な作用を受 けた後の回復性も良いことがわかる。
この回復性の向上により、 耐刷性も改良された版の寿命は格段に 伸びる。
実施例 6
実施例 1 のメ 'ン シュ織物をそれぞれ熱セ ッ ト した後、 紗張り機に てアルミ製の枠に枠張り し、 水洗浄、 乾燥した後、 P V A—酢酸ビ ニル系の感光性乳剤 N K — 1 4 (西独、 カー レ一社製) を塗布し、 乾燥し、 重ね塗りによって、 膜厚 1 2 と し、 感光性膜形成後の各 メ ッ シュ織物に次の 2種のパター ンを焼付けた。
( I ) 縦横 1 5 0 mm間隔で細線が交わる格子状バタ一ン。
( Π ) 太さ 5 0 m、 6 0 ^ 01、 8 0 ^ 1 0 0 1 2 5
1 5 0 ^ 2 0 0 ^ m. 2 5 0 ,u 3 0 0 mの細線を、 それぞれ等間隔に 5本づっ並べた 2群のテス トパター ン。 ( I ) のパター ンで 1 , 0 0 0 回、 3 , 0 0 0回印刷を行ったと きの印刷ずれを見、 ( Π ) のパター ンで細線の再現性を見る。
焼付けは、 3 K Wのメ タルハライ ドラ ンプを用い、 8 0 eraの距離 で 2分間露光して実施した。 次いで、 水に 3分間浸積した後、 水ス プレーによって未感光部分を除ました。
このよ う にして ( I ) 及び ( Π ) のパター ンを焼付けたメ ッ シュ 織物について印刷ずれテス ト、 細線再現性テス トを実施して、 印刷 精度を測定した。 その結果を表 9、 表 1 0 に示す。
製版条件 :
紗張り機 ミノ *グ ー 7 3Sエアーストレッチヤー(ノーマ ^り ) テンシ 3ン 1.00mm (張り上がり) 乳剤 N - 14 ( 西独 カ ー レ一社)
12 β
枠 880mm X 880ram ( ァ ゾレ ミ製)
画像 300mm 300mm
スキージ条件
ウ レタ ン
70'
角度 75'
幅 405mm
印刷条件 :
ギヤ 'ジフ' 3.0mm
印圧 1.5mm
インキ UV キ 5104-T6(三井東圧製)
インキ 粘度 200 P S
表 9 印刷精度 ( m ) ( I ) のパタ ー ン
& S回
願 ¾ノフイラメン 1· ポ リ エ ス テル モノフィラメント ポ リ エステノレ
織物 ( A 2 ) 織物 ( B 2 ) 織物 (A 3 ) 織物 ( B 3 )
1,000 3, 000 1, 000 3,000 1,000 3, 000 1,000 3,000 回 回 回 回 回 回 回 回
1 39 55 95 138 43 54 108 146 2 3 74 101 140 62 77 106 165 3 58 81 120 164 55 74 124 169 4 46 57 92 120 51 70 98 121 5 66 85 108 142 74 86 107 168 6 70 78 106 159 57 85 96 155 7 46 67 100 126 36 51 98 133 8 54 70 99 151 58 73 100 170 9 73 91 114 161 69 73 124 172
モノフィラメント ポ リ エス テル
織物 ( A 5 ) 織物 (B 5 )
印刷 1,000 3,000 1 , 000 3,000
回数 回 回 回 回
1 35 50 115 148
2 53 79 108 170
3 70 81 127 193
4 48 60 97 130
5 55 80 104 172
6 66 82 99 168
7 36 64 101 141
8 46 73 94 165
9 69 77 130 185
表 10 細線印刷解像性

表 9 10の結果から本発明に従つたメ ツシュ織物 ( A 2 , A 3 , A 5 ) は、 印刷精度、 細線印劂解像性に優れた高密度 · 高精密印刷 への適用を可能にすることがわかる。
これに対し、 通常のボ リ ヱステルメ ッ シュ織物 ( B 2 , B 3 , B 5 ) では、 細線印刷解像性が悪く、 印刷回数が増えるに従い、 精度 が著し く低下する。
実施例 Ί
実施例 6 の表 9に示す 3, 000 面印刷を行つた各メ ッシュ織物の、 印刷後の E . P . C . 並びに伸長弾性率を試験し、 通常のポ エス テルメ ッ シュ織物の試験結果と比較した。 その結果を表 1 1、 1 2 に示す。 試験方法は実施例 5 と同じ。
表 11 印刷後の E . P . C
荷 S モノフィラメントメッソ: ボリ Iステルモノフィラメント ^モノフィラメントメッシ: ポ ェステルモノフィラメント 織物(A2) 織物(Β2) 織物(A3) 織物(Β3) kgf 0 回 3, 000回 0回 3, 000回 0 回 3, 000回 0回 3, 000回
5 1.00 1.00 1.00 0.74 1.00 1.00 1.00 0.77 10 1.00 0.94 0.90 0.66 1.00 0.93 0.93 0.68 15 0.92 0.90 0.79 0.52 0.94 0.86 0.80 0.55 20 0.85 0.81 0.61 0.40 0.88 0.80 0.70 0.42 25 0.81 0.76 0.54 0.31 0.81 0.74 0.66 0.36 30 0.74 0.69 0.45 0.24 0.75 0.66 0.44 0.27 35 0.66 0.60 0.40 0.19 0.70 0.60
40 0.59 0.54 0.65 0.56
ί可 ^"^•ϊノフイラメン卜メッシこ ポ' Jiス ルモノフィラメント
織物(Α4) 織物(Β4)
kgf 0回 3, 000回 0 回 3, 000面
5 1.00 1.00 1.00 0.70
10 1.00 0.94 0.81 0.62
15 0.96 0.90 0.69 0.51
20 0.90 0.83 0.56 0.39
25 0.83 0.77 0.48 0.27
30 0.77 0.71
35 0.70 0.66
40 0.64 0.56
表 12 印刷後の伸長弾性率 (%)
何 ί ^·モノフィラメン卜メッシュ ポリ Iステルモノフィラメント Ϋ ^ ϊノフィラメントメッシュ ポ エステルモノフィラメント 織物 (A2) 物 (B ) 微物 (A 物(B kgf 0回 3, 000回 0 回 3, 000回 0回 3, 000回 0回 3, 000回
5 100,0 100.0 100.0 80.5 100.0 100.0 100,0 81.1
10 100.0 98.3 93.3 72,9 100.0 97.8 95.0 72.8
1
丄;) 97.7 95.5 86.9 65.5 98.6 94,8 87.3 66.7
20 93.2 89.9 79.4 57.0 92.5 88.1 74.5 59.3 o c a
O 88.8 84.0 68.2 46,1 o . b bo . b
30 82.2 79.1 60.1 39.8 82.6 78.9 S Oo . b
35 74.6 72.6 51.8 29.7 75.5 74. U
40 69.9 65.5 70.3 65.4 何 ^モノフィラメン 1*メッシュ ポリ Iステルモノフィラメント
織物(A4) 織物(B4)
kgf 0,回 3, 000回 0回 3, 000回
5 100.0 100.0 100.0 78.4
10 100.0 98.5 94.1 69.7
15 97.9 93.7 88,0 60.0
20 93.5 89.3 76.0 55.1
25 88.0 84.6 64.0 44.2
30 83.2 78.8
35 76.1 72.4
40 70.4 65.0
表 11、 12の結果から本発明に従ったメ 'ン シュ織物 ( A 2 , A 3 , A 5 ) は、 印刷後の E, P, C. 、 伸長弾性率が非常に優れており 印刷精度並びに耐印刷性を著し く 向上させ、 高密度 · 高精密印刷へ の適用を可能とすることがわかる。
これに対して、 通常のポ リ エステルモノ フ ィ ラメ ン ト織物 ( B 2 B 3 , B 5 ) では、 印刷回数が增すにつれて耐印刷性が低下する。 また、 通常のナイ ロ ンモノ フ ィ ラメ ン トメ ッ シュ織物は、 こ こには 試験結果を示していないが、 ポ リ エステルモノ フ ィ ラメ ン トメ ッ シュ織物に較べて伸長弾性率は劣り、 高密度 · 高精度印刷には適し ていない
実施例 8
複合フ ィ ラ メ ン ト の鞘素材に 0. 0 1重量%の割合で黄色顔料 (レ ピノ カ ラ—工業株式会社製の P I D イ ェ ロー No . 8 3 ) を添加して 使用した以外は、 実施例 1 の A 1 〜 A 5 と同様の方法で、 鞘部分を 黄色に原液着色した複合繊維からなるメ ッ シュ織物 X 1 〜 X 5 を得 た。
次いで、 実施例 1 の A 1 〜 A 5 のメ ッ シュ織物を表 1 3 の条件で 黄色に染色して、 複合フ ィ ラメ ン トの鞘部分が染色されたメ ッ シュ 織物 Y 1 〜 Y 5 を製造し、 更に、 比較例として実施例 1 の Β 1 〜 Β 5 のメ ッ シュ織物を表 1 3 の条件で黄色に染色して、 黄色のポリ エ ステルメ ッ シュ織物 Ζ 1 〜 Ζ 5を得た。
このよ う にして得たメ ッシュ織物は、 いずれも写真製版における 露光に対してハ レー シ ョ ン防止性を示すが、 表 1 3 に示す如く 、 原 液着色した鞘素材を使用した複合フ ィ ラ メ ン トからなるメ ッ シュ織 物 X 1 〜 X 5 は作業性の悪い染色工程を使用する必要がないため、
メ ッシュ織物は熱収縮などを伴う ことなく、 どのようなパターンの スク リ ーン版製造にも極めて品質よ く適用できることがわかる。 ま た、 本発明のメ ッ シュ織物 Y 1〜 Y 2 は、 染色した場合でも、 苛酷 な染色条件を必要とせず、 比較的簡単にハ レーショ ン防止性能を得 ることができ、 染色時の熱収縮による変形も、 比較的少なく、 緻密 なバターンを有するスクリ一ン版製造にも、 比較的安定して使用で きるものとなることがわかる。 これに対して、 通常のポリ エステル メ ッ シュ織物 Z 1〜 Z 5 は、 染色に苛酷な条件を要し、 熱収縮率の 高い製品となり、 緻密なパター ンを有するスク リ ー ン版の製造には 適用しにく いことがわかる。
表 1 3
織物の種類 染色条件 熱収縮率 (¾)
No メ'ジシ: 繊維素材 圧力 染色 平均 時間
XI 150 原液着色した複合モノフィラメント 48 0 0 0 0 0
X2 200 " 48 M m 0 0 0 0 0
X3 250 " 40 / m 0 0 0 0 0
U 270 ノ' 34 m 0 0 0 0 0
X5 300 〃 34 //m 0 0 0 0 0
Yl 150 染色した複合モノフィラメント 48 μ m 常圧 1.0 0.5 4.8 4.0 4.4 Y2 200 48 μ m 4.7 4.5 4.6 Y3 250 40 M m 4.6 4.4 4.5 Y4 270 34 μ m 5.2 4.5 4.4 Y5 300 34 μ m 5.3 4.6 4.5
Zl 150 ¾fe Lたボリ Iス ル¾ノフィラメント 48 μ m 问圧 4.0 2,0 13.8 13.5 13.7 Z2 200 48 μ m 13.7 13.4 13.6 Z3 250 40 μ m 13.8 13.6 13.7 Z4 270 34 μ m 14.1 13.6 13.9 Z5 300 34 β m 14.0 13.8 13.9
準時
備間
実施例 9
実施例 8 のメ ッ シュ織物 X 1 〜 X 5、 丫 1 〜 ¥ 5及び 2 1 〜 2 5 の各々について、 織物表面の伏態を電子顕微鏡で撮影し、 比較した その結果を表 1 4に示す。
表 1 4

X 3 、 Y 3及び Z 3 の顕微鏡写真 ( 5 0 0倍) を第 7図〜第 9図と して示す。 表 1 4及び第 7図〜第 9図から明らかな通り、 本発明の よる原液着色した複合モノ フ ィ ラメ ン トを使用したメ ツ シュ織物 X 1 〜 X 5 は表面が極めて清浄であり、 また、 染色した場合にも本発 明の複合モノ フ ィ ラメ ン トを使用したメ ッ シュ織物 Y 1 〜 Y 5 は、 ポリ エステルモノ フィ ラメ ン トを使用したメ ッ シュ織物 Z 1 〜 Z 5 に比較して異物の付着の少ない品質のよい製品となるつことがわか る。
実施例 1 0
実施例 8 のメ ッ シュ織物 X 1 〜 X 5 、 Y 1 〜 Y 5及び Z 1 〜 Z 5 と、 染色をしていない実施例 1 のメ ッ シュ織物 A 1 〜 A 5及び B 1 〜 B 5を、 0. 2 %の中性洗剤水溶液で洗浄、 乾燥した後、 P V A— 酢酸ビニル系感光性重罪 N K - 1 4 (へキス ト社製) を塗布、 乾燥 し、 重ね塗りによって膜厚を 1 0 〜 1 2 m とした。
感光製塗膜形成後の各メ ッ シュ織物に微細パター ンを焼付けて電 子顛微鏡で観察した結果を表 1 5 に示す。
表 1 5

注) ハ レ シ ョ ン防止効果 :
◎ ハ レー シ ョ ン防止効果が非常に良い。
〇 ハ レー シ ョ ン防止効果がある。
Δ ハ レー シ ョ ン防止効果が少ない。
x ノヽ レー シ ョ ンを起こす。
パタ ン状態 :
◎ 接着力が良く 、 パター ンがより鮮明である
〇 接着力が良く 、 パター ンのエ ッ ジも良い。
厶 接着力に劣り、 パター ンのエ ッジが悪い。
X 接着力がなく 、 パターンを形成しない。
総合判定 :
A ハレーショ ン防止効果、 接着力共に極めて良好。
B ハレーショ ン防止効果、 接着力共に良好。
C ハレーショ ン防止効果、 接着力のいずれかが劣る。 D ハレーショ ン防止効果、 接着力共に劣る。
第 1 0図〜第 1 4図として、 上記パターンを焼付けたメ ッ シュ織 物 X 5、 Y 5、 Ζ 5、 Α 5及び Β 5 の顕微鏡写真 ( 5 0 0倍) を示 すが、 これらの結果及び上記表 1 4の結果から明らかなように、 本 発明に従ったメ ッ シュ織物は染色及び原液着色いずれによっても、 非常に効果的にハレーショ ン防止ができ、 微細なバタ一ンをも精度 よ く スク リ —ン版に再現できるが (第 1 0図、 第 1 1図及び表 1 4 の Χ 1〜Χ ' 5、 Υ 1〜Υ 5 の欄参照) 、 通常のボリエステルモノ フ ィ ラメ ン トメ ッシュ織物では、 染色によって、 ハレーショ ン防止 効果は得られるが、 第 9図及び第 1 2図の如く繊維表面が不均一と なり、 接着力が低下し、 鮮明なパタ一ンが得られないことがわかる (表 1 4 の Ζ 1〜 Ζ 5 の欄参照) 。
なお、 本発明のメ ッ シュ織物では、 未染色状態でも、 パターンの 形成は可能であるが (第 1 3図および表 1 4の Α 1〜Α 5 の欄参 照) 、 通常のポリ エステルモノ フ ィ ラメ ン トメ ッ シュ織物では、 第 7図の如く 、 ぼけやかぶりが起こり鮮明なパターンが得られない (表 1 4の Β 1〜 Β 5 の櫃参照) 。 産業上の利甩分野
本発明のメ ッ シュ織物は、 寸法安定性に優れ、 しかも強度が強く
樹脂との接着性にも優れるため、 作業性よ く精度ある印刷ス ク リ ー ンの製造を可能とする。 また、 本発明のメ ッ シュ織物は帯電防止性 にも優れるため、 印刷ス ク リ ー ン と しての使用時の作業性をも著し く高める。
従って、 本発明の織物は、 ィ ンク通過性が良く 、 柽時変化の非常 に少ない、 狂いのないスク リ ー ンの製造を可能とするものであり、 印刷工程の作業性の向上及び耐印刷性を著し く高め、 プリ ン ト回路- 多層板、 I C回路など電子部品の精密印刷にも安定した使用できる ス ク リ ー ンを安価に作業性よ く 量産化可能とする。
Claims
1 . 複合フ イ ラメ ン トを使用したメ ッ シュ織物であって、 前記複合 フイ ラメ ン トが、 スク リ ー ンの乳剤や樹脂と接着性の良い素材を 鞘とし、 寸法安定性及び弾性回復性に優れた素材を芯とする芯鞘 型複合フイ ラメ ン トからなること、 及び上記織物を、 5 c m幅の試 験片として、 ラベルド · ス ト リ ップ法で、 摑み間隔 2 0 c mに設定 してス ト レス · ス ト レイ ン曲線を測定した場合、 破断伸度が 1 5 〜 4 0 %で、 破断強度が 2 5 kgf 上であり、 かつ 5 %以上の伸 度において、 強度 Y (kgf ) と伸度 X ( ¾ ) の関係が Y≥ ( X + 1 ) X 5 / 3であることを特徴とする印捺スク リ ー ン用メ ッシュ 織物。
2 . 前記複合フイ ラメ ン トがモノ フ ィ ラメ ン トである請求の範囲第 1項記載のメ ッ シュ織物。
3 . 芯鞘の容量比率が 1 : 5 〜 3 : 1 である請求の範囲第 1項記載 のメ ッ シュ織物。
4 . 芯鞘の容量比率が 1 : 2 〜2 : 1である請求の範囲第 3 項記載 のメ ッ シュ織物。
5 . 前記複合フイ ラメ ン トの鞘素材がポリ ア ミ ド又は低粘度ポ ェ " ステルである請求の範面第 1項記載のメ ッ シュ織物。
6 . 前記複合フ ィ ラメ ン の芯素材がポリ エステル又はポリオレ フ ィ ンである請求の範囲第 1項記載のメ ッ シュ織物。
7 . 前記複合フ イ ラメ ン ト の鞘素材がポ リ ア ミ ドで、 芯素材がポ リ エステルである請求の範囲第 1項記載のメ ッ シュ織物。
8 . 前記複合フイ ラメ ン トの少なく とも鞘表面が、 スク リ ーン版製
造時に露光さ ήる光に対して、. 光吸収性を示す請求の範囲第 1 項 記載のメ フ シュ織物■=
. 前記複合フ イ ラ メ ン 卜 の鞘素材が、 顔料及び 又は紫外線吸収 剤の混入によ って、 前記光吸収性を示す請求の範囲第 8 項記載の メ ッ シ ュ織物。
. 前記複合フ ィ ラメ ン 卜 の鞘素材が染色によ って、 前記光吸収性 を示す請求の範囲第 〗 項記載のメ 'ン シ ュ織物。
. 前記複合フ ィ ラ メ ン ト の鞘表面が 2 8 0 〜 4 5 0 n mの範囲に舍 まれる少な く と も一部の波長の光に対して光吸収性を示す請求の 範囲第 8 項記載のメ ノ シ ュ織物。
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1019880701294A KR950008185B1 (ko) | 1987-02-17 | 1987-08-10 | 인쇄 스크린용 메시직물 |
| DE8787905284T DE3776343D1 (de) | 1987-02-17 | 1987-08-10 | Gittergewebe fuer filmdruck. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP62/35252 | 1987-02-17 | ||
| JP62035252A JPH0637117B2 (ja) | 1986-02-18 | 1987-02-17 | 印捺スクリ−ン用メツシユ織物 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO1988006103A1 true WO1988006103A1 (fr) | 1988-08-25 |
Family
ID=12436632
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP1987/000601 Ceased WO1988006103A1 (fr) | 1987-02-17 | 1987-08-10 | Tissu tisse en mailles pour cadre d'impression |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US4959260A (ja) |
| EP (1) | EP0311687B1 (ja) |
| KR (1) | KR950008185B1 (ja) |
| CN (1) | CN1018812B (ja) |
| DE (1) | DE3776343D1 (ja) |
| WO (1) | WO1988006103A1 (ja) |
Families Citing this family (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO1992005958A1 (en) * | 1990-10-03 | 1992-04-16 | Newman Donald E | Improved screen material for and method of screen printing |
| EP0592215B1 (en) * | 1992-10-09 | 1998-08-12 | Riso Kagaku Corporation | Heat-sensitive stencil sheets and process for producing the same |
| JP3313177B2 (ja) * | 1993-04-01 | 2002-08-12 | 理想科学工業株式会社 | 孔版印刷機用円筒状版胴 |
| US5473981A (en) * | 1993-07-16 | 1995-12-12 | Asahi Glass Company Ltd. | Screen printing plate |
| JP3078225B2 (ja) * | 1996-03-22 | 2000-08-21 | 鐘紡株式会社 | 芯鞘複合フィラメントを使用したメッシュ状布帛からなるスクリーン状メッキ品及びロータリースクリーン用シリンダー |
| JPH10291378A (ja) * | 1997-04-17 | 1998-11-04 | Riso Kagaku Corp | 感熱孔版原紙 |
| KR100260138B1 (ko) * | 1997-12-31 | 2000-07-01 | 구자홍 | 재기록메모리의자동설정방법 |
| CN1193121C (zh) * | 1999-01-11 | 2005-03-16 | 钟纺株式会社 | 网纱用聚酯单丝 |
| MY133638A (en) * | 1999-10-18 | 2007-11-30 | Stork Screens B V A Dutch Company | Printing forme for rotary screen printing made from fibre-reinforced plastics material |
| KR100375246B1 (ko) * | 2001-04-26 | 2003-03-06 | 주식회사 코오롱 | 세탁 및 일광견뢰도가 우수한 극세사 직물 |
| US7763410B2 (en) * | 2003-11-18 | 2010-07-27 | Ricoh Company, Ltd. | Electrophotographic developing carrier, associated apparatus and methodology of classification and application |
| US20060222828A1 (en) * | 2005-04-01 | 2006-10-05 | John Boyle & Company, Inc. | Recyclable display media |
| KR101028577B1 (ko) * | 2008-12-11 | 2011-04-12 | 웅진케미칼 주식회사 | 원착사를 포함하는 스크린용 원단 |
| KR20100133834A (ko) * | 2009-06-12 | 2010-12-22 | 웅진케미칼 주식회사 | 저융점사를 포함하는 원단 |
| CN102677257B (zh) * | 2012-06-01 | 2014-08-06 | 宁波维科丝网有限公司 | 一种用于触摸屏制造的网布及其制造方法 |
| JP6851075B2 (ja) * | 2016-09-15 | 2021-03-31 | ユニチカ株式会社 | 成型用メッシュ織物の製造方法 |
| CN110214088A (zh) * | 2016-12-06 | 2019-09-06 | 株式会社Nbc纱网技术 | 丝网版及其制造方法 |
| KR102098718B1 (ko) * | 2017-12-21 | 2020-04-08 | 코오롱글로텍주식회사 | 발포 프린팅 방법 |
| KR102688797B1 (ko) * | 2018-01-29 | 2024-07-29 | 도레이 카부시키가이샤 | 액정 폴리에스테르 섬유를 포함하는 메쉬 직물 |
| CN113122024B (zh) * | 2021-03-29 | 2022-04-15 | 苏州大学 | 一种纳米片层状炭黑乳液及其制备方法和应用 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS59159349A (ja) * | 1983-03-01 | 1984-09-08 | Toray Ind Inc | 印刷用スクリ−ン紗 |
| JPS59207289A (ja) * | 1983-05-11 | 1984-11-24 | Toray Ind Inc | スクリ−ン紗用ポリエステルモノフイラメント複合糸 |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1093392A (ja) * | 1955-05-03 | |||
| US3085904A (en) * | 1960-03-28 | 1963-04-16 | Joseph R Ehrlich | Polyester printing screen |
| FR1435095A (fr) * | 1965-02-22 | 1966-04-15 | Union Gazes A Bluter L | Perfectionnement aux tissus utilisés pour les pochoirs d'impression au cadre et de sérigraphie |
| DE1546065A1 (ja) * | 1966-11-26 | |||
| AT298520B (de) * | 1969-02-27 | 1972-05-10 | Zimmer J Klagenfurter Maschine | Verfahren zum Herstellen von unbemusterten Rundschablonen für Schablonendruckwerke |
| JPS525304A (en) * | 1975-07-01 | 1977-01-17 | Nippon Filcon Kk | Fabric for paper screening |
| CH648789A5 (de) * | 1980-10-03 | 1985-04-15 | Schweizerische Seidengaze | Verfahren zur verkuerzung der belichtungszeit bei der photochemischen musteruebertragung auf lichtempfindliche schichten. |
| JPS59143688A (ja) * | 1983-02-07 | 1984-08-17 | Toray Ind Inc | 印刷用制電性スクリーン紗 |
| US4824717A (en) * | 1987-01-07 | 1989-04-25 | Shin-Etsu Chemical Co., Ltd. | Mesh screen of polyester filaments for screen printing |
-
1987
- 1987-08-10 EP EP87905284A patent/EP0311687B1/en not_active Expired - Lifetime
- 1987-08-10 WO PCT/JP1987/000601 patent/WO1988006103A1/ja not_active Ceased
- 1987-08-10 DE DE8787905284T patent/DE3776343D1/de not_active Expired - Lifetime
- 1987-08-10 KR KR1019880701294A patent/KR950008185B1/ko not_active Expired - Lifetime
- 1987-08-10 US US07/269,186 patent/US4959260A/en not_active Expired - Lifetime
- 1987-08-18 CN CN87106381A patent/CN1018812B/zh not_active Expired
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS59159349A (ja) * | 1983-03-01 | 1984-09-08 | Toray Ind Inc | 印刷用スクリ−ン紗 |
| JPS59207289A (ja) * | 1983-05-11 | 1984-11-24 | Toray Ind Inc | スクリ−ン紗用ポリエステルモノフイラメント複合糸 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP0311687A4 * |
Also Published As
| Publication number | Publication date |
|---|---|
| KR890700477A (ko) | 1989-04-25 |
| EP0311687A4 (en) | 1989-05-30 |
| DE3776343D1 (de) | 1992-03-05 |
| US4959260A (en) | 1990-09-25 |
| EP0311687A1 (en) | 1989-04-19 |
| KR950008185B1 (ko) | 1995-07-26 |
| CN1018812B (zh) | 1992-10-28 |
| CN87106381A (zh) | 1988-08-31 |
| EP0311687B1 (en) | 1992-01-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4959260A (en) | Mesh fabric for printing screen | |
| JP6975171B2 (ja) | スクリーン版およびその製造方法 | |
| JP2603481B2 (ja) | 印捺スクリーン用メッシュ織物 | |
| JPH0637117B2 (ja) | 印捺スクリ−ン用メツシユ織物 | |
| WO1997036038A1 (en) | Screen-like plated article comprising mesh-like fabric using sheath-core composite filaments and cylinder for rotary screen | |
| JP4661501B2 (ja) | スクリーン紗用モノフィラメント | |
| WO2020067224A1 (ja) | スクリーン紗用ポリエステルモノフィラメントおよびダイレクトデジタル製版用メッシュ織物 | |
| JP3998090B2 (ja) | スクリーン紗用ポリエステルモノフィラメント | |
| JP2969380B2 (ja) | 印刷スクリーン用メッシュ織物及びその製法 | |
| JP3778086B2 (ja) | スクリーン紗用ポリエステルモノフィラメントおよび製造方法 | |
| JP3166381B2 (ja) | 印刷用スクリーン紗 | |
| JP2005240266A (ja) | スクリーン紗用ポリエステルモノフィラメント | |
| JP2007332504A (ja) | スクリーン紗用三層芯鞘複合ポリエステルモノフィラメント | |
| JPH06278383A (ja) | 印刷用スクリーン紗 | |
| JP2005047020A (ja) | スクリーン紗用ポリエステルモノフィラメント | |
| JP2939015B2 (ja) | 印刷用スクリーン紗の製造方法 | |
| JPH05125638A (ja) | スクリーン紗織物 | |
| JPH0647315B2 (ja) | ポリエステルからなるスクリ−ン紗の製造方法 | |
| JPH04305495A (ja) | スクリーン紗の製造方法 | |
| JP7045297B2 (ja) | スクリーン紗用モノフィラメント及びその製造方法 | |
| JP2018111311A (ja) | スクリーン版 | |
| JP2006241632A (ja) | スクリーン紗用モノフィラメント | |
| JPS62263381A (ja) | 透明織物及びその製造方法 | |
| JP2004262007A (ja) | スクリーン紗 | |
| JP3419077B2 (ja) | 感熱孔版印刷用原紙 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| AK | Designated states |
Kind code of ref document: A1 Designated state(s): KR US |
|
| AL | Designated countries for regional patents |
Kind code of ref document: A1 Designated state(s): CH DE FR GB IT |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1987905284 Country of ref document: EP |
|
| WWP | Wipo information: published in national office |
Ref document number: 1987905284 Country of ref document: EP |
|
| WWG | Wipo information: grant in national office |
Ref document number: 1987905284 Country of ref document: EP |