WO2006006992A1 - Chromium plating method - Google Patents
Chromium plating method Download PDFInfo
- Publication number
- WO2006006992A1 WO2006006992A1 PCT/US2005/012816 US2005012816W WO2006006992A1 WO 2006006992 A1 WO2006006992 A1 WO 2006006992A1 US 2005012816 W US2005012816 W US 2005012816W WO 2006006992 A1 WO2006006992 A1 WO 2006006992A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- chromium
- bath
- sulphate
- electrolyte
- trivalent chromium
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D21/00—Processes for servicing or operating cells for electrolytic coating
- C25D21/16—Regeneration of process solutions
- C25D21/18—Regeneration of process solutions of electrolytes
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D17/00—Constructional parts, or assemblies thereof, of cells for electrolytic coating
- C25D17/10—Electrodes, e.g. composition, counter electrode
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D3/00—Electroplating: Baths therefor
- C25D3/02—Electroplating: Baths therefor from solutions
- C25D3/04—Electroplating: Baths therefor from solutions of chromium
- C25D3/06—Electroplating: Baths therefor from solutions of chromium from solutions of trivalent chromium
Definitions
- the present invention relates to a chromium plating method utilizing trivalent chromium (chromium III). More specifically, the present invention relates to an electrolyte chromium bath and method to achieve both decorative and high impact industrial trivalent chromium plating.
- Chromium plating is an electrochemical process well-known in the art. There are two general types of chromium plating, hard chromium plating and decorative chromium plating.
- Hard chromium plating includes application of a heavy coating of chromium onto steel items typically to prevent wear, and exists in thicknesses in the thousandths of an inch (10-1000 ⁇ m).
- Decorative chromium plating applies a much thinner layer of chromium, in millionths of inch (0.25-1.0 ⁇ m), providing an extremely thin but hard coating for aesthetic purposes to achieve a shiny, reflective surface and protect against tarnish, corrosion and scratching of the metal beneath.
- Chromium plating typical employs hexavalent chromium (chromium Vl) a highly toxic material and suspected carcinogen.
- hexavalent chromium produces hazardous sludge and requires use of expensive chemicals to reduce the waste to a nonhazardous form.
- Hexavalent chromium also poses an environmental risk as it mat escape through spill and leaks and a health risk to individuals working with the material as hexavalent chromium solution is carried by hydrogen gas mist which is generated through the plating process, particular when performing hard chromium plating.
- trivalent chromium is a desirable alternative with lower waste treatment and air scrubbing costs.
- Trivalent chromium solutions are instable. Trivalent chromium may be oxidized to hexavalent chromium at the anode which results in an inhibition of the cathode process. Often, anode and cathode must be separated to avoid this problem but in turn this reduces practical use of this method of chrome plating. Trivalent chromium plating is problematic as neutral salts tend to build up in the plating solution and reduce efficiency. These difficulties limit the use of trivalent chromium plating to thin coating applications. While pulse current plating has been employed to obtain thicker layers, it does not produce the desired corrosion-resistant coating.
- the present invention relates to a method of electrolytically plating a layer of metallic chromium on a substrate comprising providing an electrolyte bath of a trivalent chromium, an oxalate, aluminum sulphate, and sodium fluoride, passing a current through the bath from an anode to a cathode which receives a substrate, maintaining the electrolyte bath at a desired temperature and a desired pH and depositing the trivalent chromium onto the substrate at a desired rate.
- the present invention relates to a electrolyte bath for trivalent chromium plating comprising a trivalent chromium source, an oxalate, aluminum sulphate, and sodium fluoride, wherein the bath operates at a desired temperature and a desired pH.
- FIG. 1 is a schematic view of one advantageous embodiment of the present invention.
- the present invention achieves both decorative and hard plating of trivalent chromium with the advantages of reducing environmental hazards associated with hexavalent chromium and creating a higher level of chrome output which is applicable to both decorative and high-impact industrial hard trivalent chromium plating.
- the present invention is based upon the finding that use of particular ligands with chromium III assures stability of the aqueous electrolyte solution and high speed of inter-sphere electron jump, which results in high speed of cathodic reduction from the chromium III complex.
- the catalytic effect of the ligand increases chrome output and provides for thick plating of metal substrates such as steel, copper, and nickel as well as other metals which are first treated prior to chromium plating.
- preferred ligands are oxalates, specifically potassium oxalate or sodium oxalate.
- the aqueous electrolyte bath is prepared in enameled vessel equipped with heating element and mixer, using distilled or deionized water in volume of 40% less than the desired volume of electrolyte. The following components are used to form the bath.
- the electrolyte plating bath preferably comprises:
- NaF from about 5 to about 30 g/l.
- the electrolyte solution most preferably comprises:
- Na 2 C 2 O 4 or K 2 C 2 O 4 from about 30 to about 35 g/l
- NaF from about 15 to about 20 g/l.
- Preferable operational conditions of the bath to achieve high-rate industrial hard chromium plating include a temperature of from about 4O 0 C to about 5O 0 C and most preferably of from about 46 0 C to about 48 0 C.
- the pH of the electrolyte bath is maintained preferably from about 0.9 to about 2.2 and most preferably from about 1.1 to 1.3.
- the aforementioned conditions guarantee high-quality chrome-plating at a rate of approximately 3 ⁇ m/min, with superior thickness of approximately 100 ⁇ m and current efficiency of about 35 to 40%.
- the composition of the aqueous electrolyte solution for the plating bath preferably comprises:
- NaF from about 5 to about 30 g/I.
- the electrolyte solution more preferably comprises:
- NaF from about 15 to about 20 g/I.
- Preferable operational conditions of the bath to achieve decorative chromium plating include temperature of from about 10° C to about 40° and most preferably of from about 33 0 C to about 37 0 C.
- the pH is preferably from about 0.9 to about 2.2 and most preferably from about 1.8 to 2.2.
- the aforementioned conditions achieve decorative chromium-plating at a rate of about 0.6- 0.7 ⁇ m/min.
- the preferable and most preferable components of the electrolyte solution for a high impact industrial chromium plating bath and decorative chromium plating bath of the present invention are of identical ranges.
- the significant variation between high impact and decorative chromium plating exists in the operating conditions of the bath, specifically the parameters for the pH, temperature and current density.
- the pH and electricity are adjusted accordingly to one another.
- pH and current density are corresponded to one another according to the following parameters as listed in Table 1.
- microparticles may be added to the plating solution to increase the hardness of the plating, increase adhesive features of the coating, and provide higher wear resistance.
- microparticles of diamond, corundum AbO 3 , or silicium carbide SiC may be used to increase hardness to 1300-1500 units.
- chromium potassium sulphate CrK(SO 4 ) 2 -12H 2 ⁇ it is less expensive than chromium sulphate Cr 2 (SO 4 ) 3 -6H 2 O of example 2, and yields the same results of chromium plating.
- the electrolyte is replenished by addition of chromium salt in the bath at appropriate intervals to compensate for its loss to plating.
- the result of 30 Ah/I of electricity passing through the bath for industrial high rate plating and 100 Ah/I for decorative plating causes a depletion of the trivalent chromium in the electrolyte bath of about 7 g/l that does not significantly affect the efficiency of the process as it only reduces the current efficiency of the electrolyte bath by about 3-5%.
- the electrolyte solution must be replenished with chromium potassium sulphate or chromium sulphate about every 3 hours, or as determined necessary by continual monitoring of the electricity inputted and the chromium deposited.
- the electrolyte solution is highly stable and may be utilized for an extended period of time, approximately ten years, before it must be discarded and replaced.
- the anode and cathode need not be separated from one another within the bath.
- Anodes are preferably platinized titanium sheets which prevent undesirable oxidation of trivalent chromium to hexavalent chromium. Such oxidation to hexavalent inhibits plating process.
- Platonized titanium anodes permit the chromium plating process to occur without separation of the bath into anode and cathode chambers.
- the anode to cathode ratio is preferably 1 :2.
- the component NaF serves to increase the current efficiency of the electrolyte bath by approximately 40%.
- the pH of the bath may be regulated.
- the bath electrolyte acidifies during operation.
- a base such as sodium hydroxide NaOH or sodium carbonate Na 2 CO 3 may be added.
- sodium carbonate is added as to form CO 2 which promotes electrolyte mixing, and consequently, accelerates the dissolving of formed hydroxides.
- the plating process results in the deposition of chrome with 36% of the current efficiency corresponding to the deposit of chromium on the cathode (substrate) and 64% of the current efficiency corresponding to the discharge of hydrogen. On the anode, oxygen is formed.
- the electrode processes are the following:
- the electrolyte bath is constructed of suitable material such as polypropylene or the like.
- the bath is equipped with a pipe made of stainless steel or the like disposed preferably at the bottom of the bath to carry a water supply through the bath.
- the pipe serves as a heating element, when hot water is passed there through to heat the electrolyte solution as needed or as a cooling system when cold water is passed there through to cool the electrolyte solution as needed.
- a temperature controller disposed within the bath monitors the hot and cold water supply rate to regulate the electrolyte temperature.
- the bath is also equipped with a filter that continual circulates electrolyte through bath.
- a filter that continual circulates electrolyte through bath.
- the latter must be equipped with the appropriate monitors to measure electric current intensity, voltage, bath temperature, pH of electrolyte and level of electrolyte in the bath.
- Anodes within the bath are made of a suitable material, preferably platinized titanium, in sheets having thickness of about 2-3 mm thickness.
- a suitable material preferably platinized titanium, in sheets having thickness of about 2-3 mm thickness.
- platinized titanium sheets permits conduction of chrome plating process without separation of the cathode and anode in separate chambers of the bath and eliminates anode oxidation of chromium III to chromium Vl which inhibits plating process.
- Anodes may be shaped according to the substrate/product which is being plated to ensure even distribution of cathode current over the surface of the substrate.
- Substrates are positioned within the bath at the cathode.
- the cathode (substrate) and anode are disposed within bath at a distance of 30-40mm.
- a suspension may be constructed and placed within the bath and the substrate fixed thereto.
- Suspensions are typically constructed from stainless steel and obtained from the appropriate manufacturers.
- the bath is equipped with the cover or umbrella for permitting free gas extraction via an on-board ventilation system.
- the electrolyte solution must be at least 150 mm and preferably 200 mm lower than the upper edge of the bath.
- Electric current intensity on the bath is set based on the area of substrate being plated in a given load and on the acceptable precipitation current density for given pH value.
- the volumic current density should not exceed 10 A/I.
- FIG. 1 shows the bath 10 generally including electrolyte solution contained within working part 12 of bath.
- the working part 12 of bath 10 is filled with the desired amount of electrolyte and the heating element is turned on.
- the suspensions with substrate are hung on cathode bars.
- Precipitation current and the cooling system equipped with automatic temperature regulator, are turned on. All initial figures, such as electric current intensity, voltage on the bath, pH level, and temperature and electrolyte level in the bath are recorded.
- Maintenance of the bath consists in timely replenishment of chromium salt and maintaining desired pH of the electrolyte by means of introduction of a base such as Na 2 CO 3 .
- Chromium salt and pH regulating base is introduced by injection at 30 through a small chamber 22 at one end of the bath 10.
- Small chamber 22 is connected to the working part 12 of the bath 10 by means of a special separator 14 which prevents the direct injection into the working part 12 of the bath.
- the present invention provides an electrolyte bath and plating method utilizing the bath which achieves a fast rate of hard industrial chromium plating, up to 3 ⁇ m per minute , which is an environmentally-safe alternative to hexavalent chromium plating. Additionally, the electrolyte bath and plating method are especially useful in chromium plating of "pick-and-place" devices and machines and cylindrical rods, specifically those up to 20 m long and 20-30 cm in diameter which require chromium coatings of a thickness of 80-100 ⁇ m and greater. The present invention provides superior results in achieving uniform thickness, when plating uniform complex parts, such as long cylindrical parts.
- the present invention provides an electrolyte bath and plating method utilizing the bath which achieves a rate of decorative chromium plating , up to 0,7 ⁇ m per minute, which is an environmentally-safe alternative to hexavalent chromium plating. Additionally, the electrolyte bath and plating method are especially useful in chromium plating of parts, with most complex configurations. The present invention provides superior results in achieving uniform thickness when plating complex parts.
- a chromium plating bath according to the present invention was prepared accordingly as discussed in the following examples.
- the bath is prepared in an enameled vessel equipped with heating element and mixer, using distilled or deionized water in volume of 40% less than the desired volume of electrolyte.
- all components as set forth above in Examplei and 2, are placed in the bath, except for the chromium salt component, are introduced into the vessel and mixed with heat, preferably bringing the temperature of the solution to preferably 92 - 93 0 C.
- chromium salt preferably chromium potassium sulphate or chromium sulphate is introduced into the solution and the solution is further mixed with heat for approximately 15-20 minutes.
- the pH level is adjusted accordingly as is discussed herein and electrolyte is ready for use in operation of the bath for chromium plating.
- the time of deposition was 33 minutes.
- the time of deposition was 33 minutes.
- the time of deposition was 20 minutes.
- the trivalent chromium plating electrolyte bath and method of the present invention is identical to that of standard hexavalent chrome electrolyte baths known in the art of, while overcoming the problems that exist in the art.
- the present invention achieves hardness of the plating of 1000 units (1000HV/100g).
- the addition of microparticles to electrolytic plating solution increases hardness to 1300-1500 units.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Electroplating And Plating Baths Therefor (AREA)
- Electroplating Methods And Accessories (AREA)
Abstract
Description

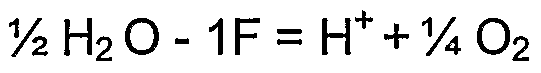
Claims
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2007518037A JP2008506035A (en) | 2004-06-24 | 2005-04-14 | Chrome plating method |
| EP05736623A EP1784527A4 (en) | 2004-06-24 | 2005-04-14 | Chromium plating method |
| CA002579670A CA2579670A1 (en) | 2004-06-24 | 2005-04-14 | Chromium plating method |
| MX2007000163A MX2007000163A (en) | 2004-06-24 | 2005-04-14 | Chromium plating method. |
| BRPI0512577-4A BRPI0512577A (en) | 2004-06-24 | 2005-04-14 | chrome plating method |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US10/876,073 US7052592B2 (en) | 2004-06-24 | 2004-06-24 | Chromium plating method |
| US10/876,073 | 2004-06-24 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2006006992A1 true WO2006006992A1 (en) | 2006-01-19 |
Family
ID=35504438
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/US2005/012816 Ceased WO2006006992A1 (en) | 2004-06-24 | 2005-04-14 | Chromium plating method |
Country Status (8)
| Country | Link |
|---|---|
| US (2) | US7052592B2 (en) |
| EP (1) | EP1784527A4 (en) |
| JP (1) | JP2008506035A (en) |
| CN (1) | CN1993500A (en) |
| BR (1) | BRPI0512577A (en) |
| CA (1) | CA2579670A1 (en) |
| MX (1) | MX2007000163A (en) |
| WO (1) | WO2006006992A1 (en) |
Families Citing this family (28)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5050048B2 (en) * | 2006-03-31 | 2012-10-17 | アトテック・ドイチュラント・ゲーエムベーハー | Crystalline chromium deposits |
| DE102006022722B4 (en) | 2006-05-12 | 2010-06-17 | Hueck Engraving Gmbh & Co. Kg | Method and device for surface structuring of a press plate or an endless belt |
| CN101096769A (en) * | 2006-06-26 | 2008-01-02 | 比亚迪股份有限公司 | A method of electroplating |
| KR100810244B1 (en) * | 2006-08-08 | 2008-03-06 | 삼성전자주식회사 | Keys on handheld terminal |
| WO2009046181A1 (en) | 2007-10-02 | 2009-04-09 | Atotech Deutschland Gmbh | Crystalline chromium alloy deposit |
| CN101768768B (en) * | 2008-12-26 | 2012-01-25 | 比亚迪股份有限公司 | Aluminum alloy cyanide-free and nickel-free electroplating method and electroplating products thereof |
| JP5394953B2 (en) * | 2010-03-08 | 2014-01-22 | 日本エレクトロプレイテイング・エンジニヤース株式会社 | Gold plating method using gold sulfite plating solution |
| US8273235B2 (en) | 2010-11-05 | 2012-09-25 | Roshan V Chapaneri | Dark colored chromium based electrodeposits |
| CN103510130B (en) * | 2012-06-26 | 2016-08-24 | 武汉材料保护研究所 | Trivalent hard chromium electro-plating method |
| CN103628098A (en) * | 2012-08-29 | 2014-03-12 | 上海宝钢工业技术服务有限公司 | Additive of electrolyte for trivalent chromium electroplating of thick chromium plating layer, and electrolyte preparation method |
| CO7190036A1 (en) * | 2014-02-11 | 2015-02-19 | Garcia Carlos Enrique Muñoz | Continuous trivalent chrome plating process |
| CH710741A2 (en) * | 2015-01-30 | 2016-08-15 | Acrom S A | Ecological procedure for continuous chrome plating of bars and relative equipment. |
| CN104746111A (en) * | 2015-04-27 | 2015-07-01 | 南京宁美表面技术有限公司 | Trivalent chromium electroplating chromium solution and electroplating method |
| CN105063676A (en) * | 2015-08-17 | 2015-11-18 | 内蒙古第一机械集团有限公司 | Method for electroplating hard chromium by using trivalent chromium |
| CN105239139B (en) * | 2015-11-16 | 2017-04-26 | 中船重工中南装备有限责任公司 | Continuous chromeplating device and method for large rod |
| CN105386089B (en) * | 2015-12-25 | 2018-04-24 | 武汉迪赛环保新材料股份有限公司 | A kind of Trivalent hard chromium electroplating solution and its application in hard chrome plating |
| US20170314153A1 (en) * | 2016-05-02 | 2017-11-02 | The Boeing Company | Trivalent chromium plating formulations and processes |
| CN106119906B (en) * | 2016-07-18 | 2018-10-02 | 浙江恩森化学科技有限公司 | The high anti-corrosion trivalent chromium plating chromium of environment-friendly type and chromium-phosphorus alloy solution for magnesium alloy |
| US10246593B2 (en) | 2016-07-20 | 2019-04-02 | The Boeing Company | Sol-gel coating compositions including corrosion inhibitor-encapsulated layered double hydroxide and related processes |
| US10246594B2 (en) | 2016-07-20 | 2019-04-02 | The Boeing Company | Corrosion inhibitor-incorporated layered double hydroxide and sol-gel coating compositions and related processes |
| US10428226B2 (en) | 2016-07-20 | 2019-10-01 | The Boeing Company | Sol-gel coating compositions and related processes |
| US10421869B2 (en) | 2017-01-09 | 2019-09-24 | The Boeing Company | Sol-gel coating compositions including corrosion inhibitor-encapsulated layered metal phosphates and related processes |
| CN108531902A (en) * | 2018-05-09 | 2018-09-14 | 昆山秀博表面处理材料有限公司 | Fluorine-free and environment-friendly trivalent blue-white chromating liquid and preparation method thereof |
| CN109537036B (en) * | 2019-01-05 | 2020-10-20 | 上海裕继金属制品有限公司 | Auxiliary system of electroplating process |
| DE102019109354A1 (en) * | 2019-04-09 | 2020-10-15 | Thyssenkrupp Rasselstein Gmbh | Process for passivating the surface of a black plate or a tin plate and an electrolysis system for carrying out the process |
| FI129420B (en) * | 2020-04-23 | 2022-02-15 | Savroc Ltd | An aqueous electroplating bath |
| CN111663159A (en) * | 2020-06-23 | 2020-09-15 | 上海理工大学 | Preparation method of wear-resistant silicon carbide doped composite coating |
| FR3150818B1 (en) * | 2023-07-07 | 2026-03-27 | Institut De Recherche Tech Materiaux Metallurgie Procedes | Hard chrome plating process using trivalent chromium |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3106484A (en) * | 1961-01-04 | 1963-10-08 | Cowles Chem Co | Metal treating |
| US4038160A (en) * | 1975-07-03 | 1977-07-26 | Albright & Wilson Limited | Method of regenerating a chromium electroplating bath |
| US4359345A (en) * | 1981-04-16 | 1982-11-16 | Occidental Chemical Corporation | Trivalent chromium passivate solution and process |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1527095A (en) * | 1923-10-12 | 1925-02-17 | Lawrence C Turnock | Method and apparatus for coating |
| FR2529581A1 (en) | 1982-06-30 | 1984-01-06 | Armines | ELECTROLYSIS BATH BASED ON TRIVALENT CHROME |
| US5958207A (en) | 1994-10-01 | 1999-09-28 | Heidelberger Druckmaschinen Ag | Process for applying a surface coating |
| JP3188361B2 (en) | 1994-06-27 | 2001-07-16 | ペルメレック電極株式会社 | Chrome plating method |
| FR2726289B1 (en) * | 1994-10-28 | 1997-03-28 | Floquet Monopole | PROCESS FOR ELECTRODEPOSITION OF A CHROME COATING COMPRISING SOLID INCLUSIONS AND BATH IMPLEMENTED IN THIS PROCESS |
| JP3810043B2 (en) | 1998-09-30 | 2006-08-16 | ペルメレック電極株式会社 | Chrome plating electrode |
| JP3332373B1 (en) | 2001-11-30 | 2002-10-07 | ディップソール株式会社 | A treatment solution for forming a hexavalent chromium-free rust preventive film on zinc and zinc alloy plating, a hexavalent chromium-free rust preventive film, and a method for forming the same. |
| US6887321B2 (en) | 2002-05-22 | 2005-05-03 | United Technologies Corporation | Corrosion resistant surface treatment for structural adhesive bonding to metal |
| RU2231581C1 (en) * | 2002-12-25 | 2004-06-27 | Федеральное государственное унитарное предприятие "Всероссийский научно-исследовательский институт авиационных материалов" | Electrolyte of chromium plating and a method of chromium coatings plating on steel parts |
-
2004
- 2004-06-24 US US10/876,073 patent/US7052592B2/en not_active Expired - Fee Related
-
2005
- 2005-04-14 BR BRPI0512577-4A patent/BRPI0512577A/en not_active IP Right Cessation
- 2005-04-14 MX MX2007000163A patent/MX2007000163A/en not_active Application Discontinuation
- 2005-04-14 EP EP05736623A patent/EP1784527A4/en not_active Withdrawn
- 2005-04-14 WO PCT/US2005/012816 patent/WO2006006992A1/en not_active Ceased
- 2005-04-14 CN CNA2005800252406A patent/CN1993500A/en active Pending
- 2005-04-14 JP JP2007518037A patent/JP2008506035A/en not_active Withdrawn
- 2005-04-14 CA CA002579670A patent/CA2579670A1/en not_active Abandoned
-
2006
- 2006-01-30 US US11/342,398 patent/US20060118427A1/en not_active Abandoned
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3106484A (en) * | 1961-01-04 | 1963-10-08 | Cowles Chem Co | Metal treating |
| US4038160A (en) * | 1975-07-03 | 1977-07-26 | Albright & Wilson Limited | Method of regenerating a chromium electroplating bath |
| US4359345A (en) * | 1981-04-16 | 1982-11-16 | Occidental Chemical Corporation | Trivalent chromium passivate solution and process |
Non-Patent Citations (2)
| Title |
|---|
| EDIGARYAN ET AL: "Effect of Fluoride Ions on Chromium Deposition From Sulfuric Acid Soultion of Cr(III)", PROTECTION OF METALS, vol. 35, no. 1, 1999, pages 1 - 3, XP000803559 * |
| See also references of EP1784527A4 * |
Also Published As
| Publication number | Publication date |
|---|---|
| EP1784527A1 (en) | 2007-05-16 |
| CN1993500A (en) | 2007-07-04 |
| EP1784527A4 (en) | 2007-09-19 |
| BRPI0512577A (en) | 2008-03-25 |
| CA2579670A1 (en) | 2006-01-19 |
| JP2008506035A (en) | 2008-02-28 |
| US20050284769A1 (en) | 2005-12-29 |
| US7052592B2 (en) | 2006-05-30 |
| MX2007000163A (en) | 2007-03-26 |
| US20060118427A1 (en) | 2006-06-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US7052592B2 (en) | Chromium plating method | |
| EP2054539B1 (en) | Method for deposition of chromium layers as hard- chrome plating, electroplating bath and hard- chrome surfaces | |
| CN104911676B (en) | Alkaline electro plating bath with filtration membrane | |
| Rashwan et al. | Electrodeposition and characterization of thin layers of Zn–Co alloys obtained from glycinate baths | |
| JPS5930797B2 (en) | Trivalent chromium electrolyte using vanadium reducing agent and its method | |
| JPH0570718B2 (en) | ||
| CN103510130A (en) | Trivalent hard chromium electroplating method | |
| WO2012067725A1 (en) | Electrolytic dissolution of chromium from chromium electrodes | |
| JPWO2013047340A1 (en) | Method for removing rare earth impurities in electro nickel plating solution | |
| Zeng et al. | A review of recent patents on trivalent chromium plating | |
| JP2002241986A (en) | Ni-WP alloy plating solution and continuous plating method thereof | |
| Rashwan | Electrodeposition of Zn–Cu coatings from alkaline sulphate bath containing glycine | |
| CN110446802A (en) | Method for the electrolytic deposition of a chromium or chromium alloy layer on at least one substrate | |
| JP2002322599A (en) | Method for plating with trivalent chromium | |
| JP5688145B2 (en) | Method and apparatus for adjusting the pH of nickel | |
| KR20070031411A (en) | Chrome plating method | |
| JPH05222599A (en) | Method and device for aluminum fused-salt plating | |
| JP2023507479A (en) | Method and system for depositing zinc-nickel alloys on substrates | |
| US20260022489A1 (en) | Method for controlling the chromium feed in an electrolysis process for producing chromium layers, and an electrolysis cell for this purpose | |
| Campbell et al. | Some uses of pyrophosphates in metal finishing part II. Cobalt-tungsten alloys to zinc, including pretreatment for magnesium | |
| JPS62139900A (en) | Electrolytic plating device | |
| Kakareka et al. | Peculiarities of electroless deposition of Ni-WP alloy on aluminum | |
| CA1220161A (en) | Metal recovery from spent electroless and immersion plating solutions | |
| Boiciuc et al. | Technologies and Installation for Electrochemical Hardening of Wear Surfaces | |
| UA5672U (en) | A method for nickel-plating aluminium alloys |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| AK | Designated states |
Kind code of ref document: A1 Designated state(s): AE AG AL AM AT AU AZ BA BB BG BR BW BY BZ CA CH CN CO CR CU CZ DE DK DM DZ EC EE EG ES FI GB GD GE GH GM HR HU ID IL IN IS JP KE KG KM KP KR KZ LC LK LR LS LT LU LV MA MD MG MK MN MW MX MZ NA NI NO NZ OM PG PH PL PT RO RU SC SD SE SG SK SL SM SY TJ TM TN TR TT TZ UA UG US UZ VC VN YU ZA ZM ZW |
|
| AL | Designated countries for regional patents |
Kind code of ref document: A1 Designated state(s): GM KE LS MW MZ NA SD SL SZ TZ UG ZM ZW AM AZ BY KG KZ MD RU TJ TM AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LT LU MC NL PL PT RO SE SI SK TR BF BJ CF CG CI CM GA GN GQ GW ML MR NE SN TD TG |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application | ||
| WWE | Wipo information: entry into national phase |
Ref document number: MX/a/2007/000163 Country of ref document: MX Ref document number: 2579670 Country of ref document: CA |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2007518037 Country of ref document: JP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWW | Wipo information: withdrawn in national office |
Ref document number: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 159/KOLNP/2007 Country of ref document: IN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2005736623 Country of ref document: EP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1020077001672 Country of ref document: KR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 200580025240.6 Country of ref document: CN |
|
| WWP | Wipo information: published in national office |
Ref document number: 1020077001672 Country of ref document: KR |
|
| WWP | Wipo information: published in national office |
Ref document number: 2005736623 Country of ref document: EP |
|
| ENP | Entry into the national phase |
Ref document number: PI0512577 Country of ref document: BR |