WO2012108442A1 - Procédé de soudage - Google Patents
Procédé de soudage Download PDFInfo
- Publication number
- WO2012108442A1 WO2012108442A1 PCT/JP2012/052780 JP2012052780W WO2012108442A1 WO 2012108442 A1 WO2012108442 A1 WO 2012108442A1 JP 2012052780 W JP2012052780 W JP 2012052780W WO 2012108442 A1 WO2012108442 A1 WO 2012108442A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- cylindrical member
- build
- welding
- cylindrical
- welded
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K33/00—Specially-profiled edge portions of workpieces for making soldering or welding connections; Filling the seams formed thereby
- B23K33/004—Filling of continuous seams
- B23K33/006—Filling of continuous seams for cylindrical workpieces
Definitions
- the present invention relates to a welding method in which cylindrical members are joined together by welding in a state where the cylindrical members are temporarily joined together by a connecting member.
- a pipe groove deformation correcting jig for performing centering between a pipe and a pipe before welding the groove formed by abutting the pipe and the pipe is known (for example, see Patent Document 1). ).
- the pipe bend deformation correction jig is modified to a perfect circle by attaching a jig body consisting of an upper frame and a lower frame to the outer periphery of the pipe, and the jig bodies attached to the corrected pipe are connected together. By doing so, the tube is centered.
- an object of the present invention is to provide a welding method capable of simply temporarily joining cylindrical members with a connecting member while satisfying quality requirements for the cylindrical members.
- the welding method of the present invention is a welding method in which the first cylindrical member and the second cylindrical member are finally joined by welding in a state where the first cylindrical member and the second cylindrical member are temporarily joined by the connecting member,
- the one cylindrical member and the second cylindrical member are made of a first material that requires preheating at the time of welding, and the connecting member is made of a second material that does not need preheating at the time of welding, and the end portion of the first cylindrical member
- Overlay welding is performed using a filler material made of the first material on the first cylindrical member and the second cylindrical member, with a groove portion formed by abutting the end portion of the second cylindrical member in the axial direction.
- one end portion of the connecting member and the first build-up portion Are joined via the first intervening portion made of the second material, and the other end of the connecting member and the second A connecting member joining step for temporarily joining the connecting member to the first cylindrical member and the second cylindrical member by joining the raised portion via the second intervening portion made of the second material.
- the first build-up portion can be formed on the first cylindrical member, and the second build-up portion can be formed on the second cylindrical member.
- each cylindrical member can be joined with a connecting member via each build-up part used as a welding material suitable for a cylindrical member, the 2nd material which is a different material is welded with respect to each cylindrical member. There is no.
- a connection member can be joined to each build-up part via each interposition part which becomes the same material, a connection member is temporarily joined to each cylindrical member via each build-up part, without preheating a connection member. be able to.
- the connecting member can be simply temporarily joined to each cylindrical member while satisfying the quality requirements for the cylindrical member.
- the first interposition part is a first batting plate joined to the first build-up part
- the second interposition part is a second batting plate joined to the second build-up part
- overlay welding After the process, the first contact plate and the first build-up portion are welded using a filler material made of the second material, and the second contact plate and the second build-up portion are welded with the second material.
- a contact plate joining step for welding using the additive and in the connecting member joining step, welding one end portion of the connecting member and the first contact plate using a filler material made of the second material. It is preferable that the other end portion of the connecting member and the second contact plate are welded using a filler material made of the second material.
- each cover plate is welded to each build-up portion by welding. Install. And when a connection member is welded to each contact plate, a part of 2nd material which is a connection member melts into each contact plate, and is prevented from mixing with the 1st material which is a cylindrical member. Moreover, when removing each pad and each build-up part, each cylindrical member is not scraped off by removing within the build-up range of each build-up part.
- the build-up range of each build-up part is set to the outer edge part of each pad. It is possible to make the range along. Thereby, it is economical to minimize the build-up range of each build-up portion, and it is possible to suppress the thermal influence on each cylindrical member due to build-up welding.
- the filler material which welds each pad to each build-up part is suitable for each build-up part and each pad, and the necessity of preheating is according to the quality requirements of each build-up part.
- the first interposition part is a first welding part formed by welding one end of the connecting member and the first build-up part using a filler material made of the second material.
- the second intervening portion may be a second welded portion formed by welding the other end of the connecting member and the second build-up portion using a filler material made of the second material. preferable.
- each build-up portion by replacing each interposed portion with each welded portion instead of each contact plate, the place where the connecting member is attached becomes each build-up portion, so there is no need to provide each contact plate.
- the mounting welding of each contact plate can be omitted.
- each built-up part attached instead of each contact plate does not need preheating at the time of attachment welding of a connection member.
- each build-up portion is preheated in advance so that preheating is not required. It is preferable to perform build-up welding on each build-up part.
- the first material is low alloy steel and the second material is carbon steel.
- the first material is low alloy steel and the second material is carbon steel
- a connecting member suitable for each cylindrical member made of low alloy steel can be used.
- the connecting member can be simply temporarily joined to each cylindrical member without preheating the connecting member while satisfying the quality requirement for the cylindrical member.
- FIG. 1 is a front view of a pressure vessel welded by a welding method according to a first embodiment.
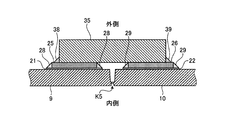
- FIG. 2 is a cross-sectional view of a temporarily joined portion that is temporarily joined by the welding method according to the first embodiment.
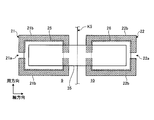
- FIG. 3 is a plan view of a temporarily joined portion that is temporarily joined by the welding method according to the first embodiment.
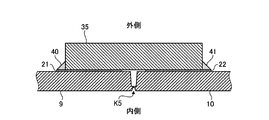
- FIG. 4 is a cross-sectional view of a temporarily joined portion that is temporarily joined by the welding method according to the second embodiment.
- the welding method according to the first embodiment is a welding method in which cylindrical members are welded to each other, and the cylindrical members are temporarily joined by a connecting plate (connecting member), and the cylindrical members are finally joined by welding in a temporarily joined state.
- a pressure vessel of a steam generator used in a pressurized water reactor is applied as an object to be welded.
- the description is applied to a pressure vessel.
- the present invention is not limited to the pressure vessel, and any member may be used as long as the cylindrical members are welded to each other.
- a pressure vessel to be welded will be described with reference to FIG.
- FIG. 1 is a front view of a pressure vessel welded by the welding method according to the first embodiment.
- the pressure vessel 1 is constituted by joining a plurality of cylindrical members, and the plurality of cylindrical members are made of low alloy steel.
- the left side in the figure is the upper side in the vertical direction
- the right side in the figure is the lower side in the vertical direction.
- the pressure vessel 1 is welded in a state where the axial direction of each cylindrical member is the horizontal direction.
- the pressure vessel 1 includes, as a plurality of cylindrical members, an upper hemispherical member 5, a first cylindrical member 6, a tapered member 7, a second cylindrical member 8, a third cylindrical member 9, a fourth cylindrical member 10, A lower hemispherical member 11 is provided.
- the cylindrical member described in the claims includes not only a cylindrical member but also a member having a cylindrical portion, and includes the upper hemispherical member 5, the tapered member 7, and the lower hemispherical member 11.
- the upper hemispherical member 5 has a cylindrical portion 5a formed on the lower side in the axial direction, and the upper side of the cylindrical portion 5a is formed in a hollow hemispherical shape. Further, the upper hemispherical member 5 is formed with an opening 5b that is open toward the outside on the upper side of the axial center thereof.
- the first cylindrical member 6 is formed in a cylindrical shape having the same diameter as the cylindrical portion 5 a of the upper hemispherical member 5.
- the first cylindrical member 6 is joined to the cylindrical portion 5 a on the upper side in the axial direction, which is the lower side of the upper hemispherical member 5.
- the pressure vessel 1 forms the groove part K1 by abutting the cylindrical part 5a of the upper hemispherical member 5 and the upper side of the first cylindrical member 6 in the axial direction, and welding the groove part K1.
- the weld M1 is formed.
- the taper member 7 is formed in a tapered shape that tapers from the upper side toward the lower side.
- the taper member 7 has an upper diameter that is the same as the lower diameter of the first cylindrical member 6, and a lower diameter that is the same as the upper diameter of the second cylindrical member 8. .
- the taper member 7 is joined to the lower side of the first cylindrical member 6 at the upper side in the axial direction. For this reason, the pressure vessel 1 is welded by forming a groove portion K2 by abutting the lower side of the first cylindrical member 6 and the upper side of the taper member 7 in the axial direction and welding the groove portion K2. Part M2 is formed.
- the second cylindrical member 8 is formed in a cylindrical shape having the same diameter as that of the lower side of the tapered member 7.
- the second cylindrical member 8 is joined to the lower side of the taper member 7 at the upper side in the axial direction. For this reason, the pressure vessel 1 is welded by forming the groove portion K3 by abutting the lower side of the taper member 7 and the upper side of the second cylindrical member 8 in the axial direction and welding the groove portion K3.
- Part M3 is formed.
- the third cylindrical member 9 is formed in a cylindrical shape having the same diameter as that of the second cylindrical member 8.
- the third cylindrical member 9 is joined to the lower side of the second cylindrical member 8 at the upper side in the axial direction.
- the pressure vessel 1 forms the groove part K4 by abutting the lower side of the second cylindrical member 8 and the upper side of the third cylindrical member 9 in the axial direction, and welding the groove part K4.
- the weld M4 is formed.
- the fourth cylindrical member 10 is formed in a cylindrical shape having the same diameter as the third cylindrical member 9.
- the fourth cylindrical member 10 is joined to the lower side of the third cylindrical member 9 on the upper side in the axial direction.
- the pressure vessel 1 forms the groove part K5 by abutting the lower side of the third cylindrical member 9 and the upper side of the fourth cylindrical member 10 in the axial direction, and welding the groove part K5.
- the weld M5 is formed.
- the lower hemispherical member 11 has a cylindrical portion 11a formed on the upper side in the axial direction, and the lower side of the cylindrical portion 11a is formed in a hollow hemispherical shape.
- the lower hemispherical member 11 is joined to the lower side of the fourth cylindrical member 10 on the upper side in the axial direction.
- the pressure vessel 1 forms a groove portion K6 by abutting the lower side of the fourth cylindrical member 10 and the upper side of the lower hemispherical member 11 in the axial direction, and welding the groove portion K6.
- a weld M6 is formed.
- the pressure vessel 1 joins the upper hemispherical member 5 and the first cylindrical member 6 at the welded part M1, joins the first cylindrical member 6 and the tapered member 7 at the welded part M2, and connects the tapered member 7 and the second cylindrical member 7 to the second.
- the cylindrical member 8 is joined at the welded part M3, the second cylindrical member 8 and the third cylindrical member 9 are joined at the welded part M4, and the third cylindrical member 9 and the fourth cylindrical member 10 are joined at the welded part M5. And it can form by joining the 4th cylindrical member 10 and the lower hemispherical member 11 in the welding part M6.
- the welds M1 to M6 are welded by the welding method of the first embodiment.
- the welding method of Example 1 is demonstrated.
- FIG. 2 is a cross-sectional view of a temporarily joined portion that is temporarily joined by the welding method according to the first embodiment.
- FIG. 3 is a plan view of a temporarily joined portion that is temporarily joined by the welding method according to the first embodiment.
- the welding method of Example 1 the case where the 3rd cylindrical member 9 and the 4th cylindrical member 10 are joined is demonstrated. Note that the welding method of the first embodiment is not limited to the joining of the third cylindrical member 9 and the fourth cylindrical member 10, but can be applied to any of the welded portions M1 to M6.
- the connecting plate 35 used in the welding method of Example 1 is made of carbon steel (second material).
- the cylindrical members 6 to 11 of the pressure vessel 1 are made of low alloy steel (first material)
- the connecting plate 35 and the cylindrical members 6 to 11 are made of different materials. ing.
- the connecting plate 35 As a characteristic of welding, when the carbon steel connecting plate 35 and the low-alloy steel cylindrical members 6 to 11 are directly joined, in order to ensure the welding quality of the cylindrical members 6 to 11 as products, that is, In order to prevent cracking of the cylindrical members 6 to 11, the connecting plate 35 needs to be preheated. At this time, when the connecting plate 35 is attached and welded in a state where the end portions of the cylindrical members 6 to 11 are axially abutted to form the groove portions K1 to K6, the cylindrical members 6 to 11 and the connecting plate 35 are attached to each other. Preheating means that the handling work of the preheating apparatus is complicated, that a large apparatus such as the pressure vessel 1 becomes a high place work, and the process of forming the groove portions K1 to K6 requires many personnel. In addition to the time required, the time until the preheating temperature is reached is a waiting time, which greatly impairs the economy and safety.
- the welding method of Example 1 in the temporary joining process, the build-up welding process, the contact plate joining process, the butting process, and the connecting plate joining process are sequentially performed.
- the build-up welding process that requires preheating, and the butting process and connection plate joining process that do not require preheating are performed separately to improve economy and safety.
- the filler metal made of low alloy steel of the same material as the third cylindrical member 9 and the fourth cylindrical member 10 is used.
- the filler metal is melted to perform build-up welding, so that the first wall is formed on the outer peripheral surface of the third cylindrical member 9 with the portion that becomes the groove portion K5 in the subsequent butting process.
- a built-up portion 21 is formed, and a second built-up portion 22 is formed on the outer peripheral surface of the fourth cylindrical member 10.
- the shape of the first build-up portion 21 and the second build-up portion 22 to be formed is a rectangular frame shape surrounded by four sides, and extends in the axial direction.
- the circumferentially central portions of the two sides are gap portions 21a and 22a that are not subjected to overlay welding. That is, the first build-up portion 21 and the second build-up portion 22 are provided with concave partial build-up portions 21b and 22b on both sides in the circumferential direction across the gap portions 21a and 22a. It is provided so that the hollow side of 22b opposes.
- a first contact plate (first interposed portion) 25 and a second contact plate (second interposed portion) 26 made of carbon steel are used, and the first contact plate 25 and the second caulking plate 26 are welded to the build-up portions 21 and 22 using a filler material made of carbon steel of the same material as the caulking plates 25 and 26.
- the size of each of the contact plates 25 and 26 is slightly larger than the inside of the four sides of each of the built-up portions 21 and 22.
- the cylindrical member 9.10 has a size that is necessary and sufficient for temporary joining.
- the first contact plate 25 is disposed on the first build-up portion 21, and the first build-up portion 21 and the first contact plate 25 are welded using a filler material of carbon steel.
- the first welded portion 28 is formed.
- the second contact plate 26 is disposed on the second build-up portion 22 and the second build-up portion 22 and the second contact plate 26 are welded using a carbon steel filler material.
- the second welded portion 29 is formed.
- the groove portion K5 is formed in the circumferential direction of the pressure vessel 1 by butting the third cylindrical member 9 and the fourth cylindrical member 10 in the axial direction. 2 and 3, the left side in the drawing is the third cylindrical member 9, and the right side in the drawing is the fourth cylindrical member 10.
- connection plate 35 made of carbon steel is used, and the connecting plate 35 is welded to the respective contact plates 25 and 26 without preheating using a filler material of carbon steel. Is done.
- the connection plate 35 has a rectangular parallelepiped block shape, and has a length that allows suspension between the first contact plate 25 and the second contact plate 26.
- the connecting plate 35 is not limited to a block shape, and may be, for example, an H steel shape as long as it has sufficient strength for temporary joining of the cylindrical members 9 and 10.
- one end portion of the connecting plate 35 is disposed on the first contact plate 25, and the first contact plate 25 and one end portion of the connecting plate 35 are joined using a carbon steel filler material.
- the third weld 38 is formed by welding without preheating.
- the other end of the connecting plate 35 is disposed on the second contact plate 26, and the other end of the second applying plate 26 and the connecting plate 35 using a carbon steel filler material. Are welded without preheating to form a fourth welded portion 39.
- the connecting plate 35 made of carbon steel is welded to the respective contact plates 25 and 26 made of carbon steel without preheating using a filler material made of carbon steel.
- the connecting plate joining step since a plurality of connecting plates 35 are joined at equal intervals in the circumferential direction of the pressure vessel 1, in the temporary joining step, the overlay welding step, the contact plate joining step, and the connecting plate joining step are connected. This is repeated as many times as the number of the plates 35 joined. Further, the number of joints of the connecting plate 35 is appropriately determined according to the diameter of the cylindrical member.
- the main joining process performed after a temporary joining process is demonstrated.
- the main joining step there are an inner peripheral surface joining step, a temporary joining removal step, and an outer peripheral surface joining step, which are generally performed in this order.
- the inner peripheral surface joining step the inner peripheral surface side of the groove portion K5 is surrounded by a filler metal made of low alloy steel in a state where the connecting plate 35 is joined to the outside of the pressure vessel 1 (temporary joined state). Welded in the direction.
- the groove portion K5 is formed using a filler material made of low alloy steel in a state where the outer connecting plate 35 of the pressure vessel 1 is removed (temporary joining release state).
- the outer peripheral surface side is welded in the circumferential direction. Note that this is an example of the main joining process, and the present invention is not limited to this.
- After removing the temporary joining member after welding a welding amount that can maintain the butt state even if the temporary joining member is removed, which is the inner circumferential surface, the outer circumferential surface, or both, or a part of each of them. Is the main point of the main joining process. Moreover, it is not necessary to remove all the temporary joining members in this step, and it is appropriately performed as long as the outer peripheral surface joining step is not hindered.
- the first and second built-up portions 21 and 22 are connected to the third and fourth cylindrical members 9 and 10 with the respective cylindrical members 9 and 10. Since overlay welding is performed using the same material, quality requirements for the cylindrical member can be satisfied. And the 1st padding part 25 and the 2nd padding board 26 are joined to the 1st buildup part 21 and the 2nd buildup part 22 via the 1st welding part 28 and the 2nd welding part 29, and further, The connection plate 35 made of carbon steel can be joined to the first and second contact plates 25 and 26 made of carbon steel without preheating.
- each cylindrical member 9 and 10 and connecting plate 35 are preheated.
- each of the contact plates 25 and 26 and the connecting plate 35 is made of carbon steel, the connecting plate 35 can be welded without preheating. There is no need to preheat in the joining process.
- the connecting plate 35 can be simply temporarily joined to the cylindrical members 9 and 10 while satisfying the quality requirements for the cylindrical members 9 and 10.
- the build-up ranges of the build-up portions 21 and 22 are A range along the outer edge may be used. For this reason, while being able to minimize the build-up range of each build-up part 21 and 22, it is economical, and the thermal influence to each cylindrical member 9 and 10 by build-up welding can be suppressed.
- the connecting plate 35 is welded to the outside of the pressure vessel 1.
- the present invention is not limited to this, and the connecting plate 35 may be welded to the inside of the pressure vessel 1.
- Each of the contact plates 25 and 26 is not limited to a flat plate, and preferably has an optimal shape according to the shape of the peripheral surface sandwiching the groove portions K1 to K6. It is preferable to have an optimum shape according to the arrangement of the contact plates 25 and 26.
- FIG. 4 is a cross-sectional view of a temporarily joined portion that is temporarily joined by the welding method according to the second embodiment.
- the welding method of Example 2 is a welding method in which the contact plates 25 and 26 of Example 1 are omitted.
- the temporary joining process in the welding method of Example 2 is demonstrated.
- the thickness of each of the built-up parts 21 and 22 is preheated for the cylindrical members 9 and 10 during welding in the connecting plate joining process. Even if it does not perform, it is the thickness which does not have a thermal influence on each cylindrical member 9 and 10.
- the thickness of each of the built-up portions 21 and 22 is determined in advance by a confirmation test. Further, when the connecting plate 35 is welded to the build-up portions 21 and 22 formed on the cylindrical members 9 and 10, when preheating is required for the build-up portions 21 and 22, the build-up welding process Then, build-up welding is performed in advance on each build-up portion 21, 22 formed on each cylindrical member 9, 10 using a filler material that does not require preheating in the connecting plate joining step. In addition, since a matching process is the same as that of Example 1, description is abbreviate
- a connecting plate 35 made of carbon steel is used, and the connecting plate 35 is welded to the respective built-up parts 21 and 22 without preheating using a filler material of carbon steel.
- the connecting plate 35 is not limited to the block shape, and may be, for example, an H steel shape as long as it has sufficient strength for temporary joining of the cylindrical members 9 and 10. .
- one end portion of the connecting plate 35 is disposed on the first build-up portion 21, and one end portion of the first build-up portion 21 and the connecting plate 35 is formed using a carbon steel filler material. Are welded without preheating to form the first welded portion 40.
- the other end of the connecting plate 35 is disposed on the second build-up portion 22, and the other of the second build-up portion 22 and the connecting plate 35 is made of a carbon steel filler material.
- the second welded portion 41 is formed by welding the end portion without preheating. At this time, each welding part 40 and 41 is welded only to the range of each build-up part 21 and 22, and is not welded to each cylindrical member 9 and 10.
- FIG. Thereby, the connection board 35 which consists of carbon steel is welded to each build-up part 21 and 22 which consists of low alloy steel without preheating using the filler material which consists of carbon steel.
- the first and second built-up portions 21 and 22 are the same as the cylindrical members 9 and 10 in the third cylindrical member 9 and the fourth cylindrical member 10. Since overlay welding is performed using a material, the quality requirement for the cylindrical member can be satisfied. Then, the connecting plate 35 is joined to the first build-up part 21 and the second build-up part 22 via the first weld part 40 and the second weld part 41. Thereby, when welding the connecting plate 35 of carbon steel and each cylindrical member 9 and 10 of low alloy steel using the filler material of low alloy steel, each cylindrical member 9 and 10 and connecting plate 35 are preheated.
- connection plate 35 can be attached and welded to each of the built-up portions 21 and 22 that do not require preheating, the connecting plate 35 can be welded without preheating, and the butting process and connecting plate joining process. No preheating is required. As described above, even in the welding method according to the second embodiment, the connection plate 35 can be simply temporarily joined to the cylindrical members 9 and 10 while satisfying the quality requirements for the cylindrical members 9 and 10.
- the welding method according to the present invention is useful when the cylindrical members are temporarily joined to each other by the connecting member, and is particularly suitable for welding the pressure vessel of the steam generator.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Butt Welding And Welding Of Specific Article (AREA)
- Arc Welding In General (AREA)
Abstract
Le procédé de soudage selon l'invention comprend: une étape de soudage en surépaisseur, consistant à constituer une première partie complètement assemblée (21) et une seconde partie complètement assemblée (22) sur un troisième élément (9) de cylindre et un quatrième élément (10) de cylindre en effectuant un soudage en surépaisseur sur le troisième élément (9) de cylindre et le quatrième élément (10) de cylindre à travers une partie en biseau (K5) constituée entre le troisième élément (9) de cylindre, qui est fait d'une première matière, et le quatrième élément (10) de cylindre amenés en butée l'un contre l'autre dans le sens axial, en utilisant un matériau d'apport identique à la première matière; et une étape d'assemblage de plaque de liaison, consistant à assembler provisoirement une plaque de liaison (35) au troisième élément (9) de cylindre et au quatrième élément (10) de cylindre en assemblant une partie terminale de la plaque de liaison (35) à la première partie complètement assemblée (21) via une tôle doublante (25) d'une seconde matière et en assemblant l'autre partie terminale de la plaque de liaison (35) à la seconde partie complètement assemblée (22) via une seconde tôle doublante (26) de la seconde matière.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2011-025285 | 2011-02-08 | ||
| JP2011025285A JP5762032B2 (ja) | 2011-02-08 | 2011-02-08 | 溶接方法 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2012108442A1 true WO2012108442A1 (fr) | 2012-08-16 |
Family
ID=46638655
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2012/052780 Ceased WO2012108442A1 (fr) | 2011-02-08 | 2012-02-07 | Procédé de soudage |
Country Status (2)
| Country | Link |
|---|---|
| JP (1) | JP5762032B2 (fr) |
| WO (1) | WO2012108442A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2021081661A1 (fr) * | 2019-10-31 | 2021-05-06 | Her Majesty The Queen In Right Of Canada As Represented By The Minister Of Natural Resources Canada | Joint hybride d'about-à recouvrement et procédé de production |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5499747A (en) * | 1978-01-25 | 1979-08-06 | Hitachi Ltd | Reinforcing method for welded joint or stainless steel pipe and construction of welded join of stainless steel pipe |
| JPS62165068A (ja) * | 1986-01-14 | 1987-07-21 | Mitsubishi Heavy Ind Ltd | 圧力容器の外部金物取付方法 |
| JPH06328245A (ja) * | 1993-05-21 | 1994-11-29 | Mitsubishi Heavy Ind Ltd | 柱材の自動溶接方法 |
-
2011
- 2011-02-08 JP JP2011025285A patent/JP5762032B2/ja active Active
-
2012
- 2012-02-07 WO PCT/JP2012/052780 patent/WO2012108442A1/fr not_active Ceased
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5499747A (en) * | 1978-01-25 | 1979-08-06 | Hitachi Ltd | Reinforcing method for welded joint or stainless steel pipe and construction of welded join of stainless steel pipe |
| JPS62165068A (ja) * | 1986-01-14 | 1987-07-21 | Mitsubishi Heavy Ind Ltd | 圧力容器の外部金物取付方法 |
| JPH06328245A (ja) * | 1993-05-21 | 1994-11-29 | Mitsubishi Heavy Ind Ltd | 柱材の自動溶接方法 |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2021081661A1 (fr) * | 2019-10-31 | 2021-05-06 | Her Majesty The Queen In Right Of Canada As Represented By The Minister Of Natural Resources Canada | Joint hybride d'about-à recouvrement et procédé de production |
Also Published As
| Publication number | Publication date |
|---|---|
| JP5762032B2 (ja) | 2015-08-12 |
| JP2012161826A (ja) | 2012-08-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5650358B1 (ja) | 板曲げ中空ロールの製造方法並びに板曲げ中空ロールおよび鋼板製造プロセス装置 | |
| CN110421238B (zh) | 一种高强度筒体对接焊的焊接工艺 | |
| JP5658420B1 (ja) | 板曲げ中空ロールの製造方法および鋼板製造プロセス装置の製造方法 | |
| CN116551230B (zh) | 一种大尺寸钛合金薄壁锥形构件的精密装配焊接方法 | |
| CN104400211A (zh) | 一种贮箱搅拌摩擦焊缺陷等强固相补焊的方法及装置 | |
| JPH05237655A (ja) | ロータの修理方法 | |
| US6754956B1 (en) | Methods for manufacturing a nozzle box assembly for a steam turbine | |
| CN113634937A (zh) | 一种制动盘分块和拼焊方法 | |
| JP5762032B2 (ja) | 溶接方法 | |
| JP2009072795A (ja) | 溶接治具 | |
| CN105364413A (zh) | 一种筒体构件的制造方法 | |
| US8536479B2 (en) | Method for welding shafts on vertical rotational axis | |
| JP2016075586A5 (fr) | ||
| CN211638744U (zh) | 压力容器用铬钼钢与低碳钢的连接结构 | |
| WO2009006671A1 (fr) | Procédé de fabrication d'un réservoir | |
| CN102744501B (zh) | 一种制造沥青搅拌设备的方法 | |
| CN110480253B (zh) | 链轮盘修复方法 | |
| KR102521687B1 (ko) | 아웃트링 용접부 금속조직 모재동질화 처리방법 | |
| CN107900544B (zh) | 一种十字焊缝不开过焊孔的焊接方法 | |
| CN105750752B (zh) | 一种防止炼钢转炉耳轴隔板结构裂纹的方法 | |
| JP2005262292A (ja) | 薄板円筒管の溶接装置 | |
| KR20190135480A (ko) | 파이프 라인의 핫탭 피팅의 왜곡 제어 및 용접 후 열처리 없는 두껍고 긴 심의 용접 시스템 및 방법 | |
| CN117548765A (zh) | 一种锥形蜂窝内环组件的真空钎焊方法 | |
| CN114952053A (zh) | 一种集箱及管座的焊接方法 | |
| JP2012245555A (ja) | 工業用ロール及びその製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 12744657 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 12744657 Country of ref document: EP Kind code of ref document: A1 |