WO2013147186A1 - 複合中空糸膜及び中空糸膜モジュール - Google Patents
複合中空糸膜及び中空糸膜モジュール Download PDFInfo
- Publication number
- WO2013147186A1 WO2013147186A1 PCT/JP2013/059594 JP2013059594W WO2013147186A1 WO 2013147186 A1 WO2013147186 A1 WO 2013147186A1 JP 2013059594 W JP2013059594 W JP 2013059594W WO 2013147186 A1 WO2013147186 A1 WO 2013147186A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- hollow fiber
- fiber membrane
- porous
- layer
- polyolefin resin
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D71/00—Semi-permeable membranes for separation processes or apparatus characterised by the material; Manufacturing processes specially adapted therefor
- B01D71/06—Organic material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D53/00—Separation of gases or vapours; Recovering vapours of volatile solvents from gases; Chemical or biological purification of waste gases, e.g. engine exhaust gases, smoke, fumes, flue gases, aerosols
- B01D53/22—Separation of gases or vapours; Recovering vapours of volatile solvents from gases; Chemical or biological purification of waste gases, e.g. engine exhaust gases, smoke, fumes, flue gases, aerosols by diffusion
- B01D53/228—Separation of gases or vapours; Recovering vapours of volatile solvents from gases; Chemical or biological purification of waste gases, e.g. engine exhaust gases, smoke, fumes, flue gases, aerosols by diffusion characterised by specific membranes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D53/00—Separation of gases or vapours; Recovering vapours of volatile solvents from gases; Chemical or biological purification of waste gases, e.g. engine exhaust gases, smoke, fumes, flue gases, aerosols
- B01D53/22—Separation of gases or vapours; Recovering vapours of volatile solvents from gases; Chemical or biological purification of waste gases, e.g. engine exhaust gases, smoke, fumes, flue gases, aerosols by diffusion
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D63/00—Apparatus in general for separation processes using semi-permeable membranes
- B01D63/02—Hollow fibre modules
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D67/00—Processes specially adapted for manufacturing semi-permeable membranes for separation processes or apparatus
- B01D67/0002—Organic membrane manufacture
- B01D67/0006—Organic membrane manufacture by chemical reactions
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D69/00—Semi-permeable membranes for separation processes or apparatus characterised by their form, structure or properties; Manufacturing processes specially adapted therefor
- B01D69/08—Hollow fibre membranes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D69/00—Semi-permeable membranes for separation processes or apparatus characterised by their form, structure or properties; Manufacturing processes specially adapted therefor
- B01D69/10—Supported membranes; Membrane supports
- B01D69/107—Organic support material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D69/00—Semi-permeable membranes for separation processes or apparatus characterised by their form, structure or properties; Manufacturing processes specially adapted therefor
- B01D69/12—Composite membranes; Ultra-thin membranes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D69/00—Semi-permeable membranes for separation processes or apparatus characterised by their form, structure or properties; Manufacturing processes specially adapted therefor
- B01D69/12—Composite membranes; Ultra-thin membranes
- B01D69/1213—Laminated layers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D69/00—Semi-permeable membranes for separation processes or apparatus characterised by their form, structure or properties; Manufacturing processes specially adapted therefor
- B01D69/12—Composite membranes; Ultra-thin membranes
- B01D69/1218—Layers having the same chemical composition, but different properties, e.g. pore size, molecular weight or porosity
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D71/00—Semi-permeable membranes for separation processes or apparatus characterised by the material; Manufacturing processes specially adapted therefor
- B01D71/06—Organic material
- B01D71/26—Polyalkenes
- B01D71/261—Polyethylene
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D71/00—Semi-permeable membranes for separation processes or apparatus characterised by the material; Manufacturing processes specially adapted therefor
- B01D71/06—Organic material
- B01D71/76—Macromolecular material not specifically provided for in a single one of groups B01D71/08 - B01D71/74
- B01D71/80—Block polymers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01F—MIXING, e.g. DISSOLVING, EMULSIFYING OR DISPERSING
- B01F25/00—Flow mixers; Mixers for falling materials, e.g. solid particles
- B01F25/40—Static mixers
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01D—MECHANICAL METHODS OR APPARATUS IN THE MANUFACTURE OF ARTIFICIAL FILAMENTS, THREADS, FIBRES, BRISTLES OR RIBBONS
- D01D5/00—Formation of filaments, threads, or the like
- D01D5/24—Formation of filaments, threads, or the like with a hollow structure; Spinnerette packs therefor
- D01D5/247—Discontinuous hollow structure or microporous structure
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D2325/00—Details relating to properties of membranes
- B01D2325/02—Details relating to pores or porosity of the membranes
- B01D2325/027—Nonporous membranes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D2325/00—Details relating to properties of membranes
- B01D2325/04—Characteristic thickness
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D2325/00—Details relating to properties of membranes
- B01D2325/20—Specific permeability or cut-off range
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D2325/00—Details relating to properties of membranes
- B01D2325/32—Melting point or glass-transition temperatures
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B01—PHYSICAL OR CHEMICAL PROCESSES OR APPARATUS IN GENERAL
- B01D—SEPARATION
- B01D2325/00—Details relating to properties of membranes
- B01D2325/52—Crystallinity
Definitions
- the present invention relates to a composite hollow fiber membrane, a method for producing the same, and a hollow fiber membrane module including the composite hollow fiber membrane.
- carbonated water is used to rinse the surface of the object to be cleaned without charging the object to be cleaned or the nozzle. That is, when ultrapure water is used for cleaning, the object to be cleaned may be charged due to friction with the object to be cleaned due to its high insulating property. When the object to be cleaned is charged, for example, when the object to be cleaned has a fine circuit pattern, the circuit may be destroyed. In order to prevent this, carbonated water in which carbon dioxide gas is dissolved in ultrapure water to improve conductivity is used. The carbon dioxide concentration of the carbonated water is only 1-100 mg / L because it only gives conductivity to the ultrapure water.
- Patent Document 1 a gas dissolving membrane module incorporating a gas permeable membrane having a property of allowing only gas to permeate is utilized.
- Patent Document 2 a gas dissolving membrane module incorporating a gas permeable membrane having a property of allowing only gas to permeate.
- Patent Document 2 a method using a porous hollow fiber membrane as a hollow fiber membrane.
- Non-porous gas separation membranes include ethylene-vinyl alcohol-based polymers and ethylene-vinyl alcohol-based polymer composite membranes for gas separation membranes (Patent Document 3) composed of amine compounds and homogeneous layers composed of linear polyethylene. Examples include a composite hollow fiber membrane having a three-layer structure sandwiched between two porous layers (Patent Document 4).
- the effective area of the membrane is reduced, the performance of the gas dissolution module is reduced, and the gas concentration contained in the functional wash water is reduced.
- the gas dissolution module feeds the gas to be dissolved into the gas chamber and transfers the gas component to the water chamber through the membrane. Normally, there is almost no consideration of water vapor migration in the reverse direction through the membrane. It has not been fully examined.
- the ethylene-vinyl alcohol polymer composite membrane for gas separation membranes comprising an ethylene-vinyl alcohol polymer and an amine compound of Patent Document 3 has a high water content of 100%, extremely high water vapor permeability, and regular drain water. There is a problem that it is necessary to discharge gas. Since the composite hollow fiber membrane of Patent Document 4 has a low oxygen permeability coefficient of the homogeneous layer, in order to obtain a practically effective dissolved gas permeation flow rate, the homogeneous layer needs to be an extremely thin membrane of 0.3 ⁇ m or less. . However, since it is difficult to reduce the thickness of the homogeneous film, the mechanical strength of the film may be reduced and pinholes may be generated.
- An object of the present invention is to solve the above-mentioned problems, to improve the gas permeation performance, to further reduce the influence of the condensed water on the performance of the gas dissolution module, and to provide a composite hollow fiber membrane for degassing excellent in elution. Is to provide.
- the homogeneous layer of the composite hollow fiber membrane is a homogeneous layer containing a non-porous polyolefin resin A that is permeable to gas
- the support layer that supports the homogeneous layer is a porous layer containing a polyolefin resin B.
- the polyolefin resin A of the layer can be solved by using a block copolymer of ethylene units and at least one olefin unit selected from ⁇ -olefin units having 3 to 20 carbon atoms. That is, the present invention provides the following.
- a composite hollow fiber membrane having a non-porous homogeneous layer that transmits a gas mainly composed of polyolefin resin A, and a porous support layer mainly composed of polyolefin resin B that supports the non-porous homogeneous layer
- the composite hollow fiber membrane wherein the polyolefin resin A of the non-porous homogeneous layer is a block copolymer of ethylene units and at least one olefin unit selected from ⁇ -olefin units having 3 to 20 carbon atoms.
- the polyolefin porous layer that supports the non-porous homogeneous layer is disposed on the outer layer side of the non-porous homogeneous layer, and the non-porous homogeneous layer extends in the film thickness direction from the innermost surface of the hollow fiber membrane.
- the polyolefin resin A of the non-porous homogeneous layer has an MFRD measured in accordance with JIS K7210 code D of 0.1 to 1.0 g / 10 min ⁇ 190 ° C.
- a hollow fiber membrane module comprising the composite hollow fiber membrane according to any one of [1] to [10].
- the present invention is a composite hollow fiber membrane that is low in water vapor permeability and excellent in gas permeability, can suppress the generation of drain water, and can increase the amount of dissolved gas with high efficiency, and a method for producing the composite hollow fiber membrane,
- a hollow fiber membrane module including the composite hollow fiber membrane can be provided.
- the composite hollow fiber membrane of the present invention (hereinafter also referred to as “the present composite hollow fiber membrane”) is a composite hollow fiber having a non-porous homogeneous layer that allows gas permeation and a porous layer that supports the homogeneous layer. It is a membrane. Since the composite hollow fiber membrane of the present invention is used for the purpose of gas permeation, it is also called a gas permeable composite hollow fiber membrane.
- the homogeneous layer is a non-porous layer having gas permeability and containing the polyolefin resin A as a main component.
- the polyolefin resin A is a block copolymer of ethylene units and at least one olefin unit selected from ⁇ -olefin units having 3 to 20 carbon atoms.
- permeate gas or “gas permeable” refers to a property of transmitting only gas without transmitting liquid or the like, for example, a film that does not transmit water but transmits water vapor.
- non-porous means a solid state in which the pores are substantially free of pores having a micrometer order and the inside is clogged with resin.
- the ⁇ -olefin unit is an olefin unit containing 3 to 20 carbon atoms, and the ⁇ -olefin unit having 6 to 20 carbon atoms is It is preferable to include.
- the ⁇ -olefin unit is more preferably an octene unit, and most preferably a 1-octene unit.
- the ethylene unit content is preferably 25 to 97 mol%, more preferably 40 to 96 mol%, and even more preferably 55 to 95 mol%.
- the MFRD (melt flow rate) measured in accordance with JIS K7210 code D of the polyolefin resin A in the present invention is preferably 0.1 to 1.0 g / 10 min ⁇ 190 ° C., preferably 0.3 to 1 More preferably, it is 0.0 g / 10 min ⁇ 190 ° C. This is because a composite hollow fiber membrane excellent in gas permeability and rigidity can be obtained within the above range.
- the polymer structure includes a crystalline polymer block mainly composed of ethylene units (hard segment) and at least one ⁇ -olefin unit selected from ⁇ -olefin units having 3 to 20 carbon atoms (soft segment). It is desirable that the block has a multi-block structure in which each block is alternately connected to 2 or more, preferably 3 or more. Further, although there are a linear structure and a radial structure, a linear structure is particularly preferable.
- the length of the block can be changed by controlling the ratio and type of the catalyst, the ratio and type of chain shuttling agent (chain shuttling agent), the polymerization temperature, and the like.
- chain shuttling agent chain shuttling agent
- the block copolymer synthesized by the chain shuttling reaction catalyst technology is composed of a crystalline ethylene / ⁇ -olefin block (hard) having a very low comonomer content and a high melting point, and an amorphous ethylene-octene block having a high comonomer content. It is an alternative to (soft).
- OBC is also referred to as an ethylene / ⁇ -olefin block interpolymer.
- a block copolymer as the non-porous homogeneous layer, a low water vapor permeable composite hollow fiber membrane can be obtained while maintaining gas permeability. With such a hollow fiber membrane, the generation of drain water can be suppressed over a long period of time, and the amount of dissolved gas in the wash water can be increased stably and efficiently.
- the density of the polyolefin resin A forming the non-porous homogeneous layer is preferably 0.860 to 0.890 g / cm 3 .
- the density of the polyolefin resin A is within the above range, the gas permeability of the homogeneous layer is improved.
- the density is higher than 0.89 g / cm 3 , the oxygen permeation coefficient at 25 ° C. (JIS K7126) is less than 50 ⁇ 10 ⁇ 16 mol ⁇ m / m 2 ⁇ s ⁇ Pa, so that sufficient gas permeation performance is obtained. I can't.
- the moisture permeability coefficient at 25 ° C. is higher than 3.00 ⁇ 10 ⁇ 3 g / m ⁇ 24 hr, and water and water
- the solution containing 50% or more is degassed and dissolved in the gas, condensed water is generated due to temperature change and pressure change during operation, and the condensed water that penetrates into the porous support layer is gas.
- the moisture permeability coefficient at 25 ° C. is preferably 3.00 ⁇ 10 ⁇ 3 g / m ⁇ 24 hr or less, more preferably 1.0 ⁇ 10 ⁇ 3 g / m ⁇ 24 hr or less.
- the melting point by DSC is preferably 100 to 135 ° C., more preferably 100 to 130 ° C., and 115 to 125 ° C. with respect to the support layer side. It is further preferable in terms of matching of moldability.
- the melting point by DSC is the peak top melting point obtained by a differential scanning calorimeter (DSC). Specifically, using DSC, a sample amount of 10 mg is taken, held at 190 ° C. for 5 minutes, and then ⁇ 10 Crystallization is performed at a rate of temperature decrease of 10 ° C./min to 50 ° C., held at ⁇ 10 ° C. for 5 minutes, and then measured to 200 ° C. at a rate of temperature increase of 10 ° C./min.
- the moisture permeability coefficient at 25 ° C. of the polyolefin resin A constituting the non-porous homogeneous layer is preferably 1.00 ⁇ 10 ⁇ 3 g / m ⁇ 24 hr or less. Even if the homogeneous membrane having gas separation ability as the gas permeable membrane is non-porous, if the moisture permeability coefficient is high, condensed water is likely to be generated due to the permeation of water vapor even if water does not leak. Therefore, it is preferable that the moisture permeability coefficient is low.
- the ratio Mw / Mn between the weight average molecular weight and the number average molecular weight of the polyolefin resin A is preferably 3.0 or less, and more preferably 1.5 to 2.5.
- the viscosity affects the moldability of the resin.
- the viscosity is highly dependent on Mw.
- Mw / Mn polydispersity
- polyethylene examples of the polyolefin resin A used in the homogeneous layer of the present invention include polyethylene.
- the polyethylene in the present invention means that there are more segments composed of ethylene units than other polymer block segments.
- Elastomeric properties are believed to depend on fringed micellar crystals that act as network junctions.
- the heat resistance that is, the operating temperature range has been limited. Therefore, in recent years, Dow Chemical Company has developed a technology for chain shuttling reaction catalysts. Specifically, it can be synthesized according to the method disclosed in JP-T-2007-529617. For example, (A) a first olefin polymerization catalyst and (B) a second polymer capable of preparing a polymer that differs in chemical or physical properties from the polymer prepared by catalyst (A) under equivalent polymerization conditions.
- a composition containing a mixture or reaction product obtained by combining an olefin polymerization catalyst and (C) a chain shuttling agent (chain shuttling agent) is prepared, and the above ethylene and ⁇ -olefin are subjected to addition polymerization conditions. Below, it can manufacture through the process made to contact with this composition.
- a continuous solution polymerization method is preferably applied. In the continuous solution polymerization method, a catalyst component, a chain shuttling agent (chain shuttling agent), monomers, and optionally a solvent, an auxiliary agent, a scavenger and a polymerization auxiliary agent are continuously fed to the reaction zone to obtain a polymer product. Are continuously removed from there.
- olefin block copolymer which is the polyolefin resin A in the present invention
- it is commercially available from Dow Chemical Company under the trade names INFUSE® D9000, D9007, D9100, D9107, D9500, D9507, D9530, D9817, D9807, and the like.
- the non-porous homogeneous layer is preferably a layer mainly composed of the polyolefin resin A.
- the layer mainly composed of the polyolefin resin A is a layer in which the content of the polyolefin resin A is 90% by mass or more based on the total mass of the homogeneous layer. 95 mass% or more is preferable, as for content of polyolefin resin A in the layer which has polyolefin resin A as a main component, 99 mass% or more is more preferable, and 100 mass% is especially preferable.
- additives such as an antioxidant, an ultraviolet absorber, a lubricant, an antiblocking agent, a colorant, a flame retardant, etc., if necessary, as long as the purpose of the present invention is not impaired. May be added.
- the thickness of the homogeneous layer is preferably 0.5 to 10 ⁇ m. When the thickness of the homogeneous layer is 0.5 ⁇ m or more, pressure resistance is improved. If the thickness of the homogeneous layer is 10 ⁇ m or less, the gas permeability is improved. When the present composite hollow fiber membrane has a plurality of homogeneous layers, the thickness of the homogeneous layer is the thickness of each homogeneous layer.
- the porous support layer is a layer containing a polyolefin resin B as a main component that supports the non-porous homogeneous layer.
- the polyolefin resin B is not particularly limited as long as it is compatible with the polymer constituting the non-porous homogeneous layer and can form a porous structure.
- high density polyethylene is preferred. In general, the higher the density of the high density polyethylene, the higher the crystallinity and the easier the porous process by the stretching method. Therefore, the preferable range of density is 0.960 to 0.968 g / cm 3 .
- the high density polyethylene is an ethylene homopolymer.
- the copolymer with another olefin may be sufficient. In this case, the amount of the olefin comonomer is preferably 0 to 20 mol%, and more preferably 5 mol% or less.
- porous means that pores having an average diameter of about 0.01 to 1 ⁇ m have a porosity of at least 20% by volume.
- the porosity of the porous support layer is preferably 30 to 80% by volume with respect to 100% by volume of the entire porous support layer. When the porosity is 30% by volume or more, excellent gas permeability is easily obtained. When the porosity is 80% by volume or less, mechanical strength such as pressure resistance is improved.
- the size of the pores of the porous support layer is not particularly limited as long as sufficient gas permeability and mechanical strength are satisfied. For example, the average diameter is preferably about 0.05 to 0.1 ⁇ m.
- a preferred range of MFRD of the polyolefin resin B used for the porous support layer is 0.1 to 1.0 g / 10 min. If the MFRD of the polyolefin resin B is 0.1 g / 10 min or more, the melt viscosity does not increase too much, and the molding range capable of improving the crystal orientation becomes wide. In addition, it becomes easy to adapt to the field where the diameter reduction is required to increase the filling rate of the module. If the MFRD of the polyolefin resin B is 1.0 g / 10 min or less, it is easy to suppress the melt viscosity from becoming too small, and the crystal orientation can be improved by increasing the draft ratio, and it can be made porous by stretching. It becomes easy.
- the rigidity is improved, and the gas permeability can be easily improved by thinning or increasing the porosity.
- the polyolefin resin A (olefin block copolymer) and the polyolefin resin B have the same melt characteristics in terms of gas permeability and solvent resistance, the smaller the difference between the MFRDs, the better.
- the difference is preferably 0.5 g / 10 min or less.
- the porous layer is preferably a layer mainly composed of polyolefin resin B.
- the layer mainly composed of the polyolefin resin B is a layer having a content of the polyolefin resin B of 90% by mass or more. 95 mass% or more is preferable, as for content of polyolefin resin B in the layer which has polyolefin resin B as a main component, 99 mass% or more is more preferable, and 100 mass% is especially preferable.
- an antioxidant, an ultraviolet absorber, a lubricant, an antiblocking agent, a colorant, a flame retardant, and the like are added to the porous layer as needed, as long as the purpose of the present invention is not impaired. A thing may be added.
- the composite hollow fiber membrane of the present invention is formed from the non-porous homogeneous layer and the porous support layer described above. For example, it can be obtained by a multilayer composite spinning process and a stretched porous process.
- the form of the composite membrane constituting the hollow fiber membrane may be a two-layer composite membrane comprising a non-porous homogeneous layer (separation layer) having gas permeation performance and a porous support layer supporting the non-porous homogeneous layer.
- it may be a three-layer composite membrane in which a non-porous homogeneous layer having gas permeation performance is sandwiched between porous support layers.
- a composite film having four or more layers may be used. In particular, it is preferably composed of a composite film having three or more layers.
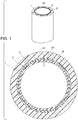
- the “position” of the homogeneous layer having gas permeability in the composite membrane of three or more layers is in the range of 1/10 to 1/4 from the inside of the hollow fiber membrane with respect to the thickness of the hollow fiber membrane (d1 in FIG. 1). It is preferable to arrange in.
- the “position of the homogeneous layer” means a distance from the innermost surface of the hollow fiber to the end surface closest to the innermost surface of the non-porous homogeneous layer (d2 in FIG. 1).
- the homogeneous layer has a non-porous structure, so the potting resin will not be impregnated inside it, and the more the area embedded in the potting resin, the more the membrane will be damaged due to bending due to pressure fluctuations in the vicinity of the potting part. Can be prevented. Further, when the thickness of the support layer inside the homogeneous layer is 1/10 or less of the film thickness, the support layer polymer is dragged to the inner support layer polymer to which the homogeneous layer polymer is welded in the stretching process for making the support layer polymer porous. This is undesirable because it causes defects.
- FIG. 1 shows a schematic diagram of the positional relationship between the non-porous homogeneous layer and the porous support layer in the composite hollow fiber membrane of the example of the present invention.
- Each figure is a schematic conceptual diagram, and does not faithfully represent the actual thickness or position of the film (layer).
- the thickness of the composite hollow fiber membrane is not particularly limited, but the hollow fiber membrane outer diameter is preferably 100 to 2000 ⁇ m. If the outer diameter of the hollow fiber membrane is 100 ⁇ m or more, a gap between the hollow fiber membranes can be easily obtained at the time of manufacturing the hollow fiber membrane module, and the potting resin can easily enter between the hollow fiber membranes. When the outer diameter of the hollow fiber membrane is 2000 ⁇ m or less, the size of the entire module can be reduced even when a hollow fiber membrane module using a large number of hollow fiber membranes is manufactured. As a result, the volume of the potting process portion is also reduced, and it is easy to suppress a decrease in dimensional accuracy due to the shrinkage of the potting resin during the potting process.
- the film thickness (d1) of the hollow fiber membrane is preferably 10 to 200 ⁇ m. If thickness is 10 micrometers or more, mechanical strength will improve. Furthermore, if the thickness is 200 ⁇ m or less, the outer diameter of the composite hollow fiber membrane becomes too thick, and it is easy to suppress the volumetric efficiency of the membrane when incorporated in the membrane module.
- the present composite hollow fiber membrane can be produced, for example, by a method having the following 1) spinning step and 2) stretching step.
- 1) Spinning step For example, in the case of the present composite hollow fiber membrane having a three-layer structure, a composite nozzle base in which the outermost layer nozzle portion, the intermediate layer nozzle portion and the innermost layer nozzle portion are arranged concentrically is used. A molten polyolefin resin B is supplied to the outermost layer nozzle portion and the innermost layer nozzle portion, and a molten polyolefin resin A is supplied to the intermediate layer nozzle portion.
- the polyolefin resin A and the polyolefin resin B are extruded from the respective nozzle portions, and are cooled and solidified in an unstretched state while appropriately adjusting the extrusion speed and the winding speed.
- a hollow fiber membrane precursor having a three-layer structure in which an unstretched homogeneous layer precursor is sandwiched between two unstretched porous layer precursors in a non-porous state is obtained.
- the discharge temperature of the polyolefin resin A and the polyolefin resin B may be in a state where they can be sufficiently melted and spun.
- the unstretched hollow fiber membrane precursor obtained by melt spinning is preferably subjected to constant length heat treatment (annealing) at a temperature equal to or lower than the melting point before stretching.
- the constant-length heat treatment is preferably performed at 105 to 120 ° C. for 8 to 16 hours. If the temperature is 105 ° C. or higher, this hollow fiber membrane with good quality can be easily obtained. If temperature is 120 degrees C or less, sufficient elongation will be easy to be obtained, the stability at the time of extending
- the hollow fiber membrane precursor is stretched under conditions that satisfy the following requirements (i) and (ii).
- the relationship between the stretching temperature T (° C.) and the melting point Tm (° C.) of the polyolefin resin A is Tm ⁇ 20 ⁇ T ⁇ Tm + 40.
- the stretching temperature T is not higher than the Vicat softening point of the polyolefin resin B.
- the stretching temperature T is Tm-20 (° C.) or higher, the porous layer precursor can be easily made porous, and the composite hollow fiber membrane having excellent gas permeability can be easily obtained.
- the stretching temperature T is Tm + 40 (° C.) or less, it is easy to suppress the occurrence of defects such as pinholes due to the disorder of the molecules.
- the stretching temperature T is equal to or lower than the Vicat softening point of the polyolefin resin B, the porous layer precursor can be easily made porous, and the composite hollow fiber membrane having excellent gas permeability can be easily obtained.
- the stretching step it is preferable to perform cold stretching before stretching (hot stretching) performed at the stretching temperature T. That is, two-stage stretching in which hot stretching is performed subsequent to cold stretching, or multi-stage stretching in which hot stretching is divided into two or more multi-stages subsequent to cold stretching is preferable.
- Cold stretching is stretching that causes structural cracking of the film at a relatively low temperature and generates microcracking.
- the temperature of cold drawing is preferably carried out at a relatively low temperature within a range from 0 ° C. to a temperature lower than Tm ⁇ 20 ° C.
- the stretching is preferably slow stretching. If it is low speed drawing, it becomes easy to make it porous while suppressing the yarn diameter from becoming too thin during drawing.
- the draw ratio varies depending on the types of polyolefin resin A and polyolefin resin B to be used, but the final ratio (total draw ratio) with respect to the unstretched hollow fiber membrane precursor is preferably 200 to 500%.
- the total draw ratio is 2 times or more, the porosity of the porous layer is improved, and excellent gas permeability is easily obtained. If the total draw ratio is 5 times or less, the breaking elongation of the composite hollow fiber membrane is improved.
- heat setting is performed in a state where the porous hollow fiber membrane is slightly relaxed under a constant length or within a range of 60% or less. It is preferable.
- the heat setting temperature is preferably not less than the stretching temperature and not more than the melting temperature.
- the present composite hollow fiber membrane described above has a non-porous homogeneous layer containing polyolefin resin A as a main component and a porous layer containing polyolefin resin B as a main component, it has excellent solvent resistance. It also has gas permeability. It also has excellent low elution properties.
- the hollow fiber membrane module of the present invention is a module comprising the composite hollow fiber membrane described above.
- the hollow fiber membrane module of the present invention has the same form as a known hollow fiber membrane module except that the present composite hollow fiber membrane is used.
- a hollow fiber membrane module of a known form in which several hundreds of the present composite hollow fiber membranes are bundled and inserted into a cylindrical housing, and the composite hollow fiber membranes are sealed with a sealing material (potting resin). It is done.
- the filling rate of the hollow fiber membrane with respect to the potting processed part volume is preferably about 20 to 60%.
- a raw solution containing dissolved gas is supplied to the inner side (primary side) of the hollow fiber membrane, and the outer side (secondary side) of the hollow fiber membrane is depressurized and dissolved.
- the dissolved gas can be permeated through the membrane by a driving force proportional to the partial pressure difference of the gas, and the dissolved gas can be discharged to the outside of the hollow fiber membrane.
- the outside of the hollow fiber membrane can be the primary side and the inside of the hollow fiber membrane can be the secondary side.
- a plurality of hollow fiber membrane modules can be connected in series to deaerate the target chemical solution to a predetermined deaeration level, or a plurality of the hollow fiber membrane modules can be connected in parallel to deaerate a large amount of chemical solution.
- MFR Melt flow rate
- Mw / Mn The ratio Mw / Mn of polyethylene was calculated by obtaining Mw and Mn from calibration curves obtained by measurement by GPC (high temperature GPC) under the following conditions.
- the calibration curve was calculated in third order by measuring a standard sample of polystyrene and using a polyethylene conversion constant (0.48). The columns used were the following three columns connected in series.
- Measurement condition Measuring device: “150-GPC” (manufactured by Waters) Column: “Shodex GPC AT-807 / S” (manufactured by Showa Denko) (1), “Tosoh TSK-GEL GMH6-HT” (manufactured by Tosoh) (2) Solvent: 1,2,4-trichlorobenzene Column temperature: 140 ° C Sample concentration: 0.05% by mass (injection amount: 500 ⁇ L) Flow rate: 1.0 mL / min Sample dissolution temperature: 160 ° C.
- Sample dissolution time 2.5 hours
- the molecular weight is approximated by a Gaussian distribution and low molecular weight Mw and Mn of each component, such as a component and a high molecular weight component, and the compounding ratio of those components were calculated.
- the porosity (unit: volume%) of the obtained gas-permeable composite hollow fiber membrane was measured using a mercury porosimeter 221 type (manufactured by Carlo Elba).
- the obtained gas permeable composite hollow fiber membrane was bundled in a U shape, and the end of the hollow fiber membrane was solidified with urethane resin to produce a hollow fiber membrane module.
- Oxygen or nitrogen is supplied from the outside of the composite hollow fiber membrane, and the oxygen permeation rate (QO2) (unit: m / hour ⁇ MPa) and nitrogen permeation at 25 ° C. with the inside (hollow part side) of the hollow fiber membrane as normal pressure.
- the speed (QN2) (unit: m / hour ⁇ MPa) was measured.
- the membrane area was calculated based on the inner diameter of the hollow fiber membrane.
- the separation factor (QO2 / QN2) was calculated
- Moisture permeability Measured by a cup method (conforming to JIS Z0208, measurement atmosphere: 25 ° C. ⁇ 90% RH) using a film sample having a thickness of 450 ⁇ m.
- Moisture permeability coefficient Calculated from the above moisture permeability by moisture permeability ⁇ film thickness.
- a chain shuttling reaction catalyst specifically, ethylene- where ⁇ -olefin is 1-octene, Octene block copolymer: trade name “INFUSE 9100”, manufactured by Dow Chemical Co., MFRD: 1.0 g / 10 min, density: 0.877 g / cm 3 , melting point Tm: 121 °
- a composite nozzle base in which the outermost layer nozzle portion, the intermediate layer nozzle portion, and the innermost layer nozzle portion are arranged concentrically was used.
- the molten polyolefin resin B is supplied to the outermost layer nozzle portion and the innermost layer nozzle portion
- the molten polyolefin resin A is supplied to the intermediate layer nozzle portion
- the polyolefin resin A / polyolefin resin B / polyolefin resin A is supplied from the outermost layer. It discharged so that it might become a ratio of 12/1/2, and these polyolefins were spun by winding-up speed 135m / min, and the unstretched hollow fiber membrane precursor was obtained.
- a homogeneous layer precursor was concentrically arranged in three layers sandwiched between two porous layer precursors.
- the hollow fiber membrane precursor was annealed at 108 ° C. for 8 hours. Next, the film was stretched 1.6 times at 23 ⁇ 2 ° C., and subsequently heat-stretched in a heating furnace at 105 ° C. until the total stretching amount reached 580%, thereby making the two porous layer precursors porous. Thereafter, a 45% relaxation step is provided in a heating furnace at 115 ° C., and finally the total draw ratio (the ratio to the unstretched hollow fiber membrane precursor) is 400%, and the gas-permeable composite hollow fiber A membrane was obtained.
- the produced composite hollow fiber membrane had an inner diameter of 165 ⁇ m, an outer diameter of 262 ⁇ m, and a film thickness of 48.3 ⁇ m, and the non-porous homogeneous layer was located at about 1/8 of the film thickness from the inside.
- the gas permeable composite hollow fiber membrane had a three-layer structure in which a homogeneous layer was sandwiched between two porous layers.
- the porosity of the gas permeable composite hollow fiber membrane was 67.2% by volume.
- the oxygen permeation rate (Q O2 ) at room temperature (25 ° C.) was 0.244 m / hr ⁇ Mpa
- the nitrogen permeation rate (Q N2 ) was 0.074 m / hr ⁇ Mpa.
- the separation factor (Q O2 / Q N2 ) was 3.3.
- IPA isopropyl alcohol
- a chain shuttling reaction catalyst specifically, ethylene- where ⁇ -olefin is 1-octene, Octene block copolymer: trade name “INFUSE 9107”, manufactured by Dow Chemical Co., MFRD: 1.0 g / 10 min, density: 0.866 g / cm 3 , melting point Tm: 120 ° C.
- the polyolefin resin B (for forming the porous support layer) was the same as in Example 1, and the discharge rate ratio was also the same as in Example 1. Spinning was carried out at a discharge temperature of 180 ° C. and a winding speed of 135 m / min. The obtained unstretched hollow fiber had an inner diameter of 160 ⁇ m, and three layers were arranged concentrically. The unstretched hollow fiber was annealed at 108 ° C. for 8 hours. Further, the annealed yarn was stretched 1.6 times at 23 ⁇ 2 ° C., and subsequently heat-stretched in a heating furnace at 105 ° C. until the total stretched amount becomes 5.8 times, and two porous layer support layers The precursor was made porous.
- the produced multilayer composite hollow fiber membrane had an inner diameter of 156 ⁇ m, an outer diameter of 251 ⁇ m, and a film thickness of 47.6 ⁇ m, and the non-porous homogeneous layer was located at about 1/8 of the film thickness from the inside.
- the multilayer composite hollow fiber membrane thus obtained had a three-layer structure in which a non-porous homogeneous layer was sandwiched between two porous support layers.
- the porosity of the gas permeable composite hollow fiber membrane was 66.6% by volume.
- the oxygen permeation rate (Q O2 ) at room temperature (25 ° C.) was 0.400 m / hr ⁇ Mpa
- the nitrogen permeation rate (Q N2 ) was 0.142 m / hr ⁇ Mpa.
- the separation factor (Q O2 / Q N2 ) was 2.8.
- a hollow fiber membrane module was prepared using the prepared gas permeable composite hollow fiber membrane. It was operated for one month by flowing 50 ° C. water inside the hollow fiber membrane and blowing carbon dioxide from the outside of the hollow fiber membrane to generate carbonated water, but the gas phase was low due to the low water vapor permeability of the membrane. No condensed water was produced on the side.
- the polyolefin resin B (for forming the porous support layer) was the same as in Example 1, and the discharge rate ratio was also the same as in Example 1. Spinning was carried out at a discharge temperature of 180 ° C. and a winding speed of 130 m / min. The obtained unstretched hollow fiber had an inner diameter of 180 ⁇ m, and three layers were arranged concentrically. The unstretched hollow fiber was annealed at 108 ° C. for 8 hours.
- the annealed yarn was stretched 120% at 23 ⁇ 2 ° C., and subsequently heat-stretched in a heating furnace at 70 ° C. until the total stretched amount reached 400% to obtain a composite hollow fiber membrane.
- the prepared multilayer composite hollow fiber membrane had an inner diameter of 160 ⁇ m, an outer diameter of 256 ⁇ m, and a film thickness of 48 ⁇ m, and the non-porous homogeneous layer was located at about 1/8 of the film thickness from the inside.
- the multilayer composite hollow fiber membrane thus obtained had a three-layer structure in which a non-porous layer was sandwiched between two porous layers.
- the porosity of the gas permeable composite hollow fiber membrane was 63.0% by volume.
- the oxygen permeation rate (Q O2 ) at room temperature (25 ° C.) was 0.36 m / hr ⁇ Mpa
- the nitrogen permeation rate (Q N2 ) was 0.13 m / hr ⁇ Mpa.
- the separation factor (Q O2 / Q N2 ) was 2.8.
- a hollow fiber membrane module was prepared using the prepared gas permeable composite hollow fiber membrane. The operation was performed by flowing water at 50 ° C. inside the hollow fiber membrane and blowing carbon dioxide from the outside of the hollow fiber membrane to generate carbonated water. Initially, it was possible to operate without generating condensed water, but due to softening of the homogeneous layer on the 4th day, the strength decreased and leakage occurred.
- thermoplastic polyurethane (Pandex T8375N manufactured by DIC Bayer Polymer Co., Ltd.) was used.
- the moisture permeability coefficient at 25 ° C. of Pandex T8375N by JIS Z0208 cup method is 25.9 g / m ⁇ 24 hr
- the oxygen permeability coefficient at 25 ° C. (JIS K7126) is 19.0 ⁇ 10 ⁇ 16 mol ⁇ m / m 2 ⁇ s ⁇ Pa.
- the polyolefin resin B (for forming the porous layer) is the same as in Example 1, and the discharge ratio is 12/1/2 from the outermost layer to the ratio of polyolefin resin A / thermoplastic polyurethane B / polyolefin resin A.
- the discharge was performed in the same manner as in Example 1. Spinning was carried out at a discharge temperature of 180 ° C. and a winding speed of 90 m / min.
- the obtained unstretched hollow fiber had an inner diameter of 200 ⁇ m, and three layers were arranged concentrically.
- the unstretched hollow fiber was annealed at 108 ° C. for 8 hours.
- the annealed yarn was stretched 160% at 23 ⁇ 2 ° C., and subsequently thermally stretched in a heating furnace at 110 ° C. until the total stretched amount reached 300%, to obtain a composite hollow fiber membrane.
- the produced multilayer composite hollow fiber membrane had an inner diameter of 200 ⁇ m, an outer diameter of 280 ⁇ m, and a film thickness of 25 ⁇ m, and the non-porous homogeneous layer was located about 1/8 of the film thickness from the inside.
- the multilayer composite hollow fiber membrane thus obtained had a three-layer structure in which a non-porous layer was sandwiched between two porous layers.
- the composite hollow fiber membrane had a porosity of 43.0% by volume.
- the oxygen permeation rate (Q O2 ) at room temperature (25 ° C.) was 0.28 m / hr ⁇ Mpa
- the nitrogen permeation rate (Q N2 ) was 0.10 m / hr ⁇ Mpa.
- the separation factor (Q O2 / Q N2 ) was 2.8.
- the separation factor 2.8 of the polymer used for the thin film layer was maintained.
- a hollow fiber membrane module was prepared using the prepared gas permeable composite hollow fiber membrane. The operation was performed by flowing water at 50 ° C. inside the hollow fiber membrane and blowing carbon dioxide from the outside of the hollow fiber membrane to generate carbonated water. After 24 hours, the invasion of water considered to be condensed water was confirmed.
- the gas-permeable composite hollow fiber membrane of the present invention is very useful for the production of functional water used for semiconductor cleaning liquids, carbon dioxide dissolution for carbonated springs, and separation of methane gas from biogas.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Oil, Petroleum & Natural Gas (AREA)
- Analytical Chemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Dispersion Chemistry (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Textile Engineering (AREA)
- Separation Using Semi-Permeable Membranes (AREA)
- Laminated Bodies (AREA)
- Multicomponent Fibers (AREA)
- Artificial Filaments (AREA)
Description
この炭酸水の炭酸ガス濃度は、超純水に導電性を与えるだけであるので1~100mg/Lと低濃度とされる。上記の気体を効率よく溶解させるために、気体のみを透過させる性質を有する気体透過膜を内蔵した気体溶解膜モジュールが活用されている(例えば、特許文献1)。気体溶解膜モジュールを用いると、気泡を含まないガス溶解水を容易に製造することができる。
他には中空糸膜として多孔質の中空糸膜を用いる方法が提案されている(特許文献2)。
気体溶解膜モジュールに多孔質中空糸膜を用いた場合、長期間の使用により膜が親水化し、水がガス側に漏れ出して膜表面を塞いでしまい、初期の炭酸ガス添加性能を得ることが出来なくなる懸念があった。
非多孔質の気体分離膜としては、エチレン-ビニルアルコール系重合体およびアミン化合物からなるガス分離膜用エチレン-ビニルアルコール系重合体複合膜(特許文献3)や直鎖状ポリエチレンからなる均質層が、2つの多孔質層で挟まれた3層構造を有する複合中空糸膜(特許文献4)などが挙げられる。
凝縮水が少量であれば、気体溶解モジュールの性能に及ぼす影響は軽微であるが、凝縮水の量が増すと、気体室の底部から次第に上方へ溜まっていき、気体の溶解に寄与する気体透過膜の有効面積が減少し、気体溶解モジュールの性能が低下して、機能性洗浄水中に含まれる気体濃度が減少する。
気体溶解モジュールは、気体室に溶解すべき気体を送り込み、気体成分を膜を通して水室へ移行させるのであり、通常、膜を通して逆方向への水蒸気の移行はほとんど考慮されず、凝縮水の対策は十分に検討されていなかった。
特許文献4の複合中空糸膜は、均質層の酸素透過係数が低いため、実用上有効な溶存気体の透過流量を得るには、均質層を0.3μm以下の極めて薄い膜とする必要がある。しかし、均質膜の薄膜化が難しいため、膜の機械的強度が低下してピンホールが発生することがある。均質層膜層がPEで有るために水蒸気透過性は低いが、ピンホールからの凝縮水の漏れを避けることができないという問題点を有する。
本発明の課題は、上記問題点を解決し、気体透過性能が良好で、更に、凝縮水による気体溶解モジュールの性能への影響を減少させ、溶出性に優れた脱気用複合中空糸膜を提供することである。
すなわち、本発明は以下を提供する。
[1]ポリオレフィン樹脂Aを主成分とする気体を透過する非多孔質均質層と、該非多孔質均質層を支持するポリオレフィン樹脂Bを主成分とする多孔質支持層とを有する複合中空糸膜において、前記非多孔質均質層のポリオレフィン樹脂Aが、エチレン単位と炭素数3~20のα-オレフィン単位から選ばれる少なくとも1種のオレフィン単位とのブロック共重合体である複合中空糸膜。
[2]非多孔質均質層の前記α-オレフィン単位が、炭素数6~20のα-オレフィン単位である[1]に記載の複合中空糸膜。
[3]非多孔質均質層の前記α-オレフィン単位が、1-オクテン単位である[2]に記載の複合中空糸膜。
[4]非多孔質均質層のポリオレフィン樹脂Aの酸素透過係数(JIS K7126)が50×10-16mol・m/m2・s・Pa(25℃)以上であであることを特徴とする[1]~[3]のいずれか一に記載の複合中空糸膜。
[5]非多孔質均質層のポリオレフィン樹脂Aの透湿係数が1.00×10⁻³g/m・24hr(25℃)以下であることを特徴とする[1]~[4]のいずれか一に記載の複合中空糸膜。
[6]該非多孔質均質層を支持するポリオレフィン多孔質層が、非多孔質均質層の外層側に配置されていると共に、非多孔質均質層が、中空糸膜の最内面から膜厚方向に膜厚の1/10~1/4以内の領域に配置されていることを特徴とする[1]~[5]のいずれか一に記載の複合中空糸膜。
[7]前記非多孔質均質層のポリオレフィン樹脂の密度が0.86~0.89g/cm3であることを特徴とする[1]~[6]のいずれか一に記載の複合中空糸膜。
[8]前記非多孔質均質層のポリオレフィン樹脂Aが、100℃以上、135℃以下の融点を有することを特徴とする[1]~[7]のいずれか一に記載の複合中空糸膜。
[9]前記非多孔質均質層のポリオレフィン樹脂Aの、JIS K7210のコードDに準拠して測定したMFRDが0.1~1.0g/10分・190℃にあることを特徴とする[1]~[8]のいずれか一に記載の複合中空糸膜。
[10]前記ポリオレフィン樹脂Aが、ポリエチレンである[1]~[9]のいずれか一に記載の複合中空糸膜。
[11][1]~[10]のいずれか一に記載の複合中空糸膜を具備する中空糸膜モジュール。
本発明の複合中空糸膜(以下、「本複合中空糸膜」ともいう。)は、気体を透過する非多孔質の均質層と、該均質層を支持する多孔質層とを有する複合中空糸膜である。本発明の複合中空糸膜は気体透過の目的で使用されるため、気体透過複合中空糸膜とも呼ぶ。
均質層は、ポリオレフィン樹脂Aを主成分として含む、気体透過性を有する非多孔質の層である。ポリオレフィン樹脂Aは、エチレン単位と、炭素数3~20のα-オレフィン単位から選ばれる少なくとも1種のオレフィン単位と、のブロック共重合体である。
本明細書において「気体を透過する」あるいは「気体透過性」とは、液体などを透過することなく気体のみを透過する特性、例えば水は透過しないが、水蒸気は透過する膜を意味する。
本明細書において「非多孔質」とは、実質的に孔径がマイクロメートルオーダーの孔が無く内部が樹脂で詰まった中実の状態を意味する。
本発明におけるオレフィンブロック共重合体において、エチレン単位含有量は、好ましくは25~97モル%、より好ましくは40~96モル%、さらにより好ましくは55~95モル%である。
本発明におけるポリオレフィン樹脂AのJIS K7210のコードDに準拠して測定したMFRD(メルトフローレート)は、0.1~1.0g/10分・190℃であることが好ましく、0.3~1.0g/10分・190℃であることが更に好ましい。前記範囲にあれば気体透過性及び剛性に優れた複合中空糸膜が得られるからである。
この技術を使用することによって連続法で新規のオレフィンブロックコポリマー(OBC)を合成することができる。チェーンシャトリング反応触媒の技術によって合成されるブロックコポリマーは、コモノマー含量が非常に少なく、融点が高い結晶性エチレン/α-オレフィンブロック(硬質)からなり、コモノマー含量が多い非晶質エチレン-オクテンブロック(軟質)に代わるものである。したがって、OBCはまた、エチレン/α-オレフィンブロックインターポリマー(ethylene/α-olefin block interpolymer)とも呼ばれる。
本発明では、非多孔質均質層としてブロック共重合体を使用することにより、気体透過性を維持しながら低水蒸気透過性の複合中空糸膜を得ることができたものである。かかる中空糸膜により、長期にわたりドレン水の発生を抑制でき、安定して、高効率に洗浄水中の溶存気体量を上げることが可能となる。
そのため0.89g/cm3より密度が大きければ、25℃における酸素透過係数(JIS K7126)50×10-16mol・m/m2・s・Paより小さくなるために十分な気体透過性能を得ることができない。また、密度が0.86g/cm3よりも小さいと、気体透過性能は満足されるが、25℃における透湿係数が3.00×10-3g/m・24hrより高くなり、水及び水を50%以上含むような溶液の脱気及び気体溶解の際に、運転時の温度変化・圧力変化などにより凝結水を生じドレン水となるのみでなく多孔質支持層に浸透した凝結水が気体の透過を抑制するため気体透過性のそのものが低下するので好ましくない。25℃における透湿係数は3.00×10-3g/m・24hr以下が好ましく、より好ましくは1.0×10-3g/m・24hr以下であることがより好ましい。
ここで、DSCによる融点は、示差走査熱量計(DSC)によって得られるピークトップ融点であり、具体的には、DSCを用い、サンプル量10mgを採り、190℃で5分間保持した後、-10℃まで10℃/分の降温速度で結晶化させ、-10℃で5分間保持した後、10℃/分の昇温速度で200℃まで測定して求める値である。
比率Mw/Mnが前記範囲内であれば、成形性を維持しつつ強度を向上させることができ、気体透過性及び欠陥の無い優れた本複合中空糸膜が得られやすいからである。
そこで、近年、Dow Chemical Companyが、チェーンシャトリング反応触媒の技術を開発した。具体的には特表2007-529617号公報に開示された方法にしたがって合成することもできる。
例えば、(A)第1のオレフィン重合触媒と、(B)同等の重合条件下で触媒(A)によって調製されるポリマーとは化学的性質又は物理的性質が異なるポリマーを調製可能な第2のオレフィン重合触媒と、(C)鎖シャトリング剤(チェーンシャトリング剤)と、を組み合わせて得られる混合物又は反応生成物を含む組成物を準備し、上記エチレンとα-オレフィンとを、付加重合条件下で、該組成物と接触させる工程を経て製造することができる。重合は、好ましくは連続溶液重合法が適用される。連続溶液重合法は、触媒成分、鎖シャトリング剤(チェーンシャトリング剤)、モノマー類、ならびに場合により溶媒、補助剤、捕捉剤および重合助剤が反応ゾーンに連続的に供給され、ポリマー生成物はそこから連続的に取り出される。
また、均質層には、本発明の目的を損なわない範囲内であれば、必要に応じて、酸化防止剤、紫外線吸収剤、滑剤、アンチブロッキング剤、着色剤、難燃化剤等の添加物が添加されていてもよい。
前記均質層の厚さとは、本複合中空糸膜が複数の均質層を有する場合は、そのそれぞれの均質層の厚さである。
多孔質支持層は、非多孔質均質層を支持する、ポリオレフィン樹脂Bを主成分として含む層である。ポリオレフィン樹脂Bは、非多孔質均質層を構成するポリマーと相溶性があり、多孔質構造を形成可能な材料であれば特に限定され無い。具体的には高密度ポリエチレンが好ましい。
高密度ポリエチレンは、一般に密度が高ければ高いほど結晶性が高く、延伸法による多孔化工程が容易である。そのため密度の好ましい範囲としては0.960~0.968g/cm3である。
高密度ポリエチレンは、エチレンホモポリマーであることが最も好ましい。また、他のオレフィンとの共重合体であってもよい。その際のオレフィンコモノマーの量は0~20モル%であることが好ましく、特に5モル%以下であることがより好ましい。
多孔質支持層の空孔率は、多孔質支持層全体100体積%に対して、30~80体積%が好ましい。空孔率が30体積%以上であれば、優れた気体透過性が得られやすい。空孔率が80体積%以下であれば、耐圧性等の機械的強度が向上する。
多孔質支持層の細孔の大きさは、特に限定されず、充分な気体透過性と機械的強度が満足される大きさであればよい。例えば0.05~0.1μm程度の平均径であることが好ましい。
また、ポリオレフィン樹脂A(オレフィンブロック共重合体)とポリオレフィン樹脂Bは、気体透過性及び耐溶剤性の点から溶融特性を合わせることが好ましいため、それぞれのMFRDの差が小さければ小さいほどが好ましく、差が0.5g/10分以下であることが好ましい。
また、多孔質層には、本発明の目的を損なわない範囲内であれば、必要に応じて、酸化防止剤、紫外線吸収剤、滑剤、アンチブロッキング剤、着色剤、難燃化剤等の添加物が添加されていてもよい。
本発明の複合中空糸膜は、上述した非多孔質均質層と多孔質支持層から形成される。例えば、多層複合紡糸工程と延伸多孔質化工程により得ることができる。
中空糸膜を構成する複合膜の形態としては、気体透過性能を有する非多孔質均質層(分離層)と非多孔質均質層を支持する多孔質支持層との二層複合膜であってもよいし、気体透過性能を有する非多孔質均質層が多孔質支持層で挟まれた三層複合膜であってもよい。更に四層以上の複合膜であってもよい。特に三層以上の複合膜からなることが好ましい。
本発明の実施例の複合中空糸膜における非多孔質均質層と多孔質支持層の位置関係について、模式的な図を図1に示す。各図は模式的な概念図であり、実際の膜(層)の厚さや位置を忠実に表したものではない。
中空糸膜の膜厚(d1)は、10~200μmが好ましい。厚さが10μm以上であれば、機械的強度が向上する。さらに厚さが200μm以下であれば、本複合中空糸膜の糸外径が太くなりすぎて、膜モジュールへ内蔵する際の膜の容積効率が低くなることを抑制しやすい。
1)紡糸工程:例えば、3層構造の本複合中空糸膜であれば、最外層ノズル部、中間層ノズル部及び最内層ノズル部が、同心円状に配された複合ノズル口金を用いる。最外層ノズル部及び最内層ノズル部には、溶融状態のポリオレフィン樹脂Bを供給し、中間層ノズル部には、溶融状態のポリオレフィン樹脂Aを供給する。そして、それら各ノズル部からポリオレフィン樹脂A及びポリオレフィン樹脂Bを押し出し、押出速度と巻取速度を適宜調節しつつ未延伸状態で冷却固化する。これにより、未延伸の均質層前駆体が、非多孔質状態である2つの未延伸の多孔質層前駆体に挟まれた3層構造を有する中空糸膜前駆体が得られる。
ポリオレフィン樹脂A及びポリオレフィン樹脂Bの吐出温度は、それらが充分に溶融して紡糸できる状態であればよい。
2)延伸工程:溶融紡糸して得た未延伸の中空糸膜前駆体は、延伸前に前記融点以下で定長熱処理(アニール処理)することが好ましい。
定長熱処理は、105~120℃で、8~16時間行うことが好しい。温度が105℃以上であれば、品質の良好な本中空糸膜が得られやすい。温度が120℃以下であれば、充分な伸度が得られやすく、延伸時の安定性が向上し、高倍率での延伸が容易になる。また、処理時間が8時間以上であれば、品質の良好な本中空糸膜が得られやすい。
(i)延伸温度T(℃)と、ポリオレフィン樹脂Aの融点Tm(℃)との関係が、Tm-20≦T≦Tm+40である。
(ii)延伸温度Tが、ポリオレフィン樹脂Bのビカット軟化点以下である。
延伸温度Tが、Tm-20(℃)以上であれば、多孔質層前駆体の多孔質化が容易になり、優れた気体透過性を有する本複合中空糸膜が得られやすい。延伸温度TがTm+40(℃)以下であれば、分子に乱れが生じてピンホール等の欠陥が生じることを抑制しやすい。
また、延伸温度Tがポリオレフィン樹脂Bのビカット軟化点以下であれば、多孔質層前駆体の多孔質化が容易になり、優れた気体透過性を有する本複合中空糸膜が得られやすい。
冷延伸は、比較的低い温度下で膜の構造破壊を起させ、ミクロなクラッキングを発生させる延伸である。冷延伸の温度は、0℃から、Tm-20℃よりも低い温度までの範囲内の比較的低温下で行うことが好ましい。
延伸は、低速延伸が好ましい。低速延伸であれば、延伸時に糸径が細くなりすぎることを抑制しつつ多孔質化することが容易になる。
さらに、前記延伸により得られた中空糸膜の寸法安定性を向上させるため、該多孔質中空糸膜を定長下、又は、60%以下の範囲内で少し弛緩させた状態で熱セットを行うことが好ましい。
熱セットを効果的に行うためには、熱セット温度は延伸温度以上、融点温度以下であることが好ましい。
本発明の中空糸膜モジュールは、前述した本複合中空糸膜を具備するモジュールである。本発明の中空糸膜モジュールは、本複合中空糸膜を用いる以外は、公知の中空糸膜モジュールと同様の形態が用いられる。例えば、本複合中空糸膜を数百本束ねて筒状のハウジングに挿入し、それら本複合中空糸膜を封止材(ポッティング用樹脂)で封止した公知の形態の中空糸膜モジュールが挙げられる。
またポッティング加工部容積に対する中空糸膜の充填率が20~60%程度であることが好ましい。
本発明の脱気膜を用いた脱気方法としては、中空糸膜の内側(一次側)に溶存ガスを含む原溶液を供給し、中空糸膜の外側(二次側)を減圧とし、溶存ガスの分圧差に比例した駆動力により溶存ガスを膜透過させ、中空糸膜の外側に溶存ガスを排出することができる。また、この逆に中空糸膜の外側を一次側とし、中空糸膜の内側を二次側とすることもできる。さらには中空糸膜モジュールを複数本直列につないで対象薬液を所定の脱気水準に脱気することもできるし、また複数本並列につないで多量の薬液の脱気を行うこともできる。
DSC(セイコー電子工業製)を用い、約5mgの試料を200℃で5分間融解後、40℃まで10℃/分の速度で降温して結晶化した後に、更に10℃/分で200℃まで昇温して融解した時の融解ピーク温度及び融解終了温度で評価した。
ポリエチレンのMFRについては、JIS K7210のコードD(測定温度:190℃、荷重:2.16kg)に準拠してMFRD(単位:g/10分)を測定した。
ポリエチレンの密度(単位:kg/m3)は、JIS K7112に準拠して測定した。
ポリエチレンの比率Mw/Mnは、下記条件のGPC(高温GPC)による測定で得られたキャリブレーションカーブから、Mw及びMnをそれぞれ求めて算出した。キャリブレーションカーブは、ポリスチレンの標準試料を測定し、ポリエチレン換算定数(0.48)を使用し、3次で算出した。カラムは、下記カラム3本を順に直列に接続して用いた。
測定装置 :「150-GPC」(Waters社製)
カラム :「Shodex GPC AT-807/S」(昭和電工社製)(1本)、「Tosoh TSK-GEL GMH6-HT」(東ソー社製)(2本)
溶媒 :1,2,4-トリクロロベンゼン
カラム温度 :140℃
試料濃度 :0.05質量%(インジェクション量:500μL)
流量 :1.0mL/分
試料溶解温度:160℃
試料溶解時間:2.5時間
また、多孔質層の形成に用いるポリエチレンについては、前記高温GPCで測定した分子量分布のチャートにおいて、ショルダーピークが見られた場合、ガウス分布で近似して、低分子量成分、高分子量成分等の各成分のMw及びMn、並びにそれらの成分の配合率を算出した。
得られた気体透過複合中空糸膜の空孔率(単位:体積%)は、水銀ポロシメーター221型(カルロエルバ社製)を用いて測定した。
得られた気体透過複合中空糸膜をU字型に束ねて中空糸膜の端部をウレタン樹脂で固め、中空糸膜モジュールを作製した。複合中空糸膜の外側から酸素又は窒素を供給し、中空糸膜の内側(中空部分側)を常圧として、25℃における酸素透過速度(QO2)(単位:m/時間・MPa)及び窒素透過速度(QN2)(単位:m/時間・MPa)を測定した。なお、膜面積は、中空糸膜の内径を基に算出した。そして、測定した酸素透過速度(QO2)及び窒素透過速度(QN2)から、分離係数(QO2/QN2)を求めた。
(1)透湿度:450μm厚みのフィルムサンプルを用い、カップ法(JIS Z0208準拠、測定雰囲気:25℃×90%RH)により測定した。
(2)透湿係数:上記の透湿度より、透湿度×膜厚により算出した。
ポリオレフィン樹脂A(非多孔質均質層形成用)として、チェーンシャトリング反応触媒により製造されたエチレンとαオレフィンとのブロック共重合体(具体的には、αオレフィンが1-オクテンである、エチレン-オクテンブロック共重合体:商品名「INFUSE 9100」、ダウケミカル社製、MFRD:1.0g/10分、密度:0.877g/cm3、融点Tm:121℃、Mw/Mn=2.0)を用いた。25℃における透湿係数は0.48×10-3g/m・24hrで、さらに25℃における酸素透過係数(JISK7126)は60.7×10-16mol・m/m2・s・Paであった。
ポリオレフィン樹脂B(多孔質支持層形成用)として、高密度ポリエチレン(商品名「サンテックB161」、旭化成ケミカルズ社製、密度:0.963g/cm3、MFRD:1.35g/10分)を用いた。
最外層ノズル部、中間層ノズル部及び最内層ノズル部が、同心円状に配された複合ノズル口金を用いた。最外層ノズル部及び最内層ノズル部に溶融状態のポリオレフィン樹脂Bを供給し、中間層ノズル部に溶融状態のポリオレフィン樹脂Aを供給し、最外層からポリオレフィン樹脂A/ポリオレフィン樹脂B/ポリオレフィン樹脂Aを12/1/2の比率になるように吐出し、それらポリオレフィンを、巻取速度135m/分で紡糸して、未延伸の中空糸膜前駆体を得た。該中空糸膜前駆体は、均質層前駆体が、2つの多孔質層前駆体で挟まれた3層が同心円状に配されていた。
前記中空糸膜前駆体を、108℃で8時間アニール処理した。次いで、23±2℃で1.6倍延伸し、引き続き105℃の加熱炉中で、総延伸量が580%になるまで熱延伸を行い、2つの多孔質層前駆体を多孔質化した。その後、115℃の加熱炉中で45%の緩和工程を設け、最終的に総延伸倍率(未延伸の中空糸膜前駆体に対する倍率)が400%になるように成形し、気体透過複合中空糸膜を得た。
作成した複合中空糸膜は、内径165μm、外径262μm、膜厚48.3μmとなっており、非多孔質均質層は、内側から膜厚の約1/8の位置にあった。
複合中間糸膜の空気透過速度を測定したところ、室温(25℃)における酸素透過速度(QO2)は0.244m/hr・Mpa、窒素透過速度(QN2)は0.074m/hr・Mpaであり、分離係数(QO2/QN2)は3.3であった。薄膜層に用いたポリマーの分離係数3.3が維持されているためにイソプロピルアルコール(IPA)を通液してもリークを生じなかった。
さらに、作成した気体透過複合中空糸膜を使用して中空糸膜モジュールを作成した。中空糸膜の内側に50℃の水を流し、中空糸膜の外側から二酸化炭素を吹き込んで炭酸水を生成するようにして1ヶ月運転したが膜の水蒸気透過性の低さの為に気相側に凝結水を生じなかった。
ポリオレフィン樹脂A(非多孔質均質層形成用)として、チェーンシャトリング反応触媒により製造されたエチレンとαオレフィンとのブロック共重合体(具体的には、αオレフィンが1-オクテンである、エチレン-オクテンブロック共重合体:商品名「INFUSE 9107」、ダウケミカル社製、MFRD:1.0g/10分、密度:0.866g/cm3、融点Tm:120℃、Mw/Mn=2.0)を用いた。25℃における透湿係数は0.76×10-3g/m・24hrであり、さらに25℃における酸素透過係数(JISK7126)が85.1×10-16mol・m/m2・s・Paであった。
吐出温度180℃、巻取速度135m/分で紡糸を実施した。得られた未延伸中空糸は内径160μmであり、三層が同心円状に配されていた。該未延伸中空糸を108℃で8時間アニール処理をした。更に該アニール糸を23±2℃下で1.6倍延伸し、引き続き105℃の加熱炉中で、総延伸量が5.8倍になるまで熱延伸を行い、2つの多孔質層支持層前駆体を多孔質化した。その後、115℃の加熱炉中で0.69倍の緩和工程を設け、最終的に総延伸倍率(未延伸の中空糸膜前駆体に対する倍率)が4倍になるように成形し、気体透過複合中空糸膜を得た。作成した多層複合中空糸膜は、内径は156μm、外径251μm、膜厚47.6μmとなっており非多孔質均質層は、内側から膜厚の約1/8の位置にあった。
複合中間糸膜の空気透過速度を測定したところ、室温(25℃)における酸素透過速度(QO2)は0.400m/hr・Mpa、窒素透過速度(QN2)は0.142m/hr・Mpaであり、分離係数(QO2/QN2)は2.8であった。薄膜層に用いたポリマーの分離係数2.8が維持されているために溶剤(IPA)を通液してもリークを生じなかった。
さらに、作成した気体透過複合中空糸膜を使用して中空糸膜モジュールを作成した。中空糸膜の内側に50℃の水を流し、中空糸膜の外側から二酸化炭素を吹き込んで炭酸水を生成するようにして1ヶ月運転したが膜の水蒸気透過性の低さの為に気相側に凝結水を生じなかった。
ポリオレフィン樹脂A(非多孔質均質層形成用)として、メタロセン系触媒により製造されたエチレンとαオレフィンとのランダム共重合体(具体的には、αオレフィンが1-オクテンである、エチレン-オクテンランダム共重合体(商品名「アフィニティEG8100G」、ダウケミカル社製、MFRD:1.0g/10分、密度:0.870g/cm3、融点Tm:55℃、Mw/Mn=2.0)を用いた。25℃における透湿係数は4.5×10-3g/m・24hrであり、さらに25℃における酸素透過係数(JISK7126)が69×10-16mol・m/m2・s・Paであった。
ポリオレフィン樹脂B(多孔質支持層形成用)は、実施例1と同じにし、吐出量比も実施例1と同様に行った。
吐出温度180℃、巻取速度130m/分で紡糸を実施した。得られた未延伸中空糸は内径180μmであり、三層が同心円状に配されていた。該未延伸中空糸を108℃で8時間アニール処理をした。更に該アニール糸を23±2℃下で120%延伸し、引き続き70℃の加熱炉中で総延伸量が400%になるまで熱延伸を行い、複合中空糸膜を得た。作成した多層複合中空糸膜は、内径は160μm、外径256μm、膜厚48μmとなっており、非多孔質均質層は、内側から膜厚の約1/8の位置にあった。
複合中間糸膜の空気透過速度を測定したところ、室温(25℃)における酸素透過速度(QO2)は0.36m/hr・Mpa、窒素透過速度(QN2)は0.13m/hr・Mpaであり、分離係数(QO2/QN2)は2.8であった。薄膜層に用いたポリマーの分離係数2.8が維持されているために溶剤(IPA)を通液してもリークを生じなかった。
さらに、作成した気体透過複合中空糸膜を使用して中空糸膜モジュールを作成した。中空糸膜の内側に50℃の水を流し、中空糸膜の外側から二酸化炭素を吹き込んで炭酸水を生成するようにして運転した。当初は凝結水を生じることなく運転可能であったが、4日目で均質層が軟化することにより強度が低下しリークを生じた。
均質層形成用として、熱可塑性ポリウレタン(DIC Bayer Polymer (社)製 Pandex T8375N)を用いた。 Pandex T8375NのJIS Z0208 カップ法による25℃における透湿係数は25.9g/m・24hrであり、さらに25℃における酸素透過係数(JISK7126)は19.0×10-16mol・m/m2・s・Paであった。
ポリオレフィン樹脂B(多孔質層形成用)は、実施例1と同じにし、吐出量比は、最外層からポリオレフィン樹脂A/熱可塑性ポリウレタンB/ポリオレフィン樹脂Aを12/1/2の比率になるように吐出しも実施例1と同様に行った。
吐出温度180℃、巻取速度90m/分で紡糸を実施した。得られた未延伸中空糸は内径200μmであり、三層が同心円状に配されていた。該未延伸中空糸を108℃で8時間アニール処理をした。更に該アニール糸を23±2℃下で160%延伸し、引き続き110℃の加熱炉中で総延伸量が300%になるまで熱延伸を行い、複合中空糸膜を得た。作成した多層複合中空糸膜は、内径は200μm、外径280μm、膜厚25μmとなっており非多孔質均質層は、内側から膜厚の約1/8の位置にあった。
複合中間糸膜の空気透過速度を測定したところ、室温(25℃)における酸素透過速度(QO2)は0.28m/hr・Mpa、窒素透過速度(QN2)は0.10m/hr・Mpaであり、分離係数(QO2/QN2)は2.8であった。薄膜層に用いたポリマーの分離係数2.8が維持されていた。さらに、作成した気体透過複合中空糸膜を使用して中空糸膜モジュールを作成した。中空糸膜の内側に50℃の水を流し、中空糸膜の外側から二酸化炭素を吹き込んで炭酸水を生成するようにして運転した。24hr後には凝結水と思われる水の侵出を確認した。
2:非多孔質均質層
3:多孔質支持層(外層)
d1:中空糸膜厚さ
d2:中空糸膜最内面から非多孔質均質層までの距離
Claims (11)
- ポリオレフィン樹脂Aを主成分とする気体を透過する非多孔質均質層と、該非多孔質均質層を支持するポリオレフィン樹脂Bを主成分とする多孔質支持層とを有する複合中空糸膜において、前記非多孔質均質層のポリオレフィン樹脂Aが、エチレン単位と炭素数3~20のα-オレフィン単位から選ばれる少なくとも1種のオレフィン単位とのブロック共重合体である複合中空糸膜。
- 非多孔質均質層の前記α-オレフィン単位が、炭素数6~20のα-オレフィン単位である請求項1に記載の複合中空糸膜。
- 非多孔質均質層の前記α-オレフィン単位が、1-オクテン単位である請求項2に記載の複合中空糸膜。
- 非多孔質均質層のポリオレフィン樹脂Aの25℃における酸素透過係数(JISK7126)が50×10-16mol・m/m2・s・Pa以上であることを特徴とする請求項1~3のいずれか一項に記載の複合中空糸膜。
- 非多孔質均質層のポリオレフィン樹脂Aの25℃における透湿係数が3.00×10⁻³g/m・24hr以下であることを特徴とする請求項1~4のいずれか一項に記載の複合中空糸膜。
- 非多孔質均質層を支持する多孔質支持層が、非多孔質均質層の外層側に配置されていると共に、非多孔質均質層が、中空糸膜の最内面から膜厚方向に膜厚の1/10~1/4以内の領域に配置されていることを特徴とする請求項1~5のいずれか一項に記載の複合中空糸膜。
- 非多孔質均質層のポリオレフィン樹脂Aの密度が0.86~0.89g/cm3であることを特徴とする請求項1~6のいずれか一項に記載の複合中空糸膜。
- 非多孔質均質層のポリオレフィン樹脂Aが、100℃以上、135℃以下の融点を有することを特徴とする請求項1~7のいずれか一項に記載の複合中空糸膜。
- 非多孔質均質層のポリオレフィン樹脂Aの、JIS K7210のコードDに準拠して測定したMFRDが0.1~1.0g/10分・190℃にあることを特徴とする請求項1~8のいずれか一項に記載の複合中空糸膜。
- 前記ポリオレフィン樹脂Aが、ポリエチレンである請求項1~9のいずれか一項に記載の複合中空糸膜。
- 請求項1~10のいずれか一項に記載の気体透過複合中空糸膜を具備する中空糸膜モジュール。
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US14/388,616 US9694326B2 (en) | 2012-03-30 | 2013-03-29 | Composite hollow fiber membrane and hollow fiber membrane module |
| CN201380028652.XA CN104334264B (zh) | 2012-03-30 | 2013-03-29 | 复合中空纤维膜及中空纤维膜组件 |
| KR1020147026600A KR101763461B1 (ko) | 2012-03-30 | 2013-03-29 | 복합 중공사막 및 중공사막 모듈 |
| EP13767601.1A EP2832431A4 (en) | 2012-03-30 | 2013-03-29 | HOLLOW FIBER COMPOSITE MEMBRANE AND HOLLOW FIBER MEMBRANE MODULE |
| JP2013519665A JP6347398B2 (ja) | 2012-03-30 | 2013-03-29 | 複合中空糸膜及び中空糸膜モジュール |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2012080259 | 2012-03-30 | ||
| JP2012-080259 | 2012-03-30 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2013147186A1 true WO2013147186A1 (ja) | 2013-10-03 |
Family
ID=49260427
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2013/059594 Ceased WO2013147186A1 (ja) | 2012-03-30 | 2013-03-29 | 複合中空糸膜及び中空糸膜モジュール |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US9694326B2 (ja) |
| EP (1) | EP2832431A4 (ja) |
| JP (1) | JP6347398B2 (ja) |
| KR (1) | KR101763461B1 (ja) |
| CN (1) | CN104334264B (ja) |
| WO (1) | WO2013147186A1 (ja) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2013202575A (ja) * | 2012-03-29 | 2013-10-07 | Mitsubishi Rayon Co Ltd | 脱気用複合中空糸膜及び中空糸膜モジュール |
| JP2015167939A (ja) * | 2014-03-10 | 2015-09-28 | 三菱レイヨン株式会社 | 脱気用中空糸膜モジュール |
| JP2015167940A (ja) * | 2014-03-10 | 2015-09-28 | 三菱レイヨン株式会社 | 脱気用中空糸膜モジュール |
| CN108686521A (zh) * | 2017-03-31 | 2018-10-23 | 旭化成医疗株式会社 | 中空纤维膜、中空纤维膜型血液净化器 |
| DE102018129165A1 (de) * | 2018-11-20 | 2020-05-20 | UMS Gmbh & Co KG | Gasdruckmessvorrichtung mit Hohlfasermembranbündel |
| JP2022147224A (ja) * | 2021-03-23 | 2022-10-06 | 三菱ケミカル株式会社 | 中空糸膜、中空糸膜モジュール、廃水処理装置及び廃水処理方法 |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| KR101482477B1 (ko) * | 2010-09-29 | 2015-01-13 | 미쯔비시 레이온 가부시끼가이샤 | 폴리올레핀 복합 중공사막 및 그 제조 방법, 그리고 중공사막 모듈 |
| KR101662518B1 (ko) | 2014-09-30 | 2016-10-06 | 현대자동차주식회사 | 테일게이트의 랫치 구조 |
| AU2015258191B2 (en) | 2014-11-19 | 2020-02-27 | Flexopack S.A. | Oven skin packaging process |
| CN109641182B (zh) * | 2016-08-30 | 2022-06-03 | 杜邦安全与建筑公司 | 多层中空纤维膜 |
| EP3501822A1 (en) | 2017-12-22 | 2019-06-26 | Flexopack S.A. | Fibc liner film |
| US11986777B2 (en) | 2018-12-27 | 2024-05-21 | 3M Innovative Properties Company | Hollow fiber membranes with nucleating agent and methods of making and using the same |
| EP3902624A4 (en) | 2018-12-27 | 2022-09-21 | 3M Innovative Properties Company | ASYMMETRIC HOLLOW FIBER MEMBRANES AND METHOD OF MAKING AND USE THEREOF |
| CN117619160A (zh) * | 2022-08-26 | 2024-03-01 | 中国石油化工股份有限公司 | 制备中空纤维复合膜的方法和中空纤维复合膜 |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01147565A (ja) | 1987-12-04 | 1989-06-09 | Konica Corp | 多色画像形成装置 |
| JPH02279158A (ja) | 1989-04-20 | 1990-11-15 | Kao Corp | 浴湯用炭酸温水の生成方法及び装置 |
| JPH07116483A (ja) * | 1993-10-26 | 1995-05-09 | Dainippon Ink & Chem Inc | 中空糸複合膜の製造方法 |
| JP2000271549A (ja) | 1999-03-25 | 2000-10-03 | Kurita Water Ind Ltd | ガス溶解水供給装置 |
| JP2007529617A (ja) | 2004-03-17 | 2007-10-25 | ダウ グローバル テクノロジーズ インコーポレイティド | エチレンマルチブロックコポリマーを形成するためのシャトリング剤を含む触媒組成物 |
| JP2008272696A (ja) * | 2007-05-02 | 2008-11-13 | Mitsubishi Rayon Eng Co Ltd | 脱気用複合中空糸膜及びその製造方法 |
| JP2008289977A (ja) * | 2007-05-23 | 2008-12-04 | Mitsubishi Rayon Eng Co Ltd | 脱気用中空糸膜モジュールの製造方法 |
| JP2010155207A (ja) | 2008-12-26 | 2010-07-15 | Kuraray Co Ltd | ガス分離膜用エチレン−ビニルアルコール系重合体複合膜 |
| WO2012043613A1 (ja) * | 2010-09-29 | 2012-04-05 | 三菱レイヨン株式会社 | ポリオレフィン複合中空糸膜及びその製造方法、並びに中空糸膜モジュール |
Family Cites Families (21)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3581900A (en) * | 1967-10-25 | 1971-06-01 | Aqua Chem Inc | Reverse osmosis liquid purification |
| US5409515A (en) * | 1992-01-14 | 1995-04-25 | Daikin Industries, Ltd. | Filter apparatus and filter element |
| US6036030A (en) * | 1994-02-02 | 2000-03-14 | Bechtel Bwxt Idaho Llc | Method for producing a selectively permeable separation module |
| EP0790279B2 (en) * | 1996-02-19 | 2007-07-18 | Sumitomo Chemical Company, Limited | Liquid crystal polyester resin composition |
| US6354444B1 (en) * | 1997-07-01 | 2002-03-12 | Zenon Environmental Inc. | Hollow fiber membrane and braided tubular support therefor |
| JP4139456B2 (ja) * | 1997-10-02 | 2008-08-27 | 三菱レイヨン株式会社 | 脱気膜 |
| JP2974999B2 (ja) | 1998-04-10 | 1999-11-10 | 三菱レイヨン株式会社 | 膜型人工肺 |
| JP2000084368A (ja) * | 1998-09-08 | 2000-03-28 | Mitsubishi Rayon Co Ltd | 薬液脱気用複合中空糸膜 |
| DE60120774T2 (de) * | 2000-12-21 | 2007-05-24 | Japan Polychem Corp. | Ethylenpolymere |
| WO2004009611A2 (en) * | 2002-07-24 | 2004-01-29 | Cuno, Inc. | Multiple layer membrane and method for fabrication thereof |
| US7355089B2 (en) | 2004-03-17 | 2008-04-08 | Dow Global Technologies Inc. | Compositions of ethylene/α-olefin multi-block interpolymer for elastic films and laminates |
| EP2221329B1 (en) * | 2004-03-17 | 2014-11-26 | Dow Global Technologies LLC | Catalyst composition comprising shuttling agent for ethylene multi-block copolymer formation |
| US7422796B2 (en) * | 2005-07-19 | 2008-09-09 | E. I. Du Pont De Nemours And Company | Film structures having improved oxygen transmission |
| JP5013769B2 (ja) * | 2006-08-03 | 2012-08-29 | 株式会社ノリタケカンパニーリミテド | 酸素分離膜 |
| WO2008134503A1 (en) * | 2007-04-27 | 2008-11-06 | Dow Global Technologies Inc. | αMICROPOROUS FILMS FROM COMPATIBILIZED POLYMERIC BLENDS |
| EP2197942A2 (en) * | 2007-09-28 | 2010-06-23 | Dow Global Technologies Inc. | Dispersions of higher crystallinity olefins |
| AU2011312881B2 (en) * | 2010-09-30 | 2015-07-16 | Porifera, Inc. | Thin film composite membranes for forward osmosis, and their preparation methods |
| US20140096825A1 (en) * | 2011-06-30 | 2014-04-10 | Dow Global Technologies Llc | Multilayered polyolefin-based films having integrated backsheet and encapsulation performance comprising a layer comprising crystalline block copolymer composite or block copolymer composite |
| US20140360560A1 (en) * | 2012-01-13 | 2014-12-11 | Mitsubishi Plastics, Inc. | Solar cell module having excellent appearance and method for manufacturing same |
| KR20210054589A (ko) * | 2012-11-06 | 2021-05-13 | 셀가드 엘엘씨 | 공중합체 멤브레인, 섬유, 제품 및 방법 |
| CN104955431A (zh) * | 2013-02-01 | 2015-09-30 | 宝洁公司 | 具有隔离片的尿布 |
-
2013
- 2013-03-29 EP EP13767601.1A patent/EP2832431A4/en not_active Withdrawn
- 2013-03-29 CN CN201380028652.XA patent/CN104334264B/zh not_active Expired - Fee Related
- 2013-03-29 JP JP2013519665A patent/JP6347398B2/ja not_active Expired - Fee Related
- 2013-03-29 KR KR1020147026600A patent/KR101763461B1/ko not_active Expired - Fee Related
- 2013-03-29 US US14/388,616 patent/US9694326B2/en not_active Expired - Fee Related
- 2013-03-29 WO PCT/JP2013/059594 patent/WO2013147186A1/ja not_active Ceased
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01147565A (ja) | 1987-12-04 | 1989-06-09 | Konica Corp | 多色画像形成装置 |
| JPH02279158A (ja) | 1989-04-20 | 1990-11-15 | Kao Corp | 浴湯用炭酸温水の生成方法及び装置 |
| JPH07116483A (ja) * | 1993-10-26 | 1995-05-09 | Dainippon Ink & Chem Inc | 中空糸複合膜の製造方法 |
| JP2000271549A (ja) | 1999-03-25 | 2000-10-03 | Kurita Water Ind Ltd | ガス溶解水供給装置 |
| JP2007529617A (ja) | 2004-03-17 | 2007-10-25 | ダウ グローバル テクノロジーズ インコーポレイティド | エチレンマルチブロックコポリマーを形成するためのシャトリング剤を含む触媒組成物 |
| JP2008272696A (ja) * | 2007-05-02 | 2008-11-13 | Mitsubishi Rayon Eng Co Ltd | 脱気用複合中空糸膜及びその製造方法 |
| JP2008289977A (ja) * | 2007-05-23 | 2008-12-04 | Mitsubishi Rayon Eng Co Ltd | 脱気用中空糸膜モジュールの製造方法 |
| JP2010155207A (ja) | 2008-12-26 | 2010-07-15 | Kuraray Co Ltd | ガス分離膜用エチレン−ビニルアルコール系重合体複合膜 |
| WO2012043613A1 (ja) * | 2010-09-29 | 2012-04-05 | 三菱レイヨン株式会社 | ポリオレフィン複合中空糸膜及びその製造方法、並びに中空糸膜モジュール |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP2832431A4 |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2013202575A (ja) * | 2012-03-29 | 2013-10-07 | Mitsubishi Rayon Co Ltd | 脱気用複合中空糸膜及び中空糸膜モジュール |
| JP2015167939A (ja) * | 2014-03-10 | 2015-09-28 | 三菱レイヨン株式会社 | 脱気用中空糸膜モジュール |
| JP2015167940A (ja) * | 2014-03-10 | 2015-09-28 | 三菱レイヨン株式会社 | 脱気用中空糸膜モジュール |
| CN108686521A (zh) * | 2017-03-31 | 2018-10-23 | 旭化成医疗株式会社 | 中空纤维膜、中空纤维膜型血液净化器 |
| DE102018129165A1 (de) * | 2018-11-20 | 2020-05-20 | UMS Gmbh & Co KG | Gasdruckmessvorrichtung mit Hohlfasermembranbündel |
| JP2022147224A (ja) * | 2021-03-23 | 2022-10-06 | 三菱ケミカル株式会社 | 中空糸膜、中空糸膜モジュール、廃水処理装置及び廃水処理方法 |
| JP7643125B2 (ja) | 2021-03-23 | 2025-03-11 | 三菱ケミカル株式会社 | 中空糸膜、中空糸膜モジュール、廃水処理装置及び廃水処理方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2832431A1 (en) | 2015-02-04 |
| JP6347398B2 (ja) | 2018-06-27 |
| US9694326B2 (en) | 2017-07-04 |
| KR20140130719A (ko) | 2014-11-11 |
| CN104334264A (zh) | 2015-02-04 |
| EP2832431A4 (en) | 2015-04-22 |
| KR101763461B1 (ko) | 2017-07-31 |
| CN104334264B (zh) | 2016-11-16 |
| US20150122129A1 (en) | 2015-05-07 |
| JPWO2013147186A1 (ja) | 2015-12-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6347398B2 (ja) | 複合中空糸膜及び中空糸膜モジュール | |
| CN103228344B (zh) | 聚烯烃复合中空纤维膜及其制造方法和中空纤维膜组件 | |
| JPWO2013147187A1 (ja) | 複合中空糸膜及び中空糸膜モジュール | |
| JP4139456B2 (ja) | 脱気膜 | |
| KR101151189B1 (ko) | 기체 분리막 | |
| JP5500765B2 (ja) | 脱気用複合中空糸膜及びその製造方法 | |
| JP5393971B2 (ja) | 脱気用複合中空糸膜 | |
| US10537856B2 (en) | Hollow fiber membrane and hollow fiber membrane module | |
| Wang et al. | Construction of high-performance thin-film composite membrane for CO2 separation via interface engineering | |
| US20170320020A1 (en) | Method for producing a carbon hollow fiber membrane | |
| CN103228341B (zh) | 聚乙烯多孔质中空纤维膜、净水器用滤芯和中空纤维膜组件 | |
| WO2022230923A1 (ja) | 分離膜及びその製造方法 | |
| JP2015016400A (ja) | 中空糸膜及び脱気用中空糸膜モジュール | |
| JP5885123B2 (ja) | 脱気用複合中空糸膜及び中空糸膜モジュール | |
| JP2008272697A (ja) | 中空糸膜モジュール及びその製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| ENP | Entry into the national phase |
Ref document number: 2013519665 Country of ref document: JP Kind code of ref document: A |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 13767601 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 20147026600 Country of ref document: KR Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 14388616 Country of ref document: US |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2013767601 Country of ref document: EP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |