WO2014178305A1 - Procédé de production d'un article absorbant et article absorbant - Google Patents
Procédé de production d'un article absorbant et article absorbant Download PDFInfo
- Publication number
- WO2014178305A1 WO2014178305A1 PCT/JP2014/061257 JP2014061257W WO2014178305A1 WO 2014178305 A1 WO2014178305 A1 WO 2014178305A1 JP 2014061257 W JP2014061257 W JP 2014061257W WO 2014178305 A1 WO2014178305 A1 WO 2014178305A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- main body
- sheet
- body sheet
- absorbent
- absorbent article
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images



Classifications
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/15577—Apparatus or processes for manufacturing
- A61F13/15756—Applying tabs, strips, tapes, loops; Knotting the ends of pads
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/15577—Apparatus or processes for manufacturing
- A61F13/15707—Mechanical treatment, e.g. notching, twisting, compressing, shaping
- A61F13/15747—Folding; Pleating; Coiling; Stacking; Packaging
-
- A—HUMAN NECESSITIES
- A61—MEDICAL OR VETERINARY SCIENCE; HYGIENE
- A61F—FILTERS IMPLANTABLE INTO BLOOD VESSELS; PROSTHESES; DEVICES PROVIDING PATENCY TO, OR PREVENTING COLLAPSING OF, TUBULAR STRUCTURES OF THE BODY, e.g. STENTS; ORTHOPAEDIC, NURSING OR CONTRACEPTIVE DEVICES; FOMENTATION; TREATMENT OR PROTECTION OF EYES OR EARS; BANDAGES, DRESSINGS OR ABSORBENT PADS; FIRST-AID KITS
- A61F13/00—Bandages or dressings; Absorbent pads
- A61F13/15—Absorbent pads, e.g. sanitary towels, swabs or tampons for external or internal application to the body; Supporting or fastening means therefor; Tampon applicators
- A61F13/56—Supporting or fastening means
- A61F13/5622—Supporting or fastening means specially adapted for diapers or the like
- A61F13/5633—Supporting or fastening means specially adapted for diapers or the like open type diaper
Definitions
- the present invention relates to a method of manufacturing an absorbent article, etc., having an absorbent body, a side flap extending outward in the width direction of the absorbent body, and a fastening member joined to the side flap.
- Patent Document 1 discloses an absorbent body and an absorbent main body having a surface sheet disposed on the skin-contacting surface side of the absorbent body, a side flap extending outward in the width direction of the absorbent main body, and a side flap A method of manufacturing an absorbent article having a fastening member is disclosed.
- the manufacturing method of the absorbent article of patent document 1 joins the side flap folded in the 1st process and the 1st process which folds the side flap to which the fastening member was joined along a longitudinal direction to an absorptive main part. And a second step.
- the side flaps of the absorbent article of Patent Document 1 are not provided continuously throughout the longitudinal direction of the absorbent article, but are intermittently disposed in the longitudinal direction. Therefore, after folding the side flaps in the first step of Patent Document 1, there is a possibility that each side flap may be individually folded back to the original state, and it can not be stably maintained that all the side flaps are folded. is there.
- the absorbent has a large thickness among the constituent members constituting the absorbent article. Therefore, the thickness is different between the region where the absorbent body of the absorbent main body is disposed and the region where the absorbent body is not disposed, and a step is formed on the absorbent main body.
- the side flaps are joined to the absorbent main body on which the step is formed, so that the entire joint surface of the side flaps can not be joined or the joint portion between the side flaps and the absorbent main body Wrinkling may occur or bonding failure may occur.
- the present invention stably stabilizes the folded state of the side flaps in an absorbent article having an absorbent body having an absorbent body and a surface sheet, and side flaps extending outward in the width direction of the absorbent body. It is an object of the present invention to provide a method of manufacturing an absorbent article and an absorbent article, which can be maintained, wrinkles and twists of joints of the side flaps and the absorbent main body, and position deviation of the side flaps.
- a method of manufacturing an absorbent article includes an absorbent body, an absorbent main body having a main body sheet disposed on the skin contact surface side of the absorbent body, and the absorbent main body A side flap extending to the outside in the width direction more than the other, and a fastening member joined to the side flap and fastened to the non-skin-contacting side surface of the absorbent main body;
- An absorbent article for producing an absorbent article wherein the length in the longitudinal direction is shorter than the length in the longitudinal direction of the absorbent article, and the length in the longitudinal direction of the main body sheet is the entire area in the longitudinal direction of the absorbent article.
- the method for manufacturing a semiconductor device comprising: bonding the fastening member to the side flap; bonding the side flap to which the fastening member is bonded to the main body sheet; and End in the width direction of the body sheet And a step of folding along, and a step of integrating said body sheet the side flaps are folded and the absorbent body.
- the absorbent article according to the present disclosure includes an absorbent body, and an absorbent main body having a main body sheet disposed on the skin-contacting surface side of the absorbent, and extends outward in the width direction than the absorbent main body.
- An absorbent article comprising: a side flap; and a fastening member joined to the side flap and fastened to the non-skin-contacting surface of the absorbent main body, wherein the fastening member is joined In a state where the side flaps are joined to the main body sheet, after the side flaps are folded along the end portion in the width direction of the main body sheet, the main body sheet and the absorber are integrated.
- an absorbent article capable of suppressing wrinkles between the joint portion of the side flaps and the absorbent main body and positional deviation of the side flaps.
- An absorbent article can be provided.
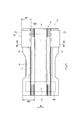
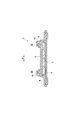
- FIG. 2 is a cross-sectional view taken along the line AA shown in FIG. It is a top view of the state which folded up the side flap of the absorbent article shown in FIG.
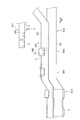
- FIG. 4 is a cross-sectional view taken along the line BB shown in FIG. It is a figure which shows typically the manufacturing method of the absorbent article which concerns on embodiment. It is a figure which shows typically the manufacturing method of the absorbent article which concerns on a modification.
- FIG. 1 is a plan view showing the absorbent article 1 according to the present embodiment.
- the top view shown in FIG. 1 is the state which expanded the main body sheet etc. to the state which can not see wrinkles, such as leg gathers provided in an absorbent article.
- the absorbent article 1 is an open-type disposable diaper.
- the open-type diaper is not a diaper that has been formed into a pants-type in advance, but is in a deployed state before use, and the predetermined parts of the product are fastened by fastening members or the like. Refers to diapers worn by the user.
- Absorbent article 1 corresponds to front waist area S1 corresponding to the wearer's front waist, back waist area S2 corresponding to the wearer's back waist, and crotch of the wearer in the longitudinal direction L of absorbent article 1 And a crotch region S3 located between the front waist region S1 and the rear waist region S2.
- the absorbent article 1 includes an absorbent main body 2 and side flaps 10 extending outward in the width direction of the absorbent main body 2.
- the side flaps 10 are disposed in the rear waist region.
- the absorbent main body 2 is disposed across the front waist region, the crotch region and the back waist region.
- the crotch region is a region in which the widthwise outer end of the absorbent body is recessed inward in the width direction with respect to the front waist region and the rear waist region.
- the widthwise outer end of the crotch region constitutes a pair of leg-surrounding openings 21 arranged along the circumference of the wearer's leg.
- the absorbent main body 2 includes an absorbent body 3, a main body sheet 4 disposed on the skin contact surface side of the absorbent body 3, a liquid permeable surface sheet 5 covering the skin contact surface of the absorbent body 3, and an absorbent body A back sheet 6 disposed on the non-skin-contacting surface 3 side, a leg side elastic member 7 as a main body elastic member, and a leg elastic member 8 positioned outside in the width direction of the leg side elastic member 7 .
- the surface sheet 5 covers the skin contact surface of the absorber.
- the surface sheet 5 should just be comprised so that the skin contacting surface of the absorber 3 may be covered at least.
- the top sheet 5 of the present embodiment extends outward in the width direction more than the absorber 3.
- the top sheet 5 is formed of a liquid-permeable sheet such as a hydrophilic non-woven fabric, a woven fabric, an apertured plastic film, or an apertured hydrophobic non-woven fabric.
- the main body sheet 4 is disposed on the skin contact surface side of the absorber.
- the main body sheet 4 covers the widthwise outer end of the topsheet 5 and extends outward in the widthwise direction more than the topsheet 5.
- the main body sheet 4 may be disposed on the skin contact surface side of the absorber 3 and may be disposed so as not to overlap with the surface sheet 5 or provided so as not to overlap with the absorbent body 3 It is also good.
- the main sheet 4 may be formed of a liquid-permeable sheet such as a hydrophilic non-woven fabric, a woven fabric, an apertured plastic film, or an apertured hydrophobic non-woven fabric, or may be formed of a liquid-impermeable sheet.
- the widthwise inner end of the main body sheet 4 is folded at the origin along a fold along the longitudinal direction.
- the leg side elastic member 7 is joined between the folded body sheets 4.
- the leg side elastic members 7 expand and contract at least in the longitudinal direction.
- the main body sheet 4 and the leg side elastic members 7 constitute upright leg side gathers positioned closer to the skin contact surface than the absorber 3.
- the absorber 3 is provided between the top sheet 5 and the back sheet 6.
- the absorber 3 absorbs excrement such as body fluid of the wearer.
- the absorbent body 3 is formed of an absorbent core such as ground pulp or superabsorbent polymer as fibers, and a core wrap that wraps the absorbent core.
- the absorbent body 3 is provided with a plurality of slits 3A along the longitudinal direction L of the absorbent article.
- the slits 3A are arranged in three rows at intervals in the longitudinal direction, and are arranged in three rows at intervals in the width direction W of the absorbent article.
- the back sheet 6 is formed of a liquid impermeable film (hereinafter referred to as a back film) formed of a waterproof film (for example, polyethylene) or the like.
- a target portion 6A to which the fastening member is fastened is provided in the front waistline region of the back sheet.
- the leg elastic members 8 are disposed along the leg-openings 21 in the crotch region.
- the leg elastic members expand and contract at least in the longitudinal direction.
- Three leg elastic members 8 of the present embodiment are arranged at intervals in the width direction.
- the back surface sheet 6 of this Embodiment is arrange
- an exterior sheet is provided in the non-skin contact surface side of a back surface sheet.
- the outer cover sheet may be configured to abut on the clothes.
- the side flaps 10 are sheets that extend outward in the width direction than the absorbent main body.
- the side flaps 10 are joined between the main sheet 4 and the back sheet 6.
- the side flaps 10 are made of, for example, a liquid-permeable nonwoven sheet.
- the length in the longitudinal direction of the main body sheet 4 is the entire area in the longitudinal direction of the absorbent article.
- the length in the longitudinal direction of the side flap 10 is shorter than the length in the longitudinal direction of the absorbent article, and is the length of a part in the longitudinal direction of the absorbent article. Therefore, when manufacturing an absorbent article, the main body sheet 4 conveys the main body sheet continuum 4C (refer to FIG. 5) continued in the conveyance direction, and the side flaps 10 are intermittently made to the main body sheet continuum 4C. Deploy.
- the side flap 10 of this Embodiment is provided only in a back waist area, it may be provided not only in a back waist area but in a front waist area.
- the fastening member 11 extends outward in the width direction of the side flaps 10 of the rear waist area S2.
- the fastening member 11 is joined to the widthwise outer end of the side flap 10.
- the fastening member 11 is configured to be fastened to the target portion 6A of the front waist area S1.
- the fastening member 11 is formed of a surface fastener, an adhesive, or the like.
- the fastening member of the present embodiment is made of an adhesive.
- the fastening member 11 is joined to the surface on the skin contact side of the side flap 10 and the surface on the non-skin contact side, and is provided on both sides of the side flap 10.
- the fastening member 11 realizes a state of being deployed outward in the width direction (the state of the fastening member on the upper side in FIG. 1) and a folded state (a state of the fastening member on the lower side in FIG. 1).
- the fastening member 11 is in a folded state prior to use.
- the adhesive surface of the fastening member 11 to which the adhesive is applied is disposed on the inner side in the thickness direction before use.
- the fastening member 11 is deployed by the wearer during use to expose the adhesive surface.
- the wearer pulls the side flap 10 toward the front waist region side with the front waist region of the absorbent article placed on the ventral side of the wearer and the rear waist region of the absorbent article placed on the dorsal side of the wearer.
- the absorbent article By bonding the adhesive surface of the fastening member 11 to the target portion 6A in the front waist area, the absorbent article can be held on the wearer's body.
- FIG. 3 is a plan view of the absorbent article 1 in a state in which the side flaps 10 are folded
- FIG. 4 is a cross-sectional view taken along the line BB shown in FIG.
- the method of manufacturing the absorbent article includes a bonding step S11 of the side flap 10 and the fastening member 11, a bonding step S12 of the main sheet 4 and the top sheet 5, a bonding step S13 of the side flap 10 and the main sheet 4, and a side flap At least a folding step S14 and an absorber bonding step S15 are included.
- the fastening member 11 is joined to the side flap continuum 10C in which the side flaps are continuous in the longitudinal direction. Specifically, the fastening member 11 is joined to the outer end in the width direction of the side flap continuous body 10C. The end to which the fastening member 11 is joined is the end 10A of the side flap 10 located on the outer side in the width direction when attached to the absorbent main body and the side flap is deployed. Then, the individual side flaps 10 to which the fastening member 11 is joined can be manufactured by cutting the side flap continuum 10C into the product length of the side flaps.
- fastening member 11 is joined to the side flap continuous body 10C, for example, fastening is performed to the outer end in the width direction of the side flap 10 cut into individual product lengths.
- the members 11 may be joined.
- the method of joining of the side flap 10 and a fastening member can use various methods, it can join by an adhesive agent, for example.
- the fastening member of this embodiment is joined to the skin contact side and the non-skin contact side of the side flap 10, the skin and the skin side of the side flap 10 are not It may be joined to at least one of the contact side surfaces.
- the main sheet 4 and the top sheet are bonded. More specifically, a body sheet continuum 4C in which the body sheet 4 is continuous in the longitudinal direction and a top sheet continuum 5C in which the surface sheet is continuous in the longitudinal direction are joined.
- the main body sheet continuum 4C and the top sheet continuum 5C are transported in the transport direction MD along the longitudinal direction.
- the body sheet continuum 4C is folded at the origin along the fold along the longitudinal direction, and the leg side elastic member 7 is disposed between the folded body sheet continuum 4C.
- the non-skin contact side surface of the main body sheet continuum 4C continuous in the transport direction is joined to the skin contact side surface of the top sheet continuum 5C.
- joining process S11 of the side flap 10 and the fastening member 11, and joining process S12 of the main body sheet 4 and the surface sheet 5 is not limited.
- the side flap 10 to which the fastening member 11 is bonded and the main body sheet 4 are bonded. More specifically, the side flaps 10 are temporarily fixed intermittently in the transport direction to the skin contact side of the main sheet continuum. Temporary fixation is fixation which becomes peelable. Specifically, the side flaps 10 may be joined to the main body sheet 4 before use and fixed so that the side flaps 10 can be separated from the main body sheet 4 at the time of use.
- the temporarily fixed portion 32 of the skin contact surface of the main body sheet continuum 4C and the side flaps 10 is schematically shown.
- the side flaps 10 are folded along the widthwise end of the main body sheet continuum. Specifically, the outer end (the inner end 10B in the width direction in the product state) of the cross direction CD intersecting the transport direction of the side flaps 10 is folded back to the non-skin contact surface side of the main body sheet continuum 4C. At this time, the folded-back portion of the side flap 10 is fixed to the non-skin contact surface of the main body sheet continuous body 4C. In FIG. 1, the fixed portions 31 of the non-skin contact surface of the main body sheet continuous body 4 ⁇ / b> C and the folded back portion of the side flaps 10 are hatched.
- the main body sheet 4 and the absorbent body are integrated. More specifically, the skin contact surface of the absorber 3 and the main sheet 4 to which the top sheet continuous body 5C and the side flaps 10 are joined are joined.
- the absorber 3, the surface sheet continuous body 5C, the side flap 10, the fastening member 11, and the main body sheet 4 are integrated.
- the absorber and the back surface sheet 6 are joined before the absorber bonding process, and the main body sheet 4 to which the absorber and the back surface sheet, the surface sheet continuum, and the side flap 10 were joined in the absorber bonding process. And may be joined.
- the back sheet 6 may be joined after the absorber joining step. By joining the back sheet to the absorber, the main body sheet 4 or the like, the side flaps 10 are disposed between the main body sheet 4 and the back sheet.
- positioning other structural members such as a leg elastic member, the process of forming a leg periphery opening part, etc. can be manufactured using a well-known manufacturing method.
- the absorbent article manufactured in this manner includes an absorbent body, an absorbent main body having a main body sheet 4 disposed on the skin-contacting surface side of the absorbent body, and a side extending outward in the width direction than the absorbent main body.
- An absorbent article comprising a flap 10 and a fastening member joined to the side flap 10 and fastened to the non-skin-contacting surface of the absorbent body, the side flap to which the fastening member is joined After the side flaps 10 are folded along the end in the width direction of the main body sheet 4 in a state in which the main body sheet 4 is joined to the main body sheet 4, the main body sheet 4 and the absorber are integrated.
- the side flaps 10 are joined to the main body sheet 4, And, after the side flaps 10 are folded, the main body sheet can be joined quickly to the absorber 3 and the back sheet 6.
- the folded end 10 B of the side flap 10 is joined between the main sheet 4 and the back sheet 6.
- the side flap folding step S14 and the back sheet 6 are used.
- the adhesive may be dried, or the adhesive may be stuck to another member during the conveyance process.
- the folding step of the side flaps is performed as the next step of joining the main sheet 4 and the top sheet 5, the folded end 10B of the side flap 10 can be smoothly fixed between the main sheet 4 and the back sheet 6. .
- the absorbent article includes a liquid-permeable top sheet covering the skin contact surface of the absorber, and a main body elastic member which is joined to the main body sheet 4 and extends and contracts in the longitudinal direction.
- the members constitute upright leg side gathers positioned closer to the skin contact surface than the absorber, and the side flaps 10 are joined to the main sheet 4 joined to the top sheet.
- one end in the width direction of the side flap 10 (outside end in the width direction in the unfolded state) 10A is temporarily fixed releasably to the skin contact side surface of the main body sheet 4,
- the other end in the width direction of the side flap 10 (inside end in the width direction in the unfolded state) 10B is fixed to the surface on the non-skin contact side of the main body sheet 4, and the side flap 10 is temporarily fixed and fixed
- the widthwise length W1 (see FIG. 3) of one end 10A in the width direction of the side flap 10 and the fold FL along the side of the body sheet 4 of the side flap 10 is the body sheet It is shorter than the length W2 (see FIG. 3) in the width direction of 4.
- the said main body sheet 4 is integrated with an absorber.
- the side flaps 10 are joined to the main body sheet 4, no step due to the thickness of the absorber is formed on the main body sheet 4, so the side flaps 10 and the absorber can be made to abut each other with a smooth surface. It is possible to suppress the shakiness.
- step difference by the thickness of an absorber is formed in the main body sheet 4, the position of the main body sheet 4 or the side flap 10 may shift
- the side flaps 10 are joined to the main body sheet 4, since the step due to the thickness of the absorber is not formed in the main body sheet 4, the positional deviation of the side flaps 10 can be suppressed.
- the leg side elastic member is joined in a stretched state to the main body sheet continuum 4C, and the elastic force by the leg side elastic member partially acts on the main body sheet continuum 4C. It may be difficult to maintain a smooth condition.
- a main body sheet 4 when a step due to the thickness of the absorber is formed, the positions of the main body sheet 4 and the side flaps 10 may be shifted due to the step.
- the step due to the thickness of the absorber is not formed in the main body sheet 4, so the positional deviation of the side flaps 10 can be effectively suppressed.
- the side flaps 10 extend outward in the width direction of the main body sheet 4 and are intermittently arranged with respect to the main body sheet 4. In the side flaps 10 arranged intermittently as described above, it is difficult to hold the part extending outward in the width direction of the main body sheet 4 at the time of conveyance, and the part may be scooped at the time of conveyance. However, by temporarily fixing a portion to be the outer end in the width direction of the side flap 10 in the product state to the main body sheet 4 and folding the side flap 10, an area extending outward in the width direction from the main body sheet 4 is obtained. It is possible to reduce the size and prevent the side flaps 10 from being shaken during transportation.
- the process of folding the side flap 10 is comprised so that it may be folded on the basis of the position which does not overlap with a fastening member.
- the folds of the side flaps are formed so as not to overlap with the fastening member. For example, when a fold is formed in the fastening member, a desired engagement force may not be obtained due to deformation of the adhesive surface of the fold portion or the engagement member.
- the side flap 10 by folding the side flap 10 based on the fold that does not overlap the fastening member, the fold is not formed in the fastening member, and the engagement force of the fastening member can be stably maintained.
- the widthwise length W1 of one end 10A in the width direction of the side flap 10 and the fold FL along the side of the body sheet 4 of the side flap 10 ( 3) is shorter than the length W2 (see FIG. 3) in the width direction of the main body sheet 4, it is easier to arrange the side flaps smoothly.
- the length W1 in the width direction of the widthwise end 10A of the side flap 10 and the fold FL along the side of the body sheet 4 of the side flap 10 is the width of the side flap 10 when the side flap 10 is folded. It is the length of the direction.
- the end 10A in the width direction of the side flap 10 exceeds the body sheet 4 and the width It is placed inside the direction.
- the side flap 10 is disposed on the step by the inner end of the main body sheet 4, and it is difficult to maintain a smooth state.
- the side flap 10 can be disposed on the main body sheet 4 and wrinkles and twisting due to a step can be suppressed.
- the manufacturing method of the absorbent article which concerns on a modification is comprised so that side flap folding process S14 may be performed before joining process S12 of a main body sheet
- the absorbent article manufactured in this manner further comprises a liquid-permeable top sheet covering the skin contact surface of the absorber, and a main body elastic member joined to the main body sheet and capable of stretching in the longitudinal direction,
- the leg side elastic members constitute upright leg side gathers positioned closer to the skin contact surface than the absorber, and the top sheet is joined to the main sheet to which the side flaps 10 are joined.
- the side flap 10 is temporarily fixed to the skin contact side surface of the main body sheet, and the side flap 10 is temporarily fixed to the skin contact side surface of the surface sheet.
- It may be configured as follows. When one end 10A of the side flap 10 extends inward in the width direction beyond the main body sheet, the side flap 10 is joined to the main body sheet and the surface sheet to extend inward in the width direction beyond the main body sheet.
- the side flaps 10 extending up to the end can be temporarily fixed, and it is possible to suppress the side flaps 10 being turned during transport and to stably transport.
- the length of the width direction of a main body sheet or the length of the width direction of a surface sheet can be changed.
- the folding position of the side flaps in the cross direction varies depending on the size. Therefore, it is necessary to change the crosswise position of the device for folding the side flaps itself, or to use a folding device capable of folding the side flaps at different folding positions, resulting in an increase in the size of the manufacturing device.
- the main sheet and the top sheet are joined after the side flap folding step, absorbent articles of different sizes can be easily manufactured.
- the present invention can be applied to an absorbent article having an absorbent body having an absorbent body and a top sheet, and side flaps extending outward in the width direction of the absorbent body.
- Absorbent article 2 Absorbent body 3: Absorbent 3A: Slit 4: Body sheet 5: Surface sheet 6: Back sheet 6A: Target portion 7: Leg side elastic member 8: Leg elastic member 10: Side flap 11: Fastening member 21: leg opening 31: fixed portion L: longitudinal direction W: width direction CD: cross direction MD: transport direction
Landscapes
- Health & Medical Sciences (AREA)
- Engineering & Computer Science (AREA)
- Heart & Thoracic Surgery (AREA)
- Epidemiology (AREA)
- Biomedical Technology (AREA)
- Vascular Medicine (AREA)
- Life Sciences & Earth Sciences (AREA)
- Animal Behavior & Ethology (AREA)
- General Health & Medical Sciences (AREA)
- Public Health (AREA)
- Veterinary Medicine (AREA)
- Manufacturing & Machinery (AREA)
- Mechanical Engineering (AREA)
- Absorbent Articles And Supports Therefor (AREA)
- Orthopedics, Nursing, And Contraception (AREA)
Abstract
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201480024393.8A CN105163699B (zh) | 2013-05-01 | 2014-04-22 | 吸收性物品的制造方法 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2013096156A JP6186167B2 (ja) | 2013-05-01 | 2013-05-01 | 吸収性物品の製造方法及び吸収性物品 |
| JP2013-096156 | 2013-05-01 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2014178305A1 true WO2014178305A1 (fr) | 2014-11-06 |
Family
ID=51843438
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2014/061257 Ceased WO2014178305A1 (fr) | 2013-05-01 | 2014-04-22 | Procédé de production d'un article absorbant et article absorbant |
Country Status (4)
| Country | Link |
|---|---|
| JP (1) | JP6186167B2 (fr) |
| CN (1) | CN105163699B (fr) |
| MY (1) | MY165121A (fr) |
| WO (1) | WO2014178305A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017063942A (ja) * | 2015-09-29 | 2017-04-06 | 大王製紙株式会社 | テープタイプ使い捨ておむつ |
| US11026848B2 (en) | 2016-03-18 | 2021-06-08 | The Procter & Gamble Company | Method and apparatus for advancing and folding an absorbent article |
| US11039961B2 (en) | 2016-03-18 | 2021-06-22 | The Procter & Gamble Company | Method and apparatus for advancing and folding an absorbent article |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5922288B1 (ja) * | 2015-08-19 | 2016-05-24 | 株式会社アルバ | 使い捨て着用物品及び使い捨て着用物品の製造方法 |
| JP6129291B1 (ja) * | 2015-12-29 | 2017-05-17 | ユニ・チャーム株式会社 | 吸収性物品の製造方法 |
| WO2018123047A1 (fr) * | 2016-12-28 | 2018-07-05 | ユニ・チャーム株式会社 | Article absorbant |
| JP7274354B2 (ja) * | 2019-05-31 | 2023-05-16 | 花王株式会社 | パンツ型吸収性物品 |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2007004640A1 (fr) * | 2005-07-05 | 2007-01-11 | Zuiko Corporation | Procede de fabrication d’une couche |
| JP2010119423A (ja) * | 2008-11-17 | 2010-06-03 | Zuiko Corp | 着用物品の製造方法 |
| WO2012131509A1 (fr) * | 2011-03-31 | 2012-10-04 | Fameccanica.Data S.P.A. | Procédé pour produire des articles hygiéniques à porter tels que des culottes pourvues de panneaux latéraux, et article correspondant |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ZA927394B (en) * | 1991-09-27 | 1994-03-25 | Johnson & Johnson Inc | No-waste absorbent product |
-
2013
- 2013-05-01 JP JP2013096156A patent/JP6186167B2/ja not_active Expired - Fee Related
-
2014
- 2014-04-22 CN CN201480024393.8A patent/CN105163699B/zh active Active
- 2014-04-22 WO PCT/JP2014/061257 patent/WO2014178305A1/fr not_active Ceased
- 2014-04-22 MY MYPI2015703893A patent/MY165121A/en unknown
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2007004640A1 (fr) * | 2005-07-05 | 2007-01-11 | Zuiko Corporation | Procede de fabrication d’une couche |
| JP2010119423A (ja) * | 2008-11-17 | 2010-06-03 | Zuiko Corp | 着用物品の製造方法 |
| WO2012131509A1 (fr) * | 2011-03-31 | 2012-10-04 | Fameccanica.Data S.P.A. | Procédé pour produire des articles hygiéniques à porter tels que des culottes pourvues de panneaux latéraux, et article correspondant |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017063942A (ja) * | 2015-09-29 | 2017-04-06 | 大王製紙株式会社 | テープタイプ使い捨ておむつ |
| US11026848B2 (en) | 2016-03-18 | 2021-06-08 | The Procter & Gamble Company | Method and apparatus for advancing and folding an absorbent article |
| US11039961B2 (en) | 2016-03-18 | 2021-06-22 | The Procter & Gamble Company | Method and apparatus for advancing and folding an absorbent article |
Also Published As
| Publication number | Publication date |
|---|---|
| CN105163699A (zh) | 2015-12-16 |
| CN105163699B (zh) | 2018-10-02 |
| MY165121A (en) | 2018-02-28 |
| JP2014217413A (ja) | 2014-11-20 |
| JP6186167B2 (ja) | 2017-08-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| TWI473602B (zh) | Absorbent article manufacturing apparatus and method for manufacturing absorbent article | |
| TWI453003B (zh) | 吸收性物品及吸收性物品之製造方法 | |
| CN103582471B (zh) | 吸收制品 | |
| JP6186167B2 (ja) | 吸収性物品の製造方法及び吸収性物品 | |
| WO2017002461A1 (fr) | Couche jetable | |
| CN105517522B (zh) | 吸收性物品 | |
| JP5902845B1 (ja) | 使い捨ての着用物品 | |
| JP5524022B2 (ja) | ファスニングテープの製造方法およびおむつ | |
| KR102419798B1 (ko) | 흡수성 물품 및 팬티형 흡수성 물품의 제조 방법 | |
| WO2017149683A1 (fr) | Article absorbant de type culotte | |
| JP6711849B2 (ja) | 吸収性物品の製造方法 | |
| JP6825046B2 (ja) | 吸収性物品の製造方法 | |
| US20130020736A1 (en) | Stretching apparatus and method of manufacturing absorbent article | |
| JP5942911B2 (ja) | 使い捨ておむつの製造方法 | |
| WO2017002392A1 (fr) | Article absorbant | |
| JP7241007B2 (ja) | 吸収性物品の包装体 | |
| MX2013000029A (es) | Pañal desechable. | |
| WO2017002391A1 (fr) | Article absorbant | |
| JP6469038B2 (ja) | 使い捨ておむつ | |
| JP6763263B2 (ja) | 吸収性物品 | |
| JP6226909B2 (ja) | 吸収性物品 | |
| JP6436771B2 (ja) | 使い捨ての着用物品 | |
| JP6275571B2 (ja) | 使い捨ておむつ | |
| JP6825045B2 (ja) | 吸収性物品の製造方法 | |
| JP7100977B2 (ja) | 吸収性物品 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 201480024393.8 Country of ref document: CN |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 14791772 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: IDP00201507453 Country of ref document: ID |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 14791772 Country of ref document: EP Kind code of ref document: A1 |