WO2014196291A1 - Élément revêtu de métal noble et procédé de fabrication correspondant - Google Patents
Élément revêtu de métal noble et procédé de fabrication correspondant Download PDFInfo
- Publication number
- WO2014196291A1 WO2014196291A1 PCT/JP2014/062006 JP2014062006W WO2014196291A1 WO 2014196291 A1 WO2014196291 A1 WO 2014196291A1 JP 2014062006 W JP2014062006 W JP 2014062006W WO 2014196291 A1 WO2014196291 A1 WO 2014196291A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- nickel
- layer
- noble metal
- cobalt
- gold
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D7/00—Electroplating characterised by the article coated
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D5/00—Electroplating characterised by the process; Pretreatment or after-treatment of workpieces
- C25D5/60—Electroplating characterised by the structure or texture of the layers
- C25D5/605—Surface topography of the layers, e.g. rough, dendritic or nodular layers
- C25D5/611—Smooth layers
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D5/00—Electroplating characterised by the process; Pretreatment or after-treatment of workpieces
- C25D5/10—Electroplating with more than one layer of the same or of different metals
- C25D5/12—Electroplating with more than one layer of the same or of different metals at least one layer being of nickel or chromium
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D5/00—Electroplating characterised by the process; Pretreatment or after-treatment of workpieces
- C25D5/60—Electroplating characterised by the structure or texture of the layers
- C25D5/623—Porosity of the layers
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D3/00—Electroplating: Baths therefor
- C25D3/02—Electroplating: Baths therefor from solutions
- C25D3/48—Electroplating: Baths therefor from solutions of gold
-
- C—CHEMISTRY; METALLURGY
- C25—ELECTROLYTIC OR ELECTROPHORETIC PROCESSES; APPARATUS THEREFOR
- C25D—PROCESSES FOR THE ELECTROLYTIC OR ELECTROPHORETIC PRODUCTION OF COATINGS; ELECTROFORMING; APPARATUS THEREFOR
- C25D3/00—Electroplating: Baths therefor
- C25D3/02—Electroplating: Baths therefor from solutions
- C25D3/56—Electroplating: Baths therefor from solutions of alloys
- C25D3/562—Electroplating: Baths therefor from solutions of alloys containing more than 50% by weight of iron or nickel or cobalt
Definitions
- a nickel-phosphorus layer, a nickel-tin layer, a palladium-nickel layer, or cobalt-tin is plated on the surface of a member made of a copper-based material.
- a technique in which a layer or the like and a noble metal layer such as gold are sequentially formed has been reported (Patent Document 1).
- an object of the present invention is to provide a noble metal covering member with improved corrosion resistance.
- a noble metal layer is provided by providing a nickel-cobalt alloy layer containing cobalt in a specific content before providing a noble metal layer on the surface of the member.
- the present invention has been completed by finding that corrosion resistance can be imparted to the noble metal-coated member even when the film is thin or when the nickel layer contains sulfur.
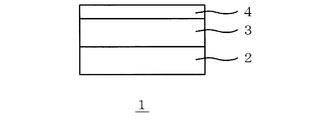
- the present invention is a noble metal-coated member in which a nickel-cobalt alloy layer containing 0.5 to 99% by mass of cobalt and a noble metal layer are laminated in this order on the surface of the member.
- the present invention is a method for improving the corrosion resistance of a noble metal-coated member, characterized in that a nickel-cobalt alloy layer containing 0.5 to 99% by mass of cobalt and a noble metal layer are laminated in this order on the surface of the member. .
- corrosion resistance can be imparted to the precious metal-coated member. Specifically, even if the thickness of the precious metal layer to be coated is reduced, problems due to pinholes and the like hardly occur, so that the corrosion resistance can be improved. Moreover, even if sulfur is contained in the nickel layer, the corrosion resistance is not affected, so that the insertion / extraction property of the conventional nickel plating solution containing a brightener can be maintained.
- the member used for the noble metal-coated member of the present invention is not particularly limited, but may be any member as long as the surface is formed of a metal or alloy such as copper, copper alloy, nickel, nickel alloy, stainless steel, or the like. Further, the material inside the member and the shape of the member are not particularly limited.
- a nickel-cobalt alloy layer containing 0.5 to 99 mass% (hereinafter simply referred to as “%”), preferably 1 to 80%, of cobalt is provided on the surface of the member.
- the nickel-cobalt alloy layer can be formed by a known forming method, for example, plating using a nickel-cobalt plating solution, sputtering using a nickel-cobalt alloy as a sputtering source, vapor deposition, or the like.
- the thickness of the nickel-cobalt alloy layer is not particularly limited, but is, for example, 0.01 to 100 ⁇ m, preferably 0.5 to 5 ⁇ m.
- the nickel-cobalt alloy layer may further contain sulfur or the like.
- the content of sulfur and the like is not particularly limited, but is, for example, 0.001 to 1%, preferably 0.001 to 0.25%.
- the plating solution or the sputtering source may contain sulfur or a compound containing sulfur. When sulfur is contained, precipitation becomes fine and the surface becomes smooth.
- a noble metal layer is provided on the nickel-cobalt alloy layer.
- the noble metal include gold, silver, platinum, palladium, rhodium, iridium, ruthenium and osmium. Among these noble metals, gold, silver and palladium are preferable.
- This noble metal layer can be formed by a known forming method, for example, noble metal plating, sputtering using a noble metal as a sputtering source, vapor deposition, or the like.
- the thickness of the noble metal layer is not particularly limited, but is, for example, 0.01 ⁇ m or more, preferably 0.01 to 10 ⁇ m, more preferably 0.05 to 2 ⁇ m.
- this noble metal layer may further contain cobalt or the like.
- the content of cobalt or the like is not particularly limited, but is, for example, 0.1 to 8%, preferably 0.2 to 0.4%.
- the plating solution or the sputtering source may contain cobalt or a compound containing cobalt. When cobalt is contained, precipitation becomes fine and the hardness of the film increases.
- the noble metal-coated member of the present invention further includes one or more intermediate layers selected from a nickel-tin layer, a palladium layer and a palladium-nickel layer, preferably between the nickel-cobalt alloy layer and the noble metal layer, preferably Two kinds of intermediate layers may be provided (however, when the noble metal layer is formed of palladium or when the palladium layer is provided alone as the intermediate layer, two or more kinds of intermediate layers may be provided with palladium as the noble metal layer side layer). Layer can be removed). By providing these intermediate layers, the corrosion resistance is further improved.
- the nickel-tin layer can be formed by a known formation method, for example, nickel-tin plating, sputtering using a nickel-tin alloy as a sputtering source, vapor deposition, or the like.
- the content of tin contained in the nickel-tin layer is not particularly limited, but is, for example, 40% to 70%.
- the thickness of the nickel-tin layer is not particularly limited, but is, for example, 0.001 to 10 ⁇ m, preferably 0.05 to 1 ⁇ m.
- the palladium layer can be formed by a known formation method, for example, palladium plating, sputtering using palladium as a sputtering source, vapor deposition, or the like.
- the thickness of the palladium layer is not particularly limited, but is, for example, 0.001 to 10 ⁇ m, preferably 0.05 to 2 ⁇ m.
- the palladium-nickel layer can be formed by a known formation method, for example, by palladium-nickel plating, sputtering using a palladium-nickel alloy as a sputtering source, vapor deposition, or the like.
- the content of nickel contained in the palladium-nickel layer is not particularly limited, but is, for example, 10 to 50%, preferably 15 to 20%.
- the thickness of the palladium-nickel layer is not particularly limited, but is, for example, 0.001 to 10 ⁇ m, preferably 0.05 to 2 ⁇ m.
- the noble metal covering member of the present invention may further be provided with a sealing agent layer for improving insertion / extraction.
- This sealing agent layer can be formed of a commercially available sealing agent.
- the sealing agent layer is preferably provided on the noble metal layer.
- Nickel sulfate 200 to 400 g / l, preferably 250 to 300 g / l Nickel chloride: 30-60 g / l, preferably 40-50 g / l Boric acid: 30-50 g / l, preferably 30-40 g / l Cobalt sulfate: 0.4 to 70 g / l, preferably 0.4 to 40 g / l Saccharin sodium: 0.5 to 8 g / l, preferably 1 to 3 g / l (Sulfamic acid bath) Nickel sulfamate: 300 to 800 g / l, preferably 300 to 600 g / l Nickel chloride: 5 to 15 g / l, preferably 5 to 10 g / l Boric acid: 30-60 g / l, preferably 30-40 g / l Cobalt sulfate: 0.4 to 70 g g l
- ⁇ Nickel-cobalt plating conditions Bath temperature: 45-60 ° C, preferably 50-55 ° C pH: 3.0 to 4.5, preferably 3.5 to 4.0 Current density: 2 to 20 A / dm 2 , preferably 4 to 10 A / dm 2
- one or more intermediates selected from a nickel-tin layer, a palladium layer and a palladium-nickel layer with the above-mentioned thickness Provide a layer.
- the composition of the plating solution used for forming these intermediate layers and the plating conditions are as follows.
- ⁇ Nickel-tin plating solution composition Tin (II) chloride: 20 to 40 g / l, preferably 25 to 30 g / l Nickel chloride: 15 to 45 g / l, preferably 20 to 40 g / l Potassium pyrophosphate: 100 to 300 g / l, preferably 150 to 250 g / l Glycine: 10-30 g / l, preferably 10-25 g / l Ammonia water (28%): 5 ml / l
- ⁇ Nickel-tin plating conditions Bath temperature: 40-60 ° C, preferably 40-50 ° C pH: 7.5 to 8.5, preferably 7.5 to 8 Current density: 1 to 10 A / dm 2 , preferably 2 to 5 A / dm 2
- ⁇ Palladium plating solution composition Diaminopalladium sulfite: 10-30 g / l, preferably 10-15 g / l Ammonium chloride: 5 to 140 g / l, preferably 80 to 120 g / l Boric acid: 5-50 g / l, preferably 10-20 g / l 3-pyridinesulfonic acid: 1 to 10 g / l, preferably 3 to 5 g / l Selenium potassium: 0.01 to 0.1 g / l, preferably 0.03 to 0.05 g / l
- ⁇ Palladium-nickel plating solution composition Dichlorodiammine palladium: 20 to 100 g / l, preferably 20 to 50 g / l Nickel sulfate hexahydrate: 50 to 400 g / l, preferably 100 to 200 g / l Ammonium sulfate: 10 to 70 g / l, preferably 30 to 50 g / l 3-pyridinesulfonic acid: 1 to 10 g / l, preferably 3 to 5 g / l
- ⁇ Gold plating solution composition Potassium cyanide: gold concentration 4 to 16 g / l, preferably 8 to 12 g / l Cobalt sulfate: 0.25 to 25 g / l, preferably 0.5 to 10 g / l Citric acid: 10 to 150 g / l, preferably 50 to 100 g / l
- the term “corrosion resistance” means that, for example, after performing a salt spray test (JIS C 60068-2-11) or a nitrate aeration test (based on JIS H 8620), the corroded portion is 30% or less of the total, Preferably it means 10% or less.
- Example 5 Formation of gold-coated member: As in Example 1 (1), a member having a 1.5 ⁇ m nickel-cobalt alloy layer formed on the surface of the member was placed in a palladium plating solution having the following composition at a bath temperature of 55 ° C. and a current density of 2 A / dm 2 . It was immersed under the conditions, and a 0.05 ⁇ m palladium layer was formed on the surface of the member. Thereafter, a gold layer having a thickness of 0.1 ⁇ m was formed on the surface of the member in the same manner as in (2) of Example 1 to obtain a gold-coated member.
- a palladium plating solution having the following composition at a bath temperature of 55 ° C. and a current density of 2 A / dm 2 . It was immersed under the conditions, and a 0.05 ⁇ m palladium layer was formed on the surface of the member. Thereafter, a gold layer having a thickness of 0.1 ⁇ m was formed on the surface of the member in the same
- Example 6 Formation of gold-coated member: A gold layer having a thickness of 0.1 ⁇ m was formed on the surface of the member in the same manner as in Example 5 and then heat-treated in an oven at 260 ° C. for 2 minutes to obtain a gold-coated member.
- Example 7 Formation of gold-coated member: A sample in which a 1.5 ⁇ m nickel-cobalt alloy layer was formed on the surface of the member in the same manner as in Example 1 (1) was applied to a nickel-tin plating solution having the composition described in Example 3 at a bath temperature of 55 ° C. and a current. It was immersed under conditions of a density of 2 A / dm 2 to form a 0.3 ⁇ m nickel-tin layer on the surface of the member. Then, it was immersed in a palladium plating solution having the composition described in Example 5 under conditions of a bath temperature of 55 ° C. and a current density of 2 A / dm 2 to form a 0.05 ⁇ m palladium layer on the surface of the member. Finally, a gold layer having a thickness of 0.1 ⁇ m was formed on the surface of the member in the same manner as in (2) of Example 1 to obtain a gold-coated member.
- Example 8 Formation of gold-coated member: A gold layer having a thickness of 0.1 ⁇ m was formed on the surface of the sample in the same manner as in Example 7 and then heat-treated in an oven at 260 ° C. for 2 minutes to obtain a gold-coated member.
- Example 9 Formation of gold-coated member: A gold-coated member was obtained in the same manner as in Example 1 except that the nickel-cobalt plating solution used in Example 1 was a nickel-cobalt plating solution having the following composition.
- Example 10 Formation of gold-coated member: A gold-coated member was obtained in the same manner as in Example 2, except that the nickel-cobalt plating solution used in Example 2 had the composition described in Example 9.
- Example 11 Formation of gold-coated member: A gold-coated member was obtained in the same manner as in Example 3 except that the nickel-cobalt plating solution used in Example 3 had the composition described in Example 9.
- Example 12 Formation of gold-coated member: A gold-coated member was obtained in the same manner as in Example 4 except that the nickel-cobalt plating solution used in Example 4 had the composition described in Example 9.
- Example 13 Formation of gold-coated member A gold-coated member was obtained in the same manner as in Example 5 except that the nickel-cobalt plating solution used in Example 5 had the composition described in Example 9.
- Example 14 Formation of gold-coated member: A gold-coated member was obtained in the same manner as in Example 6 except that the nickel-cobalt plating solution used in Example 6 had the composition described in Example 9.
- Example 15 Formation of gold-coated member: A gold-coated member was obtained in the same manner as in Example 7 except that the nickel-cobalt plating solution used in Example 7 had the composition described in Example 9.
- Example 16 Formation of gold-coated member A gold-coated member was obtained in the same manner as in Example 8, except that the nickel-cobalt plating solution used in Example 8 had the composition described in Example 9.
- a gold-coated member was obtained in the same manner as in Examples 1 to 8 except that the nickel-cobalt plating solution used in Examples 1 to 8 was a nickel plating solution having the following composition.
- Nickel sulfate 300 g / l Nickel chloride: 40 g / l Boric acid: 30 g / l Saccharin sodium: 2 g / l
- a gold-coated member was obtained in the same manner as in Examples 1, 2, 7, and 8 except that the nickel-cobalt plating solution used in Examples 1, 2, 7, and 8 was a nickel plating solution having the following composition.
- a gold-coated member was obtained in the same manner as in Examples 9, 10, 15, and 16 except that the nickel-cobalt plating solution used in Examples 9, 10, 15, and 16 was a nickel plating solution having the following composition.
- Corrosion part is 10% or less of the whole ⁇ : Corrosion part is more than 10% to 30% or less ⁇ : Corrosion part is more than 30% to 50% or less ⁇ : Corrosion part is more than 50% of the whole Many to 80% or less XX: More than 80% of corroded parts
- Test example 2 Scratch resistance test: Using the gold-coated members obtained in Examples 1 to 16 and Comparative Examples 1 to 24, the following scratch test was performed. After this test, the degree of scratches on the gold-coated member was evaluated visually based on the following evaluation criteria. In addition, after the scratch test, a nitric acid aeration test was performed in the same manner as in Test Example 1 to evaluate the corrosivity from the damaged part, and the degree of corrosion was evaluated. The results are shown in Table 2.
- ⁇ Scratch test> A constant load surface property measuring machine (manufactured by Shinto Kagaku Co., Ltd .: Tribogear TYPE: 22H) was used to apply a constant load (500 gf) to a jig whose tip is a zirconia sphere to scratch the surface of the gold-coated member.
- scratch resistance can be obtained by sequentially forming a nickel plating layer (including sulfur) containing cobalt and a gold layer as in the example. Further, it was found that when the intermediate layer was provided, the scratch resistance was improved, and particularly when two types of intermediate layers were provided, the scratch resistance was significantly improved. On the other hand, it was found that, as in the comparative example, even if an intermediate layer and a gold layer were sequentially formed on a nickel plating layer (containing sulfur) not containing cobalt, only a low scratch resistance could be obtained.
- Example 17 Relationship between cobalt content, corrosion resistance and scratch resistance in nickel-cobalt alloy layers: In order to investigate the relationship between cobalt content, corrosion resistance and scratch resistance in the nickel-cobalt alloy layer, the nickel and cobalt concentrations in the plating solution were adjusted, and the amount of eutectoid of nickel and cobalt was changed. A nickel-tin layer, a palladium layer, and a gold layer were formed in the same manner as in Example 15 except that the cobalt alloy layer was formed to obtain a gold-coated member. These gold-coated members were evaluated for corrosion resistance and scratch resistance in the same manner as in Test Examples 1 and 2. The results are shown in Table 3.
- the precious metal-coated member of the present invention has high corrosion resistance, it can be suitably used for coating contacts and terminals of pitch connectors, switches, relays and the like for industrial equipment.
- Precious metal covering member 2 Member 3 Nickel-cobalt alloy layer 4 Precious metal layer 5 Intermediate layer more than
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Electrochemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Electroplating Methods And Accessories (AREA)
- Electroplating And Plating Baths Therefor (AREA)
Abstract
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2015521344A JPWO2014196291A1 (ja) | 2013-06-07 | 2014-04-30 | 貴金属被覆部材およびその製造方法 |
| CN201480031587.0A CN105392928A (zh) | 2013-06-07 | 2014-04-30 | 贵金属被覆构件及其制造方法 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2013120525 | 2013-06-07 | ||
| JP2013-120525 | 2013-06-07 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2014196291A1 true WO2014196291A1 (fr) | 2014-12-11 |
Family
ID=52007944
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2014/062006 Ceased WO2014196291A1 (fr) | 2013-06-07 | 2014-04-30 | Élément revêtu de métal noble et procédé de fabrication correspondant |
Country Status (4)
| Country | Link |
|---|---|
| JP (1) | JPWO2014196291A1 (fr) |
| CN (1) | CN105392928A (fr) |
| TW (1) | TW201509643A (fr) |
| WO (1) | WO2014196291A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017027446A (ja) * | 2015-07-24 | 2017-02-02 | 住友金属鉱山株式会社 | 導電性基板、導電性基板の製造方法 |
| KR20230050237A (ko) * | 2021-10-07 | 2023-04-14 | 이이쟈 가부시키가이샤 | PtRu 합금 도금막 및 해당 PtRu 합금 도금막을 구비하는 적층 구조 |
| KR20230145270A (ko) * | 2022-04-09 | 2023-10-17 | 이이쟈 가부시키가이샤 | PtRu 합금 박막을 구비하는 적층 구조 |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS59180908A (ja) * | 1983-03-30 | 1984-10-15 | 古河電気工業株式会社 | 銀被覆導体とその製造方法 |
| JPS6013078B2 (ja) * | 1978-09-05 | 1985-04-04 | 日本特殊陶業株式会社 | 金メツキされた電子部品及びその製法 |
| JPS62199795A (ja) * | 1986-02-27 | 1987-09-03 | Nippon Mining Co Ltd | 電子・電気機器用部品 |
| JPS62199794A (ja) * | 1986-02-27 | 1987-09-03 | Nippon Mining Co Ltd | 電子・電気機器用部品 |
| JPS6383291A (ja) * | 1986-09-25 | 1988-04-13 | Kyocera Corp | 金の導電層を有する電子部品 |
| JP2001003194A (ja) * | 1999-06-21 | 2001-01-09 | Nippon Mining & Metals Co Ltd | 耐熱,耐食性銀めっき材 |
| JP2006117983A (ja) * | 2004-10-20 | 2006-05-11 | Matsushita Electric Works Ltd | めっき皮膜ステンレス鋼 |
| JP2008196010A (ja) * | 2007-02-13 | 2008-08-28 | Hitachi Cable Ltd | コネクタ端子用めっき材料 |
| JP2008270192A (ja) * | 2007-03-27 | 2008-11-06 | Furukawa Electric Co Ltd:The | 可動接点部品用銀被覆材およびその製造方法 |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4767508A (en) * | 1986-02-27 | 1988-08-30 | Nippon Mining Co., Ltd. | Strike plating solution useful in applying primer plating to electronic parts |
| JP2004307954A (ja) * | 2003-04-08 | 2004-11-04 | Matsushita Electric Works Ltd | めっき形成部材 |
| JP4834023B2 (ja) * | 2007-03-27 | 2011-12-07 | 古河電気工業株式会社 | 可動接点部品用銀被覆材およびその製造方法 |
-
2014
- 2014-04-30 CN CN201480031587.0A patent/CN105392928A/zh active Pending
- 2014-04-30 WO PCT/JP2014/062006 patent/WO2014196291A1/fr not_active Ceased
- 2014-04-30 JP JP2015521344A patent/JPWO2014196291A1/ja active Pending
- 2014-05-29 TW TW103118808A patent/TW201509643A/zh unknown
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS6013078B2 (ja) * | 1978-09-05 | 1985-04-04 | 日本特殊陶業株式会社 | 金メツキされた電子部品及びその製法 |
| JPS59180908A (ja) * | 1983-03-30 | 1984-10-15 | 古河電気工業株式会社 | 銀被覆導体とその製造方法 |
| JPS62199795A (ja) * | 1986-02-27 | 1987-09-03 | Nippon Mining Co Ltd | 電子・電気機器用部品 |
| JPS62199794A (ja) * | 1986-02-27 | 1987-09-03 | Nippon Mining Co Ltd | 電子・電気機器用部品 |
| JPS6383291A (ja) * | 1986-09-25 | 1988-04-13 | Kyocera Corp | 金の導電層を有する電子部品 |
| JP2001003194A (ja) * | 1999-06-21 | 2001-01-09 | Nippon Mining & Metals Co Ltd | 耐熱,耐食性銀めっき材 |
| JP2006117983A (ja) * | 2004-10-20 | 2006-05-11 | Matsushita Electric Works Ltd | めっき皮膜ステンレス鋼 |
| JP2008196010A (ja) * | 2007-02-13 | 2008-08-28 | Hitachi Cable Ltd | コネクタ端子用めっき材料 |
| JP2008270192A (ja) * | 2007-03-27 | 2008-11-06 | Furukawa Electric Co Ltd:The | 可動接点部品用銀被覆材およびその製造方法 |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017027446A (ja) * | 2015-07-24 | 2017-02-02 | 住友金属鉱山株式会社 | 導電性基板、導電性基板の製造方法 |
| KR20230050237A (ko) * | 2021-10-07 | 2023-04-14 | 이이쟈 가부시키가이샤 | PtRu 합금 도금막 및 해당 PtRu 합금 도금막을 구비하는 적층 구조 |
| KR102897099B1 (ko) * | 2021-10-07 | 2025-12-08 | 이이쟈 가부시키가이샤 | PtRu 합금 도금막 및 해당 PtRu 합금 도금막을 구비하는 적층 구조 |
| KR20230145270A (ko) * | 2022-04-09 | 2023-10-17 | 이이쟈 가부시키가이샤 | PtRu 합금 박막을 구비하는 적층 구조 |
| KR102839170B1 (ko) | 2022-04-09 | 2025-07-28 | 이이쟈 가부시키가이샤 | PtRu 합금 박막을 구비하는 적층 구조 |
Also Published As
| Publication number | Publication date |
|---|---|
| TW201509643A (zh) | 2015-03-16 |
| JPWO2014196291A1 (ja) | 2017-02-23 |
| CN105392928A (zh) | 2016-03-09 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5667152B2 (ja) | 表面処理めっき材およびその製造方法、並びに電子部品 | |
| JP5086485B1 (ja) | 電子部品用金属材料及びその製造方法 | |
| JP6046406B2 (ja) | 高温耐性銀コート基体 | |
| JP6050664B2 (ja) | 電子部品用金属材料及びその製造方法、それを用いたコネクタ端子、コネクタ及び電子部品 | |
| KR100521550B1 (ko) | 루테늄층을 갖는 단자 및 그것을 갖는 부품 | |
| JPH0776436B2 (ja) | 導電性表面のメッキ方法 | |
| JP6267404B1 (ja) | 表面処理めっき材、コネクタ端子、コネクタ、ffc端子、ffc、fpc及び電子部品 | |
| KR20160119141A (ko) | 전기접점 재료 및 그 제조방법 | |
| WO2014054190A1 (fr) | Matériau métallique pour composants électroniques et son procédé de production | |
| JP2018123422A (ja) | 表面処理めっき材、コネクタ端子、コネクタ、ffc端子、ffc、fpc及び電子部品 | |
| WO2014054189A1 (fr) | Matériau métallique pour composants électroniques et son procédé de production | |
| CN110103584A (zh) | 老化测试插座用表面处理金属材料、使用了其的老化测试插座用连接器及老化测试插座 | |
| JP5980746B2 (ja) | 電子部品用金属材料及びその製造方法、それを用いたコネクタ端子、コネクタ及び電子部品 | |
| JPWO2014196291A1 (ja) | 貴金属被覆部材およびその製造方法 | |
| JP2004190065A (ja) | コネクタ端子およびそれを有するコネクタ | |
| TW201834313A (zh) | 連接器用端子材及端子以及電線終端構造 | |
| JP5185759B2 (ja) | 導電材及びその製造方法 | |
| CN110997984B (zh) | 镀锡铜端子材、端子及电线终端部结构 | |
| JP2015045045A (ja) | 電子部品用金属材料及びその製造方法、それを用いたコネクタ端子、コネクタ及び電子部品 | |
| JP2009149965A (ja) | 銀めっき方法 | |
| JP5298233B2 (ja) | 電子部品用金属材料及びその製造方法 | |
| JP2011099128A (ja) | めっき部材およびその製造方法 | |
| JP2014139345A (ja) | 表面処理めっき材およびその製造方法、並びに電子部品 | |
| JP5681378B2 (ja) | めっき部材およびその製造方法 | |
| JP2005068445A (ja) | 金属被覆された金属部材 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 201480031587.0 Country of ref document: CN |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 14807187 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2015521344 Country of ref document: JP Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| 122 | Ep: pct application non-entry in european phase |
Ref document number: 14807187 Country of ref document: EP Kind code of ref document: A1 |