WO2017179625A1 - Matériau d'ailette en alliage d'aluminium, feuille de brasage en alliage d'aluminium et échangeur de chaleur - Google Patents
Matériau d'ailette en alliage d'aluminium, feuille de brasage en alliage d'aluminium et échangeur de chaleur Download PDFInfo
- Publication number
- WO2017179625A1 WO2017179625A1 PCT/JP2017/015001 JP2017015001W WO2017179625A1 WO 2017179625 A1 WO2017179625 A1 WO 2017179625A1 JP 2017015001 W JP2017015001 W JP 2017015001W WO 2017179625 A1 WO2017179625 A1 WO 2017179625A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- fin material
- aluminum alloy
- particles
- fin
- thickness
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28D—HEAT-EXCHANGE APPARATUS, NOT PROVIDED FOR IN ANOTHER SUBCLASS, IN WHICH THE HEAT-EXCHANGE MEDIA DO NOT COME INTO DIRECT CONTACT
- F28D1/00—Heat-exchange apparatus having stationary conduit assemblies for one heat-exchange medium only, the media being in contact with different sides of the conduit wall, in which the other heat-exchange medium is a large body of fluid, e.g. domestic or motor car radiators
- F28D1/02—Heat-exchange apparatus having stationary conduit assemblies for one heat-exchange medium only, the media being in contact with different sides of the conduit wall, in which the other heat-exchange medium is a large body of fluid, e.g. domestic or motor car radiators with heat-exchange conduits immersed in the body of fluid
- F28D1/04—Heat-exchange apparatus having stationary conduit assemblies for one heat-exchange medium only, the media being in contact with different sides of the conduit wall, in which the other heat-exchange medium is a large body of fluid, e.g. domestic or motor car radiators with heat-exchange conduits immersed in the body of fluid with tubular conduits
- F28D1/053—Heat-exchange apparatus having stationary conduit assemblies for one heat-exchange medium only, the media being in contact with different sides of the conduit wall, in which the other heat-exchange medium is a large body of fluid, e.g. domestic or motor car radiators with heat-exchange conduits immersed in the body of fluid with tubular conduits the conduits being straight
- F28D1/0535—Heat-exchange apparatus having stationary conduit assemblies for one heat-exchange medium only, the media being in contact with different sides of the conduit wall, in which the other heat-exchange medium is a large body of fluid, e.g. domestic or motor car radiators with heat-exchange conduits immersed in the body of fluid with tubular conduits the conduits being straight the conduits having a non-circular cross-section
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/06—Continuous casting of metals, i.e. casting in indefinite lengths into moulds with travelling walls, e.g. with rolls, plates, belts, caterpillars
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B23—MACHINE TOOLS; METAL-WORKING NOT OTHERWISE PROVIDED FOR
- B23K—SOLDERING OR UNSOLDERING; WELDING; CLADDING OR PLATING BY SOLDERING OR WELDING; CUTTING BY APPLYING HEAT LOCALLY, e.g. FLAME CUTTING; WORKING BY LASER BEAM
- B23K1/00—Soldering, e.g. brazing, or unsoldering
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F1/00—Tubular elements; Assemblies of tubular elements
- F28F1/10—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses
- F28F1/12—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses the means being only outside the tubular element
- F28F1/24—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses the means being only outside the tubular element and extending transversely
- F28F1/32—Tubular elements and assemblies thereof with means for increasing heat-transfer area, e.g. with fins, with projections, with recesses the means being only outside the tubular element and extending transversely the means having portions engaging further tubular elements
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F21/00—Constructions of heat-exchange apparatus characterised by the selection of particular materials
- F28F21/08—Constructions of heat-exchange apparatus characterised by the selection of particular materials of metal
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F21/00—Constructions of heat-exchange apparatus characterised by the selection of particular materials
- F28F21/08—Constructions of heat-exchange apparatus characterised by the selection of particular materials of metal
- F28F21/089—Coatings, claddings or bonding layers made from metals or metal alloys
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B3/00—Rolling materials of special alloys so far as the composition of the alloy requires or permits special rolling methods or sequences ; Rolling of aluminium, copper, zinc or other non-ferrous metals
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F28—HEAT EXCHANGE IN GENERAL
- F28F—DETAILS OF HEAT-EXCHANGE AND HEAT-TRANSFER APPARATUS, OF GENERAL APPLICATION
- F28F2215/00—Fins
- F28F2215/12—Fins with U-shaped slots for laterally inserting conduits
Definitions
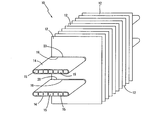
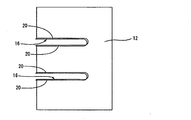
- the fin-and-tube heat exchanger for example, has the same position of the plate fins along each of the edge portions of a plurality of plate fins arranged at a predetermined distance from each other.
- a plurality of notch grooves that are open to penetrate therethrough are provided.
- a collar is formed so as to contact the surface of the flat tube through which the heat transfer fluid flows, and the flat tube is fitted into the cutout groove.
- a heat exchanger is manufactured by assembling
- Cu 0.05 to 1.50%
- Cu is an element having an effect of improving the strength by dissolving in a matrix.
- the Cu content exceeds 1.50%, the corrosion resistance decreases.
- the Cu content is less than 0.05%, the above effects are insufficient. Therefore, the Cu content is set to 0.05 to 1.50%.
- the Cu content is preferably 0.10 to 1.00%.
- the holding time of 0 hour means that the holding is stopped as soon as a predetermined holding temperature is reached. Due to the restriction of such heating conditions, all Si particles existing within the range of the length W in the entire cross section of the fin material and satisfying D ⁇ L and L + D> 0.04t are 0 ⁇ ⁇ D 2 ⁇ 0. 08 tW can be satisfied. On the other hand, when held at a temperature of 530 ° C. or higher for more than 10 hours, coarsening due to Ostwald growth occurs remarkably. As a result, among the Si particles in the surface layer, the number of Si particles satisfying D ⁇ L and L + D> 0.04t and the equivalent circle diameter of each Si particle increase, and 0 ⁇ ⁇ D 2 ⁇ 0.08 tW is not satisfied.
- the hot rolling process includes a hot rough rolling stage and a hot finish rolling stage.
- the total rolling reduction in the hot rough rolling stage is 92 to 97%, and each pass of the hot rough rolling includes three or more passes where the rolling reduction is 15% or more.
- the slab thickness is rolled from about 300 to 700 mm to about 15 to 40 mm in the hot rough rolling stage, but the total rolling reduction in the hot rough rolling stage is 92 to 97%, preferably 94 to 96%.
- the coarse rough crystallization product is finely divided by including a pass in which the hot rough rolling stage has a reduction rate of 15% or more, preferably 4 times or more, preferably a pass having a reduction rate of 20% or more. can do.
- Si particles and Al—Fe—Mn—Si-based intermetallic compounds that are crystallized substances can be miniaturized, and an appropriate distribution state defined in this embodiment can be obtained.
- the total rolling reduction in the hot rough rolling in the hot rolling process was 92.5%, and the pass in which the rolling reduction was 15% or more in each pass of the hot rough rolling was performed three or more times.
- the rolled plate was rolled to a thickness of 0.09 mm.
- the rolled material was subjected to an intermediate annealing process at 380 ° C. for 2 hours, and finally rolled to a final thickness of 0.07 mm in the final cold rolling stage to obtain a test material.
- the processing rate in the final cold rolling stage was 22.2%.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- General Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Geometry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Continuous Casting (AREA)
Abstract
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP17782438.0A EP3444368A4 (fr) | 2016-04-12 | 2017-04-12 | Matériau d'ailette en alliage d'aluminium, feuille de brasage en alliage d'aluminium et échangeur de chaleur |
| CN201780023251.3A CN109072350A (zh) | 2016-04-12 | 2017-04-12 | 铝合金制的翅片材料、铝合金制的硬钎焊板、以及热交换器 |
| US16/091,776 US20190162492A1 (en) | 2016-04-12 | 2017-04-12 | Aluminum alloy fin material, aluminum alloy brazing sheet, and heat exchanger |
| KR1020187025190A KR20180126465A (ko) | 2016-04-12 | 2017-04-12 | 알루미늄 합금제의 핀재, 알루미늄 합금제의 브레이징 시트, 및 열교환기 |
| MX2018012354A MX2018012354A (es) | 2016-04-12 | 2017-04-12 | Material de aleta de aleacion de aluminio, lamina de soldadura de bronce de aleacion de aluminio, e intercambiador de calor. |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2016-079933 | 2016-04-12 | ||
| JP2016079933 | 2016-04-12 | ||
| JP2017060744A JP6909028B2 (ja) | 2016-04-12 | 2017-03-27 | アルミニウム合金製フィン材及びこれを用いたアルミニウム合金製ブレージングシート、ならびに、当該フィン材又はブレージングシートをフィンに用いた熱交換器 |
| JP2017-060744 | 2017-03-27 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2017179625A1 true WO2017179625A1 (fr) | 2017-10-19 |
Family
ID=60042073
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2017/015001 Ceased WO2017179625A1 (fr) | 2016-04-12 | 2017-04-12 | Matériau d'ailette en alliage d'aluminium, feuille de brasage en alliage d'aluminium et échangeur de chaleur |
Country Status (1)
| Country | Link |
|---|---|
| WO (1) | WO2017179625A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPWO2022176420A1 (fr) * | 2021-02-16 | 2022-08-25 | ||
| WO2023243630A1 (fr) * | 2022-06-17 | 2023-12-21 | 株式会社Uacj | Matériau d'alliage d'aluminium monocouche pour brasage, son procédé de production, structure d'aluminium et échangeur de chaleur |
| WO2024209964A1 (fr) * | 2023-04-03 | 2024-10-10 | 株式会社Uacj | Feuille d'alliage d'aluminium, son procédé de production et échangeur de chaleur |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2004156108A (ja) * | 2002-11-07 | 2004-06-03 | Denso Corp | ろう付け用アルミニウムクラッド材 |
| WO2014196183A1 (fr) * | 2013-06-02 | 2014-12-11 | 株式会社Uacj | Échangeur thermique et matériau d'ailette pour ledit échangeur thermique |
-
2017
- 2017-04-12 WO PCT/JP2017/015001 patent/WO2017179625A1/fr not_active Ceased
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2004156108A (ja) * | 2002-11-07 | 2004-06-03 | Denso Corp | ろう付け用アルミニウムクラッド材 |
| WO2014196183A1 (fr) * | 2013-06-02 | 2014-12-11 | 株式会社Uacj | Échangeur thermique et matériau d'ailette pour ledit échangeur thermique |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPWO2022176420A1 (fr) * | 2021-02-16 | 2022-08-25 | ||
| WO2022176420A1 (fr) * | 2021-02-16 | 2022-08-25 | 株式会社Uacj | Tôle en alliage d'aluminium et son procédé de production, et échangeur de chaleur |
| WO2023243630A1 (fr) * | 2022-06-17 | 2023-12-21 | 株式会社Uacj | Matériau d'alliage d'aluminium monocouche pour brasage, son procédé de production, structure d'aluminium et échangeur de chaleur |
| JP2023184177A (ja) * | 2022-06-17 | 2023-12-28 | 株式会社Uacj | ろう付用単層アルミニウム合金材、その製造方法、アルミニウム構造体及び熱交換器 |
| EP4524274A4 (fr) * | 2022-06-17 | 2025-08-13 | Uacj Corp | Matériau d'alliage d'aluminium monocouche pour brasage, son procédé de production, structure d'aluminium et échangeur de chaleur |
| WO2024209964A1 (fr) * | 2023-04-03 | 2024-10-10 | 株式会社Uacj | Feuille d'alliage d'aluminium, son procédé de production et échangeur de chaleur |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5345264B1 (ja) | 熱交換器フィン用のアルミニウム合金材及びその製造方法、ならびに、当該アルミニウム合金材を用いた熱交換器 | |
| JP6909028B2 (ja) | アルミニウム合金製フィン材及びこれを用いたアルミニウム合金製ブレージングシート、ならびに、当該フィン材又はブレージングシートをフィンに用いた熱交換器 | |
| JP6452627B2 (ja) | アルミニウム合金クラッド材及びその製造方法、ならびに、当該アルミニウム合金クラッド材を用いた熱交換器及びその製造方法 | |
| KR101581607B1 (ko) | 알루미늄 합금재를 이용한 열교환기용 핀재와 이를 포함하는 알루미늄 합금 구조체 | |
| JP6452626B2 (ja) | アルミニウム合金クラッド材及びその製造方法、ならびに、当該アルミニウム合金クラッド材を用いた熱交換器及びその製造方法 | |
| KR102118856B1 (ko) | 단층으로 가열 접합 기능을 가지는 알루미늄 합금재와 그 제조방법 및 상기 알루미늄 합금재를 이용한 알루미늄 접합체 | |
| JP5698416B1 (ja) | 熱交換器及び当該熱交換器用フィン材 | |
| JP6418714B2 (ja) | アルミニウム合金クラッド材及びその製造方法、ならびに、当該アルミニウム合金クラッド材を用いた熱交換器及びその製造方法 | |
| JP6726370B1 (ja) | フラックスフリーろう付用アルミニウムブレージングシート | |
| JP5985973B2 (ja) | アルミニウム合金ブレージングシート及びその製造方法、ならびに、当該アルミニウム合金ブレージングシートを用いた熱交換器 | |
| JP2005254329A (ja) | クラッド材およびその製造方法、ならびにクラッド材の製造装置 | |
| JP2012051028A (ja) | アルミニウム合金材を用いた構造体とその接合方法 | |
| JP2019094517A (ja) | 耐変形性に優れる単層加熱接合用のアルミニウム合金材 | |
| JP6154645B2 (ja) | ろう付け接合構造体 | |
| CN110139940B (zh) | 换热器用的铝合金翅片材及其制造方法 | |
| WO2015147256A1 (fr) | Tôle à brasage en alliage d'aluminium pour soudage par résistance électrique | |
| WO2016147627A1 (fr) | Matériau d'ailette à base de tôle à brasage en alliage d'aluminium pour échangeur de chaleur et son procédé de fabrication | |
| CN116848277A (zh) | 铝合金板、其制造方法以及热交换器 | |
| JP2009046705A (ja) | 耐食性に優れた熱交換器用押出扁平多穴管及び熱交換器 | |
| JP7665332B2 (ja) | 熱交換器及び熱交換器用チューブ材 | |
| CN120958155A (zh) | 铝合金板、其制造方法和热交换器 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| ENP | Entry into the national phase |
Ref document number: 20187025190 Country of ref document: KR Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2017782438 Country of ref document: EP |
|
| ENP | Entry into the national phase |
Ref document number: 2017782438 Country of ref document: EP Effective date: 20181112 |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 17782438 Country of ref document: EP Kind code of ref document: A1 |