WO2018069765A1 - 插芯组件,制造插芯组件的方法及光纤固定模具 - Google Patents
插芯组件,制造插芯组件的方法及光纤固定模具 Download PDFInfo
- Publication number
- WO2018069765A1 WO2018069765A1 PCT/IB2017/001387 IB2017001387W WO2018069765A1 WO 2018069765 A1 WO2018069765 A1 WO 2018069765A1 IB 2017001387 W IB2017001387 W IB 2017001387W WO 2018069765 A1 WO2018069765 A1 WO 2018069765A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- housing
- fiber
- optical
- ferrule assembly
- mold
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
- G02B6/3807—Dismountable connectors, i.e. comprising plugs
- G02B6/3833—Details of mounting fibres in ferrules; Assembly methods; Manufacture
- G02B6/3834—Means for centering or aligning the light guide within the ferrule
- G02B6/3838—Means for centering or aligning the light guide within the ferrule using grooves for light guides
- G02B6/3839—Means for centering or aligning the light guide within the ferrule using grooves for light guides for a plurality of light guides
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/3608—Fibre wiring boards, i.e. where fibres are embedded or attached in a pattern on or to a substrate, e.g. flexible sheets
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
- G02B6/3807—Dismountable connectors, i.e. comprising plugs
- G02B6/3833—Details of mounting fibres in ferrules; Assembly methods; Manufacture
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
- G02B6/3807—Dismountable connectors, i.e. comprising plugs
- G02B6/3869—Mounting ferrules to connector body, i.e. plugs
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
- G02B6/3807—Dismountable connectors, i.e. comprising plugs
- G02B6/3869—Mounting ferrules to connector body, i.e. plugs
- G02B6/387—Connector plugs comprising two complementary members, e.g. shells, caps, covers, locked together
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
- G02B6/3807—Dismountable connectors, i.e. comprising plugs
- G02B6/3873—Connectors using guide surfaces for aligning ferrule ends, e.g. tubes, sleeves, V-grooves, rods, pins, balls
- G02B6/3885—Multicore or multichannel optical connectors, i.e. one single ferrule containing more than one fibre, e.g. ribbon type
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/3628—Mechanical coupling means for mounting fibres to supporting carriers
- G02B6/3684—Mechanical coupling means for mounting fibres to supporting carriers characterised by the manufacturing process of surface profiling of the supporting carrier
- G02B6/3696—Mechanical coupling means for mounting fibres to supporting carriers characterised by the manufacturing process of surface profiling of the supporting carrier by moulding, e.g. injection moulding, casting, embossing, stamping, stenciling, printing, or with metallic mould insert manufacturing using LIGA or MIGA techniques
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
- G02B6/3807—Dismountable connectors, i.e. comprising plugs
- G02B6/3833—Details of mounting fibres in ferrules; Assembly methods; Manufacture
- G02B6/3855—Details of mounting fibres in ferrules; Assembly methods; Manufacture characterised by the method of anchoring or fixing the fibre within the ferrule
- G02B6/3861—Adhesive bonding
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/24—Coupling light guides
- G02B6/36—Mechanical coupling means
- G02B6/38—Mechanical coupling means having fibre to fibre mating means
- G02B6/3807—Dismountable connectors, i.e. comprising plugs
- G02B6/3833—Details of mounting fibres in ferrules; Assembly methods; Manufacture
- G02B6/3865—Details of mounting fibres in ferrules; Assembly methods; Manufacture fabricated by using moulding techniques
Definitions
- the guiding member is used to guide the housing to the fiber fixing structure, and the alignment is made; the optical fibers in the housing are aligned with the grooves on the optical mold ;
- the bladder is a V-shaped or U-shaped groove
- the trench is formed by nanoetching
- the first section of the optical fiber fixing die 00]02 and the second section of the Zhengzhou 102..2 further include two pairs of guiding grooves.
- the guiding OS is placed in the plurality of slots 106 respectively.
- the two copper guide slots! 08 is used to locate the position of the guiding element, and the positioning element from the positioning can align the housing with the optical fiber to fix the mold. 1.00.
- the guiding groove 8 can be a ⁇ -shaped groove or a V-shaped groove.
- step 205 > 210, 2J 5 in. Travel.
- step 205 > 210, 2J 5 in. Travel.
- step 302 the main function of the step of placing the plurality of diaphragms of the different cladding.
- the main function of the step is to position the fibers. The positioning is performed and the light fixtures are held by the clamps to move the movements.
- the specificity of the fiber> The middle part of the fiber with the coated layer is clamped by the clamp and the fibers are fixed at a certain distance of ⁇ 3 ⁇ 4. The accuracy of the fixture is not high enough.
- the separation distance has a certain error, in some implementations, the distance is 0, 25mm,
- step 405, 410, 415 and 420 is made below by a specific embodiment.
- a pull is applied to both ends of the plurality of optical fibers.
- step 507 : -ft v[ ⁇ ⁇ : : : ? ? ? ? ? ? ? ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇ ⁇
- the injection, L is in communication with the gap between the fiber and the housing for injecting the curable body into the gap between the fiber and the housing.
- the chemistry is in a tear state, and can be deuterated by further processing (for example, ultraviolet irradiation or warming).
- the curable body is epoxy condensed ( ⁇ ⁇ in order to avoid insertion due to moving m
- the position of the optical fiber in the core assembly is changed, and the ferrule assembly is subjected to ultraviolet irradiation to inject the bismuth body after injecting the chemistry, and the position of the aperture is made larger from the 3 ⁇ 4.
- step SOB the ferrule assembly is removed from the fiber sizing mold, and the curable body is further advanced by the ultraviolet ray!cca
- the guiding element is removed from the ferrule assembly and the ferrule assembly is inserted.
- the fiber that cuts one end of the mill is stripped of the cladding
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Mechanical Coupling Of Light Guides (AREA)
Abstract
本公开提供了涉及带预制光纤的低损耗插芯组件的制造方法、通过该方法制造出的带预制光纤的低损耗插芯组件、以及用于制造该插芯组件的光纤固定模具。其中一种制造高精度的插芯组件的方法,包括:把多根光纤两端的纤芯分別放置在光纤固定模具两端的多个槽内,以使得多根光纤相互之间保持特定的距离;把所述多根光纤设置在壳体中;并使得所述多根光纤相对于所述壳体固定;其中所述壳体是分体式的;对壳体第一侧的光纤实施切割及打磨。本公开提供的方案术实现了采用低成本方式制造的高精度的光纤连接器件的插芯组件,该方法简单而高效,极具使用价值。
Description

本公开的实施例涉及光纤连接器领域, 具体的, 涉及光纤连接器 中插芯組件的制造方法 >通过该方法制造出的插芯组件以及用于制造 高精度的插芯组件的光纤闺定模具
应用于光纤连接器的插芯; 又称插针体 插芯是光纤连接器的核 心部件 它是一种通过精密加工技术 ¾成的高精度元件 在光纤连接 器生产制遞.过程中 , 通常采用将剝离并清洁好的裸光纤穿过充满胶水 的 孔 5 然后固化胶水 将光纤 ]定在插芯内, 然后经由打磨>滅 > 测试等一系列程序制成 需的光纤连接器件, 由于所有制造过程会产 生不可避.免的误差以及为 τ尺寸.配合 , 装配需要 人为地 ¾!入 τ公 纤外径和内孔尺寸需要存在先天的偏差 再如, 光 轴心与内孔由于 有空隙而存在不同心以及内 1,与对准基准(对以外圖 ¾对准基准的连 接器 言主要是指插芯外径 )存在加工制造误差等; 这些因素都会引
袁、明内容 造方法; 通过该方法制造出的带预制光 i 的低损耗插芯组件、 以及用 于制造该插芯组件的光纤 ]定模具 法、包括:把多根光纤两端分別放置在光釺 i定模具两端的多个櫓内 ,
体式的; 对壳体第一側的光纤实施切割及打磨„
在此方 ¾ 5 把多根光纾两端分別放置在光纤國定模具两端的多个 槽内包括: 把具有包覆层的多根光纤放置于夹具中; 至少剝去所述.多 根光纤两端中实施切割及 4了磨一端的包覆层 以裸露 纤芯; 把所述. 夹真放置到所述光纤固定模具的开孔中 其中所 ¾光纤 l定模具的相 对的两个部段上具有多对相对应的稽; 在.新'述多根光纤的两端施加拉 力> 从而使得所述光纤绷直并使得所述,每根光纤两端分別置于一对相 在此方面, 还包括: 通过纳束蚀刻生成所迷光纤固定模具中的多 个精 , 以使得所述多个槽之间保持特定的距离 其中所述糟是 V型槽 或 ϋ型槽
在此方面 把所迷多根光纾设置在壳体中并使得所迷.多根光纤相 对于所述壳体闺定包括: 在所述.多根光纤两侧放置 !导元件; 移除所 述.夹具, 并把所途多根光纤和引导元件安装在所迷壳体中; 在所述光 纤和壳体同的缝隙内填入可 1化体; 通过紫外线 射國化所述可闺化 体: 从 ^使得所述光纤相对于所述壳林园定; 移除 导元件,
在此方面、 在所迷光纤和壳体闽的缝隙内填入可 @化体包括; 通 过注入方式和 /或利用毛细现象把可 ¾化体填入所 '述光紆和壳体间的 在此方面 ; 所述可闺化体为环氣树脂、、
在此方面 > 所述具有包覆.层的光纤具有第一预定长度; 所述光纾 两端裡.露出的纤芯具有第二预定长度
在此方面, 所述特定的距离的误差符合对插芯组件中光纤间距离 本.公开的第二方面提供了一种制造高精度的插芯组件的方法 包 括: 至少剝去多根光纤两端中实施切割及打廢一端的包覆层 以:歸. 纤芯; 把所迷多根光 f插入在壳体的光鋒孔中, 并把引导元件插入 在壳体的引导孔中, 其中所述壳体是一体式的; 把所述多根光纤两端
分别放置在光纾固定.模具 端的多个槽内 , 以使得多根光 相互之间 保持特定的距离; 使,得所述多根光纤相对于所述壳体闺 ; 对壳体第 —側的光纤实施切割及打磨::
在此方面 把多.根光纤两端分别放置在光纤固定模具两端的多个 定模具的开孔中 其申所述.光紆 i定摸.具.的相对的两个部段上具有多 对相对应的褙; 在所述多根光纤的两端施加拉力, 从 使得所述光纤 縐直并使得所途每根光纤两端分 置于一对相对应的槽内 ;.
在此方面, 还.包括: 通过纳米蚀刻生成所迷光纤闺定模具中的多 个槽, 以使得所述多个槽之间保持特定的距. « , 其中所迷槽是 V型槽
ί:ϊ:'
在此方面 其中使得所述.多根光纤相对于所述壳体 定包括: 在 所述光纤和壳体间的缝隙内填入可固化体; 通过紫外线照射 Β化所述 可固化体, 从¾使得所述.光纤相对于所述壳体 ¾定。
在 ;方面 其中在所述光纤和壳体闰的缝義填入可固化体包 If:通过注入方式和 /或利用毛细现象把可闺化体.填入所述光纤和壳体 在此方面, 其中所述.可 ϋ化体为环氣树脂 ,
在此方面, 其中所述具有包復层的光纤具有第一预定长度; 纖. 光纤两端棵露出的纤芯具有第二预定长度
在此方靣 其中所述.特定的距离的误差符合对插芯组件中光纤间 ί · 2 矛 7¾H、 - ·>
在此方 f面 所述引导元件用于引导所述壳体与 述光纤固定樓具、 对准 从;¾使得壳体中的光纤与光f i定模具上的槽对齐 ;.
本公开的第三方面提供了、 -种高精度的插芯組件; 其中所迷插芯 组件根据上述方面中任一所述-的方法制遞 ,
本公开、的第 方面提供了一种用于制造高精度的插芯組件的光 纤 ϋ定模具 包括: 主体板 所述主体板的中间異省 孔; 多个稽 ; 所述槽用于放置光纤以校准多个光纤之间的位置
在此方面 还包括: 紧固部件、 所迷紧固部件用于把所述光纤压 在此方面 途.多个褙被等间距的设置于所述主体板的第一部殺 和第二部段上、 并且.所述.第一部段上的槽与所述第二部段上的槽—— ~ 对应
在此方面, 所述膽为 V型精或 U型槽 ,
在此方面 > 職多个.槽之间间距.的误差符合对插芯组件中光纤间 距离的精度要求
在此方面 所述槽是通过纳米蚀刻生成的 ,
通过下文中参照附國对本公开所作的描述, 本公开的其它 的和 优点将显 ¾易见 ; 并可帮助对本公开有全面的理解
例 .作
更加明屋:
;¾ .!„■■
图 2示出了根据本公开的一种制造髙精度的插 S 3示出了根据本公开的一种制造高精座、的插 ) 4示出 造.高精度的

5示出了根据本公开的另一种制造高精度的插芯 件的流程示 图 6示出了根据 ^ 、…-、、:甲 • Ά ^
、:开- ¾一^ ψ 、体式的壳体
在以下优逸的实施 的具体描述中 , 将参考构成本公开一部分的 所附的 it围 , 所附的附围通过示例的方式 *出了能够实现本公升的特 可以理解 , 在不偏离本公开的范围的前提下 > 可以利用其他实施例 也可以进,行結构性或者逻 #性的修政 ¾此, 以下的具体描述并非限 制性的 5 且本公.开的范围由所附的权利要求所限定
在^使用的术语 "包括" 及其变形是开放 包括, 即 "包括但不 限于^ 术语 基于 是 至少部分地基于 术 ¾―个实施倒'¾ 表 示 "至少一个实旅 Γ; 术语 "另一实:施例" 表示 "至少 -- 个另外的 实施例 " , 其他术语的相关定义将在下文描迷中给 ¾ ,
为弥孙光纤连接器生产制造领域的不足 本.公开推荐一种简单 有效的制造.高精度的插芯組件的方法 该方法的基本构思是通过光纤 ¾定模具中的多个槽使得插芯组件中的光纤之间保持特定的 E离 , 然 后邇.过.可 II化体把光纤固定在插芯组件的壳体内 , 由于该光纤固定糢 具的槽是通过納米蚀刻技术来制成的 @此槽之同的距离可以保持非 常高的精度:: 从;; 令光纤连接器的插芯组件加工误差大大.降低、、 以下 我 】将对本方案进行详细的说明 , 精度的插芯组件的光 定樓具- 100 如围!.所示该光纤闺定.模具 100 包括主体板 !02, 该主体板 10.2的中间具有开孔 !04:, 在某些实施剩 中该主体板 102和开孔 104都是方形
主体极 102的第一部.歡 !02 和第二部段 !02-2.上包括多个等间 距设置的槽 106, 第一部段 .1024的多个槽 106与第二部段 102-2 ..!:. 的多个槽 106分別对齐, 从 当光紆两端放置于所迷槽 . )6上时, 光 纤之间可以保持特定的距离 在-一个具体实施例中> 置于 06中的 芯。 在另一个異 -体实施例中 > 置于槽 106中的该光纤两端都是已去除
包覆层的棵露鋒芯 制造 因此槽之间的距离具有非常高的精度 在某些实施詞中褙 ίθδ 之间的距.离根据插芯组件规格所要求的纤芯距离而设定; 也就是说多 些实施例中该楷 106为 U型精或 V
在某些实施铜中, 光纤固定楱具〗00还包括紧固部件 ( S中未示 至主体板 !02上 以 if助光纤 定模具 100樣紧光纤
在某些实施例中 光纤固定模具 00的第一部段】02»〗和第二.鄭 段 102..2上还包括两对引导槽】0 该引导稽 !OS分别置于多个槽 106 的两铜 该引导槽!08用于定位引导元件的位置, 从¾使.得定位后的 引导元件能令壳体对准该光纤 II定模具 1.00. 该^导槽 )8可以是 ϋ 型槽或 V ·型槽
以下详细介绍本公开的利用上述光纤面定模具〗 00制逸高翁度的 插芯组件的方法 图 2示 了银椐本公开的一种制造高精度的插芯组 件的方法流程 L
如 a m示, 在步骤 5> 把多根光纤两端分别放置在光纤闺定模 具 !00两端的多个槽 106内., 以使得多根光纤相互之间保持特定的距 离 由于槽〗06是通过納来蚀刻生成的 因此光纤可以通过该褙被准 确的定位 . 该槽可 是 U型槽或 V型槽
在步骤 210; 把所述.多根光纤设置在壳体中 并使得所述.多裉光 纤相对于所述壳体闺定 具体的、 可以通过可固化体把通过槽定位的 光纤固定在插芯组件的壳体中:, 从 保证纡芯内的光纤的位置具有较 高的精度, 其.申 如 S 6所示 该壳体是分体式的 壳体可以拆分为 上下两部分 上下雨部分通过壳体中的销扣部件可以组合成一个完整 的壳体
在步骤 215 对壳体第 -、倒的光紆实施切.割及打 J 具体的 把
―个真有高精度的插芯組件
以下通过一个具体的实施例结合 ® 3 ; 对步骤 205 > 210, 2J 5进. 行进.一 ·步的 明
在步骤 301 , 按特定的长度.截取多根具有包覆 的光纤 其中该 纤固定模具的主体板长度 在某些实施例中, 该具有包覆层的光纤直 径为 200um;.
在步驟 302, 把異有包覆.县的多根光纾放置于夹具中 这一步骤 的主要作用是对光纤之间的间距.实施^步定位 并通过夹具把光乡 f保 持住 以便移动这些光纤 具体的> 通过夹具夹住多银具有包覆.层的 光纤的中间部分 并使得这些光纤以一定的 ί¾隔距离被固定 可以理 解 ; ¾予夹具的精度不够高, 此时光纤之间的闹隔距离具有一定的误 差、: 在某些实施倒中 , 该距离为 0,25mm,
在步 303 , 至少剥去所述多根光纤两端申实施切割及打磨一端 的&覆层, 以裰露出纤芯 具体的 > 剝去所述多根光纤两端中至少一 端的包覆.崖从而使得光纤两端輕:露 ώ的纤芯具有预定的长度 在某些 实施例中, 被刹离包覆层之后的紆芯的直径为 !25u.m. 在某些实施例 在步骤 304 , 把所述夹具放置到所迷光纤固定模具的开、 中 異、 体的, 把持有多根光纤的夹具放置到所述光紆固定模具的丹礼中 并- 使得光纤两端分別置于光纤固定填異第―部段和第二部段的槽上、 其 中所述.第一部段和第二部歡上的槽是—一-对应的 ,
在―个具体实施倒中 ? 该光纤两端分别是: 已去除包覆层的樣露 纤芯和未去除包覆层的纤芯 在另、、 个具体.实施例中 , 该光纤两端都 是已去除包覆层的擁露纤芯
在步骤 305, 在所述多根光纤的两端旅加拉力 从 ; 使得所述光 纤绷直并使得所述每根光纤两端分别置于一对相对应的槽内 具体 的 ? 在所述光纤两端上施加平行于光纤闺定模具的主体板的拉力 , 从 r¾使得光纤处于绷紧状态 并借助纤芯 .上的张力使得纤芯分别落入一
具 ; 并在所述多个光 If的两销的 f 1 装? 导; '件 , 可以通过光
 具 体的 , 壳体分为上壳体和下 两部分壳体分 从先纤固 定模具开孔的上倒和下侧 接合 从;¾把光纤和引导元件设置予壳
一.
够正确的对准綺固定.模具, 从而使得光纤被安装在壳体的正确位置 内 ,
在步骤 307, 在所述光纤和壳体间的缝隙内填入可闺化像 具体 的,可以通过注入.:方式和 /或利用毛细现象把可闺化体填入所述光纤和 壳体间的缝隙内 , 在莱些实施例中 , 上壳体的上方可以设置注入孔; 该注入 与光紆和壳体间的缝隙连.通 以用于把可'闺化 注入到光纤 和壳体间的缝:隙内 ,.可阖化体是液态的; 并且通过进一步加工 (倒如 紫外线照射或加温)可以被 化 在.某些实施例中 ¾可闺化体是环氡
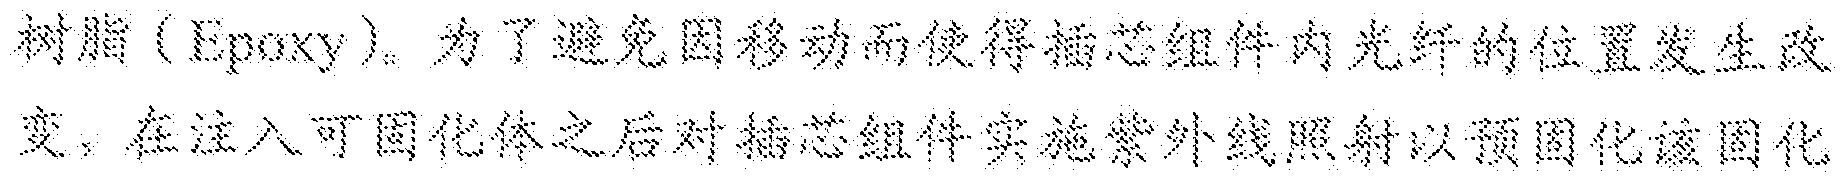
体 从¾使该光紆的位置大. 、
并通过紫 - :

件 ·、端的光 if
轰.后对切割侧

割 -IT If-一端的光纤是被剝去包覆层的
以上方案中壳体是分体式的 , 即壳体由上下
此在制造的时候可以先设定好光纤位置 再安装 ^ 体. 凝'下
紹一种针对一体式壳体.的制造高精度插芯组件的方法, 由于壳体是 体的 ? ¾此在该方法中需要先把光纤插入到壳体中然后再
图 4 示 ά了根据本-公开的一种制造高精度插芯组件的方法流程 如 ¾所示 在步骤 405 > 把多根光纤插入在壳体的光歼孔中 并 把引导元件插入在该壳体-的引导礼中 其中 如 ¾ 7所^ 该壳体是 -体式的, 光纾需要穿过壳体的光纤孔 > 从而使得光纤被设置在壳体 、
在步骤 4) 0, 把多根光纤两端分別放置在光纤固定.模具】00两端 的多个 ! 06内、 以使得多根光纤相互之间保持 44:定的距离 , 在一个 具体实施倒 Φ , 置于槽 106中的该光纤两端分别是: 已去除包覆展的 裸露纤芯和未去除包覆层的纤芯 在另―个具体实施铜 ,置于槽 106 中的该光纤两端 *是已去除包覆层的裸露纤芯 由千槽 10 是通过纳 米蚀 生成的 固此光纤可以通过读槽被准确的定位 该槽可以是 U 型槽或 V型槽
在步骤 415, 使得所述多根光纤相对于所述壳体.固定。 具体的 可以通过可 H匕体把通过槽定位的光乡 Γ ϋ定在插芯组件的壳体中 > 从 在步骤 420、 对壳体第一俩的光纤实施切割及 磨 .> 具体的 把 纤芯接口端的光纤进行裁剪; 从对裁剪侧的光 实施、打磨, 从 ¾生成 一个具有高精度的插芯组件,
以下通过一个具体的实施例结合围 5, 对步尊 405、 410, 415和 420进行进一步的说明
在步尊 501; 按特定的长度截取多根具有包覆层 .的光纤, 其中该 长度可以根据光纤函定模具的尺寸设定.; 例如该长度至少大于所述光 纤 ϋ定模具的主体板长度 , 在某些实施銅中, 该具:有包覆层的光纤直 径为 200um6
在步骤 502,. 把具有包覆层的多根光纤放置于夹具中 这一步骤 持住 以便.移动这些光纤 具体的, 通过夹具夹住多根異省包覆层的 光纤的申闹部分 , 并使得这些光纤以— .定的闻隱距离被 !¾定 可以理
解 由亍夹具的粮度不够高 , ^时光纤之间的闻鶴距离具有一定的误 差 在某些实施例中5 该距离为 0、25mm
在步骤 503 ? 至少剝去所述多根光纤两端中六 切割及打磨一端 少、一 施销

在步骤 504, 移
 把多根光纤插入在壳体的光 券 把引导元件插入在 导孔中。 具体的 由于光纤已经通过.

是已去除包覆层的棵露纤芯
在步骤 506, 在所述多根光纤的两端施加拉
纤纖直并使得所迷每根光纤两端分別置于 .对相对应的褙内 , 具体 的, 在所述光纾两端上施加平行于光紆 定模具的主体板的拉力 从 使得光纤处于纖紧状态 > 并借助纤芯上的张力使得 i '芯分别落入一 ite . 在某些具体.的实施例中 可以通过.光纤園定模具的紧闺部件 体极上 以保证光纾可以被设置在槽中
在.步.錄 507:: -ft v[ 纤 ί-Τ' :?Ρ: ? ί ^ί¾ .休.间的缝 i 内填入可园化体
的;可以通过注入方式和 /或利用毛细现象把可固化体填、入所述.光纤 φ
:缝陈 在某些实 入: !
该注入、L与光纤和壳体间的缝隙连通, 以用于把可固化体注入到光纤 和壳体间的缝隙内 可 II!化体是淚态的、. 并且通过进一步加工 (例如, 紫外线照射或加温 )可以被闺化 在某些实施例中该可固化体是环氧 树凝 ( Εροχν λ 为了避免因移动 m使得插芯组件内光纤的位置发生改 变, 在注入可 !3化体之后对插芯组件实施紫外线照射以预闺化锬闺化 体 , 从 ¾使该光纾的位置大.致固定 .;
在步骤 SOB, 把. 述插芯组件从光纤闺定模具中移出, 并通过紫 外线对该可固化体进行进一歩的 I!化„
在步骤 509、 把引导元件从插芯组件中移出 并进 -歩对插芯组
割打磨一端的光纤是被剝去包覆层的
另外 尽管操作以特定順序被描给 ? 但这并不应该理解 %要求此 类搡.作以示出的 定顺序或 相继 序完成 , 或者执行所有 a示的操 作以获取期望結杲 在某些情况下 , 多任务或并行处理会是有益的 同祥地 尽管上述讨论包舍了某些特定的实: 细节, 但这并不应解释 的特'定实施例的描述 本说明书中在分开的实施例的上下文中 述的 某些特征也可以整合实絲举.个实翻中 , 反之 , 在单个-实施例的上 下文中描述的 特征 · ,可以分离地在多个实途例或在任意合适的 子组合中实施 ::
对于本领域技束人员而言 显.然本公开不限于上.述.示范性实施例 的细节 r¾且在不背离本公开的精神或基本特征的情况'下'、 能够以其 他的具体形式实现本公开的实施 'L H 无论如何来看 均应将实 施倒看作是示范性的; ¾且是非 ί Φ生的 此外 明显的, "包括 "一 词不排除其他元素和步.雜. 并且措辞"一个" 排除复数, 装置权利要 求中陈述的多个元件也可以由一个元件来实现 第 -- , 第二等词语用 来..表示'名称 而并不表示任何特 '定的顺序
Claims
_ ― 杈 利 要 求 书
L —种制造高精度的插芯组件的方法, 包括:
把多根光纤两端分別放置在光野固定模具两端的多个槽内 , 以使
壳体 i定 , 其中 述壳体是分体式的;
对壳体第一倒的光纤实施切割及打磨 , 光纤 ®定模具两端的多个槽内包括:
把真有包覆层的多根光纤放置于夹具中;
至少翁去所述多根光纤两端中实施切割及打磨一端的包覆层, 以 裸露出纤芯;
把所述夹具放置到所述光纤固定摸具的开孔中, 其中所述光乡 f ¾ 定模具的相对的两个部段上具有多对相对应的槽; 所速每根光纤两端分別置子一对相对应的褙内 ::
3, 根握权利要求!或 2 . 述的方法 还包括:
通过纳米蚀刻生成所迷光纤 定賴具中的多个槽, 以使得所述多 个槽之 保持特定的距离 , 其 Φ所述.槽是 V.型槽或 U型槽 ,
4> 根据权利要求 2所迷的方法;其中把所述多根光纤设置在壳体 中并'使得所迷多很光鋒相对于所迷壳体 定包括:
在所迷多根光纤两倜放置 !导元件;
移除所述夹具 , 并把所述多根光纤和引导元件安装在纖.壳体 中、
在所述光纤和壳体间的缝隙内填入可固化体;
通过紫外线照射困化所述可固化体 5 从而使得所連光纤相对于所 述壳体固定.;
内填入可固化体包括:
通过注入方式和 /或利用毛细现象把可固化体填入所迷光^和壳 体间的缝隙 4
6, 根据杈利要求 4所迷的方法 其中 -述可固化体为 ^氣树脂 7、 根据杈利要求 2所述.的方法;其中所述具有包覆层的光 具有 第一预定长度; 所述光纤两端樑露出的纤芯具有第二预定长.度
8, 根据权利耍求 2所述.的方法 其中所述特定的距离的误差符合
9, ― '种制造高精度的插芯组件的方法 包括:
把多根光鋒插入在壳体的光纤孔申 5 并把引导元件插入在所述.壳 体的引导孔中 , 其中所述壳体是一体式的; 以使得多根光纤相互之间保持特定的距离;
使得所述多根光纤相对于所迷壳体闺定;
对壳体第一侧的光纤实.施切割及打磨
! ().. 根据杈利要求 9所述的方法 其中把多根光纤两端分别放置 在光纤 ϋ定模具两端的多个槽内包括:
把插有所述光纤和^导元件的所述壳体放置到 述光纤 ¾定模 真的开礼中, 其中所述光纤固定模具的相对的两个部段上具有多对相 对应的稽;
在所述多根光纤的两端施加拉力 从 ; 使得所述光纤绷直并使,得 所述每根光纤两端分别置于一对相对应的槽内
! 1 根据权利要求〗0 ^述的方法; 还包括:
通过纳來蚀剩生咸.浙述光纤固定.摸具中的多个槽 , 以使得所述多 个椿之间保持特定的距离 , 其中所迷槽是 V型槽或 U型槽„
12 根据权利要求 10所述的方法 其中使得所述多根光纤相对于 ^述壳体固定包括:
述.壳体固定.
13. 根.据权利要求 12所述的方法 其中
内填入可闺.化体包括:
通过注入方式和 /或利用毛细现象把可' ¾化体填 ϋ纤和壳 s 体间的缝隙内::
14. 根据权利要求 12 所述的方法, 其中所述可闺化体为 ^辈
.職
15. 根据权利要求 !0所迷的:方法, .包括步骤:
至少剥去多根光 if两端中实施切割及打磨一端的包覆.层 5 以裸露0 出纤芯; 其中所述具有包覆层的光 '具有第一预定长度; 所述光纾两 端棵露出的纤芯具有第二预定长度 ;:
16. 根据权利要求 10所迷的方法 其中所述特'定的距离的误差符 合对'插芯纽件中光纤间距.离的精度要求、、
17. —种高精度的插芯组件 > 其 .插芯组件根据权利要求 i5 至! 6中任一所述的方法制造
18.. ―种用于制造高精度的插 光纤固定模具 5 包括: 主体板; 所述主体板的中 具有丹
多个槽 所述槽用于放置光乡 †v. :
19, 根. ¾权利要求. 18所述的模具,
0 紧 部件, 所述紧固部件用亍 >纤压至所述主体
20, 根椐权利要求】8所述的模具
置于所迷主体板的第一部段和第二部段 J:

与所述第二部段丄的槽 一对应
2 L 根据权利.要求. 18所述 -的模具 其中断述構为 V型櫓或 U型5 槽 .
22, 根据钗利要求 J 8所述的模異 其中所述多个槽之 间距的误 差符合对插芯组件中光纤间距.离的精度要求
23、 根据权利要求 18所述的模真,其中所述槽是通过納束蚀 生 成的 ,.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP17859426.3A EP3528021A4 (en) | 2016-10-11 | 2017-10-09 | FERRULE ASSEMBLY, METHOD FOR MANUFACTURING FERRULE ASSEMBLY, AND FIBER OPTIC FIXING MOLD |
| US16/341,298 US11307363B2 (en) | 2016-10-11 | 2017-10-09 | Ferrule assembly, method for manufacturing a ferrule assembly and optical fiber fixing mold |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201610889090.3 | 2016-10-11 | ||
| CN201610889090.3A CN107918174A (zh) | 2016-10-11 | 2016-10-11 | 插芯组件、制造插芯组件的方法及光纤固定模具 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2018069765A1 true WO2018069765A1 (zh) | 2018-04-19 |
Family
ID=61892746
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/IB2017/001387 Ceased WO2018069765A1 (zh) | 2016-10-11 | 2017-10-09 | 插芯组件,制造插芯组件的方法及光纤固定模具 |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US11307363B2 (zh) |
| EP (1) | EP3528021A4 (zh) |
| CN (1) | CN107918174A (zh) |
| WO (1) | WO2018069765A1 (zh) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108139547B (zh) * | 2015-10-12 | 2020-09-08 | 3M创新有限公司 | 多波导连接器中的光波导定位特征结构 |
| WO2021020073A1 (ja) | 2019-08-01 | 2021-02-04 | 株式会社フジクラ | 光コネクタ |
| JP2021026217A (ja) * | 2019-08-01 | 2021-02-22 | 株式会社フジクラ | 光コネクタ |
| CN119335659A (zh) * | 2023-07-19 | 2025-01-21 | 苏州旭创科技有限公司 | 插接结构及其制造方法、光模块 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20020146216A1 (en) * | 2001-04-05 | 2002-10-10 | Schofield Philip W. | Optical ferrule having multiple rows of multiple optical fibers |
| US20030002806A1 (en) * | 2001-06-29 | 2003-01-02 | Keith Kang | High-precision female format multifiber connector |
| EP0747740B1 (en) * | 1991-09-06 | 2003-02-26 | Minnesota Mining And Manufacturing Company | Multiple optical fiber splice element |
| EP2589993A1 (en) * | 2011-11-02 | 2013-05-08 | Ntt Electronics Corporation | Microlens array and optical transmission component |
| US20140169743A1 (en) * | 2011-06-14 | 2014-06-19 | Molex Incorporated | Ferrule assembly with lateral fiber insertion |
Family Cites Families (59)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1480445A (en) | 1975-05-06 | 1977-07-20 | Standard Telephones Cables Ltd | Termination of optical fibres |
| FR2436406A1 (fr) | 1978-09-12 | 1980-04-11 | Socapex | Connecteur pour fibre optique, dispositif de centrage et procede de fabrication dudit connecteur |
| US4215937A (en) | 1979-01-29 | 1980-08-05 | International Telephone And Telegraph Corporation | Method and apparatus for detecting optimum alignment of optical fibers in a connector arrangement |
| FR2503388A1 (fr) | 1981-04-06 | 1982-10-08 | Socapex | Embout de connecteur pour fibre optique, procede de centrage d'une fibre dans cet embout et dispositif pour la mise en oeuvre de ce procede |
| JPS58108507A (ja) | 1981-12-23 | 1983-06-28 | Omron Tateisi Electronics Co | 光フアイバ・コネクタの製造方法 |
| JPS58152214A (ja) | 1982-03-05 | 1983-09-09 | Omron Tateisi Electronics Co | 光フアイバ・コネクタの結線方法 |
| US4712864A (en) | 1985-05-02 | 1987-12-15 | Luxtron Corporation | Multi-channel fiber optic connector |
| US4738508A (en) | 1985-06-28 | 1988-04-19 | American Telephone And Telegraph Company, At&T Technologies, Inc. | Terminated optical fiber and methods of making |
| EP0271721B1 (en) | 1986-11-15 | 1993-08-04 | Sumitomo Electric Industries Limited | Optical connector and process for producing the same |
| JPS6417010A (en) | 1987-07-10 | 1989-01-20 | Sumitomo Electric Industries | Device for terminating optical cable |
| JPH0196608A (ja) | 1987-10-08 | 1989-04-14 | Nippon Telegr & Teleph Corp <Ntt> | 接着剤塗布、充填装置 |
| GB2215082B (en) | 1988-02-16 | 1992-02-26 | Stc Plc | Optical fibre gland |
| JPH01300207A (ja) * | 1988-05-30 | 1989-12-04 | Hitachi Ltd | 光フアイバアレイの製造方法 |
| JPH04345106A (ja) | 1991-05-22 | 1992-12-01 | Hirose Electric Co Ltd | 光ファイバのフェルール挿着方法 |
| AU649162B2 (en) | 1991-08-17 | 1994-05-12 | Nippon Telegraph & Telephone Corporation | Optical connector |
| JP3164852B2 (ja) | 1991-10-25 | 2001-05-14 | 日本電気株式会社 | 多心光ファイバの整列構造 |
| JP3363479B2 (ja) | 1992-07-17 | 2003-01-08 | 住友電気工業株式会社 | 光コネクタ |
| US5664039A (en) | 1994-06-08 | 1997-09-02 | The Whitaker Corporation | High density fiber ferrules and connectors |
| JP2901517B2 (ja) * | 1995-06-09 | 1999-06-07 | 日本電気株式会社 | 多心光ファイバコネクタ |
| JP3515677B2 (ja) | 1996-10-09 | 2004-04-05 | 住友電気工業株式会社 | 光コネクタおよびその取付方法 |
| JPH10123359A (ja) | 1996-10-16 | 1998-05-15 | Furukawa Electric Co Ltd:The | 光コネクタの作成方法 |
| JP3363333B2 (ja) | 1996-11-28 | 2003-01-08 | 京セラ株式会社 | 光ファイバー固定具 |
| JP2000193844A (ja) * | 1998-10-20 | 2000-07-14 | Sumitomo Metal Mining Co Ltd | 光ファイバアレイの製造方法 |
| US6328479B1 (en) | 1999-05-24 | 2001-12-11 | Stratos Lightwave, Inc. | Multi-terminator optical interconnect system |
| JP2001215358A (ja) | 2000-01-31 | 2001-08-10 | Molex Inc | 光ファイバ用フェルール及びその製造方法 |
| JP2001249249A (ja) | 2000-03-07 | 2001-09-14 | Fujikura Ltd | 多心光コネクタおよびその光ファイバ取付方法および光ファイバ取付治具 |
| US20010051026A1 (en) * | 2000-04-06 | 2001-12-13 | Steinberg Dan A. | Optical fiber ferrule made from dry etched parts |
| US6634800B2 (en) | 2000-04-27 | 2003-10-21 | Furukawa Electric Co., Ltd. | Ferrule for optical connector |
| BR0111551A (pt) | 2000-06-12 | 2003-09-09 | Krone Gmbh | Conjunto de e processo para aplicação na terminação de uma ou mais fibras ópticas |
| JP2002023018A (ja) | 2000-07-05 | 2002-01-23 | Sumitomo Electric Ind Ltd | 光コネクタ用フェルール、光コネクタ及び光コネクタの製造方法 |
| JP2002040294A (ja) | 2000-07-21 | 2002-02-06 | Ykk Corp | 光コネクタ部品の光ファイバ挿入孔内に接着剤を注入する方法及び装置 |
| JP3908015B2 (ja) | 2000-12-25 | 2007-04-25 | 日本碍子株式会社 | 偏波ファイバアレイ |
| US6648521B2 (en) | 2001-02-23 | 2003-11-18 | Fiber Systems International | Single terminus connector with preterminated fiber and fiber guide tube |
| CN1284990C (zh) | 2001-04-03 | 2006-11-15 | 莫列斯公司 | 安装光纤的装置和方法 |
| KR100937284B1 (ko) * | 2001-11-29 | 2010-01-18 | 스미토모 덴키 고교 가부시키가이샤 | 광 커넥터 페룰, 광 커넥터, 광 부품 및 광 배선 시스템 |
| EP1649312A1 (de) * | 2003-07-31 | 2006-04-26 | Huber + Suhner Ag | Verfahren zum lösbaren verbinden zweier gruppen von optischen fasern sowie steckverbinder zur durchführung des verfahrens |
| JP4778860B2 (ja) | 2006-08-18 | 2011-09-21 | 三和電気工業株式会社 | 光コネクタの光ファイバ固定機構 |
| US7467899B2 (en) | 2007-01-31 | 2008-12-23 | The Furukawa Electric Co., Ltd. | Ferrule transfer method and ferrule holder |
| US9195011B2 (en) | 2008-12-11 | 2015-11-24 | Afl Telecommunications Llc | “Secured” fiber optic connecting system and method using offset fiber position in a single-fiber connector |
| CN201464676U (zh) | 2009-06-12 | 2010-05-12 | 深圳市光网科技有限公司 | 光纤插芯用多功能高效真空吸胶机 |
| JP5640534B2 (ja) * | 2010-08-03 | 2014-12-17 | 住友電気工業株式会社 | 光ファイババンドルの製造方法及び光ファイバ整列用治具 |
| US9563027B2 (en) | 2010-10-19 | 2017-02-07 | Us Conec, Ltd. | Unitary multi-fiber optical ferrule with integrated lenses |
| CN201828690U (zh) | 2010-10-29 | 2011-05-11 | 广州光耀通讯设备有限公司 | 单芯光纤冷接器及冷接工装 |
| JP2012185283A (ja) | 2011-03-04 | 2012-09-27 | Furukawa Electric Co Ltd:The | 多心光コネクタ、多心光コネクタの製造方法、多心光コネクタ製造用の整列部材 |
| US8936401B2 (en) | 2011-08-30 | 2015-01-20 | Claude Belleville | Method for disposable guidewire optical connection |
| CN104169765B (zh) * | 2011-12-09 | 2016-08-17 | 康宁光电通信有限责任公司 | 采用凹槽对齐特征结构和全内反射(tir)表面的梯度折射率(grin)透镜架以及相关组件、连接器与方法 |
| KR20140146648A (ko) * | 2012-04-11 | 2014-12-26 | 나노프리시젼 프로덕츠 인코포레이션 | 밀폐식 광섬유 정렬 조립체 |
| CN105408789B (zh) * | 2013-04-23 | 2018-10-12 | 富加宜(亚洲)私人有限公司 | 用于光学连接器的插芯 |
| CN203299417U (zh) | 2013-05-28 | 2013-11-20 | 泰科电子(上海)有限公司 | 校准工具 |
| CN104181644B (zh) | 2013-05-28 | 2016-07-06 | 泰科电子(上海)有限公司 | 对准工具、对准方法、光纤插芯组件和光纤连接器 |
| CN203299418U (zh) | 2013-05-28 | 2013-11-20 | 泰科电子(上海)有限公司 | 对准工具 |
| CN104181645B (zh) | 2013-05-28 | 2016-06-01 | 泰科电子(上海)有限公司 | 校准工具、校准方法、光纤插芯组件和光纤连接器 |
| CN104238047A (zh) | 2013-06-06 | 2014-12-24 | 泰科电子(上海)有限公司 | 光纤互连系统及方法 |
| WO2014195893A1 (en) | 2013-06-07 | 2014-12-11 | Tyco Electronics (Shanghai) Co. Ltd. | Indexing tool, calibrating method, ferrule assembly and fiber optic connector |
| CN105445864B (zh) | 2014-07-01 | 2017-12-05 | 泰科电子(上海)有限公司 | 插芯组件和插芯器件 |
| CN107608032B (zh) | 2014-07-01 | 2019-12-20 | 泰科电子(上海)有限公司 | 光纤对准装置、插芯器件和插芯器件的制造方法 |
| CN105334582A (zh) | 2014-07-01 | 2016-02-17 | 泰科电子(上海)有限公司 | 插芯器件和插芯器件的制造方法 |
| CN105445861A (zh) | 2014-07-01 | 2016-03-30 | 泰科电子(上海)有限公司 | 插芯器件、制造插芯器件的装置和方法 |
| US9285542B2 (en) * | 2014-07-09 | 2016-03-15 | International Business Machines Corporation | Fiber optic interface with adhesive fill system |
-
2016
- 2016-10-11 CN CN201610889090.3A patent/CN107918174A/zh active Pending
-
2017
- 2017-10-09 EP EP17859426.3A patent/EP3528021A4/en not_active Withdrawn
- 2017-10-09 US US16/341,298 patent/US11307363B2/en active Active
- 2017-10-09 WO PCT/IB2017/001387 patent/WO2018069765A1/zh not_active Ceased
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0747740B1 (en) * | 1991-09-06 | 2003-02-26 | Minnesota Mining And Manufacturing Company | Multiple optical fiber splice element |
| US20020146216A1 (en) * | 2001-04-05 | 2002-10-10 | Schofield Philip W. | Optical ferrule having multiple rows of multiple optical fibers |
| US20030002806A1 (en) * | 2001-06-29 | 2003-01-02 | Keith Kang | High-precision female format multifiber connector |
| US20140169743A1 (en) * | 2011-06-14 | 2014-06-19 | Molex Incorporated | Ferrule assembly with lateral fiber insertion |
| EP2589993A1 (en) * | 2011-11-02 | 2013-05-08 | Ntt Electronics Corporation | Microlens array and optical transmission component |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP3528021A4 * |
Also Published As
| Publication number | Publication date |
|---|---|
| EP3528021A1 (en) | 2019-08-21 |
| US20210294046A1 (en) | 2021-09-23 |
| EP3528021A4 (en) | 2020-05-20 |
| CN107918174A (zh) | 2018-04-17 |
| US11307363B2 (en) | 2022-04-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4998796A (en) | Method of assembling multi-grooved silicon chip fiber optic terminations | |
| CN106687840A (zh) | 制造光纤阵列的工具装备和方法 | |
| CN111487722A (zh) | 八芯光纤复用解复用器及其制备方法 | |
| TWI234671B (en) | Device having multiple optical fibers | |
| US6769811B2 (en) | Multi-fiber optic device | |
| US11307363B2 (en) | Ferrule assembly, method for manufacturing a ferrule assembly and optical fiber fixing mold | |
| JP2019045794A (ja) | 屈曲部を有する光ファイバの製造装置および製造方法 | |
| CN104181644B (zh) | 对准工具、对准方法、光纤插芯组件和光纤连接器 | |
| TWI654456B (zh) | Waveguide termination module and termination method | |
| CN114522856B (zh) | 一种分支光纤连接器的制作方法 | |
| CN100458480C (zh) | 光导纤维和蚀刻的阵列波导管的对准 | |
| WO2000020908A1 (en) | Multicore optical fiber connector and assmbling method therefor | |
| CN112255739B (zh) | 一种多芯光纤连接器对轴封装系统 | |
| KR100671121B1 (ko) | 광섬유 접속용 부품, 광섬유 접속 구조 및 광섬유 접속 방법 | |
| CN114859468B (zh) | 一种仿形化剥纤治具以及剥纤方法 | |
| US20250004209A1 (en) | Optical fiber fixing structure and optical fiber guiding device comprising the optical fiber fixing structure | |
| JP3989317B2 (ja) | 光ファイバ接続方法 | |
| JP2001249249A (ja) | 多心光コネクタおよびその光ファイバ取付方法および光ファイバ取付治具 | |
| CN116974018A (zh) | 一种多芯光纤复用解复用器及其制备方法 | |
| JP2004045935A (ja) | 光ファイバ接続用部品、光ファイバ接続構造および光ファイバ接続方法 | |
| JP2013142791A (ja) | 光ファイバの加工方法、光ファイバの加工装置、光ファイバ、及び光ファイバ入出力構造 | |
| KR20130140538A (ko) | 고성능 광섬유 신속 접합장치 | |
| JP2002023018A (ja) | 光コネクタ用フェルール、光コネクタ及び光コネクタの製造方法 | |
| CN116670548A (zh) | 光纤连接部件的制造方法 | |
| JPS61252508A (ja) | 多心光フアイバ心線端末形成方法および多心光フアイバ心線端末形成部 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 17859426 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2017859426 Country of ref document: EP Effective date: 20190513 |