WO2019065748A1 - 射出成形用樹脂組成物 - Google Patents
射出成形用樹脂組成物 Download PDFInfo
- Publication number
- WO2019065748A1 WO2019065748A1 PCT/JP2018/035721 JP2018035721W WO2019065748A1 WO 2019065748 A1 WO2019065748 A1 WO 2019065748A1 JP 2018035721 W JP2018035721 W JP 2018035721W WO 2019065748 A1 WO2019065748 A1 WO 2019065748A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- vinyl chloride
- injection molding
- mass
- resin composition
- chloride resin
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08F—MACROMOLECULAR COMPOUNDS OBTAINED BY REACTIONS ONLY INVOLVING CARBON-TO-CARBON UNSATURATED BONDS
- C08F8/00—Chemical modification by after-treatment
- C08F8/18—Introducing halogen atoms or halogen-containing groups
- C08F8/20—Halogenation
- C08F8/22—Halogenation by reaction with free halogens
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08F—MACROMOLECULAR COMPOUNDS OBTAINED BY REACTIONS ONLY INVOLVING CARBON-TO-CARBON UNSATURATED BONDS
- C08F8/00—Chemical modification by after-treatment
- C08F8/18—Introducing halogen atoms or halogen-containing groups
- C08F8/20—Halogenation
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K5/00—Use of organic ingredients
- C08K5/04—Oxygen-containing compounds
- C08K5/09—Carboxylic acids; Metal salts thereof; Anhydrides thereof
- C08K5/098—Metal salts of carboxylic acids
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L27/00—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by a halogen; Compositions of derivatives of such polymers
- C08L27/02—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by a halogen; Compositions of derivatives of such polymers not modified by chemical after-treatment
- C08L27/04—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by a halogen; Compositions of derivatives of such polymers not modified by chemical after-treatment containing chlorine atoms
- C08L27/06—Homopolymers or copolymers of vinyl chloride
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L27/00—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by a halogen; Compositions of derivatives of such polymers
- C08L27/22—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by a halogen; Compositions of derivatives of such polymers modified by chemical after-treatment
- C08L27/24—Compositions of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and at least one being terminated by a halogen; Compositions of derivatives of such polymers modified by chemical after-treatment halogenated
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C45/00—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor
- B29C45/0001—Injection moulding, i.e. forcing the required volume of moulding material through a nozzle into a closed mould; Apparatus therefor characterised by the choice of material
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29K—INDEXING SCHEME ASSOCIATED WITH SUBCLASSES B29B, B29C OR B29D, RELATING TO MOULDING MATERIALS OR TO MATERIALS FOR MOULDS, REINFORCEMENTS, FILLERS OR PREFORMED PARTS, e.g. INSERTS
- B29K2027/00—Use of polyvinylhalogenides or derivatives thereof as moulding material
- B29K2027/06—PVC, i.e. polyvinylchloride
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29K—INDEXING SCHEME ASSOCIATED WITH SUBCLASSES B29B, B29C OR B29D, RELATING TO MOULDING MATERIALS OR TO MATERIALS FOR MOULDS, REINFORCEMENTS, FILLERS OR PREFORMED PARTS, e.g. INSERTS
- B29K2105/00—Condition, form or state of moulded material or of the material to be shaped
- B29K2105/0005—Condition, form or state of moulded material or of the material to be shaped containing compounding ingredients
- B29K2105/0044—Stabilisers, e.g. against oxydation, light or heat
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L2201/00—Properties
- C08L2201/08—Stabilised against heat, light or radiation or oxydation
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L2205/00—Polymer mixtures characterised by other features
- C08L2205/02—Polymer mixtures characterised by other features containing two or more polymers of the same C08L -group
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L2205/00—Polymer mixtures characterised by other features
- C08L2205/02—Polymer mixtures characterised by other features containing two or more polymers of the same C08L -group
- C08L2205/025—Polymer mixtures characterised by other features containing two or more polymers of the same C08L -group containing two or more polymers of the same hierarchy C08L, and differing only in parameters such as density, comonomer content, molecular weight, structure
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L2205/00—Polymer mixtures characterised by other features
- C08L2205/03—Polymer mixtures characterised by other features containing three or more polymers in a blend
- C08L2205/035—Polymer mixtures characterised by other features containing three or more polymers in a blend containing four or more polymers in a blend
Definitions
- the present invention is a resin composition for injection molding which can produce a molded article having excellent thermal stability and thermal fluidity and high water pressure resistance without using heavy metals such as lead and tin, and
- the present invention relates to a molded article using a resin composition for injection molding.
- the vinyl chloride resin composition is widely used, for example, as a material for resin moldings such as building materials.
- the vinyl chloride resin composition is required to have high thermal stability because it may be processed at a high temperature. Also, in order to obtain the thermal stability of the molded body, it is necessary to have high thermal stability.
- the vinyl chloride resin composition is also required to have color resistance, since the resin molded product used as a building material is regarded as important in color tone. In order to improve various performances, such as thermal stability and color resistance, to these requirements, it is general to add a heat stabilizer to vinyl chloride resin before melt molding.
- a heat stabilizer a heat stabilizer containing heavy metals such as lead, cadmium and barium is used.
- heavy metals such as lead, cadmium and barium
- heat stabilizers and resin molded articles that do not contain highly toxic metals such as lead have been proposed.
- a halogen-containing resin composition comprising a complex of a divalent metal such as Zn, Cu, etc., x and y in the range of 0 ⁇ x ⁇ 0.4, 0 ⁇ y ⁇ 0.1) ing.
- Patent Document 2 discloses a stabilizer composition containing a nitrogen-containing cyclic organic compound.
- a stabilizer composition containing a nitrogen-containing cyclic organic compound.
- chlorinated vinyl chloride resins obtained by chlorinating vinyl chloride resins are known.
- Chlorinated vinyl chloride resin is expected to improve heat resistance while retaining the flame retardancy and chemical resistance characteristics of vinyl chloride resin, but it is used for injection molded products such as joints and valve products.
- a drawback that it is difficult to develop a sufficiently satisfactory impact resistance and surface appearance.
- a method is disclosed in which a methyl methacrylate-butadiene-styrene copolymer, an acrylonitrile-butadiene-styrene copolymer or the like is added to a chlorinated vinyl chloride resin as an impact modifier.
- JP 2008-214466 A Japanese Patent Application Publication No. 2008-535997
- the present invention is a resin composition for injection molding which can produce a molded article having excellent thermal stability and thermal fluidity and high water pressure resistance without using heavy metals such as lead and tin, and
- An object of the present invention is to provide a molded article using a resin composition for injection molding.
- the present invention is a resin composition for injection molding comprising a chlorinated vinyl chloride resin, a vinyl chloride resin, and a heat stabilizer, wherein the heat stabilizer contains a calcium alkylcarboxylate and a zinc compound.
- the vinyl chloride resin has a polymerization degree of 400 to 1000, and is a resin composition for injection molding containing 1 to 30 parts by mass of the vinyl chloride resin with respect to 100 parts by mass of the chlorinated vinyl chloride resin. It is.
- the present invention will be described in detail below.
- the resin composition for injection molding of the present invention contains a chlorinated vinyl chloride resin (hereinafter also referred to as "CPVC").
- CPVC chlorinated vinyl chloride resin
- the above-mentioned chlorinated vinyl chloride resin is one in which the chlorine content is increased by chlorinating a vinyl chloride resin.
- the chlorinated vinyl chloride resin refers to a vinyl chloride resin having a chlorine content of 56.8% by mass or more.
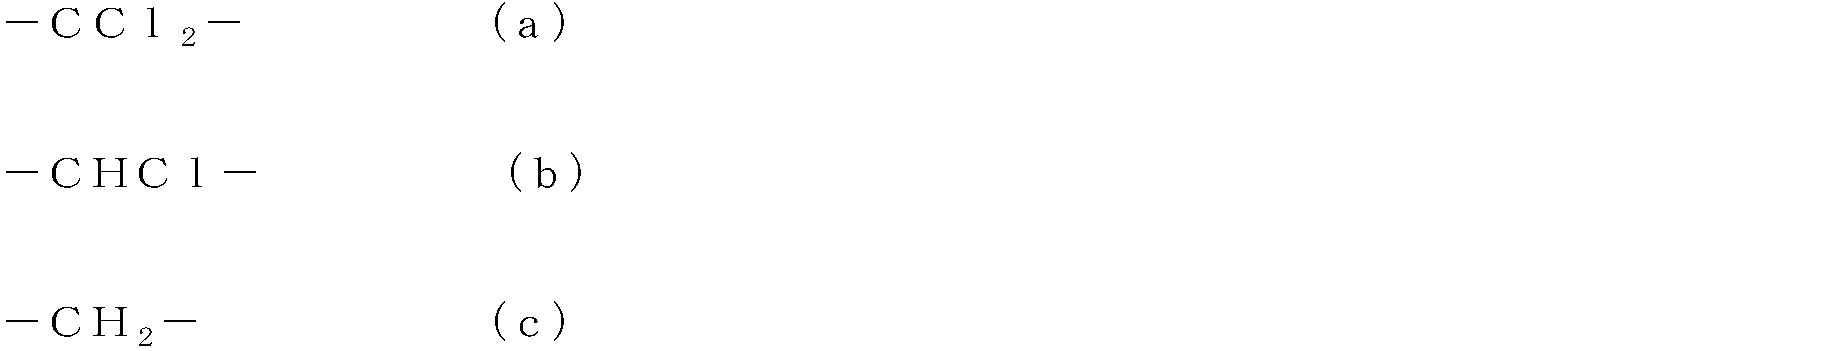
- the CPVC has structural units (a) to (c) represented by the following formulas (a) to (c), and the total mole number of the following structural units (a), (b) and (c) is It is preferable that the ratio of the structural unit (a) is 17.5 mol% or less, the ratio of the structural unit (b) is 46.0 mol% or more, and the ratio of the structural unit (c) is 37.0 mol% or less.
- Such CPVC has high thermal stability and good moldability.
- the molar ratio of the structural units (a), (b) and (c) of the CPVC reflects the site where chlorine is introduced when the vinyl chloride resin (PVC) is chlorinated.
- the PVC before chlorination is in a state where the structural unit (a) is approximately 0 mol%, the structural unit (b) is 50.0 mol%, and the structural unit (c) is 50.0 mol%.
- the structural unit (c) decreases with chlorination, and the structural unit (b) and the structural unit (a) increase.
- the ratio of the structural unit (a) is 17.5 mol% or less with respect to the total number of moles of the structural units (a), (b) and (c), but the structural unit (a)
- the ratio of is preferably 16.0 mol% or less. Moreover, it is preferable that it is 2.0 mol% or more.
- the ratio of the structural unit (b) is 46.0 mol% or more with respect to the total number of moles of the structural units (a), (b) and (c), but the ratio of the structural unit (b) Is preferably 53.5 mol% or more. Moreover, it is preferable that it is 70 mol% or less.
- the ratio of the structural unit (c) is 37.0 mol% or less based on the total number of moles of the structural units (a), (b) and (c), but the ratio of the structural unit (c) 30.5 mol% or less is preferable. Moreover, it is preferable that it is 1.0 mol% or more.
- the proportion of the structural unit (b) is preferably 58.0 mol% or more, and the proportion of the structural unit (c) is preferably 35.8 mol% or less.
- the proportion of the structural unit (c) is preferably 35.8 mol% or less.
- the molar ratio of the structural units (a), (b) and (c) of the above CPVC can be measured by molecular structure analysis using NMR.
- NMR analysis is as described by R.S. A. Komoroski, R .; G. Parker, J.J. P. It can be carried out according to the method described in Shocker, Macromolecules, 1985, 18, 1257-1265.
- the unchlorinated PVC part in the molecular structure of the above CPVC can be represented by the structural unit (d) shown in the following formula (d), which is herein referred to as a VC unit.
- a VC unit As for CPVC used by the present invention, it is preferred that content of VC unit of four or more telelinks contained in molecular structure is 30.0 mol% or less.
- a VC unit having four or more trains means a portion in which four or more VC units are continuously connected.
- the VC unit present in the above CPVC is the origin of de-HCl, and when the VC unit is continuous, a continuous de-HCl reaction called zipper reaction tends to occur. That is, as the amount of VC units of four or more ligatures increases, de-HCl tends to occur, and the thermal stability in CPVC decreases. Therefore, it is preferable that it is 30.0 mol% or less, and it is more preferable that it is 28.0 mol% or less.
- the VC unit of tetrad or more is preferably 18.0% by mol or less, more preferably 16.0% by mol or less .
- the content of vinyl chloride units having four or more bonds contained in the above molecular structure can be measured by the above molecular structure analysis using NMR.
- the above-mentioned CPVC preferably has a chlorine content of 63 to 72% by mass.
- a chlorine content of 63 to 72% by mass.
- the heat resistance as a molded article becomes sufficient, and by setting the content to 72% by mass or less, the formability is improved.
- the said chlorine content it is more preferable that it is 66 mass% or more, and it is more preferable that it is 69 mass% or less.
- the chlorine content in the above-mentioned CPVC can be measured by the method described in JIS K 7229.
- the polymerization degree of CPVC is not particularly limited, and is preferably 500 to 800. By setting the degree of polymerization within the above-mentioned range, it is possible to achieve both the flowability at the time of injection and the strength of the molded product.
- the CPVC preferably has a UV absorbance at a wavelength of 216 nm of 8.0 or less, more preferably 0.8 or less.
- the heterostructure in the molecular chain during the chlorination reaction can be quantified and used as an indicator of thermal stability.
- the chlorine atom attached to the carbon next to the double bonded carbon is unstable. Therefore, dechlorination occurs from the chlorine atom. That is, as the value of the UV absorbance at a wavelength of 216 nm is larger, de-HCl tends to occur, resulting in lower thermal stability.
- the value of the UV absorbance is preferably 0.8 or less.
- the value of UV absorbance exceeds 0.8, the influence of the heterostructure in the molecular chain becomes large, and as a result, the thermal stability may be reduced.
- the chlorine content of the said CPVC is 69 mass% or more and 72 mass% or less, it is preferable that the value of UV absorbance is 8.0 or less. When the value of the UV absorbance exceeds 8.0, the influence of the heterostructure in the molecular chain becomes large, and the thermal stability decreases.
- the time required for the amount of HCl removal at 190 ° C. to reach 7000 ppm is preferably 60 seconds or more, and more preferably 100 seconds or more.
- the above-mentioned CPVC is thermally decomposed at a high temperature and generates HCl gas.
- the degree of chlorination of CPVC increases, the amount of HCl removal tends to decrease because the above-described VC unit decreases.
- heterogeneous chlorination states and heterogeneous structures increase and thermal stability decreases. Therefore, by measuring the amount of HCl removal, it is possible to analyze the increase in heterogeneous chlorination state and heterostructure.
- the time required for the amount of HCl removal at 190 ° C. to reach 7000 ppm can be used as an indicator of thermal stability, and the shorter the time, the lower the thermal stability.
- the time required for the amount of HCl removal at 190 ° C. to reach 7000 ppm is 60 seconds or more. If the time is less than 60 seconds, the thermal stability is greatly impaired. Therefore, the time is preferably 60 seconds or more, more preferably 70 seconds or more, and still more preferably 80 seconds or more. Moreover, when the chlorine content of the said CPVC is 69 mass% or more and 72 mass% or less, it is preferable that this time is 100 seconds or more.
- the thermal stability is greatly reduced, so it is preferably 100 seconds or more, more preferably 120 seconds or more, and still more preferably 140 seconds or more.
- the time for the above-mentioned amount of HCl removal at 190 ° C. to reach 7000 ppm can be measured as follows. First, 1 g of chlorinated vinyl chloride resin is put into a test tube, and heated at 190 ° C. using an oil bath to recover generated HCl gas. The recovered HCl gas is dissolved in 100 ml of deionized water to measure pH. Based on the value of pH, the concentration of HCl (ppm) (ie how many HCl's evolved per million g of chlorinated vinyl chloride resin) is calculated. Measure the time for the concentration of HCl to reach 7000 ppm.
- ppm concentration of HCl
- the resin composition for injection molding of the present invention contains a vinyl chloride resin (hereinafter also referred to as "PVC").
- PVC vinyl chloride resin
- a vinyl chloride resin is a polymer mainly having a structural unit (d) represented by the above formula (d). Specifically, the proportion of the structural unit (d) is preferably 51 to 100 mol%.
- PVC polyvinyl chloride
- copolymer of vinyl chloride monomer and copolymer having unsaturated bond copolymerizable with vinyl chloride monomer graft copolymer obtained by graft copolymerizing vinyl chloride monomer to polymer A polymer etc.
- These polymers may be used alone or in combination of two or more.
- Examples of the monomer having an unsaturated bond copolymerizable with the vinyl chloride monomer include ⁇ -olefins, vinyl esters, vinyl ethers, (meth) acrylic esters, aromatic vinyls, vinyl halides, N-substituted maleimides etc. may be mentioned, and one or more of these may be used.
- Examples of the ⁇ -olefins include ethylene, propylene and butylene.
- the vinyl esters include vinyl acetate and vinyl propionate.
- Examples of the vinyl ethers include butyl vinyl ether and cetyl vinyl ether.
- examples of the (meth) acrylic esters include methyl (meth) acrylate, ethyl (meth) acrylate, butyl acrylate, phenyl methacrylate and the like, and examples of the aromatic vinyls include styrene, ⁇ -methylstyrene and the like Can be mentioned.
- examples of the vinyl halides include vinylidene chloride and vinylidene fluoride, and examples of the N-substituted maleimides include N-phenyl maleimide and N-cyclohexyl maleimide. Among them, ethylene and vinyl acetate are preferable.
- the polymer for graft copolymerization of vinyl chloride is not particularly limited as long as it graft-polymerizes vinyl chloride.
- a polymer for example, ethylene-vinyl acetate copolymer, ethylene-vinyl acetate-carbon monoxide copolymer, ethylene-ethyl acrylate copolymer, ethylene-butyl acrylate-carbon monoxide copolymer, Ethylene-methyl methacrylate copolymer, ethylene-propylene copolymer and the like can be mentioned.
- acrylonitrile-butadiene copolymer polyurethane, chlorinated polyethylene, chlorinated polypropylene and the like may be mentioned, and these may be used alone or two or more kinds may be used in combination.
- the polymerization method of the above-mentioned PVC is not particularly limited, and conventionally known water suspension polymerization, bulk polymerization, solution polymerization, emulsion polymerization and the like can be used.
- the above PVC has a chlorine content of less than 56.8% by mass.
- the average chlorine content of the chlorinated vinyl chloride resin and the vinyl chloride resin is preferably 65 to 68% by mass. By setting it as such a range, heat resistance and moldability can be ensured.
- the average chlorine content of the chlorinated vinyl chloride resin and the vinyl chloride resin is obtained by multiplying the chlorine content of the chlorinated vinyl chloride resin by the content ratio of the chlorine content of the vinyl chloride resin. After, it is a total.
- the polymerization degree of PVC is 400 to 1000. By setting it in the said range, it can be set as the product which satisfies both fluidity and product strength.
- the preferable lower limit of the polymerization degree of PVC is 500, and the preferable upper limit is 800.
- the difference in polymerization degree between the chlorinated vinyl chloride resin and the vinyl chloride resin is preferably 500 or less. By making the difference of the said polymerization degree into the above-mentioned range, it can be set as the product which satisfies both fluidity and product intensity. More preferably, it is 300 or less.
- the content of the vinyl chloride resin is preferably 1 part by mass with a preferable lower limit and 30 parts by mass with a preferable upper limit with respect to 100 parts by mass of the chlorinated vinyl chloride resin.
- a vinyl chloride resin in this range, the thermal stability can be further improved, and a good appearance of the molded article can be maintained.
- the more preferable lower limit of the content of the vinyl chloride resin is 5 parts by mass, and the more preferable upper limit is 20 parts by mass.
- the content of the vinyl chloride resin with respect to the entire resin composition for injection molding of the present invention is preferably 2 to 18% by mass.
- the heat stabilizer contains a calcium alkylcarboxylate and a zinc compound. Since the heat stabilizer does not contain heavy metals, heavy metal-free molding compositions can be obtained.
- the heat stabilizer contains a calcium alkylcarboxylate and a zinc compound. When such a heat stabilizer is used, hydrochloric acid generated by thermal decomposition of the chlorinated vinyl chloride resin immediately reacts with the zinc compound to form zinc chloride. In addition, the growth of polyene produced by dehydrochlorination of the chlorinated vinyl chloride resin is stopped by the binding with the calcium alkylcarboxylate, and the color development is suppressed.
- zinc chloride produced has the property of promoting thermal decomposition of chlorinated vinyl chloride resin, but in the present invention, zinc chloride reacts with calcium alkylcarboxylate to produce calcium chloride and zinc alkylcarboxylate. Be done.
- the above-mentioned heat stabilizer has a remarkable synergistic effect because the thermal decomposition promoting action of zinc chloride is suppressed while making use of the rapid hydrochloric acid scavenging action of the zinc compound.
- Examples of the calcium alkylcarboxylate include pentanoic acid, hexanoic acid, heptanoic acid, octanoic acid, cyclohexyl propionic acid, nonanoic acid, decanoic acid, lauric acid, myristic acid, palmitic acid, stearic acid, 12-hydroxystearic acid, And calcium salts such as arachidic acid, behenic acid, lignoceric acid and montanic acid. Among them, calcium alkyl carbonate having 8 to 28 carbon atoms is preferably used.
- an inorganic zinc compound or an organic zinc compound is mentioned.
- the inorganic zinc compound include compounds from the group consisting of zinc carbonate, chloride, sulfate, oxide, hydroxide, basic oxide, and mixed oxide.
- organozinc compounds examples include alkylzinc compounds such as di- and / or mono-alkylzinc, zinc organic aliphatic carboxylic acid, zinc unsubstituted or substituted organic aromatic carboxylic acid, zinc organic phosphorous acid, substituted or unsubstituted phenol Zinc, amino acids and their derivatives zinc, organic mercaptan zinc and the like can be mentioned.
- organic aliphatic carboxylic acids that constitute the above organic aliphatic carboxylic acid zinc include montanic acid, rice bran fatty acid, behenic acid, erucic acid, stearic acid, oleic acid, linoleic acid, rice fatty acid, licinoleic acid, myristic acid And palmitic acid, lauric acid, lower fatty acid, octylic acid, isostearic acid, dimer acid, naphthenic acid, acetic acid and the like.
- malic acid and its monoester, tartaric acid and its monoester, citric acid and its monoester or diester, lactic acid, glycolic acid, thiodipropionic acid and its monoester, etc. may be mentioned.
- Examples of the unsubstituted or substituted aromatic carboxylic acid constituting the above-mentioned unsubstituted or substituted zinc of organic aromatic carboxylic acid include benzoic acid, o-, m- and p-toluic acid, p-tert-butylbenzoic acid, Examples thereof include p-hydroxybenzoic acid, salicylic acid, phthalic acid of polybasic acid, metaphthalic acid, terephthalic acid, trimellitic acid and the like, and monoesters or diesters thereof.
- organic phosphorous acid constituting the organic zinc phosphite examples include acid phosphite which is a reaction product of an aliphatic alcohol and phosphorus pentoxide. Specifically, butyl acid phosphite, octyl acid phosphite, stearyl acid phosphite, behenyl acid phosphite and the like can be mentioned.
- Examples of the substituted or unsubstituted phenol constituting the above-mentioned substituted or unsubstituted phenol zinc include phenol, cresol, xylol, octylphenol, nonylphenol, dinonylphenol, cyclohexylphenol and phenylphenol. Further, examples of the substituted or unsubstituted phenol include bisphenol A, bisphenol S, bisphenol F, esters of p-hydroxybenzoic acid, esters of salicylic acid, and the like.
- amino acid and its derivative a baking glutamic acid, glycine, an alanine etc. can be mentioned, for example.
- organic mercaptan constituting the organic mercaptan zinc examples include lauryl mercaptan, thioglycolic acid and esters thereof, mercaptopropionic acid and esters thereof, thiomalic acid and monoesters or diesters thereof.
- the heat stabilizer contains a calcium alkylcarboxylate and a zinc compound, and is preferably a mixture of the calcium alkylcarboxylate and the zinc compound.
- a form of the said heat stabilizer a powder, a granular material, etc. are mentioned, for example. Such a form can be used as a one-pack heat stabilizer.
- the heat stabilizer is in the form of powder, its particle size can be arbitrarily adjusted according to the purpose, and in general, the average particle size is preferably 50 ⁇ m to 5 mm, particularly preferably 70 ⁇ m to 2 mm .
- Examples of the method for producing a heat stabilizer for the above-mentioned granular material include, for example, extrusion granulation method, spray granulation method, rotary disk granulation method, rolling granulation method, compression granulation method, etc.
- the grain method can be used.
- the heat stabilizer preferably has a heating loss at 230 ° C. of less than 5% by mass. If the heat loss rate at 230 ° C. is 5% by mass or more, bubbles may be contained in the inside of the molded article, resulting in insufficient strength or occurrence of streaks in the vicinity of the surface to cause appearance defects. is there.
- the heat loss at 230 ° C. is more preferably less than 3% by mass. The lower limit is not particularly limited, but 0.1% by mass is preferable.
- the rate of loss on heating at 230 ° C. can be measured by a thermogravimetry (TG) device.
- the heat stabilizer contains a calcium alkylcarboxylate and a zinc compound, but the mixing ratio of the calcium alkylcarboxylate and the zinc compound (calcium calcium carboxylate: zinc compound) is 9: 1 to 4 : 6 is preferable. Further, the mixing ratio is more preferably 8: 2 to 5: 5.
- the content of the heat stabilizer is preferably 0.4 to 20 parts by mass, and more preferably 1 to 10 parts by mass with respect to 100 parts by mass of the chlorinated vinyl chloride resin. More preferably, it is in the range of parts. By including the heat stabilizer in this range, the thermal stability can be further improved, and the good appearance of the molded article can be maintained.
- a heavy metal-free resin composition for injection molding can be obtained by using the above-mentioned heat stabilizer.
- heavy metal means metal having high density and generally refers to metal having density of 4 to 5 g / cm 3 or more.
- Heavy metal free means that the content of heavy metal is 1000 ppm or less. In addition, it is preferable that content of the said heavy metal is 100 ppm or less.
- transition metals other than scandium For example, Mn, Ni, Fe, Cr, Co, Cu, Au etc. are mentioned.
- metals of p-block elements of the fourth period or less for example, Sn, Pb, Bi), Cd, Hg and the like are also included.
- the resin composition for injection molding of the present invention preferably further contains an antioxidant.
- an antioxidant a phenolic antioxidant, phosphoric acid type antioxidant, sulfur type antioxidant, an amine type antioxidant etc. can be used, for example. These may be used alone or in combination of two or more. Among them, phenolic antioxidants are preferable, and hindered phenolic antioxidants are particularly preferable.
- hindered phenol-based antioxidants examples include 2,6-di-t-butyl-p-cresol, 2,6-diphenyl-4-octadecyloxyphenol, stearyl (3,5-t-butyl- 4-hydroxyphenyl) propionate, distearyl (3,5-t-butyl-4-hydroxybenzyl) phosphonate, 2,2'-methylenebis (4-methyl-6-t-butylphenol), 2,2'-methylenebis ( 4-ethyl-6-t-butylphenol), bis [3,3-bis (4-hydroxy-3-t-butylphenyl) butyric acid] glycol ester, 4,4′-butylidene bis (6-t-butyl- m-cresol), 2,2′-ethylidene bis (4,6-di-t-butylphenol), 2,2′-ethylidene bis -Sec-butyl-6-tert-butylphenol), 1,1,3-trimeth
- 1,3,5-tris (3,5-di-t-butyl-4-hydroxybenzyl) isocyanurate, pentaerythrityl-tetrakis [methylene-3- (3,5-di-t-) Butyl 4-hydroxyphenyl) propionate] and the like are preferable. These may be used alone or in combination of two or more.
- the antioxidant preferably has a heating loss at 200 ° C. of less than 5% by mass. If the heat loss rate at 200 ° C. is 5% by mass or more, bubbles may be contained inside the molded product to cause insufficient strength, or streaky patterns may be generated in the vicinity of the surface to cause appearance defects. .
- the heating loss at 200 ° C. is more preferably less than 3% by mass.
- the content of the antioxidant is preferably 0.1 to 3 parts by mass with respect to 100 parts by mass of the chlorinated vinyl chloride resin, and 0.2 More preferably, it is in the range of -2.5 parts by mass. By including an antioxidant in this range, it is possible to obtain a molded article with little coloration due to yellowing.
- the resin composition for injection molding of the present invention preferably further contains a stabilization aid.
- the thermal stability can be further improved by including the above-mentioned stabilizing aid.
- the above-mentioned stabilizing assistant those not containing heavy metals can be used.
- organic acid salts epoxidized soybean oil, epoxidized linseed oil epoxidized tetrahydrophthalate, epoxy compounds such as epoxidized polybutadiene, organophosphorus compounds, phosphites, phosphates, calcium hydroxide, sodium hydroxide, etc.
- stabilization adjuvant sodium adipate, a bisphenol A type epoxy compound, a glycidyl (meth) acrylate copolymer, an oxetanyl compound, a vinyl ether compound, and a zeolite compound are mentioned as said stabilization adjuvant. These may be used alone or in combination of two or more.
- the above-mentioned stabilizing assistant is different from calcium alkylcarboxylate and zinc compound.
- the heat-loss-loss rate in 200 degreeC of the said stabilization adjuvant is less than 5 mass%.
- the resin composition for injection molding of the present invention may be added with a lubricant, a processing aid, an impact modifier, a heat resistance improver, an ultraviolet absorber, a light stabilizer, a filler, a thermoplastic elastomer, a pigment, etc., as necessary.
- the agents may be mixed.
- the lubricant examples include internal lubricants and external lubricants.
- the internal lubricant is used for the purpose of lowering the flow viscosity of the molten resin at the time of molding processing and preventing frictional heat generation.
- the internal lubricant is not particularly limited, and examples thereof include butyl stearate, lauryl alcohol, stearyl alcohol, glycerin monostearate, stearic acid, bisamide and the like. These may be used alone or in combination of two or more.
- the lubricant preferably has a heating loss at 200 ° C. of less than 5% by mass.
- the external lubricant is used for the purpose of enhancing the sliding effect between the molten resin and the metal surface during molding.
- the external lubricant is not particularly limited, and examples thereof include paraffin wax, polyolefin wax such as polyethylene lubricant, ester wax such as fatty acid ester lubricant, and montanic acid wax. These may be used alone or in combination of two or more.
- the processing aid is not particularly limited, and examples thereof include acrylic processing aids such as alkyl acrylate-alkyl methacrylate copolymers having a weight average molecular weight of 100,000 to 2,000,000.
- the above-mentioned acrylic processing aid is not particularly limited, and examples thereof include n-butyl acrylate-methyl methacrylate copolymer, 2-ethylhexyl acrylate-methyl methacrylate-butyl methacrylate copolymer and the like. These may be used alone or in combination of two or more.
- the processing aid preferably has a heating loss at 200 ° C. of less than 5% by mass.
- the impact modifier is not particularly limited, and examples thereof include methyl methacrylate-butadiene-styrene copolymer (MBS), chlorinated polyethylene, acrylic rubber and the like.
- MFS methyl methacrylate-butadiene-styrene copolymer
- the heat resistance improver is not particularly limited, and examples thereof include ⁇ -methylstyrene resins and N-phenylmaleimide resins.
- the light stabilizer is not particularly limited, and examples thereof include light stabilizers such as hindered amines.
- the ultraviolet absorber is not particularly limited, and examples thereof include ultraviolet absorbers such as salicylic acid ester type, benzophenone type, benzotriazole type and cyanoacrylate type.
- the pigment is not particularly limited, and, for example, organic pigments such as azo, phthalocyanine, srene, dye lake, and the like; oxides such as titanium dioxide, inorganics such as sulfide / selenide, and ferrocyanide Pigment etc. are mentioned.
- a plasticizer may be added to the resin composition for injection molding of the present invention for the purpose of improving the processability at the time of molding, but since the heat stability of the molded body may be reduced, it is used in large amounts. It is not desirable to do so.
- the plasticizer is not particularly limited, and examples thereof include dibutyl phthalate, di-2-ethylhexyl phthalate and di-2-ethylhexyl adipate.
- thermoplastic elastomer may be added to the resin composition for injection molding of the present invention for the purpose of improving the workability.
- the thermoplastic elastomer is not particularly limited.
- an acrylonitrile-butadiene copolymer (NBR) an ethylene-vinyl acetate copolymer (EVA), an ethylene-vinyl acetate-carbon monoxide copolymer (EVACO) And copolymers of the like.
- thermoplastic elastomers examples include vinyl chloride-based thermoplastic elastomers, styrene-based thermoplastic elastomers, olefin-based thermoplastic elastomers, urethane-based thermoplastic elastomers, polyester-based thermoplastic elastomers, and polyamide-based thermoplastic elastomers.
- vinyl chloride-based thermoplastic elastomer examples include vinyl chloride-vinyl acetate copolymer, vinyl chloride-vinylidene chloride copolymer and the like. These thermoplastic elastomers may be used alone or in combination of two or more.
- the resin composition for injection molding of the present invention preferably contains no ⁇ -diketone.
- ⁇ -diketones are components that are incorporated into conventional thermal stabilizers to improve thermal stability.
- the appearance of the molded product tends to be impaired. For example, yellow to reddish brown streaks of about 0.1 to 1 mm in thickness parallel to the flow direction of the resin are generated on the surface of the molded body.
- the molded object in which the appearance was impaired turns into inferior goods. Such a defect is likely to occur particularly when a die used for a long time is used.
- a resin composition for injection molding having excellent heat stability can be provided without using a heat stabilizer containing ⁇ -diketone.
- the resin composition for injection molding of the present invention preferably has a heat loss rate at 230 ° C. of less than 2.0% by mass. If the heat loss rate at 230 ° C. is 2.0% by mass or more, bubbles may be contained in the inside of the molded article, resulting in insufficient strength, or streaky patterns in the vicinity of the surface to cause appearance defects. .
- the heat loss at 230 ° C. is more preferably less than 1.0% by mass.
- the lower limit is not particularly limited, but 0.1% by mass is preferable.
- the rate of loss on heating at 230 ° C. can be measured by a thermogravimetry (TG) device.
- a suspension is prepared by suspending the vinyl chloride resin in an aqueous medium in a reaction vessel, and chlorine is introduced into the reaction vessel, A method of chlorinating the above-mentioned vinyl chloride resin by any method can be used.
- a part of the chlorinated vinyl chloride resin may be chlorinated to make the chlorinated vinyl chloride resin and the vinyl chloride resin coexist.
- a reaction container to be used for example, a commonly used container such as a stainless steel reaction container with glass lining or a titanium reaction container can be used. .
- the method for preparing the suspension by suspending the above vinyl chloride resin in an aqueous medium is not particularly limited, and it may be a cake-like PVC obtained by demonomerizing PVC after polymerization, or dried May be suspended again in an aqueous medium, or a suspension from which substances undesirable for the chlorination reaction have been removed may be used from the polymerization system. Among them, it is preferable to use a cake-like resin obtained by demonomerizing PVC after polymerization.
- aqueous medium for example, ion-exchanged pure water can be used.
- the amount of the aqueous medium is not particularly limited, but in general, 150 to 400 parts by mass is preferable with respect to 100 parts by mass of PVC.
- the chlorine introduced into the reaction vessel may be either liquid chlorine or gaseous chlorine.
- Chlorine may be added during the reaction to adjust pressure or to replenish chlorine.
- gaseous chlorine may be appropriately blown in addition to liquid chlorine. It is preferable to use chlorine after purging 5 to 10% by mass of cylinder chlorine.
- the gauge pressure in the reaction vessel is not particularly limited, but is preferably in the range of 0.3 to 2 MPa because chlorine is more likely to penetrate into the PVC particles as the chlorine pressure is higher.
- the method for chlorinating PVC in the suspended state is not particularly limited.
- a method of promoting chlorination by exciting PVC bond or chlorine by thermal energy hereinafter referred to as thermal chlorination), ultraviolet light And the like (hereinafter referred to as “photochlorination”), etc., in which chlorination is promoted photoreactively by irradiating light energy such as, for example.
- the heating method in the case of chlorination by thermal energy is not particularly limited, and, for example, heating by the outer jacket system from the reactor wall is effective.
- light energy such as an ultraviolet ray
- the apparatus which can be irradiated with light energy, such as ultraviolet irradiation under the conditions of high temperature and high pressure, is required.
- the chlorination reaction temperature in the case of photochlorination is preferably 40 to 80.degree.
- a thermal chlorination method which does not perform ultraviolet irradiation is preferable, and a method of exciting a bond or chlorine of a vinyl chloride resin with heat alone or heat and hydrogen peroxide to promote chlorination reaction is preferable.
- the magnitude of the light energy required to chlorinate the PVC is greatly influenced by the distance between the PVC and the light source. Therefore, the amount of energy received differs between the surface and the inside of the PVC particles, and chlorination does not occur uniformly. As a result, CPVC with low uniformity is obtained.
- the method of performing chlorination by heat without performing ultraviolet irradiation more uniform chlorination reaction becomes possible, and CPVC with high uniformity can be obtained.
- the temperature is preferably in the range of 70 to 140.degree. If the temperature is too low, the chlorination rate is reduced. When the temperature is too high, a deHCl reaction occurs in parallel with the chlorination reaction, and the obtained CPVC is colored.
- the heating temperature is more preferably in the range of 100 to 135.degree.
- the heating method is not particularly limited, and for example, it can be heated from the reaction vessel wall by the outer jacket method.
- the rate of chlorination can be improved by the addition of hydrogen peroxide.
- Hydrogen peroxide is preferably added in an amount of 5 to 500 ppm, based on PVC, per hour of reaction time. If the amount added is too small, the effect of improving the rate of chlorination can not be obtained. If the amount is too large, the thermal stability of CPVC will be reduced.
- the heating temperature can be relatively lowered because the chlorination rate is improved. For example, it may be in the range of 65 to 110.degree.
- chlorination after reaching a point 5 mass% before the final chlorine content is carried out in a chlorine consumption rate in the range of 0.010 to 0.015 kg / PVC-Kg ⁇ 5 min, It is preferable to carry out chlorination after reaching the point of 3% by mass from the final chlorine content, in a chlorine consumption rate in the range of 0.005 to 0.010 kg / PVC-Kg ⁇ 5 min.
- the chlorine consumption rate refers to chlorine consumption for 5 minutes per kg of the raw material PVC.
- a vinyl chloride resin, a heat stabilizer, and, if necessary, an antioxidant are added to and mixed with the above-mentioned chlorinated vinyl chloride resin. Perform the process. It does not specifically limit as method to mix the said heat stabilizer and antioxidant, For example, the method by hot blending, the method by cold blending, etc. are mentioned.
- a resin composition for injection molding which has excellent thermal stability and does not contain heavy metals such as lead, cadmium and tin.
- a molded article molded from the resin composition for injection molding of the present invention is also one of the present invention.
- a method of the above-mentioned injection molding a conventionally known arbitrary molding method may be adopted.
- a general injection molding method for example, a general injection molding method, an injection foam molding method, a supercritical injection foam molding method, an ultra high speed injection molding method, an injection compression Methods such as molding method, gas assist injection molding method, sandwich molding method, sandwich foam molding method, insert / outsert molding method and the like can be mentioned.
- the molded article of the present invention is free of heavy metals like the resin composition for injection molding of the present invention, it has an excellent advantage of not adversely affecting the environment, and has excellent thermal stability, and Since the appearance state is good, it can be suitably used for applications such as building materials, pipework equipment, and housing materials.
- a resin composition for injection molding capable of producing a molded article having excellent thermal stability and thermal fluidity and high water pressure resistance without using heavy metals such as lead and tin.
- the molded object using the resin composition for injection molding can be provided.
- by reducing the occurrence of weld lines appearance defects and strength reduction due to stress concentration can be prevented.
- Example 1 (Preparation of chlorinated vinyl chloride resin) 200 kg of ion-exchanged water and 56 kg of vinyl chloride resin having an average degree of polymerization of 700 were charged into a glass-lined reaction container having an inner volume of 300 L. The mixture was stirred and more water was added to the reaction vessel to disperse the mixture in water. Then, the pressure was reduced to remove oxygen in the reaction vessel, and the temperature was raised to 90.degree. Next, chlorine is supplied into the reaction vessel so that the chlorine partial pressure is 0.4 MPa, and 0.2 mass% hydrogen peroxide is added at a rate of 1 mass part per hour (320 ppm / hour) , Chlorination reaction.
- pentaerythrityl-tetrakis [3- (3,5-di-t-butyl-4-hydroxyphenyl) propionate] hindered phenolic antioxidant, Irganox 1010, manufactured by BASF AG
- a heating loss ratio of 200 ° C. (1.0% by mass) were used.
- the obtained resin composition for injection molding was supplied to a biaxial 30-mm-diameter twin-screw counter-directional conical extruder (“OSC-30” manufactured by Nagata Mfg. Co., Ltd.) to prepare pellets at a resin temperature of 190 ° C.
- the obtained pellet was supplied to an injection molding machine ("J100E-C5" manufactured by Nisshin Steel Co., Ltd.), and a socket-like injection-molded article having a nominal diameter of 25 mm was produced at a resin temperature of 230 ° C when purged from a nozzle.
- Example 2 A resin composition for injection molding and an injection molded article were produced in the same manner as in Example 1 except that the addition amount of the vinyl chloride resin was changed to 3 parts by mass.
- Example 3 A resin composition for injection molding and an injection molded article were produced in the same manner as in Example 1 except that the addition amount of the vinyl chloride resin was changed to 25 parts by mass.
- Example 4 Chlorinated vinyl chloride resin, resin composition for injection molding and extrusion molding in the same manner as in Example 1 except that the vinyl chloride resin was changed to a vinyl chloride resin (chlorine content: 56.7 mass%, degree of polymerization: 1000) The body was made.
- Example 5 A resin composition for injection molding and an injection molded article were produced in the same manner as in Example 1 except that the amount of the vinyl chloride resin added was changed to 18 parts by mass.
- Example 6 A resin composition for injection molding and an extrusion-molded product were prepared in the same manner as in Example 1 except that the chlorinated vinyl chloride resin was changed to a chlorinated vinyl chloride resin (chlorine content: 67.3 mass%, degree of polymerization: 600). Made.
- Example 7 A resin composition for injection molding and an extrusion-molded product were prepared in the same manner as in Example 1 except that the chlorinated vinyl chloride resin was changed to a chlorinated vinyl chloride resin (chlorine content: 67.3 mass%, degree of polymerization: 500). Made.
- Example 8 Chlorinated vinyl chloride resin, resin composition for injection molding and extrusion molding in the same manner as in Example 1 except that the vinyl chloride resin was changed to a vinyl chloride resin (chlorine content: 56.7 mass%, degree of polymerization: 500) The body was made.
- Comparative Example 1 The resin composition for injection molding and extrusion were the same as in Example 1 except that the vinyl chloride resin was not added and the heat stabilizer was changed to 2.0 parts by mass of calcium montanate and 2.0 parts by mass of zinc laurate. A molded body was produced.
- Comparative Example 2 A resin composition for injection molding and an injection molded article were produced in the same manner as in Example 1 except that the addition amount of the vinyl chloride resin was changed to 35 parts by mass.
- Comparative Example 3 The type and amount of vinyl chloride resin were changed to 7 parts by mass of vinyl chloride resin (chlorine content: 56.7 mass%, degree of polymerization: 1300), and the other components to be added were changed to those described in Table 1.
- a resin composition for injection molding and an extrusion molded article were produced in the same manner as in Example 1 except for the above.
- Comparative Example 4 A resin composition for injection molding and an extrusion-molded product in the same manner as in Example 1 except that the addition amount of the vinyl chloride resin was changed to 0.5 parts by mass, and the components to be added were changed to those described in Table 1. Was produced.
- the obtained chlorinated vinyl chloride resin composition was supplied to two 8-inch rolls, and was kneaded at 205 ° C. for 3 minutes to prepare a 1.0 mm-thick sheet.
- the obtained sheets were stacked, preheated for 3 minutes with a press at 205 ° C., and then pressed for 4 minutes to obtain a press plate with a thickness of 3 mm.
- the test piece was cut out by machining from the obtained press board. Using this test piece, tensile strength and tensile modulus were measured in accordance with ASTM D638. Further, the heat distortion temperature was measured under a load of 186 N / cm 2 in accordance with ASTM D648. The heat distortion temperature was measured after annealing the obtained press plate in a 90 ° C. gear oven for 24 hours.
- Flow evaluation was performed using Shimadzu flow tester (CFT-500D / 100D, manufactured by Shimadzu Corporation). Specifically, a roll sheet produced by ⁇ mechanical properties (tensile strength, heat deformation temperature)> is cut into about 5 mm square, supplied to a barrel heated to 210 ° C., die diameter 1 mm, die length 10 mm capillary And extruded with a load of 205 kgf. After that, measurement was started when the molten resin came out of the 3 mm capillary, and it was measured how many seconds it took per 1 mm. The case where a measured value is 0.2 mm / sec or more was considered as "pass", and the case less than 0.2 mm / sec was evaluated as "fail”.
- a resin composition for injection molding capable of producing a molded article having excellent thermal stability and thermal fluidity and high water pressure resistance without using heavy metals such as lead and tin. And the molded object using the resin composition for injection molding can be provided.
Landscapes
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Compositions Of Macromolecular Compounds (AREA)
- Injection Moulding Of Plastics Or The Like (AREA)
Abstract
Description
これらの要求に対して、熱安定性や耐着色性等の種々の性能を向上させるため、塩化ビニル系樹脂には、溶融成形の前に熱安定剤が添加されることが一般的である。
例えば、特許文献1には、含ハロゲン樹脂に酸性白土及び/又は活性白土と、Ca1-x-yM2+ xAly(OH)2で表される水酸化カルシウム系化合物(M2+はMg,Zn,Cu等の2価金属、x及びyは、0≦x<0.4,0≦y<0.1の範囲にある)との複合物を含有する含ハロゲン樹脂組成物が開示されている。
しかしながら、このような安定剤組成物でも、成形品が着色し易く、着色を防止するため、高価な顔料や酸化チタンを多く添加しなければならないという問題点があった。
これらの重金属を含まない熱安定剤を用いた射出成形用樹脂組成物や成形体に対して、さらなる性能の改善が望まれていた。
塩素化塩化ビニル系樹脂には、塩化ビニル系樹脂の難燃性、耐薬品性の特性を残しつつ、耐熱性を改良することが期待されているが、継手、バルブ製品等の射出成形品用途において、充分に満足し得る程度の耐衝撃性や表面外観性が発現しにくいという欠点がある。
このため、塩素化塩化ビニル系樹脂にメタクリル酸メチル-ブタジエン-スチレン共重合体や、アクリロニトリル-ブタジエン-スチレン共重合体等を耐衝撃強化剤として添加する方法が開示されている。
しかしながら、塩素化塩化ビニル樹脂にこれら強化剤を配合する場合、射出成形時の流動性が低下し、製造条件面での問題が生じていた。
また、流動性の改善を目的として、可塑剤等を用いる方法が行われているが、この方法では、得られる成形体の耐水圧の低下を招くといった課題があった。
以下に本発明を詳述する。
しかしながら、このような熱安定剤を使用する場合でも、熱安定性が依然として低いという欠点があった。特に、射出成形に使用する場合は、より高度な熱安定性が必要とされていた。
本発明者らは、鋭意検討の結果、射出成形用樹脂組成物に使用する樹脂として、塩素化塩化ビニル系樹脂に加えて、重合度が規定範囲内の塩化ビニル系樹脂を所定量添加することで、鉛、スズ等の重金属を使用せずに、優れた熱安定性、熱流動性を有し、耐水圧が高い成形体を製造することが可能となることを見出し、本発明を完成させるに至った。
上記塩素化塩化ビニル系樹脂とは、塩化ビニル系樹脂を塩素化することによって塩素の含有率を高くしたものである。なお、塩素化塩化ビニル系樹脂とは、塩素含有量が56.8質量%以上の塩化ビニル系樹脂をいう。
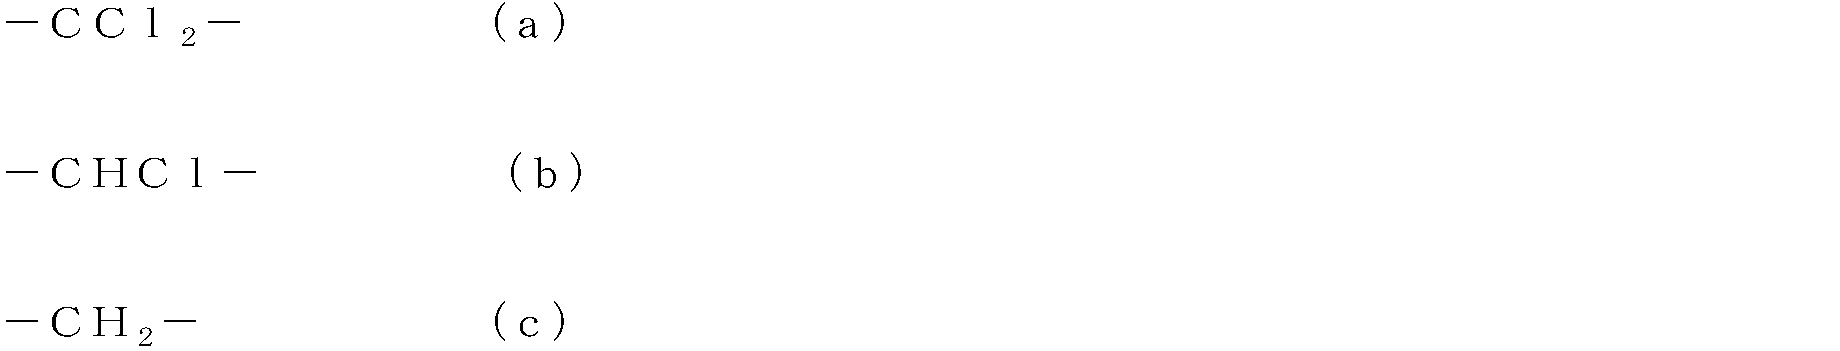
一方で、本発明では、上記CPVCの構成単位(a)、(b)及び(c)のモル比を上述の範囲内とすることで、CPVCの均一性が高くなり、良好な熱安定性を有する。
また、上記構成単位(a)、(b)及び(c)の合計モル数に対して、構成単位(b)の割合が46.0モル%以上であるが、上記構成単位(b)の割合は、53.5モル%以上が好ましい。また、70モル%以下であることが好ましい。
更に、上記構成単位(a)、(b)及び(c)の合計モル数に対して、構成単位(c)の割合が37.0モル%以下であるが、上記構成単位(c)の割合は、30.5モル%以下が好ましい。また、1.0モル%以上であることが好ましい。
本発明で用いるCPVCは、分子構造中に含まれる4連子以上のVC単位の含有量が30.0モル%以下であることが好ましい。ここで、4連子以上のVC単位とは、VC単位が4個以上連続して結合している部分を意味する。

上記分子構造中に含まれる4連子以上の塩化ビニル単位の含有率は、上記のNMRを用いた分子構造解析により測定することができる。
上記塩素含有量を63質量%以上とすることで、成形品としての耐熱性が充分なものとなり、72質量%以下とすることで、成形性が向上する。
上記塩素含有量は、66質量%以上であることがより好ましく、69質量%以下であることがより好ましい。
上記CPVC中の塩素含有量は、JIS K 7229に記載の方法により測定することができる。
上記重合度を上述の範囲内とすることで、射出時の流動性と成型品の強度を両立することができる。
また、紫外吸収スペクトルにおいて、216nmの波長は、CPVC中の異種構造である、-CH=CH-C(=O)-及び-CH=CH-CH=CH-が吸収を示す波長である。
上記CPVCのUV吸光度の値から、塩素化反応時の分子鎖中の異種構造を定量化し、熱安定性の指標とすることができる。CPVCの分子構造において、二重結合した炭素の隣の炭素に付いた塩素原子は不安定である。そのため、該塩素原子を起点として、脱HClが生じる。即ち、波長216nmにおけるUV吸光度の値が大きいほど脱HClが起こり易く、熱安定性が低いことになる。
また、上記CPVCの塩素含有量が69質量%以上、72質量%以下である場合は、UV吸光度の値が8.0以下であることが好ましい。上記UV吸光度の値が8.0を超えると、分子鎖中の異種構造の影響が大きくなり、熱安定性が低下する。
上記CPVCは高温で熱分解を起こし、その際にHClガスを発生する。一般に、CPVCはその塩素化度が高くなるにつれて、上述したVC単位が減少するため、脱HCl量が減少する傾向にある。しかし、塩素化度が高くなるにつれて、不均一な塩素化状態や異種構造が増加し、熱安定性が低下する。それ故、脱HCl量を測定することにより、不均一な塩素化状態や異種構造の増加を分析することができる。例えば、190℃における脱HCl量が7000ppmに到達するのに必要な時間を熱安定性の指標とすることができ、その時間が短いほど、熱安定性が低いと言える。
また、上記CPVCの塩素含有量が69質量%以上、72質量%以下である場合は、該時間は100秒以上であることが好ましい。該時間が100秒未満であると、熱安定性が大きく低下してしまうため、100秒以上であることが好ましく、120秒以上であることがより好ましく、140秒以上であることが更に好ましい。
上記190℃における脱HCl量が7000ppmに到達する時間は、以下のように測定することができる。まず、塩素化塩化ビニル樹脂1gを試験管に入れ、オイルバスを使用して190℃で加熱し、発生したHClガスを回収する。回収したHClガスを100mlのイオン交換水に溶解させてpHを測定する。pHの値に基づいて、HClの濃度(ppm)(即ち、塩素化塩化ビニル樹脂100万gあたり何gのHClが発生したか)を算出する。HClの濃度が7000ppmに到達する時間を計測する。
上記塩化ビニル系樹脂を塩素化塩化ビニル系樹脂と併用することで、アルキルカルボン酸カルシウム及び亜鉛化合物を熱安定剤として用いた場合に、充分な熱安定性を付与することができ、射出成形においても好適に使用することができる。
本発明において、塩化ビニル系樹脂とは、上記式(d)に示す構成単位(d)を主に有する重合体である。具体的には、構成単位(d)の割合が51~100モル%であることが好ましい。
上記α-オレフィン類としては、エチレン、プロピレン、ブチレン等が挙げられ、上記ビニルエステル類としては、酢酸ビニル、プロピオン酸ビニル等が挙げられ、上記ビニルエーテル類としては、ブチルビニルエーテル、セチルビニルエーテル等が挙げられる。
また、上記(メタ)アクリル酸エステル類としては、メチル(メタ)アクリレート、エチル(メタ)アクリレート、ブチルアクリレート、フェニルメタクリレート等が挙げられ、上記芳香族ビニル類としては、スチレン、α-メチルスチレン等が挙げられる。
更に、上記ハロゲン化ビニル類としては、塩化ビニリデン、フッ化ビニリデン等が挙げられ、上記N-置換マレイミド類としては、N-フェニルマレイミド、N-シクロヘキシルマレイミド等が挙げられる。
なかでも、エチレン、酢酸ビニルが好ましい。
上記PVCの重合方法は、特に限定されず、従来公知の水懸濁重合、塊状重合、溶液重合、乳化重合等を用いることができる。
上記塩素含有量を上記範囲内とすることで、成形性が向上するとともに、成形品としての耐熱性が高くなる。好ましくは36.8~56.7質量%である。
また、塩素化塩化ビニル系樹脂と塩化ビニル系樹脂の平均塩素含有量は65~68質量%であることが好ましい。このような範囲とすることで、耐熱性と成形性を確保することができる。
なお、塩素化塩化ビニル系樹脂と塩化ビニル系樹脂の平均塩素含有量とは、塩素化塩化ビニル系樹脂の塩素含有量と、塩化ビニル系樹脂の塩素含有量のそれぞれに、含有比率を掛けた後、合計したものである。
上記塩化ビニル系樹脂の含有量のより好ましい下限は5質量部、より好ましい上限は20質量部である。
また、本発明の射出成形用樹脂組成物全体に対する上記塩化ビニル系樹脂の含有量は、2~18質量%であることが好ましい。
上記熱安定剤は、アルキルカルボン酸カルシウム及び亜鉛化合物を含有する。
このような熱安定剤を用いた場合、塩素化塩化ビニル系樹脂の熱分解で生成した塩酸が、直ちに亜鉛化合物と反応して塩化亜鉛となる。また、塩素化塩化ビニル系樹脂の脱塩酸により生成したポリエンの成長がアルキルカルボン酸カルシウムとの結合で停止されて発色が抑えられる。
一方で、生成した塩化亜鉛は、塩素化塩化ビニル系樹脂の熱分解を促進させる性質があるが、本発明では、塩化亜鉛がアルキルカルボン酸カルシウムと反応して塩化カルシウムとアルキルカルボン酸亜鉛が生成される。その結果、上記熱安定剤は、亜鉛化合物の迅速な塩酸捕捉作用を生かしながら、塩化亜鉛の熱分解促進作用が抑制されるため、顕著な相乗効果を有する。
なかでも、炭素数8~28のアルキルカルボン酸カルシウムを用いることが好ましい。
上記無機亜鉛化合物としては、例えば、亜鉛の炭酸塩、塩化物、硫酸塩、酸化物、水酸化物、塩基性酸化物及び混合酸化物からなる系統からの化合物等が挙げられる。
上記熱安定剤の形態としては、例えば、粉末、粒状物等が挙げられる。このような形態とすることで、ワンパックの熱安定剤として使用することができる。
上記熱安定剤が粉粒体である場合、その粒度は目的に応じて任意に調節することができ、一般に平均粒子径が50μm~5mmであることが好ましく、特に70μm~2mmであることが好ましい。
上記粒状物の熱安定剤を製造する方法としては、例えば、押出成形造粒法、噴霧造粒法、回転円盤造粒法、転動造粒法、圧縮造粒法等のそれ自体公知の造粒法を用いることができる。
上記230℃における加熱減量率が5質量%以上であると、成形品内部に気泡が含まれることで強度不足になったり、表面近傍に筋状の模様が発生し外観不良が生じたりすることがある。
上記230℃における加熱減量率は、3質量%未満であることがより好ましい。
下限については特に限定されないが0.1質量%が好ましい。
なお、上記230℃における加熱減量率は、熱重量測定(TG)装置によって測定することができる。
上記酸化防止剤としては、例えば、フェノール系酸化防止剤、リン酸系酸化防止剤、イオウ系酸化防止剤、アミン系酸化防止剤等を用いることができる。これらは、単独で使用しても良く、二種以上を併用しても良い。なかでも、フェノール系酸化防止剤が好ましく、特にヒンダードフェノール系酸化防止剤が好ましい。
上記200℃における加熱減量率が5質量%以上であると、成形品内部に気泡が含まれて強度不足になったり、表面近傍に筋状の模様が発生し外観不良が生じたりすることがある。
なお、上記200℃における加熱減量率は3質量%未満であることがより好ましい。
上記安定化助剤としては、重金属を含まないものを用いることができる。例として、有機酸塩、エポキシ化大豆油、エポキシ化アマニ豆油エポキシ化テトラヒドロフタレート、エポキシ化ポリブタジエン等のエポキシ化合物、有機リン化合物、亜リン酸エステル、リン酸エステル、水酸化カルシウム、水酸化ナトリウム等の金属水酸化物等が挙げられる。また、上記安定化助剤としては、アジピン酸ナトリウム、ビスフェノールA型エポキシ化合物、グリシジル(メタ)アクリレート共重合体、オキセタニル化合物、ビニルエーテル化合物及びゼオライト化合物が挙げられる。これらは単独で使用しても良く、2種以上を併用してもよい。なお、上記安定化助剤は、アルキルカルボン酸カルシウム及び亜鉛化合物とは異なるものである。
また、上記安定化助剤は、200℃における加熱減量率が5質量%未満であることが好ましい。
上記滑剤は、200℃における加熱減量率が5質量%未満であることが好ましい。
上記加工助剤は、200℃における加熱減量率が5質量%未満であることが好ましい。
上記耐熱向上剤としては特に限定されず、例えばα-メチルスチレン系、N-フェニルマレイミド系樹脂等が挙げられる。
上記光安定剤としては特に限定されず、例えば、ヒンダードアミン系等の光安定剤等が挙げられる。
上記顔料としては特に限定されず、例えば、アゾ系、フタロシアニン系、スレン系、染料レーキ系等の有機顔料;二酸化チタン等の酸化物系、硫化物・セレン化物系、フェロシアニン化物系などの無機顔料などが挙げられる。
これらの熱可塑性エラストマーは、単独で用いられてもよいし、2種類以上が併用されてもよい。
上記230℃における加熱減量率が2.0質量%以上であると、成形品内部に気泡が含まれることで強度不足になったり、表面近傍に筋状の模様が発生し外観不良が生じたりする。
上記230℃における加熱減量率は、1.0質量%未満であることがより好ましい。
下限については特に限定されないが0.1質量%が好ましい。
なお、上記230℃における加熱減量率は、熱重量測定(TG)装置によって測定することができる。
なお、上記塩素化する工程において、塩素化塩化ビニル系樹脂の一部を塩素化することで、塩素化塩化ビニル系樹脂と塩化ビニル系樹脂を併存させる状態としてもよい。
上記光エネルギーによる塩素化反応の場合、PVCが塩素化されるのに必要な光エネルギーの大きさは、PVCと光源との距離に大きく影響を受ける。そのため、PVC粒子の表面と内部とでは、受けるエネルギー量が相違し、塩素化が均一に生じない。その結果、均一性の低いCPVCが得られる。一方、紫外線照射を行わず、熱により塩素化する方法では、より均一な塩素化反応が可能となり、均一性の高いCPVCを得ることができる。
上記過酸化水素を添加する場合、塩素化速度が向上するため、加熱温度を比較的低くすることができる。例えば、65~110℃の範囲であってよい。
上記方法で塩素化を行うことにより、塩素化状態の不均一性が少なく、熱安定性の優れたCPVCを得ることができる。
上記熱安定剤及び酸化防止剤を混合する方法としては、特に限定されず、例えば、ホットブレンドによる方法、コールドブレンドによる方法等が挙げられる。
更に、本発明の他の側面によれば、本発明の射出成形用樹脂組成物から成形された成形体が提供される。このような成形体もまた本発明の1つである。
上記射出成形の方法としては、従来公知の任意の成形方法が採用されてよく、例えば、一般的な射出成形法、射出発泡成形法、超臨界射出発泡成形法、超高速射出成形法、射出圧縮成形法、ガスアシスト射出成形法、サンドイッチ成形法、サンドイッチ発泡成形法、インサート・アウトサート成形法等の方法が挙げられる。
また、本発明を用いることで、射出成形時の溶融性を大幅に改善して優れたプロセス特性を得ることができる。更に、本発明を用いることで、得られる成形品のヤケやシルバーストリーク等の不具合を効果的に防止することができる。加えて、ウェルドラインの発生を低減することで、外観不良、応力集中による強度低下を防止することができる。
(塩素化塩化ビニル樹脂の作製)
内容積300Lのグラスライニング製反応容器に、イオン交換水200kgと平均重合度700の塩化ビニル樹脂56kgを投入した。混合物を撹拌し、反応容器にさらに水を添加して、混合物を水中に分散させた。次いで、減圧して反応容器内の酸素を除去すると共に、90℃に昇温した。
次に、反応容器内に塩素を、塩素分圧が0.4MPaになるように供給し、0.2質量%過酸化水素を1時間当たり1質量部(320ppm/時間)の割合で添加しながら、塩素化反応を行った。塩素化された塩化ビニル樹脂の塩素含有量が67.3質量%になるまで反応を継続した。塩素化された塩化ビニル樹脂の塩素含有量が62.3質量%(5質量%手前)に達した時に、0.2質量%過酸化水素の添加量を1時間当たり0.1質量部(200ppm/時間)に減少し、平均塩素消費速度が0.012kg/PVC-kg・5minになるように調整して塩素化を進めた。さらに、塩素含有量が65.3質量%(3質量%手前)に達した時に、0.2質量%過酸化水素の添加量を1時間当たり150ppm/時間に減少し、平均塩素消費速度が0.008kg/PVC-kg・5minになるように調整して塩素化を進めた。このようにして、塩素含有量が67.3質量%の塩素化塩化ビニル樹脂を得た。なお、塩素含有量は、JIS K 7229に準拠して測定を行った。
得られた塩素化塩化ビニル樹脂(重合度:700)100質量部に対して、塩化ビニル樹脂(塩素含有量:56.7質量%、重合度:700)7質量部、熱安定剤4質量部、酸化防止剤0.5質量部を添加し混合した。なお、熱安定剤としては、ステアリン酸カルシウム2.0質量部と、ステアリン酸亜鉛2.0質量部を用いた。また、酸化防止剤としては、ペンタエリスリチル-テトラキス〔3-(3,5-ジ-t-ブチル-4-ヒドロキシフェニル)プロピオネート〕(ヒンダードフェノール系酸化防止剤、イルガノックス1010、BASF社製、200℃の加熱減量率1.0質量%)を用いた。
更に、衝撃改質剤5.0質量部、ポリエチレン系滑剤(三井化学社製、Hiwax220MP)2.0質量部、脂肪酸エステル系滑剤(エメリーオレオケミカルズジャパン社製、LOXIOL G-32)0.3質量部、二酸化チタン(石原産業社製、TIPAQUE CR-90)5.0質量部を添加した。なお、衝撃改質剤としては、MBS(メタクリルブタジエンスチレン)樹脂(カネカ社製、カネエース M-511)を用いた。その後、スーパーミキサーで均一に混合して、射出成形用樹脂組成物を得た。
得られた射出成形用樹脂組成物を、直径30mmの2軸異方向コニカル押出機(長田製作所社製「OSC-30」)に供給し、樹脂温度190℃でペレットを作製した。
得られたペレットを射出成形機(日新製鋼社製「J100E-C5」)に供給し、ノズルからパージした際の樹脂温度230℃で、呼び径25mmのソケット状射出成形体を作製した。
塩化ビニル樹脂の添加量を3質量部に変更した以外は、実施例1と同様に射出成形用樹脂組成物及び射出成形体を作製した。
塩化ビニル樹脂の添加量を25質量部に変更した以外は、実施例1と同様に射出成形用樹脂組成物及び射出成形体を作製した。
塩化ビニル樹脂を塩化ビニル樹脂(塩素含有量:56.7質量%、重合度:1000)に変更した以外は、実施例1と同様に塩素化塩化ビニル樹脂、射出成形用樹脂組成物及び押出成形体を作製した。
塩化ビニル樹脂の添加量を18質量部に変更した以外は、実施例1と同様に射出成形用樹脂組成物及び射出成形体を作製した。
塩素化塩化ビニル樹脂を塩素化塩化ビニル樹脂(塩素含有量:67.3質量%、重合度:600)に変更した以外は、実施例1と同様に射出成形用樹脂組成物及び押出成形体を作製した。
塩素化塩化ビニル樹脂を塩素化塩化ビニル樹脂(塩素含有量:67.3質量%、重合度:500)に変更した以外は、実施例1と同様に射出成形用樹脂組成物及び押出成形体を作製した。
塩化ビニル樹脂を塩化ビニル樹脂(塩素含有量:56.7質量%、重合度:500)に変更した以外は、実施例1と同様に塩素化塩化ビニル樹脂、射出成形用樹脂組成物及び押出成形体を作製した。
塩化ビニル樹脂を添加せず、熱安定剤をモンタン酸カルシウム2.0質量部と、ラウリン酸亜鉛2.0質量部に変更した以外は、実施例1と同様に射出成形用樹脂組成物及び押出成形体を作製した。
塩化ビニル樹脂の添加量を35質量部に変更した以外は、実施例1と同様に射出成形用樹脂組成物及び射出成形体を作製した。
塩化ビニル樹脂の種類、添加量を塩化ビニル樹脂(塩素含有量:56.7質量%、重合度:1300)7質量部に変更し、他の添加する成分を表1に記載のものに変更した以外は、実施例1と同様に射出成形用樹脂組成物及び押出成形体を作製した。
塩化ビニル樹脂の添加量を0.5質量部に変更し、他の添加する成分を表1に記載のものに変更した以外は、実施例1と同様に射出成形用樹脂組成物及び押出成形体を作製した。
実施例及び比較例で得られた射出成形用樹脂組成物及び成形体について以下の評価を行った。結果を表1に示した。
<静的熱安定性>
得られた塩素化塩化ビニル樹脂組成物を2本の8インチロールに供給し、205℃で3分間混練して、厚さ1.0mmのシートを作製した。得られたシートを200℃のギヤオーブン中で加熱し、発泡又は黒化するまでの時間(分)を測定した。
得られた塩素化塩化ビニル樹脂組成物をプラストミル(東洋精機社製「ラボプラストミル」)に供給し、回転数50rpm、195℃、充填量63gで混練し、ゲル化時間(秒)を測定した。混練開始から、混練トルクがピークになるまでの時間をゲル化時間とした。また、ゲル化後、更に混練及び加熱を続け、塩素化塩化ビニル樹脂の分解時間(分)を測定した。混練開始から、ゲル化後に安定した樹脂温度が再び上昇し始めるまでの時間を分解温度到達時間とした。
得られた塩素化塩化ビニル樹脂組成物を2本の8インチロールに供給し、205℃で3分間混練して、厚さ1.0mmのシートを作製した。得られたシートを重ね合わせて、205℃のプレスで3分間予熱した後、4分間加圧して、厚さ3mmのプレス板を得た。得られたプレス板から、機械加工により試験片を切り出した。この試験片を用いて、ASTM D638に準拠して引張強度及び引張弾性率を測定した。また、ASTM D648に準拠して負荷荷重186N/cm2で熱変形温度を測定した。尚、熱変形温度は、得られたプレス板を90℃のギヤオーブンで、24時間アニール処理した後測定した。
島津フローテスター(CFT-500D/100D、島津製作所社製)を用いて、フロー評価を行った。具体的には、<機械物性(引張強度、熱変形温度)>で作製したロールシートを約5mm角に切り出し、210℃に加熱したバレルに供給して、ダイ径1mm ダイ長さ10mmのキャピラリーにて荷重205kgfで押出した。その後、溶融樹脂が3mmキャピラリーから出た時点で測定を開始し、1mmあたり何秒かかったかを測定した。
測定値が0.2mm/sec以上の場合を「合格」とし、0.2mm/sec未満の場合を「不合格」として評価した。
<外観観察>
得られたソケット状射出成形体についても、気泡(発泡)の有無、シルバーストリークの有無、及びヤケ(変色)の有無を評価した。
また、得られたソケット状射出成形体について、ウェルド部分の深さをワンショット3D形状測定機(キーエンス社製、VR-3000)により測定した。
ASTM D1599の「耐水圧試験」に準拠した方法で、「合格」、「不合格」を判定した。

Claims (10)
- 塩素化塩化ビニル系樹脂と、塩化ビニル系樹脂と、熱安定剤とを含有する射出成形用樹脂組成物であって、
前記熱安定剤は、アルキルカルボン酸カルシウム及び亜鉛化合物を含有し、
前記塩化ビニル系樹脂は、重合度が400~1000であり、
前記塩素化塩化ビニル系樹脂100質量部に対して、塩化ビニル系樹脂を1~30質量部含有する
ことを特徴とする射出成形用樹脂組成物。 - 塩素化塩化ビニル系樹脂は、下記式(a)~(c)に示す構成単位(a)~(c)を有し、下記構成単位(a)、(b)及び(c)の合計モル数に対して、構成単位(a)の割合が17.5モル%以下、構成単位(b)の割合が46.0モル%以上、構成単位(c)の割合が37.0モル%以下であることを特徴とする請求項1記載の射出成形用樹脂組成物。
- 塩素化塩化ビニル系樹脂は、重合度が500~800であることを特徴とする請求項1又は2記載の射出成形用樹脂組成物。
- 塩素化塩化ビニル系樹脂中の塩素含有量は、63~72質量%であることを特徴とする請求項1、2又は3記載の射出成形用樹脂組成物。
- 塩素化塩化ビニル系樹脂と塩化ビニル系樹脂との重合度の差が500以下であることを特徴とする請求項1、2、3又は4記載の射出成形用樹脂組成物。
- 塩素化塩化ビニル系樹脂と塩化ビニル系樹脂の平均塩素含有量が65~68質量%であることを特徴とする請求項1、2、3、4又は5記載の射出成形用樹脂組成物。
- 塩素化塩化ビニル系樹脂100質量部に対して、熱安定剤を0.4~20質量部含有することを特徴とする請求項1、2、3、4、5又は6記載の射出成形用樹脂組成物。
- 更に、酸化防止剤を含有することを特徴とする請求項1、2、3、4、5、6又は7記載の射出成形用樹脂組成物。
- β-ジケトンを含まないことを特徴とする請求項1、2、3、4、5、6、7又は8記載の射出成形用樹脂組成物。
- 請求項1、2、3、4、5、6、7、8又は9記載の射出成形用樹脂組成物から成形されてなることを特徴とする成形体。
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201880025100.6A CN110520473B (zh) | 2017-09-27 | 2018-09-26 | 注塑成形用树脂组合物 |
| US16/637,000 US11692091B2 (en) | 2017-09-27 | 2018-09-26 | Resin composition for injection molding |
| EP18862125.4A EP3689963A4 (en) | 2017-09-27 | 2018-09-26 | Resin composition for injection molding |
| JP2018557434A JP6589069B2 (ja) | 2017-09-27 | 2018-09-26 | 射出成形用樹脂組成物 |
| KR1020197024454A KR102337920B1 (ko) | 2017-09-27 | 2018-09-26 | 사출 성형용 수지 조성물 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2017187164 | 2017-09-27 | ||
| JP2017-187164 | 2017-09-27 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2019065748A1 true WO2019065748A1 (ja) | 2019-04-04 |
Family
ID=65901934
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2018/035721 Ceased WO2019065748A1 (ja) | 2017-09-27 | 2018-09-26 | 射出成形用樹脂組成物 |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US11692091B2 (ja) |
| EP (1) | EP3689963A4 (ja) |
| JP (1) | JP6589069B2 (ja) |
| KR (1) | KR102337920B1 (ja) |
| CN (1) | CN110520473B (ja) |
| SA (1) | SA520411215B1 (ja) |
| TW (1) | TWI746889B (ja) |
| WO (1) | WO2019065748A1 (ja) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11912855B2 (en) * | 2019-03-29 | 2024-02-27 | Sekisui Chemical Co., Ltd. | Resin composition for molding |
| CN113667249A (zh) * | 2021-08-27 | 2021-11-19 | 山东高信化学股份有限公司 | 一种高强度耐高温氯化聚氯乙烯棒材及其制备方法 |
Citations (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH08127688A (ja) * | 1994-10-28 | 1996-05-21 | Yazaki Corp | 高難燃性塩化ビニル樹脂組成物 |
| JP2000086732A (ja) * | 1998-09-17 | 2000-03-28 | Kureha Chem Ind Co Ltd | 耐衝撃強化剤およびこれを含む耐衝撃性および成形性に優れる塩化ビニル系樹脂組成物 |
| JP2002226659A (ja) * | 2001-02-01 | 2002-08-14 | Takiron Co Ltd | 難燃性塩化ビニル系樹脂成形体 |
| JP2003292712A (ja) * | 2002-04-01 | 2003-10-15 | Mitsubishi Plastics Ind Ltd | 塩素化塩化ビニル系樹脂組成物およびそれを押出成形してなる成形品 |
| JP2004099697A (ja) * | 2002-09-06 | 2004-04-02 | Sekisui Chem Co Ltd | 更生管用塩素化塩化ビニル系樹脂組成物及び更生管 |
| JP2004231718A (ja) * | 2003-01-29 | 2004-08-19 | Tokuyama Sekisui Ind Corp | 繊維用塩化ビニル系樹脂組成物 |
| WO2008018521A1 (en) * | 2006-08-08 | 2008-02-14 | Mitsubishi Plastics, Inc. | Transparent flame-retardant vinyl chloride resin composition and molded body |
| JP2008535997A (ja) | 2005-04-15 | 2008-09-04 | サン エース カコー (ピーティーイー.) リミテッド | ハロゲン化物含有ポリマーのための安定剤組成物 |
| JP2008214466A (ja) | 2007-03-02 | 2008-09-18 | Kaisui Kagaku Kenkyusho:Kk | 安定化された含ハロゲン樹脂組成物 |
| JP2010265365A (ja) * | 2009-05-13 | 2010-11-25 | Sekisui Chem Co Ltd | 塩化ビニル系樹脂成形体 |
| WO2012160943A1 (ja) * | 2011-05-20 | 2012-11-29 | 株式会社Adeka | 射出成形用塩化ビニル系樹脂組成物 |
| WO2013080563A1 (ja) * | 2011-11-29 | 2013-06-06 | 徳山積水工業株式会社 | 押出成形用塩素化塩化ビニル樹脂組成物 |
| WO2016013638A1 (ja) | 2014-07-24 | 2016-01-28 | 積水化学工業株式会社 | 成形用樹脂組成物 |
Family Cites Families (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2661182B1 (fr) | 1990-04-20 | 1992-07-03 | Rhone Poulenc Chimie | Compositions stabilisees de polymere halogene. |
| JPH06287388A (ja) | 1993-04-01 | 1994-10-11 | Sekisui Chem Co Ltd | 塩化ビニル系樹脂組成物 |
| JPH10296821A (ja) | 1997-04-25 | 1998-11-10 | Sekisui Chem Co Ltd | スプリンクラー配管用塩素化塩化ビニル樹脂管 |
| JPH1112420A (ja) | 1997-06-23 | 1999-01-19 | Sekisui Chem Co Ltd | 塩化ビニル系樹脂組成物 |
| JP2002138179A (ja) | 2000-10-31 | 2002-05-14 | Nippon Zeon Co Ltd | 塩化ビニル樹脂組成物及びそれを用いた成形品 |
| JP2002254576A (ja) | 2001-02-28 | 2002-09-11 | Mitsubishi Plastics Ind Ltd | 塩化ビニル樹脂パイプ |
| JP2002273790A (ja) | 2001-03-15 | 2002-09-25 | Sekisui Chem Co Ltd | 耐熱性塩化ビニル樹脂管の製造方法、並びに、耐熱性塩化ビニル樹脂成形体 |
| JP2003097768A (ja) | 2001-09-21 | 2003-04-03 | Sekisui Chem Co Ltd | 更生管用塩化ビニル系樹脂組成物及び更生管 |
| JP2005028756A (ja) | 2003-07-14 | 2005-02-03 | Green Techno Japan Hanbai Kk | 人工木材の製造方法および人工木材用組成物粉体並びにペレット |
| EP1877481B1 (en) | 2005-04-15 | 2016-02-17 | Sun Ace Kakoh (Pte.) Ltd. | Stabiliser composition for halide-containing polymers |
| JP4901130B2 (ja) | 2005-05-25 | 2012-03-21 | 積水化学工業株式会社 | 塩素化塩化ビニル系樹脂の製造方法 |
| CN103102631B (zh) | 2012-02-09 | 2015-11-04 | 芜湖特贝特材料科技有限公司 | 基于超临界co2挤出发泡的cpvc/pvc耐热复合材料及制备方法 |
| CN103665684B (zh) | 2012-09-19 | 2015-10-21 | 中国石油化工股份有限公司 | 注塑用高流动性cpvc组合物 |
| JP2014224176A (ja) | 2013-05-15 | 2014-12-04 | 積水化学工業株式会社 | 熱塩素化塩化ビニル系樹脂組成物および成形体 |
| KR102188216B1 (ko) | 2013-09-27 | 2020-12-08 | 세키스이가가쿠 고교가부시키가이샤 | 염소화 염화비닐계 수지를 함유하는 성형용 수지 조성물 및 그 성형체 |
| JP6263128B2 (ja) | 2013-09-27 | 2018-01-17 | 積水化学工業株式会社 | 塩素化塩化ビニル系樹脂を含む成形用樹脂組成物及びその成形体 |
| CN106147092A (zh) * | 2015-03-31 | 2016-11-23 | 安徽华润仪表线缆有限公司 | 一种电力电缆用耐热氯化聚氯乙烯材料 |
| CN105968642A (zh) * | 2016-06-17 | 2016-09-28 | 顾地科技股份有限公司 | 高抗冲高强度的电力管材 |
| CN106432994B (zh) * | 2016-10-31 | 2019-08-30 | 成都脉通管业有限公司 | 一种增韧电力电缆cv环保管及其制备方法 |
| CN107177147A (zh) * | 2017-06-05 | 2017-09-19 | 潍坊高信新材料有限公司 | 一种高维卡、耐腐蚀、高强度cpvc板材及其制备方法 |
-
2018
- 2018-09-26 WO PCT/JP2018/035721 patent/WO2019065748A1/ja not_active Ceased
- 2018-09-26 EP EP18862125.4A patent/EP3689963A4/en not_active Ceased
- 2018-09-26 US US16/637,000 patent/US11692091B2/en active Active
- 2018-09-26 CN CN201880025100.6A patent/CN110520473B/zh active Active
- 2018-09-26 KR KR1020197024454A patent/KR102337920B1/ko active Active
- 2018-09-26 JP JP2018557434A patent/JP6589069B2/ja active Active
- 2018-09-27 TW TW107134046A patent/TWI746889B/zh active
-
2020
- 2020-01-31 SA SA520411215A patent/SA520411215B1/ar unknown
Patent Citations (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH08127688A (ja) * | 1994-10-28 | 1996-05-21 | Yazaki Corp | 高難燃性塩化ビニル樹脂組成物 |
| JP2000086732A (ja) * | 1998-09-17 | 2000-03-28 | Kureha Chem Ind Co Ltd | 耐衝撃強化剤およびこれを含む耐衝撃性および成形性に優れる塩化ビニル系樹脂組成物 |
| JP2002226659A (ja) * | 2001-02-01 | 2002-08-14 | Takiron Co Ltd | 難燃性塩化ビニル系樹脂成形体 |
| JP2003292712A (ja) * | 2002-04-01 | 2003-10-15 | Mitsubishi Plastics Ind Ltd | 塩素化塩化ビニル系樹脂組成物およびそれを押出成形してなる成形品 |
| JP2004099697A (ja) * | 2002-09-06 | 2004-04-02 | Sekisui Chem Co Ltd | 更生管用塩素化塩化ビニル系樹脂組成物及び更生管 |
| JP2004231718A (ja) * | 2003-01-29 | 2004-08-19 | Tokuyama Sekisui Ind Corp | 繊維用塩化ビニル系樹脂組成物 |
| JP2008535997A (ja) | 2005-04-15 | 2008-09-04 | サン エース カコー (ピーティーイー.) リミテッド | ハロゲン化物含有ポリマーのための安定剤組成物 |
| WO2008018521A1 (en) * | 2006-08-08 | 2008-02-14 | Mitsubishi Plastics, Inc. | Transparent flame-retardant vinyl chloride resin composition and molded body |
| JP2008214466A (ja) | 2007-03-02 | 2008-09-18 | Kaisui Kagaku Kenkyusho:Kk | 安定化された含ハロゲン樹脂組成物 |
| JP2010265365A (ja) * | 2009-05-13 | 2010-11-25 | Sekisui Chem Co Ltd | 塩化ビニル系樹脂成形体 |
| WO2012160943A1 (ja) * | 2011-05-20 | 2012-11-29 | 株式会社Adeka | 射出成形用塩化ビニル系樹脂組成物 |
| WO2013080563A1 (ja) * | 2011-11-29 | 2013-06-06 | 徳山積水工業株式会社 | 押出成形用塩素化塩化ビニル樹脂組成物 |
| WO2016013638A1 (ja) | 2014-07-24 | 2016-01-28 | 積水化学工業株式会社 | 成形用樹脂組成物 |
Non-Patent Citations (2)
| Title |
|---|
| R. A. KOMOROSKIR. G. PARKERJ. P. SHOCKER, MACROMOLECULES, vol. 18, 1985, pages 1257 - 1265 |
| See also references of EP3689963A4 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP3689963A4 (en) | 2021-06-16 |
| EP3689963A1 (en) | 2020-08-05 |
| US11692091B2 (en) | 2023-07-04 |
| KR102337920B1 (ko) | 2021-12-09 |
| CN110520473B (zh) | 2022-11-04 |
| US20200199342A1 (en) | 2020-06-25 |
| SA520411215B1 (ar) | 2023-10-22 |
| KR20200056955A (ko) | 2020-05-25 |
| CN110520473A (zh) | 2019-11-29 |
| TW201920436A (zh) | 2019-06-01 |
| TWI746889B (zh) | 2021-11-21 |
| JPWO2019065748A1 (ja) | 2019-11-14 |
| JP6589069B2 (ja) | 2019-10-09 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6532875B2 (ja) | 成形用樹脂組成物 | |
| TWI651354B (zh) | 含有氯化氯乙烯系樹脂之成形用樹脂組成物及其成形體 | |
| TWI651353B (zh) | 含有氯化氯乙烯系樹脂之成形用樹脂組成物及其成形體 | |
| KR102578301B1 (ko) | 성형용 수지 조성물 | |
| JP6589069B2 (ja) | 射出成形用樹脂組成物 | |
| US11174381B2 (en) | Resin composition for molding |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| ENP | Entry into the national phase |
Ref document number: 2018557434 Country of ref document: JP Kind code of ref document: A |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 18862125 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2018862125 Country of ref document: EP Effective date: 20200428 |
|
| WWW | Wipo information: withdrawn in national office |
Ref document number: 2018862125 Country of ref document: EP |